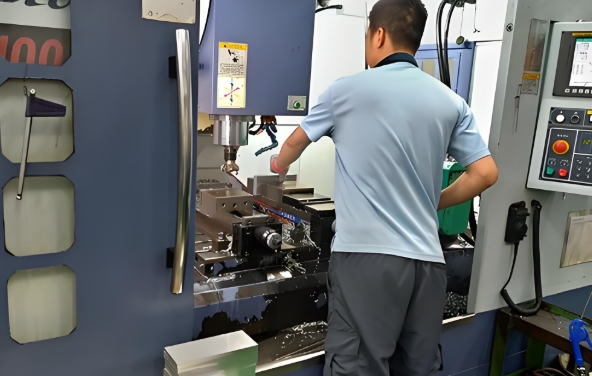
Is Milling or Turning Harder?
A practical CNC process guide comparing milling and turning by geometry, programming, setups, tolerance, cost and production requirements — so you can specify the process that fits your part.
- Shafts, pins, bushings, fittings
- OD / ID, threads, faces, grooves
- Housings, brackets, manifolds, plates
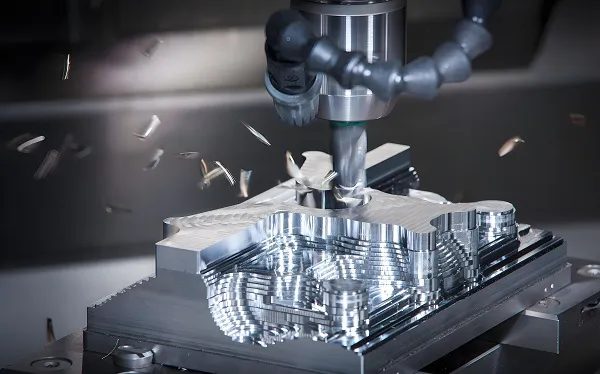
- Pockets, slots, holes, 3D contours
Quick Answer: Is Milling Harder Than Turning?
Neither CNC milling nor CNC turning is universally harder. Turning is generally simpler for rotational parts such as shafts, pins and bushings. Milling becomes more demanding when parts require multiple faces, complex 3D surfaces, difficult tool access or multi-axis tool motion. For production, the right process is the one that achieves the required geometry and tolerance with the fewest setups and lowest overall manufacturing risk.
Requirement vs Process — At a Glance
| Requirement | Turning | Milling |
|---|---|---|
| Simple cylindrical part | ★★★★★★★ | ★★★★★★★ |
| Shaft / pin / bushing | ★★★★★★★ | ★★★★★★★ |
| Flat faces | ★★★★★★★ | ★★★★★★★ |
| Pockets / slots | ★★★★★★★ | ★★★★★★★ |
| Multiple side features | ★★★★★★★ | ★★★★★★★ |
| Complex 3D surfaces | ★★★★★★★ | ★★★★★★★ |
| Concentricity | ★★★★★★★★ | ★★★★★★★★ |
| Multi-face machining | ★★★★★★★ | ★★★★★★★ |
| Programming complexity | Lower for simple parts | Higher for complex parts |
| Best combined solution | Mill-turn | |
Relative comparison for typical part geometries; actual difficulty depends on part design, material, tolerance and machine/process requirements.
What Does "Harder to Machine" Actually Mean?
"Harder" is not simply about which machine has more axes. Difficulty is the sum of seven factors — and each one affects your cost and lead time differently.
Process Planning
How complex the manufacturing route is — how many operations, tool changes and sequences the part needs.
Programming
Toolpaths, coordinates and tool orientations. Milling of 3D geometry is usually more programming-intensive than simple turning.
Setup
How many setups and datum transfers the part requires. Each setup adds time and tolerance risk.
Tool Access
Whether the tool can physically reach the critical feature — deep pockets, undercuts and angled features matter here.
Tolerance Control
How strictly dimensions and position relationships must be held, and how stable the process is at that level.
Material
Hardness, work hardening, heat and chip behavior. Material can matter more than the machine type.
Inspection
Whether the final geometry is easy to measure and verify against the drawing.
CNC Milling vs Turning at a Glance
Both are subtractive CNC processes. The difference is which part moves — and the shapes each process is best at.
| CNC Turning | CNC Milling | |
|---|---|---|
| Part shape | Rotational — shafts, discs, sleeves, bushings | Prismatic — plates, housings, brackets, pockets |
| Main motion | Workpiece rotates, tool feeds | Tool rotates, workpiece feeds |
| Typical features | Cylinders, tapers, bores, threads, faces | Planes, slots, pockets, holes, 3D surfaces |
| Setup complexity | Lower for simple rotary parts | Higher for multi-axis and complex geometry |
| Programming | Simpler for regular rotary shapes | More demanding for 3D surfaces and toolpaths |
| Best suited to | Pins, rollers, valve stems, threaded parts | Brackets, enclosures, manifolds, molds |
Geometry Is the First Process-Selection Decision
Before comparing machines, look at the dominant geometry of your part. This is the first question our engineers ask on every RFQ.
Choose Turning When
- Primary shape is cylindrical
- Features are concentric
- OD / ID dominates
- Threads dominate
- Grooves and tapers
- Shafts, bushings, pins
Choose Milling When
- Flat surfaces dominate
- Pockets and slots
- Side holes and bosses
- Non-round profiles
- 3D contours
- Multiple faces
What About Parts That Need Both Turning and Milling?
Many parts are neither purely rotational nor purely prismatic. When a part combines a round body with milled features, the answer is not "milling or turning" — it is a combined route.
Mill-Turn Route
When Is CNC Turning Easier — and When Is It More Difficult?
Turning Is Usually Easier When
- The part is a simple rotational shape
- Features are concentric on the spindle axis
- The part can be finished in one setup
- Standard OD, ID, thread and face work dominates
Turning Becomes More Difficult When
- Slender shafts — deflection and vibration risk
- Deep bores — tool overhang and chip evacuation
- Tight concentricity between features
- Complex or multi-start threads
- Thin-wall rotational parts — deformation risk
- Difficult materials that work-harden or wear tools
When Is CNC Milling More Complex?
Milling is not always harder — but it becomes more complex for five common reasons.
Multiple Tool Orientations
The tool must reach features from different directions, which adds planning and sometimes multi-axis motion.
Multiple Faces
Features on several faces mean more setups or more complex workholding to keep datum relationships.
More Toolpath Decisions
Climb vs conventional, stepover, entry and exit, tool selection — each decision affects finish and accuracy.
More Potential Setups
Each setup transfers datum and adds tolerance risk and handling time.
3D / Multi-Axis Motion
Complex 3D surfaces push milling toward 4-axis or 5-axis machining, where axis coordination is critical.
Programming Difficulty: Milling vs Turning
For simple parts, both can be straightforward. Milling generally becomes more programming-intensive as tool access, 3D geometry, multiple faces and multi-axis motion increase. Turning can also become complex for advanced contours, live tooling, sub-spindle operations and mill-turn parts.
You do not need to learn CNC programming to order parts — but it helps to know that complex geometry is where programming time, and therefore engineering cost, rises.
Setup Complexity and Datum Control
The harder process is often the one that requires more setups and datum transfers — not simply the one with the more complicated machine.
Turning — often 1 setup
One datum, one clamping — strong for concentric features.
Milling — often multiple setups
Each setup transfers the datum; more setups mean more risk to position accuracy.
Tool Access and Part Geometry
Whether a feature is reachable often decides the process. Deep pockets, undercuts and angled features can force a more capable machine.
3-Axis — fixed tool axis
Tool approaches from a fixed vertical direction; features must be reachable from that orientation.
5-Axis — changing tool axis
The tool axis can tilt, so difficult-to-reach features and angled surfaces can be machined in fewer setups.
Milling vs Turning for Tight Tolerances
Neither process is "more accurate" in general. Accuracy depends on which feature you are holding.
| Requirement | Turning | Milling |
|---|---|---|
| Diameter tolerance | Excellent | Usually less efficient |
| Concentricity | Excellent for same-setup features | More setup-dependent |
| Flatness | Limited role | Excellent |
| Hole position | Limited | Excellent |
| Multi-face relationship | Limited | Excellent |
| Complex GD&T | Depends on geometry | Depends on setup / machine |
Milling vs Turning Surface Finish
Turning
Rotational surfaces can be finished directly with a single-point tool; finish is governed by feed and tool geometry. Excellent for cylindrical and tapered surfaces.
Milling
Milled surface finish depends on stepover, toolpath and tool condition. Good finishes are routine, and Ra 0.4 μm is achievable on qualified features.*
* Confirm finish targets and inspection method with our engineers on your drawing. See CNC Surface Finishing.
How Material Changes Milling vs Turning Difficulty
| Material | Turning consideration | Milling consideration |
|---|---|---|
| Aluminum | Generally easy | Generally easy |
| 303 SS | Good machinability | Good |
| 316L | Work hardening | Heat + tool wear |
| Titanium | Heat / tool wear | Heat / tool engagement |
| Inconel | High cutting difficulty | High cutting difficulty |
| PEEK | Thermal / deformation | Thermal / deformation |
| CF-PEEK | Abrasive | Abrasive |
Which Is More Expensive: Milling or Turning?
It depends primarily on part geometry, setup count, material removal, tooling, cycle time and production volume. Simple round parts tend to be cheaper to turn. Complex prismatic parts are typically milled. Parts with both round and milled features may be cheaper as mill-turn.
| Part type | Likely cost advantage |
|---|---|
| Simple shaft | Turning |
| Simple plate | Milling |
| Bushing | Turning |
| Housing | Milling |
| Shaft + cross holes | Mill-turn |
| Complex impeller | 5-Axis |
| High-volume round component | Turning / Swiss / mill-turn |
Milling vs Turning Lead Time — Which Is Faster?
Turning
Often faster for simple rotational parts because the part can be completed in one setup — clamping, machining and inspection on a single reference.
Milling
May be faster overall for a complex part if it eliminates multiple secondary operations that a different route would need.
Which CNC Process Should You Use?
A quick reference for common part families.
| Part | Recommended process |
|---|---|
| Shaft | CNC Turning |
| Pin | CNC Turning |
| Bushing | CNC Turning |
| Spacer | CNC Turning |
| Fitting | Turning / Mill-Turn |
| Bracket | CNC Milling |
| Housing | CNC Milling |
| Manifold | CNC Milling |
| Plate | CNC Milling |
| Impeller | 5-Axis Milling |
| Turbine blade | 5-Axis Milling |
| Shaft + cross holes | Mill-Turn |
| Connector pin | Swiss Turning |
Milling or Turning? Use This Decision Tree
You Don't Have to Choose the Machine Yourself
As a buyer, you usually do not need to specify whether a part must be milled or turned. Provide the drawing, material, quantity and functional requirements. A capable supplier should evaluate the geometry and recommend the manufacturing route.
You say "I need this part made" — not "Please mill this part". That is exactly how we review every RFQ.
CNC Milling and Turning at Goldcattle
Example Machine Fleet
* Machine models are examples for illustration; confirm against the current machine fleet before publishing.
Real CNC Milling and Turning Examples
How geometry decides the route — typical selections, shown for illustration.
Simple Shaft
- Material: 316L
- Process: CNC Turning
- Why: Rotational geometry + concentric diameter requirements
Aluminum Housing
- Material: 6061-T6
- Process: CNC Milling
- Why: Multiple faces + pockets + threaded holes
Shaft With Cross Holes
- Material: 17-4PH
- Process: Turning + Live Tooling
- Why: Round main body + off-axis milled features
Inconel 718 Impeller
- Process: Simultaneous 5-Axis
- Why: Complex blade surfaces + tool orientation
Illustrative route-selection examples. See CNC machining precision titanium parts and how to CNC machine turbine blades.
Relative Process Complexity
A qualitative ladder — not a universal ranking.
This is a qualitative guide, not a universal ranking. Material, tolerance, part size and production volume can change the actual process difficulty.
What to Include in Your CNC RFQ
- 2D drawing or 3D STEP file (with GD&T if available)
- Material and grade
- Quantity and target lead time
- Critical tolerance and surface-finish requirements
- Inspection and documentation needs (material certificates, dimensional report)
Milling vs Turning — Frequently Asked Questions
Is milling harder than turning?
Neither is universally harder. Turning is usually simpler for parts whose primary geometry is rotational. Milling becomes more complex when a part needs multiple faces, 3D surfaces, difficult tool access or multi-axis motion. Difficulty depends on the part, material, tolerance and required production volume.
Is CNC milling harder to program than CNC turning?
For simple parts, both are straightforward. Milling becomes more programming-intensive as tool access, 3D geometry, multiple faces and multi-axis motion increase. Turning can also become complex for advanced contours, live tooling, sub-spindle and mill-turn parts.
Is CNC turning easier than milling?
For simple rotational parts such as shafts, pins and bushings, turning is often easier because the part can be completed in one setup. For parts with flat faces, pockets or 3D contours, milling is usually the more appropriate process.
Which process is better for shafts?
CNC turning is normally the better choice for shafts because the workpiece rotates around the spindle axis, which naturally supports diameter, roundness and concentricity requirements.
Which process is better for housings?
CNC milling is usually better for housings, because they typically have flat faces, pockets, holes and positional relationships across multiple planes.
Which process is more accurate?
Accuracy depends on the feature. Turning has a natural advantage for many diameter, roundness and concentricity requirements. Milling is strong for positional relationships across multiple planes and for flatness. The right question is which process holds your critical features best with the fewest setups.
Which process is cheaper?
Cost depends on geometry, setup count, material removal, tooling, cycle time and volume. Simple round parts are often cheaper to turn; complex prismatic parts are typically milled; parts with both cylindrical and milled features may be cheaper as mill-turn.
Which process is faster?
Turning is often faster for simple rotational parts because it can be completed in one setup. Milling may be faster overall for a complex part if it eliminates multiple secondary operations. Total manufacturing time matters more than machine cycle time.
What is harder to machine, milling or turning?
There is no universal answer. Simple rotational parts are usually easier to turn; parts with multiple faces, 3D surfaces, difficult tool access or multi-axis motion are usually more demanding to mill. Material, tolerance and part size can change the difficulty more than the machine type.
When should I use mill-turn machining?
Use mill-turn when a part combines a rotational body with milled features — for example a shaft with flats, cross holes, slots or off-axis features. Live-tool turning or turn-then-mill keeps these features in fewer setups.
Can a CNC lathe also perform milling?
Yes. Many CNC lathes with live tooling can perform milling operations such as flats, slots and cross holes without moving the part to a separate machine.
What is live-tool turning?
Live-tool turning is turning on a lathe equipped with driven (motorized) tools. The lathe spindle can be indexed or controlled to allow milling features such as flats, slots and cross holes to be machined in the same setup as the turned features.
Can 5-axis CNC replace turning?
Not generally. 5-axis milling is excellent for complex prismatic parts and sculpted surfaces, but for pure rotational parts with diameters and threads, turning remains more efficient. For parts needing both, a combined turn-mill or multi-axis route is often the best answer.
What parts are best for CNC turning?
Shafts, pins, bushings, spacers, rollers, valve stems, fittings, threaded components and other rotationally symmetric parts are best suited to CNC turning.
What parts are best for CNC milling?
Brackets, housings, manifolds, plates, enclosures, molds and parts with pockets, slots, holes or complex 3D contours are best suited to CNC milling.
Does material affect whether milling or turning is harder?
Yes, often more than the machine type. Difficult materials such as titanium, Inconel and 316L can make otherwise simple work demanding, while easy materials such as aluminum can keep complex geometry manageable.
Which process is better for tight tolerances?
Turning is naturally strong for diameter, roundness and concentricity on rotational parts. Milling is strong for positional relationships across multiple planes and for flatness. The best process is the one that holds your critical features with the fewest setups and datum transfers.
Which process is better for high-volume production?
For high volumes of simple round parts, turning (including Swiss-type turning) is very efficient. For high volumes of prismatic parts, a machining center with optimized fixtures and automation is usually the better route.
How do I choose between CNC milling and turning?
Start with the dominant geometry: rotationally symmetric parts suit turning, parts with flat faces, pockets or 3D contours suit milling, and parts with both suit mill-turn. When in doubt, send the drawing — a capable supplier should recommend the manufacturing route.
Related Guides
Choose this page as your starting point, then follow the process that fits your geometry.
Not Sure Whether Your Part Should Be Milled or Turned?
Send us your 2D drawing or STEP file. We will review the geometry, critical features, tolerance, quantity and material, then recommend the most suitable machining route — before production.