2D, 3D & CNC Toolpath Guide
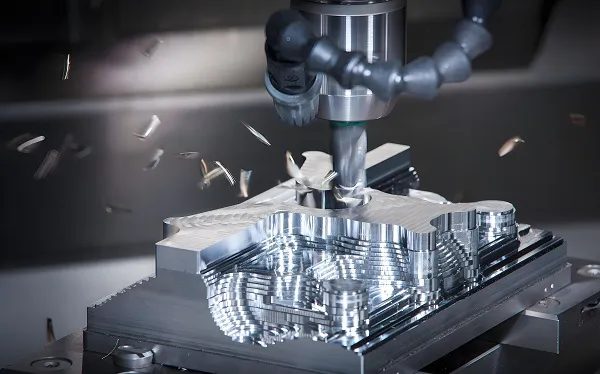
Contour milling is a CNC machining strategy in which the cutting tool follows a defined boundary, wall or surface path to create the required part profile. Depending on the geometry and CAM system, contouring can be performed as 2D profile machining, 3D Z-level contour finishing, or multi-axis contouring.
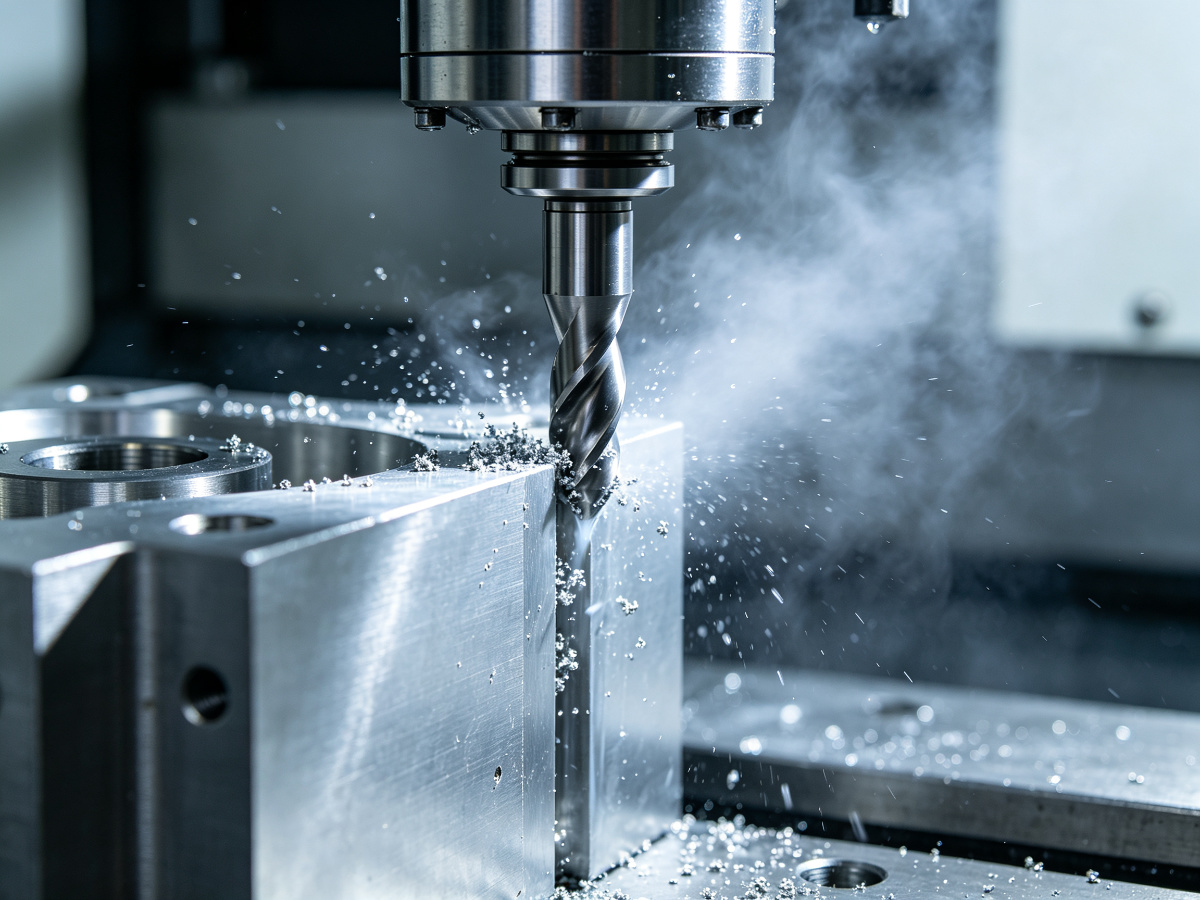
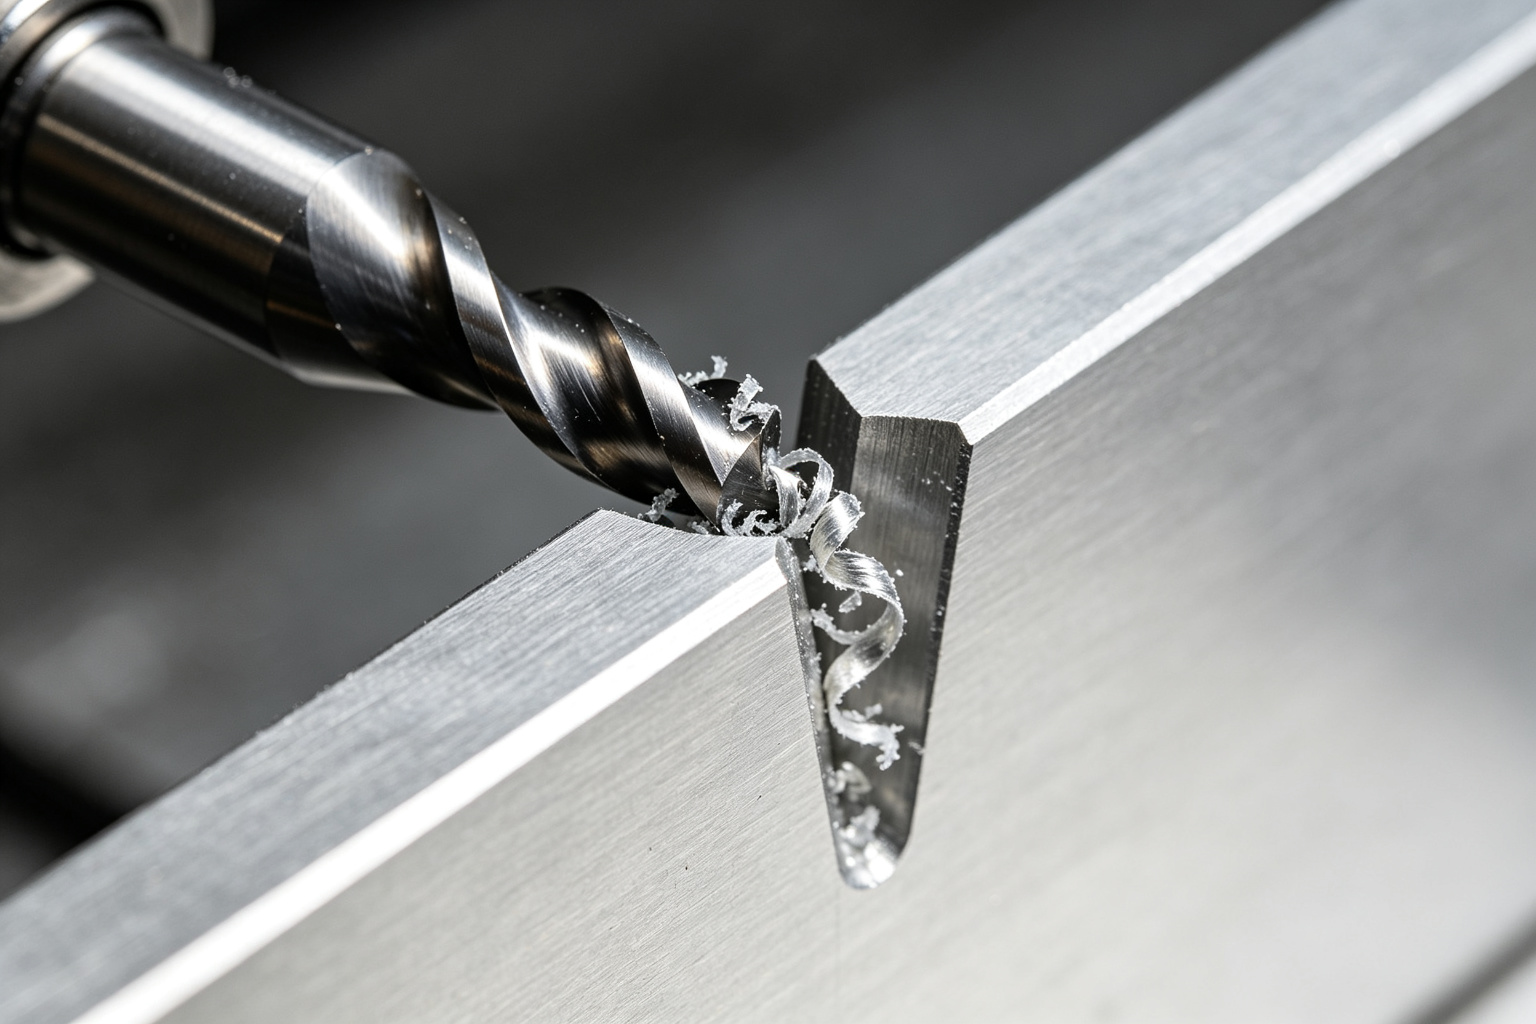
The cutter follows the part profile; the programmed centerline controls every pass.
| Type | Geometry | Main motion | Typical role |
|---|---|---|---|
| 2D Contour | Defined 2D boundary / wall | Mainly XY at fixed Z depths | External profiles, internal walls, finish passes |
| 3D Contour | Steep 3D geometry | Z-level contour paths | Steep walls, mold surfaces, near-vertical areas |
| Multi-Axis Contour | Complex / hard-to-reach surfaces | Linear + rotary / tool-axis movement | Complex surfaces, collision avoidance, undercuts |
Irregular brackets, plates, covers and housings with shaped outlines.
Cavity walls, openings and shaped pockets with defined boundaries.
Mold walls, inclined structures and deep curved surfaces.
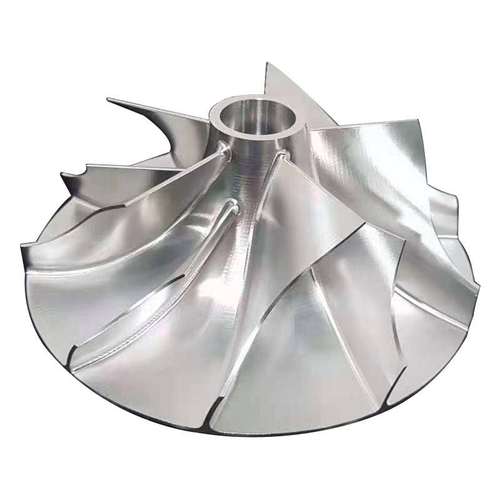
Blades, impellers and complex molds with changing surface normals.
| Operation | Main objective | Typical geometry |
|---|---|---|
| Contour | Follow a boundary or wall | Profiles, walls, shaped edges |
| Remove material inside a boundary | Cavities, enclosed areas | |
| Face milling | Produce a flat plane | Top / datum surfaces |
| Adaptive clearing | Efficient bulk material removal | Roughing, varied stock |
| 3D contour | Finish steep 3D walls | Mold / shaped surfaces |
Tool deflection, cutter wear, incorrect compensation or workpiece movement during cutting.
Tool deflection, long tool overhang, unstable workholding or unequal cutting engagement.
Poor rigidity, excessive radial engagement, long tool or insufficient support.
Abrupt direction changes, unsuitable minimum cutting radius or changing cutter engagement.
Excessive stepdown, insufficient finishing strategy or unsuitable tool orientation.
Cutting force exceeds the wall's stiffness; the wall deflects during the pass.
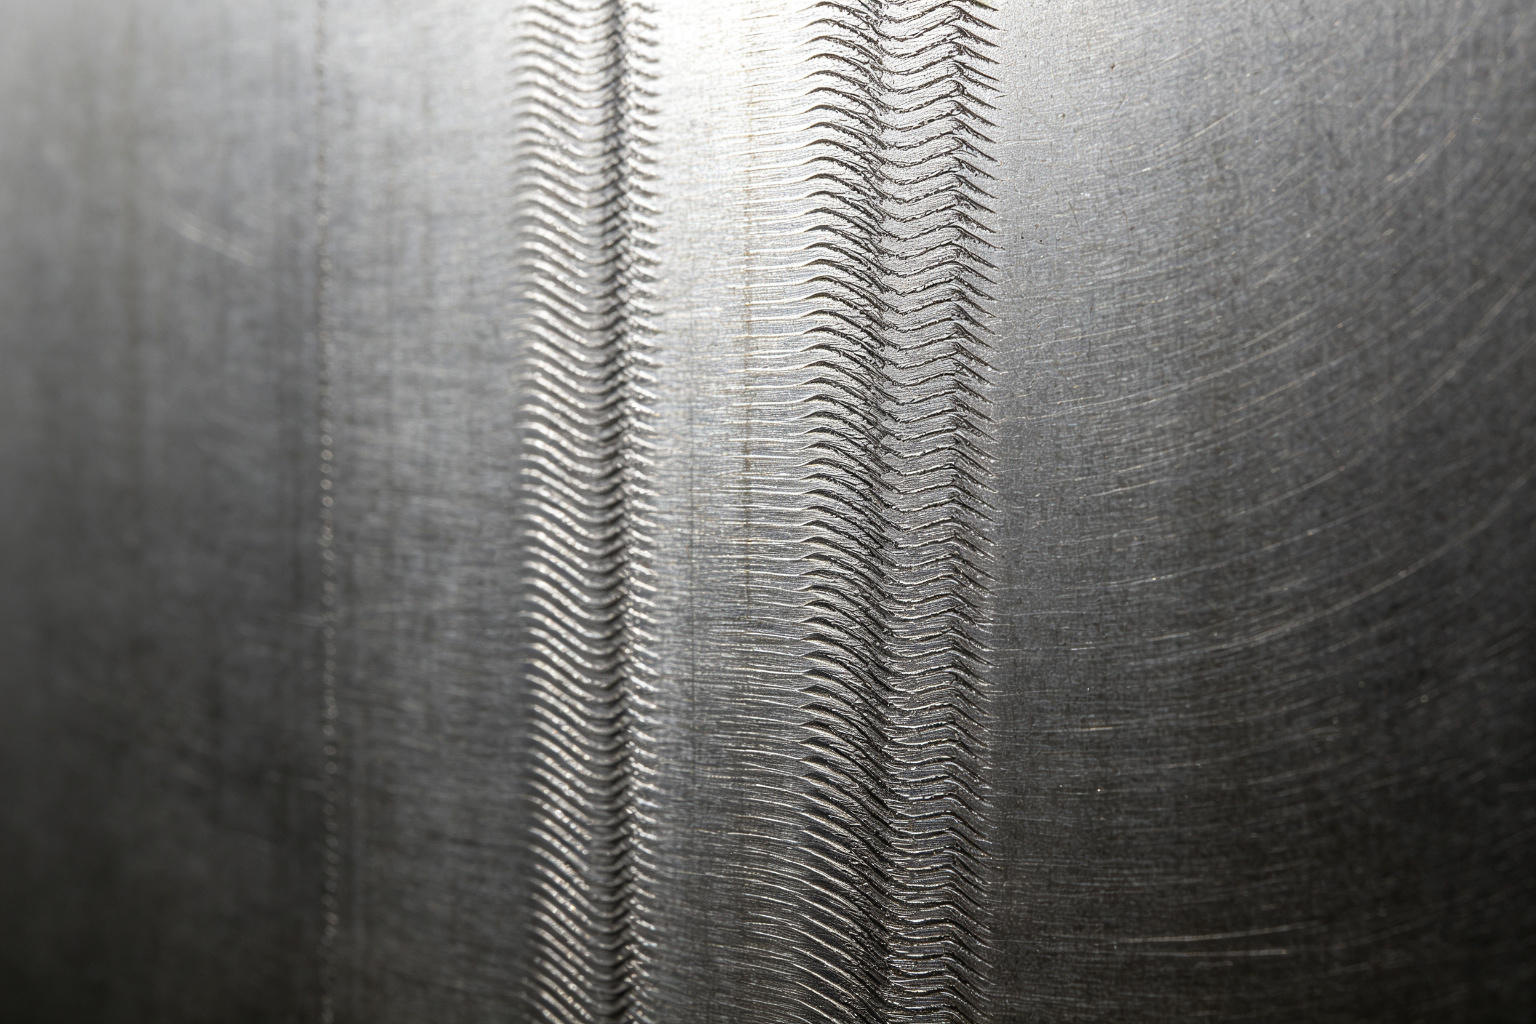
Visible waviness across a wall usually points to chatter from weak rigidity or excessive engagement — not a bad toolpath alone.
| Symptom | Likely cause | First engineering check |
|---|---|---|
| Profile undersize | Tool deflection / wear | Tool condition + radial load |
| Profile oversize | Compensation / tool size | Tool offset and diameter |
| Wall taper | Deflection / workholding | Tool overhang + fixture |
| Chatter | Rigidity / engagement | Tool + fixture rigidity |
| Burrs | Tool condition / cutting direction | Tool geometry + climb direction |
| Corner marks | Path transition | Toolpath smoothing / radius |
| Visible Z-banding | Excessive stepdown | Stepdown + finishing strategy |
| Holder collision | Poor clearance | Tool orientation / holder simulation |
There is no universal feed, speed or depth table for contour milling. These five variables control the result on every job.
Sets minimum reachable radius, stiffness and access.
Longer overhang increases deflection risk.
Controls cutting load, wall quality and cycle time.
Drives cutting force, chatter and tool life.
Controls geometric approximation and surface fidelity.
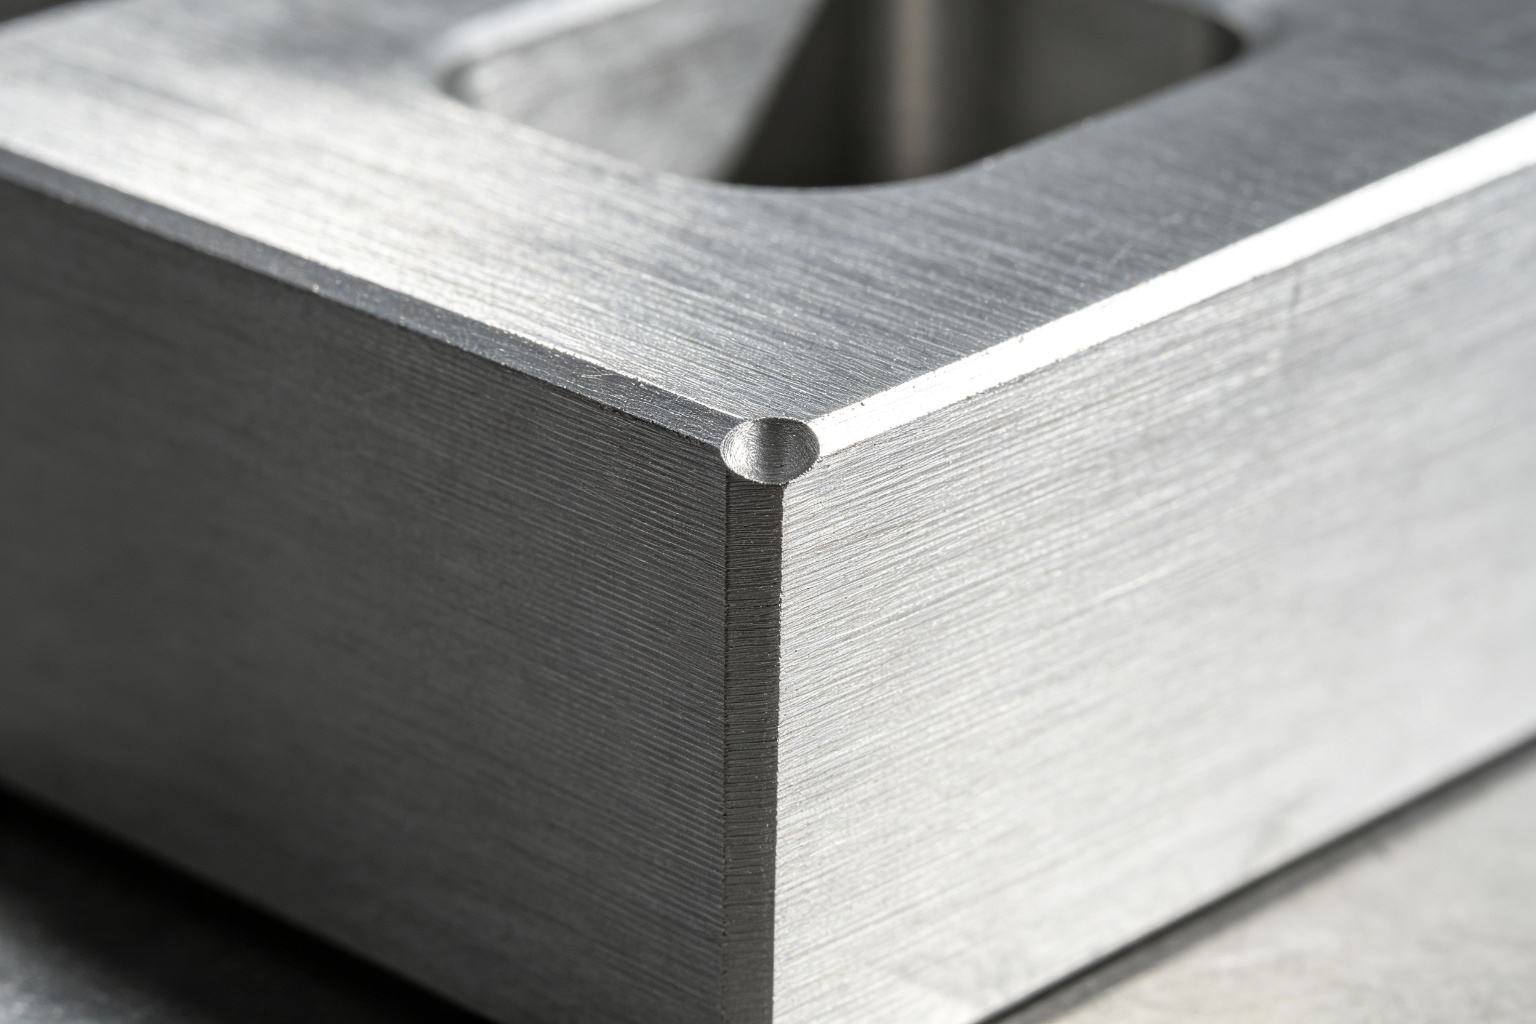
A round cutting tool leaves a radius at an internal corner. The smaller the cutter, the smaller the achievable radius — but smaller cutters are generally less rigid and can increase machining time or deflection risk.
If the drawing calls for a sharp internal corner, the machined part will show a radius; specify the smallest acceptable radius or plan a secondary operation.
External and internal profiles, straight walls, simple curved boundaries and stepped depths.
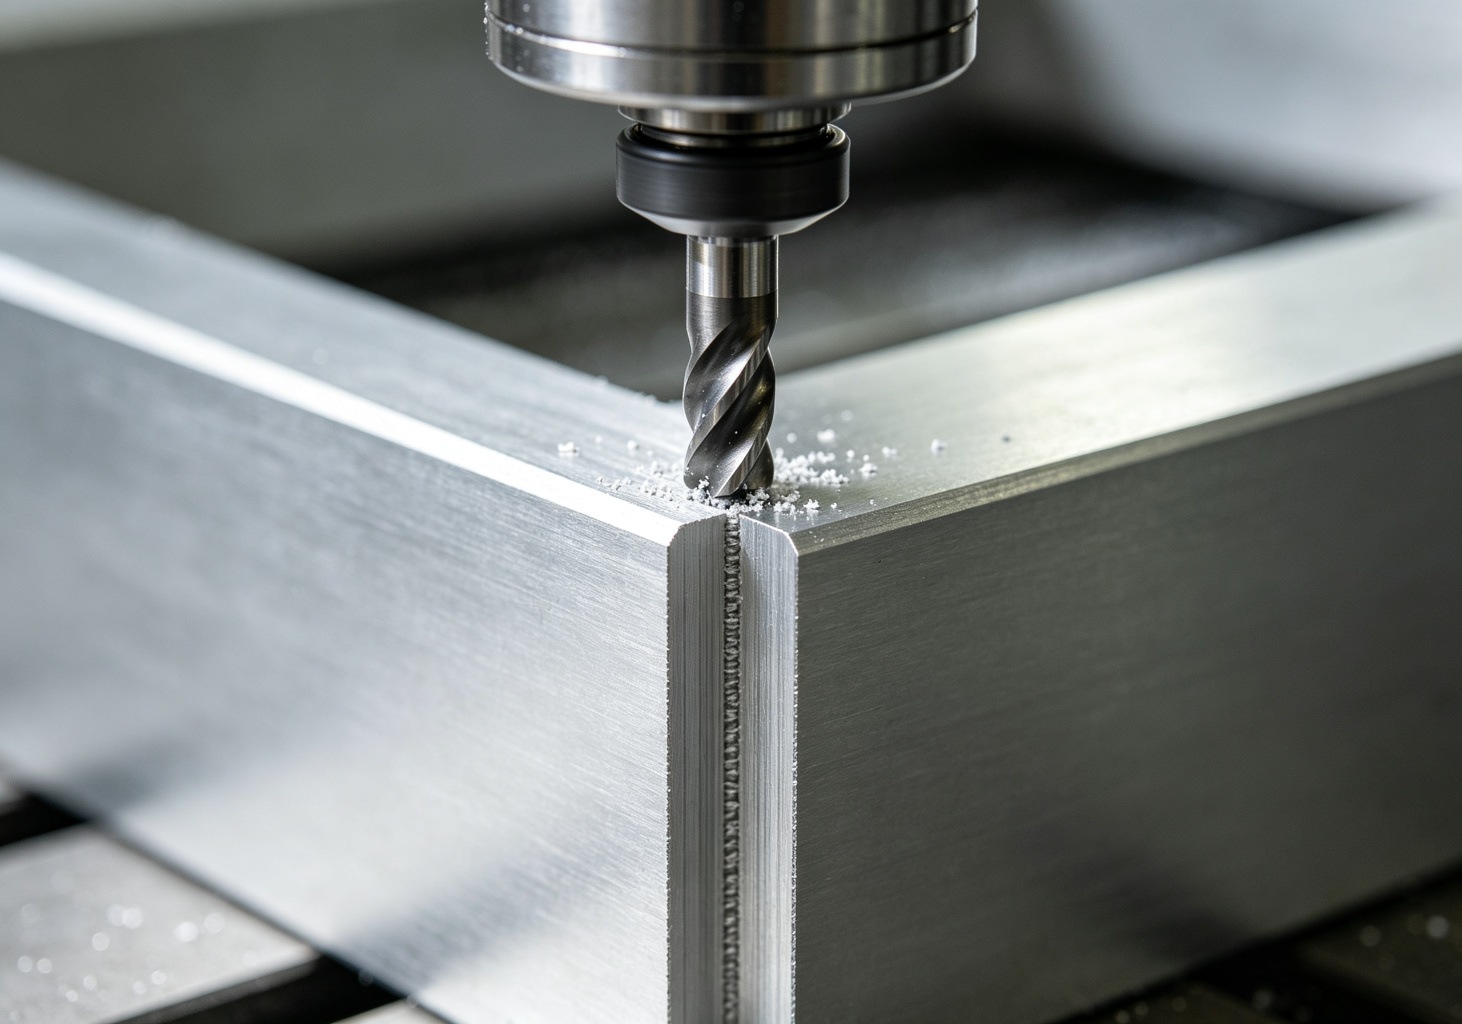
3D contour creates successive XY profiles at different Z heights, effectively slicing the geometry into horizontal levels. This suits steep or near-vertical surfaces.

The tool cannot reach the surface with a fixed 3-axis orientation.
The tool holder collides with the workpiece; the cutter must tilt.
Freeform surfaces require tool orientation control to keep engagement stable.
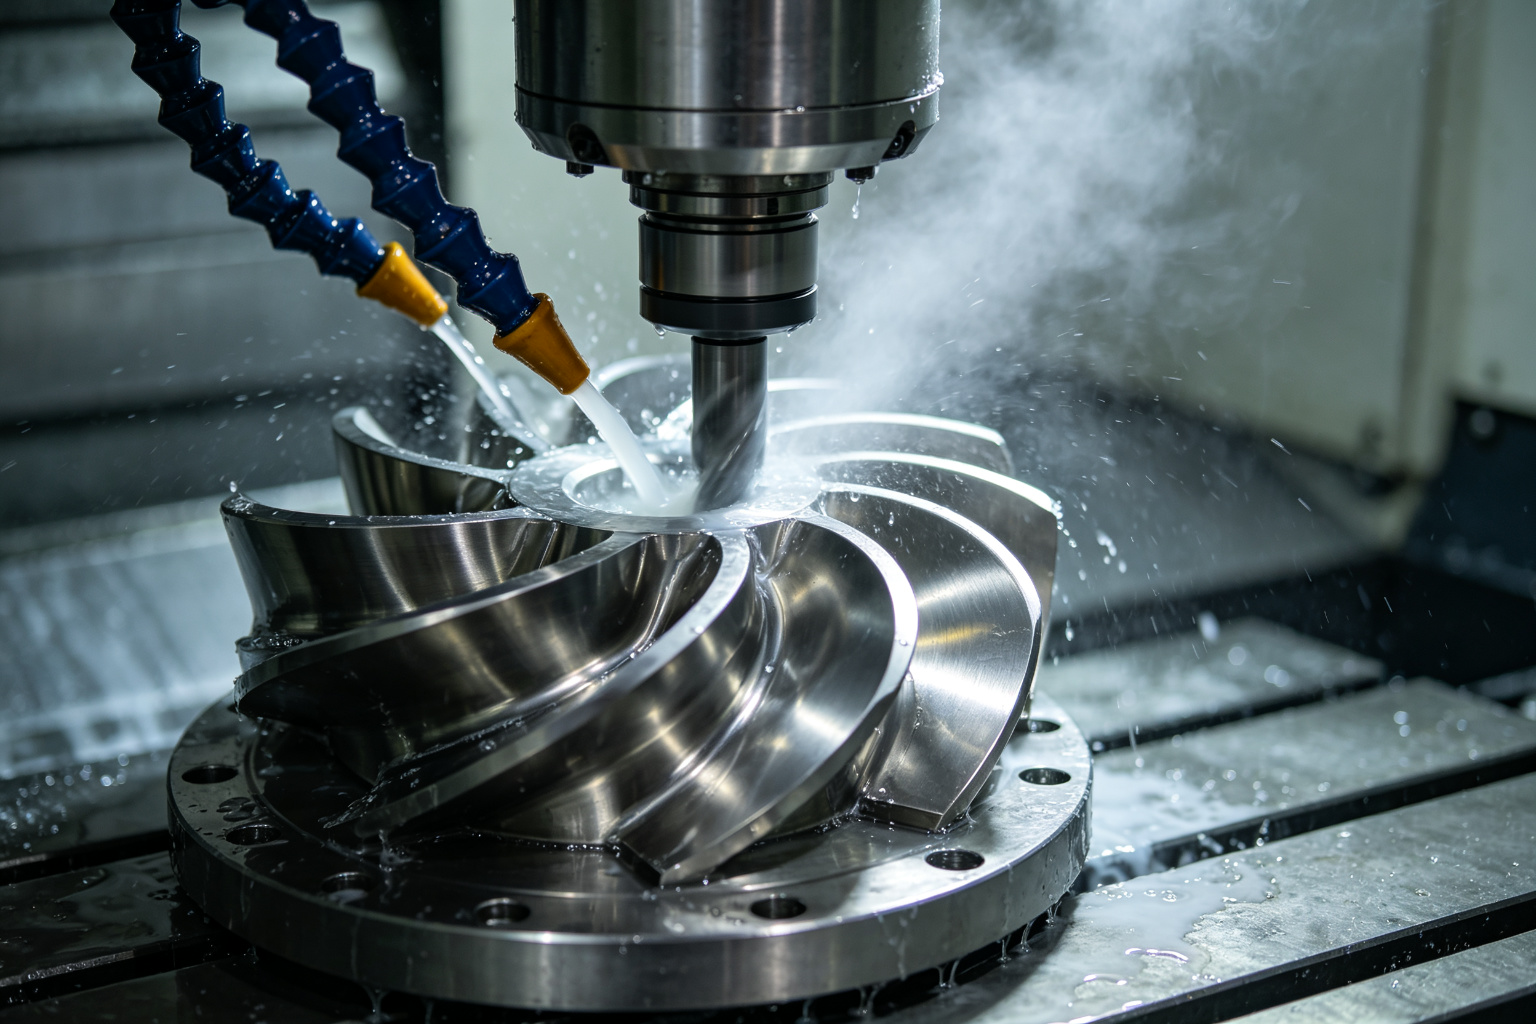
Freeform surfaces such as impeller blades need tilted tool orientation to stay in a stable cutting position.
Multi-axis strategies add lead / lag, tilt and holder-clearance control. When your geometry needs them, the toolpath review is part of the quotation — not an afterthought. 5-axis CNC machining services →
| Material | Main contour challenge |
|---|---|
| Aluminum | High-speed cutting is effective; tool geometry and chip evacuation matter |
| Stainless steel | Higher cutting forces and heat at the contour wall |
| Titanium | Heat management and stable tool engagement |
| Tool steel | Rigidity, tool wear and finishing behavior |
| PEEK / plastics | Lower stiffness and thermal sensitivity |
| Composites | Fiber direction and tool wear |
Yes — but contour milling itself does not define a universal tolerance. Achievable accuracy depends on machine condition, tool rigidity, cutter size, material, workholding, thermal stability, tool wear, path compensation and the required geometry.
Generally easier to hold.
Difficulty increases with depth and overhang.
Moves under cutting force; support and light passes matter.
Needs a smaller cutter, which can raise deflection risk.
Surface finish is affected by tool radius, stepdown, toolpath tolerance, cutter condition, tool orientation, cutting stability and remaining stock. A smaller stepdown can reduce visible scalloping on 3D contour walls but increases toolpath length and machining time.
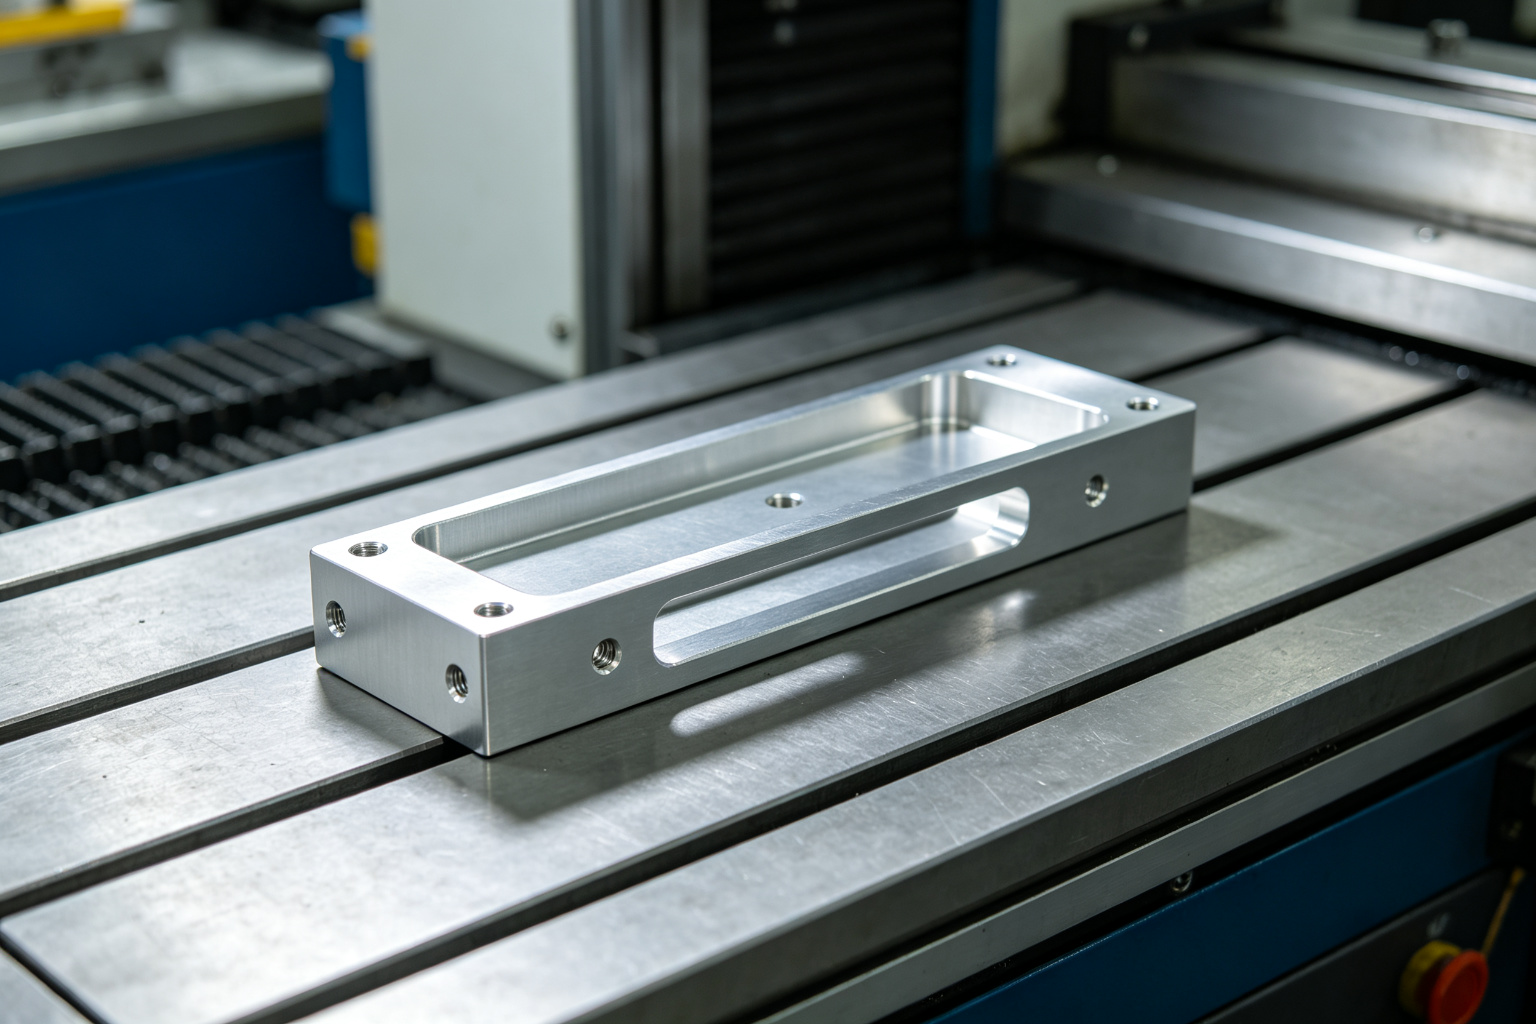
Thin-wall brackets need light finishing passes and stable support; the same wall can move if the cutting strategy ignores it.
| Geometry | Typical inspection |
|---|---|
| 2D profile | Dimensional measurement, optical inspection, CMM |
| 3D profile | CMM, CAD comparison, surface / profile inspection |
| Critical walls | Thickness, angle, position, profile |
| Complex freeform | Profile deviation, datum-based CAD comparison |
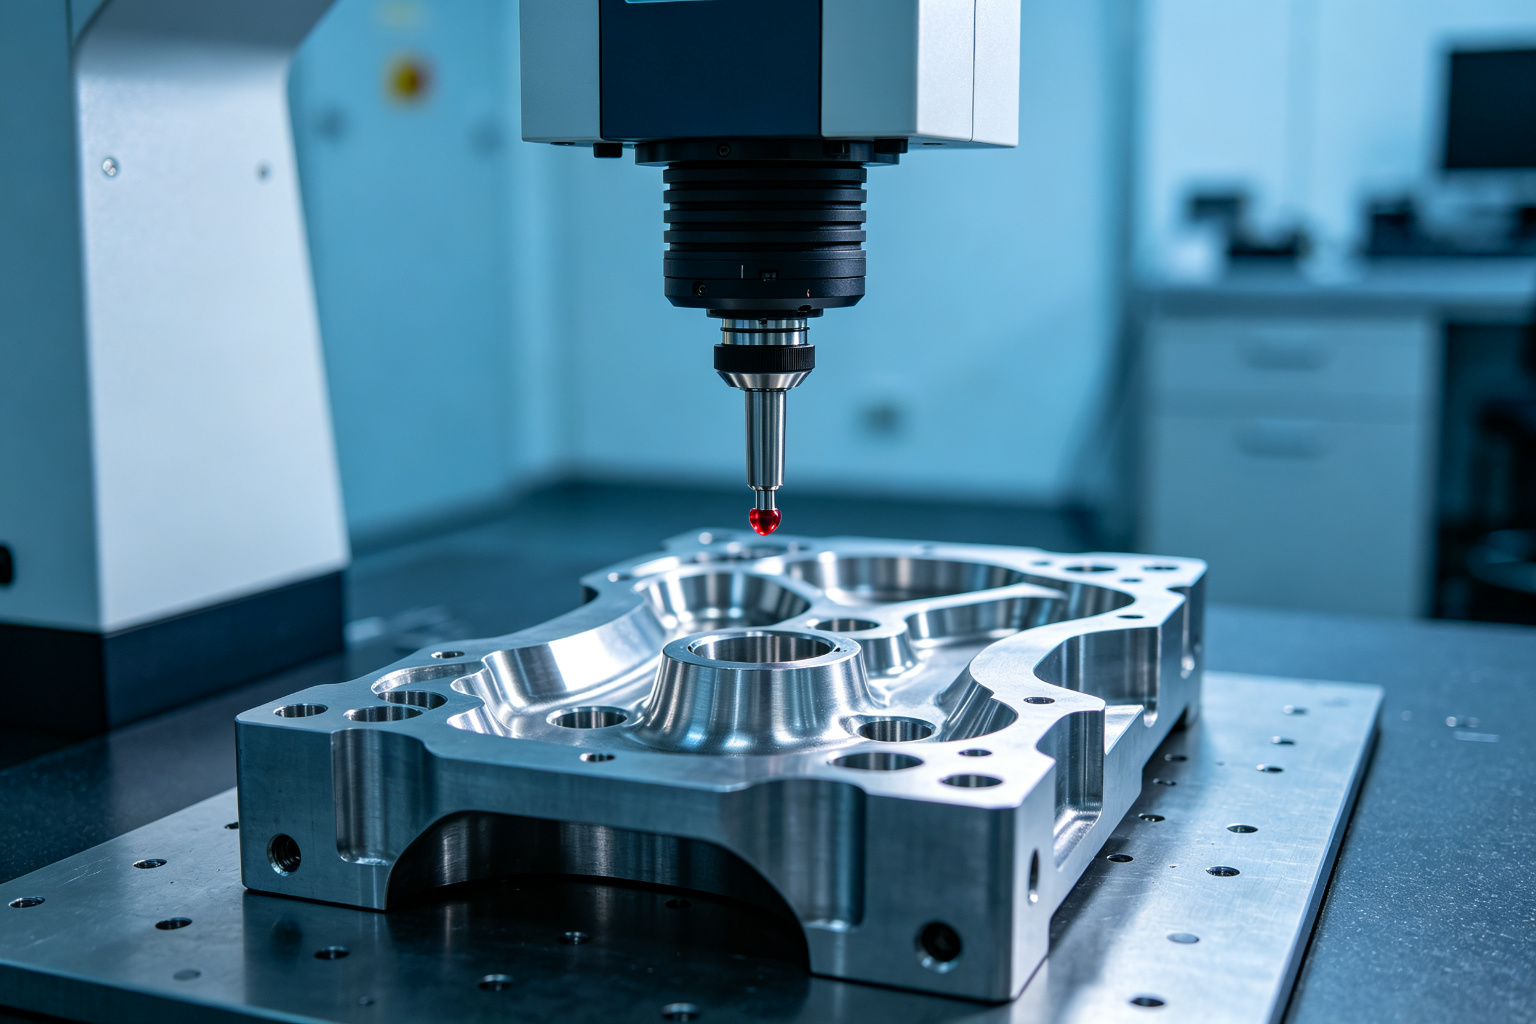
Datum-based CMM inspection compares the machined profile to the CAD model, not just individual edge measurements.
Goldcattle uses CMM inspection for applicable critical dimensions and complex profiles.
- Profile geometry and finished shape
- Dimensional tolerance and GD&T
- Surface roughness where it matters
- Material and condition
- Critical edge condition, radii / chamfers
- Datum references
The drawing should define the required geometry and acceptance criteria. The manufacturer should determine the appropriate toolpath, tooling and machining parameters.
You are not expected to specify "use an end mill at 4,000 rpm." You define what the finished part must achieve.
Material: 6061-T6
External contour tolerance: ±0.05 mm
Critical hole positions: per GD&T
Surface finish: Ra 1.6 μm on visible faces
Quantity: 50 pcs
Step file + 2D drawing provided
With this input, the supplier can decide whether 2D contour, 3+2 or another strategy fits the geometry and access.
2D and 3D contour toolpaths on prismatic parts.
Multi-face, angled and difficult-access contour geometry.
Rotational components that combine turned and contoured features.
Critical dimensions and profile verification against the drawing.
Material selection matched to the contour duty and environment.
First-part validation before batch production.
Complex curved geometry example: an Inconel 718 impeller was machined with simultaneous 5-axis contouring to manage tool access and holder clearance across the blade surfaces. See related CNC machining services →
Contour milling is a CNC strategy where the tool follows a defined boundary, wall or surface path to create the required profile. It can be 2D, 3D or multi-axis depending on the geometry and CAM system.
2D contour follows a defined boundary mainly in XY at fixed depths. 3D contour creates successive profiles at different Z heights, which suits steep or near-vertical surfaces and mold walls.
No. Most contour operations run with 3-axis motion. 5-axis is added when tool orientation, access, undercuts or holder clearance need rotary movement.
The terms overlap; in many CAM systems profile milling is called contour milling. Contour is a machining concept, and the exact operation name varies by software.
Taper, undersize or oversize profiles and chatter usually trace to tool deflection, tool wear, compensation errors, workholding stability or excessive engagement.
Drawing or STEP, material, tolerance and surface requirements, critical features, datums and quantity. The supplier selects the toolpath and machining parameters.
Yes, where geometry, tooling, workholding and machine condition support it. Tolerance should be assigned to functional features rather than applied to every dimension.
What tool is used for contour milling?
End mills are the most common, with diameter and reach chosen for the profile radius, wall depth and stiffness required.
How do you prevent chatter during contour milling?
Improve rigidity, reduce radial engagement, shorten tool overhang and check the tool and fixture before adjusting speeds.
What causes taper in contour milling?
Usually tool deflection, long overhang, unstable workholding or unequal cutting engagement. Check tool rigidity and fixture support first.
Can contour milling replace pocket milling?
No. Contour follows a boundary or wall; pocket clearing removes material inside an enclosed area. The two are complementary strategies.
How is a CNC contour measured?
2D profiles by dimensional measurement or CMM; 3D and freeform profiles by CMM and CAD comparison against the drawing.
Is 3D contour the same as 5-axis milling?
No. 3D contour is a Z-level finishing strategy that can run on a 3-axis machine. 5-axis adds tool-axis movement for access and clearance.
Send your 2D drawing, 3D CAD file, material and quantity. We can review the contour geometry, tooling access and manufacturing route before quotation.