Two material-removal processes, two different cutting mechanisms, two different jobs. This guide explains which one your part actually needs — and when the right answer is both.
- Cutting Mechanism
- Hardness & Material
- Tolerance & Finish
- Process Route
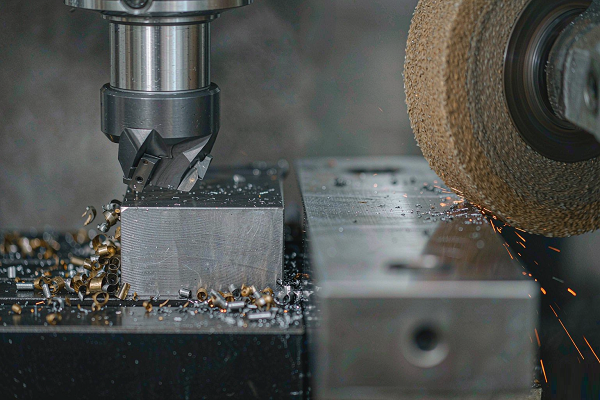
Milling and grinding are different machining processes. Milling uses a rotating cutting tool with defined cutting edges and is generally suited to creating geometry and removing larger amounts of material. Grinding uses abrasive grains and is commonly used for final dimensional, geometric and surface-finish refinement. In many precision parts, the most effective route is not milling or grinding, but milling followed by grinding.
Milling vs Grinding at a Glance
Ten factors, side by side. Where a cell says "typical", it means typical — not guaranteed.
| Factor | Milling | Grinding |
|---|---|---|
| Cutting tool | Multi-edge cutter with defined geometry | Abrasive wheel with bonded grains |
| Main role | Geometry creation and material removal | Precision finishing and final correction |
| Material removal | Generally higher | Generally lower, but process-dependent |
| Surface finish | Good functional surface | Typically better for fine finishing |
| Tight tolerance | Good, application-dependent | Strong for precision finishing |
| Hardened materials | Application-dependent | Often advantageous |
| Pockets and slots | Excellent | Limited |
| Complex 3D geometry | Excellent | More process-specific |
| Final sizing | Good | Excellent |
| Typical route position | Roughing, semi-finishing, often finishing | Finishing and final correction |
These are typical roles, not fixed categories. Modern CNC milling handles a great deal of finishing work, and certain grinding operations — creep-feed grinding in particular — can remove substantial material. The useful question is not "which process is more precise" but "which process produces this feature most reliably and economically".
Is Milling the Same as Grinding?
They share a purpose — removing material — and almost nothing else.
Both processes remove material from a workpiece to change its shape or dimensions. Beyond that, the tool, the cutting mechanism, the volume removed and the stage at which each is used are different enough that they behave as complementary operations rather than alternatives.
What Is Milling?
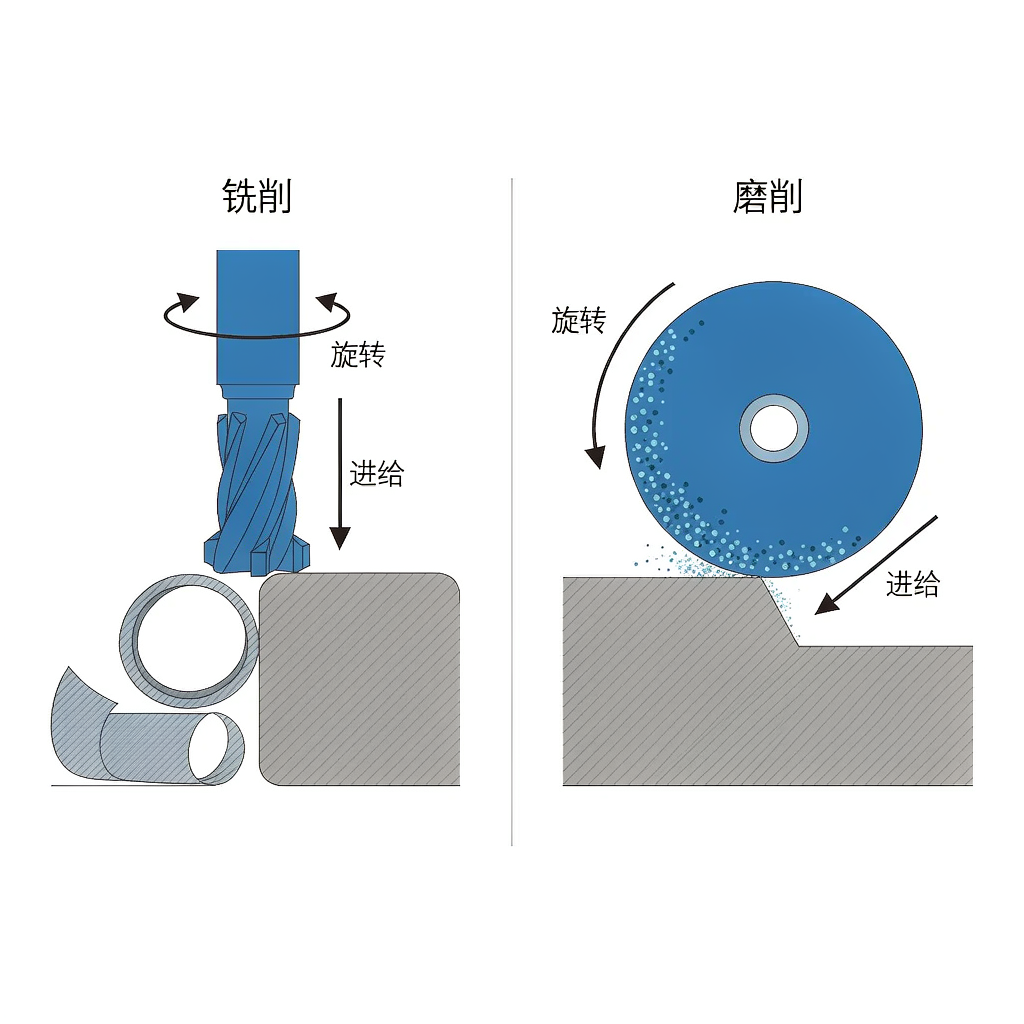
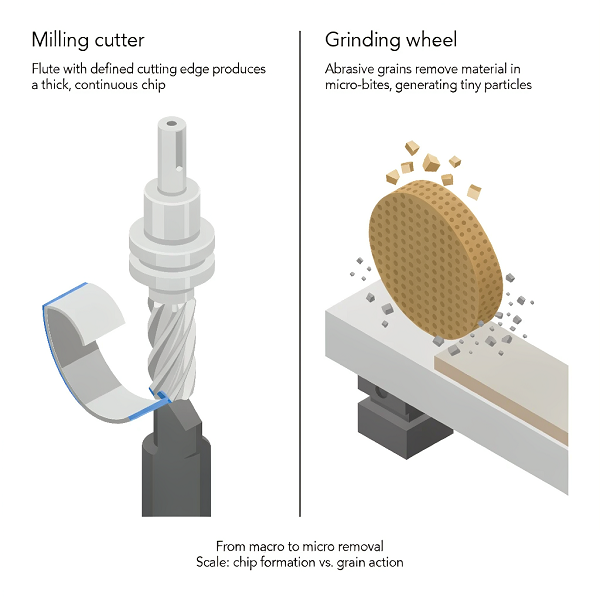
Milling uses a rotating multi-point cutter with defined cutting edges. Each edge shears a chip from the workpiece in a controlled, predictable way, which is why milling can be programmed to produce specific geometry: pockets, slots, faces, contours, steps and complex three-dimensional surfaces.
Because the cutter geometry is known, material removal can be planned and simulated. That makes milling the natural choice when the part needs geometry that does not yet exist.
What Is Grinding?
Grinding uses a wheel made of abrasive grains held in a bond. Each grain takes a microscopic cut, and the combined action of thousands of grains refines the surface. Where milling creates form, grinding refines it: final dimensional correction, flatness, roundness, cylindricity and surface finish.
Because the grains are not arranged in a defined cutting geometry, grinding is less suited to generating complex free-form shapes and more suited to bringing selected surfaces to a specified size, geometry and finish.
Why They Are Different
The difference is not precision level; it is mechanism. A milling cutter has a known edge position relative to the spindle, so it can cut a defined path through solid material. A grinding wheel has thousands of irregular cutting points, so it excels at removing small, uniform amounts across a surface but cannot be commanded to produce an arbitrary pocket in the way a cutter can.
That single mechanical difference explains most of the practical guidance on this page: milling creates, grinding refines, and the best route often uses both.
What Is the Difference Between Milling and Grinding?
Four dimensions: tool, mechanism, removal rate, and where the process sits in the route.
Cutting Tool
A milling cutter is a manufactured tool with a countable number of cutting edges, each with a defined rake, clearance and edge preparation. Its geometry is selected for the material and operation. A grinding wheel is an aggregate of abrasive grains — aluminium oxide, silicon carbide, CBN or diamond — held by a bond, and its behaviour depends on grain type, grain size, grade, structure and bond as much as on the machine.
Cutting Mechanism
In milling, the tool edge shears material ahead of it, forming a chip whose thickness is set by feed per tooth. Chip formation is intended and manageable. In grinding, each grain removes a very small amount, often with a high negative rake angle, producing fine particles rather than chips. The energy per unit volume removed is generally higher, which is why heat management and coolant strategy matter so much in grinding.
Material Removal
Milling generally removes material faster, particularly when a large volume has to go. Grinding typically removes less per pass and is most economical when applied to a small, controlled finishing allowance. There are exceptions — creep-feed grinding is designed for deep cuts in a single pass and can compete with milling in specific hardened-material applications — which is exactly why "grinding is always slow" is not a safe assumption.
Typical Production Stage
Milling usually appears early and often: roughing, semi-finishing, and in many cases finishing. Grinding usually appears late: after heat treatment, bringing selected features to final size and finish. But the dividing line is economic and technical, not categorical. If a milling operation can hold the required tolerance and finish reliably, adding a grinding operation increases cost without adding value.
When Is Milling the Better Choice?
Milling wins when the part needs geometry that does not exist yet.
Complex Geometry
Pockets, slots, contours, angled surfaces, steps, bosses and multiple faces in a single setup. A defined cutting edge can be commanded along a toolpath, so form is generated rather than approximated.
Large Material Removal
When a significant amount of stock has to come off, milling removes it faster and more cheaply than an abrasive process. Removing bulk with a precision finishing process is usually the expensive way to do it.
Multi-Axis Machining
3-axis covers prismatic work; 4- and 5-axis capability extends access to angled and undercut features, reducing setups and improving feature-to-feature relationship. See our CNC milling capability.
Pockets, Slots and Cavities
Internal geometry is where milling has no practical substitute. A grinding wheel cannot generate an enclosed pocket or a deep narrow slot the way an end mill can.
Prototype and Production Parts
Milling does not require the part geometry to suit the process. Change the program, change the part — which is why milling dominates prototypes, fixtures and low-to-mid volume production.
Non-Rotational Components
Brackets, housings, manifolds, mold components, plates and structural parts are naturally prismatic and are produced by milling rather than by a rotational abrasive process.
When Is Grinding the Better Choice?
Grinding wins when a surface has to end up at a specified size, geometry and finish — especially after heat treatment.
Final Dimensional Control
Bearing seats, precision fits, gauge surfaces and any feature whose final size governs assembly. Grinding removes material in small, controlled increments, which makes it suited to closing on a target dimension.
Flatness and Parallelism
Mold plates, precision inserts, tooling surfaces and sealing faces. Where two faces must be flat and parallel to each other, grinding is the conventional answer.
Roundness and Cylindricity
Shafts, pins, rollers and bearing journals. Cylindrical and centerless grinding address the geometric relationship between a diameter and its axis, not just the diameter value.
Fine Surface Finish
As the surface requirement becomes finer, abrasive refinement becomes increasingly attractive relative to a cutting process. Fine finishes on hardened surfaces in particular favour grinding.
Hardened Materials
After heat treatment, many steels are difficult or uneconomic to cut with a defined edge. Abrasive removal is not limited by the same tooling constraint, so hardened steel is one of grinding's most common applications.
Correcting Heat-Treatment Distortion
Heat treatment moves material. Grinding is frequently the operation that brings a distorted part back to its specified geometry — which is why it sits after heat treatment in most hardened-steel routes.
Is Grinding Always More Precise Than Milling?
No — and treating it as automatically true is one of the most expensive assumptions in process planning.
Whether a feature is produced accurately depends on machine capability, tool or wheel condition, material behaviour, geometry, workholding, thermal control, process parameters and the inspection method — not on the name of the process.
A well-maintained machining centre cutting a stable aluminium feature can hold geometry that a poorly set-up grinder will not. Conversely, a hardened steel shaft journal is usually finished by grinding because a cutting tool would struggle with the material, not because grinding is intrinsically more precise.
Precision tables that assign a fixed tolerance band to each process are popular and misleading, because they usually omit the conditions the number depends on: feature size, part geometry, material, stock allowance, thermal state and how the result was measured. A tolerance achieved on a small ground pin tells you little about what is achievable on a large milled plate.
Not "what tolerance does this process achieve" but: what tolerance can you hold on this feature, in this material, in this geometry, measured this way, on a production basis? That is a question with an answer, and it is the one worth getting in writing before tooling or process planning begins. We state achievable tolerance per feature after engineering review rather than quoting a general figure.
Typical Process Direction by Requirement
This table describes typical direction, not universal law. Actual capability depends on machine, material, geometry, workholding, tooling or wheel specification, and inspection method.
| Requirement | Typical Process Direction |
|---|---|
| Bulk stock removal | Milling |
| Complex pockets | Milling |
| 3D contours | Milling |
| Hardened precision surface | Grinding |
| Precision flatness | Grinding |
| Precision outside diameter | Cylindrical grinding |
| High-quality bore | Grinding or honing |
| Very fine surface finish | Grinding or honing |
| Mixed geometry plus tight finish | Milling followed by grinding |
Milling vs Grinding for Surface Finish
Why the process name does not determine the surface you get.
- Geometry and material removal first
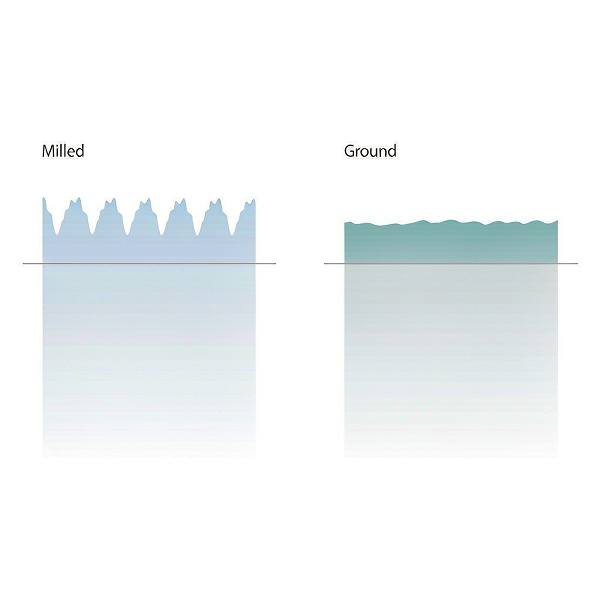
- Produces a good functional surface
- Finish influenced by feed, stepover, tool geometry and tool condition
- Can be improved with fine finishing passes and appropriate tooling
- Micro-scale abrasive removal
- Refines the surface and closes on final size
- Finish influenced by grain size, wheel grade, dressing and parameters
- Suited to fine finishes, particularly on hardened surfaces
The critical point is that surface finish is not determined by the process name alone. Cutter or wheel condition, material, cutting parameters, coolant, machine and setup rigidity, and the amount of stock being removed all influence the result. A worn tool on a well-specified machine produces a worse surface than a sharp tool on a modest one.
Finish Is More Than Roughness
Roughness is one parameter, and it is the one most often specified because it is easy to put on a drawing. But function usually depends on other characteristics as well: flatness for a sealing face, roundness for a bearing journal, lay direction for a sliding surface, and whether the surface has been affected thermally.
Grinding introduces its own surface considerations. Because abrasive removal generates significant heat at the contact zone, poor thermal control can produce surface damage that a roughness reading will not reveal. That is a reason to specify the functional requirement rather than a single number, and to agree how it will be measured.
Specify What the Surface Has to Do
The most useful drawing note describes the function: sealing, sliding, load-bearing, cosmetic, or a surface that will be coated. That allows the process and parameters to be selected to achieve it, instead of chasing a number that may not be the thing that matters.
Milling vs Grinding for Material Hardness
Hardness matters — but it is one input among several, not a switch.
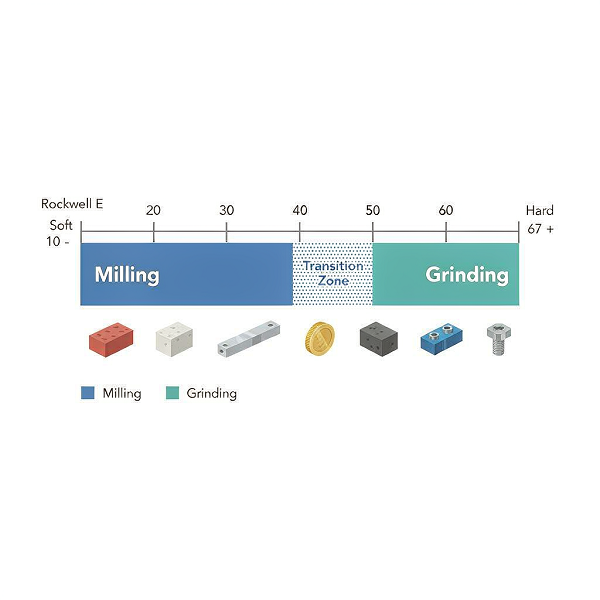
Hardness influences process choice because a defined cutting edge wears rapidly as the workpiece material gets harder, while abrasive grains are not limited in the same way. The practical effect is that grinding becomes increasingly attractive as hardness, dimensional requirement and finishing requirement rise together. It is not a threshold that flips at a particular value.
| Material Condition | General Consideration |
|---|---|
| Soft, free-machining materials | Milling is often efficient; tool life is generally good and material removal can be aggressive |
| Medium-hard materials | Both may be appropriate; the decision is driven more by geometry, tolerance and finish than by hardness alone |
| Hardened tool steels | Grinding often becomes more attractive; hard milling may be viable depending on hardness level, geometry and tooling |
| Very hard or brittle materials | Process selection becomes highly material-specific; abrasive processes are commonly considered |
| Ceramics and similar | Specialised grinding or other abrasive processes; not a general machining decision |
Hardness Is Only One Input
Geometry, stock allowance, tolerance, heat generation, surface requirement, part size and production volume all influence the decision. A large pocket in a medium-hard steel is milled, because grinding cannot generate the pocket. A hardened shaft journal is ground, because cutting it would be uneconomic. Both decisions are correct and neither was made on hardness alone.
The Heat-Treatment Question
In hardened-steel routes the sequence usually determines the process split: machine the geometry while the material is in a machinable condition, heat treat for properties, then grind the surfaces that must be accurate afterwards. The alternative — hard milling the finished geometry after heat treatment — removes a process step but increases tooling cost and demands a very stable setup. Which is better depends on the part.
Milling vs Grinding: Which Is More Cost-Effective?
Compare the total process route, not the hourly machine rate.
- Large amounts of stock must be removed
- Geometry is complex or three-dimensional
- Multiple features can be produced in one setup
- Tolerances and finish are within milling capability
- Volume is low, or the design is still changing
- The material is hardened
- Final dimensions are tight on specific features
- Surface finish requirements are fine
- Flatness, roundness or cylindricity is specified
- It removes a manual finishing or fitting operation
The mistake is comparing machine-hour rates. A grinding operation can look expensive per hour and still be the cheaper route if it replaces several manual operations, eliminates scrap, or makes a hardened part possible at all. Equally, adding a grinding step to a part that milling already holds comfortably is pure added cost.
A route of milling + heat treatment + deburring + manual finishing is not automatically cheaper than milling + heat treatment + grinding. The second route may remove the manual operation entirely, improve consistency and reduce rejection. The only way to know is to price the whole route against the part's actual requirements — which is a normal part of a process review.
Why Milling and Grinding Are Often Combined
For most precision parts the question is not which process, but in what order.
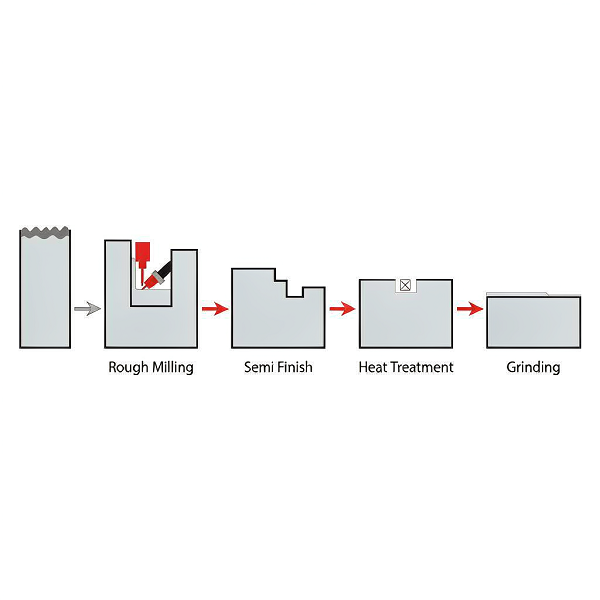
The two processes are usually complementary. Milling creates geometry and removes the bulk of the stock while the material is easiest to cut; grinding then brings selected surfaces to final size and finish after the material has been hardened. Asking which single process to use is often the wrong question.
Rough Milling
Remove the bulk of the stock efficiently while the material is in a machinable condition, leaving a controlled, uniform allowance for what follows. Uniformity matters: a consistent finishing allowance gives the downstream operation a stable starting point.
Heat Treatment
Achieve the required material properties. Heat treatment changes dimensions — parts move — and that movement is why a subsequent finishing operation exists in hardened-steel routes.
Finish Grinding
Bring the specified surfaces to final size, geometry and finish, removing the allowance left after milling and correcting distortion introduced by heat treatment. Because the allowance is small and controlled, grinding stays economical.
Honing
Where a bore needs controlled geometry and surface characteristics beyond what grinding delivers, honing follows. It is a bore-specific finishing operation rather than a general-purpose one.
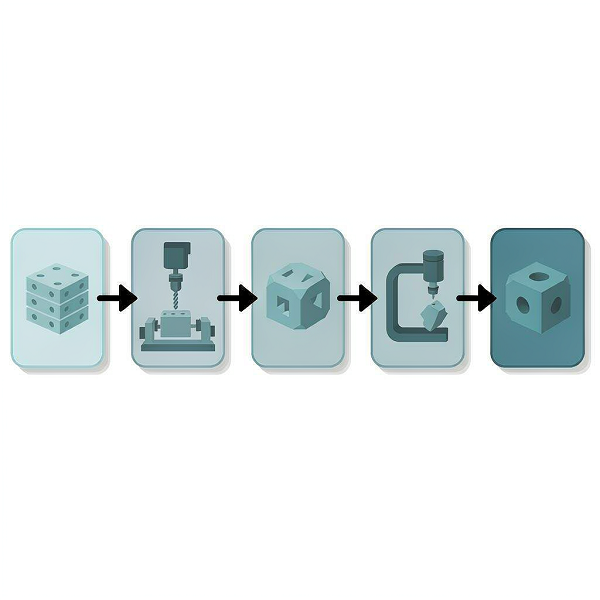
Why Milling + Grinding Is Often More Efficient Than Grinding Alone
The principle is straightforward: do not use a precision finishing process to perform a bulk-removal task, unless the specific process makes economic and technical sense. Milling removes the majority of the stock quickly; grinding then removes a small finishing allowance. The reverse — grinding away everything — consumes more time, more wheel and more energy for no additional accuracy on the surfaces that do not need it.
The same logic sets the finishing allowance. Too little and grinding cannot clean up the surface left by the previous operation or correct heat-treatment movement. Too much and grinding becomes a slow stock-removal operation, generating heat and consuming wheel life. Setting that allowance is a process planning decision, and it should be made with the actual part and route in mind.
Milling vs Grinding vs EDM
When milling cannot do it, the answer is not automatically grinding.
In mold work, hardened components and intricate internal features, the real choice is frequently between three processes rather than two. Electrical discharge machining removes material by controlled spark erosion rather than by cutting or abrasion, which means hardness is largely irrelevant to it and it can produce internal shapes with sharp corners that a rotating tool cannot reach.
| Requirement | Consider |
|---|---|
| Complex pocket or cavity | Milling |
| Tight final flatness | Grinding |
| Very hard steel with an intricate cavity | EDM |
| Internal sharp corners | EDM |
| Precision bore | Grinding or honing |
| Large stock removal | Milling |
| Hardened precision surface | Grinding |
EDM brings its own trade-offs: it is generally slower than cutting, it leaves a recast surface layer that may need removal for some applications, and electrode design and wear affect accuracy. It earns its place where geometry or hardness rules out the alternatives, not as a general substitute. More detail on our EDM machining services.
Which Grinding Process Should You Use?
"Grinding" is a family, not a single operation.
| Requirement | Process |
|---|---|
| Flat precision surface | Surface grinding |
| Precision outside diameter | Cylindrical grinding |
| High-volume round parts | Centerless grinding |
| Precision internal diameter | Internal grinding |
| Bore geometry and surface character | Honing |
| Fine surface finish | Grinding or honing, depending on the feature |
Surface Grinding
Produces flat surfaces and controls parallelism between opposing faces. Common for mold plates, precision inserts, tooling surfaces and sealing faces.
Cylindrical Grinding
Works on outside diameters between centres or in a chuck, controlling diameter, roundness and cylindricity. Typical for shafts, pins and bearing journals.
Centerless Grinding
Supports the part between a grinding wheel, a regulating wheel and a work rest rather than between centres. Suited to high-volume round parts where throughput matters.
Internal Grinding
Addresses bores and internal diameters, where access and wheel size constrain the operation more than in external work.
Honing
A bore-specific finishing operation using abrasive stones, controlling bore geometry and surface character in ways that grinding does not. See our precision grinding and honing capability.
Typical Parts: Milling vs Grinding
Concrete examples rather than industry labels.
- Brackets and mounting plates
- Housings and enclosures
- Manifolds and valve bodies
- Mold cavities and cores
- Pockets, slots and contoured features
- Structural components
- Prototypes and fixtures
- Shafts and spindles
- Bearing seats and journals
- Precision pins and dowels
- Mold plates and precision inserts
- Hardened tool steel components
- Sealing and mating surfaces
- Bores requiring honing
Many parts appear on both lists at different features. A mold insert is milled to create its form and ground on its mounting faces; a shaft is turned for its geometry and ground at its bearing journals. The split is by feature, not by part.
Workholding, Datums and Process Sequence
The detail that decides whether a multi-process route actually works.
A part that goes through milling, heat treatment and grinding changes hands, machines and setups several times. If the datum structure is not managed across those transitions, the final grinding operation cannot guarantee alignment with the features created earlier — and no amount of machine precision will fix it.
Datum Definition and Transfer
Primary, secondary and tertiary datums should be defined on the drawing and maintained physically through each setup. When a datum surface is machined away or distorted by heat treatment, the datum has to be transferred deliberately — not assumed to still exist.
Setup Repeatability
Each setup introduces location variation. A route with fewer, better-controlled setups generally produces more consistent feature-to-feature relationships than one with many re-clamps, which is one reason multi-axis capability can improve accuracy as well as reduce handling.
Distortion Management
Heat treatment moves material, and so does removing stock from a part with internal stress. Allowance for that movement, and a finishing operation capable of correcting it, is part of route design rather than a problem to be solved on the shop floor.
Clamping on Thin or Delicate Features
Workholding force can distort a part that will spring back after release, producing a feature that measures correctly while clamped and incorrectly afterwards. This is a common cause of "it measured fine in the machine".
Inspection After Milling and Grinding
How you know the requirement was actually met.
Inspection method has to match the characteristic being verified. Measuring a diameter with a micrometer tells you about size, not roundness; measuring roughness does not tell you about flatness. Choosing the wrong method produces confident readings of the wrong thing.
| Requirement | Typical Inspection |
|---|---|
| Linear dimension | Micrometer, caliper or CMM depending on tolerance |
| Flatness | CMM or dedicated flatness measurement |
| Roundness | CMM or roundness measurement |
| Bore | Bore gauge or CMM |
| Surface roughness | Profilometer |
| Parallelism | CMM |
| Runout | CMM or dial indication |
Which features, at what frequency, to which method, with what record. Inspection scope is part of the quotation, not an afterthought — and defining it early is what prevents the common dispute where a part meets the drawing under one method and fails under another.
Common Misconceptions About Milling and Grinding
Five assumptions that regularly lead to the wrong process route.
Grinding always replaces milling.
A grinding wheel cannot generate a pocket, a slot or a three-dimensional contour the way a cutter can. Grinding refines surfaces that already exist; it does not create form.
Grinding is always more accurate than milling.
Accuracy depends on machine capability, tool or wheel condition, material, geometry, workholding, thermal control and inspection — not on the process name.
Milling is only for roughing.
Modern CNC milling performs a large amount of finishing work. If milling reliably holds the tolerance and finish, adding a grinding operation adds cost without adding value.
The tighter the tolerance, the better.
Unnecessary tolerance increases manufacturing and inspection cost, and can add process steps for no functional benefit. Tolerance the features that affect fit and function.
The roughness value alone determines the process.
Flatness, roundness, size, geometry, material behaviour and the surface's function all matter. A roughness number is one parameter among several.
Milling + Grinding Case Study
One representative hardened tool steel programme, described by process reasoning.
This is a representative programme type drawn from the kind of hardened tool steel work we run. It is anonymised — no customer name, part number or measured figures — because we do not publish customer-identifying information or results without written permission. If you want evidence relevant to your part, ask us what we can share.
Hardened Tool Steel Insert
- Part
- Precision insert for a production tool, with formed working geometry and ground mounting and locating faces
- Material
- Tool steel, supplied in an annealed or pre-hardened condition for machining
- Initial stock
- Sawn blank with allowance on all faces for the full route
- Milling requirement
- Generate the working form, pockets and clearance geometry; establish the datum faces that later operations will reference
- Heat treatment
- Harden and temper to the specified condition; dimensional movement expected and allowed for
- Grinding requirement
- Bring the mounting, locating and sealing faces to final size and geometry after heat treatment, correcting distortion
- Critical dimensions
- The locating and mounting features governing how the insert sits in the tool; stated per feature after engineering review
- Surface requirement
- Defined by function — sealing and locating faces specified for flatness as well as roughness
- Inspection
- Dimensional and geometric verification against the agreed features, with the method and scope set before production
- Final result
- Parts released against the drawing, with inspection records for the agreed features; process route recorded so repeat orders follow the same sequence
Why This Route
The form had to be created, so milling was not optional. The material had to be hardened, so heat treatment was not optional. Heat treatment moves material, so a finishing operation capable of correcting geometry was required on the faces that matter. Every step in the route exists because the part required it — which is the test a process route should always pass.
The alternative — hard milling the finished geometry after heat treatment — was considered and rejected on this programme because the tooling cost and setup risk outweighed the benefit of removing an operation. On a different part, with different geometry and volume, that answer could legitimately reverse.
Milling vs Grinding Decision Tree
Start from what the part needs, not from which machine is available.

Most real parts land on the final branch. The proportion of milling and grinding depends on part geometry, stock allowance, material condition and final specification — a complex mold insert may be almost entirely milling with minimal grinding, while a hardened shaft may be turning followed by grinding. There is no fixed split, and any single ratio quoted as a general rule should be treated with suspicion.
Frequently Asked Questions
The questions behind "milling vs grinding", answered without universal numbers.
No. Both remove material, but milling uses a rotating cutter with defined cutting edges to create geometry and remove stock efficiently, while grinding uses abrasive grains to refine dimensions, geometry and surface finish. They are usually complementary rather than interchangeable.
The cutting mechanism. A milling cutter has defined edges that shear chips and can be commanded along a toolpath, so it creates form. A grinding wheel has thousands of abrasive grains that remove tiny amounts, so it refines surfaces. That difference drives tool capability, removal rate and typical position in the process route.
Neither automatically. Accuracy depends on machine capability, tool or wheel condition, material, geometry, workholding, thermal control and inspection method. Grinding is commonly selected for precision finishing, especially on hardened material, but the reliable question is what tolerance can be held on a specific feature rather than which process name is more precise.
Sometimes. If milling can hold the required tolerance, geometry and finish reliably on the feature in question, grinding adds cost without adding value. Modern CNC milling performs a substantial amount of finishing work. On hardened surfaces or where flatness and roundness are specified, grinding usually remains the better answer.
Generally no, because a grinding wheel cannot generate enclosed pockets, deep slots or complex three-dimensional contours the way a cutter can. Some grinding operations, such as creep-feed grinding, can remove substantial material in specific applications, but they refine or cut profiles rather than create arbitrary geometry.
No. Hardened steel is one of the most common applications because abrasive removal is not limited by the same tooling constraints as a cutting edge, but grinding is also used on unhardened material where flatness, roundness or a fine finish is required.
No. That assumption is outdated. Modern CNC milling routinely performs semi-finishing and finishing operations to close tolerances and good surface finishes, which is why adding a grinding step is sometimes unnecessary.
Grinding is typically selected when a finer finish is required, particularly on hardened surfaces. But finish is not determined by the process name alone: tool or wheel condition, parameters, coolant, rigidity and stock removal all matter. Specify the functional requirement and the measurement method, not just a roughness number.
Per hour it often does, but that is the wrong comparison. A grinding operation that replaces manual finishing, reduces rejection or makes a hardened part possible can lower total cost. Compare the whole process route against the part's requirements, not individual machine rates.
If the part has features that must be accurate after hardening, usually yes. Heat treatment moves material, and a finishing operation is what brings those features back into specification. Whether that operation is grinding, hard milling or EDM depends on the geometry and the requirement.
Grinding is a general abrasive process covering flat, cylindrical, centerless and internal work. Honing is bore-specific: abrasive stones are used to control bore geometry and surface character in ways grinding does not. They are often sequential rather than alternative.
When geometry or hardness rules out the alternatives: intricate cavities in very hard steel, internal sharp corners a rotating tool cannot reach, or features where electrode-based removal is the practical option. EDM is generally slower and leaves a recast layer, so it is chosen for capability, not for speed.
Yes, and for many precision parts that is the correct route. We run CNC machining including 3-, 4- and 5-axis milling, precision grinding and honing, and EDM, so the route is planned around the part rather than around whichever process happens to be available.
A 3D model, a 2D drawing with tolerances and the features that matter, material specification and heat-treatment condition, surface requirements, quantity and target timeline. The drawing's critical features and datum structure are the most useful inputs for deciding where grinding is genuinely needed.
How Goldcattle Approaches Milling and Grinding
Relevant because the processes sit under one roof and one quality system.
Xiamen Goldcattle Plastic & Metal Products Co., Ltd. was founded in 1998 and operates six processes in-house: CNC machining, injection molding, mold making, 3D printing, die casting and sheet metal fabrication. For the decision on this page, the relevant point is that CNC machining — including 3-, 4- and 5-axis milling and turning — sits in the same facility as precision grinding and honing, under a single ISO 9001:2015 quality system.
That changes the conversation in one specific way: a process recommendation is not steered by which operation we happen to own. If your part does not need grinding, we will not add it. If it does, the route is planned as one sequence, with datum structure, heat treatment and finishing allowance decided together rather than handed between suppliers.
- Process review before quotation — geometry, material condition, tolerance and finish reviewed against the route, not against a single operation.
- Tolerance stated per feature — achievable tolerance confirmed after engineering review rather than quoted as a general capability.
- Inspection scope agreed up front — which features, which method, what record.
- Route recorded — so repeat orders follow the same sequence and the same decisions.
Request a CNC Machining & Grinding Process Review
Send your 3D model, 2D drawing, material specification, heat-treatment condition, quantity and target timeline. We will review which features genuinely need grinding, which can be finished by milling, and whether EDM belongs in the route.
- Milling vs grinding assessment by feature
- Heat treatment and finishing allowance planning
- Datum and workholding review
- Tolerance stated per feature
- Inspection scope agreed before production
- ISO 9001:2015
Related Pages
Where to go for the individual processes.