What Is the Biggest Disadvantage of Using CNC Machining?
CNC machining makes precise, repeatable custom parts — but it is not the cheapest route for every geometry, material, or volume. This guide explains where the cost and limitations come from, and how to judge whether CNC is the right process for your part.
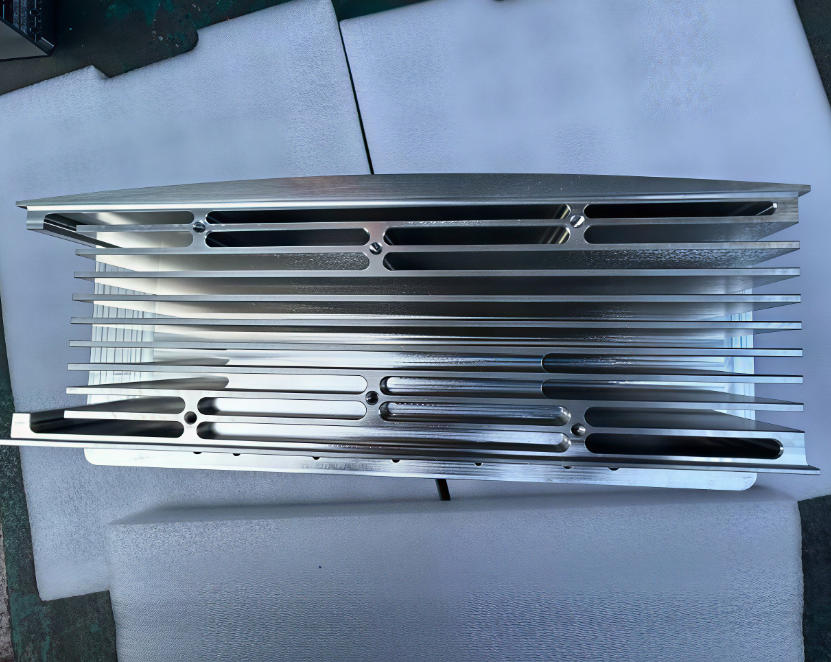
The biggest disadvantage of CNC machining is that programming, setup, material removal, tooling, and inspection can make certain parts expensive — most of all when the part's design or production volume does not justify that effort. The practical question is not "is CNC costly?" but "is CNC the right process for this part's function and quantity?"
At a glance
CNC machining removes material from a solid blank to create a finished shape. That single fact drives most of its limitations: you pay for the machine time, the tooling, and the scrap that the process leaves behind. The sections below break down where those costs and constraints actually come from, and how a procurement or engineering team can judge them before requesting a quote.
1 · High production cost for certain parts
A CNC program does not begin at the spindle. Every part carries the cost of programming, machine setup, cutting tools, workholding, and inspection — and for a small quantity those fixed activities can dominate the price. Cost rises further when a design includes deep pockets, thin walls, difficult-to-machine materials, or tolerances that do not affect how the part works.
Setup & fixtures
Multiple setups and dedicated fixtures add time and cost before any chip is cut. Fewer, well-planned setups reduce both.
Material & removal
Starting from a large billet and removing most of it means paying for material you discard, especially with expensive alloys.
Unneeded tolerance
Tight tolerances on noncritical features add machining time, inspection effort, and rejection risk without improving function.
CNC remains cost-effective for prototypes, low-volume production, complex components, and parts that require production-grade materials or precise interfaces. The fair comparison is total manufacturing requirement versus total delivered cost — not the machine's hourly rate alone.
2 · Material waste in subtractive manufacturing
Because CNC is subtractive, parts with large cavities or extensive removal generate significant chips and unused stock. This matters most when machining expensive alloys such as titanium, or when a part begins as a large billet that is mostly cut away.
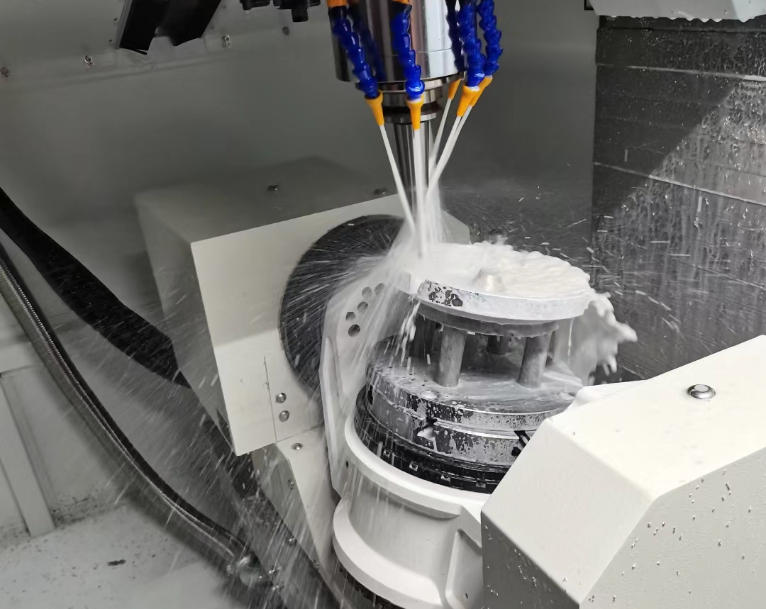
Designers can reduce unnecessary removal by reviewing pocket depths, wall thicknesses, stock dimensions, and alternative processes. For suitable parts, sheet-metal fabrication, casting, forging, or additive manufacturing may offer a better starting geometry. The right option depends on material properties, geometry, volume, and the required final condition — there is no universal rule.
3 · Setup and programming time
A CNC machine does not remove engineering preparation. A typical project may require CAD review, CAM programming, toolpath verification, workholding design, machine setup, and first-article inspection. For a simple one-off component, those activities can be a substantial share of the total cost; for repeat orders, the initial effort spreads across a larger quantity.
4 · Design and geometry limitations
CNC can produce many complex shapes, but tool access, cutter diameter, reach, workholding, and machine travel still impose practical limits. Deep narrow pockets, sharp internal corners, very thin walls, and features requiring access from several directions raise machining difficulty and cost.
A design-for-manufacturing review can identify opportunities to use larger internal radii, simplify nonfunctional features, reduce unnecessary setups, and specify tight tolerances only where needed. These changes improve manufacturability without compromising the part's intended function — and they are far cheaper to make on a drawing than on a finished batch.
5 · Tool wear, maintenance, and interruptions
Cutting tools wear during machining, and tool condition affects surface finish, dimensional accuracy, and consistency. Difficult materials, aggressive cutting conditions, and long cycles increase tool consumption. Machines also need preventive maintenance and periodic inspection; unplanned downtime can affect delivery, particularly when production depends on a specialized machine or fixture.
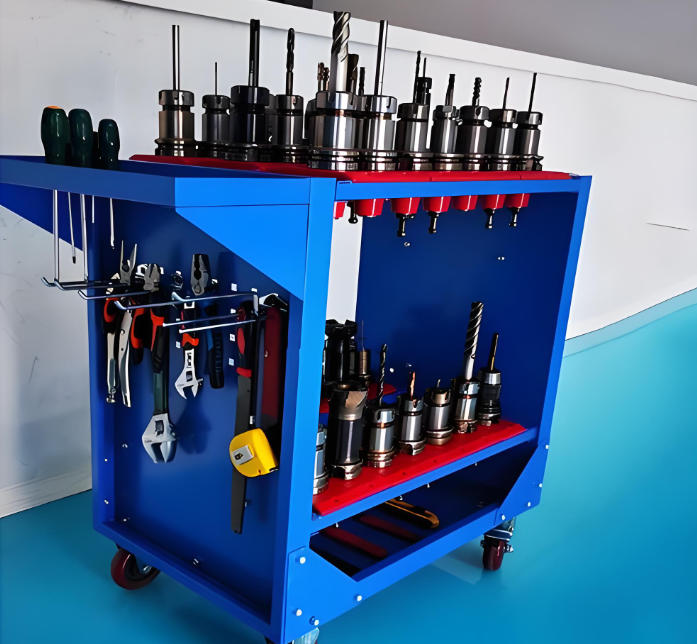
These risks are managed through tool-life monitoring, preventive maintenance, suitable cutting parameters, and appropriate inspection plans. They are normal parts of running a capable shop — but they are also reasons a quoted lead time should include buffer for the unexpected, not a promise that nothing will ever go wrong.
6 · Tight tolerances can increase cost
CNC can achieve tight results, but the achievable value depends on material, geometry, machine condition, setup, thermal effects, measurement method, and inspection requirements. Typical CNC tolerance is about ±0.01 mm, with tighter values reserved for qualified features and confirmed per project. Applying very tight tolerances to every dimension can increase machining time, inspection effort, and rejection risk without improving performance.
Drawings should identify critical dimensions and geometric tolerances by function. A manufacturing review then determines whether the specified requirements are practical and what additional controls are necessary — which is exactly where a design-for-manufacturing discussion pays for itself.
7 · CNC machining vs. alternative processes
CNC should be compared with other processes on geometry, material, required properties, volume, tooling investment, and total delivered cost. The table below is a selection guide, not an absolute rule — some parts need a hybrid of processes.
| Process | Worth evaluating when |
|---|---|
| CNC machining | Complex features, prototypes, low-to-medium volumes, or precise interfaces matter |
| Injection molding | Plastic parts need repeatable high-volume production and tooling investment is justified |
| Die casting | Suitable metal parts need repeatable near-net-shape production at appropriate volumes — see CNC vs die casting |
| Sheet-metal fabrication | Parts can be formed from sheet through cutting, bending, and joining |
| Metal stamping | Sheet-metal components suit dedicated tooling and repeated production |
| Additive manufacturing | Complex geometry, internal channels, or reduced material use justify the process — see CNC vs 3D printing |
8 · How to reduce CNC machining costs
The most effective cost reductions start with the design and specification — not with squeezing the machine hour. Aim to avoid paying for manufacturing complexity the finished part does not need:
- Remove nonfunctional features that require unnecessary machining.
- Use practical internal radii and accessible toolpaths where the design allows.
- Apply tight tolerances only to dimensions that affect fit, function, or performance.
- Select materials by functional requirement rather than assuming the strongest option is always best.
- Review whether multiple parts can be combined, or a simpler process is suitable.
- Consolidate repeat orders where demand and inventory justify it.
- Confirm inspection requirements and surface finishes before production begins.
- Request a design-for-manufacturability review before finalizing the drawing.
9 · How to choose the right manufacturing process
Before selecting CNC, work through these questions. A supplier should assess them with you before recommending a route.
- What functions must the finished part perform?
- Which dimensions, surfaces, and material properties are critical?
- What is the expected prototype quantity and annual demand?
- Does the design require complex geometry or tight tolerances?
- Would casting, stamping, molding, fabrication, or additive manufacturing reduce total cost?
- What inspection documents and delivery conditions are required?
Material choice is part of the same decision — see the materials overview for how grade, condition, and form affect machinability and cost. For many components, CNC is the most practical option; for others, a different or hybrid process offers a better balance of cost, quality, and delivery.
Not sure whether CNC is right for your part?
Send your drawing and model for a manufacturing review. We will assess process, setups, achievable tolerance, and a realistic cost and lead time — with no obligation.
Request a CNC Manufacturing ReviewXiamen Goldcattle Plastic & Metal Products Co., Ltd. — Founded in 1998 · ISO 9001:2015 · AS9100- and ISO 13485-aligned process controls