Custom automotive spoilers · OEM / ODM
Custom Automotive Spoiler Manufacturer for Prototypes and Production
From a single prototype bracket to a hardened production mold for a model-specific wing — we build spoiler parts to your drawing, validate the fitment physically, and run the program under one quality system. You specify the geometry, material and market; we engineer the path from sample to volume.
Who this page is for
Spoiler programs are not one buyer type. The questions that matter change by who you are — so the page is built around the four purchasing situations we actually support.
Tier-1 / OEM supplier
You need a sub-component made exactly to print, with traceable material, PPAP-style documentation and consistent lots. Fitment is defined by your CAD, not by us guessing the vehicle.
Aftermarket brand
You want a model-specific body part at low volume, branding-neutral, with finish and packaging that match your catalog. Bridge tooling lets you launch without a full production mold.
Motorsport / startup
You need a light, stiff part fast — often carbon or aluminum — and you will iterate the geometry between revisions. Prototype-first routing keeps you moving without tooling lock-in.
EV / aero program
You care about drag, downforce balance and weight as engineering targets. We build to your aero specification and validate dimensions; we do not invent performance numbers for you.
Spoiler types we manufacture
Six common geometries, each with a different mounting and manufacturing logic. We build to your drawing — these are the families we see most, not a fixed catalog.
Rear wing
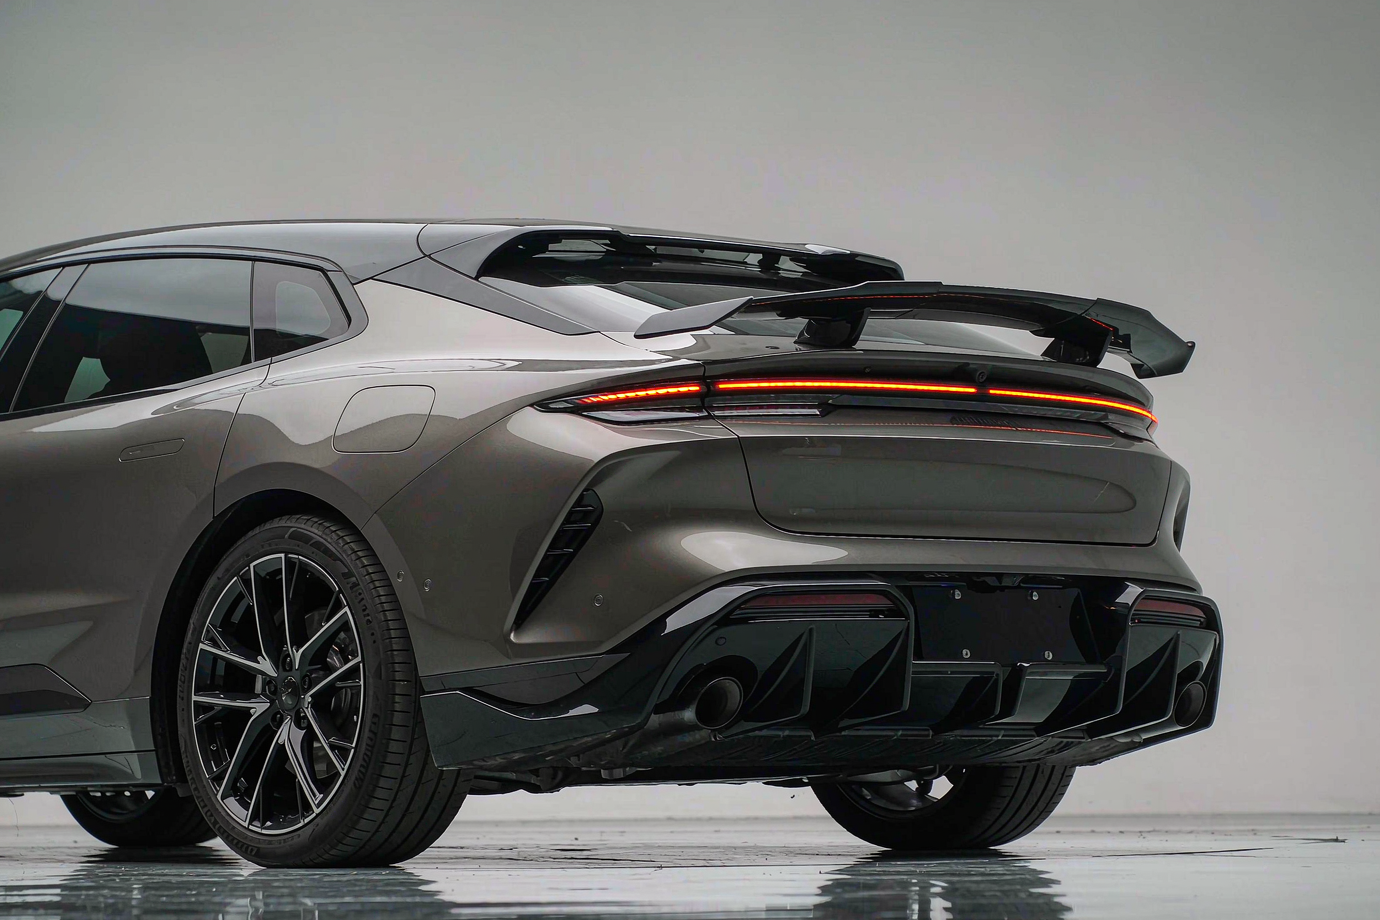
Adjustable or fixed GT-style wings with end plates and uprights. Often aluminum brackets + molded or carbon airfoil, built to a downforce spec you provide.
Lip spoiler
Low-profile trunk or bumper lip that sits flush to the panel. Usually injection-molded ABS/PC, painted or textured to match body color.
Roof spoiler
Small rear-roof fin or lip for hatchbacks and SUVs. Thin-wall molded part where fitment to the glass/roof radius is the critical dimension.
Diffuser-integrated
Rear lower valance or diffuser element paired with the spoiler. Larger molded or SMC panel where stiffness and mounting points dominate.
Ducktail / bootlid
Subtle integrated bootlid spoiler for a factory-style look. Molded as one piece with the lid or as an add-on blade.
Bespoke to drawing
A geometry that is none of the above — a concept study, a one-off aero part, or a part with no production equivalent yet. We start from your 3D model.
Material and process, chosen together
The material decides the process, and the process decides the cost and the fitment method. We pick the pair against your stiffness, temperature, weight and finish targets — not a default.
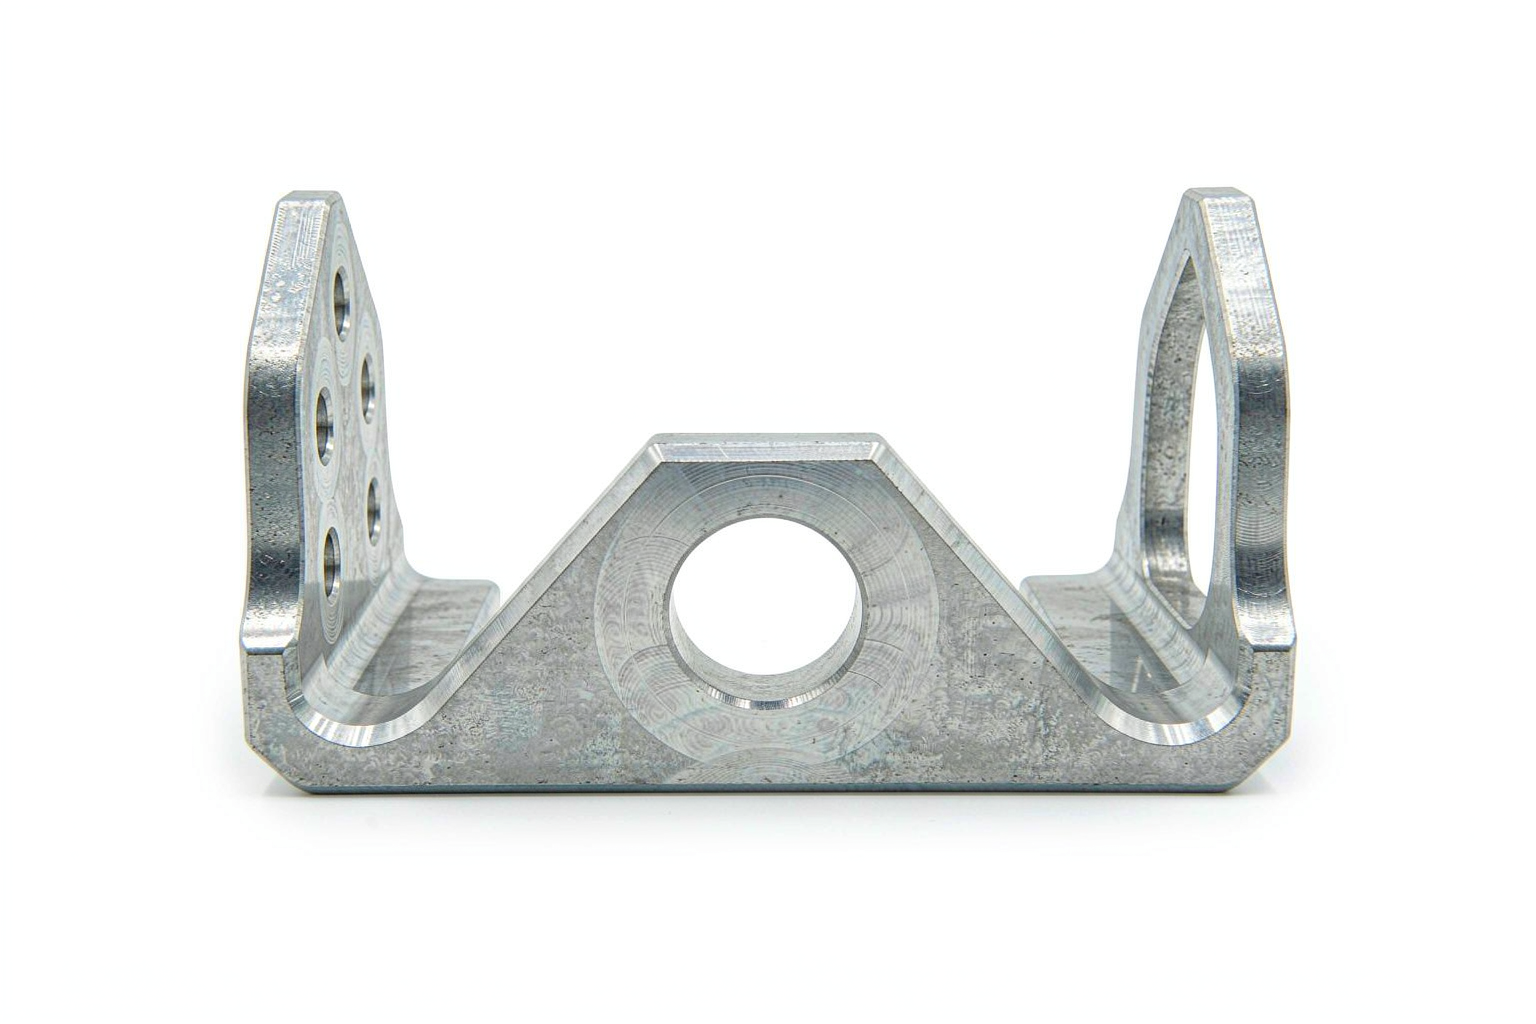
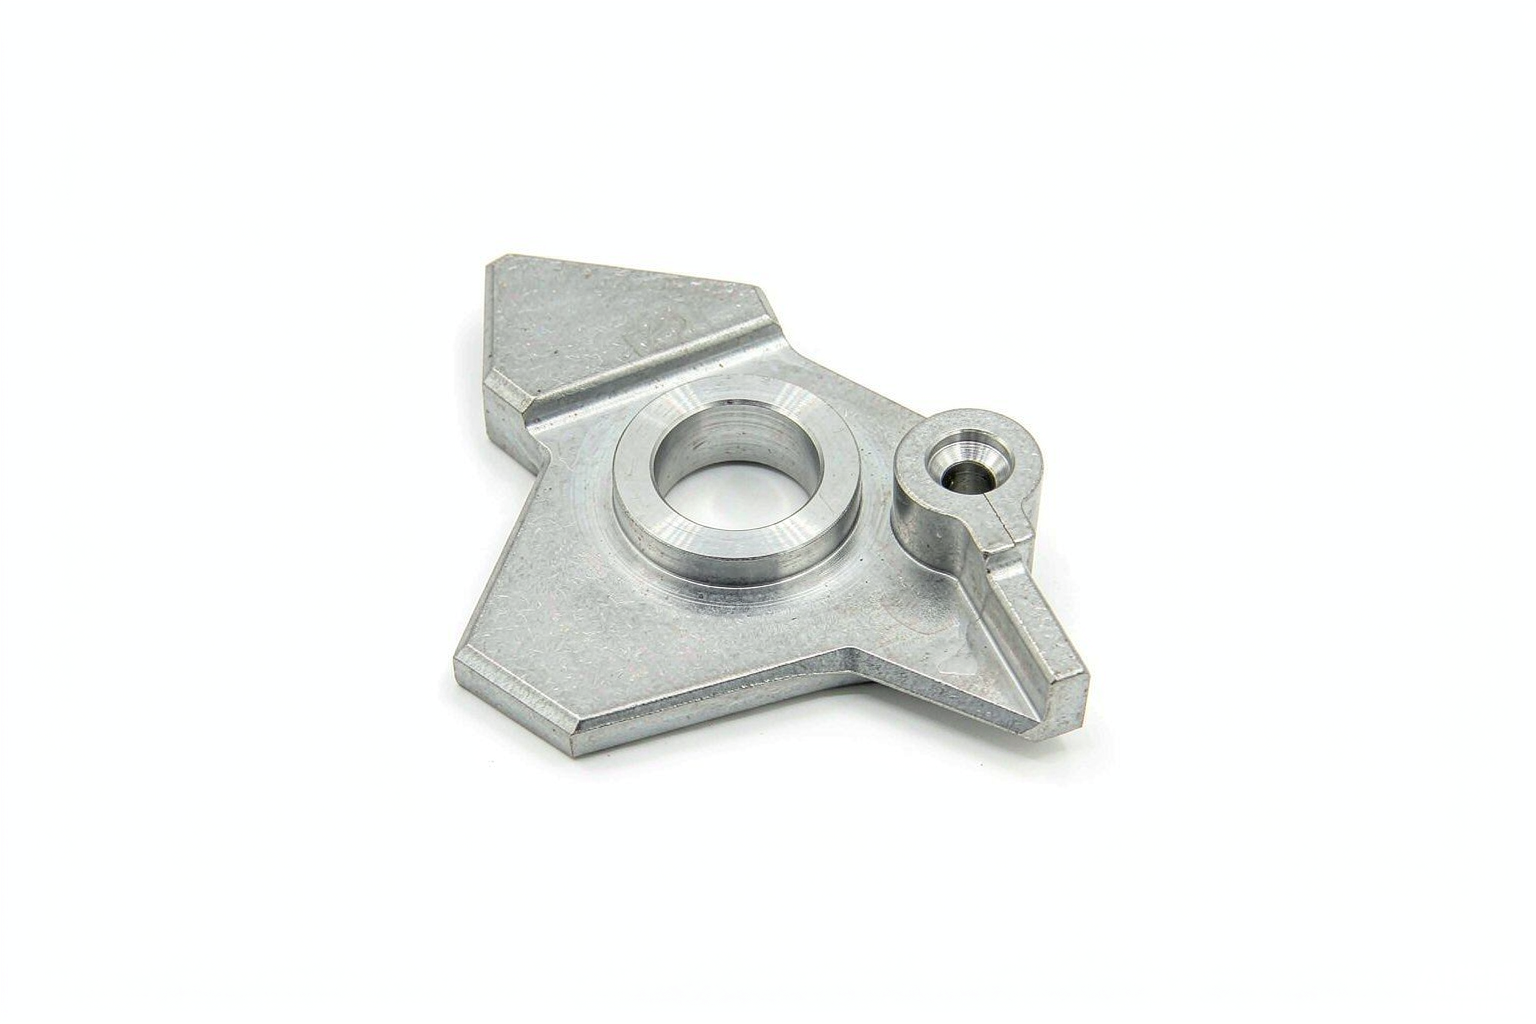
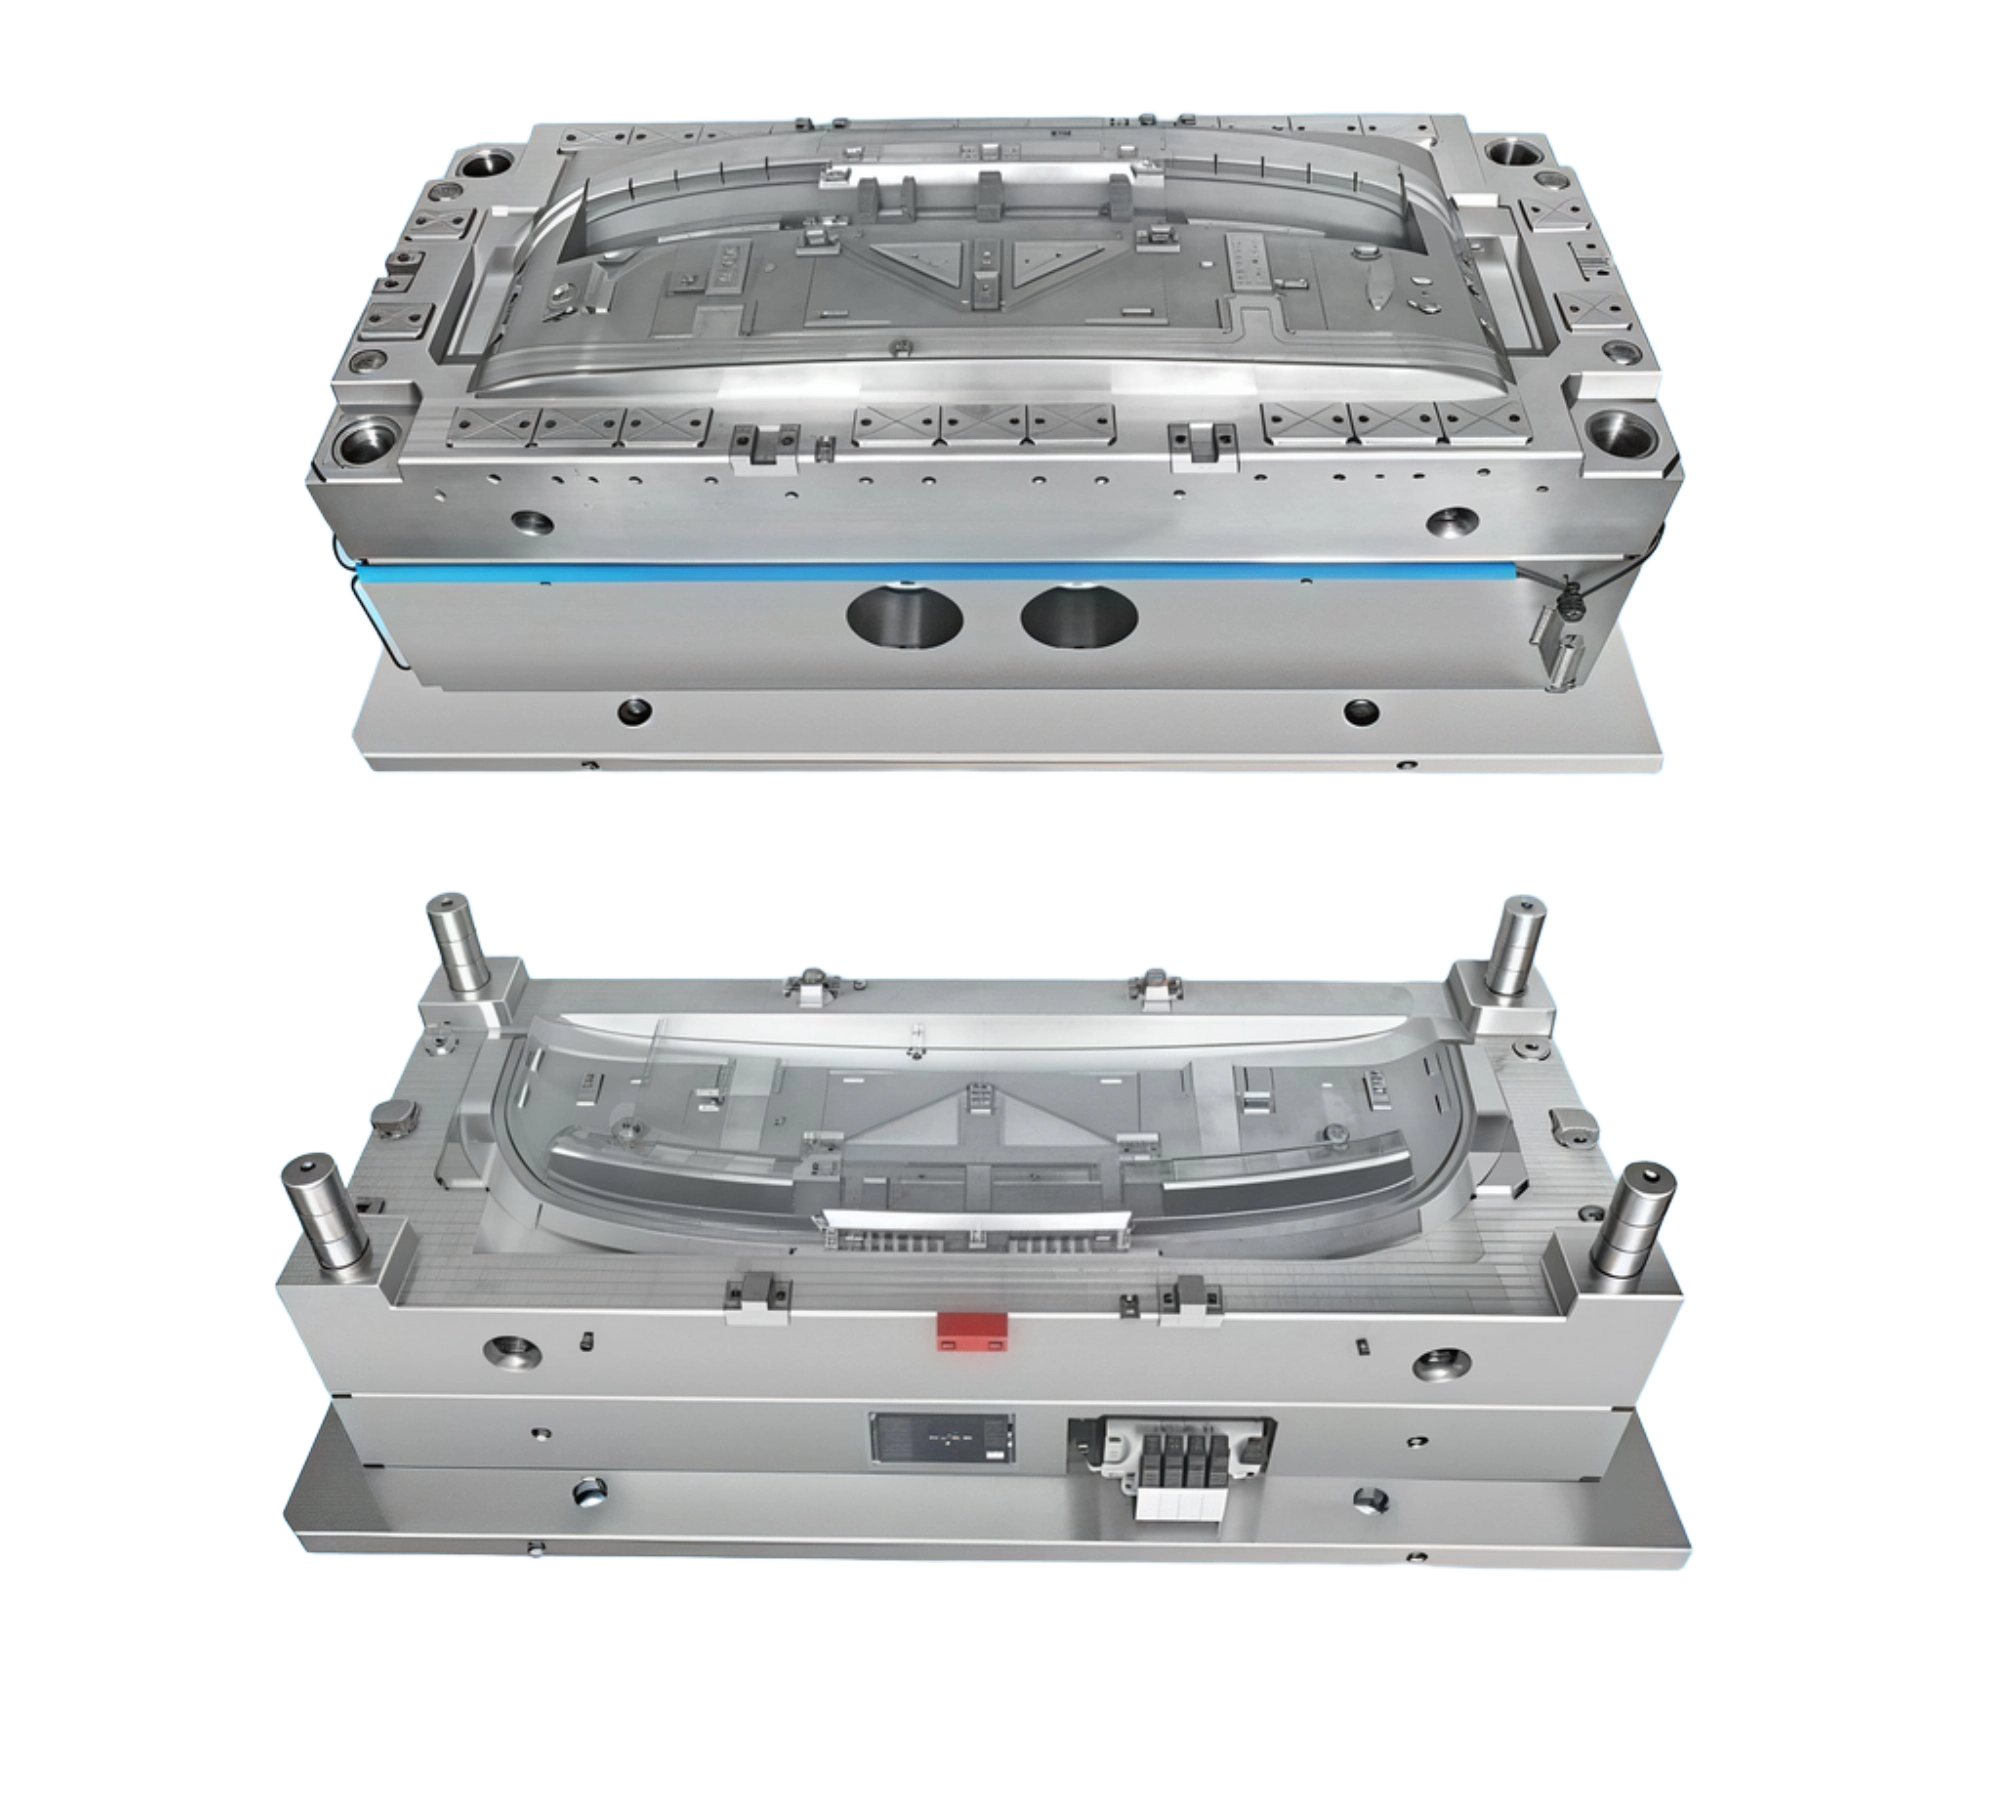
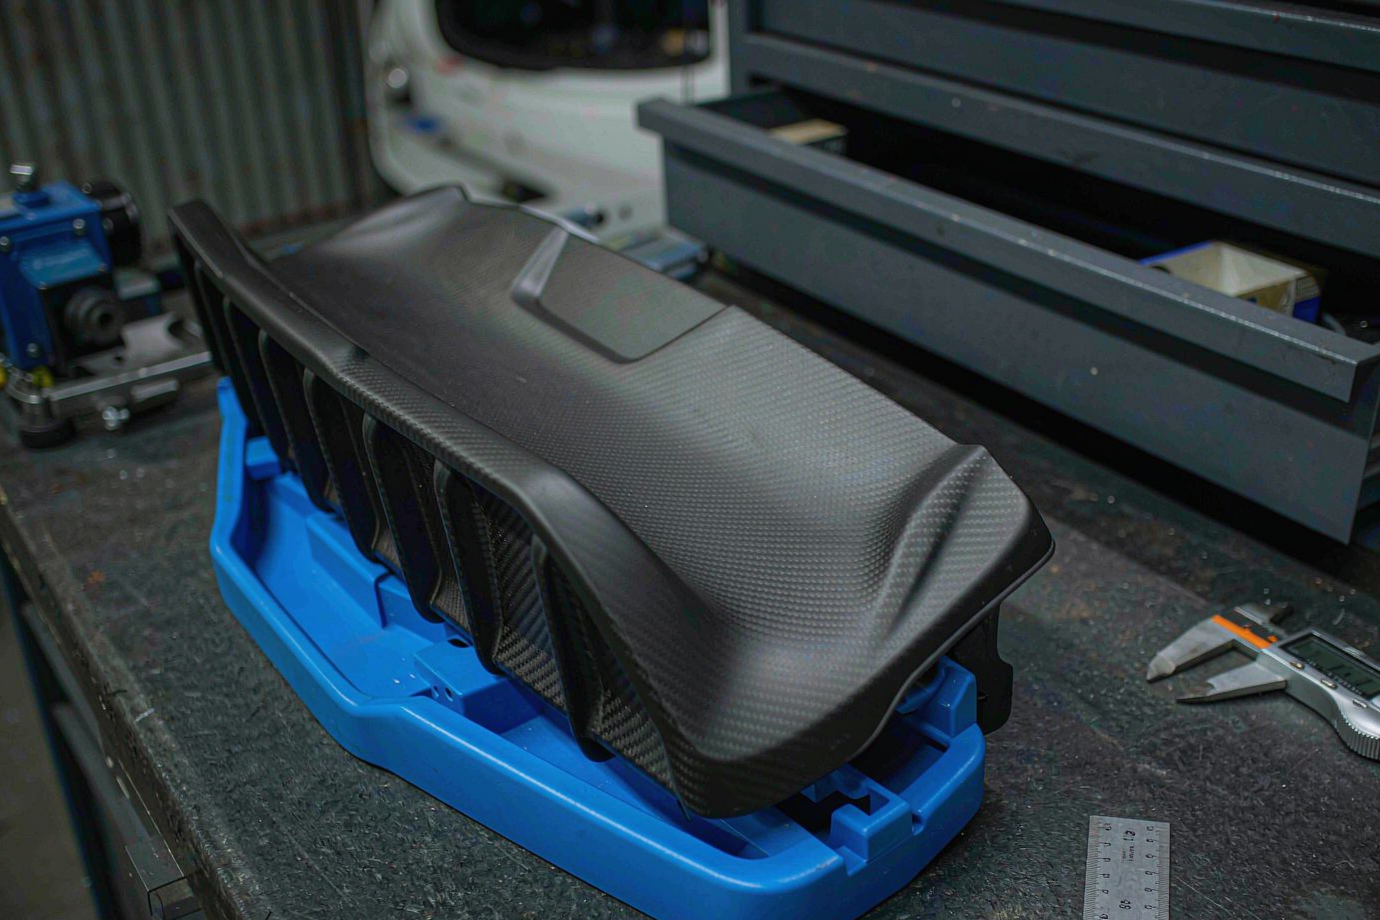
Most spoiler bodies are injection-molded ABS/PC or glass-filled nylon. Where weight matters, carbon fiber by RTM gives the best stiffness-to-weight. Mounting brackets and fixtures are CNC-machined aluminum. Large lower panels use SMC. The table shows the common pairings.
| Material | Why use it | Process | Typical use |
|---|---|---|---|
| ABS / PC blend | Cost-effective, paintable, good surface | Injection molding | Lip & ducktail spoilers |
| PA + GF (glass-filled nylon) | Stiff, heat-resistant, dimensionally stable | Injection molding | Structural body parts |
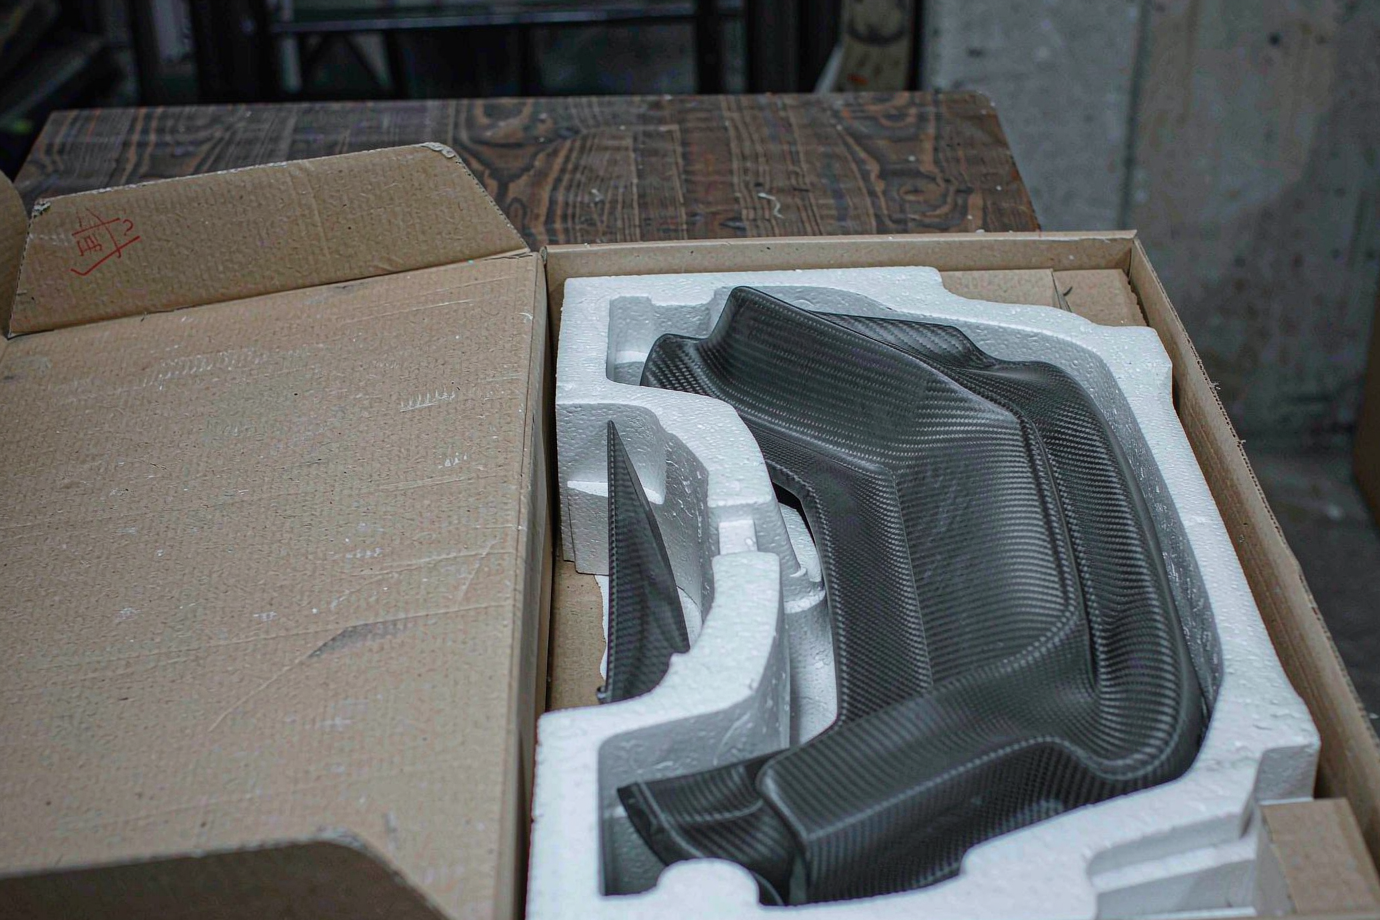
| Carbon fiber | High stiffness-to-weight | RTM / composite lay-up | Wings, aero parts |
| Aluminum | Structural mount, tight tolerance | CNC machining (3/4/5-axis) | Brackets, uprights, fixtures |
| SMC | Large panel, press-formed | Compression molding | Diffusers, lower valances |
From prototype to production — the path
A spoiler program is a sequence, not a single step. Here is the route from your file to volume, with the decision points where cost and risk are set.
Drawing & DFM
Review 3D model, flag mold/assembly risks, confirm critical dimensions.
Material & process
Select material + route against volume, weight and finish.
Tooling / fixture
Bridge tool, production mold or CNC fixture — set by volume.
Prototype
CNC, 3D print or RTM sample for fit and look.
Fitment check
Dry-fit on buck or vehicle; align to reference.
Inspection & docs
FAI, material certs, RoHS as required.
Production
Mass run, packaging, logistics to your Incoterms.
Fitment is validated, not assumed
Answer for buyers: model-specific spoilers are fitted by physical validation, not by a quoted gap number. Our CNC envelope is typically ±0.01 mm (qualified features to ±0.005 mm), but on molded and composite parts the real limit is tooling shrink and fixture repeatability — so we prove the part sits correctly on a buck or vehicle before release.
1 · CAD alignment
Model is aligned to your vehicle reference surfaces and mounting points before any metal is cut.
2 · Prototype mock-up
A 3D-printed or CNC sample is produced to check shape, stance and clearances early.
3 · Physical dry-fit
The sample is dry-fitted on a buck or vehicle to confirm panel line and mounting.
4 · Sign-off
Fitment tolerance is documented and signed off before production tooling is cut.
What we need from you to quote well
A tight quote comes from a tight spec. Send these and the gap between "roughly" and "confirmed" disappears.
- Drawing or 3D model with critical dimensions and tolerances.
- Target material and grade — or the property targets if the grade is open.
- Expected annual volume and target lead time.
- Mounting method and any vehicle reference platform.
- Required finish (paint, texture, raw) and packaging.
- Market and documentation needs (PPAP, material cert, RoHS, REACH).
Tooling and volume — pay for the right stage
You should not amortize a hardened production mold to validate a design. The route scales with your volume and how frozen the design is.
Prototype & low volume
- CNC machining, 3D printing or bridge tooling.
- MOQ 1 piece — validate fit and finish first.
- No hardened-tool commitment while the design moves.
- Lead time 3–7 days for prototypes.
Production volume
- Hardened steel injection molds for frozen designs.
- Unit cost drops as volume amortizes tooling.
- Mass production 15–25 working days per plan.
- Consistent lots under one quality system.
What actually drives the price
Spoiler cost is a stack, not a single surcharge. Knowing the drivers lets you only pay for what the function needs.
- Tooling stage: bridge tooling or CNC is cheaper to start than a hardened production mold; the mold cost is amortized only at volume.
- Material: carbon fiber and glass-filled compounds cost more than standard ABS/PC, and scrap is harder to recover.
- Finish: painting, texture and Class-A surface add steps versus a raw molded part.
- Complexity: undercuts, inserts and tight true-position call for more tooling and inspection.
- Documentation: PPAP, FAI and material certs add engineering time proportional to program rigor.
The cheapest path is usually: prototype in the right material, confirm fitment, then commit to production tooling only once the design is frozen. We will flag where a tolerance or finish is driving avoidable cost.
Inspection and documentation
A dimension is only meaningful if it is measured the way the part will be used, and backed by paper you can audit.
Documentation packages, inspection reports and material certificates are available on request and can be provided under NDA. Certificate copies are supplied against the specific lot you receive.
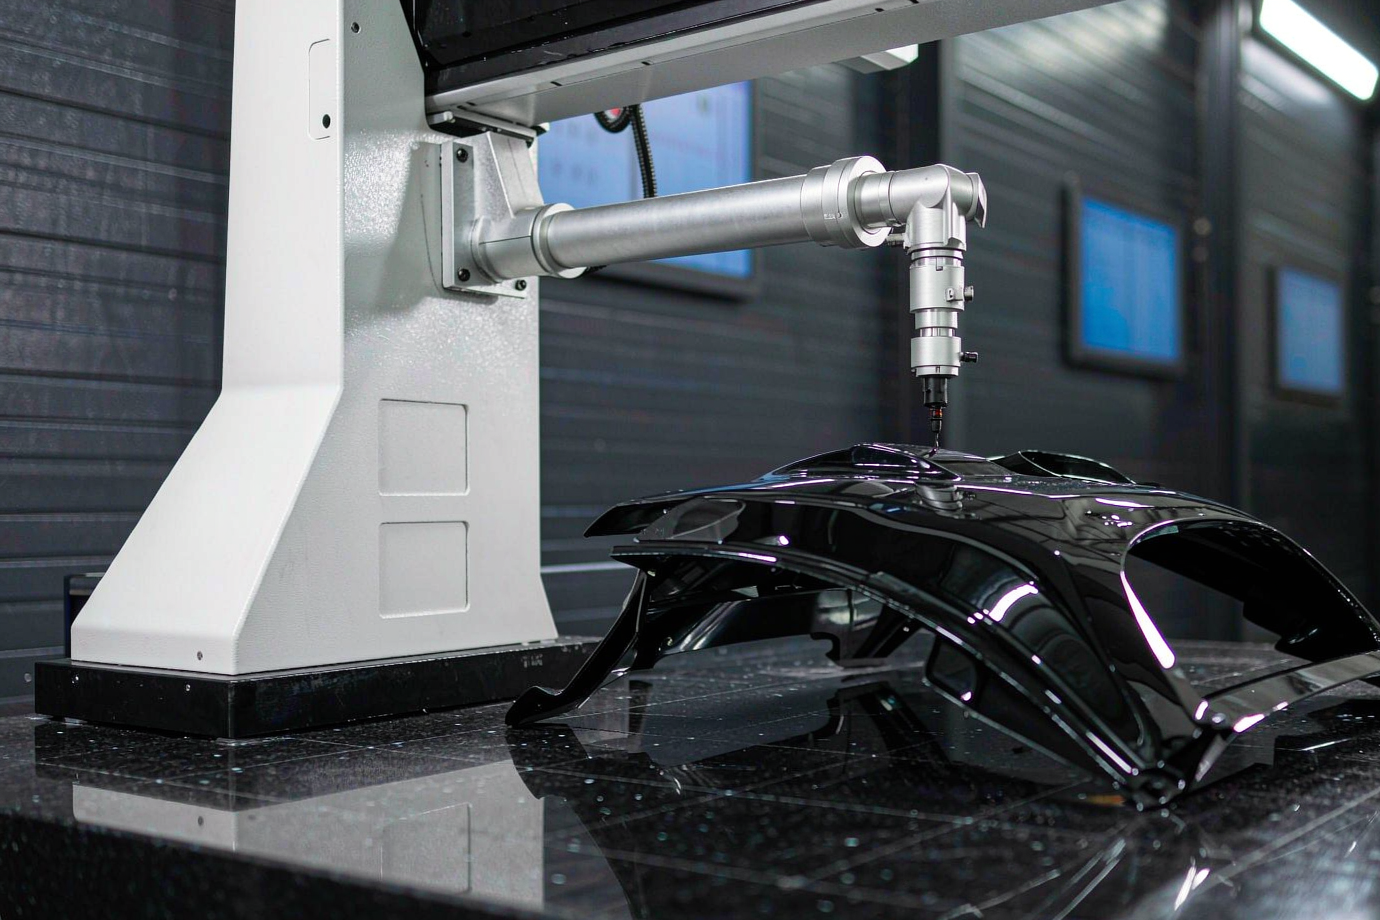
Compliance for EU and North America
We state what we can document, and we do not claim certifications we do not hold. Confirm specific substance and marking rules at RFQ for your target market.
European Union
- REACH: we work to REACH substance restrictions for EU-bound orders; confirm the specific substance list for your part at RFQ.
- RoHS: RoHS test report TQT7737B1373EC is available for relevant electronic-adjacent assemblies.
- Material certs: supplied per lot to support your declaration file.
North America
- PPAP: PPAP-style documentation packages available on request for automotive programs.
- Marking: we mark and document per your drawing and regional requirement, not a generic claim.
- Traceability: lot-level traceability under ISO 9001:2015 for production runs.
We are ISO 9001:2015 certified and work to IATF 16949 requirements; we do not represent an IATF 16949 certificate. Regulatory responsibility for the finished part rests with the brand owner — we support it with traceable material and inspection records.
Representative engineering example
How the controls come together on a real class of part. (Illustrative of our process; parameters confirmed per project, not a published case statistic.)
Aluminum mounting bracket + molded ABS lip spoiler for a model-specific aftermarket program
Flush fit to the trunk panel radius; bracket stiffness under vibration; consistent lots for a catalog
DFM on the 3D model · CNC aluminum bracket (3-axis) · injection-molded ABS body · dry-fit on buck · FAI per AS9102 on request
Physical fitment validated before tooling release; material cert and RoHS report available per lot
Why Xiamen Goldcattle
A spoiler program touches several processes. Running them under one roof — and one quality system — is what keeps fitment and lead time coherent.
1 · CNC machining
3/4/5-axis milling and turning for brackets, fixtures and prototype bodies.
2 · Injection molding
ABS/PC and glass-filled nylon bodies at volume, with in-house tooling.
3 · Mold making
Bridge and production molds built and maintained in-house.
4 · 3D printing
Rapid prototypes and validation mock-ups without tooling.
5 · Die casting
Structural aluminum parts where casting beats machining.
6 · Sheet metal
Brackets and mounting hardware where formed metal fits.
All six core processes — CNC machining, injection molding, mold making, 3D printing, die casting and sheet metal fabrication — are performed in-house under one ISO 9001:2015 quality system. Xiamen Goldcattle Plastic & Metal Products Co., Ltd. has been an OEM/ODM manufacturer since 1998.
Frequently asked questions
What spoiler types can you manufacture?
We make rear wings, lip spoilers, roof spoilers, diffuser-integrated profiles, ducktail / bootlid spoilers, and fully bespoke geometries built to your drawing. The right type is driven by your vehicle platform, mounting method and the performance or styling target you specify — not by a catalog we push.
Which materials are used for automotive spoilers?
Common choices are ABS/PC blends and glass-filled nylon (PA+GF) for injection-molded parts, carbon fiber for high stiffness-to-weight via RTM, aluminum for structural brackets via CNC machining, and SMC for larger panels. Material is selected against your stiffness, temperature, weight and finish requirements.
What manufacturing processes are involved?
Spoiler programs typically combine injection molding for volume bodies, CNC machining for aluminum brackets and fixtures, in-house mold making, 3D printing for prototypes and validation, and RTM or composite lay-up for carbon parts. All six core processes are performed in-house under one ISO 9001:2015 quality system.
What tolerance can you hold on a spoiler?
Our CNC envelope is typically ±0.01 mm, with qualified features held to ±0.005 mm where geometry allows. For molded and composite parts the binding limit is often tooling shrink and fixture repeatability rather than the machine, so fitment is validated physically on a buck or vehicle rather than quoted as a single gap number.
How do you ensure fitment to my vehicle?
Fitment is validated in four steps: CAD alignment to your vehicle reference, a printed or CNC prototype mock-up, a physical dry-fit on a buck or vehicle, and a documented tolerance sign-off before production release. We do not rely on a generic "universal" fit claim for model-specific parts.
What should I send for a spoiler quote?
A drawing or 3D model with critical dimensions, the target material and finish, expected annual volume, mounting method, any regulatory market (EU/NA), and required documentation (PPAP, material certs, RoHS). The more the spec is defined, the tighter and faster the quote.
What tooling and volume options do you offer?
For low volume and pre-production we use CNC, 3D printing or bridge tooling; for frozen high-volume designs we build hardened steel production molds. MOQ is 1 piece for prototypes, so you can validate fit and finish before committing to production tooling.
What are the typical lead times?
Prototype parts typically run 3–7 working days, low-volume production 7–20 working days, and mass production 15–25 working days, depending on material, complexity, tooling status and order size. These are planning ranges confirmed per project, not fixed guarantees.
Do you provide inspection and material certificates?
Material certificates, RoHS test reports and first-article inspection (FAI) reports per AS9102 are available on request. We are ISO 9001:2015 certified; documentation packages and inspection reports can be provided under NDA.
Are you certified for automotive supply (IATF 16949)?
We are ISO 9001:2015 certified and work to IATF 16949 requirements (the standard that replaced ISO/TS 16949 in 2016) for automotive programs, including PPAP-style documentation on request. We do not claim an IATF 16949 certificate; we state the requirement level we support and the documents we provide.
Can you handle low-volume and prototype spoilers?
Yes. MOQ is 1 piece for prototypes, and bridge tooling or direct CNC/3D-printed routes cover pre-production without a full production mold. This lets you test market and fit before amortizing hardened tooling.
What is the minimum order quantity?
MOQ is 1 piece for prototypes. Production volumes run from low-volume batches into mass production under one ISO 9001:2015 quality system across all six core processes performed in-house.
Build your spoiler from sample to volume — in one quality system
Send your drawing or 3D model. We return a DFM review, a fitment plan and a quote that states the process, the tooling stage and the documentation — with no invented performance numbers.
Xiamen Goldcattle Plastic & Metal Products Co., Ltd. · Founded 1998 · OEM/ODM custom manufacturing