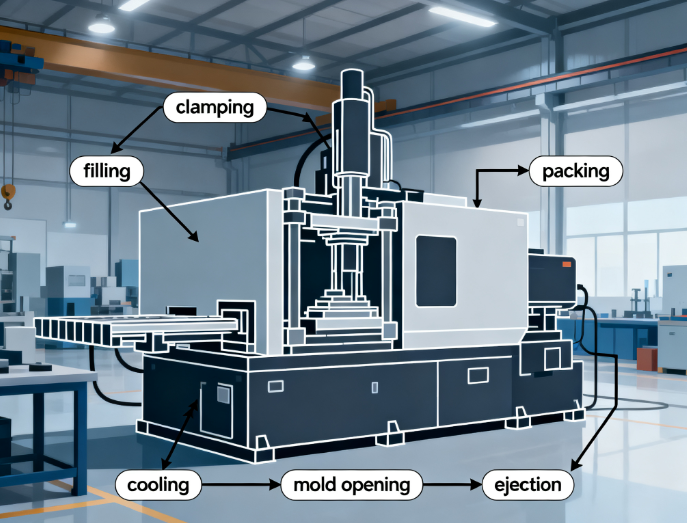
Injection mold manufacturing converts part geometry, material and production requirements into a tool that can make the plastic part repeatedly. The process runs from drawing review and DFM, through mold design, steel selection, CNC machining, EDM, assembly and trial molding, to sample inspection and approval. This guide explains each stage, what drives mold cost and lead time, and the decisions buyers confirm before tooling starts.
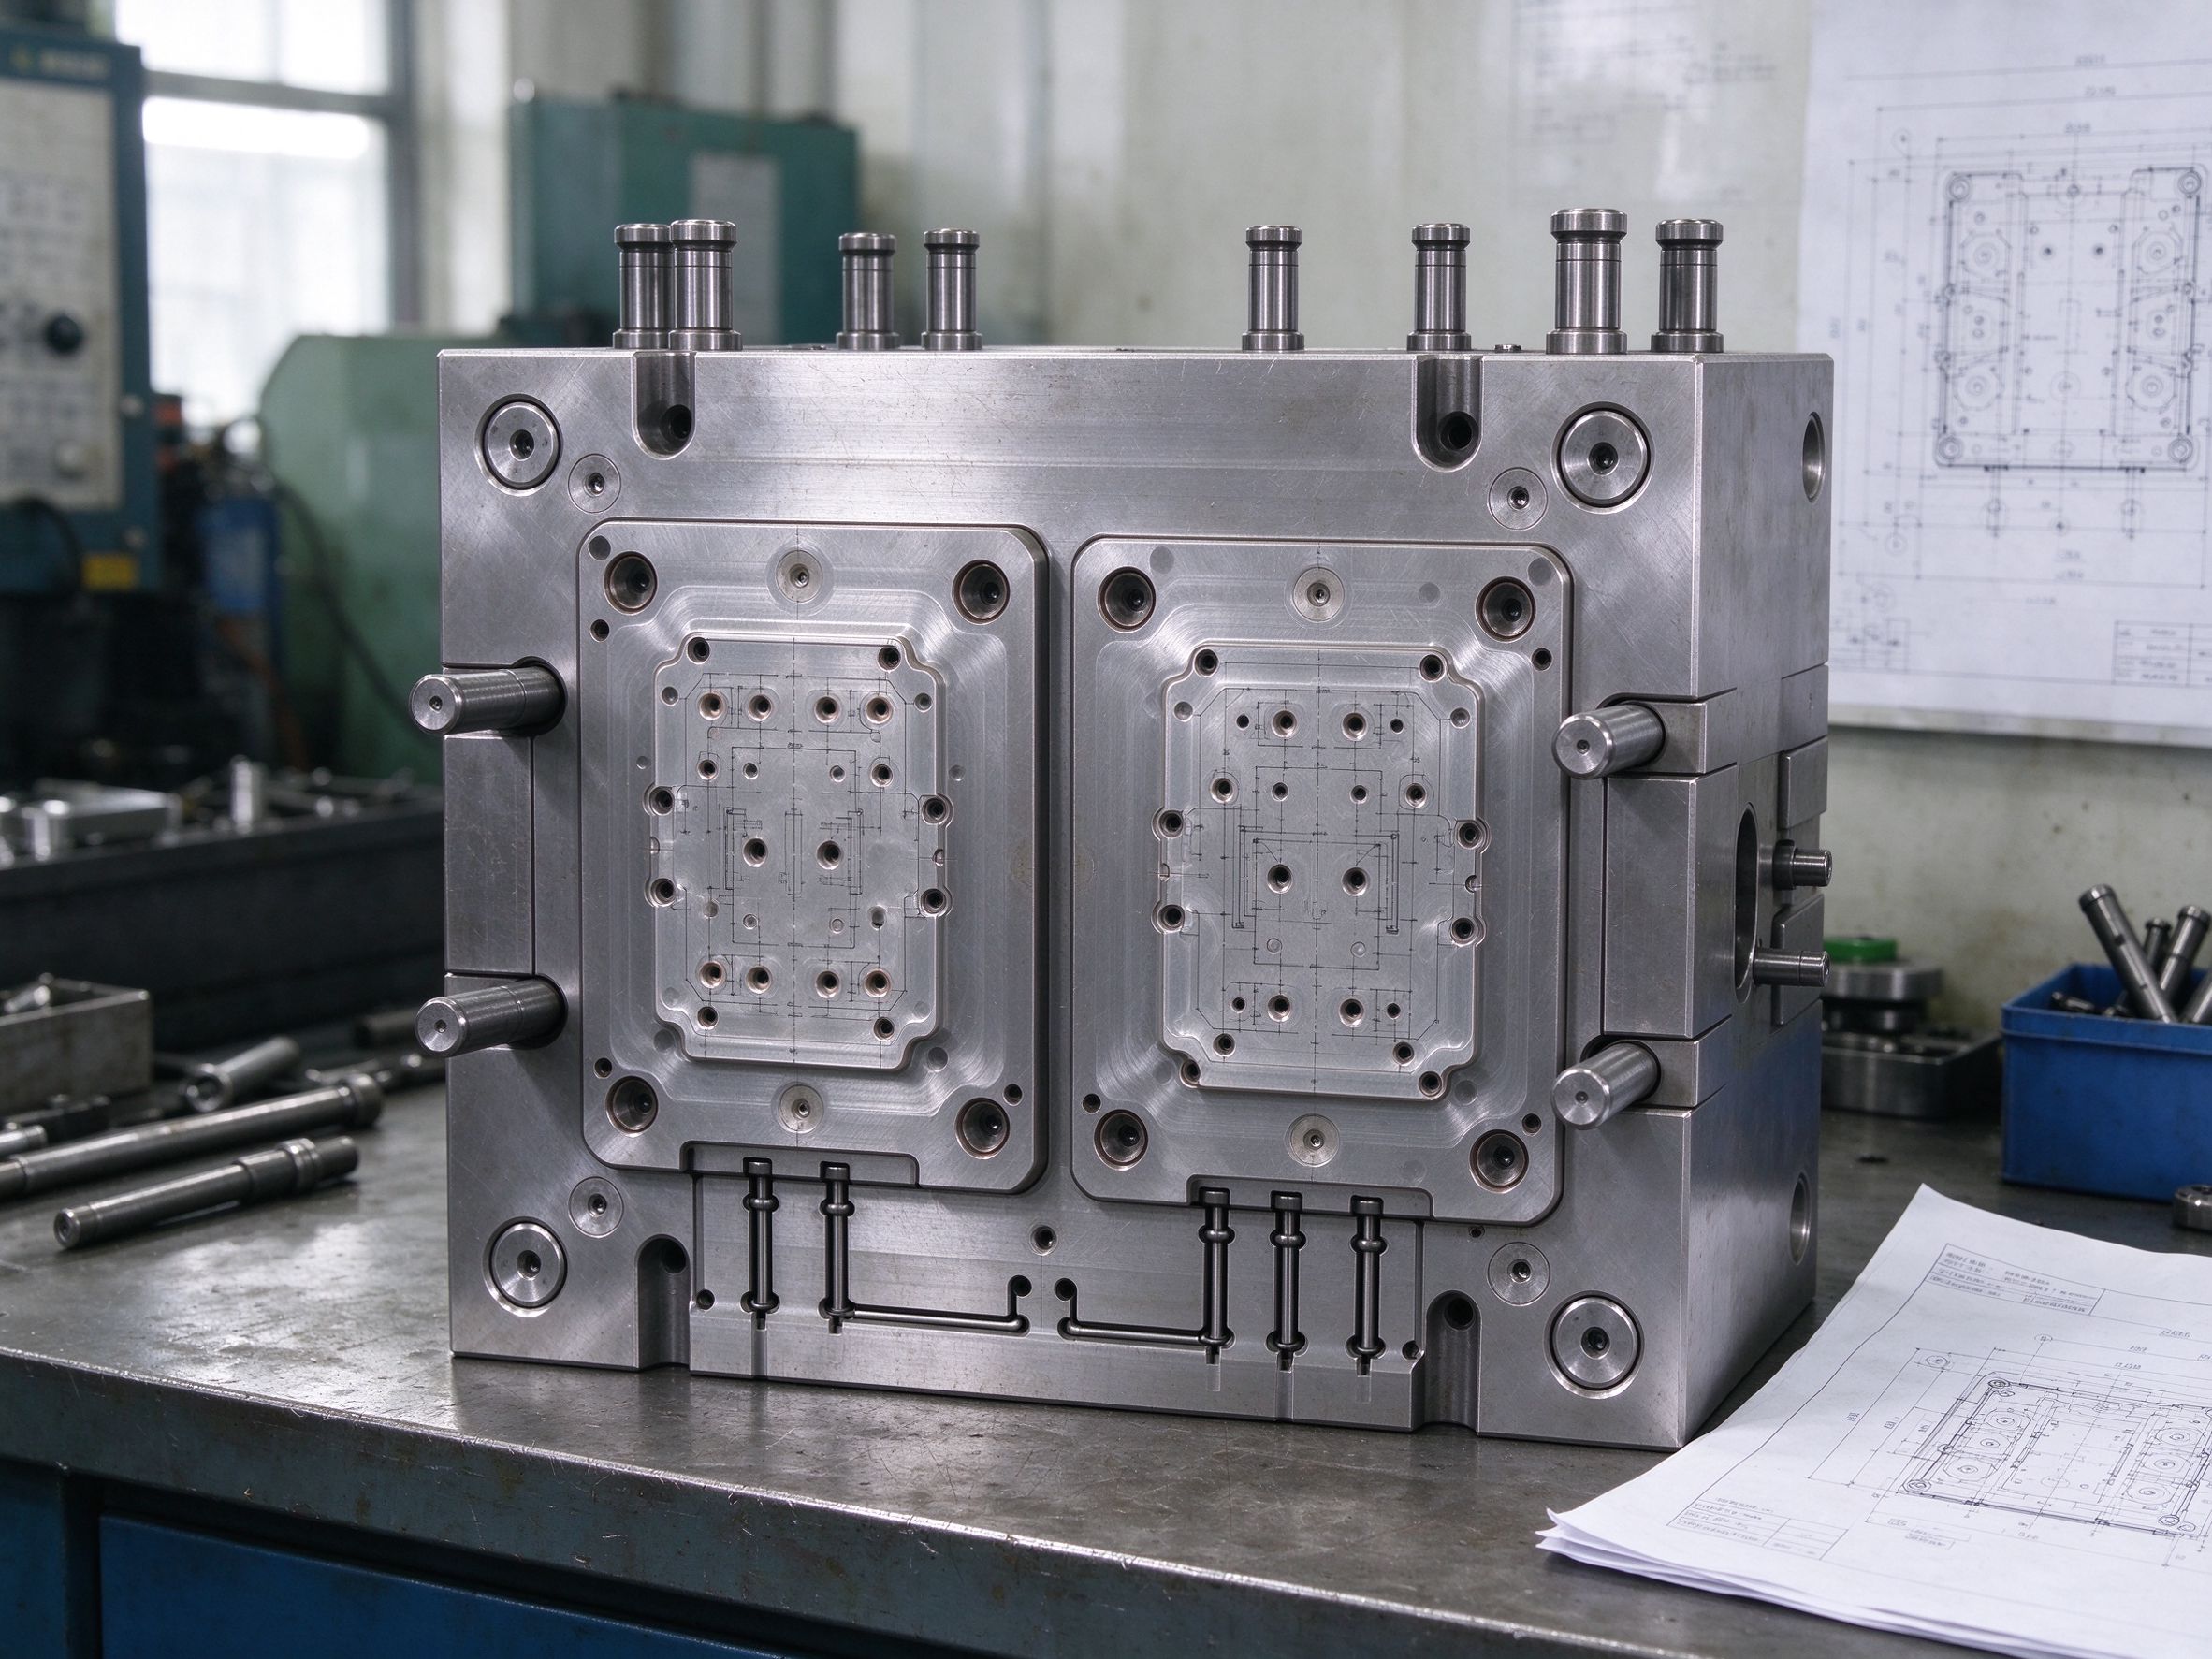
Plastic injection molds are manufactured through a controlled chain: drawing review and DFM, mold structure design, steel selection, CNC machining with EDM where required, fitting and assembly, trial molding, sample inspection, mold modification and final approval. Each stage has an output that the next stage depends on. Design decisions made early — draft, wall thickness, undercuts, gate location, cooling and ejection — affect machining difficulty, mold cost and the quality of the parts the mold will produce. A mold is approved only after trial samples meet the agreed dimensional, appearance and function checks.
Mold Manufacturing vs. Injection Molding
Two different scopes are often sold together:
- Mold manufacturing — mold design, machining of mold parts, assembly and trial molding. The output is the tool.
- Injection molding — using the mold to shape plastic material into parts in production. The output is the part.
Some suppliers only build molds; others also run production. Confirm the scope with the supplier: what is quoted, what the mold is verified against, and who runs production once the mold is approved.
The Plastic Injection Mold Manufacturing Process
Part geometry, material, volume and quality requirements are reviewed against moldability. Design changes that avoid tooling complexity are identified before any cutting.
Cavity layout, gate and runner, cooling, ejection and side actions are defined into a mold design that fits the part and press.
Mold base, cavity steel, hardness target and surface requirement are set against expected production volume and resin.
Cavity and core geometries are machined; EDM handles deep ribs, small radii and features cutters cannot reach.
Mating surfaces, parting lines and cavity surfaces are fitted and finished to the required condition.
Mold is assembled on the press and trialed with the target resin to check filling, cooling, ejection and part quality.
First samples are measured against the drawing; defects are recorded, the mold is modified, and trial results are re-verified.
Approved mold, trial records and maintenance guidance transfer to production, with repair and modification support as agreed.
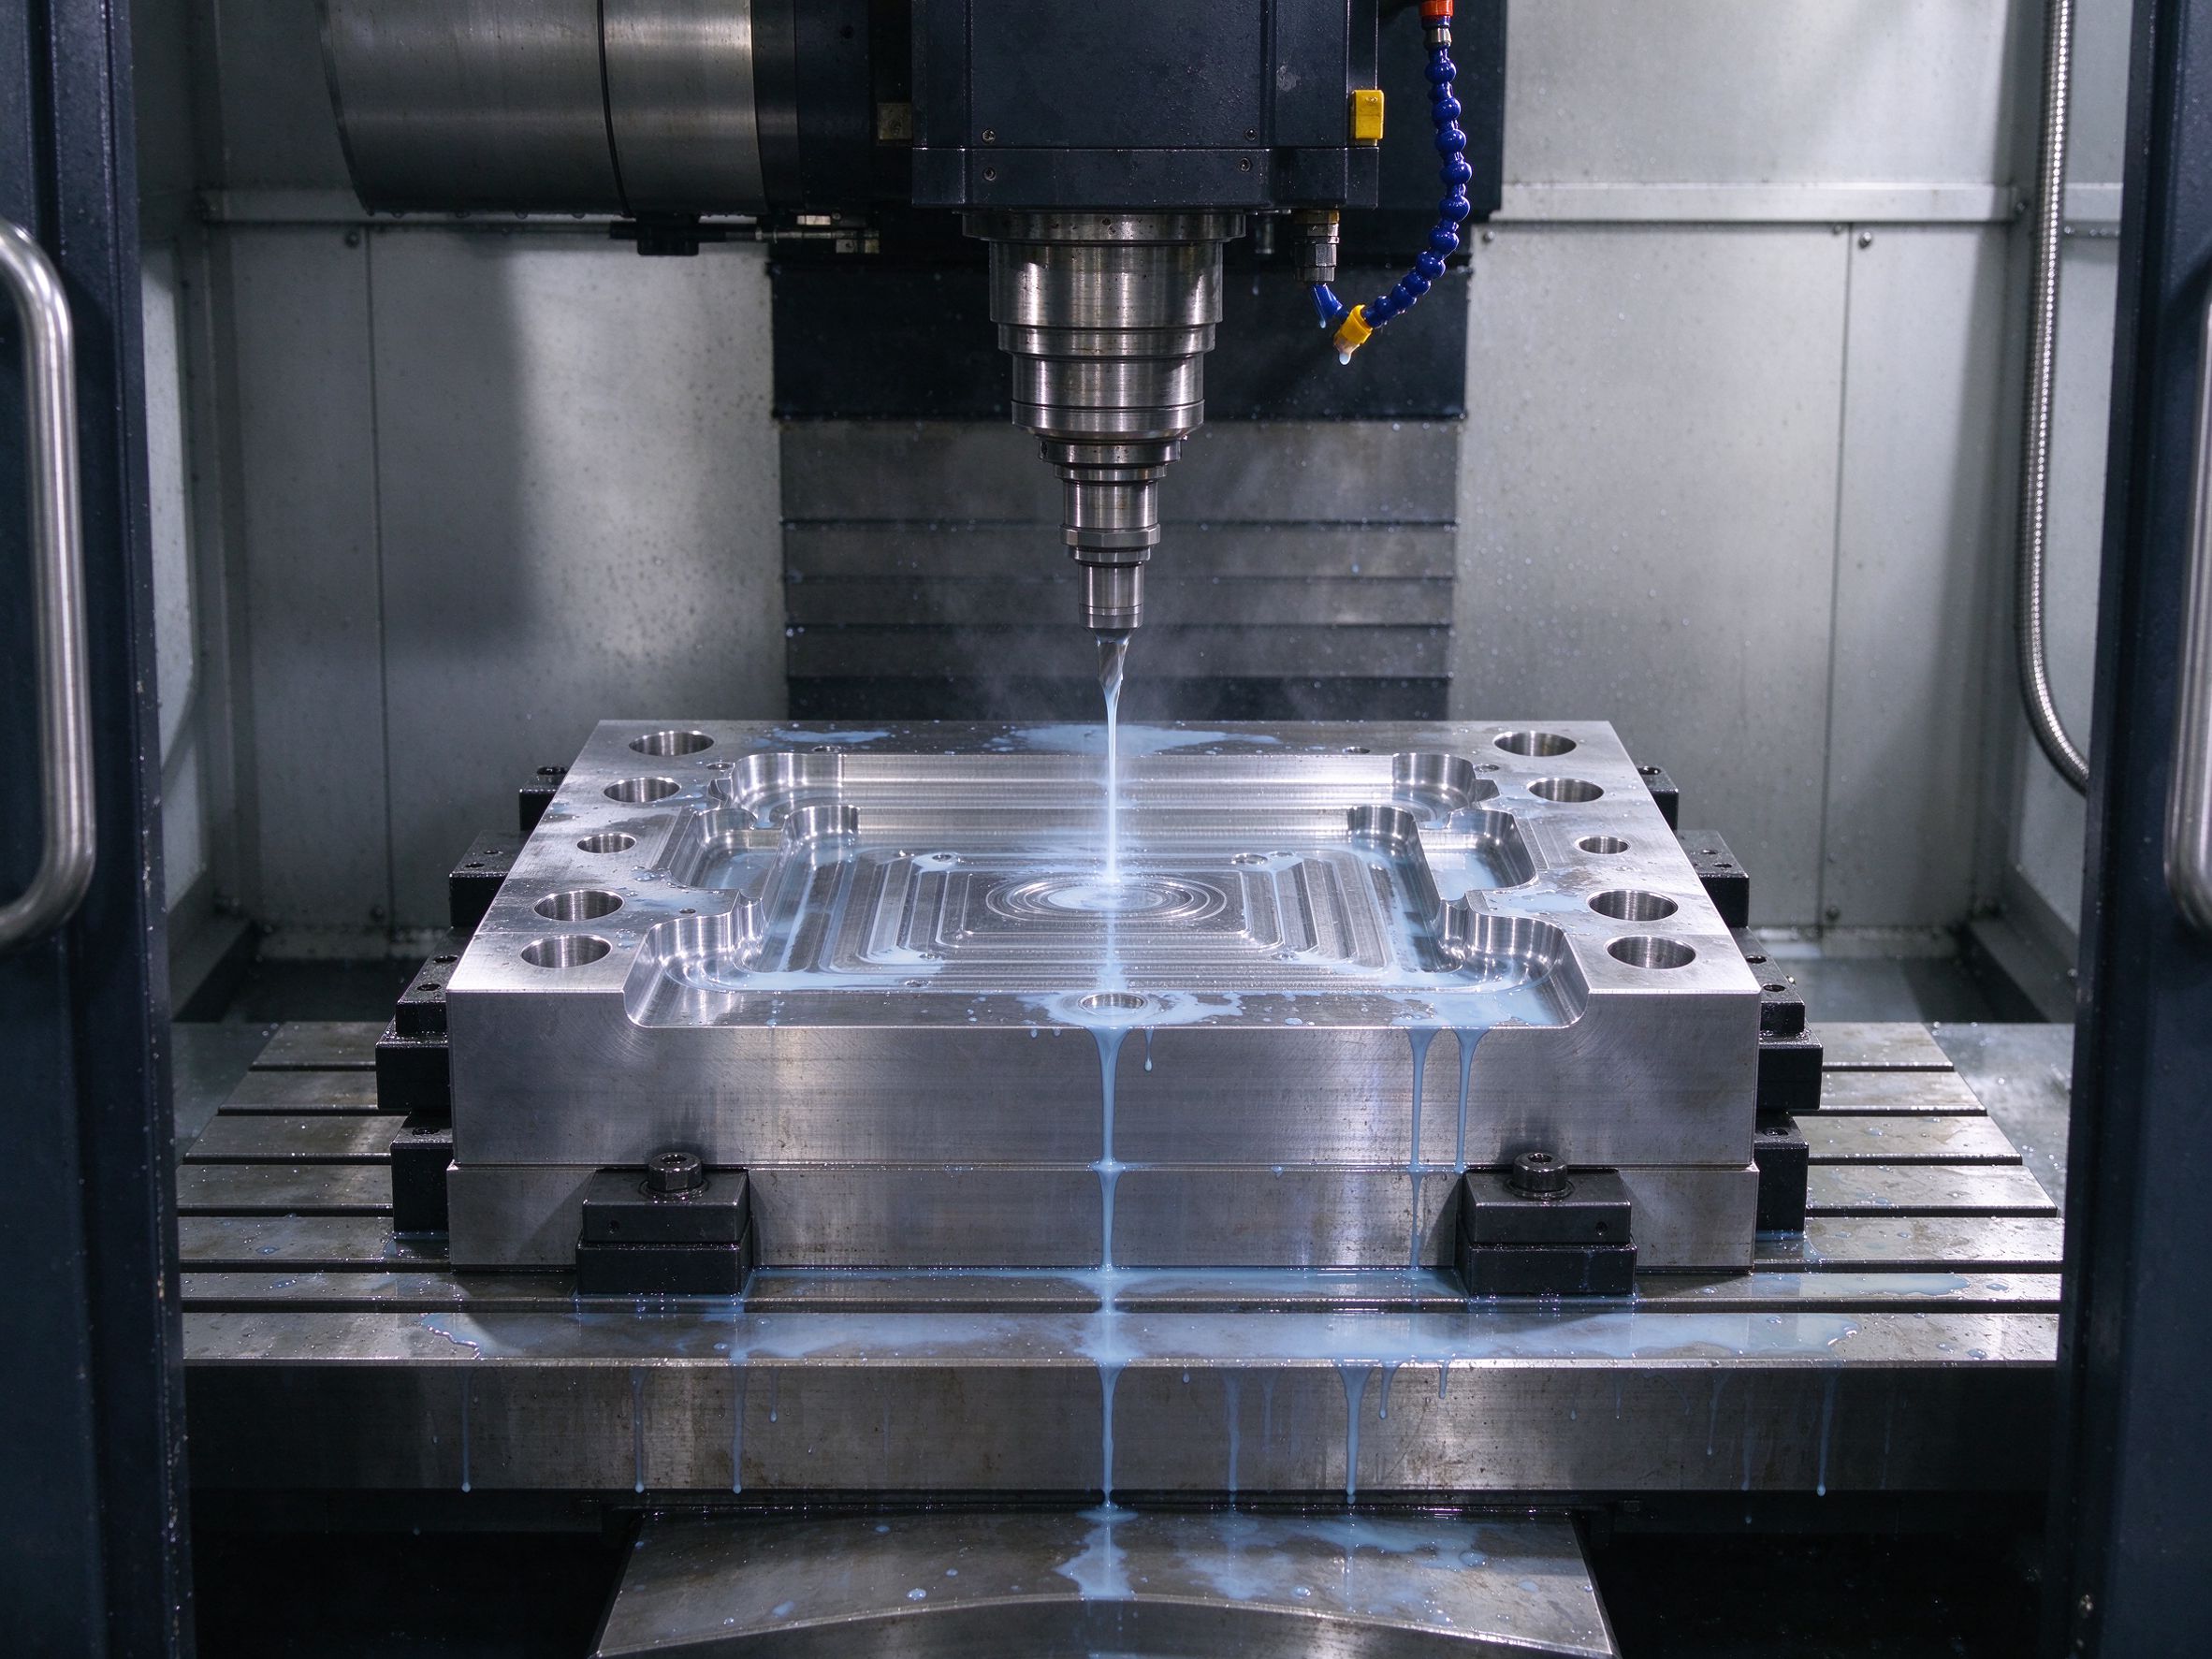
Key Components of an Injection Mold
| Component | What it does |
|---|---|
| Core and cavity | Define the plastic part's main geometry |
| Mold base and alignment | Provide structure, support and plate alignment |
| Gate and runner system | Control how melt enters and fills the cavity |
| Venting | Let trapped air escape during filling |
| Cooling channels | Affect cooling efficiency, cycle time and part stability |
| Ejection system | Push the finished part out of the mold |
| Slides and lifters | Form undercut features where the design needs them |
Each of these affects cost, manufacturability and part quality. A simple design may not need slides or hot runners; a complex one will. The mold structure is matched to the part, not maximized.
How to Choose Mold Steel and Tooling Type
| Consideration | Aluminum tooling | Steel tooling |
|---|---|---|
| Typical fit | Lower volume, faster lead, prototypes, early validation | Higher volume, longer life, tighter wear resistance |
| Advantage | Quicker to machine, lower initial cost in suitable designs | Wear resistance, dimensional stability over long runs |
| Limit | Wear and damage risk in high-volume or abrasive resins | Longer machining time, higher tooling cost |
The choice is not a fixed rule ("aluminum for prototypes, steel for production only"). It is evaluated on production volume, target life, resin type, surface requirements, geometry and delivery plan. Steel grade, heat treatment and surface finishing are specified for the application, and confirmed in the quote.
Design for Manufacturability: What Makes a Mold Easier to Build
- Draft angles — enough draft eases ejection and reduces surface drag marks.
- Wall thickness and transitions — even walls fill and cool more predictably; abrupt changes create stress and sink.
- Ribs and bosses — proportions that avoid sink marks while keeping stiffness.
- Undercuts — side actions add cost and cycle; avoidable undercuts are simplified in DFM.
- Gate placement — gate position shapes weld lines, flow marks and stress points.
- Parting lines, tolerances and finish — the parting line location and surface finish class are agreed before machining.
DFM values are engineering guidance with application conditions — they are not universal standards that apply to every resin and geometry. The review states what is being changed and why, so the buyer sees the trade-off.
What Affects Injection Mold Cost and Lead Time
| Cost drivers | Lead time drivers |
|---|---|
| Mold size and structure complexity | Design freeze and engineering review |
| Cavity count | Material and standard-part procurement |
| Steel grade and heat treatment | Number of machining operations |
| Slides, lifters and side actions | Heat treatment schedule |
| Hot runner or special gating | Mold assembly and fitting |
| Surface finish and texture | Trial molding and modification rounds |
| Dimensional and inspection requirements | Re-verification after each mold change |
No fixed price or universal lead time is quoted here. A serious quote lists the assumptions: geometry, steel, cavities, features, surface, inspection scope and trial rounds. Compare quotes on those assumptions, not on the headline number.
Mold Trials, Sample Inspection and Production Validation
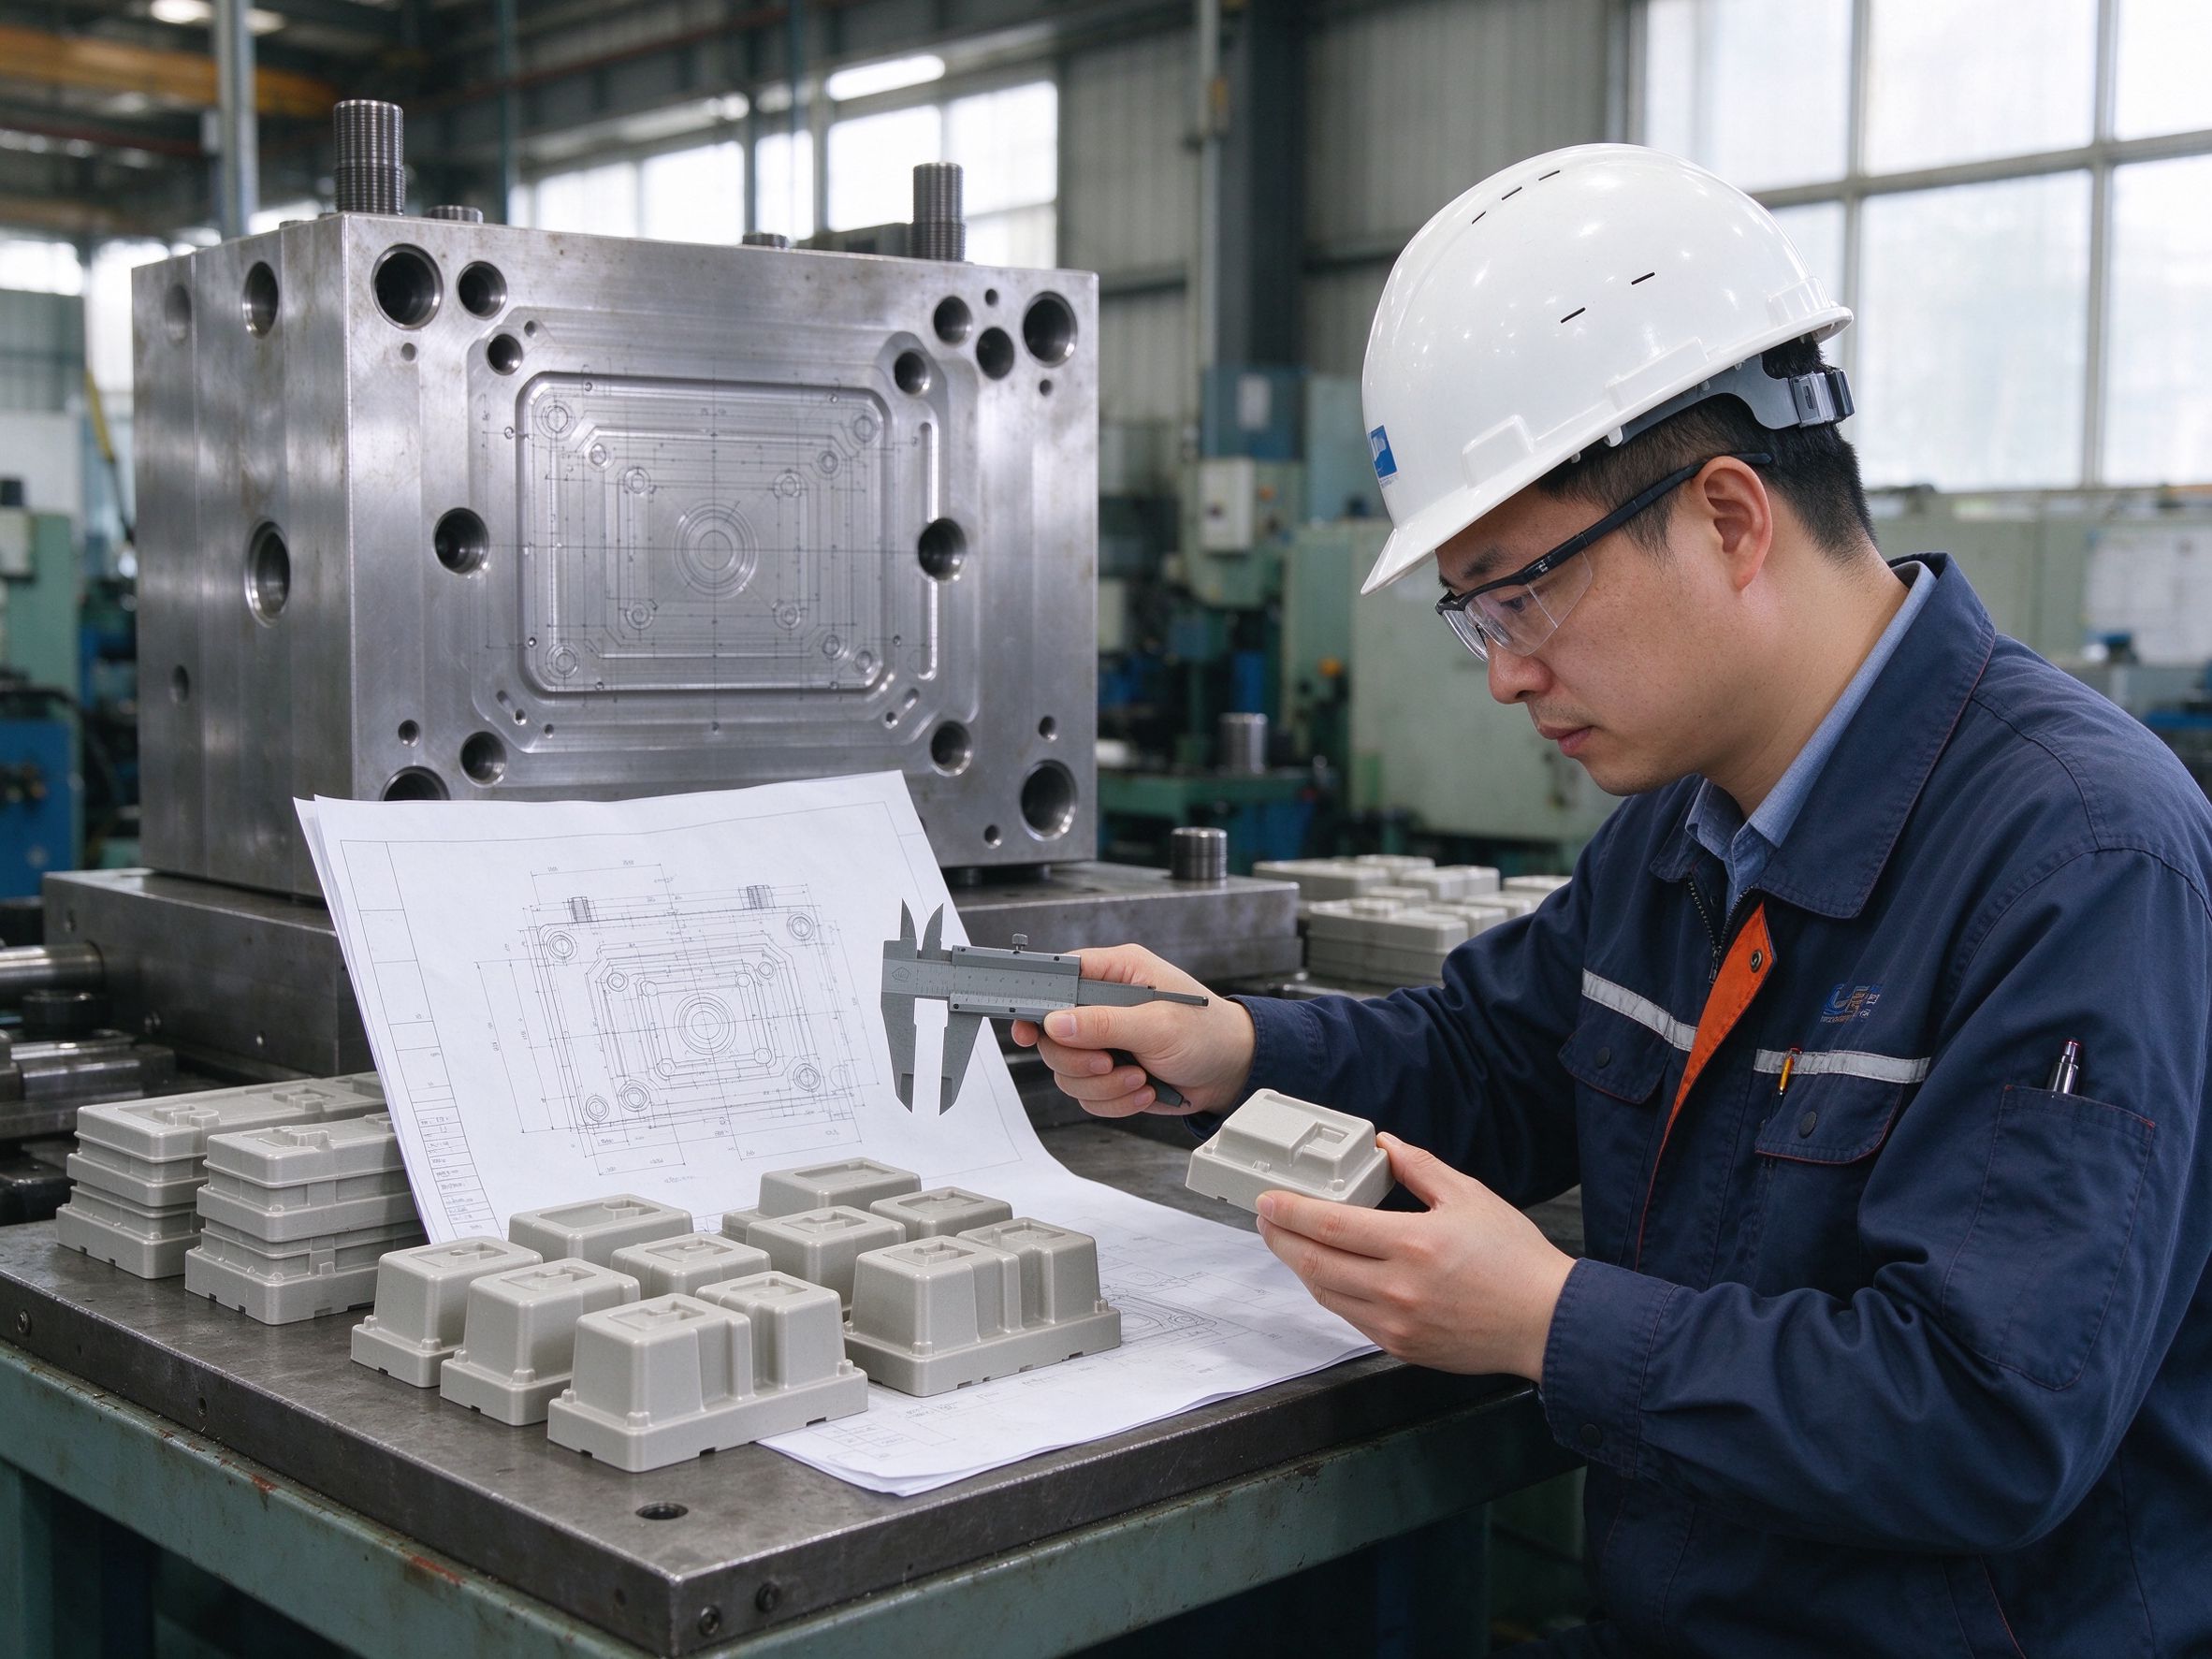
Trial molding exists to prove the mold can make parts to the agreed standard. The purpose of a trial round is to check material behavior, filling, cooling, ejection, dimensions, appearance and function — then record what needs modification and verify it in the next round.
- Material and trial conditions are recorded with the run.
- Dimensions are measured against the drawing on first samples.
- Appearance defects — flash, short shot, sink, flow marks, weld lines — are logged with locations.
- Modifications are listed per issue, and the mold is re-verified after each change.
- Approval criteria (dimensions, appearance, function) are agreed before the trial, so both sides judge the same result.
Labels such as T0 and T1 are used consistently inside each project's workflow; a trial number describes the round, not a guarantee that the mold already meets every production requirement.
Mold Ownership, Maintenance and Project Handoff
For overseas buyers, the following points should be confirmed in the order or purchase agreement before payment:
- When mold ownership transfers, and what it covers — plates, inserts and auxiliary assets.
- Which engineering files and inspection records are delivered with the mold.
- Usage limits, confidentiality and maintenance responsibility.
- Repair, modification, storage and periodic inspection arrangements.
- Mold retrieval, packing and cross-border shipping at project end.
These are written as a purchasing checklist. Paying for a mold does not automatically transfer every file and all IP — the terms are what the agreement says.
How to Evaluate a Plastic Mold Manufacturer
A useful audit covers the ability to design, machine, assemble and validate — not just the brochure:
- Actual equipment and machining capability, confirmed with process photos and shop visits
- Mold design documentation and engineering review output
- Trial and sample validation records with measurements
- Quality records and inspection capability
- Maintenance and modification support
- Lead time communication and change management
- Ownership, confidentiality and IP terms in writing
Goldcattle builds injection molds and runs production under one roof. For commercial mold procurement — capabilities, specifications, cases and quoting — see injection mold manufacturing →.
Frequently Asked Questions
What is plastic mold manufacturing?
What are the main steps of injection mold manufacturing?
What is the difference between mold manufacturing and injection molding?
Should I choose an aluminum or steel mold?
What affects the cost of an injection mold?
What causes mold manufacturing delays?
How are injection molds tested before production?
Who owns a custom injection mold after payment?
What information is needed to request a mold quote?
Request a Mold Manufacturing Review
Send the part drawing, resin, annual volume and surface requirements. The review covers DFM, mold structure, steel choice, cost drivers and trial validation scope before the quote is issued.
Xiamen Goldcattle · Manufacturing since 1998 · Injection mold making and custom CNC machining · Related: injection mold manufacturing → · injection molding services →