Sandwich injection molding — also called co-injection — forms a skin-core structure inside one molded part: a skin material makes the outer layer, and a different core material fills the interior. The value is a controlled material split inside a single part: premium surface with a lower-cost or functional core, selected barrier properties, or recycled content where the application allows. Feasibility depends on the material pair, melt-flow behavior, skin-to-core ratio, mold design, injection sequence and the required surface and mechanical performance.
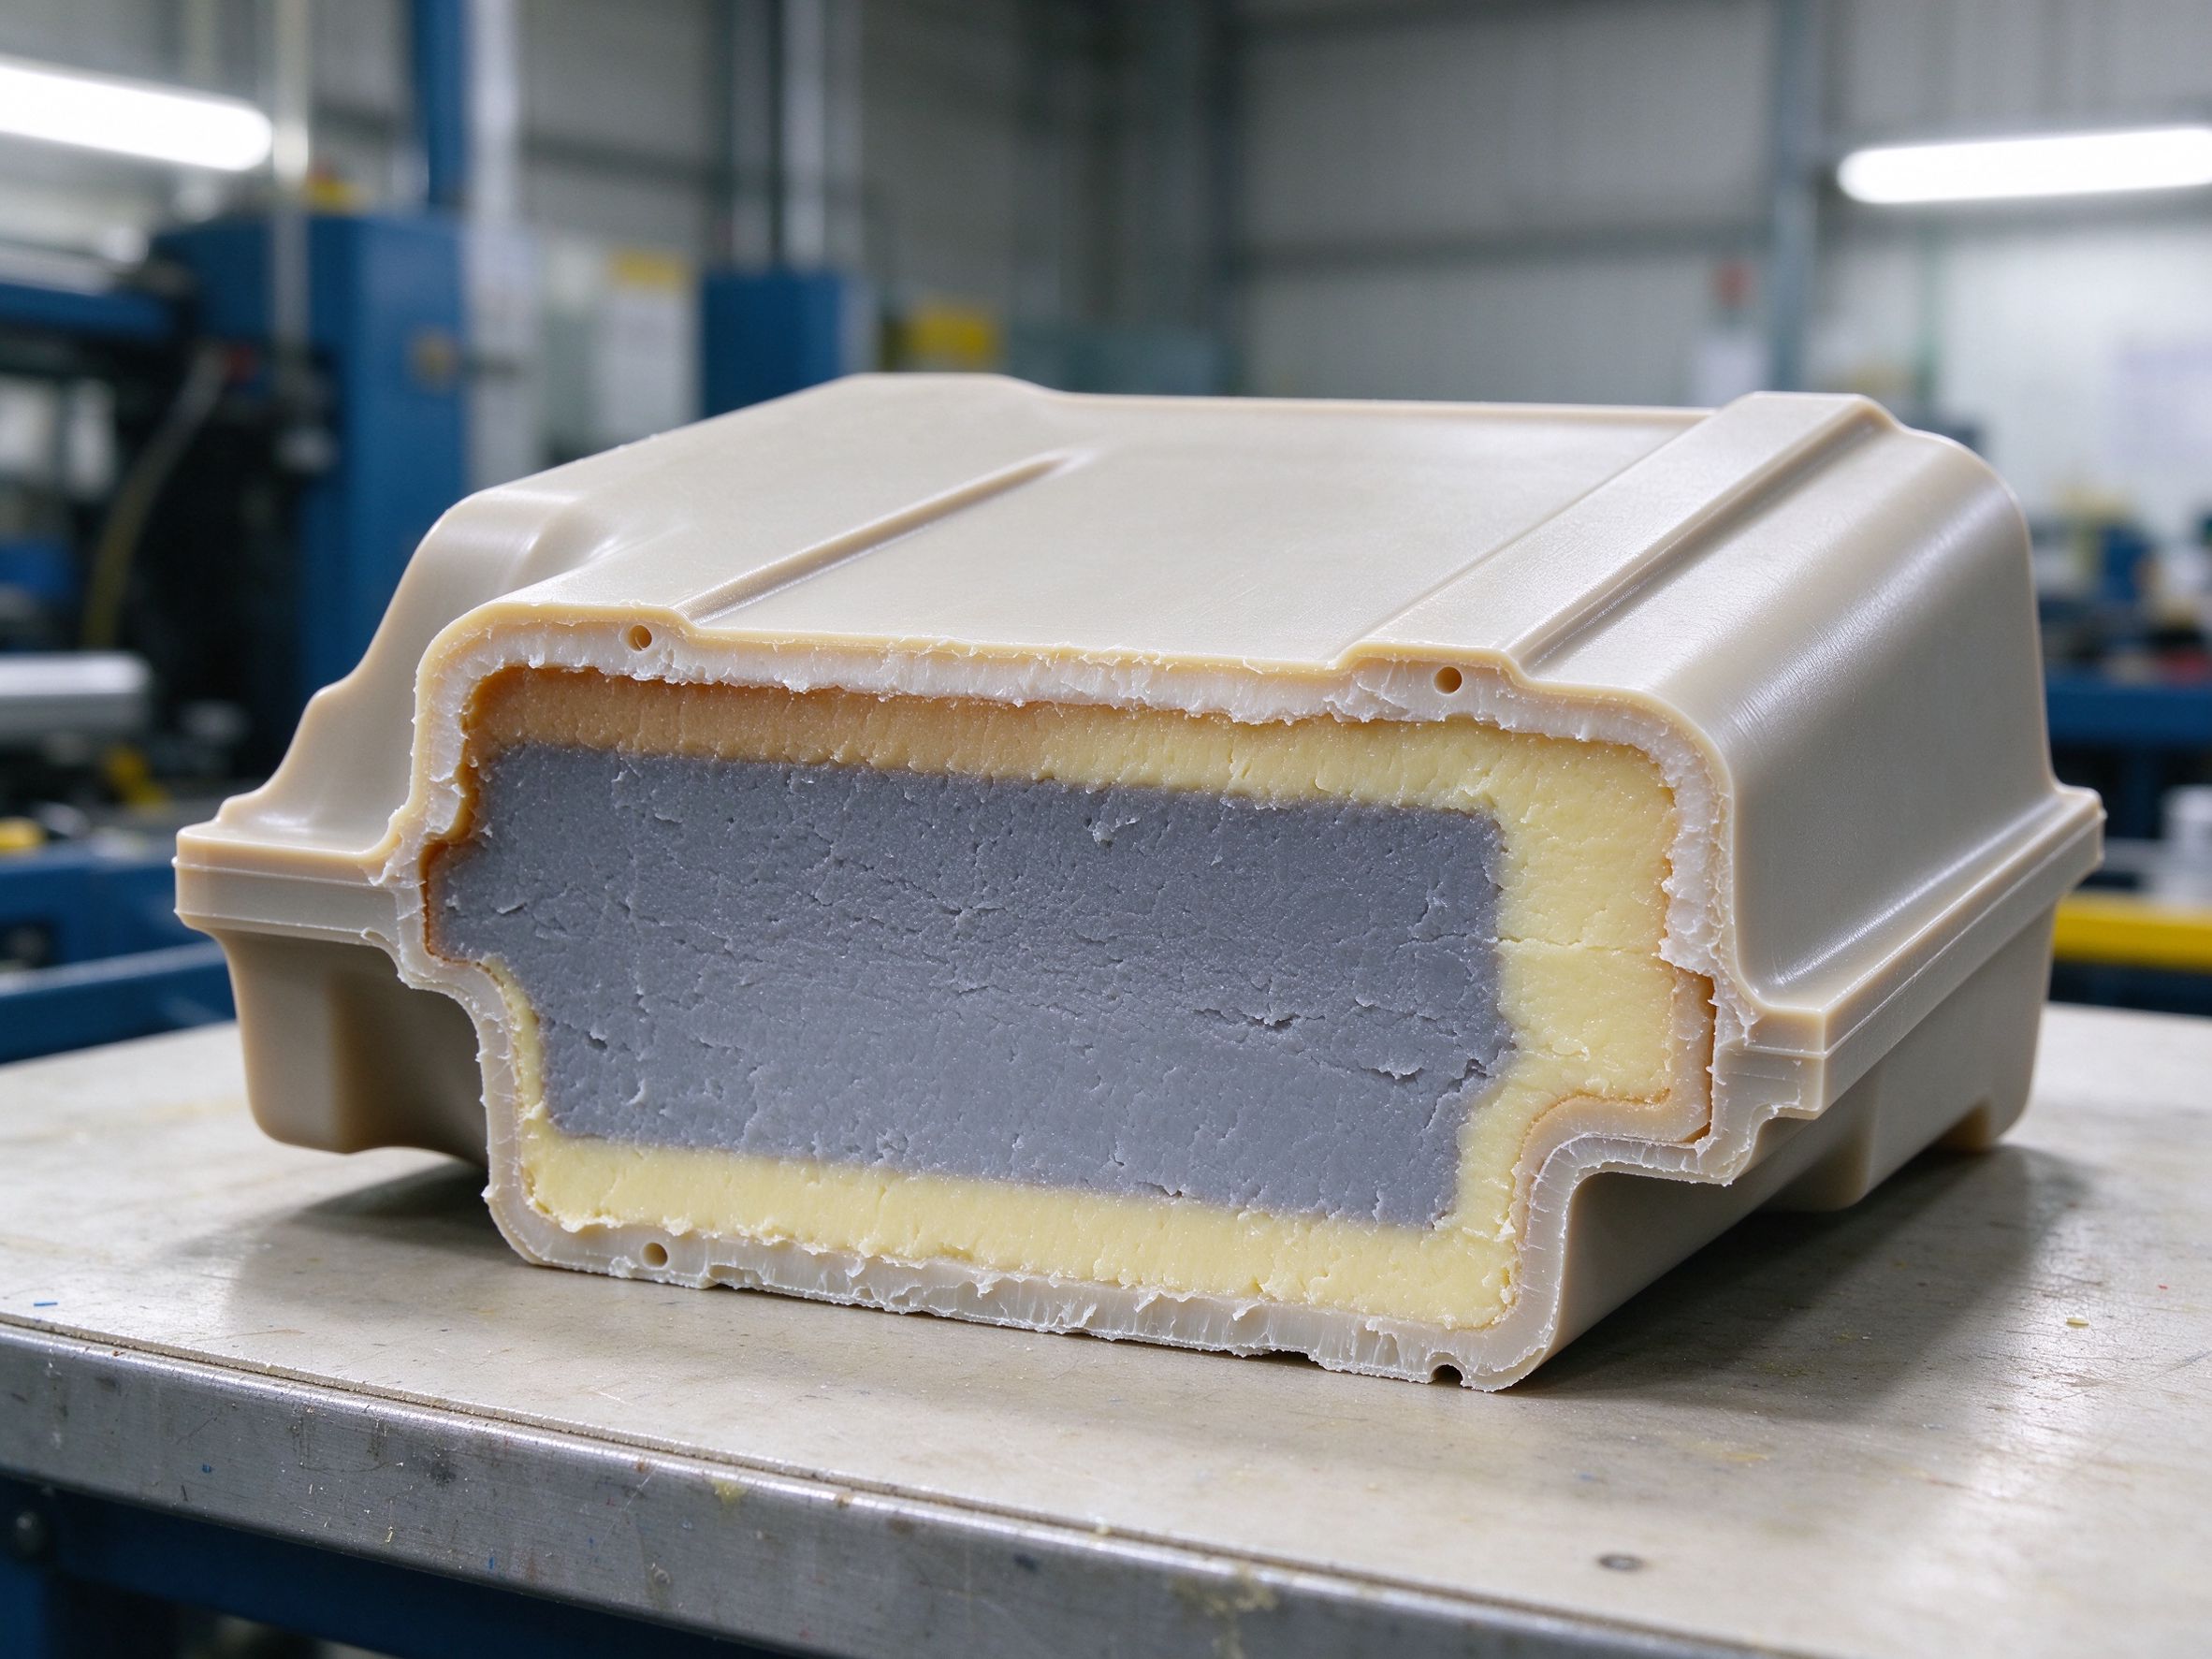
Sandwich molding suits parts where a controlled skin-core split adds real value: premium surface with a lower-cost, recycled, foamed or functional core. It is not simply "two plastics in one part." The skin must stay continuous, the core must distribute evenly, and the material pair must run in one processing window. Feasibility is confirmed by engineering review and samples, not by the process name alone. Where Goldcattle does not hold dedicated co-injection equipment, the review still applies — the manufacturing route is confirmed per project before quoting.
How Sandwich Injection Molding Works
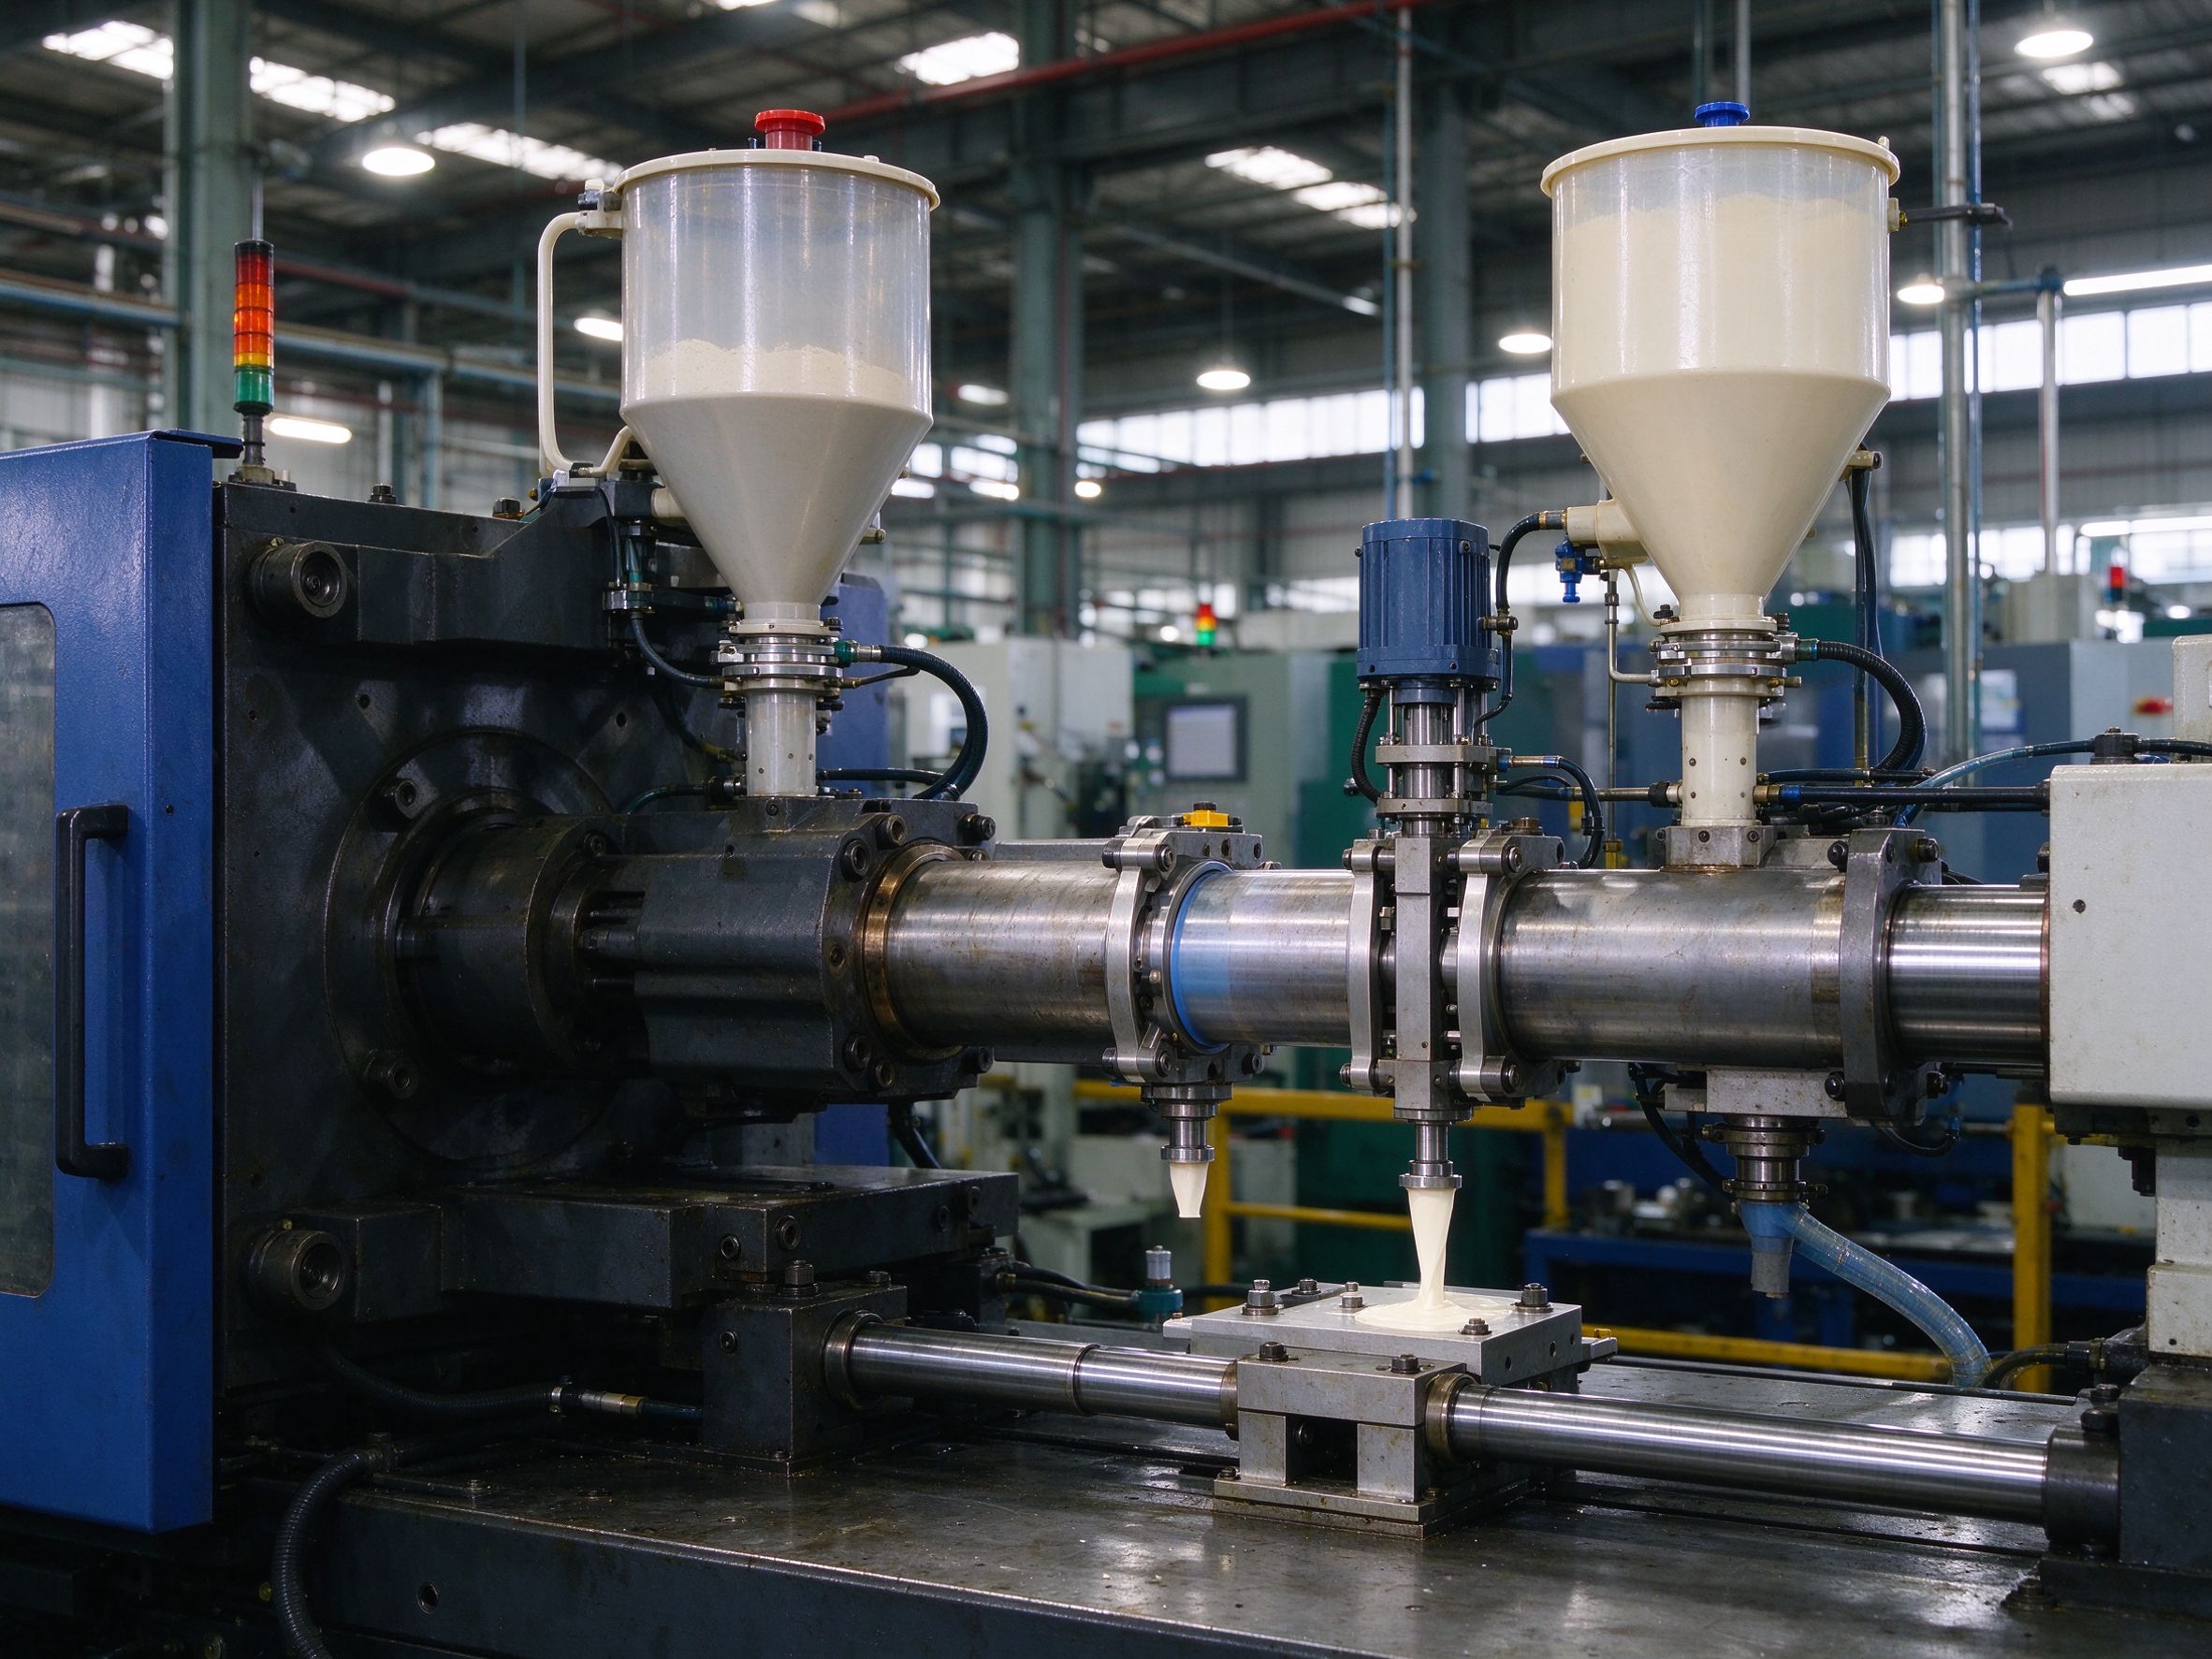
- Skin injection — the skin material fills the cavity and forms a continuous outer layer against the mold surface.
- Core injection — the core material follows through the same or a second nozzle and fills the interior behind the skin layer.
- Skin closing — a final skin push seals the core inside, so the core does not show on the surface.
- Ejection — the part exits as one piece with a skin-core structure.
The result is a Skin–Core–Skin cross-section. Layer thickness is not a fixed value — it depends on the material pair, part geometry, injection sequence and processing conditions. That is why section checks and core-distribution validation matter.
Sandwich, Co-Injection, 2K, Overmolding: Not Synonyms
| Process | How the structure forms | Why buyers choose it |
|---|---|---|
| Sandwich / co-injection molding | Skin and core materials distributed inside one part during molding | Surface performance with different interior material, cost or function |
| Two-shot / 2K molding | Two materials or colors formed in sequence in one integrated system | Two-material parts, two-color appearance, reduced assembly |
| Overmolding | Second material overmolded onto an already formed substrate | Soft touch, sealing, cushioning, protection |
| Gas-assisted molding | Pressurized gas creates a controlled cavity or channel during injection | Weight reduction, material savings in suitable structures |
Industry terms overlap — some sandwich processes sit inside co-injection and multi-component molding families. The page separates them by how the structure forms, not by the number of materials used.
Applications Worth Evaluating
Quality skin + recycled core
Returnable containers, industrial boxes, pallets, some household products. Verify skin continuity, recycled-material stability, mechanical properties and batch consistency.
Barrier or functional core
Selected food packaging, containers, preforms. Food contact, barrier effect and regulation compliance are confirmed by material and finished-part validation, not assumed from the sandwich structure.
Cost and stiffness balance
Furniture parts, thick-wall structures, industrial and logistics components. Low-cost or filled cores are evaluated against appearance, stiffness, impact and dimensional requirements.
Appearance with material split
Some automotive interiors, equipment housings, consumer parts. Core exposure, flow marks and color anomalies on visible surfaces are checked explicitly.
These are directions to study, not a claim that Goldcattle currently runs food-contact, barrier or large-structure sandwich production. The application fit is assessed from your part, materials and acceptance requirements.
Skin and Core Material Selection
Start from what the skin must do and what the core should carry, not from a ready-made material list.
| Skin objective | Core candidates | Engineering checks |
|---|---|---|
| High-quality surface and durability | Applicable low-cost recycled resin | Color difference, skin continuity, core exposure, mechanical performance |
| Specific barrier property | Barrier resin matched to skin and use | Barrier layer distribution, continuity, thickness, final product validation |
| Stiffness or structural function | Applicable filled or reinforced engineering core | Flow, layer distribution, shrinkage, mechanical behavior |
| Weight and density target | Applicable foamed core system | Core structure, appearance, weight, functional performance |
A stable skin-core structure needs resin grades with matched processing temperatures and compatible melt viscosity, plus a mold design that controls distribution. Candidate pairs are reviewed from supplier data, specific grades, processing conditions and the use environment — samples validate the layer structure before tooling is finalized.
Core Breakthrough and Other Risks
| Risk | What to review | Verification direction |
|---|---|---|
| Core breakthrough | Skin-core ratio, material viscosity, flow timing, local geometry | Cross-section, surface continuity, material distribution check |
| Uneven core distribution | Gates, runner, cavity geometry, multi-cavity balance | Cross-sections at different locations or suitable internal inspection |
| Flow marks / visible transitions | Injection switching, skin material, process parameters | Appearance standard, samples, key surface verification |
| Warpage / dimensional variation | Shrinkage difference between materials, cooling, layered structure | Dimensional measurement, warpage check, functional tests where required |
| Incomplete encapsulation | Injection sequence, core position, closing stage | Section check, skin continuity in critical areas |
These risks are why sandwich molding cannot be approved from a drawing alone. Section inspection and core-distribution evidence are part of the validation plan, not an option.
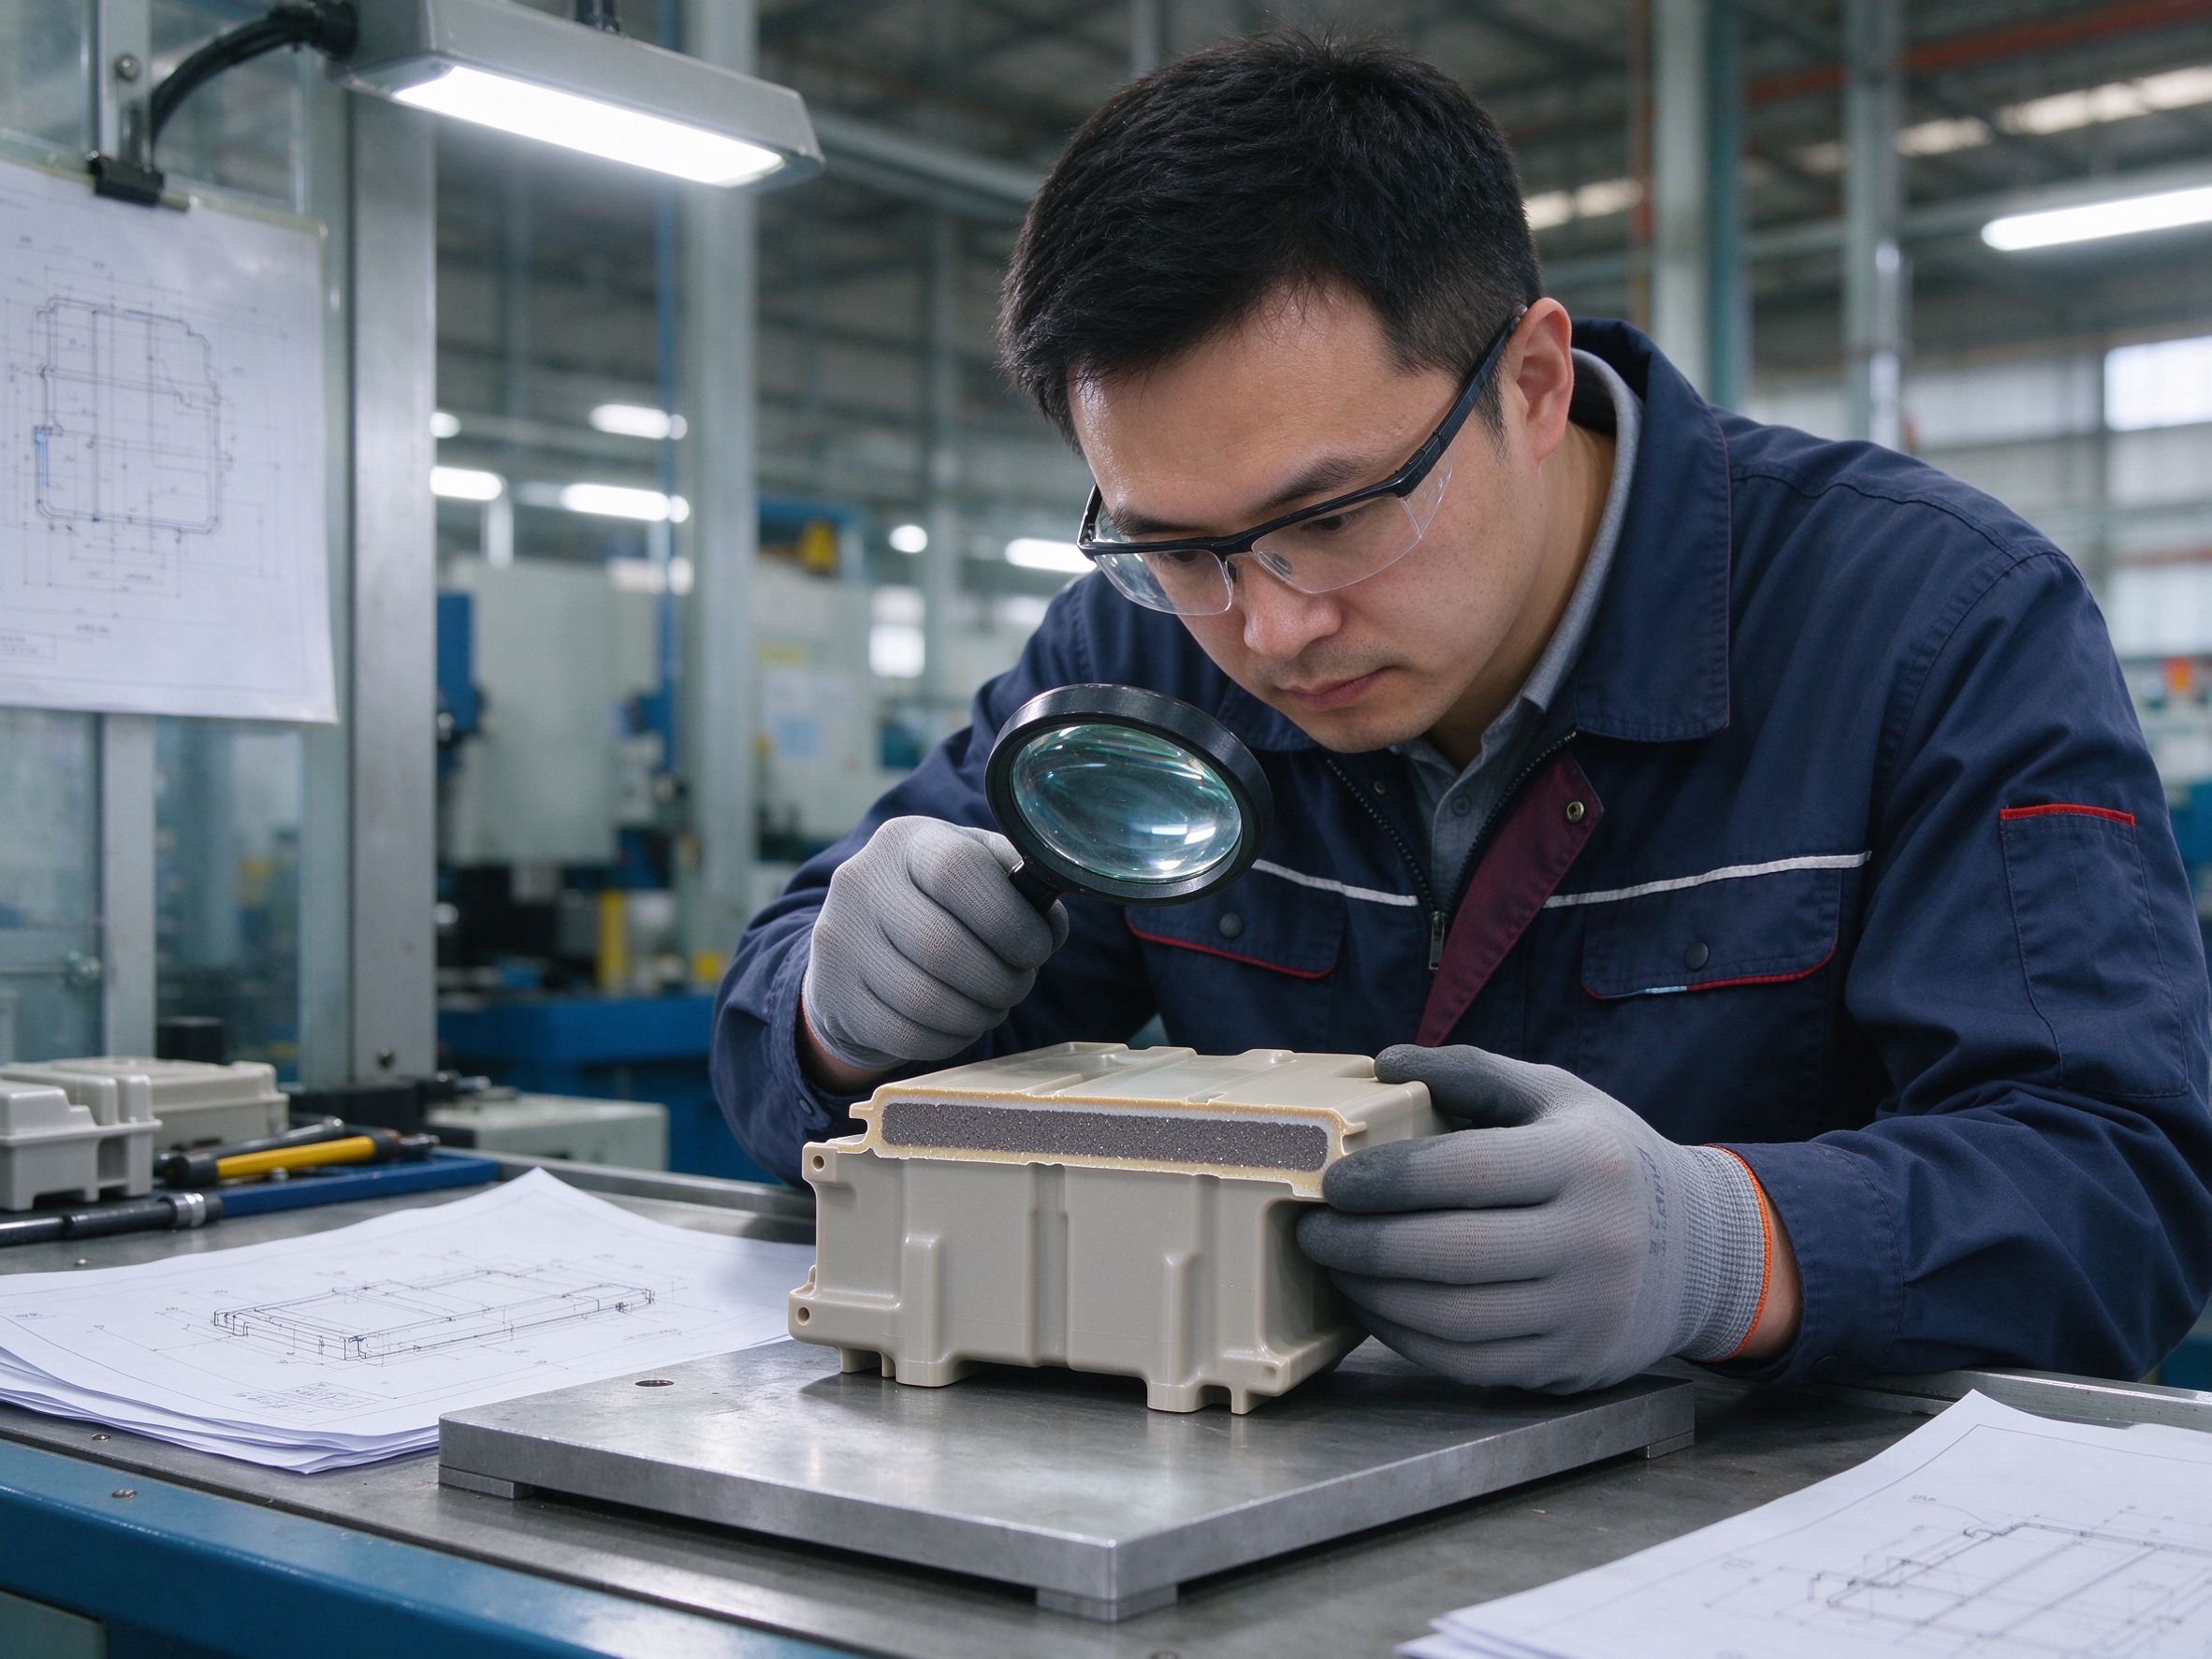
Validation: What the Part Must Prove
- Skin continuity — no core breakthrough on visible or functional surfaces.
- Core ratio and distribution — measured against the agreed target at representative locations.
- Dimensional check — critical dimensions and warpage against the drawing.
- Appearance — color, flow marks and surface quality to the agreed standard.
- Mechanical or barrier function — tested to the application requirement when specified.
- Batch consistency — material records, first-article reports and process documentation as agreed.
Cost and Process Selection
| Route | Look at it when | Main trade-off |
|---|---|---|
| Conventional molding | One material meets all requirements | Simple tooling and process, but no skin-core material split |
| Sandwich / co-injection | Skin performance plus a different interior material | Potential material or performance gains, but specialized process, tooling and validation |
| Two-shot / 2K | Two materials in separate functional or color zones | Mold structure, positioning, material compatibility, cycle time |
| Overmolding | Functional layer over an existing substrate | Substrate handling, interface, second-stage tooling |
| Gas-assisted molding | Controlled cavity in a specific area | Gas control, channel design, tooling investment, structure validation |
| Structural foam molding | Density reduction through a foamed structure | Foaming system, surface quality, process trade-offs |
The economical route is decided under one set of assumptions: tooling cost, material cost, cycle, yield, inspection, secondary operations and lifecycle volume. Sandwich molding is not automatically cheaper than conventional molding, and recycled content is not automatically acceptable for every application.
How to Verify a Sandwich Molding Supplier
Because much of the public content on this process comes from equipment makers, confirm the shop's own capability before quoting:
- Dedicated multi-component injection unit or co-injection nozzle, or a documented partner route
- Mold designs that sequence skin, core and closing stages
- Trial records and core-distribution validation from real parts
- Material grade records for the skin-core pairs actually processed
- Section, surface, dimensional or function reports from previous projects
Goldcattle reviews sandwich molding feasibility from your CAD, materials and requirements. Where dedicated co-injection equipment is needed, the manufacturing route is confirmed and stated per project rather than presented as standing in-house capability.
Frequently Asked Questions
What is sandwich injection molding?
Is sandwich molding the same as co-injection molding?
What is the difference between sandwich molding and two-shot molding?
Can sandwich molding use recycled core material?
How do you prevent core breakthrough?
How much does sandwich injection molding cost?
How can core distribution be inspected?
Submit Your Part for a Skin-Core Feasibility Review
Send the CAD or 2D drawing, proposed skin and core materials, annual volume and surface requirements. The review covers part fit, material pair, layer distribution risks and the realistic manufacturing route — with the actual equipment capability stated per project.
Xiamen Goldcattle · Manufacturing since 1998 · Injection mold making and custom CNC machining · Related: two-shot injection molding services →