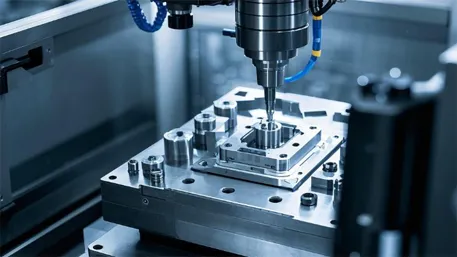
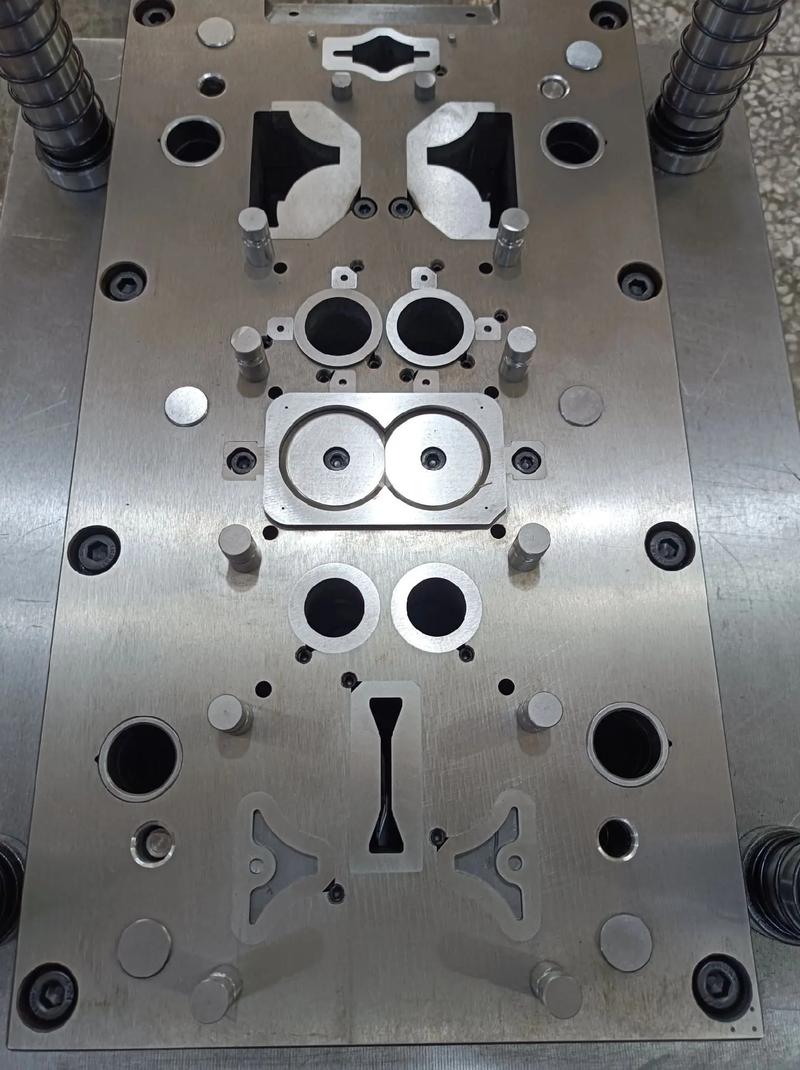
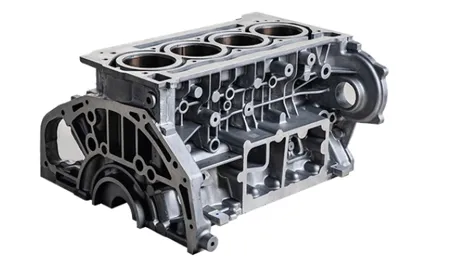
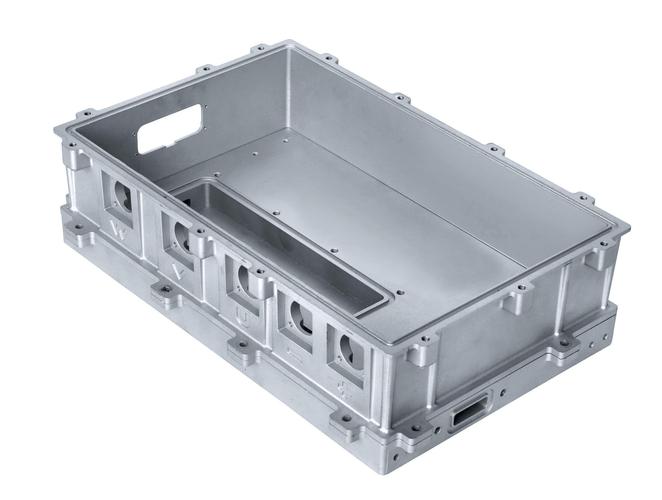
Send one drawing and get one supplier for die design, high-pressure casting, CNC finishing and inspection. Goldcattle runs the full path from prototype to mass production under a single ISO 9001 quality system — so tolerances and schedules do not slip between vendors.
Engineering reply within 4 working hours (EST / CET) · NDA available · Since 1998
Die Casting or CNC? Decide Before You Commit Tooling
Most custom parts can be made two ways. The wrong choice locks capital into a die that never pays back — or pays CNC prices for a part that should have been cast. This is the decision a purchasing engineer actually has to make, so here it is on one screen.
- Annual volume is high enough to amortize tooling (typically from a few thousand pieces upward)
- The part is near-net shape — complex ribs, bosses, thin walls and integrated features
- You want repeatable part-to-part dimensions at speed, not one part at a time
- Weight matters: cast aluminum is lighter than a solid machined block
- You can live with general casting tolerance and machine only critical faces
- Volume is low or the design is still changing — no die to re-cut
- The part needs tight, all-over tolerance that casting cannot hold directly
- Geometry is simple or 2.5D, or the material is not a casting alloy
- You need a prototype or a bridge run before mass-production tooling is approved
- Lead time from drawing to first good part matters more than piece price
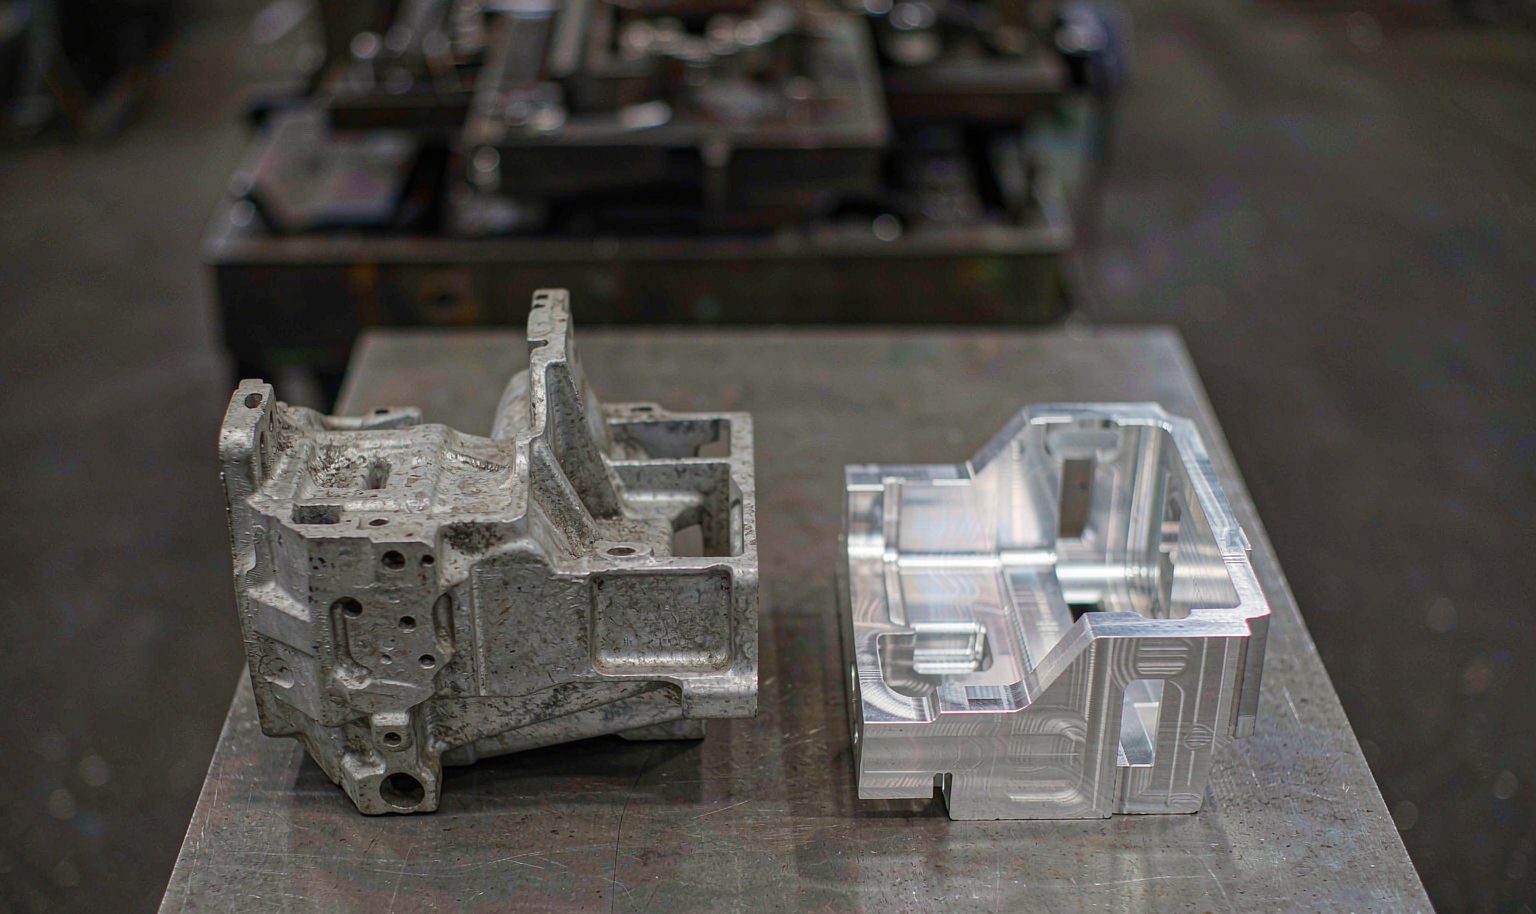
Want the long version? Read the full Die Casting vs CNC Machining comparison →
Custom Die Casting Capability at a Glance
The numbers an engineer checks before shortlisting a supplier. Values marked Confirm at quotation are evaluated against your drawing and project requirements.
| Capability | Metric | Note |
|---|---|---|
| Machine clamp force (HPDC) | 160 – 1,250 t | Aluminum, zinc and magnesium |
| Max part weight | Al ≤ 8 kg · Zn ≤ 5 kg | Larger on request |
| Max part size | ≈ 600 × 600 mm | Per machine window |
| Casting tolerance | ±0.05 mm | Per ISO 8062 CT5–CT6 |
| CNC-machined features | ±0.005 mm | On qualified features called out on the drawing |
| Min wall thickness | Al 0.8 mm · Zn 0.5 mm | Uniform section preferred |
| Surface roughness (as-cast) | Ra 1.6–3.2 µm | Before any finishing |
| Mold life | Al 50,000–100,000 shots · Zn 500,000+ | Depends on alloy and die care |
| Production volume | 500 – 1,000,000+ pcs | Prototype to high volume |
| Insert casting | Yes | Steel bushings, threaded inserts |
Die Casting Alloys for Custom Parts
Alloy follows function. Aluminum for weight and thermal performance, zinc for thin walls and plating, magnesium where mass is the constraint. Final composition and mechanical values are confirmed per your drawing and process validation.
ADC12 / A380 / A360
Light, corrosion-resistant and thermally conductive. The default for housings, enclosures, brackets and covers. A360 offers better ductility for parts that see load.
Zamak 3 / Zamak 5
Thinner walls, higher strength per volume and the best castability of the three. Plates easily for decorative or wear surfaces. Costs more per kg but often needs less machining.
AZ91D
The lightest of the die casting alloys. Chosen where weight reduction is the whole point — portable devices, robotics links, lightweight structures.
| Alloy | Standard | Density (g/cm³) | Tensile (MPa) | Typical use |
|---|---|---|---|---|
| ADC12 | JIS H 5302 (≈ A380) | 2.74 | 228 | Auto and electronics housings, brackets |
| A380 | ASTM B85 | 2.74 | 320 | General-purpose enclosures, frames |
| A360 | ASTM B85 | 2.68 | 317 | Corrosion-resistant, more ductile parts |
| Zamak 3 | ASTM B86 / EN 1774 | 6.60 | 283 | Hardware, electronics, best castability |
| Zamak 5 | ASTM B86 | 6.70 | 328 | Automotive and mechanical components |
| AZ91D (Mg) | ASTM B93 / EN 1753 | 1.81 | 230 | Lightweight electronics and structures |
How a Custom Die Casting Part Is Made
Every order follows the same controlled path, with a defined input, output and quality check at each stage. This is the sequence your part travels, from molten metal to packed carton.
Alloy heated to liquid in a furnace.
Forced into the die at 1,000–20,000 psi.
Part cools and takes the die shape in seconds.
Die opens; part ejected and runner trimmed.
Critical faces, bores and threads machined.
Anodize, powder coat, plating or chromate.
Dimensional check and documentation.
Export packing and commercial documents.
Tooling & DFM: Where Quality and Cost Are Set
Buyers do not buy “casting” — they buy tooling plus process plus repeatability. The die is designed once and used for the life of the program, so getting it right is the highest-leverage step in the whole job.
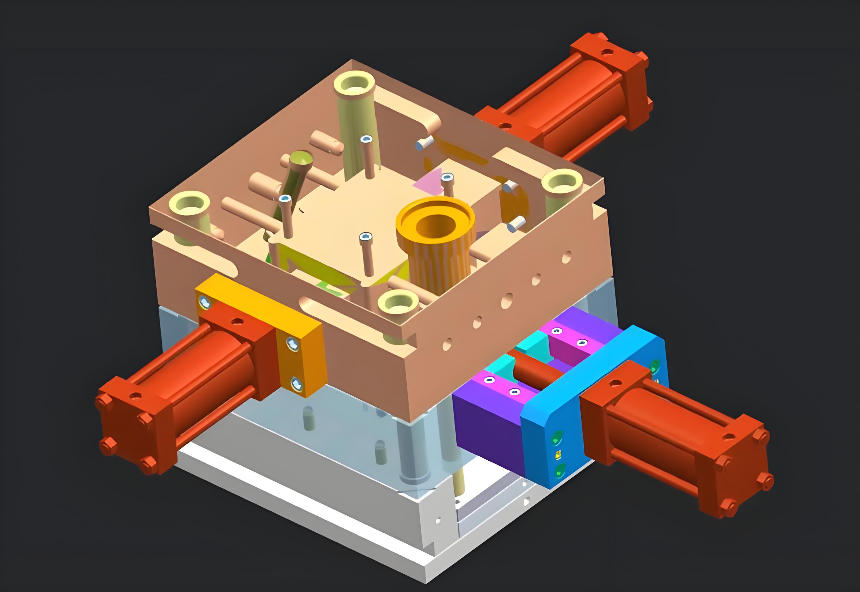
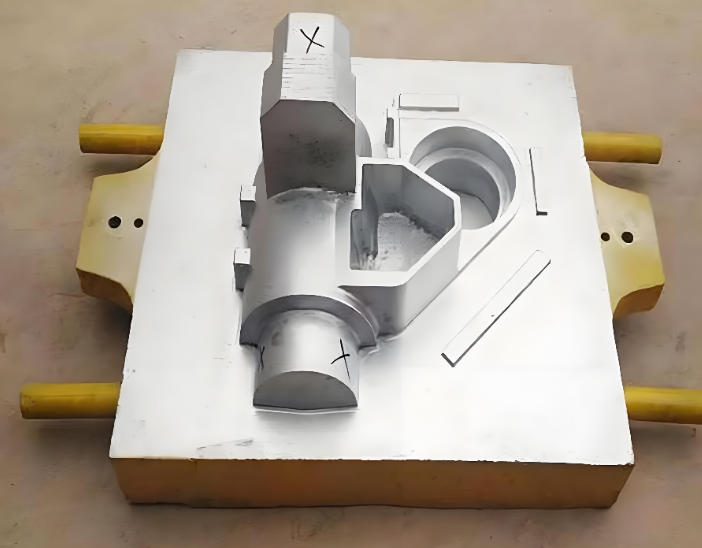
Model and requirements received.
Wall, draft, parting line, undercuts and shrinkage checked.
Filling, venting and cooling planned to control porosity.
Tool steel cut, heat-treated and assembled.
Sample casting and first-article dimensional check.
Validated against the drawing, then mass production.
Yours, and transferable
Tooling ownership is agreed up front. Customer-owned dies are stored, maintained and kept transferable on request — you are not locked in by geography you did not agree to.
Shrinkage is designed out
Allow 0.5–0.7% shrinkage for aluminum and 0.5–0.6% for zinc; the die is sized to compensate. Draft and uniform walls are built into the model so the part fills cleanly.
Die casting design rules — a starting checklist
Standard starting points for a die-cast part that fills cleanly and machines economically. They are guidelines, not laws — the DFM review confirms them against your specific geometry.
| Feature | Typical guideline | Why it matters |
|---|---|---|
| Wall thickness | Al 0.8 mm min · uniform section | Uneven walls cause shrinkage and porosity |
| Draft angle | 1–2° typical | Clean ejection without drag or scoring |
| Fillets / radii | ≥ 0.5 × wall thickness | Reduces stress concentration and improves fill |
| Bosses | Rib-supported; wall ≤ 0.8 × main wall | Avoids shrinkage voids at thick sections |
| Holes | Cast where possible; drill or machine for tight tolerance | Cored holes need draft and depth limits |
| Threads | Machine-cut, or cast-in metal inserts | Cast threads rarely hold the class a drawing specifies |
| Shrinkage allowance | Al 0.5–0.7% · Zn 0.5–0.6% | Compensated when the die is sized |
Tolerance: Where Casting Ends and CNC Begins
The single most useful thing to understand about custom die casting is that not every dimension comes out of the die. General form is cast; critical features are machined. Knowing the split is how you specify a part that is both manufacturable and affordable.
General dimensions, non-critical surfaces and features not called out on the drawing. Held to ISO 8062 CT5–CT6, with surface roughness Ra 1.6–3.2 µm.
Sealing faces, bores, threads, flatness and any fit that has to be exact. Machined on 3/4/5-axis centers to ±0.005 mm on qualified features called out on the drawing.
Datum schemes, functional gauging and where needed a first-article inspection report that ties every critical dimension back to your drawing before the first production run.
Post-Machining & Surface Finishing
A die cast part is rarely finished the moment it leaves the die. Secondary operations turn a casting into a delivered component — and because they happen in-house, they do not add another vendor to your quality chain.
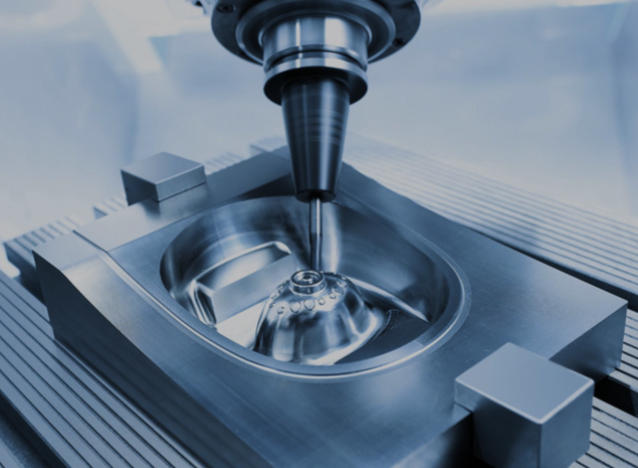
- CNC milling (3/4/5-axis)
- CNC turning
- Drilling, tapping, reaming
- Deburring and edge break
- Anodize
- Powder coating
- Electroplating
- Chromate conversion
- Insert casting (bushings, threads)
- Leak / pressure testing
- Sub-assembly
- Laser marking and packing
Quality System & Inspection
A supplier that cannot prove a part is correct is a risk, not a saving. Every batch ships with the documentation to support it, against a quality system held across all in-house processes.
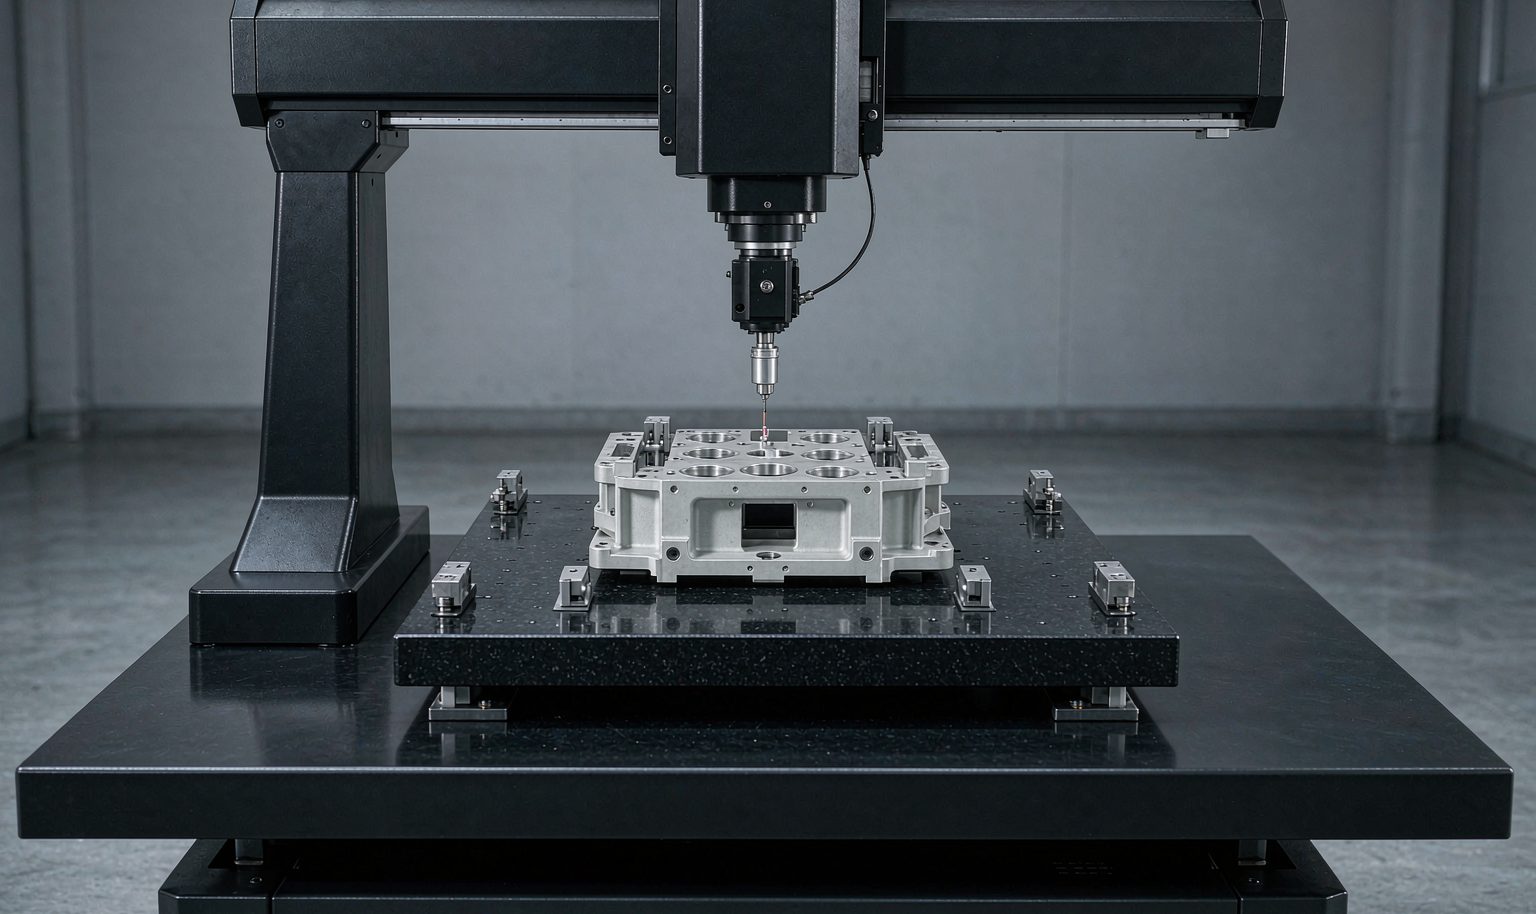
- ISO 9001:2015 quality management system
- IATF 16949-aligned process controls for automotive programs
- Material certification support — SGS / RoHS / Rmbond
- Traceability from melt to shipped carton
- CMM dimensional inspection against your GD&T
- First-article inspection (FAI) report before production
- X-ray porosity check on critical sections where specified
- Salt-spray and coating-adhesion checks available on request
- PPAP documentation packages on request
Industries & Part Types We Cast
Custom die casting shows up wherever a part needs to be strong, light, geometrically complex and repeatable. These are the categories that make up most of our inquiry mix.
- Motor and inverter housings
- ECU and sensor enclosures
- Battery-tray and structural brackets
- Engine and transmission covers
- EMI / RF shielding enclosures
- Heat-sink housings
- Connector bodies and chassis
- Device shells
- Pump and valve housings
- Motor frames and gearbox cases
- Pneumatic manifold blocks
- Machine-tool components
- Joint and arm-link housings
- Servo-motor end-bells
- Gripper components
- Sensor mounting brackets
- Battery-module enclosure parts
- Inverter housing covers
- Charger-shell castings
- Thermal-management plates
- Instrument housings
- Device enclosures
- Mounting and support frames
- Clean-surface components
From Prototype to Mass Production
No one should have to commit to a full production die before the design is proven. The volume ladder below shows how a program can start small and scale on the same supply chain.
Validate form, fit and function without production tooling. Machined or soft-tooled samples get the design into testers' hands fast.
A short production run to prove the design and start shipping while the final die and volumes are confirmed.
Full HPDC tooling with amortized piece price, secondary machining and finishing in one purchase order.
What Drives the Price of a Custom Die Casting Part
Die casting price has two parts: a one-time tooling cost and a per-piece price. Buyers who understand the levers get a better part for less — and know where not to cut.
Tooling
Die design, steel, machining and trials. Spread across the production volume, so it dominates low-volume pricing and fades at high volume. Tool ownership stays with you.
Piece price
Set by alloy, part weight, wall uniformity, complexity, secondary operations and volume. Higher volume lowers unit cost; simpler geometry lowers it more.
Levers that lower piece price without lowering quality
- Keep walls uniform — varying thickness creates shrinkage, porosity and rejects.
- Add draft so the part ejects cleanly; missing draft forces manual work and slows the cycle.
- Reduce undercuts where a slanted surface or a slide-free design will do.
- Specify tolerance by function — machine only the faces that need it.
- Consolidate parts into one casting instead of several pieces plus fasteners.
- Choose the right alloy rather than the cheapest one; the wrong alloy costs more in scrap.
How to Send an RFQ for Custom Die Casting Parts
A complete RFQ is one message. The list below is everything our engineers need to return a manufacturability review and a price — and nothing you have to go looking for.
What to include
- 3D CAD model (STEP / IGES / X_T)
- 2D drawing (PDF) with tolerances and GD&T
- Alloy or material, and any heat treatment
- Surface finish and any coating or plating
- Annual volume and first-order quantity
Helpful if you have it
- Target piece price or budget
- Critical-to-function dimensions
- Compliance needs (PPAP, RoHS / REACH)
- Delivery location and Incoterms
- Tooling ownership preference
Why Buyers Consolidate with Goldcattle
Most die casting programs touch five or six shops. Every hand-off is a place where tolerances and schedules slip. Consolidation removes those hand-offs.
Die to delivered part
Tool design, casting, CNC finishing, surface treatment and sub-assembly run under one roof and one ISO 9001 system — not three vendors and a broker.
East-coast and Europe friendly
We work on your time zone (EST / CET) with an engineering reply within 4 working hours, so a question does not cost you a day.
Frequently Asked Questions
The questions engineers and buyers ask most when sourcing custom die casting parts.
What is die casting, and when should I use it for custom parts?
Should I choose die casting, CNC machining, or both?
What tolerance can custom die casting hold?
What is the minimum wall thickness?
How long does die casting tooling take?
What is the minimum order quantity for a custom die casting part?
Which alloys do you cast?
Can you make the tooling, and who owns it?
What documentation ships with the parts?
How much does a custom die casting part cost?
Send Your Drawing — Get a DFM Review and Die Casting Quote
Upload a 3D model and 2D drawing. An engineer reviews manufacturability and returns a tooling-and-piece-price quotation, typically within one business day.
NDA available · 24-hour response · ISO 9001:2015 / SGS / ROHS / Rmbond · Founded in 1998
Explore Related Capabilities
Custom die casting parts manufactured by Xiamen Goldcattle Plastic & Metal Products Co., Ltd. — a one-stop OEM/ODM manufacturer in Xiamen, China, serving OEMs in North America and Europe.