Custom CNC-Machined Brass Screws & Fasteners
Manufactured to your drawing or approved sample, with a specified brass grade, thread geometry, head and drive form, dimensions, surface finish and inspection requirement. This page is written for the buyer who has to justify the choice — so it documents the screw geometry, the thread standards, the material decision, the manufacturing route and the acceptance method rather than describing brass in general.
At a Glance
Four requirements decide whether a brass screw can be made as drawn: the thread specification, the material specification, the head and drive geometry, and the acceptance method. A drawing that states all four can be quoted and inspected without interpretation; a drawing that states “brass screw” and a size cannot, because the alloy, the thread class and the finish are all still open.
What changes the part
- Thread diameter, pitch, form and tolerance class
- Head style and drive recess
- Shoulder, shank and tip geometry
- Brass grade, temper and condition of supply
- Plating or coating, and whether it is applied before or after gauging
What changes the price
- Material grade and bar diameter against the part volume
- Number of operations: turn only, or turn plus mill
- Thread class and the gauging it requires
- Finish and its handling between operations
- Quantity, batch size and inspection scope
Where the surrounding brass content lives. Screw geometry, threads, materials and acceptance are on this page. For brass parts that are not fasteners — fittings, bushings, terminals, connectors and other turned components — see brass CNC turned components, which covers that family in its own right.
Types of Custom Brass Screws
Short answer: the useful question is not which catalogue category a screw falls into, but which features on it have to be controlled. The families below are the ones quoted most often; each one exists because a particular set of features drives its manufacture.
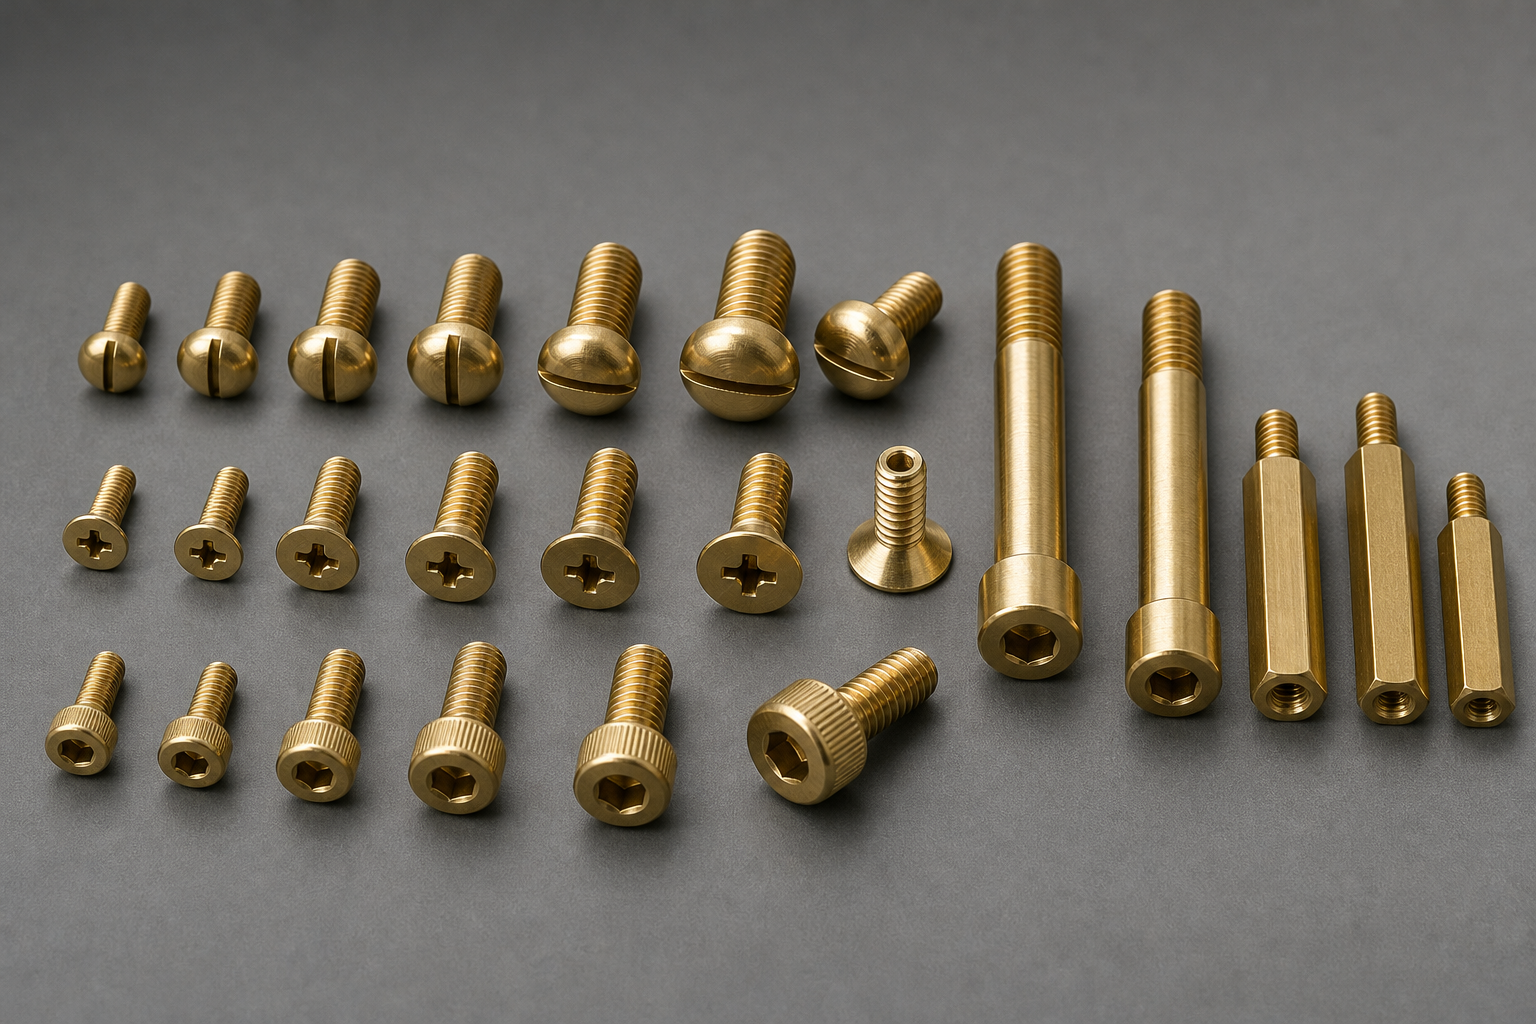
Machine screws
Slotted or cross-recessed, with pan, cheese, countersunk or fillister heads. The head form and the drive recess decide the tool, the head geometry and the operations.
Hex-socket cap screws
Internal hex drive for higher tightening torque and a low head profile. The socket depth and hex form are acceptance features, not decoration.
Shoulder screws
A ground or turned plain shoulder that locates, with a threaded end that clamps. Shoulder diameter, shoulder length and the thread-to-shoulder alignment all matter.
Terminal & binding screws
Used where a conductor or a lug is clamped under a head. Head pressure area, thread class and conductivity of the grade are the functional points.
Knurled & thumb screws
Knurled or lobed heads for hand tightening. Knurl form, grip diameter and the resulting burr condition are the appearance and handling requirements.
Threaded standoffs & spacers
Turned from bar with male and female threads, often with a milled flat or a cross-hole. Thread concentricity to the body axis is the usual critical requirement.
Special threaded parts
Stepped shanks, cross-drilled holes, milled flats and slots, or non-standard tips. These are the parts where turning alone is not enough and the route has to be planned.
What Can Be Customized on a Brass Screw?
Short answer: almost everything — but each feature has to be stated rather than implied, because an unstated feature is a decision handed to the supplier. The table below is the list worth working through before sending an enquiry.
| Feature | What you need to state | Why it matters on the shop floor |
|---|---|---|
| Head style | Pan, cheese, fillister, countersunk, button, hex or a drawing-defined form | Sets the head geometry, the tool path to form it and how the part is held for the next operation |
| Drive / recess | Slotted, cross-recessed (and which type), internal hex, Torx-type, or none | Determines the recess dimensions, the acceptance check and the tooling interface — an unstated recess cannot be gauged |
| Thread specification | Diameter, pitch, thread form and tolerance class, plus the standard where one applies | Decides the fit and interchangeability, and the gauge used for acceptance — not a general dimensional tolerance |
| Thread length | Threaded length, unthreaded shank length, and whether the thread runs to the head | Sets the clamping range and changes the turning sequence; a full-thread and a part-thread screw are different programmes |
| Overall length | Total length and its tolerance, measured from which datum | Length is measured from a defined face; an ambiguous datum becomes a rejected batch |
| Tip geometry | Flat, chamfered, radiused, cone point, dog point or cup point | Affects starting, seating and contact; also changes the finishing operation and the burr risk |
| Shoulder / shank | Plain diameter, step, locating length, flats or a cross-hole | Non-rotational features need milling or live tooling, which changes both the route and the cost |
| Surface finish | As-machined, polished, or a named plating or coating with its specification | Affects appearance, corrosion behaviour and — for plated parts — the effective thread dimensions |
| Critical dimensions | Tolerances, datums and the characteristics that will be inspected | Decides the process plan and the acceptance method; critical features should be marked on the drawing, not listed separately |
| Material | Brass grade, material specification and condition of supply | Determines machinability, corrosion behaviour, conductivity, lead content and the certificate you receive |
Thread Specification and Thread Inspection
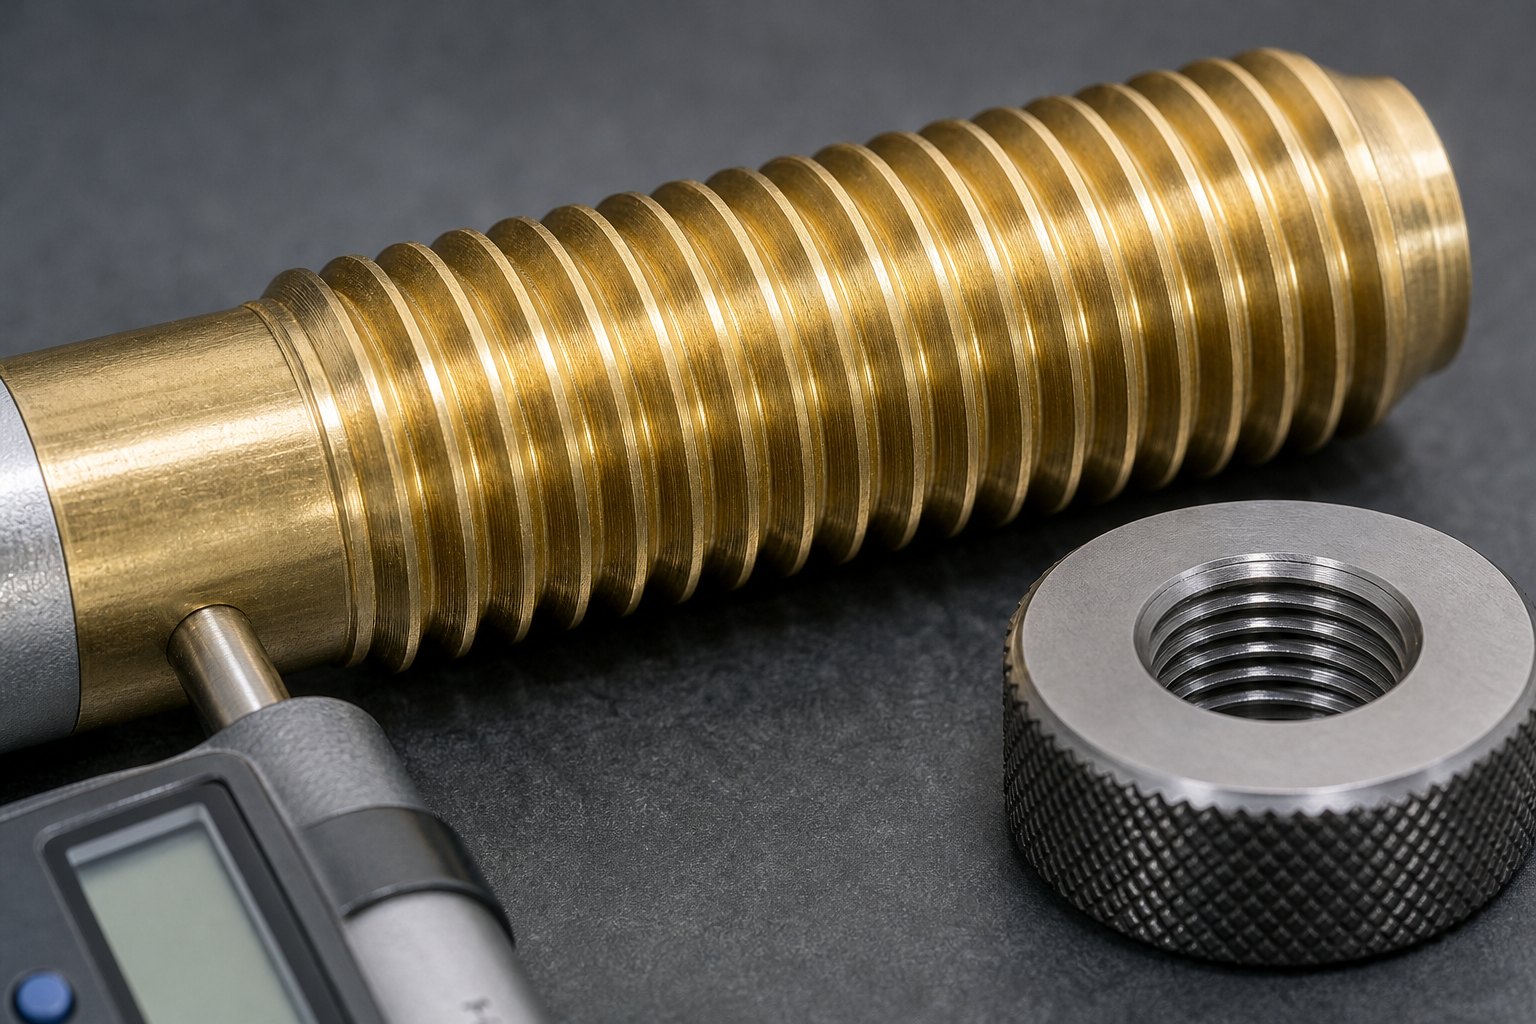
Short answer: a thread is accepted against a thread specification and a gauge, not against a general dimensional tolerance. “M6 brass screw, ±0.01” does not describe a thread: it leaves the pitch, the form and the tolerance class undecided.
| Thread family | Standard that defines it | What it fixes | What it does not fix |
|---|---|---|---|
| Metric (M) | ISO 68-1 basic profile; ISO 261 / ISO 262 for the general plan and selected sizes; ISO 965-1 and ISO 965-2 for tolerances | The thread profile, the diameter and pitch series, and the tolerance classes such as 6H for internal and 6g for external threads | The material grade, the plating, or the strength of the finished screw |
| Unified inch (UNC / UNF) | ASME B1.1 | The inch thread form and the classes, for example 2A/2B and 3A/3B | Metric profiles and pipe threads |
| Pipe threads | ASME B1.20.1 for NPT, ISO 228-1 for G / BSPP, ISO 7-1 for R / BSPT | The sealing or parallel pipe thread forms used on threaded fittings, ports and connectors | Plain machine screws, which do not use these forms |
| Drawing-defined thread | Your drawing | Whatever it states about form, diameter, pitch and class | Nothing outside what it states — so it has to state enough to be gauged |
How thread acceptance is actually agreed
- Name the standard and the class — for example “M4 × 0.7, 6g” or “1/4-20 UNC 2A” — rather than a diameter alone.
- State the gauge requirement where GO/NO-GO gauging or another specific method is expected, so it appears on the quotation and the inspection record rather than being raised after delivery.
- Decide the gauging order when a finish is involved — plating adds thickness to the flanks, so a screw gauged before plating can fail after it (see finish and thread fit).
- Mark partial threads explicitly. A part-thread screw needs its threaded length and its unthreaded shank length stated; leaving it to interpretation produces the wrong clamp length.
- Say whether the thread is rolled, cut or chased where the programme depends on it, because the three are not equivalent in fatigue behaviour or in how they are produced.
Brass Grades and Material Selection
Short answer: “brass” is a family, not a specification. Three things have to be named before material can be purchased for your part: the grade, the material specification it is bought to, and the condition of supply.
| Material direction | Where it suits | What has to be confirmed with it |
|---|---|---|
| Free-cutting brass (UNS C36000 series) | The usual starting point for turned fasteners: it machines cleanly and quickly, which is why it is the stock that screw machines were designed around | The applicable material specification for the product form. ASTM B16 / B16M covers free-cutting brass rod, bar and shapes for use in screw machines — it is an input-material specification and does not define finished screw dimensions or thread tolerances. Temper and condition of supply also have to be stated. |
| Wrought brass such as C26000 | Where electrical conductivity, formability or a specific customer material specification applies rather than maximum machinability | The geometry and route, because a less free-cutting grade changes cycle time; and the material specification from your drawing |
| European rod grades (the CW-series machined-rod family) | Where a European material specification is called for on the drawing | The correct EN standard for the product form — free-machining rod and forging rod are covered by different standards, so the standard number should be taken from your specification rather than copied from a supplier page |
| Low-lead and lead-free grades | Where a lead limit is a programme requirement rather than a preference | The exact grade, the permitted limit, the applicable requirement and the certificate that has to accompany the material — see lead content and compliance |
What brass is good at — and what it is not
| Property | The accurate version | Why the distinction matters |
|---|---|---|
| Machinability | Free-cutting brass is the reference material for the copper-alloy machinability scale, conventionally rated 100 | This is why it turns quickly and cleanly. It is a machining property, not a statement about strength. |
| Electrical conductivity | Substantially better than steel — around a quarter of copper, approximately 26% IACS for C36000 | It is why brass is standard in terminals and electrical connections. Quote it as approximate, because it varies with grade and temper. |
| Corrosion resistance | Good in normal atmospheric and water exposure — but not unconditional | High-zinc yellow brass is susceptible to dezincification in aggressive, stagnant or chlorinated water. Where that applies, a dezincification-resistant grade or a different alloy is required; the alloy must not be selected as though all brasses behave alike. |
| Wear resistance | Moderate. Leaded free-cutting brass is a comparatively soft material | It is the reason bearings and wear bushes use bronze rather than free-cutting brass. A brass fastener is not the right answer to a wear problem, and the page does not present it as one. |
| Strength | Dependent on grade, temper and section — there is no single figure for “brass” | Where strength matters, the grade, temper and the applicable material specification have to be stated and the properties taken from that specification for the section in question. |
Lead Content, RoHS and Market-Specific Requirements
Short answer: lead content in brass is a property of the alloy, not of the category. It cannot be established from the word “brass”, and it cannot be answered for a group of parts as though they shared one composition.
| Requirement | What it applies to | What has to be established |
|---|---|---|
| RoHS — electrical and electronic equipment | Products in scope of the directive, where a brass part is a component of that product | The alloy actually supplied, and the current status of the relevant exemption. Copper alloys containing up to 4% lead are covered by a time-limited exemption in the RoHS restricted-substance framework, currently listed as valid until 30 June 2027. Exempt from the restriction is not the same as lead-free, and the status of such an exemption should be confirmed for the programme rather than assumed indefinitely. |
| REACH — substance information in articles | Articles placed on the EU market, where a candidate-list substance is present above 0.1% by weight in the article | Whether your programme requires substance information for the part, and which party in the chain carries the reporting obligation. The obligation typically sits with the party placing the article on the market, so the material data has to be passed along the chain rather than replaced by a supplier statement. |
| Drinking-water contact — United States | Components in contact with potable water | The grade and the certification route. The US route combines NSF/ANSI 61, including Annex G, with the lead-free definition in the Safe Drinking Water Act, which sets a weighted-average lead limit of 0.25% for wetted surfaces. This is a product-level certification and cannot be inferred from the alloy name. |
| Food-contact and other regulated applications | Parts in contact with food or in other regulated duty | The applicable requirement, the grade that satisfies it, and the documentation your customer accepts. These are programme-specific and are confirmed as such. |
| Customer material specification | Whatever your drawing, programme or industry requirement states | The grade, the permitted composition and the certificate format. A supplier cannot certify to a specification it was not given. |
We do not state that all brass screws are RoHS compliant, that brass is lead-free, or that a brass part is automatically suitable for drinking water or food contact. None of those statements can be made about the category, because they depend on the alloy, the application and the obligation that applies to the product.
What we do instead: the alloy is purchased to the specification you name, and the material documentation is issued according to the requirements of your programme. If your programme needs a low-lead grade, an exemption recorded, or a substance declaration, say so in the enquiry, because that requirement decides which material is bought and what evidence travels with it.
CNC Machining vs Dedicated Screw Manufacturing
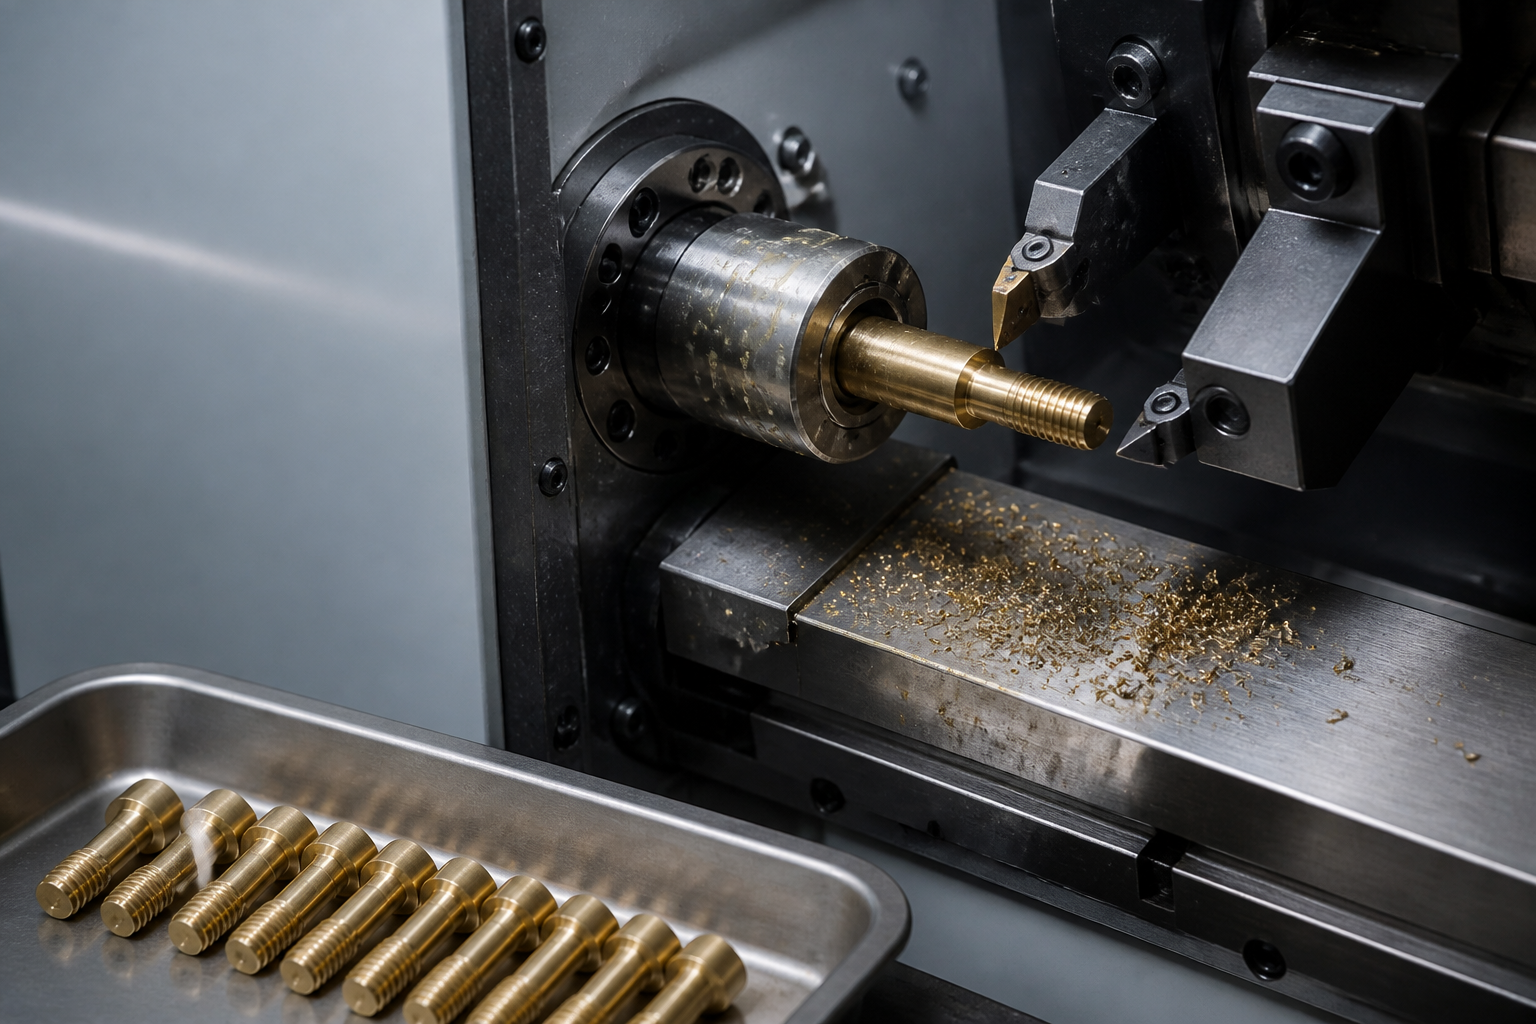
Short answer: CNC turning is not automatically the right route for a screw. It is the right route for a particular set of features, and where those features are absent the honest answer may be a different process.
| Part situation | Route to evaluate | Why |
|---|---|---|
| A special screw, an unusual shoulder, or a form that is not a standard fastener | CNC turning, with milling where the geometry needs it | No tooling commitment, and the geometry can still be revised between batches |
| Features that are not rotational: slots, flats, cross-holes, milled steps | CNC turning plus a second milling operation, or a turn-mill approach | These features cannot be produced by turning alone, and they are the main reason a “simple screw” becomes a multi-operation part |
| A design that still has to be validated | Machined prototypes or the applicable rapid route | Shape, fit and function can be proved before any tooling decision is made |
| A standard geometry in large quantity | Evaluate dedicated fastener manufacturing, cold heading and thread rolling | Forming metal is faster and less wasteful than cutting it away, once the volume justifies the setup — and for a standard screw, this is frequently the correct answer |
| Tight requirements, an unusual material, or a heavier inspection scope | Engineering review first, then confirm both the route and the acceptance plan | The inspection requirement can decide the route as much as the geometry does |
Our own production of these parts is CNC turned, with milling added where the part needs it. Cold heading and thread rolling are dedicated fastener processes; where a programme makes them the better choice, they are evaluated and confirmed as part of the quotation rather than presented as equipment on our floor.
The reason to write this out is that a supplier who quotes every screw as a turned part has either not looked at the volume or cannot offer the alternative. For a standard screw at production quantity, the second process is often what the price actually depends on.
Surface Finish and Thread Fit
Short answer: a finish is part of the specification, not a cosmetic afterthought, because it changes what the gauge sees. A screw that gauges correctly in bare brass can fail after plating.
| Finish direction | What it provides | Effect on the thread and the dimensions | What to state |
|---|---|---|---|
| As-machined brass | The appearance of cleanly turned brass, unchanged conductivity, no added process | No dimensional change beyond the machining itself | Whether burrs are acceptable, and where |
| Deburring and edge blending | Safe handling and a clean thread lead-in | Removes the lead-in burr that damages the mating thread and the assembly operator | Whether deburring is a process step or an inspection criterion |
| Barrel or abrasive polishing | A uniform appearance with tool marks blended out | Can round thread crests slightly and lightly alter the major diameter | Whether threads are gauged after polishing rather than before |
| Electroplated finishes, where specified | Corrosion protection, appearance or solderability, depending on the finish named | Adds a measurable layer to the thread flanks and the shank; the effective thread dimensions change and the gauge result can change with them | The finish specification and thickness, and whether gauging is required after finishing |
| Anti-tarnish or appearance treatments | Keeps the brass appearance stable in storage and transit | No dimensional change | The appearance standard and how it will be judged |
Thread, Dimensional and Appearance Inspection
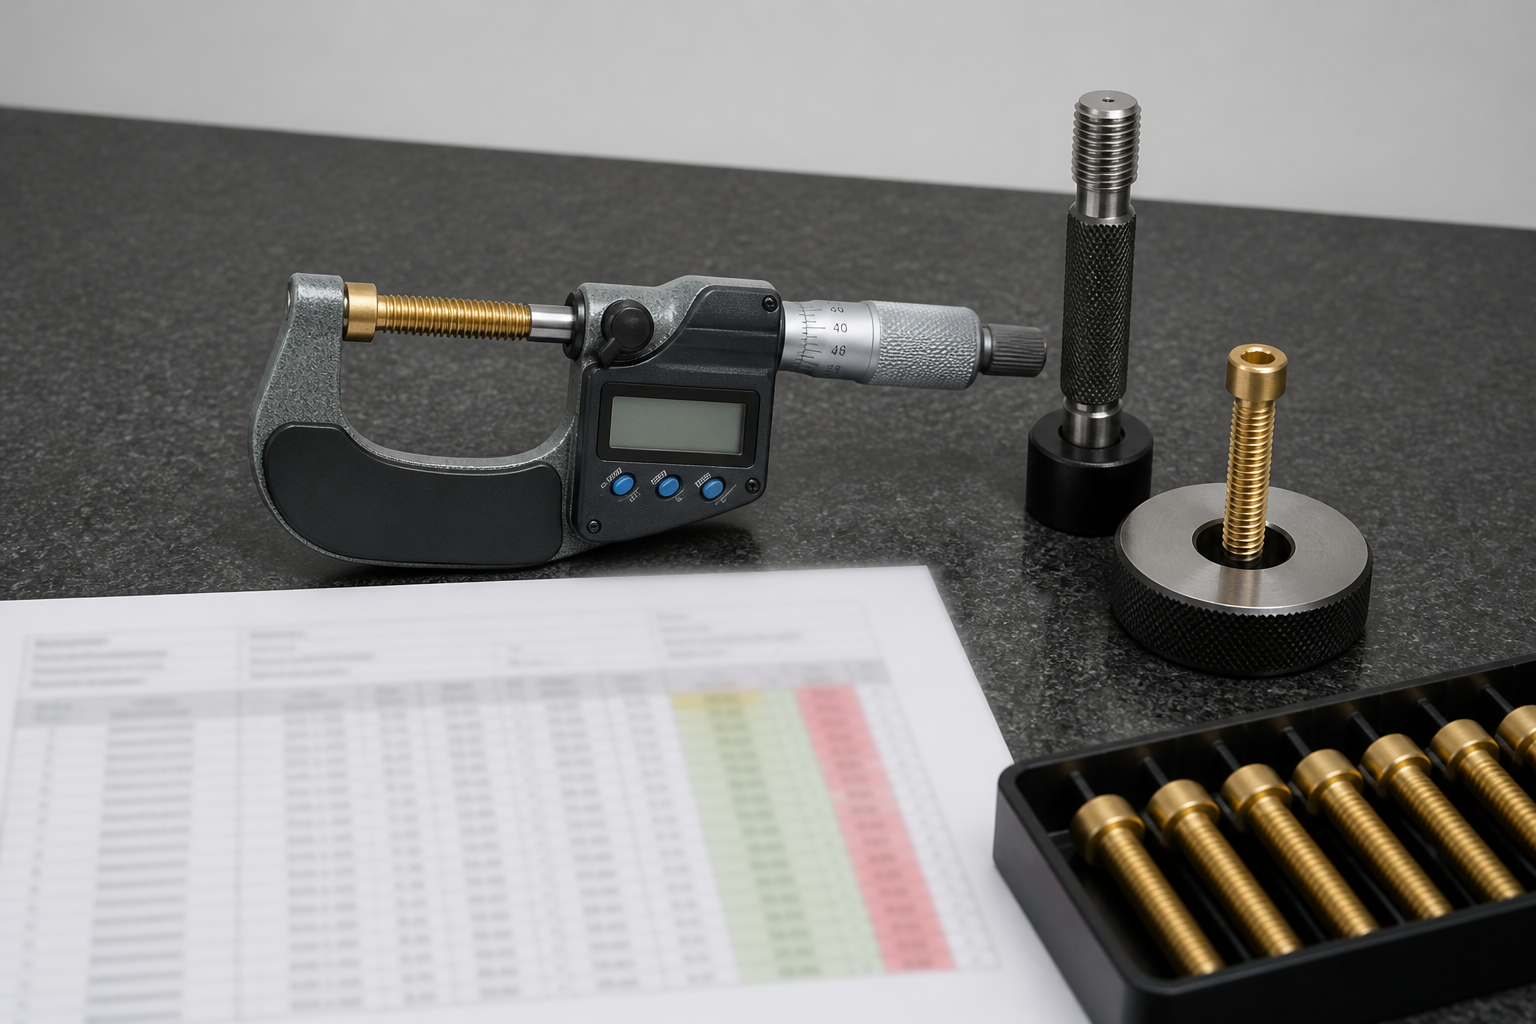
Short answer: on a fastener, inspection is mostly about the thread, and the thread is inspected with a gauge rather than with a general dimension. Everything else is confirmed against the drawing, and the scope is agreed before the order rather than after it.
| Inspection stage | What it covers | What it depends on |
|---|---|---|
| Material verification | Grade, specification and batch identity against the material certificate | The material specification named in your drawing or enquiry |
| In-process checks | The characteristics that drift during a run: overall length, head or shoulder diameter, thread start condition | The checks agreed for the part, and how often they are repeated |
| Thread inspection | Thread form and tolerance class, checked with the gauge appropriate to the specification | The thread standard and class stated on the drawing — and whether gauging happens before or after finishing |
| Drive and head inspection | Recess form and depth, slot width, head diameter and height, and the appearance of the formed surfaces | The drawing, plus an agreed appearance standard where the head is a visible feature |
| Finish verification | That the specified finish was applied, and the thickness where a thickness is specified | The finish specification, and whether verification is part of the order or supplied by the finishing process |
| Final dimensional check | The listed characteristics measured against the drawing before packing | The report scope agreed at quotation |
| Packing and traceability | Part number, batch identity, quantity and packaging against the order | The order, the destination and any labelling your process requires |
The sequence we work to: material verification → machining → thread inspection → finish verification → final dimensional check → shipment documentation.
Material Certificates and Inspection Documentation
Short answer: the useful question is not whether certificates exist, but which document, covering which characteristics, arrives with which shipment. That scope is agreed at quotation.
| Document | What it demonstrates | What it does not demonstrate |
|---|---|---|
| Material certificate | The grade, specification and batch of the bar that was purchased | That a particular screw was made from that bar, unless batch records link the two |
| Dimensional inspection record | Measured values against the drawing for the characteristics listed on it | Anything outside the listed characteristics, or the sampling basis unless it is stated |
| Thread inspection record | The gauge used, the thread class and the result recorded | That every part was gauged, unless 100% gauging was agreed |
| First-article documentation | Every characteristic documented for a first article at the start of a programme | Later production, unless the process is held and monitored after it |
| Certificate of conformity | A declaration that the order conforms to the agreed specification | It is an assertion of conformity, not a measurement |
| Finish documentation, where applicable | The finish specification applied by the finishing process | The final dimensional result, unless gauging after finishing is included in the scope |
Where Custom Brass Screws Are Used
Short answer: brass fasteners are chosen where conductivity, corrosion behaviour in normal exposure, non-magnetic properties or appearance matter — and the specific grade follows from which of those actually applies.
| Application area | Typical parts | What usually drives the choice |
|---|---|---|
| Electrical and electronic equipment | Terminal screws, binding screws, earth and chassis screws, contacts fastened into assemblies | Conductivity and stable contact resistance; also the substance-compliance requirements of the finished product |
| Connectors and wiring accessories | Clamping and terminal hardware, threaded inserts in connector bodies | Thread class consistency, torque behaviour and resistance to loosening |
| Instrumentation and meters | Small machine screws, shoulder screws for pivots, knurled thumb screws | Non-magnetic material, fine thread control and appearance on visible hardware |
| Mechanical and equipment assembly | Special threaded parts, standoffs, spacers and stepped screws | Geometry that is not available as a standard part, and repeatability across batches |
| Decorative and architectural hardware | Visible brass fasteners where the finish is part of the product | Appearance consistency and a finish that holds up in the intended environment |
What Affects the Cost of Custom Brass Screws
Short answer: the price of a brass screw is decided by how many operations it needs, how much material it consumes against the bar it was cut from, and how much verification the order carries. Material grade alone explains very little of it.
Brass Screw RFQ Checklist
Work through this list before sending an enquiry. Each item that is answered removes a round of questions and reduces the risk of a quotation that is based on an assumption.
- 2D drawing and/or 3D CAD file, with the revision identified
- Brass grade, material specification and condition of supply
- Thread diameter, pitch, form and tolerance class
- Head style, drive recess, shank, shoulder and overall dimensions
- Critical dimensions and the inspection you expect on them
- Surface finish, plating or appearance requirement, and whether gauging follows the finish
- Prototype quantity, batch quantity and expected annual demand
- Lead-content, RoHS or REACH requirements where the programme has them
- Material certificate, first-article or other documentation you need
- Packaging, labelling and delivery destination
Direct Answers
Brass Screw FAQ
Can you manufacture custom brass screws from drawings or samples?
Yes, and both routes are quoted from the same review. A drawing or 3D model is the stronger input because it carries the thread class, tolerance and material specification. A sample can be measured to establish geometry, but the requirements it cannot communicate — material specification, thread class, acceptable variation — have to be confirmed by you before the part is quoted and produced.
What brass grades are suitable for CNC-machined screws?
Free-cutting brass is the usual starting point, because it machines quickly and cleanly and is the reference material for the copper-alloy machinability scale. Wrought grades such as C26000 are used where conductivity, formability or a customer specification matters more than machinability. The decisive point is not the grade family but the material specification and condition you require, since the same alloy name can be purchased to different specifications.
Can custom brass screws use metric, UNC or UNF threads?
Metric threads are covered by the ISO thread standards, which define the profile, the diameter and pitch series and the tolerance classes such as 6H and 6g; unified inch threads are covered by ASME B1.1, with classes such as 2A/2B and 3A/3B. State the family, the size and the class, and the gauging follows. Other thread forms are quoted against the drawing or specification that defines them.
Can you produce special screw heads and drive recesses?
Head geometry and drive recess are two of the features most often customized, and both need to be defined on the drawing: the head form, the recess type and its dimensions. A recess that is not dimensioned cannot be gauged, and a head profile that is only shown pictorially cannot be inspected. Where a recess follows a published product standard, naming the standard is usually the clearest way to define it.
Does surface treatment affect thread fit?
It does. Plated and coated layers add thickness to the thread flanks, so the effective dimensions change and a screw gauged before finishing may not gauge afterwards. Where a finish is specified, the gauging order should be agreed at quotation, and masking or pre-plate dimensions settled for any thread that has to assemble to a controlled fit.
Can you supply lead-free brass screws?
Where a programme requires it, the part is quoted against a named low-lead or lead-free grade and purchased to that material specification, with the supporting documentation. What cannot be done is to declare brass lead-free by default: lead content is a property of the specific alloy, and copper alloys containing up to 4% lead are also currently covered by a time-limited exemption in the RoHS restricted-substance framework. Both facts have to be handled against your specification rather than replaced by a general claim.
What inspection documents can be supplied?
Depending on the order: a material certificate naming the grade and specification, a dimensional inspection record for the characteristics listed for the part, thread inspection records showing the gauge and class used, first-article documentation where a programme requires it, and packing or traceability information. Finish documentation comes from the finishing process where a specialist finish is applied. The document scope is agreed with the quotation.
Is CNC machining the most economical route for every screw?
No. It is efficient for special geometry, small quantities, prototypes and any part that needs milling in addition to turning. For a standard screw made in quantity, dedicated fastener manufacturing — cold heading with rolled threads — is normally the more economical route and should be evaluated rather than assumed. Our own turning capacity is CNC, and where another route suits the part better we say so at quotation.
What affects the minimum order quantity?
Material purchasing increments, the setup and programming for the part, the number of operations, finishing batch minimums and the inspection scope. Because those vary with the part and the route, the practical minimum is quoted per item rather than published as a single number for brass screws.
What should I include in a brass screw RFQ?
The drawing or model with its revision, the brass grade and material specification, the thread specification including class, the head and drive geometry, the critical dimensions and the inspection you expect, the finish, the quantities, any lead-content or substance requirement, the documentation you need and the delivery destination. That list is set out above as the RFQ checklist.
Send the drawing, not just the part name
A brass screw can only be quoted accurately against its thread specification, material specification, head and drive geometry, finish and inspection requirement. Send the drawing or model and we will review those requirements before quoting — including the route that suits the part, which is not always turning.
Free drawing review · NDA available on request · Quotation states the material specification, thread class and inspection scope it is based on
Scope and claims on this page
- No price ranges or pass rates. This page does not publish price bands, minimum order numbers, delivery times or yield figures, because each of them depends on the part, the material and the order that would follow it.
- Material properties are stated by grade, not by category. Where a figure appears — the machinability reference for free-cutting brass, or a conductivity value — it is tied to the grade it belongs to and given as approximate. Where a property depends on temper and section, it is described qualitatively rather than given a number.
- Standards are named only where they define the subject. Thread standards define threads; input-material standards define the bar a part is made from. Neither is used to claim that a finished screw conforms to a product standard it was not made against.
- Substance compliance is not claimed in general terms. Lead content, RoHS status and drinking-water suitability are properties of a specific alloy in a specific application, and are handled that way.
- No customer names, project data or borrowed part photographs. Nothing on this page describes another customer's programme, and no third-party product image is presented as our work.
- Specialist processes are identified as such. Where a finish or a test is carried out by a qualified partner, the record comes from that process and is not described as in-house work.