What Wood Is Best for CNC Machining? A Material Selection Guide
There is no single "best" wood. The right choice depends on what the part has to do — how it looks, how stable it must stay, how much detail it carries and what environment it goes into.
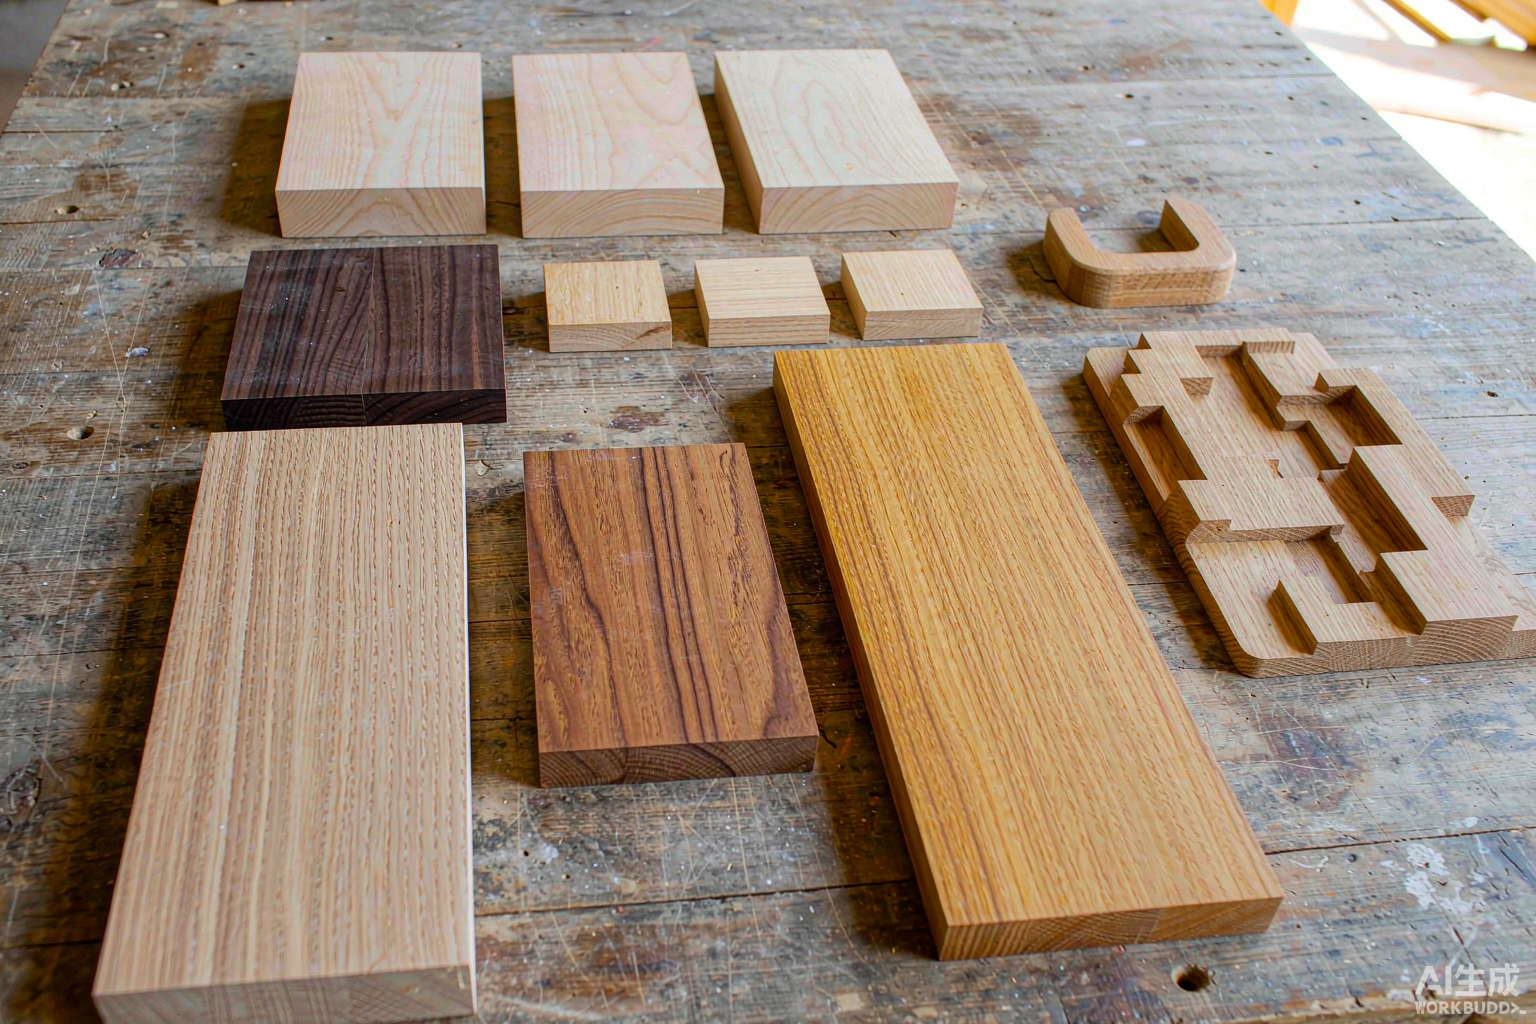
Most commonly CNC-machined wood materials include hardwoods such as oak, maple and walnut, softwoods such as pine and cedar, and engineered wood products such as MDF and plywood. The best choice depends on the required strength, surface finish, dimensional stability, grain appearance, moisture exposure and machining detail.
For stable, repeatable production, MDF and plywood can be easier to control than solid wood; for visible furniture and premium decorative components, hardwoods such as oak, maple and walnut are often preferred.
Best Wood Materials for CNC Machining
Eight materials that cover the large majority of CNC wood work. Ratings are relative and qualitative — they describe typical behaviour, not certified values.
| Material | Machinability | Dimensional stability | Appearance | Typical applications |
|---|---|---|---|---|
| Oak | Good | Good | Distinct grain | Furniture, structural and decorative parts |
| Maple | Good | Good | Fine, uniform grain | Furniture, instruments, detail work |
| Walnut | Good | Moderate–Good | Premium dark grain | Furniture, decorative components |
| Cherry | Good | Good | Smooth, warm grain | Furniture, architectural components |
| Pine | Very good | Moderate | Visible softwood grain | Prototypes, signs, lightweight parts |
| Cedar | Very good | Moderate | Distinctive grain | Decorative and outdoor applications depending on species |
| MDF | Excellent | Good | Uniform, no grain | Panels, molds, painted parts |
| Plywood | Good | Good | Layered / veneer appearance | Structural panels, furniture, prototypes |
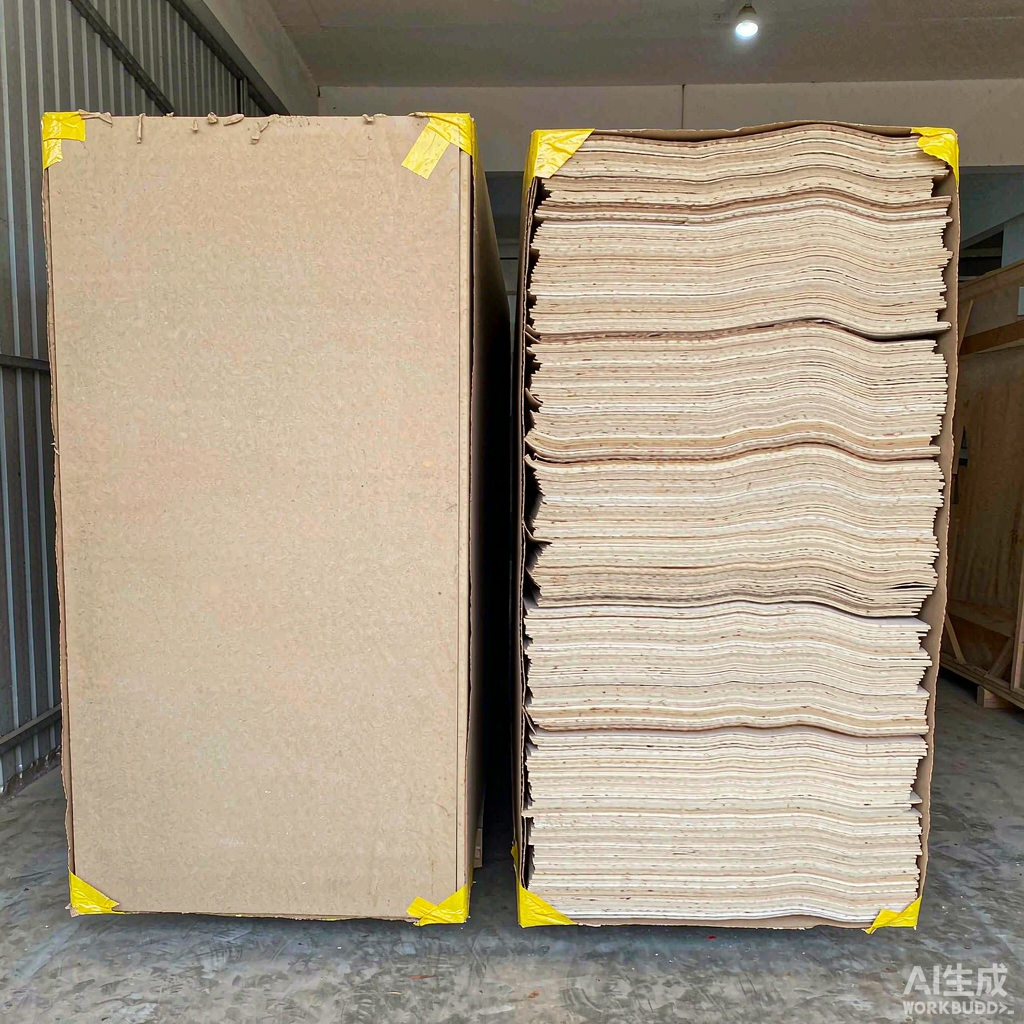
Hardwood is not automatically the better CNC material. MDF and plywood often machine more predictably than solid wood because their structure is uniform and their sheet dimensions are consistent — which is exactly what repeatable production needs. Solid wood wins on appearance and on the structural characteristics of specific species.
Solid Wood vs Engineered Wood for CNC Machining
The first decision is not the species — it is whether you need solid stock or a manufactured sheet.
- Natural grain and premium appearance
- Good structural characteristics depending on species
- Can be sanded, stained and finished as a visible surface
- Repairable and refinishable in service
- Responds to moisture with dimensional movement
- Grain variation, knots and natural defects
- Material yield is harder to plan than sheet goods
- Dimensional movement after machining is possible
- More uniform internal structure
- Predictable sheet dimensions
- Consistent machining behaviour across a batch
- Easier material yield and nesting planning
- Appearance usually needs veneer, paint or edge treatment
- Exposed edges require finishing
- Moisture behaviour is product- and grade-dependent
Solid hardwood
Oak
Hardwood
- Machining Good
- Stability Good
- Best for Furniture, structural
Maple
Hardwood
- Machining Good
- Stability Good
- Best for Detail work, instruments
Walnut
Hardwood
- Machining Good
- Stability Moderate–Good
- Best for Premium decorative
Cherry
Hardwood
- Machining Good
- Stability Good
- Best for Furniture, architectural
Softwood
Pine
Softwood
- Machining Very good
- Stability Moderate
- Best for Prototypes, signs
Cedar
Softwood
- Machining Very good
- Stability Moderate
- Best for Decorative, selected outdoor
Spruce
Softwood
- Machining Good
- Stability Moderate
- Best for Lightweight panels, models
MDF and plywood
MDF
Engineered panel
- Machining Excellent
- Structure Uniform, no grain
- Best for Painted parts, molds, panels
Plywood
Engineered panel
- Machining Good
- Strength Higher than MDF
- Best for Structural panels, furniture
Oak vs Maple vs Walnut for CNC Machining
These three come up in almost every furniture and decorative enquiry. They are compared here by what each does well — not ranked, because there is no universal best.
Oak
Chosen for durability and a distinctive open grain that reads clearly even after finishing. A common starting point for furniture components and parts that need to look substantial and wear well.
Maple
Chosen for a fine, uniform grain and a smooth appearance. Well suited to detail-oriented work where a clean, consistent surface matters more than dramatic figure — instrument components and fine furniture being typical examples.
Walnut
Chosen for a premium dark grain and decorative value. Usually specified where the wood itself is the visual feature rather than a substrate for paint.
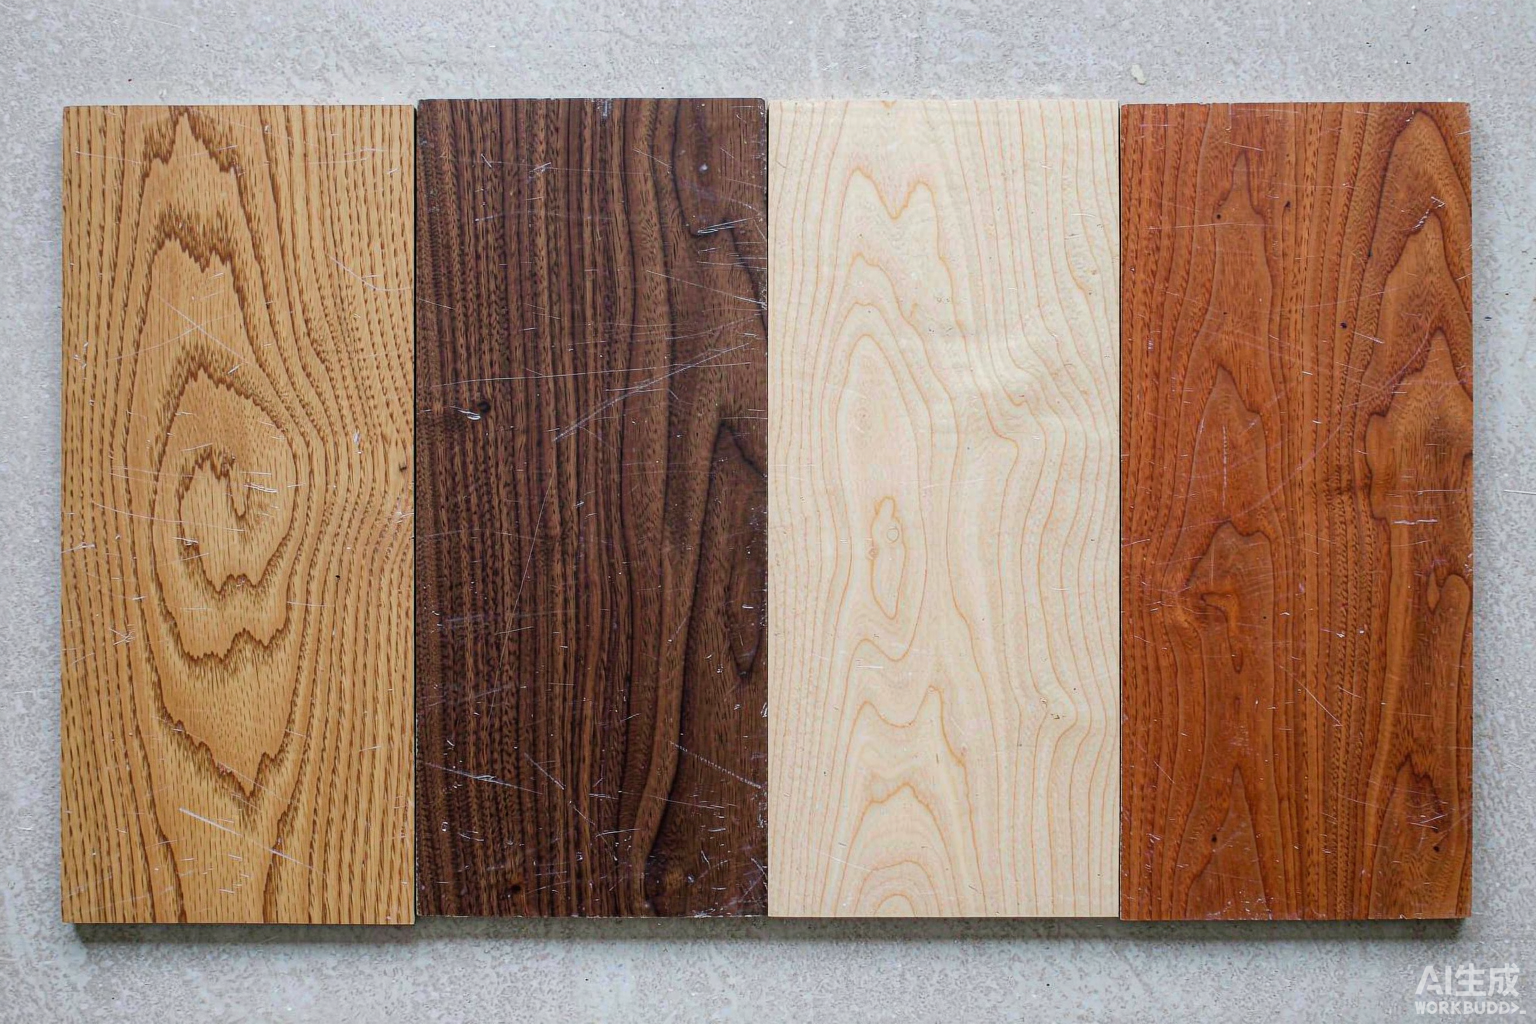
The best choice depends more on application and finish requirements than on a universal "best wood" ranking. A painted cabinet door and a visible walnut inlay are solving completely different problems with the same machine.
MDF vs Plywood for CNC Machining
The most common sheet-material decision in cabinet work, shop fittings and prototypes.
| Factor | MDF | Plywood |
|---|---|---|
| Surface uniformity | Excellent | Good |
| Grain | None | Veneer / grain visible |
| CNC detail | Excellent | Good |
| Structural strength | Lower | Higher |
| Painting | Excellent | Good |
| Moisture resistance | Limited unless specified | Grade dependent |
| Typical use | Panels, molds, painted parts | Furniture, structural components |
Which Wood Is Best for Different CNC Applications?
A more useful question than "which wood is best" is "which wood is best for this part".
| Application | Recommended starting materials | Main reason |
|---|---|---|
| Furniture components | Oak, maple, walnut | Appearance plus strength |
| Cabinet components | MDF, plywood, maple | Stable sheet material and finish quality |
| CNC signs | Pine, cedar, MDF | Easy machining and good appearance |
| 3D carving | Basswood, MDF, selected hardwoods | Detail capability and uniform structure |
| Architectural models | MDF, plywood, hardwood | Consistency and machinability |
| Prototypes | MDF, plywood, pine | Cost and availability |
| Decorative parts | Walnut, maple, cherry | Grain figure and finish |
| Structural panels | Plywood | Strength and dimensional stability |
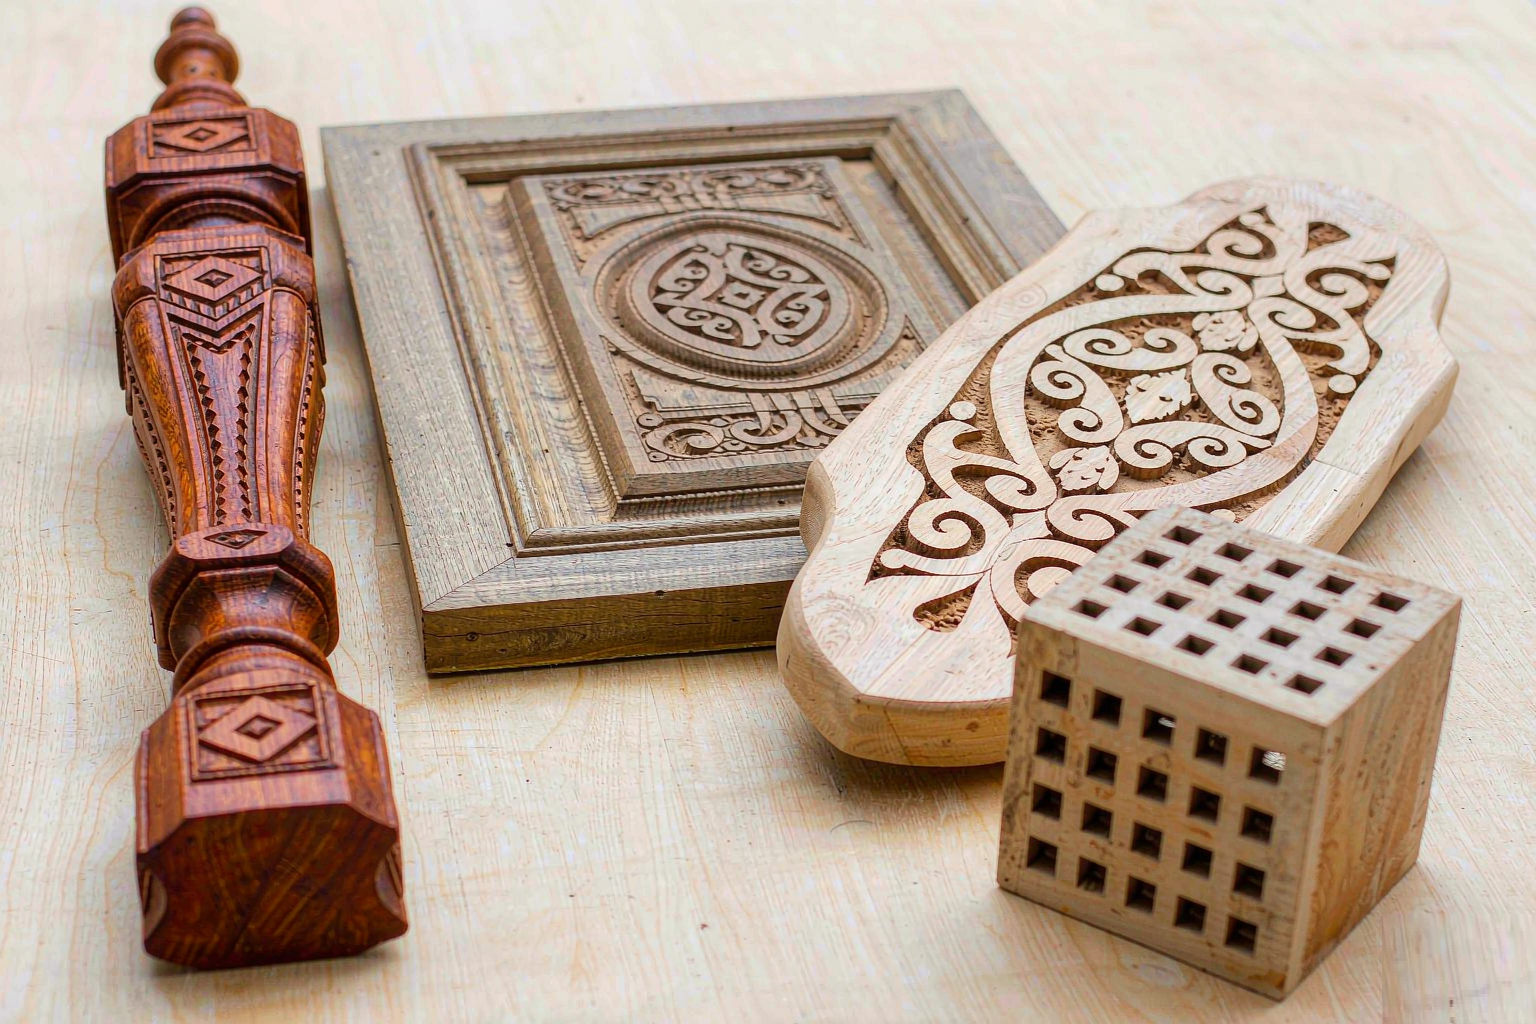
How Wood Grain Affects CNC Machining
Wood is anisotropic — its mechanical behaviour changes with direction relative to the grain. That single fact drives most edge-quality problems in CNC wood work.
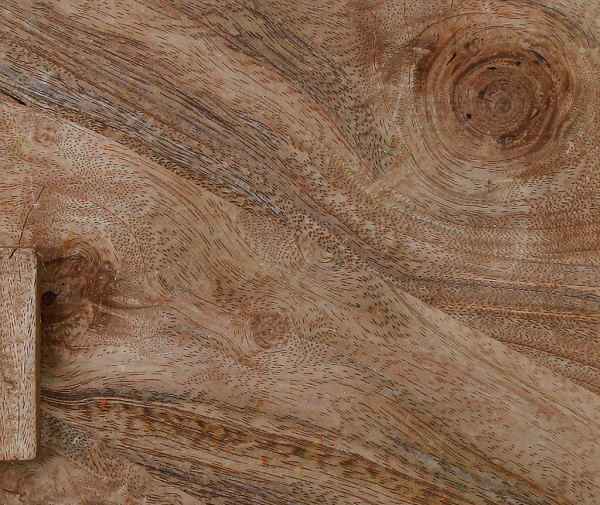
Grain direction
Cutting with the grain and cutting against it do not behave the same way. Toolpath direction relative to grain is a real process variable, not a finishing detail.
End grain
End grain is the most demanding orientation for edge quality and typically the first place tear-out appears on a part.
Tear-out and chipping
Most tear-out traces back to grain orientation, tool condition or cutting direction — rarely to the machine itself.
What this means in practice
Grain orientation is an important machining consideration, especially when edge quality and visible surface finish matter. "Clear grain" is not automatically a better CNC material — it is one factor among several.
Why Moisture Content and Wood Stability Matter
Wood is a hygroscopic material. It takes up and releases moisture until it reaches equilibrium with the surrounding air — and it changes dimension while doing so.
The chain that matters for CNC work is simple: moisture content → dimensional movement → machining accuracy.
Before machining
Stock that is not conditioned for its service environment can move after material is removed, because machining releases internal stress and exposes new surfaces.
During machining
Material that is stable at the spindle holds feature geometry more consistently. Unstable stock may measure correctly on the machine and drift afterwards.
After delivery
A part machined in one climate and shipped to another will respond to the new environment. This is a material property, not a machining defect.
Wood should be conditioned appropriately for its intended service environment, but a single target figure quoted without context is not useful. The right requirement depends on species, end use, climate, indoor or outdoor service, and whether the part is solid wood or an engineered panel. We confirm the requirement for your application rather than applying a default.
Choosing CNC Router Bits for Wood
Bit geometry is chosen against the job — chip evacuation, surface quality, sheet material or 3D form. The categories that matter most:
Upcut spiral
Flutes lift chips up and out of the cut.
Use for deep pockets and slots where chip evacuation is the priority.
Downcut spiral
Flutes push chips down, pressing the top surface fibres against the work.
Use for clean top-surface edges on visible faces.
Compression
Combines upcut and downcut geometry in one bit.
Use for sheet goods and laminated surfaces where both faces must stay clean.
Straight / straight flute
Neutral geometry, general-purpose cutting.
Use for straightforward profiling and general routing.
Ball nose
Rounded tip leaves a scalloped surface whose size depends on stepover.
Use for 3D carving and contoured surfaces.
V-bit
Angled profile produces a cut that varies in width with depth.
Use for engraving, lettering and fine detail.
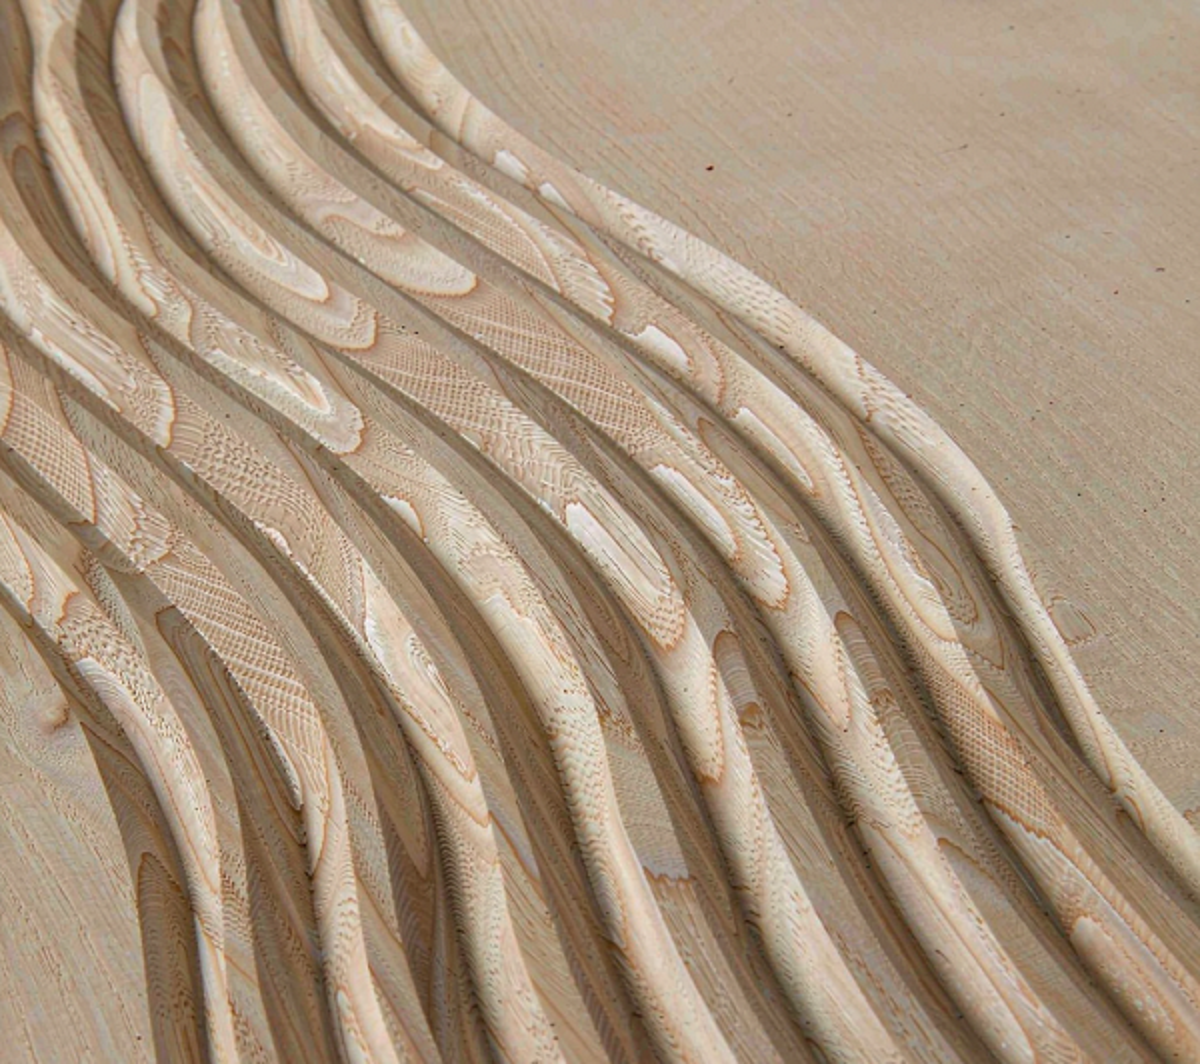
Cutting Parameters for CNC Wood Machining
Four variables decide whether a wood cut is clean or burned, sharp-edged or fuzzy. We describe them by relationship rather than by number, because the correct values depend on the specific machine, bit, material and geometry.
Set in relation to bit diameter and material. Larger diameters and harder species generally call for different combinations than small bits in soft material; the aim is a clean cut rather than a fast one.
Feed and spindle speed must be balanced. Too slow relative to the cut generates heat and burn marks; too fast risks tear-out, chipping and poor edge quality.
Deeper cuts remove more material per pass but increase load, deflection and heat. Multiple shallower passes usually give better edge quality and more predictable results than one aggressive pass.
Sets the minimum internal corner radius and directly affects chip evacuation, rigidity and the depth that can reasonably be taken per pass.
Specific speed and feed figures quoted without the machine, bit geometry, material and part geometry are not transferable — they are a starting guess at best. We establish parameters during process development for the actual job and document what works.
Common CNC Wood Machining Problems
Most defects have a small number of recurring causes. This is the diagnostic table we work from.
| Problem | Likely cause |
|---|---|
| Tear-out | Grain direction or tooling not suited to the cut |
| Chipping | Tool condition or cutting direction |
| Burn marks | Excessive heat from unsuitable cutting conditions or a worn tool |
| Fuzzy edges | Tool condition or material characteristics |
| Warping | Moisture content or internal stress in the stock |
| Dimensional variation | Material movement or insufficient workholding |
| Poor surface finish | Toolpath strategy, tool geometry or feed conditions |
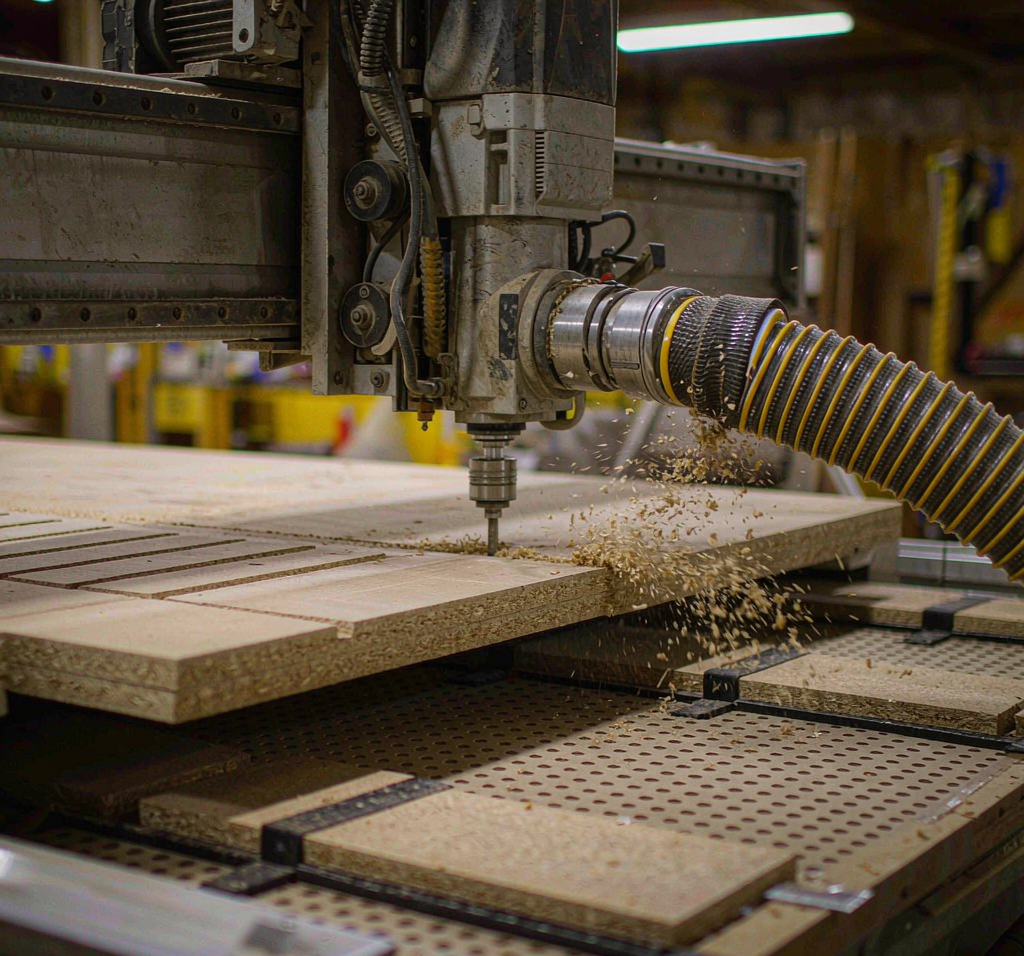
Dust Collection and Workholding
In wood CNC, dust extraction and workholding are process controls — they affect cut quality, dimensional consistency and the working environment at the same time.
Dust extraction and chip evacuation
Routers generate a high volume of fine dust and chips. Effective extraction keeps the cutting zone clear, reduces re-cutting of chips, improves visibility of the cut and controls airborne dust at source — which is why local extraction at the tool is treated as standard practice in woodworking operations.
Workholding
Vacuum tables hold sheet goods flat over a large area with no clamps in the toolpath. Mechanical clamps suit irregular or thick stock. Either way, the workpiece must not move: movement during cutting shows up as dimensional variation and poor edge quality.
How Accurate Can CNC Wood Machining Be?
Achievable dimensional accuracy depends on material stability, machine capability, tooling, workholding, feature geometry and environmental conditions. Wood should not be treated like a dimensionally stable metal.
A machine may position very accurately and still produce a part that measures differently a week later, because the material responded to humidity. That is why we separate two ideas on wood projects: machine accuracy and final part dimensional stability. They are not the same number, and quoting a metal-style tolerance for a wood part usually creates false expectations on both sides.
Where tight fits matter, the practical approach is to design for the material's behaviour, condition the stock for the service environment, and specify which features genuinely need control.
Can All Types of Wood Be CNC Machined?
Most commercially available solid woods and engineered wood products can be machined with the appropriate tooling and cutting strategy. But "can be machined" does not mean "is the best choice".
Highly variable stock, excessive moisture, hidden internal defects, knots, voids or unstable material can all make machining less predictable — producing inconsistent edge quality, movement after machining and higher scrap rates. Where a part will be visible or must assemble reliably, material selection up front is usually cheaper than solving those problems at the machine.
If you are unsure whether your preferred species is practical for a given geometry, send the model and we will say so during review.
How to Choose the Right Wood for Your Part
Three questions usually settle it.
Natural appearance → hardwood. Low-cost prototype → MDF, plywood or a selected softwood. Structural sheet → plywood. Painted or highly uniform surface → MDF. Premium visible furniture → oak, maple or walnut. High dimensional stability requirement → carefully conditioned material, with engineered wood where the application allows it.
Need Help Choosing a CNC Wood Material?
Send us the details and our engineers will review the part geometry and recommend a suitable wood material and machining approach.
- Part drawing or 3D model
- Required quantity
- Intended application
- Required finish
- Preferred wood species, if known
Material selection is part of the quotation review — not an afterthought.
CNC Wood Material FAQs
The questions buyers ask when specifying a wood part.
There is no single best wood. Hardwoods such as oak, maple and walnut suit visible furniture and decorative parts; softwoods such as pine and cedar suit prototypes, signs and lightweight parts; MDF and plywood suit stable, repeatable panel work and painted components. The right answer depends on appearance, stability, strength, finish and environment.
No. Hardwood generally offers better wear and a finer appearance, but softwoods machine readily and cost less, which makes them practical for prototypes, signs and lightly loaded parts. Engineered panels outperform both where dimensional consistency and yield planning matter most.
Yes. MDF machines very cleanly because it has no grain and a uniform structure, which makes it excellent for detailed work, painted parts, molds and panels. Its limitations are lower structural strength and limited moisture resistance unless a specific grade is specified.
It depends on the job. MDF gives a more uniform surface and better fine detail and takes paint extremely well. Plywood is stronger, performs better structurally and is grade-dependent for moisture. Neither is universally better.
Basswood, MDF and selected fine-grained hardwoods are common starting points because they hold detail without excessive tear-out. The bit geometry and stepover strategy matter as much as the species.
Yes, significantly. Wood is anisotropic, so cutting with, across or into end grain produces different edge quality. Grain orientation is an important machining consideration wherever visible surfaces and clean edges matter.
Because wood moves as it gains or loses moisture. Stock that is not conditioned for its service environment can change dimension after machining, which affects fit, flatness and assembly. The right requirement depends on species, end use, climate and panel versus solid wood — not on one universal figure.
Most commercial solid woods and engineered wood products can be machined with suitable tooling, but being machinable is not the same as being the best choice. Variable stock, high moisture, knots, voids or internal defects make results less predictable.
Accuracy depends on material stability, machine capability, tooling, workholding, feature geometry and environment. Wood should not be treated like a dimensionally stable metal: machine accuracy and final part dimensional stability are two different things, and the material's moisture response is often the limiting factor.
Yes. Send a drawing or 3D model, the quantity, the intended application, the required finish and any preferred species. We review the geometry and recommend a material and machining approach as part of the quotation.