Two-shot injection molding — also written 2K molding — forms two materials or two colors in one production cycle. A first shot builds the rigid base, then the tool rotates or a core retracts, and a second shot adds the soft-touch, sealing, or colored layer. Multi-shot molding is the broader term; this page covers two-material, two-stage parts and what must be verified before tooling: material compatibility, interface design, mold structure, color boundaries and production economics.
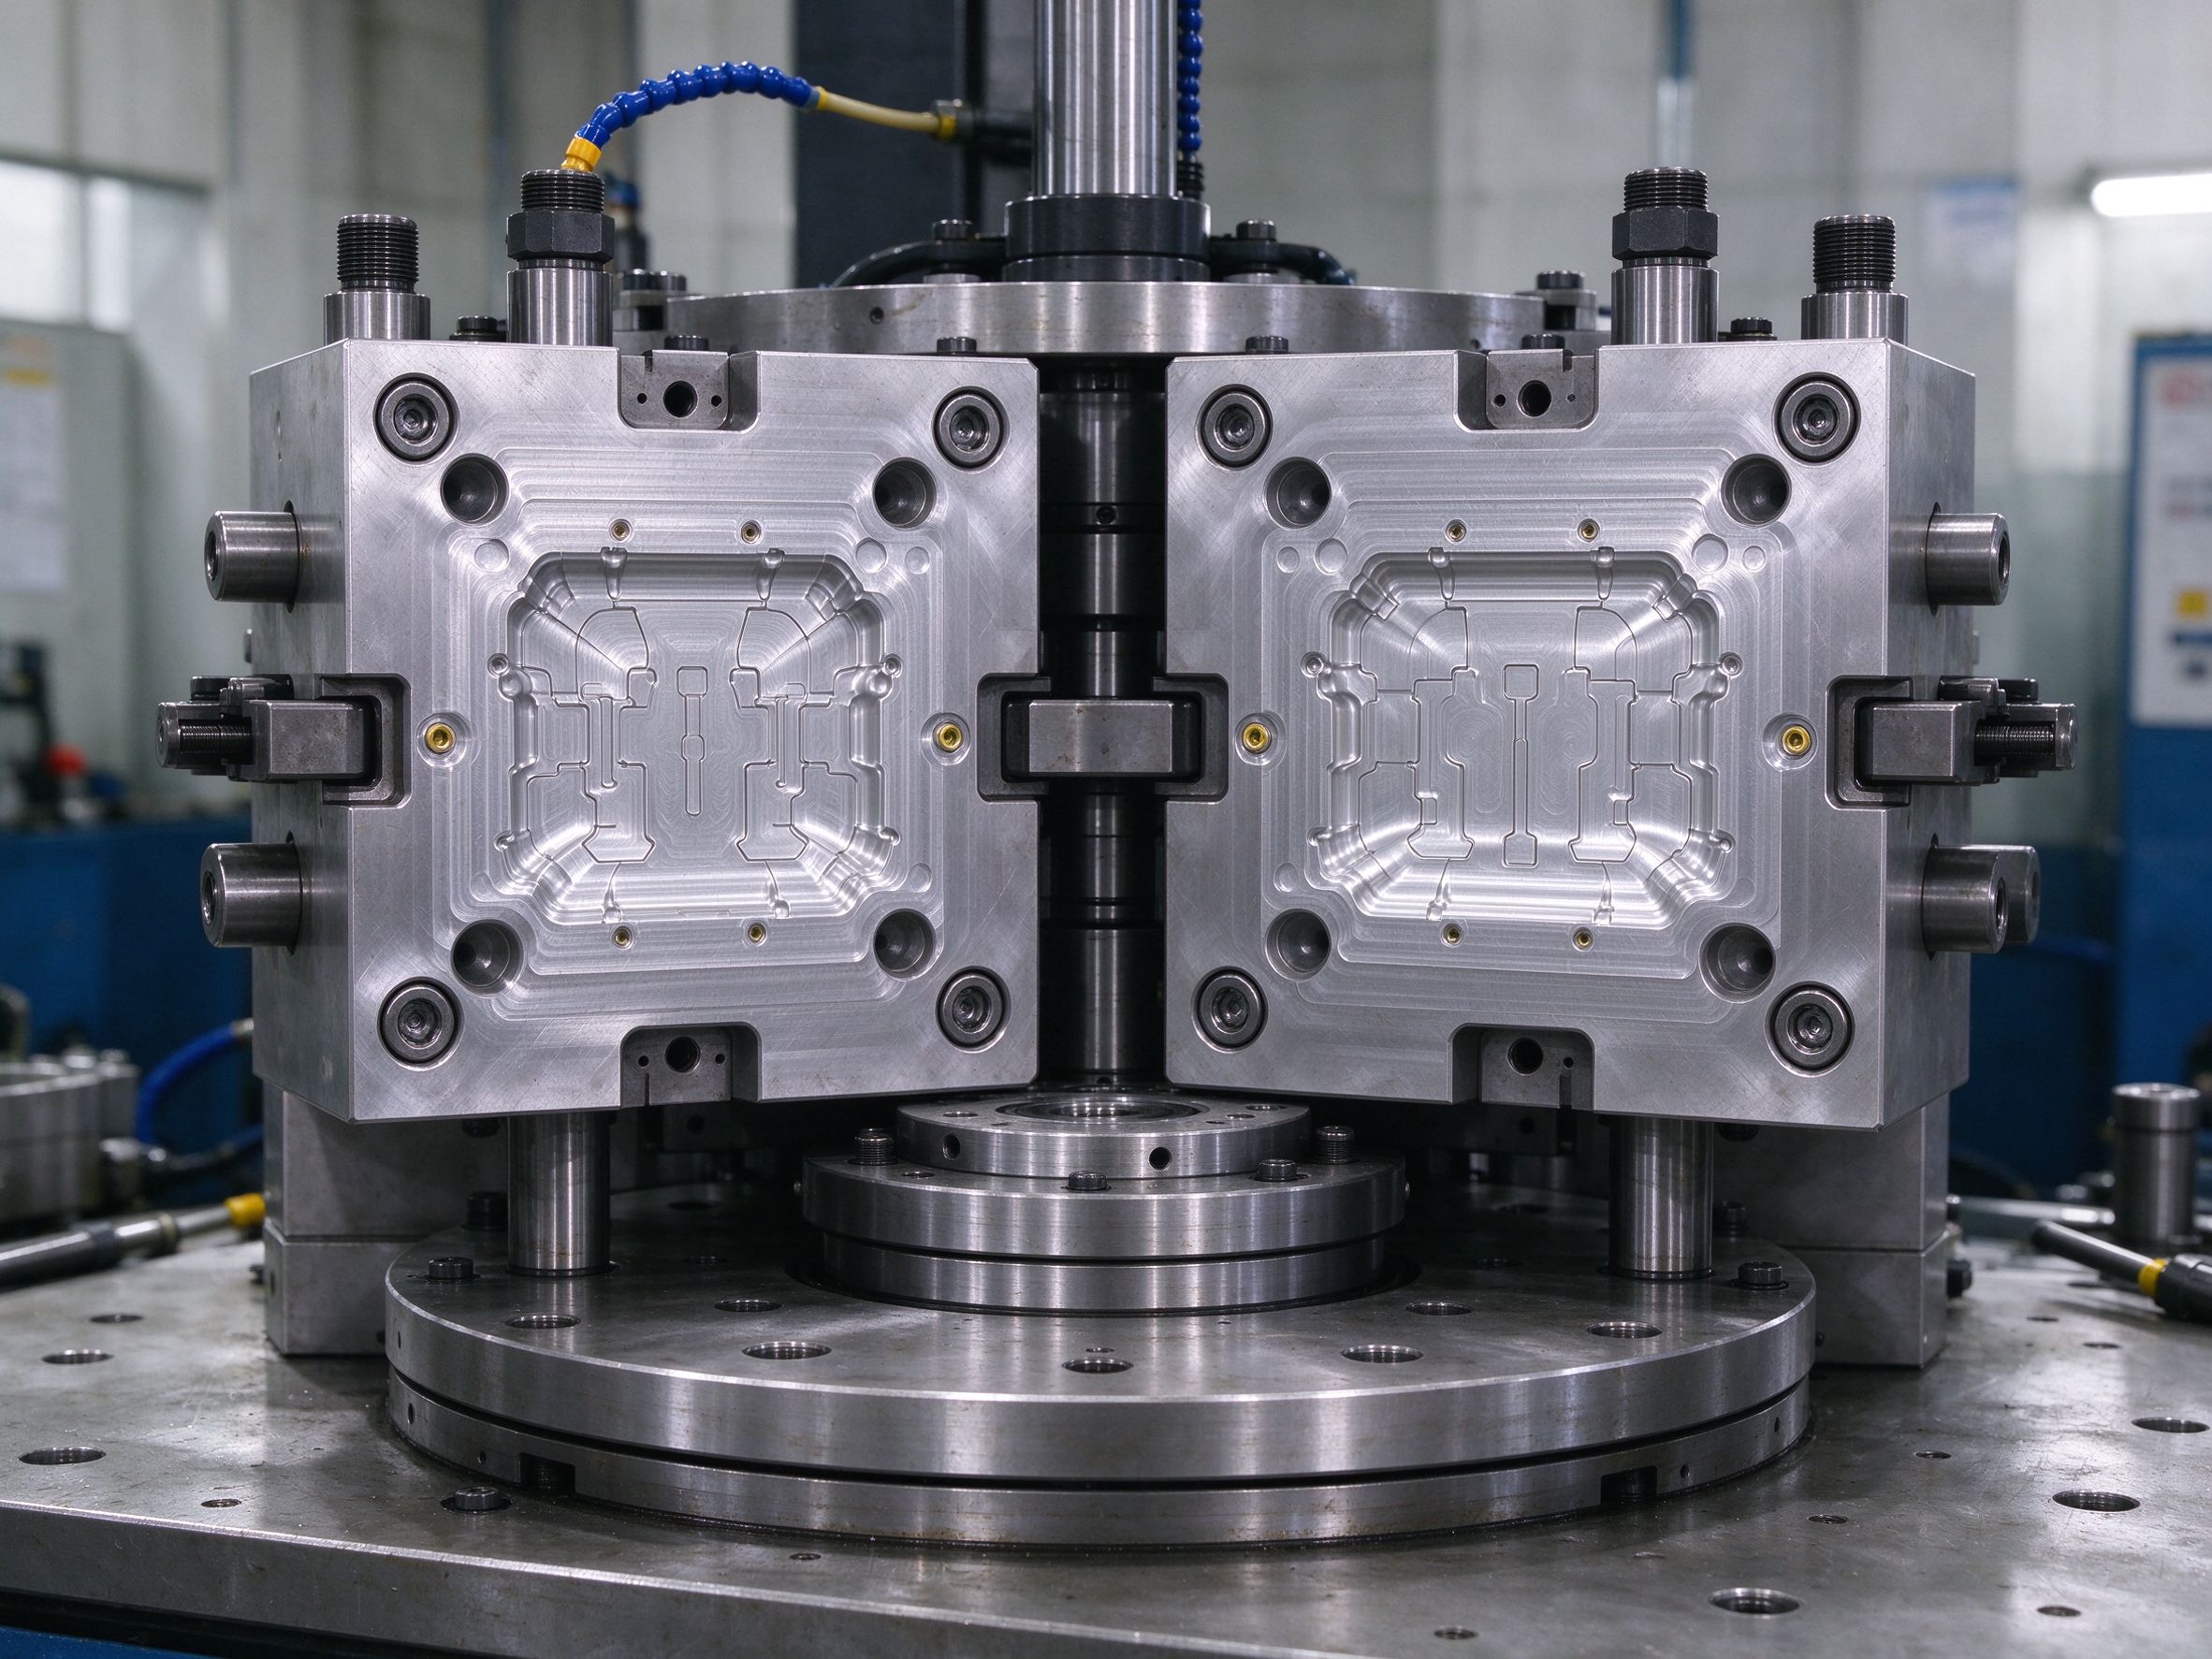
Two-shot / 2K molding suits parts that genuinely need two materials or two colors in one integrated part. The value comes from functional integration, controlled color boundaries, or reduced assembly. The trade-off is a more complex mold and a longer setup than single-material molding. Before tooling, the specific resin grades, interface geometry, thermal window and production volume need to be reviewed — candidate combinations are not a guarantee of adhesion until validated.
How Two-Shot / 2K Molding Works
- First shot — the rigid base material fills the first cavity set.
- Tool position change — the mold rotates, a core retracts, or the part transfers to the second station.
- Second shot — the second material or color is injected over, around or against the first-shot part.
- Ejection — the finished two-material part is ejected from the closed mold.
Two-shot and 2K normally describe two injection stages with two materials or two colors. Multi-shot is broader and can cover three or more stages — the actual number this page supports is two materials in two stages. Any higher-shot work would be confirmed against equipment and tooling before quoting.
Three Mold Routes, Not a Ranking
| Mold route | Look at it when | Must be confirmed |
|---|---|---|
| Rotary / indexing | Two materials formed continuously in one cycle at separate stations | Indexing accuracy, machine compatibility, cycle and tooling complexity |
| Core-back | Part geometry allows a retracting core to open space for the second shot | Structural feasibility, shut-off, slide mechanisms and ejection |
| Transfer / two-station | The first-shot part moves physically to a second position | Transfer location, part stability, machine layout and handling |
The route is chosen by part geometry, material, volume, quality requirements and available equipment. Rotary and core-back tools are built and validated at Goldcattle on a per-project basis; if a route needs outside collaboration, the quote states it rather than presenting it as in-house capability.
Material Compatibility: Candidate Pairs Must Be Verified
| Rigid substrate | Second material (example) | Typical goal | What to verify |
|---|---|---|---|
| ABS | Compatible TPE grade | Grip, soft touch, operating parts | Grade compatibility, interface adhesion, color boundary |
| PC | TPE / TPU | Housings, protection, flexible contact areas | Substrate heat resistance, grade selection, warpage |
| PC/ABS | TPE | Electronic and industrial housings, functional areas | Material pairing, dimensional and appearance stability |
| PP | Compatible TPE grade | Covers, lids, flexible features | Specific formulation adhesion, mechanical locks if needed |
| PA / nylon | Compatible TPE grade | Tools, industrial functional parts | Reinforcement fillers, substrate thermal behavior, interface stability |
| Same resin, two colors | Different masterbatch of the same family | Two-color appearance, part marking | Color difference, boundary, shrinkage mismatch |
These are candidate combinations, not a guarantee that every grade in the family bonds reliably. Compatibility is confirmed from material supplier data, the specific resin grades, processing conditions and the actual use environment. Where the application depends on it, samples validate chemical bonding, mechanical interlock and final part function.
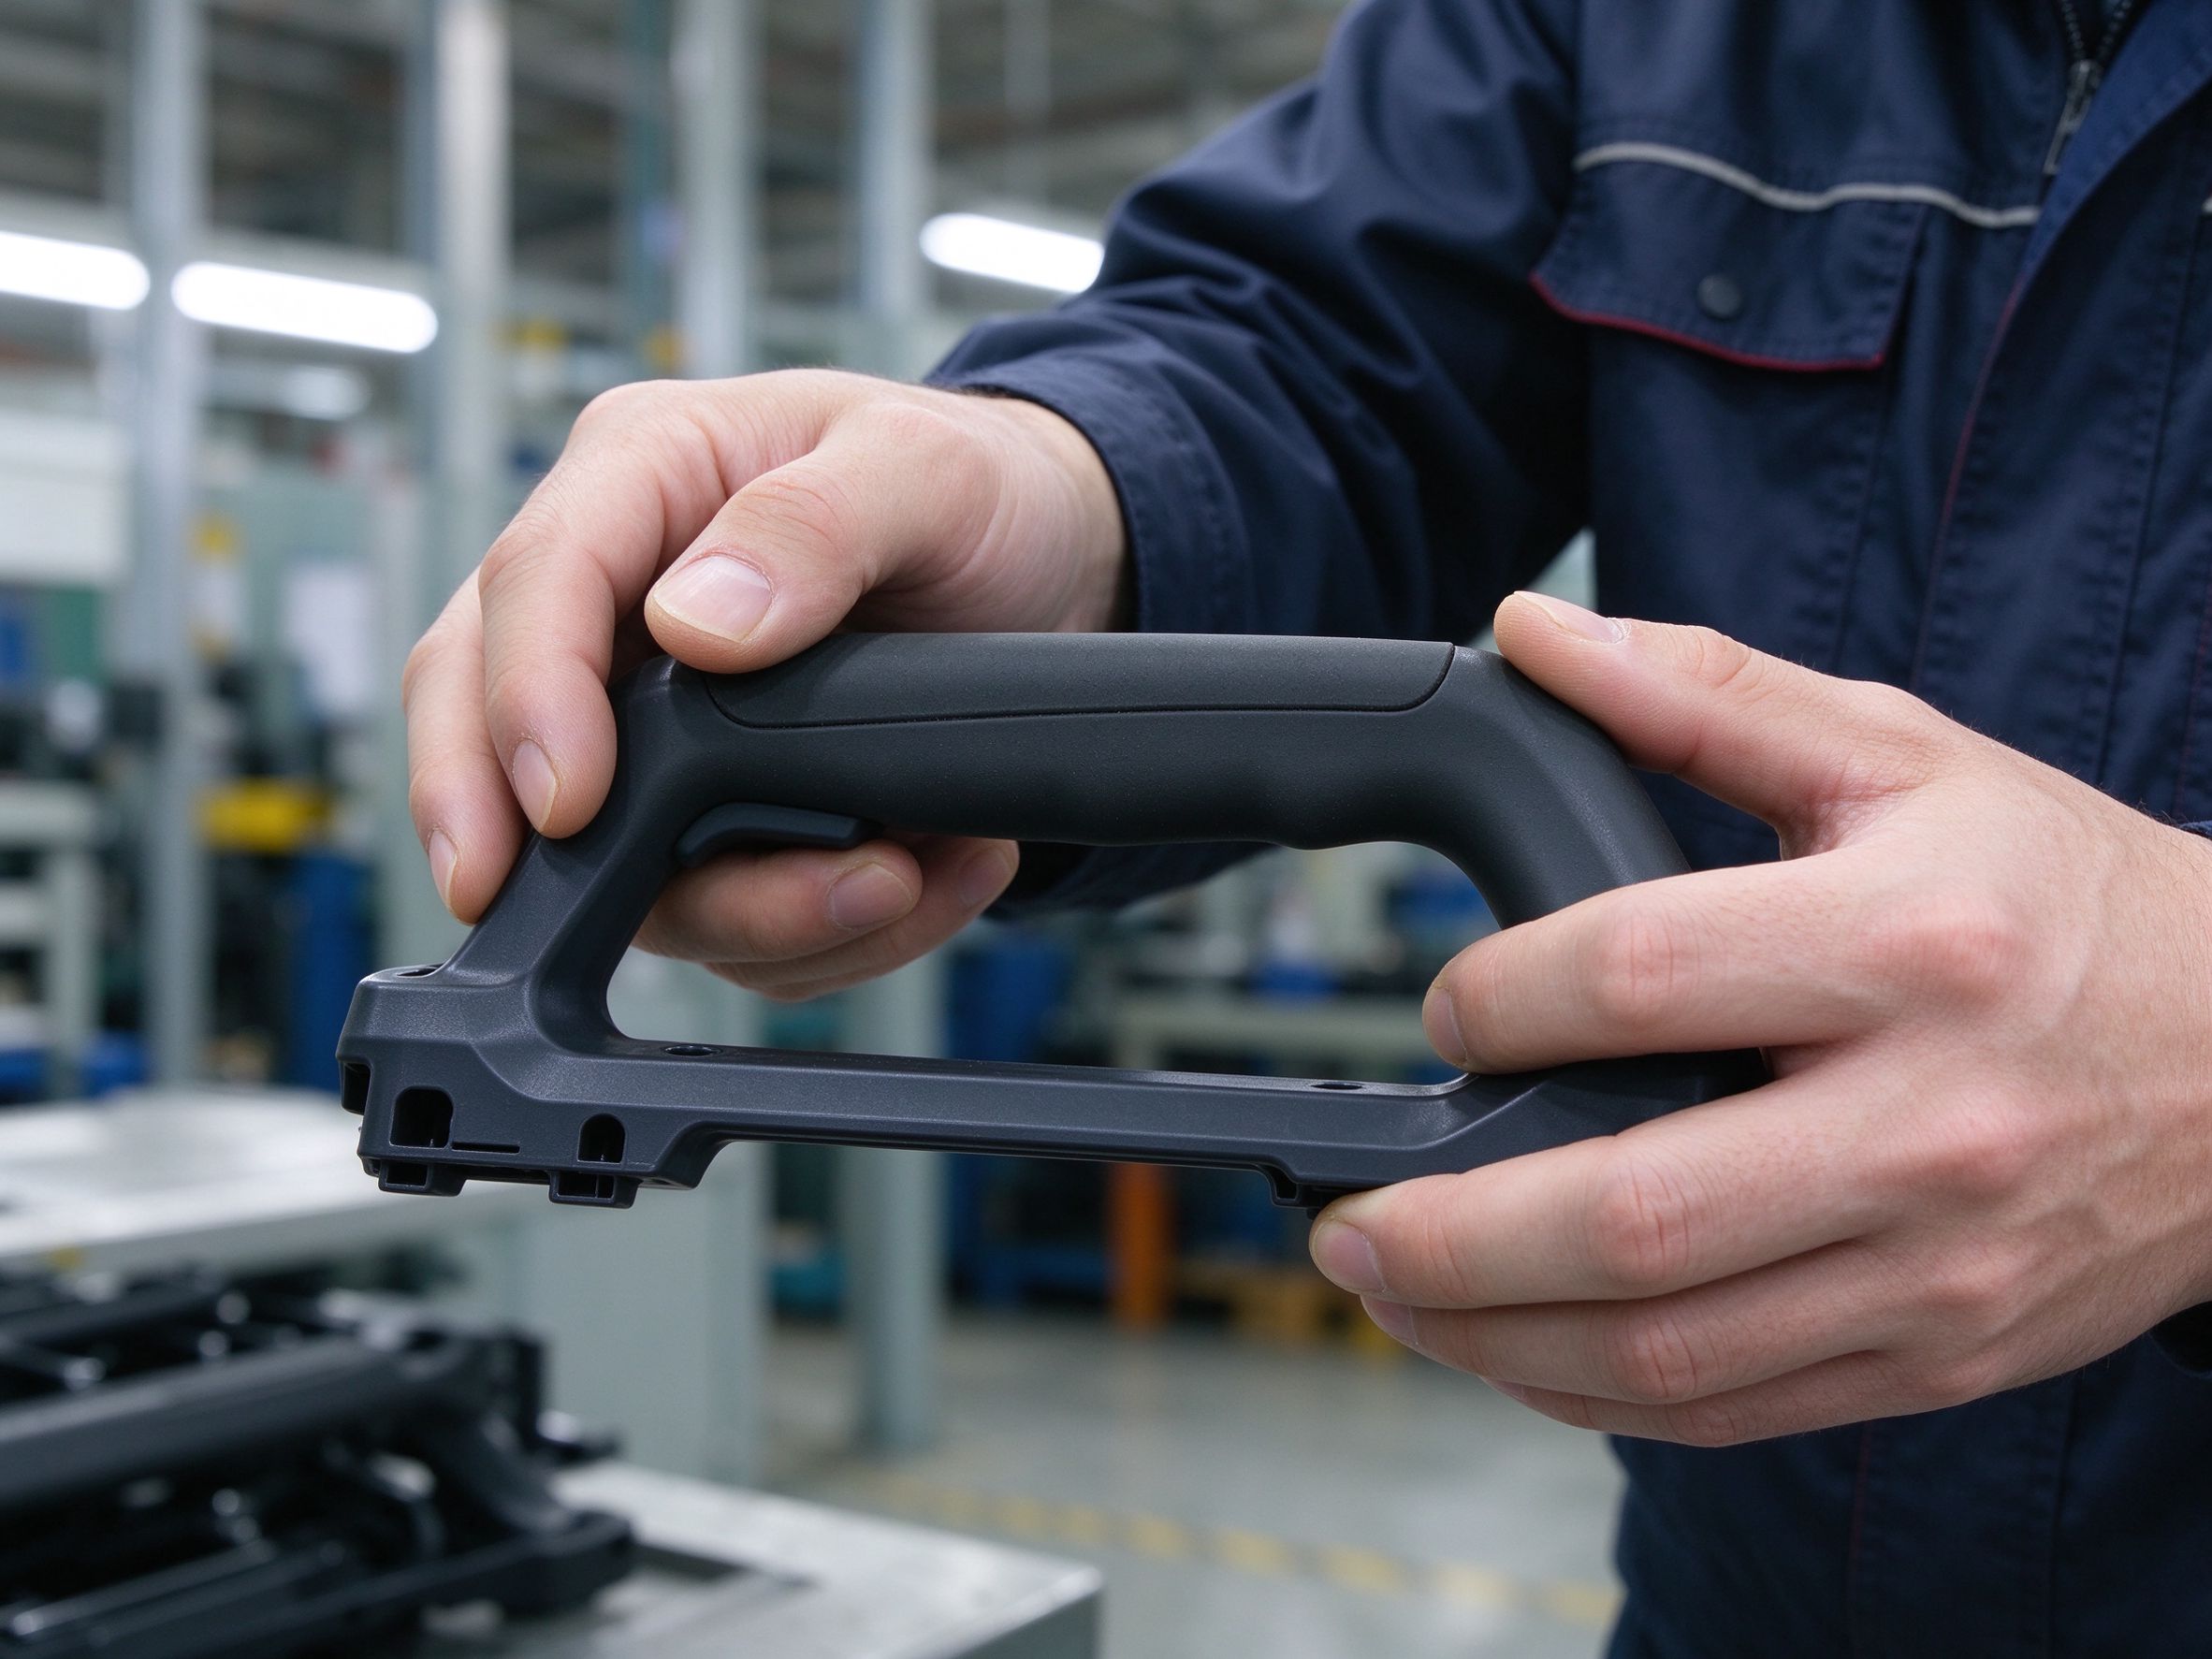
Two-Shot DFM: What a Review Should Return
A useful two-shot DFM review covers these points before tooling starts:
| DFM checkpoint | What the buyer gets |
|---|---|
| First-shot filling and wall thickness | Identification of fill risk, local thickness and substrate deformation |
| Second-shot coverage and thickness | Identification of under-coverage, local over-thickness or uneven layering |
| Gate and runner layout | Flow path assessment for both materials and appearance risk |
| Shut-off and color boundary | Flash control and boundary position on visible surfaces |
| Material and thermal window | Risk of second shot softening or deforming the first-shot part |
| Cooling and warpage | Cooling mismatch and dimensional stability across the part |
| Interface design | Whether mechanical interlock is needed and how the interface is validated |
| Critical tolerance review | Separation of critical dimensions from general tolerances |
| Tooling and cycle feasibility | Mold approach, equipment needs, cycle and quote assumptions |
Bond, Dimensional and Appearance Validation
| Validation area | What is checked |
|---|---|
| Dimensional inspection | Critical dimensions, datum structure, tolerance stack at the material boundary |
| Interface inspection | Interface completeness, separation, unfilled areas and applicable defects |
| Bond / adhesion validation | Method and acceptance criteria matched to the application where adhesion matters |
| Color boundary and appearance | Boundary position, flash, surface defects and color consistency |
| Functional / assembly checks | Final assembly, sealing, operation or customer-specified function |
| Durability / environmental testing | Planned against temperature, humidity or chemical exposure when the product requires it |
| Process and batch documentation | Material certificates, first-article reports and batch records as agreed |
Plastic part tolerances follow plastic molding standards such as ISO 20457, which ties dimensional deviation to material, part design, mold layout and processing conditions. The applicable tolerances and acceptance criteria are agreed per project rather than copied from metal machining assumptions.

Cost Drivers and Route Choice
| Cost factor | Impact on the quote | What to clarify |
|---|---|---|
| Two-shot tooling architecture | Rotary or core-back mechanisms add tooling investment | Which structure the part requires and which options exist |
| Material combination | Resin and elastomer cost and processing differ by grade | How the specific grades affect function, appearance and processing |
| Part size and machine requirements | Projected area, materials and mold size drive press selection | Available equipment and mold specification before quoting |
| Cavity count and automation | Higher output and automation change capacity and upfront cost | Whether the higher-capacity configuration pays for itself |
| Cosmetic and tolerance requirements | Special boundaries and critical dimensions add tooling and inspection work | Which features must be tight and which can use standard tolerances |
| Annual volume and product life | Tooling, maintenance and startup costs spread over expected volume | Lifecycle cost comparison instead of unit price alone |
| Assembly avoided | Two-shot can remove separate assembly, bonding and inspection steps | Which downstream costs are genuinely eliminated |
Compare three routes on the same volume, material, acceptance and product-life assumptions:
Two-shot / 2K
For parts that need two materials or two colors in one integrated cycle, where scale and process conditions support dedicated tooling.
Sequential overmolding
Base part molded first, second material overmolded in a later step. Mold and equipment requirements are confirmed per route.
Single material + assembly
When volume is low, bonding is not a critical property, or a proven low-cost assembly path already exists.
Two-shot is not automatically cheaper than assembly, and high volume does not automatically justify 2K. The comparison is made on tooling investment, piece manufacturing cost, secondary assembly cost and quality risk for the specific project.
Frequently Asked Questions
What is two-shot injection molding?
Is 2K injection molding the same as two-shot molding?
What is the difference between two-shot molding and overmolding?
What materials can be used for two-shot injection molding?
How do you prevent delamination between the two materials?
When is multi-shot molding worth the investment?
Request a Two-Shot Injection Molding Quote
Send the 3D model or 2D drawing, first- and second-shot materials (or ask for a material suggestion), estimated quantities and appearance requirements. The review covers DFM comments, mold route, material compatibility and validation scope before the tooling quote is issued.
Xiamen Goldcattle · Manufacturing since 1998 · Injection mold making and custom CNC machining · Related: how to compare China mold makers →