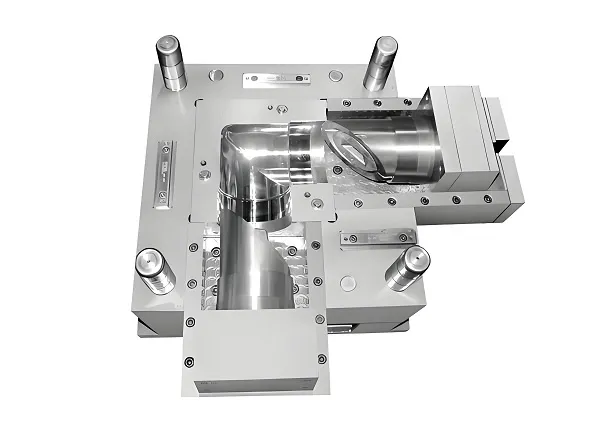
Plastic components used in chemical-processing and fluid-handling equipment must be selected for the actual media, concentration, operating temperature, exposure duration and mechanical load. Material compatibility alone does not establish that a finished component will work in service. Goldcattle reviews drawings and operating conditions for material fit, manufacturing route and validation scope.
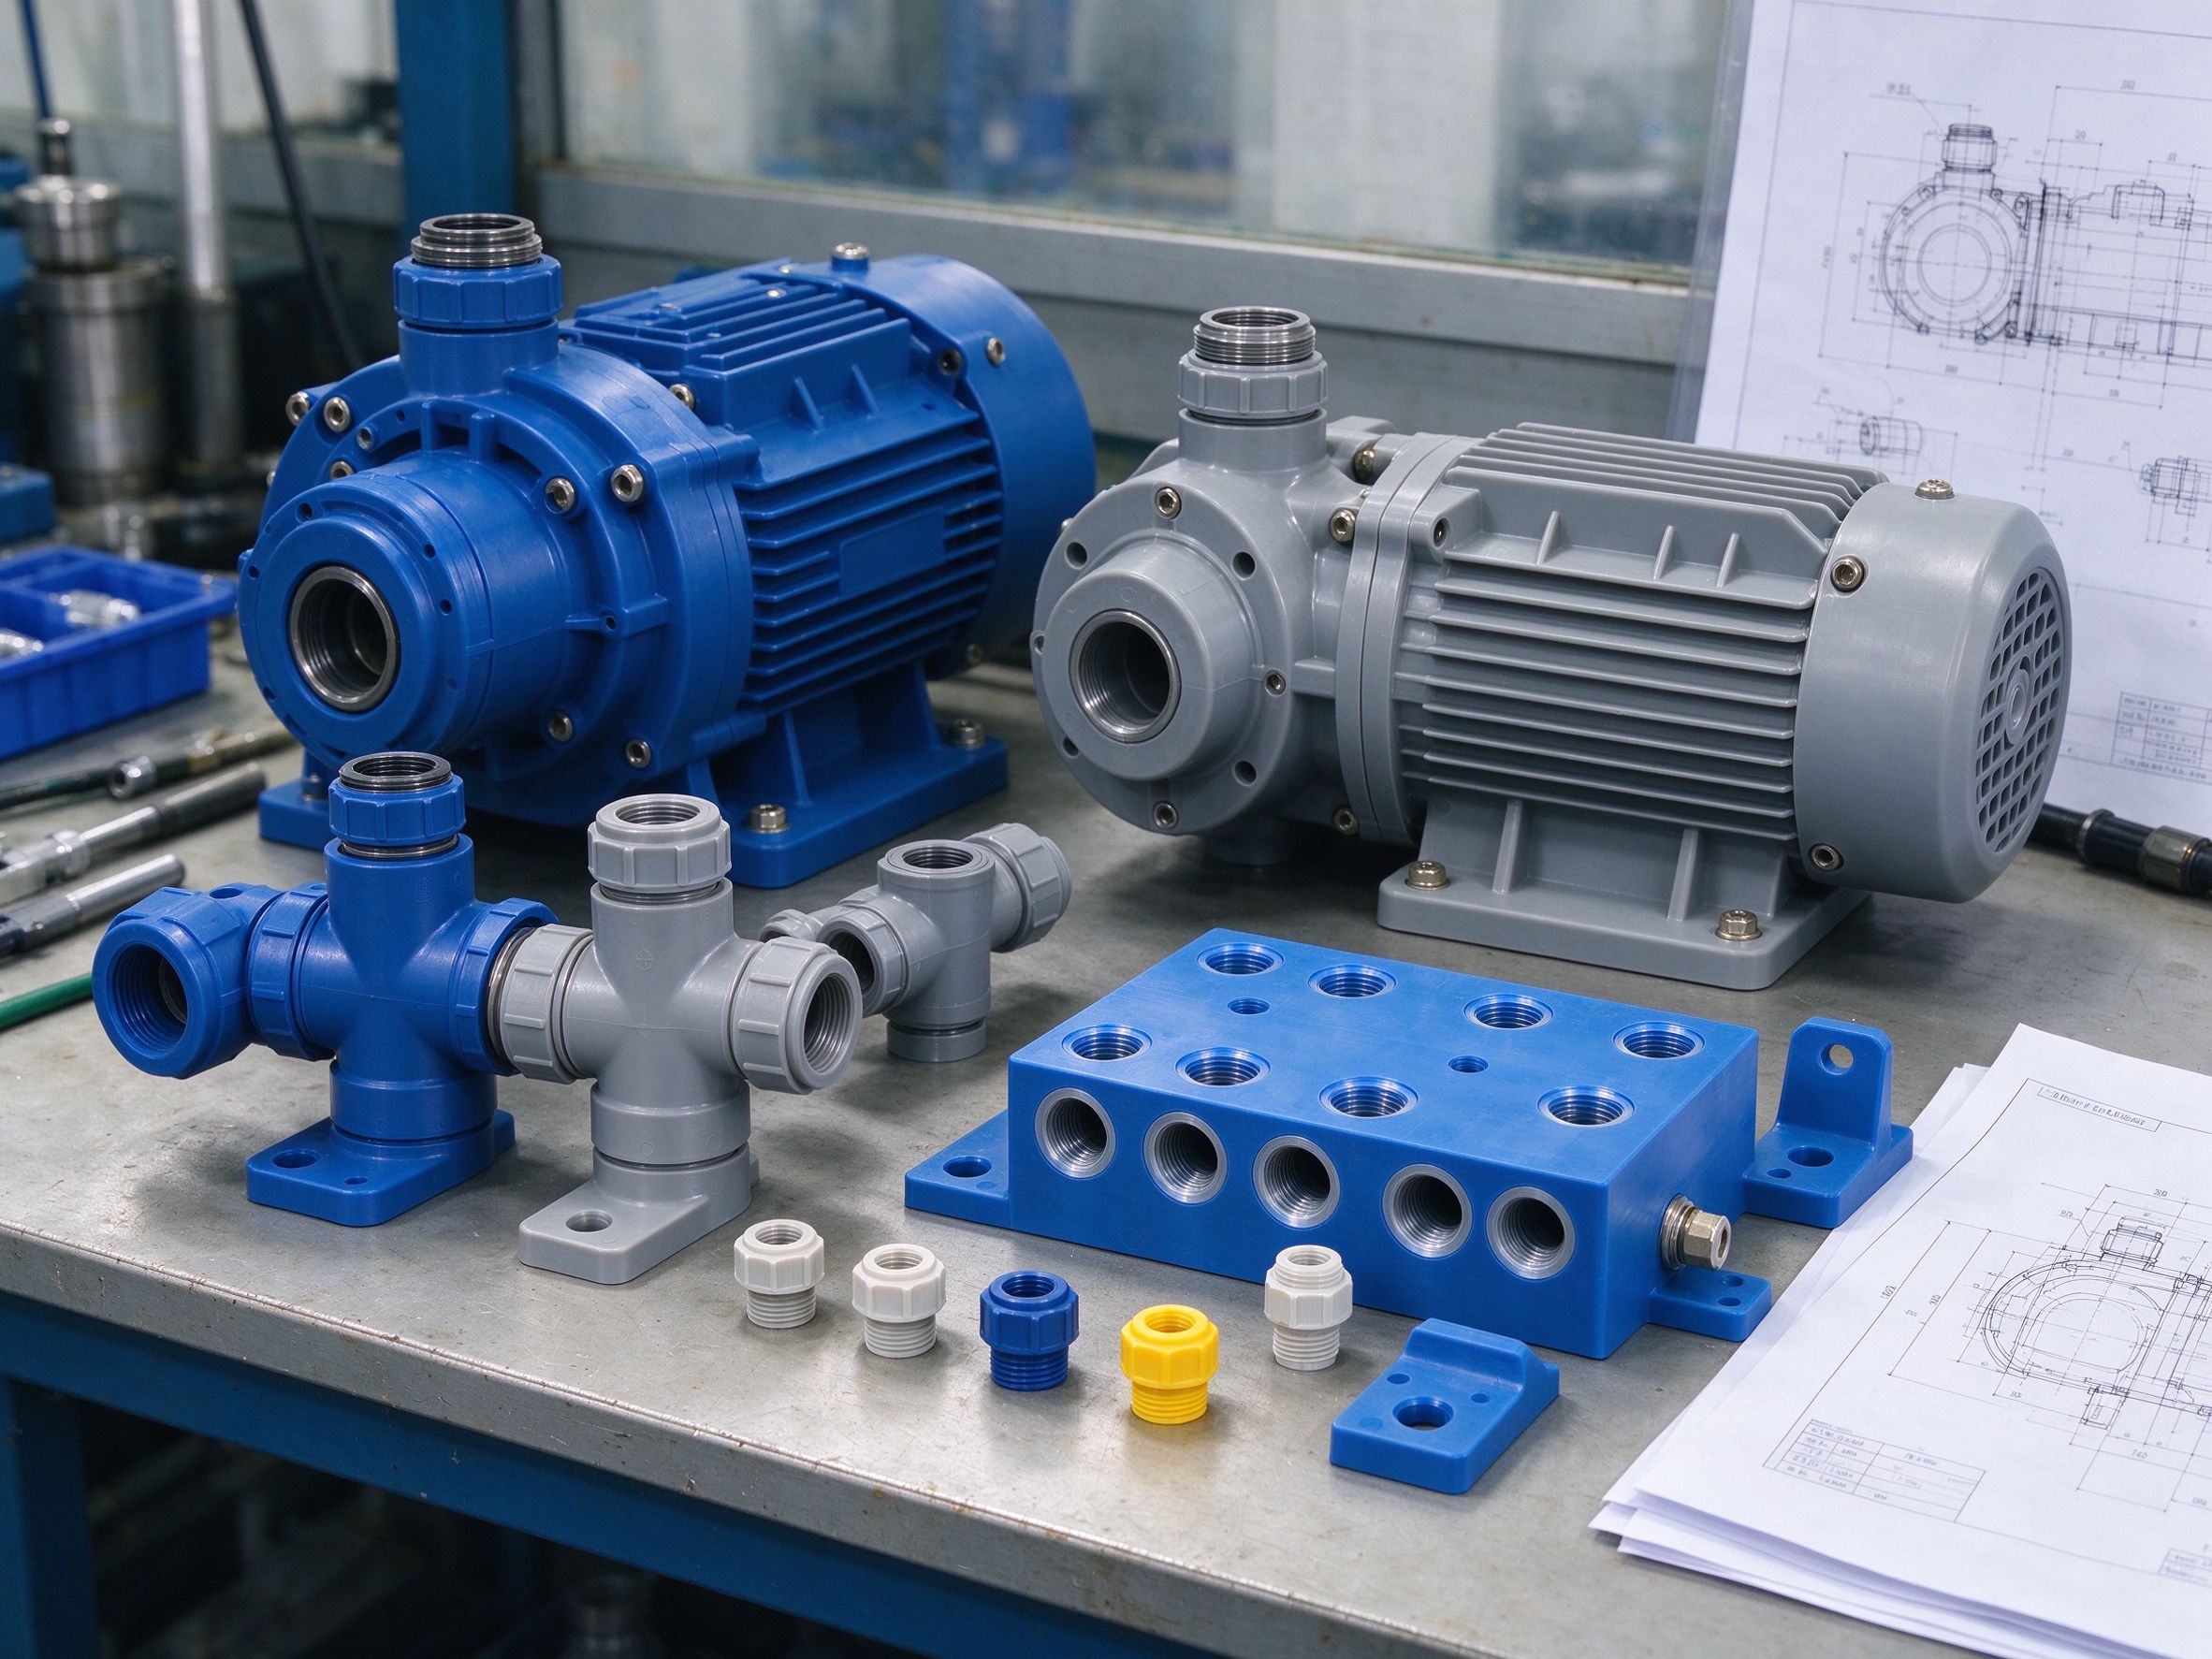
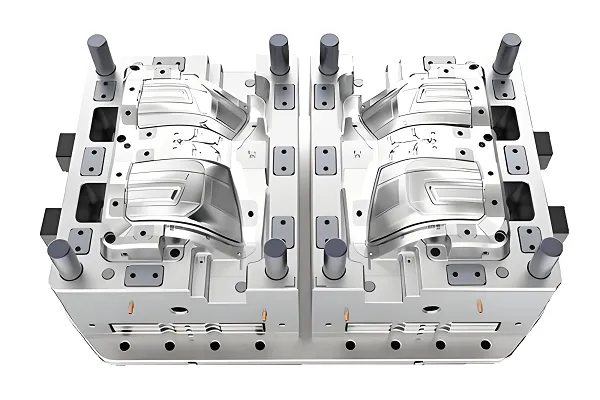
Chemical-resistant equipment components are parts for industrial equipment that contact specific chemicals or operate in chemically exposed environments. Suitability depends on medium, concentration, temperature, exposure time, mechanical load, resin grade and part design — not on the material name alone. Goldcattle evaluates custom plastic components through drawing review, material assessment and manufacturability checks, covering injection molding, CNC machining and combined routes where the geometry and volume call for them.
Components We Manufacture
| Component | Function | Review focus |
|---|---|---|
| Pump housings and covers | Contain fluid, support impeller or motor interface | Sealing faces, mounting interfaces, pressure exposure, material compatibility |
| Valve covers and selected valve components | Enclose valve body, connect actuator or ports | Port geometry, seal grooves, thread fit, dimensional stability |
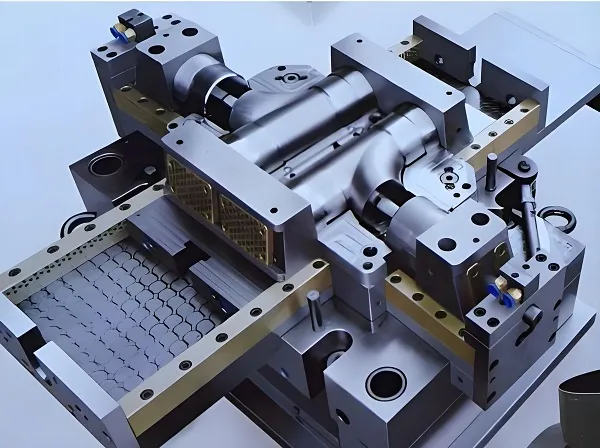
| Manifolds, blocks and fittings | Distribute flow across multiple ports | Internal channels, port threads, wall thickness, leakage paths |
| Equipment housings and covers | Protect equipment in splash or washdown conditions | Exposure type (splash, vapor, wash), UV and cleaning agents |
| Mounting brackets and supports | Hold components in place in exposed environments | Load, fastener holes, creep under sustained load, environmental exposure |
Parts that directly carry fluid or pressure are reviewed separately from structural parts that only sit in a chemical-exposed environment. The two groups have different material, sealing and validation requirements.
Application Environments
| Environment | Typical parts | Conditions to review |
|---|---|---|
| Chemical dosing and transfer | Dosing pump heads, injection fittings, transfer connectors | Chemical name and concentration, suction and discharge pressure, wetted surface |
| Water and wastewater treatment | Filter housings, valve bodies, distribution blocks | Disinfectants, pH range, water temperature, cleaning cycles |
| Washdown-exposed equipment | Covers, enclosures, brackets, cable glands | Detergent chemistry, spray frequency, ambient temperature, splash vs immersion |
| Industrial fluid-control equipment | Valve components, adapters, flow-control parts | Seal compatibility, port standards, torque on assembly, leakage criteria |
Operating Conditions Before Selecting a Resin
- Chemical identity — exact chemical name or mixture; unknown blends and cleaners need separate review.
- Concentration and impurities — concentration changes compatibility; additives and contaminants matter.
- Temperature range — minimum, maximum and normal operating temperature; compatibility tables shift with heat.
- Exposure duration and frequency — continuous immersion, intermittent contact, splash or vapor exposure behave differently.
- Contact type — wetted flow path versus external splash or washdown.
- Pressure and mechanical load — internal pressure, assembly torque, vibration and sustained clamp load.
- Cleaning and maintenance chemistry — detergents, sanitizers and lubricants used during service, not only the process fluid.
Preliminary Material Comparison
| Material | Considered direction | Limits to verify | Typical route |
|---|---|---|---|
| PP | Many aqueous acids, alkalis, brines and general equipment parts | Strong oxidizers, high concentration, elevated temperature and stress cracking | Injection molding |
| PE / HDPE | Liquid-handling parts, tanks accessories, impact-resistant structures | Solvent permeation, long-term exposure, creep and temperature | Injection molding / machined stock |
| PPS | Combined heat, chemical and mechanical requirements | Grade, filler and crystallization state; specific media check | Injection molding |
| PEEK | High-temperature, high-performance chemical and mechanical parts | Cost; does not replace compatibility testing for the actual medium | Injection molding / CNC from stock |
| PVDF | Selected corrosive fluid applications after confirmation | Grade, processing conditions and supply availability confirmed per project | Route reviewed per project |
| PTFE / PFA | Broad chemical inertness where other resins fall short | Not a standard injection-molding resin; compression molding, sintering or machining from stock may apply | Special forming / CNC, not standard molding |
This table is a starting screen, not a universal resistance rating. A resin compatible with one concentration or temperature can fail under another. Grade-level supplier data and project testing follow where conditions are critical.
DFM, Sealing Geometry and Process Route
- Wall thickness, ribs and local stress concentrations reviewed for creep and cracking risk.
- Threads, flanges, ports and connection interfaces matched to mating hardware.
- O-ring grooves, sealing faces and gasket compatibility defined before tooling.
- Insert molding or mechanical reinforcement considered where loads or threads require it.
- Shrinkage, dimensional stability and assembly tolerances accounted for in the drawing.
| Route | Fits when | Watch-outs |
|---|---|---|
| Injection molding | Repeat production, stable geometry, tooling cost justified by volume | Gate and weld-line position near seals; shrinkage and warpage control |
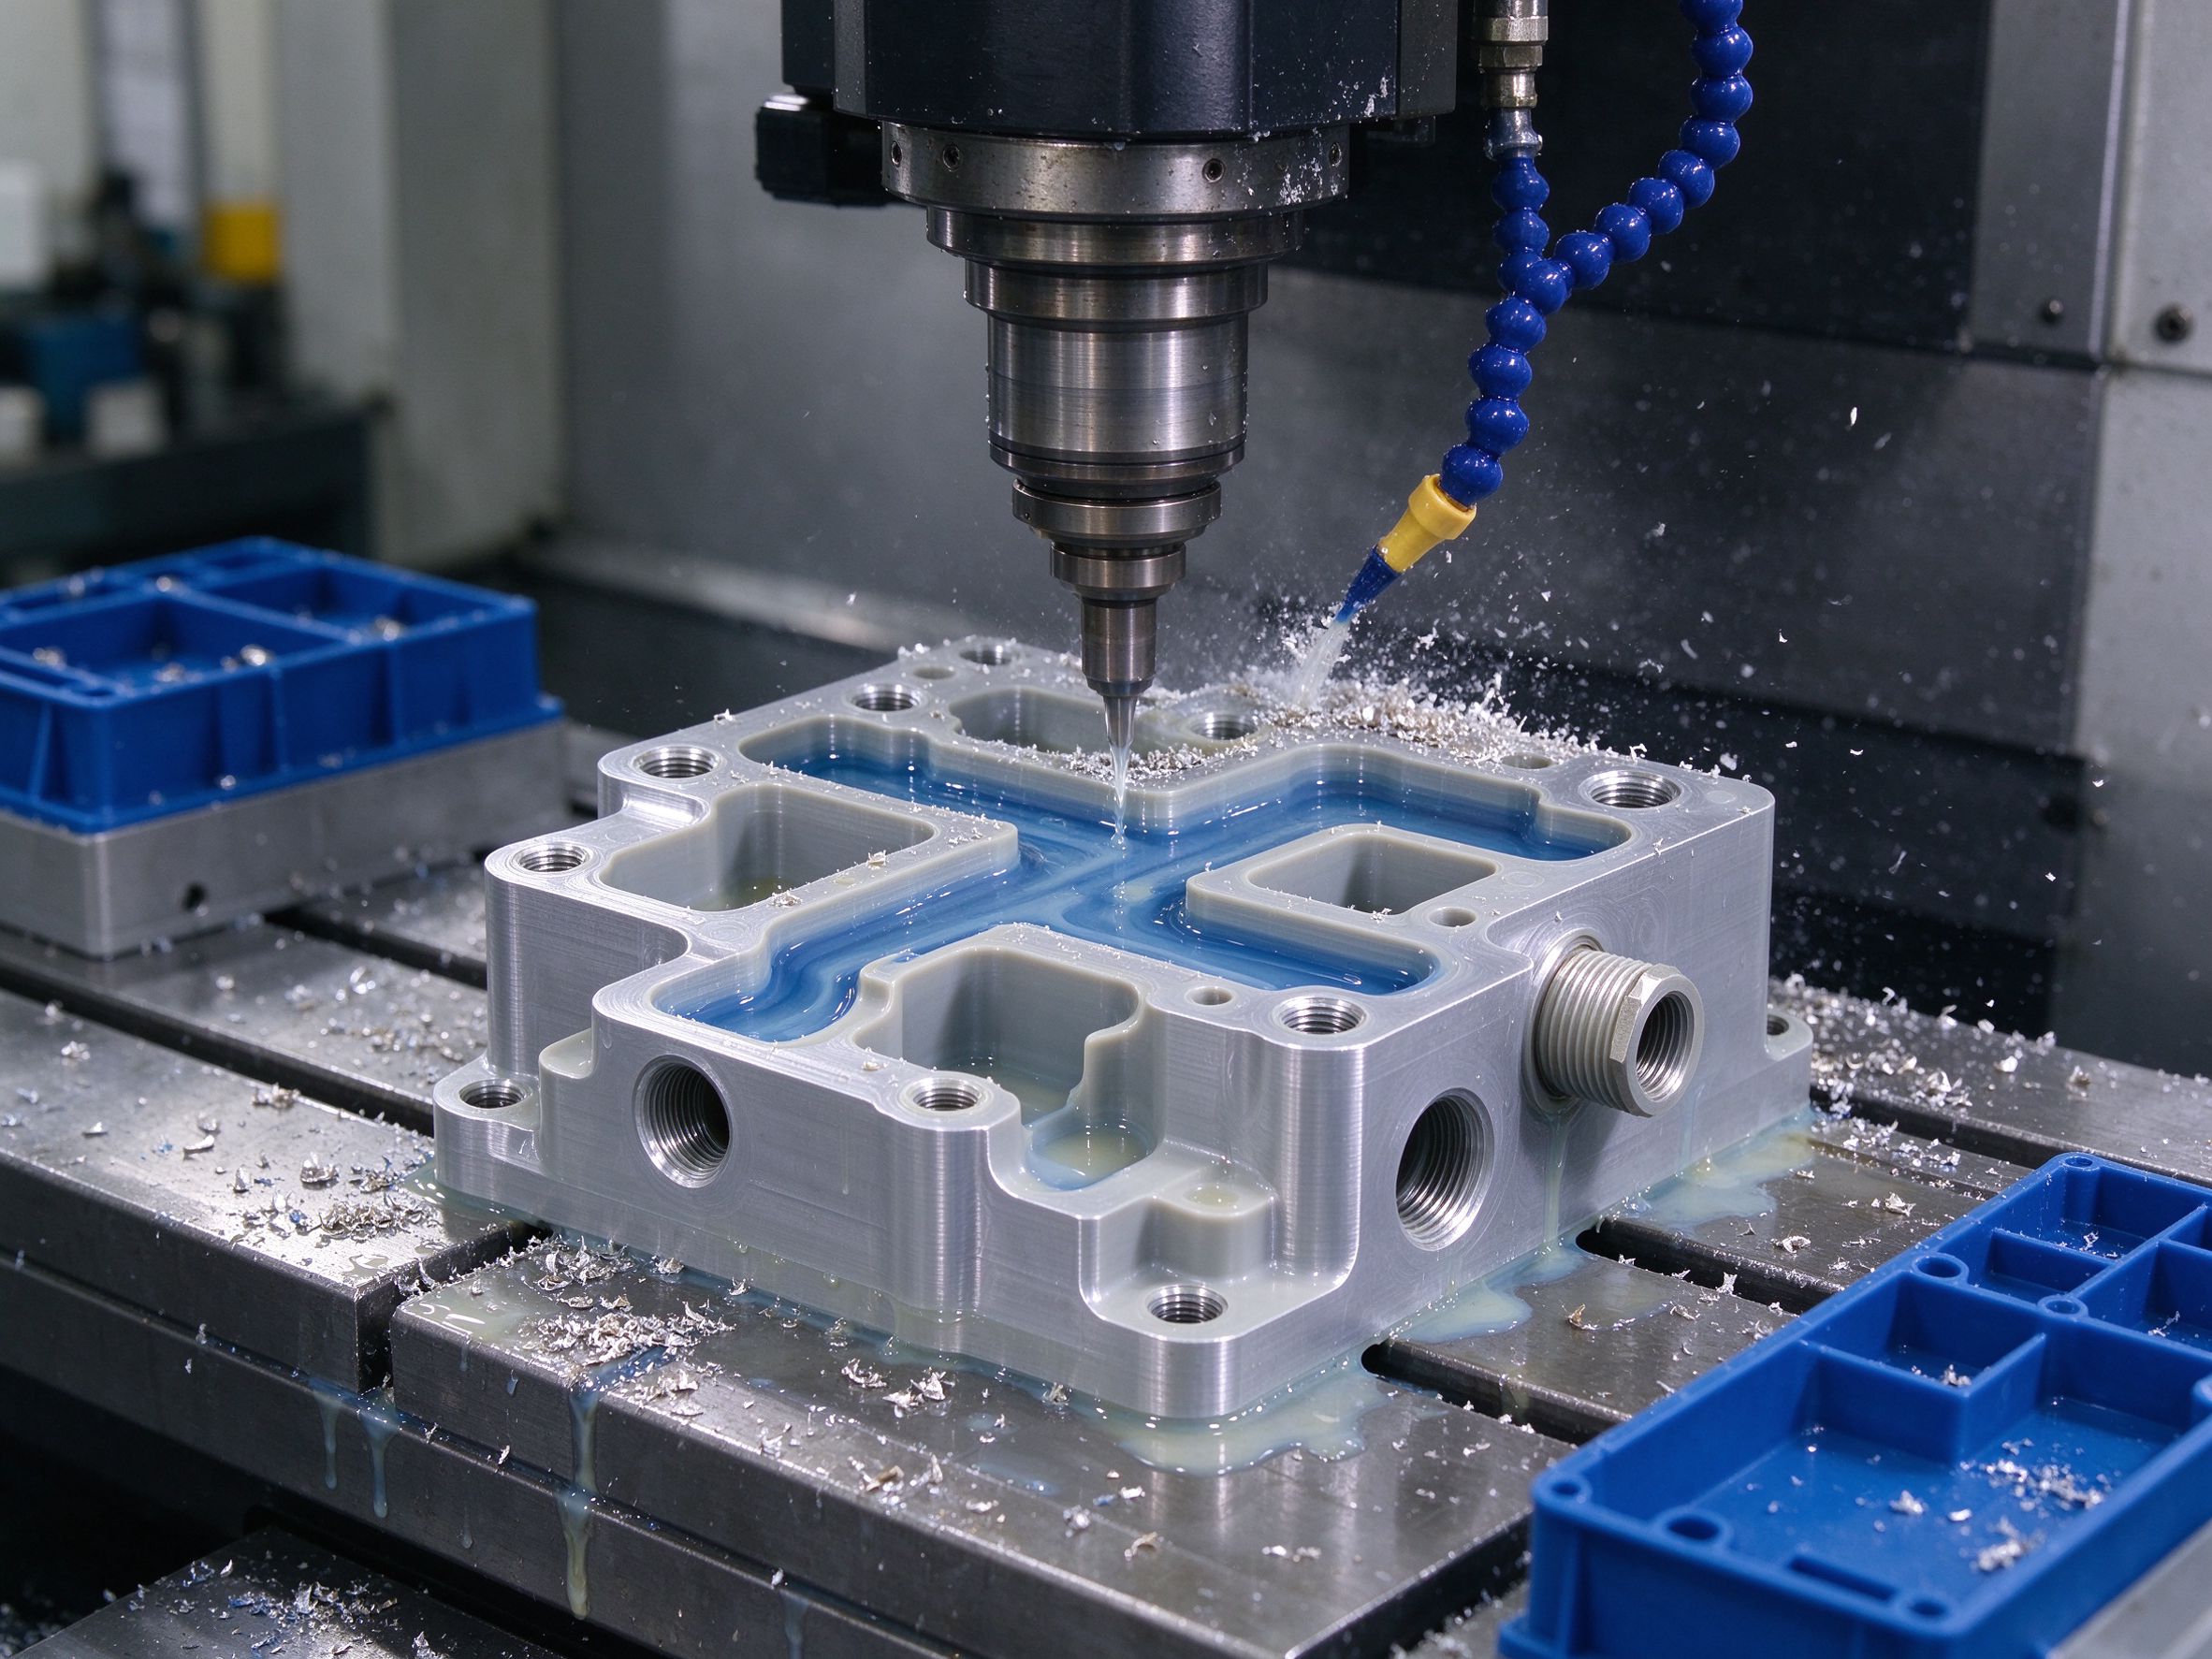
| CNC machining | Prototypes, lower volumes, stock shapes, complex internal channels | Resin stock availability, fiber orientation in filled grades, surface finish |
| Combined route | Molded body plus machined ports, seals or inserts | Interface tolerance and repeatability between operations |
Chemical compatibility, pressure capability and seal performance are separate engineering questions. A compatible resin does not by itself prevent leakage through a thread, weld line, sealing face or assembly load.
Validation Checklist
| Check | What is confirmed |
|---|---|
| Chemical exposure | Medium, concentration, temperature and exposure duration per project |
| Dimensional change | Dimensions and weight before and after exposure |
| Mechanical performance | Strength, stiffness and cracking after exposure where required |
| Stress cracking | Combined effect of chemical exposure and mechanical or residual stress |
| Leak / pressure test | Only for parts carrying pressure or sealing fluid; criteria set by the buyer |
| Thread and seal fit | Port thread, seal groove, gasket and mating interface compatibility |
| Material documentation | Resin grade, technical data sheet reference and batch traceability where agreed |
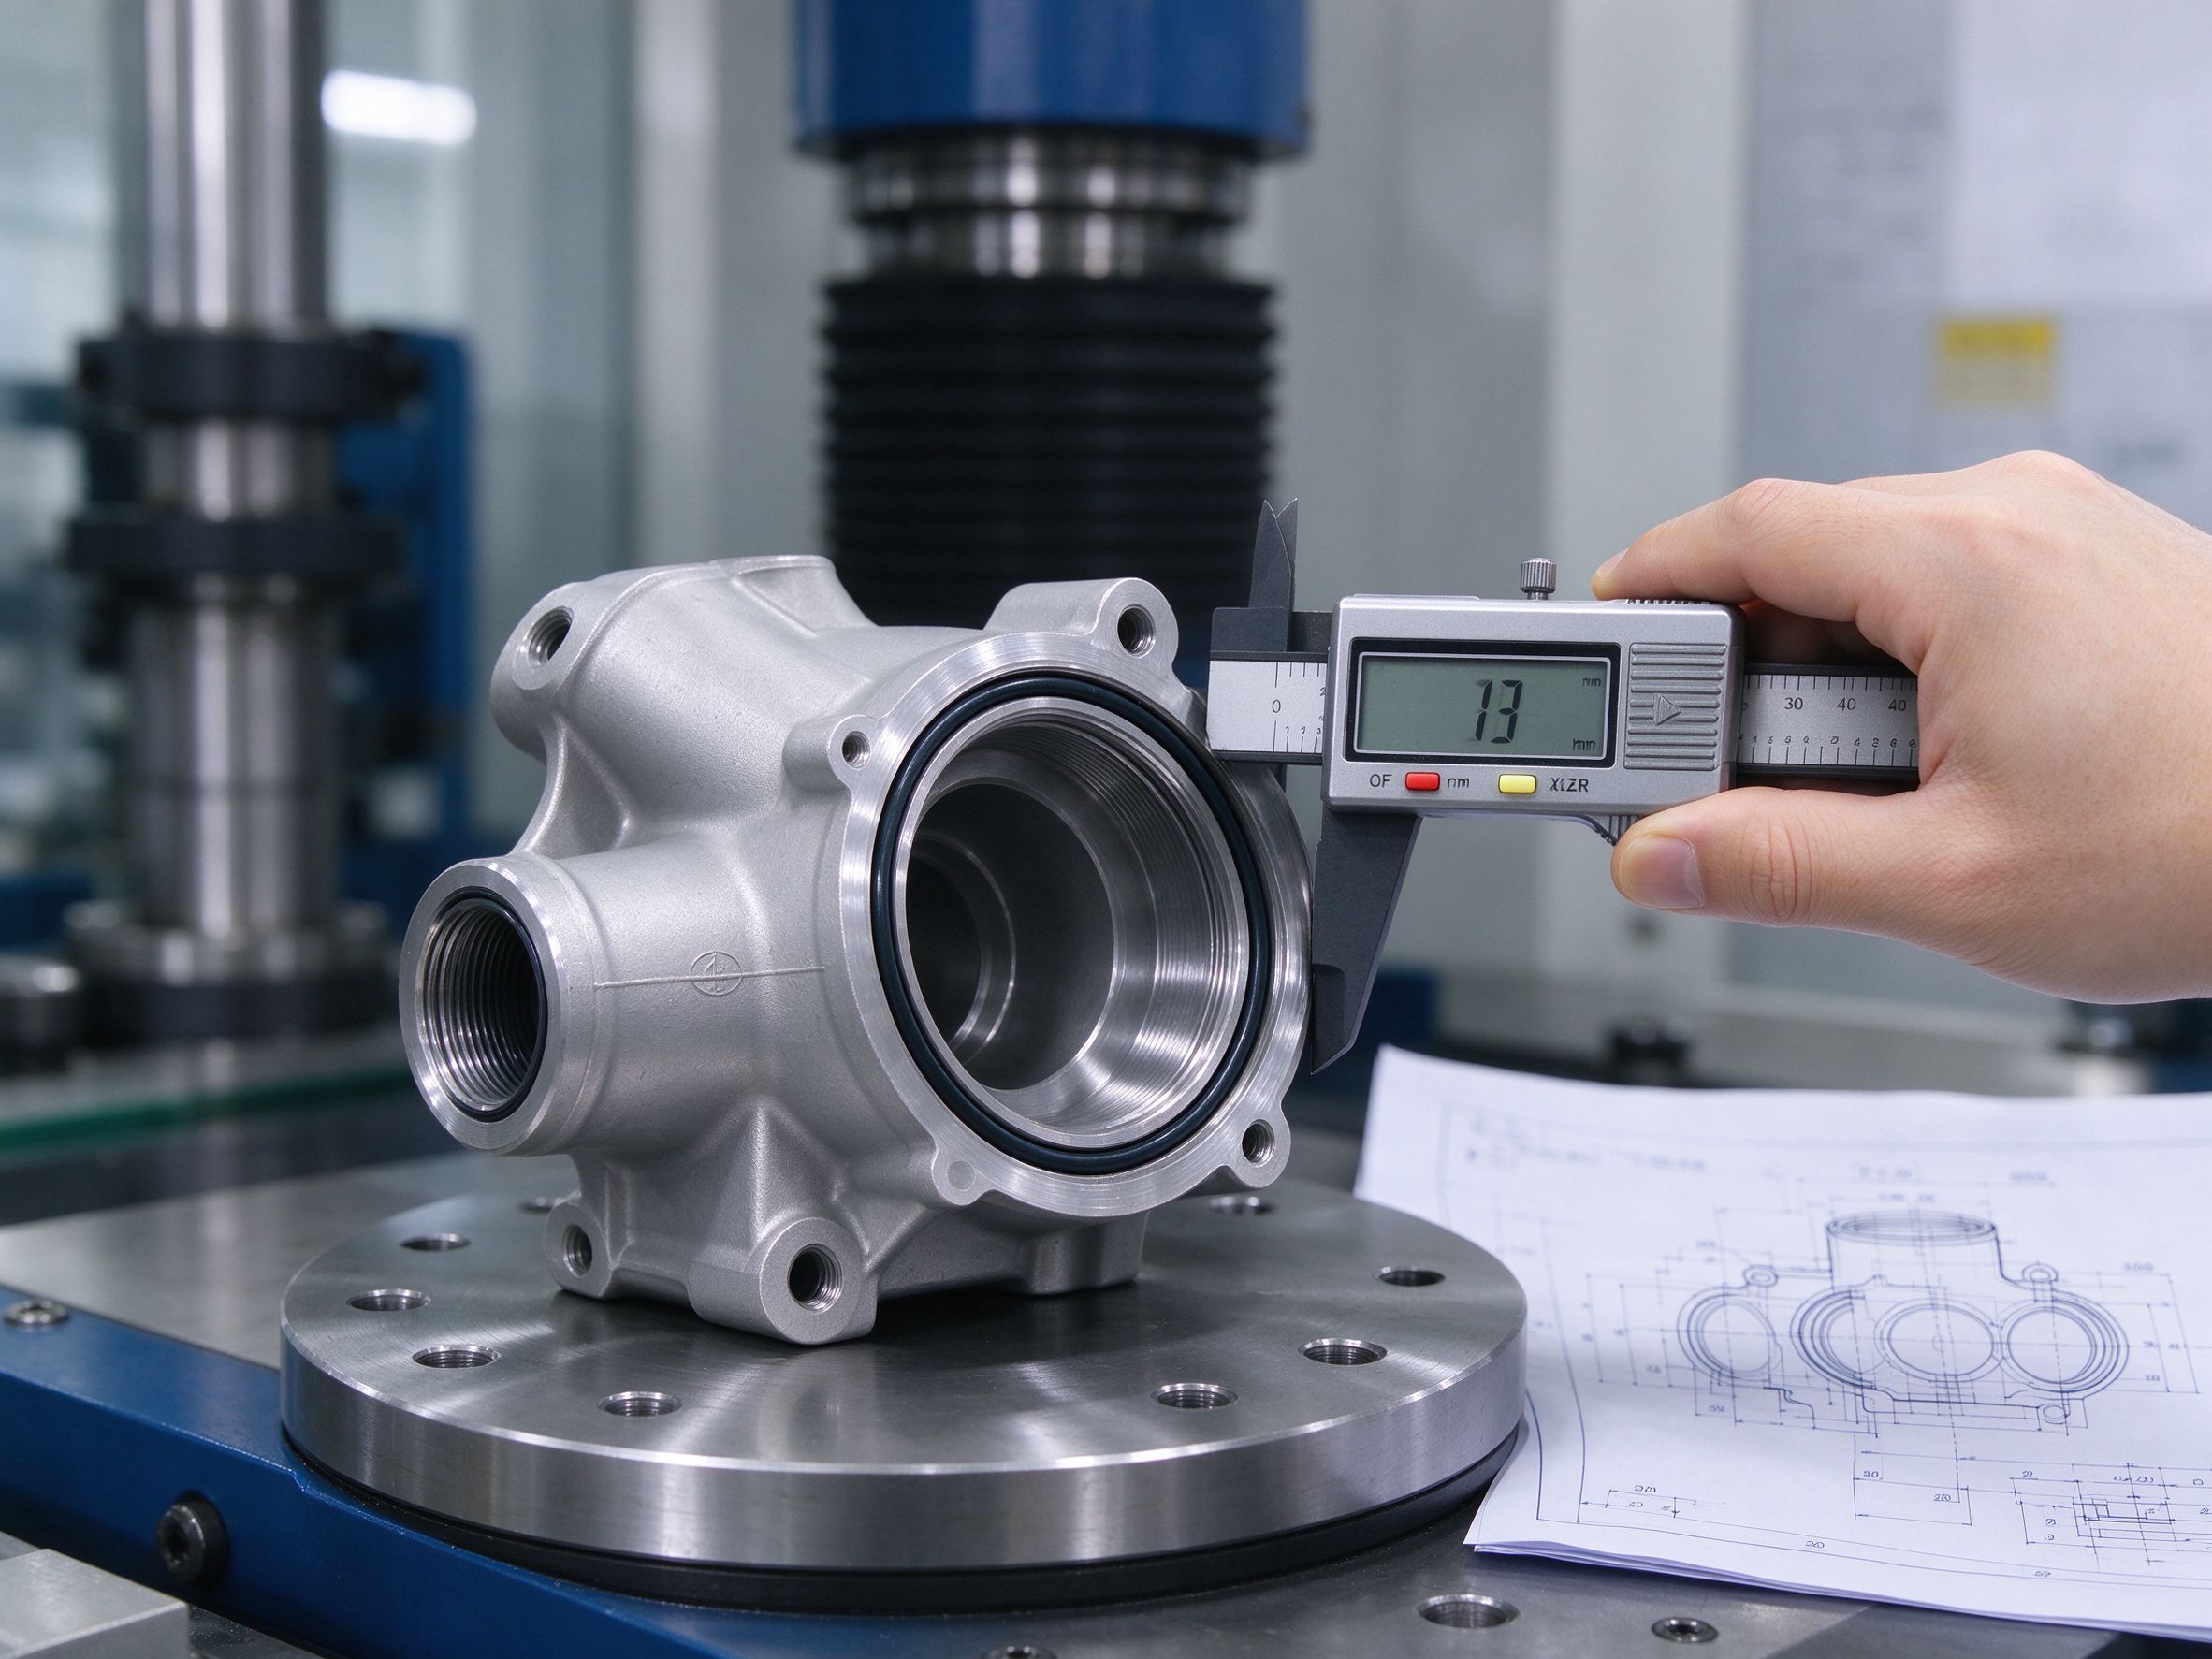
Checks are selected from the part's function and available testing scope. In-house checks, external laboratory testing and buyer-defined acceptance criteria are listed per project rather than presented as a fixed test lab.
Quality, Documentation and Change Control
- Drawing and resin grade locked before tooling or production release.
- DFM and mold or machining review recorded before sample build.
- First-article measurement of critical dimensions, seal faces and ports.
- Batch identification and material records kept for repeat orders.
- Material grade substitutions and drawing revisions reviewed before release to production.
Cost Factors
- Tooling or fixturing investment, cavity count and expected annual volume.
- Resin grade: commodity polymers versus high-performance grades such as PEEK or PPS.
- Part size, wall complexity, internal channels and secondary operations.
- Tight tolerances, sealing features and inspection documentation.
- Pressure, leak or chemical-exposure testing required by the project.
RFQ Checklist
| Information | Purpose |
|---|---|
| Company and business email | Identify the project |
| CAD / 2D drawing / sample photo | Part geometry |
| Component type and function | Housing, valve part, manifold, bracket or fitting |
| Chemical name or mixture | Medium compatibility review |
| Concentration and temperature range | Compatibility screening conditions |
| Exposure duration and contact type | Immersion, intermittent, splash or vapor |
| Pressure and mechanical load | Structural and sealing requirements |
| Resin preference, if any | Material and supply check |
| Annual volume and initial order | Process route and tooling decision |
| Required testing or documents and target delivery | Validation scope and schedule |
Frequently Asked Questions
Which plastic is best for chemical-resistant equipment components?
Can injection-molded plastic components withstand acids and alkalis?
What information is needed to select a chemical-resistant resin?
What is the difference between chemical resistance and corrosion resistance?
Should I use injection molding or CNC machining for chemical-resistant components?
Can a chemically compatible material guarantee a leak-free pump housing?
How can chemical resistance be validated?
Request a Chemical-Resistant Components Quote
Submit the part drawing, chemical media, concentration and temperature range, exposure type, pressure or load, and estimated volume. The review covers material fit, manufacturing route, sealing design and validation scope.
Xiamen Goldcattle · Manufacturing since 1998 · Injection molding, tooling and CNC machining · Related: injection molding services →