How Hard Is Brass to Machine? Alloys, Challenges and CNC Tips
Brass is generally considered relatively easy to machine, particularly free-cutting grades such as C36000. However, machinability varies by alloy, material condition, part geometry, cutting operation and required surface finish.
The term "brass" alone is not enough to predict machining time, tool life or finished-part cost. Common challenges in CNC brass machining include burr control, thread and hole quality, thin-wall stability, surface appearance and dimensional consistency — all manageable when the material grade, tooling, workholding, cutting strategy and inspection requirements are defined for the actual part.
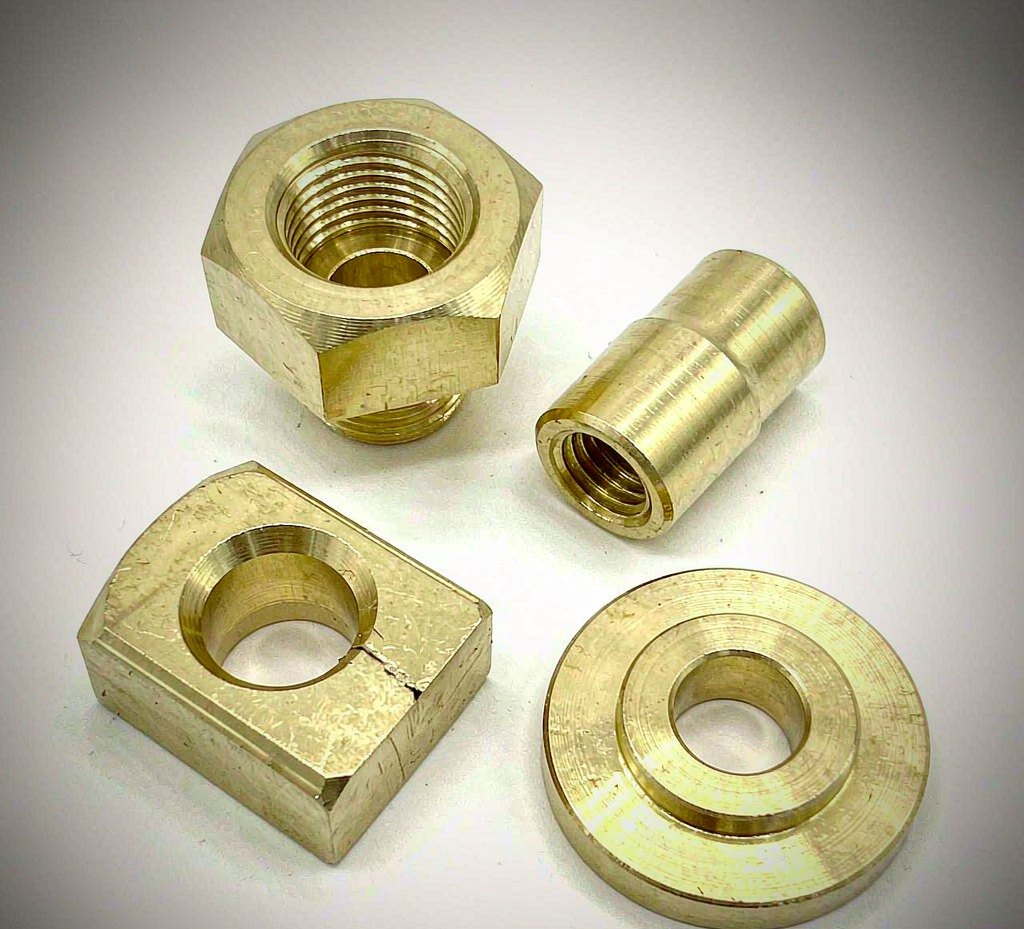
What Makes Brass Relatively Easy to Machine?
Free-cutting grades cut cleanly, but the advantage is not uniform across all brass.
Free-cutting brasses, especially leaded grades such as C36000, are known for good chip-breaking, lower cutting resistance and predictable tool behavior compared with many steels and some aerospace alloys. That is why brass is often described as easy to machine.
But "easy" is a relative statement. Machinability depends on the specific alloy, its condition (hardness, temper), the cutting operation (turning, milling, drilling, threading), the tool material and geometry, the machine and the required surface and tolerance. A lower-lead or high-ductility grade does not behave like C36000, and a complex thin-wall geometry can be demanding even in a free-cutting alloy.
Buyer takeaway: ask for the specific alloy and temper, not just "brass". The alloy name drives tool life, cycle time, burr behavior and finishing cost.
Brass Alloys Compared by Machinability
Relative machinability ratings help compare grades within one system; they are not speed or cost promises.
| Alloy | Key characteristics | Machining considerations | Selection caution |
|---|---|---|---|
| C36000 Free-Cutting Brass | Leaded; high machinability. CDA relative rating is 100; lead content is typically about 2.5–3.0%. | Excellent chip control and tool behavior for high-volume turning and milling. | Leaded grade — confirm end-use, market and any material or compliance specification before specifying. |
| C26000 Cartridge Brass | 70/30 copper-zinc; more ductile and formable. CDA relative machinability is about 30. | Lower machinability than C36000; tool and burr strategy differ. | Not a drop-in substitute for C36000 just because both are "brass". |
| C69300 ECO Brass | Silicon brass; lower-lead alternative. CDA relative machinability about 85. | Workable, but confirm cutting data from the actual material data sheet. | "ECO" / "lead-free" labels do not by themselves prove compliance; verify composition and spec. |
| C46400 Naval Brass | Used where corrosion resistance and strength matter. | Balance machinability against the service environment. | Do not assume one "marine brass" fits every seawater or humidity case. |
| C37700 Forging Brass | Common for forged brass blanks. | Machining depends on forging stock, allowance and follow-on cutting. | Compare forging plus machining cost together, not material alone. |
Material data source note
The relative machinability figures above follow the CDA rating system (C36000 = 100). They are a comparison reference, not a multiplier for cycle time or a price. The "Technical Characteristics and Engineering Applications of Brass Parts" family includes copper-nickel alloys such as C70600 — that alloy is not a brass and is intentionally excluded from the brass comparison here.
Common CNC Brass Machining Challenges
Even easy-machining brass has failure modes that depend on grade, tooling and design.
| Process step | Possible issue | Engineering response |
|---|---|---|
| Turning | Chip form, surface finish, edge wear, dimensional repeatability. | Define strategy by grade, insert geometry and part structure. |
| Milling | Thin-wall deflection, vibration, clamping stability, tool marks. | Control tool access, workholding and operation sequence. |
| Drilling | Burr at entry/exit, hole depth, chip evacuation, diameter control. | Select tool and process by through/blind hole, aspect ratio and acceptance. |
| Tapping / threading | Thread size, entry burr, full thread depth, assembly fit. | State thread standard, class, full depth and inspection in the drawing. |
| Deburring | Residual burrs at holes, thin-edge damage, sharp-edge spec. | Define which edges need deburring and acceptable edge condition. |
| Finish & appearance | Color variation, scratches, polishing, plating effect. | State in RFQ: as-machined, polished, plated or other. |
| Packaging | Staining, tarnish, scratches, contact contamination. | Set protective packaging and storage by appearance/cleanliness need. |
Tooling and Cutting Parameters
Explain what influences results — without publishing universal fixed values.
Tool geometry
Edge angle, rake, coating and sharpness change chip formation and finish across grades.
Cutting speed
Depends on alloy, tool material, tool diameter, operation and machine — not a number by itself.
Feed
Turning often uses feed per revolution; milling uses per-tooth or linear feed. Do not mix them.
Depth of cut
Influences force, deflection and surface; set per operation and stock.
Coolant / lubrication
Affects finish, tool life and chip handling; choose by alloy and process.
Verification
Confirm parameters on the actual part, tooling and machine — not from a generic table.
Why no fixed table here: a single speed/feed set applied to all brass, across turning, drilling and milling, would be misleading. Parameters should be set per alloy, tool diameter, tool material, operation and machine.
Design for Machinability
Good machinability is partly designed in, which protects cost and lead time.
Inside radii
Generous radii reduce tool stress and improve finish at corners.
Deep holes
High aspect ratios raise burr and evacuation risk; plan drill strategy early.
Threads
State standard, class, full depth and inspection to avoid rework.
Thin walls
Minimize deflection with sequencing, support and clamping.
Workholding
Design clamp surfaces so the part stays stable through all ops.
Inspection access
Keep critical features reachable for measurement and records.
What Actually Drives the Price of CNC Brass Parts?
Material price is only one input; process and quality requirements often matter more.
| Cost factor | How it affects price |
|---|---|
| Material grade & price | Specialty or lower-lead grades may cost more than standard C36000 stock. |
| Machinability | Higher machinability shortens cycle time; harder-to-cut grades raise it. |
| Part geometry | Thin walls, deep holes and complex shapes increase setup and risk. |
| Quantity | Volume spreads fixture and setup cost; prototypes cost more per piece. |
| Deburring & finish | Manual edge work and plating/polishing add labor and process steps. |
| Inspection & certs | Tight tolerances, CMM reports and material certificates add cost. |
| Packaging | Tarnish-sensitive or clean-room parts need protective packing. |
Choosing Brass for Different Applications
Examples show where grades are commonly used — they are not approvals for every substitution.
Mechanical connectors
C36000 is widely used for fittings and fasteners where machinability dominates.
Instrument parts
Stable, close-tolerance features favor free-machining grades with defined inspection.
Electrical connectors
Confirm conductivity, contact and finish requirements against the spec.
Decorative parts
Finish and color consistency matter; specify polished or plated condition.
Fluid fittings
For potable or process media, confirm alloy, composition and documentation.
Marine / corrosion-exposed
C46400-type choices need environment and coating review.
Lead Content and Material Compliance
Free-cutting brass is effective, but lead content creates real procurement limits.
CDA data shows C36000 lead content is typically about 2.5–3.0%, while C26000 is a low-lead grade (lead content typically up to about 0.07%). That difference is why a blanket "brass is lead-free" statement is incorrect, and why the end-use must be checked.
Compliance is end-use specific
For electrical and electronic equipment, RoHS places limits on lead, with exemptions that are narrow in scope and time. For example, the EU exemption for copper alloys with lead up to 4% currently runs to 2027-06-30 — but that is an exemption within RoHS, not a general permit for all leaded-brass parts, all industries or all uses. Do not assume "C36000 meets all EU/US standards." Buyers should confirm the alloy, composition evidence and applicable requirements against the final product, target market and customer specification.
Manufacturing and Inspection Support
Real process control backs the machining guidance above.
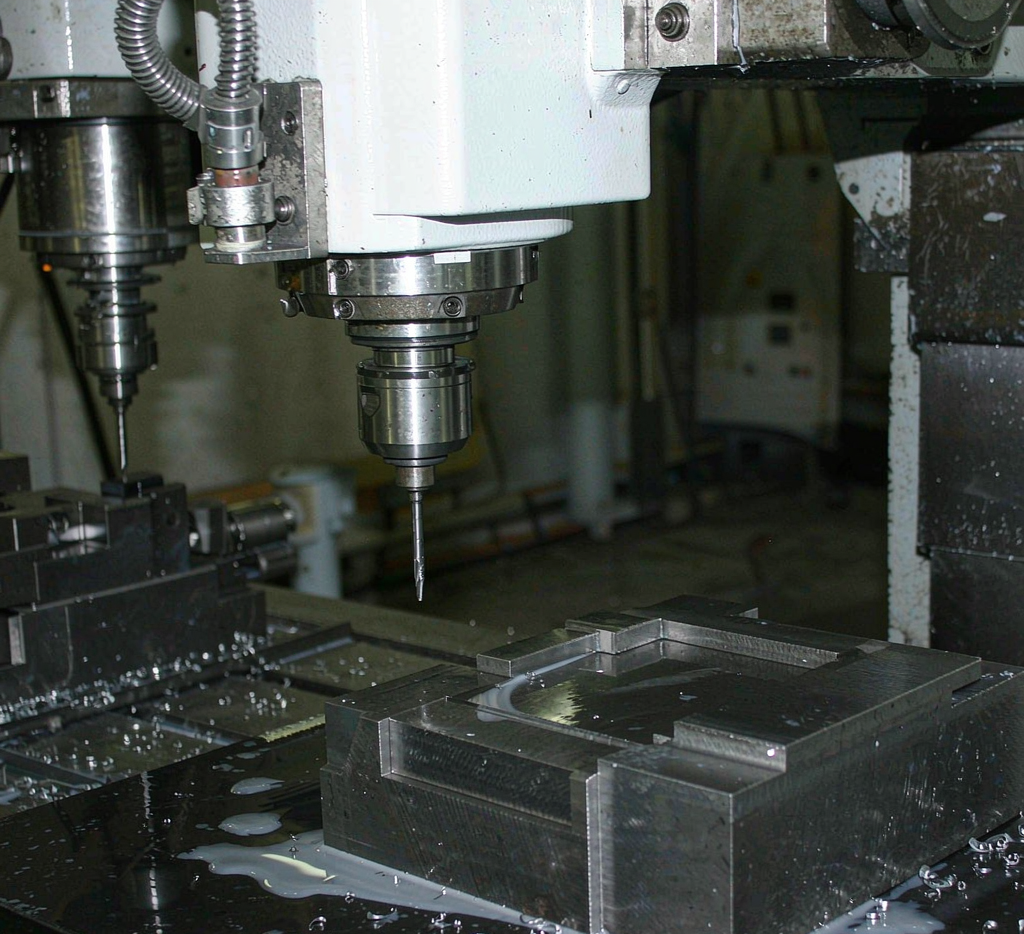
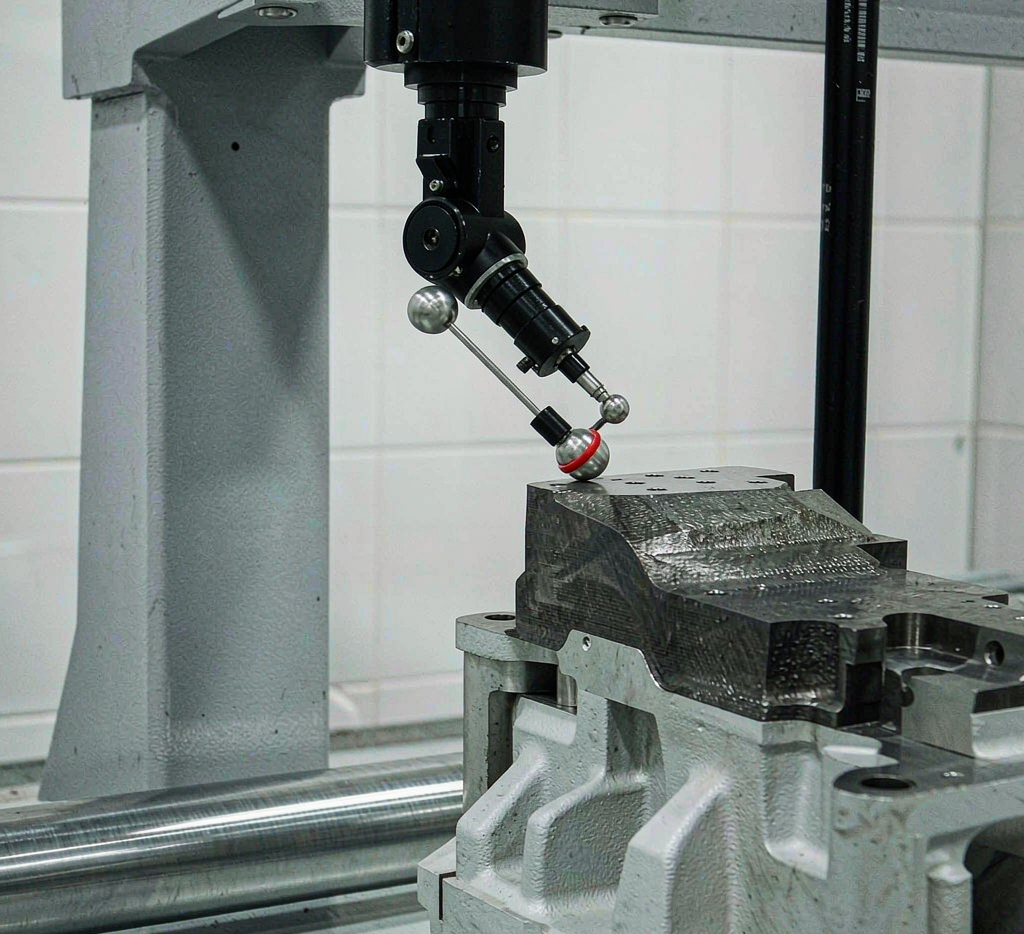
Why it matters: consistent machining and inspection are how tolerances and finish requirements from the RFQ are actually verified — not assumed from the alloy name.
RFQ Checklist for CNC Brass Parts
The clearer the input, the more comparable the quote and the lower the rework risk.
| Item | Provide |
|---|---|
| Alloy & condition | Designation (e.g. C36000) and temper or material standard. |
| Drawing / CAD | 2D drawing or 3D model with critical dimensions called out. |
| Tolerances | Critical vs general tolerances; datum and key features. |
| Finish | As-machined, polished, plated, or other, with appearance limits. |
| Deburr / edges | Which edges, and the acceptable edge condition. |
| Quantity & program | Prototype, low-volume or production volumes. |
| Documents | Material certificate, CoC, inspection or test reports required. |
Frequently Asked Questions
Is brass easy to machine?
Brass is generally considered relatively easy to machine, especially free-cutting grades such as C36000. But machinability varies by alloy, material condition, part geometry, cutting operation and required surface finish. The term 'brass' alone is not enough to predict machining time, tool life or finished-part cost.
What is the difference between C36000 and C26000?
C36000 is a leaded free-cutting brass with high machinability (CDA relative rating 100) and lead content around 2.5-3.0%. C26000 is a 70/30 cartridge brass that is more ductile and formable but has lower machinability (CDA relative rating about 30). They are not interchangeable just because both are called brass; selection depends on the part, process and any material or compliance specification.
Can a lead-free brass replace C36000 in any application?
Some lower-lead alternatives, such as certain silicon brasses like C69300, may suit applications with specific material or compliance needs. They should be selected against the relevant material specification and the end-use requirement, not by the 'ECO' or 'lead-free' label alone. Confirm composition and any required documentation with the customer specification.
Why do brass parts still get burrs?
Even easy-machining brass produces burrs at drilled holes, threads, edges and thin features. Burr size and removal difficulty depend on the alloy, tool geometry, cutting strategy and part design. Define which edges need deburring and the acceptable edge condition in the RFQ to avoid rework and cost surprises.
Does C36000 comply with all EU and US standards?
No single grade should be assumed to satisfy every standard. C36000 is leaded; its use in electrical and electronic equipment is subject to RoHS exemptions that are limited in scope and time (for example, the EU exemption for copper alloys with lead up to 4% currently runs to 2027-06-30). Buyers must confirm the alloy, composition evidence and applicable requirements against the end-use and target market.
What cutting parameters should I use for brass?
There is no single set of speeds and feeds that applies to all brass. Cutting speed depends on alloy, tool material, tool diameter, operation, machine and target surface. Turning feeds are often expressed per revolution, while milling uses per-tooth or linear feed; do not apply one value across turning, drilling and milling. Define parameters per the actual part, tooling and machine.
Which brass alloy should I choose?
Start from the function: C36000 for high-volume free-machining parts, C26000 where forming or higher ductility matters, C69300-type alloys where lower lead content is required, C46400 for marine-corrosion-conscious designs, C37700 for forged blanks. Confirm lead content, market and documentation needs before finalizing.
What drives the cost of CNC brass parts?
Cost is driven by material grade and price, machinability, part geometry, quantities, workholding, deburring, surface finish, inspection level, packaging and any material certification. A harder-to-machine or specialty grade, tight tolerances, deep holes or heavy deburring can raise cost more than the raw material price alone.
What should I send a supplier for a brass CNC quote?
Provide the alloy designation, material condition, CAD or drawing, critical tolerances, required finish, order quantity, any deburring or edge requirements, and the material and inspection documents you need (material certificate, test or CoC). Clear drawings reduce quoting risk and rework.
Can Goldcattle machine brass parts to my specification?
We support custom CNC brass parts against customer drawings and material specifications, including common grades such as C36000, C26000, C69300 and C46400 where applicable. Share the drawing, alloy, tolerances and finish requirements so we can review the machining route and any compliance-documentation needs.
Need a CNC brass part machined to drawing?
Send the alloy designation, material condition, drawing, critical tolerances and finish requirements for a review of the machining route and any documentation needs.
- Material and grade reviewed against your specification
- DFM input on threads, holes, thin walls and deburring
- Agreed inspection and material documentation on request
Reviewed the alloy comparison, machining-challenge and compliance content for this guide on 2026-10-12. Material ratings reference publicly available CDA data; lead-content and RoHS statements describe general principles and are not a substitute for project-specific compliance confirmation.