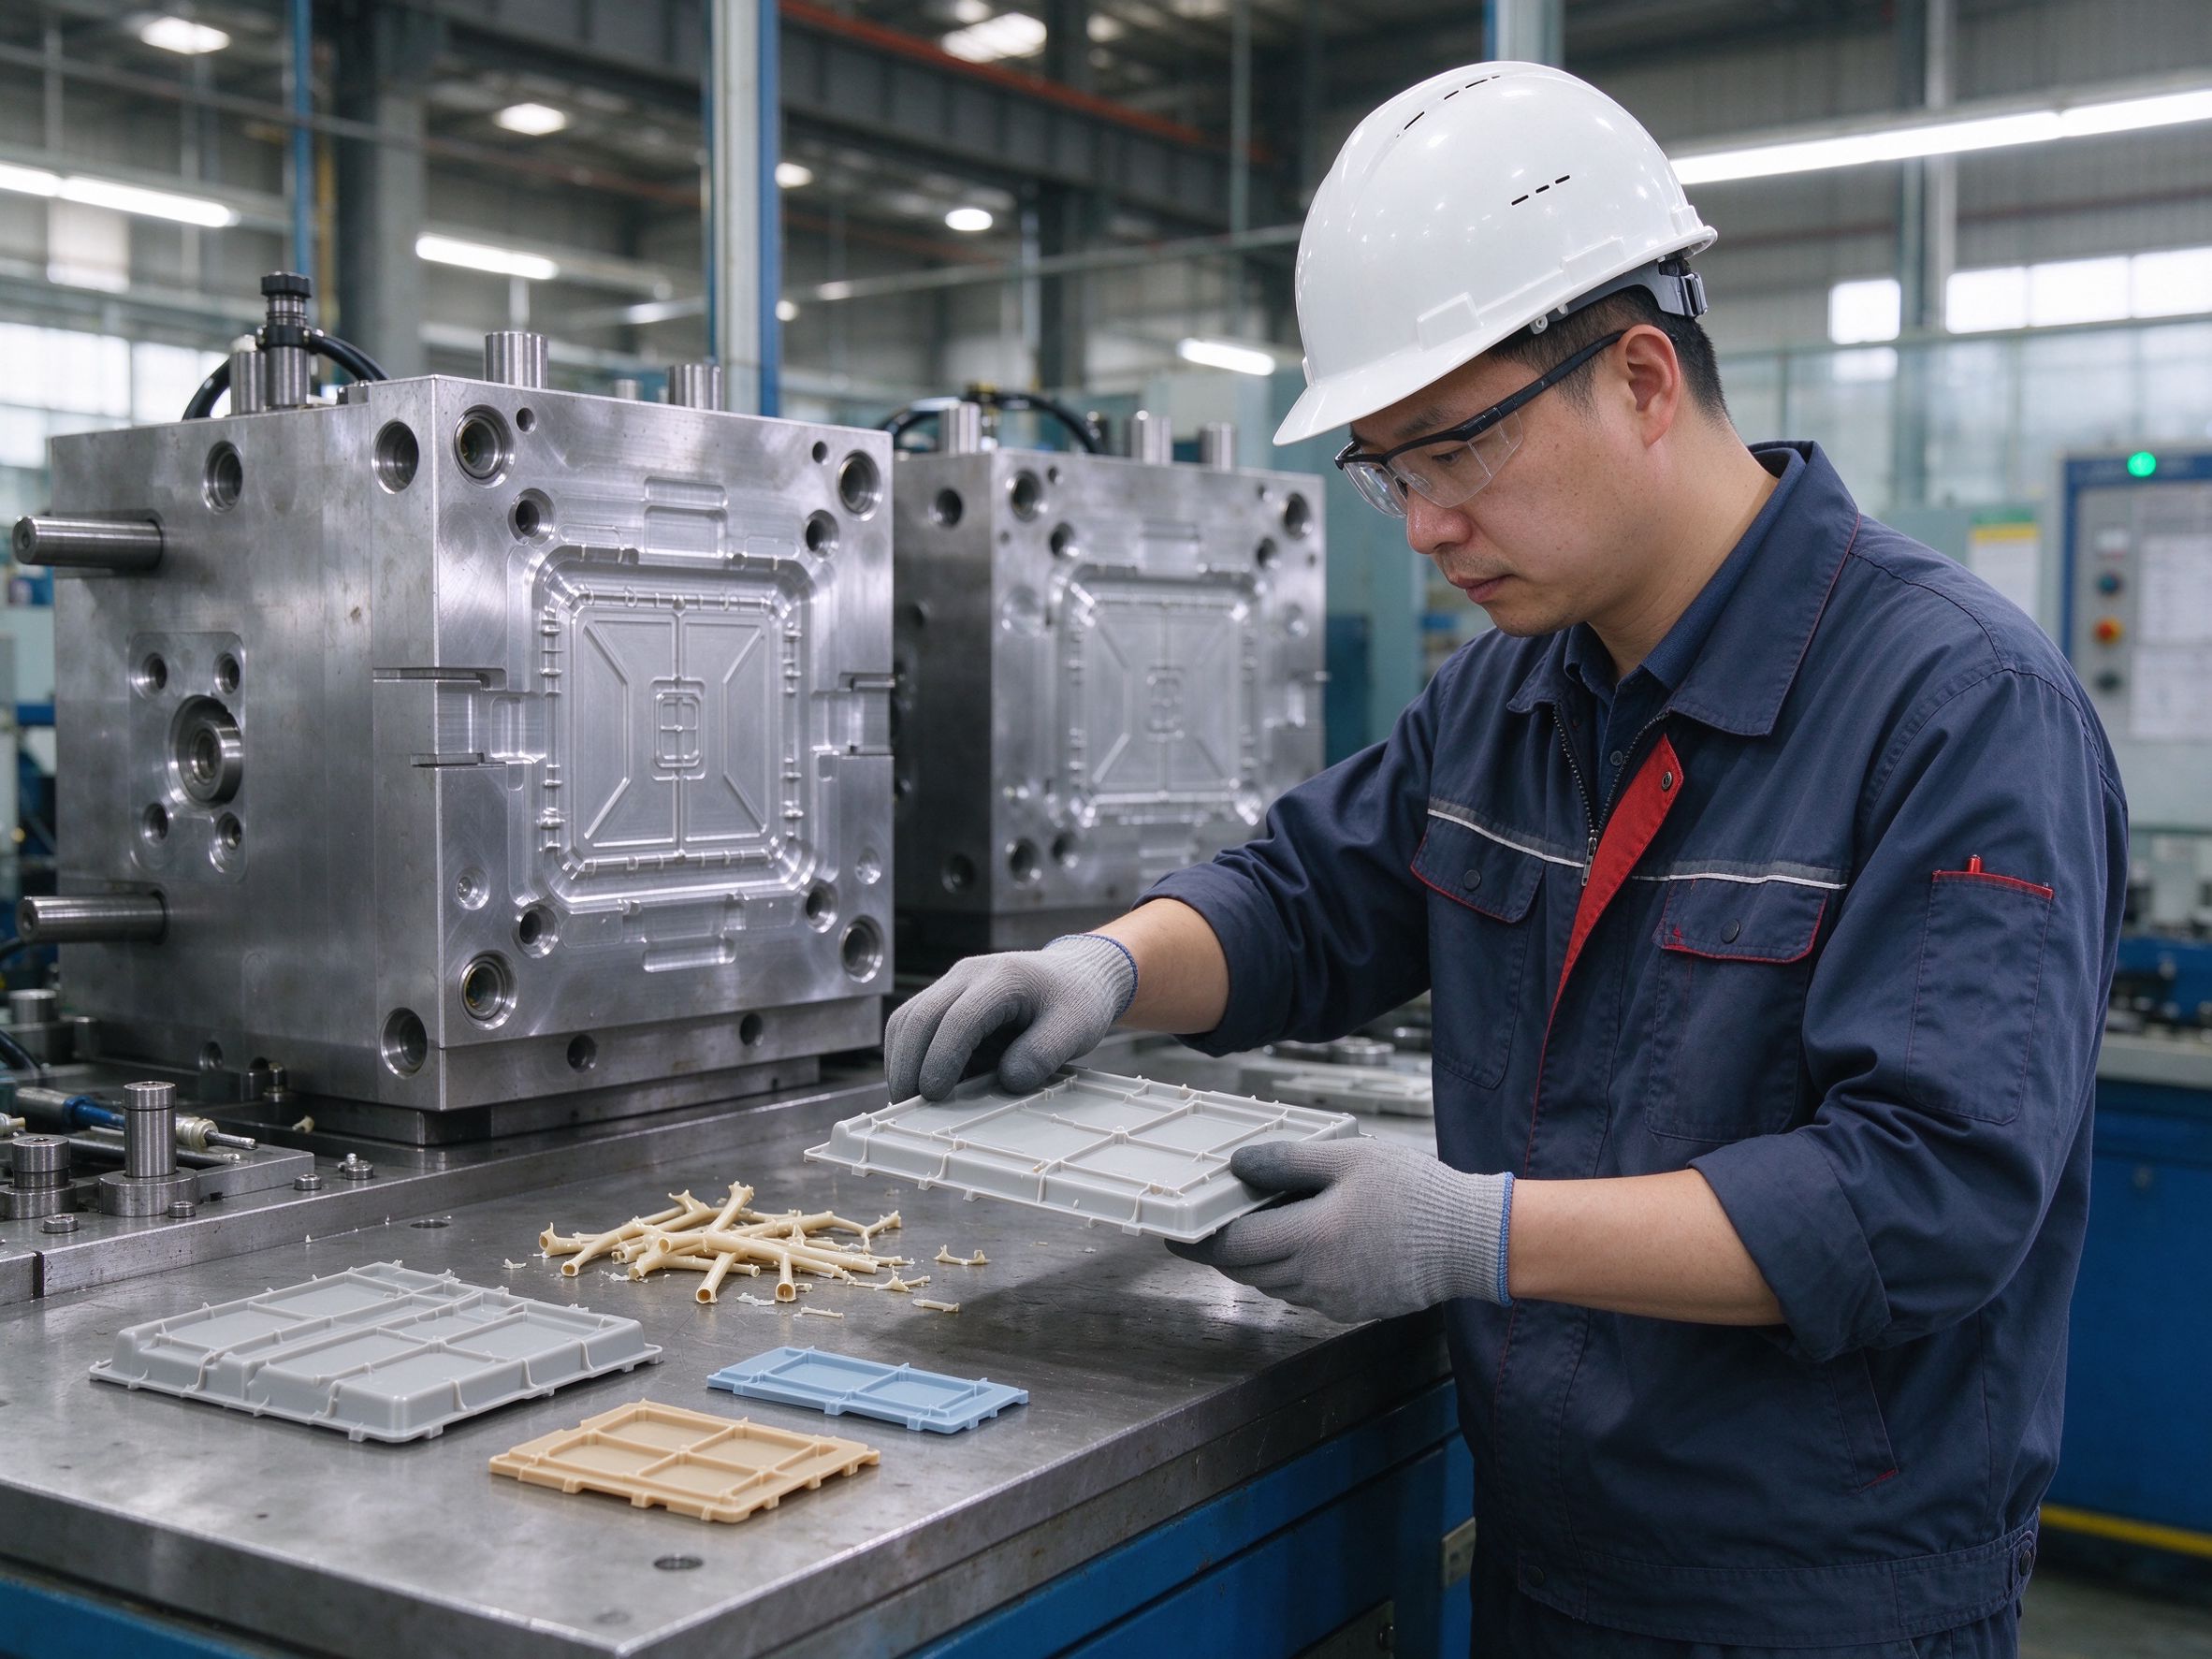
Custom semi-hot runner molds evaluated from your part geometry, resin grade, gate layout and production requirements. The design keeps part of the runner heated while other branches stay cold, so the right configuration depends on the actual melt path, the sections held at processing temperature, the remaining cold-runner layout, material behavior and production economics — not on the runner system's name.
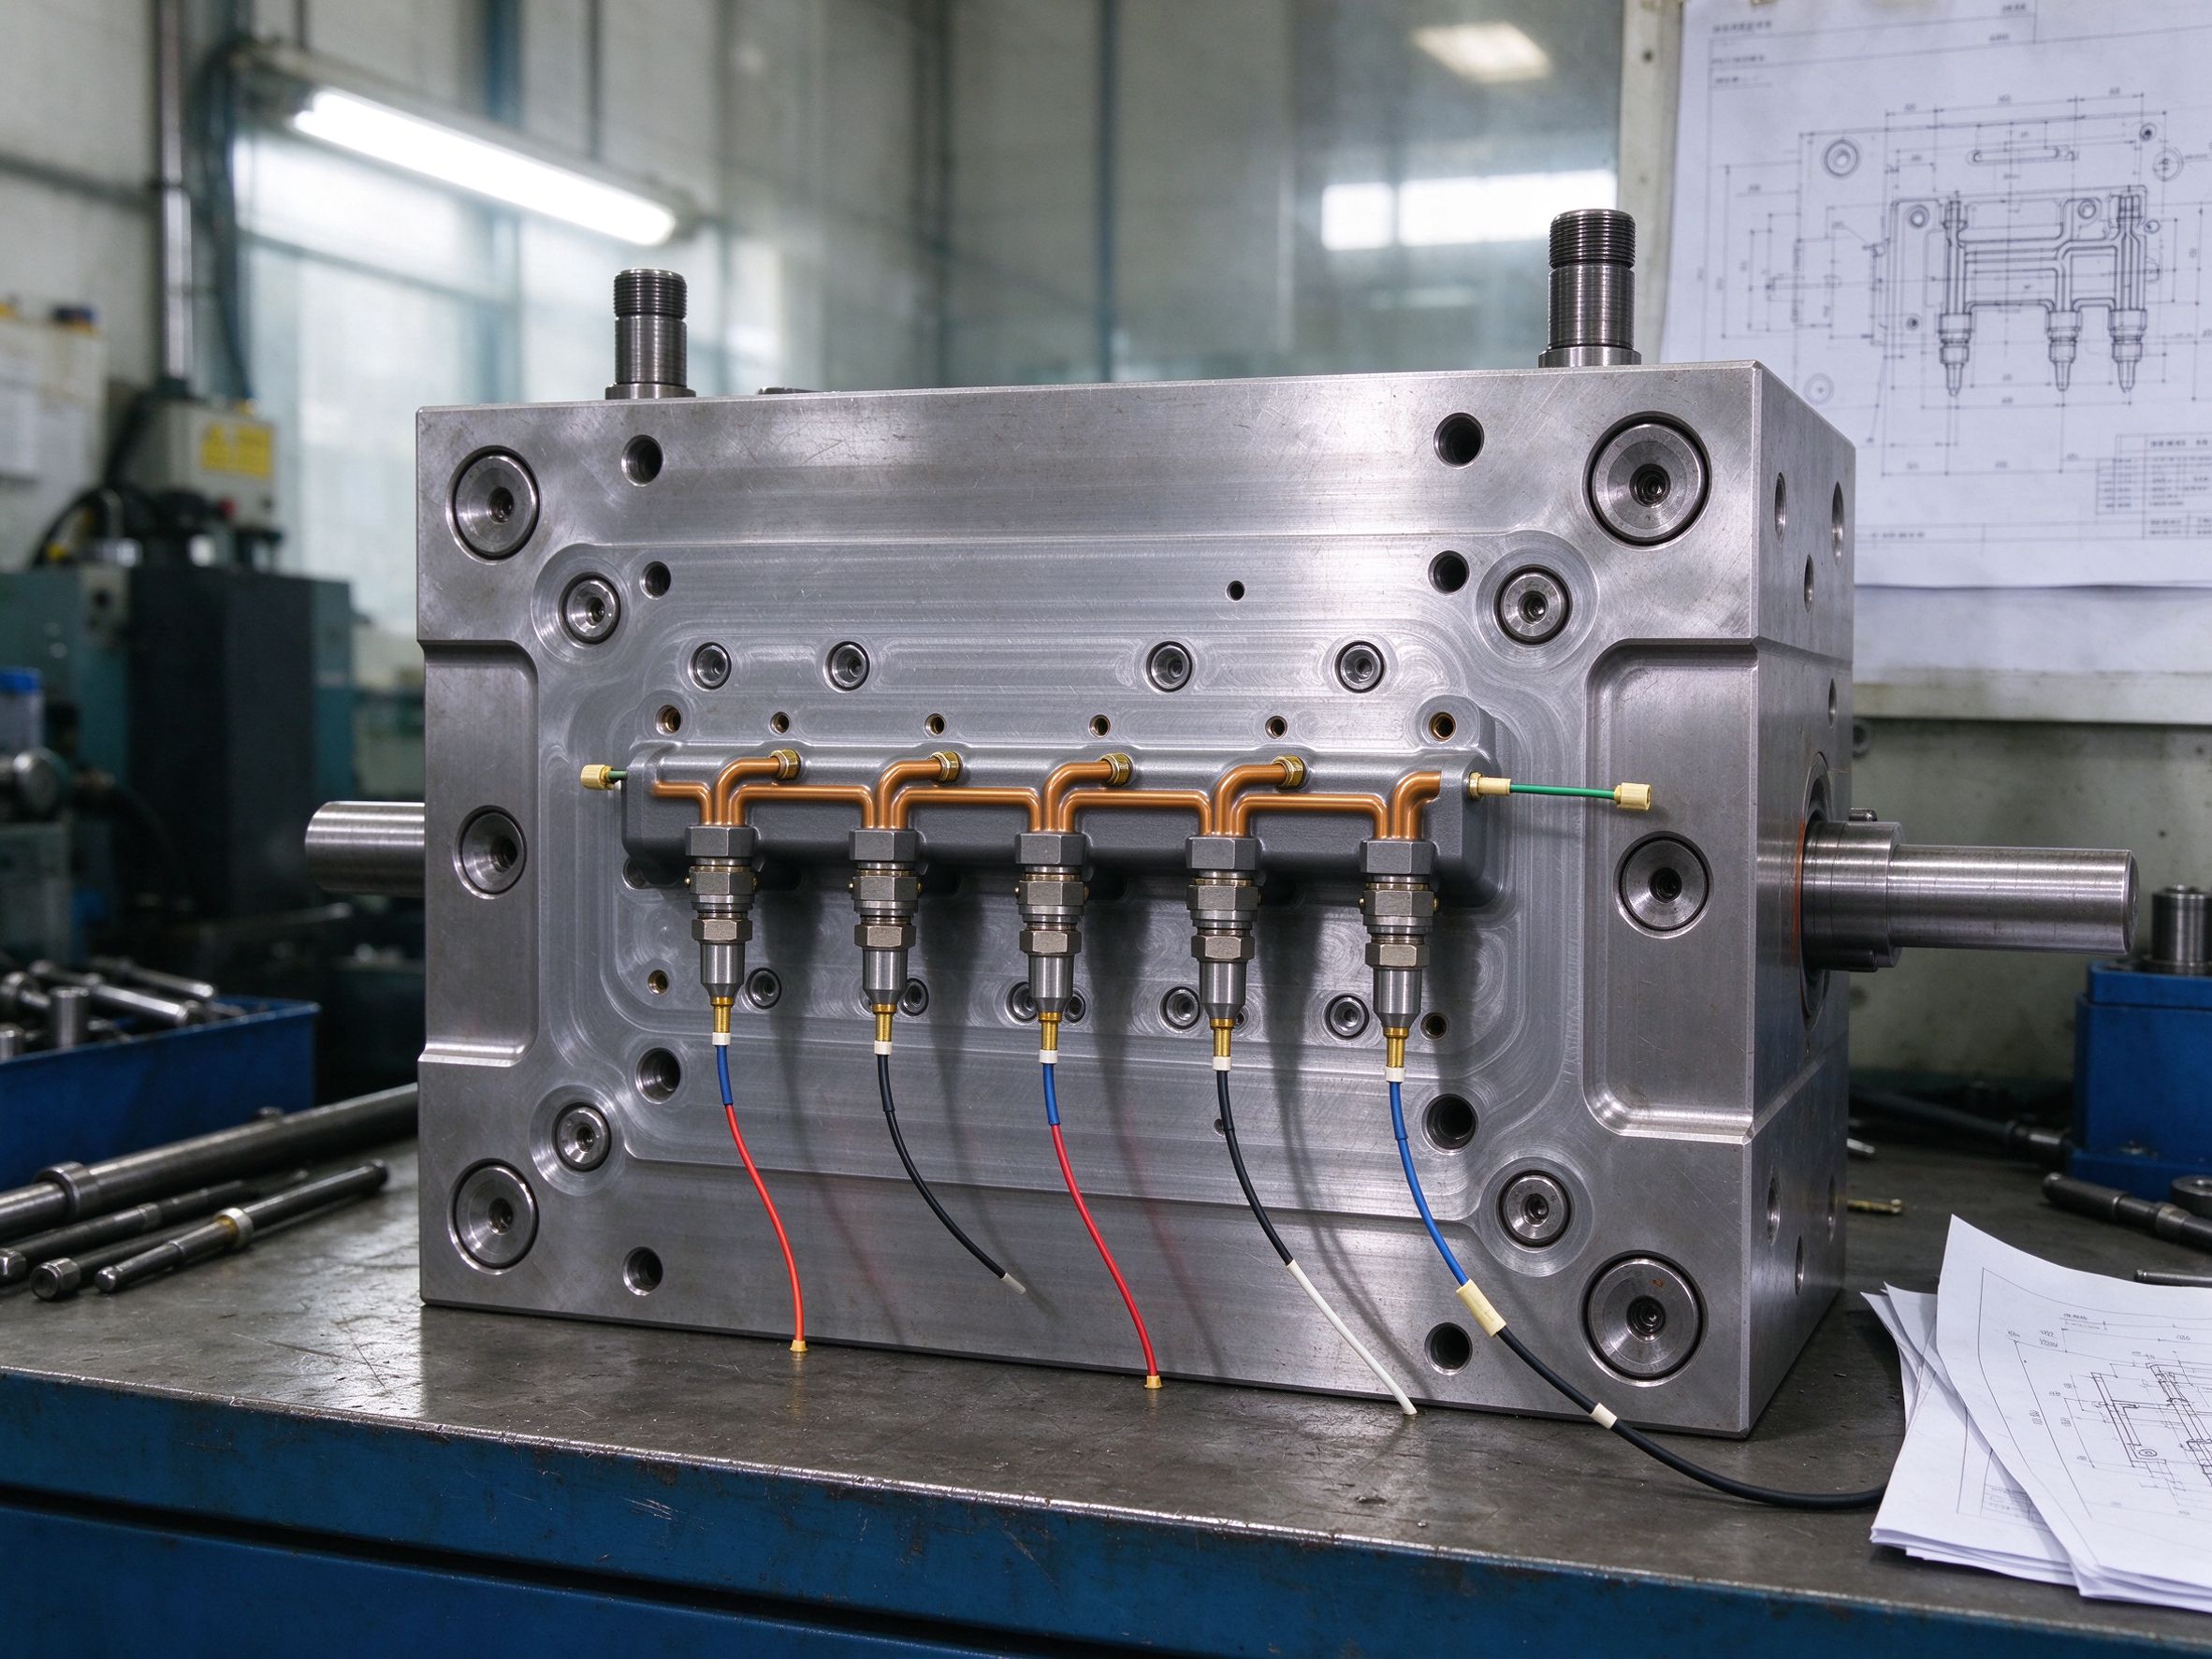
A semi-hot runner mold is evaluated as a balance between cold-runner tooling investment and full hot-runner material efficiency — not as a design that is automatically cheaper or faster. Goldcattle reviews your part, resin, gate layout and annual production to recommend which runner sections stay heated, which branches stay cold, and whether the economics work. Quotes and trial plans are built from the actual design, not from a fixed percentage claim.
What Is a Semi-Hot Runner Mold?
A semi-hot runner (also called a hybrid hot/cold runner) combines a heated runner section with cold runner branches in one mold. In the configuration Goldcattle evaluates, part of the melt path is held at processing temperature through a heated manifold and nozzles, while the remaining branches cool and are ejected with the part or as runner scrap.
The term is not used identically by every supplier. Before comparing designs, confirm which runner sections are heated, which solidify, how the gates are set, and what path the melt actually takes. A section view of the mold shows this better than the name of the system.
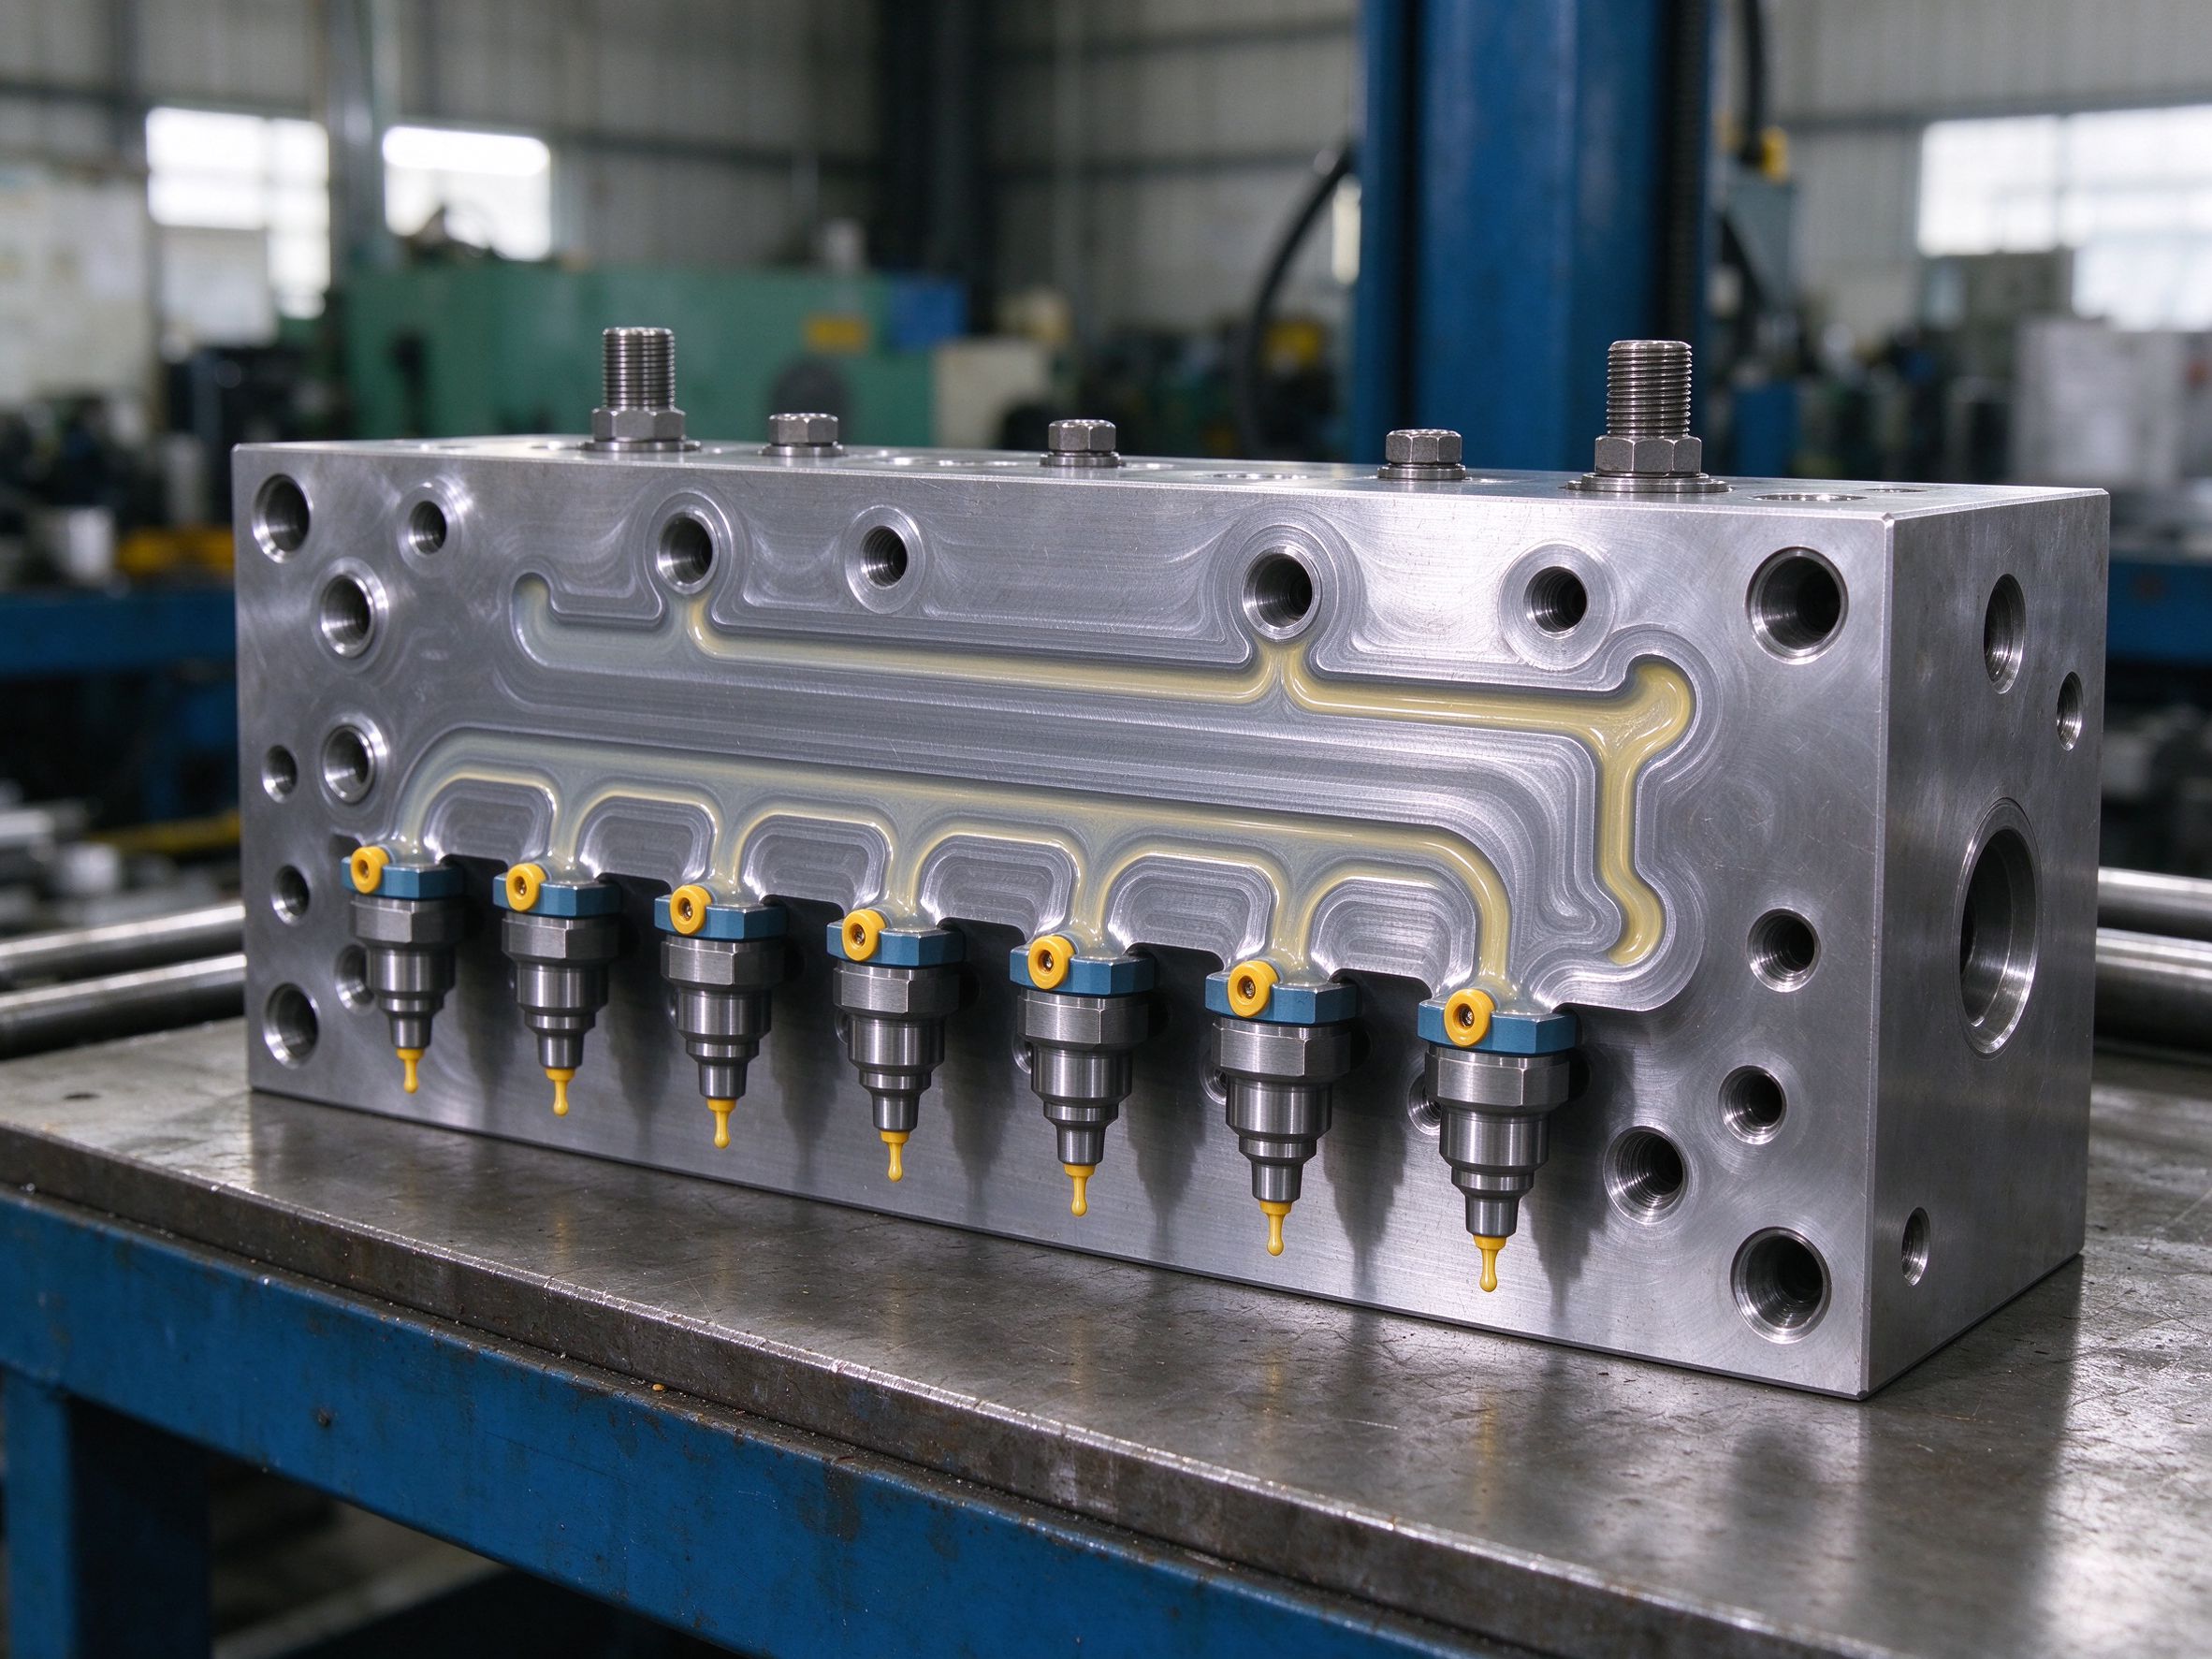
Semi-Hot Runner vs. Cold Runner vs. Full Hot Runner
| Assessment | Cold runner | Semi-hot / hybrid | Full hot runner |
|---|---|---|---|
| Initial tooling investment | Usually lower | Depends on the hybrid structure and heating components | Usually higher: manifold, nozzles, heating and temperature control |
| Runner material | Runner cools and ejects with each shot | Part of the runner still solidifies; amount depends on the design | No regular solidified runner in steady production; startup and purge still use material |
| Maintenance complexity | Relatively simple | Heated sections and cold branches both need care | Hot-runner components, temperature control and electrical systems |
| Color / material change | Usually easier | Depends on melt path and purge structure | Can involve more purge residue and downtime |
| Material fit | Wide range, still limited by gate and design | Thermal stability of the resin and the mixed runner layout assessed | Processing window, residence time and temperature control reviewed |
| Economics | Low upfront cost; runner scrap accounted for | Targets a balance of investment, material and process | Makes sense when combined savings cover extra investment and running cost |
The comparison follows the actual design Goldcattle uses, not a generic claim about what a semi-hot runner always delivers.
When Does a Semi-Hot Runner Make Sense?
Suitability is assessed from the project, not from a fixed annual-volume band:
- Runner weight share — the cold-runner weight as a share of the shot and the resin cost per shot.
- Actual injections per year — calculated from annual production, not just finished part count.
- Regrind policy — whether the cold runner can be recycled under the customer's material and quality rules.
- Added investment — extra tooling for heated sections, plus maintenance, energy, color-change and downtime cost.
- Cycle improvement — any cycle gain is verified by trial, not assumed.
- Gate location and appearance — gate position, visible marks and multi-cavity filling balance.
Part geometry, resin, gate layout, cavity count and maintenance conditions decide the recommendation. The review states when a cold runner or a full hot runner is the more economical route.
Tooling Cost and Payback
Material savings and possible cycle gains are weighed against the full cost picture in one model: additional mold investment, energy, purge and cleaning, maintenance and downtime. Runner weight per shot, resin price, annual injections, regrind policy and the mold design all enter the calculation.
No universal percentage for material saving or mold-cost advantage is claimed here — the numbers come from the specific design and production assumptions listed in the quote.
DFM, Runner Layout and Material Assessment
- Melt path — which runner sections are heated, which solidify, and how the melt reaches each cavity.
- Gate design — gate type, position and vestige against the appearance and function requirements.
- Material behavior — resin grade, thermal stability, fillers, color, residence time and heat-degradation risk reviewed per grade, not by resin family name.
- Cavity balance — filling and pressure balance across cavities with the chosen runner layout.
- Temperature control — heater zones, thermocouple positions and maintenance access to heated sections.
Trial, Validation and Mold Handover
- Mold design and DFM review, with runner layout approved before machining
- Trial molding, sample inspection and agreed mold adjustments
- Acceptance on critical dimensions, gate quality, appearance and molding stability
- Mold technical files, temperature-control interface data and agreed spare parts
- Mold ownership, maintenance responsibility, warranty boundary and follow-up support stated in the order
Each item is confirmed within the agreed project scope; services that cannot be provided are not promised on the page.
What We Need to Quote a Semi-Hot Runner Mold
| Information | Why it matters |
|---|---|
| 3D CAD and controlled 2D drawings | Part geometry, datums, critical dimensions and gate feasibility |
| Resin grade, color and fillers | Flow, temperature control, purge and heat-degradation risk |
| Part weight and annual demand | Runner scrap, injection count, cavity layout and economics |
| Target cavity count / output | Mold structure, filling balance and cycle target |
| Appearance surface, gate and allowed marks | Gate position and cosmetic acceptance |
| Injection machine parameters | Machine spec, mounting space and interfaces for exported molds |
| Mold life, acceptance and maintenance requirements | Mold steel, spares, trial scope, files and support |
| Delivery destination and installation plan | Delivery, commissioning, temperature-control equipment and technical support |
Frequently Asked Questions
What is a semi-hot runner mold?
What is the difference between semi-hot, cold and full hot runners?
Does a semi-hot runner always cost less than a full hot runner?
What production volume justifies a semi-hot runner mold?
Which plastic resins are suitable for semi-hot runners?
Can a semi-hot runner reduce cycle time?
What affects the cost of a custom semi-hot runner mold?
What do you need to quote a custom mold?
Request a Semi-Hot Runner Mold Design Review
Send the CAD, resin grade, part weight, annual demand and target cavity count. The review covers the runner layout, heated and cold sections, payback calculation and trial plan before the quote is issued.
Xiamen Goldcattle · Manufacturing since 1998 · Injection mold making and custom injection molding · Related: hot runner vs cold runner cost comparison →