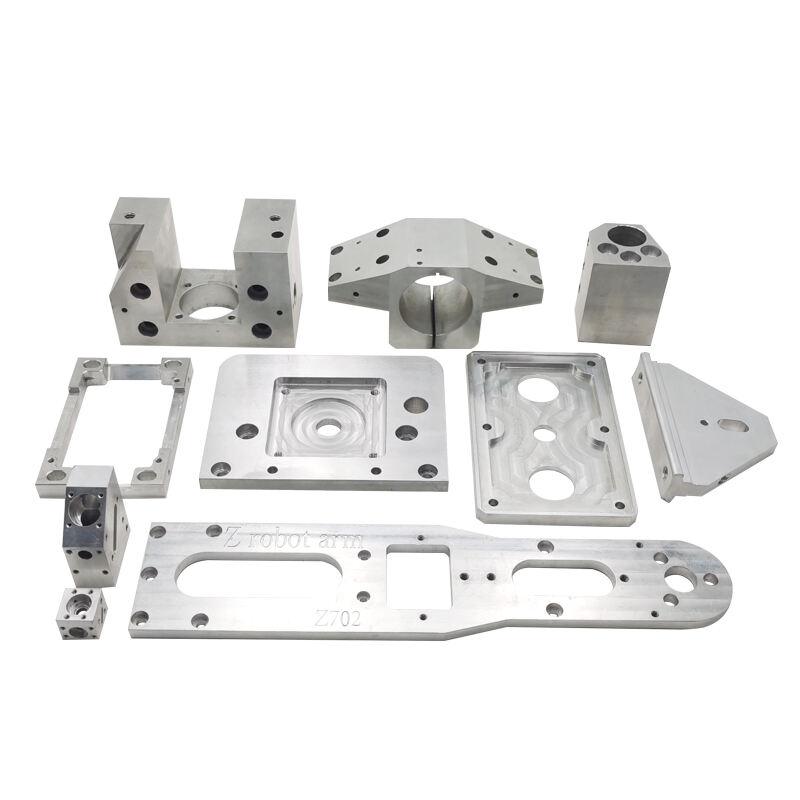
The cheapest aluminium for CNC machining is not always the alloy with the lowest price per kilogram. Total part cost also depends on material availability, stock form, machinability, machining time, material waste, setup, tolerances and surface finishing. This guide explains how to compare alloys by finished-part cost, not raw-material price.
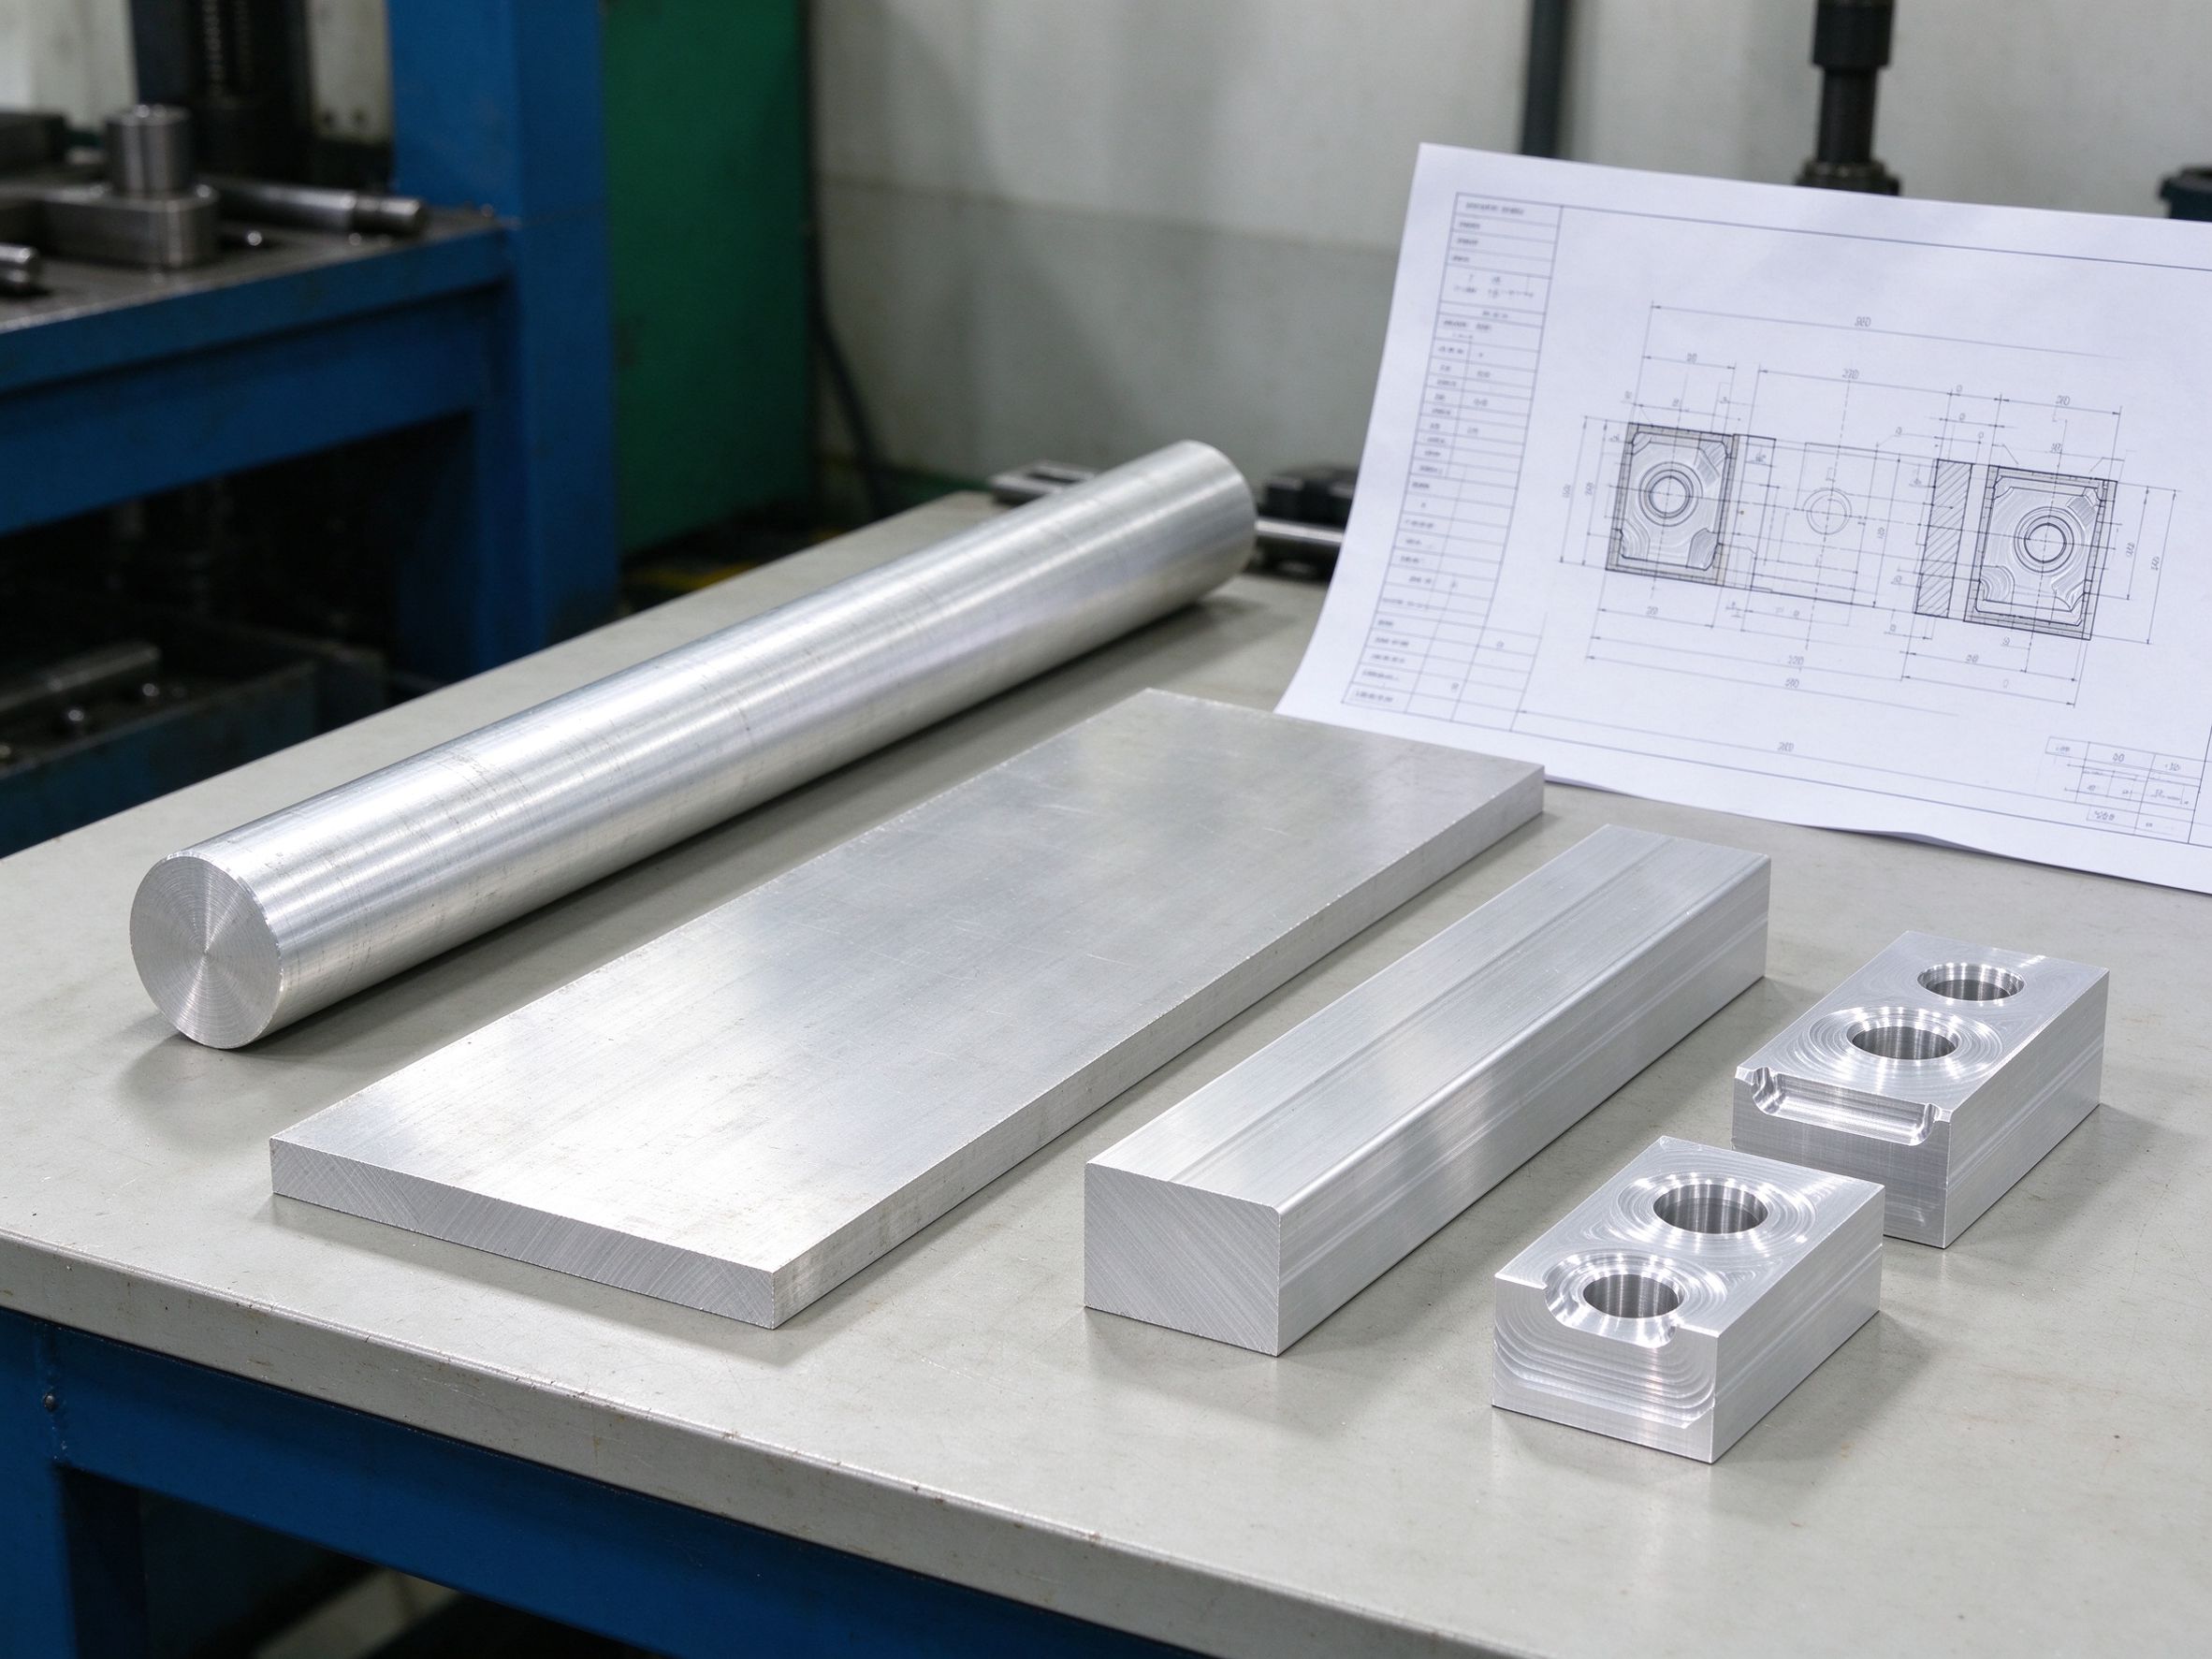
At a Glance
For many general-purpose CNC-machined parts, 6061-T6 is a cost-effective starting point because it is widely available and balances strength, machinability and corrosion resistance. In European projects, 6082-T6 may be competitive depending on local stock and supply. 1100 and 3003 are economical in specific applications, but a low material price does not mean the lowest finished-part cost.
Raw Material Price vs Finished Part Cost
Material price per kilogram is one input, not the total. The finished-part cost includes:
Stock & utilization
Bar, plate, sheet, tube or extrusion form; size availability; material yield and waste from machining.
Time & setup
Programming, fixturing, cutting time, tool wear, chip control and secondary deburring.
Inspection & finishing
Dimensional checks, surface treatment, packaging and the documentation the project requires.
An alloy with a low per-kg price can still cost more overall if it is slow to machine, produces gummy chips, needs more setup or finishing, or is only available in an unsuitable stock form. The comparison belongs at finished-part level, quoted against the actual drawing.
Compare 1100, 3003, 6061-T6 and 6082-T6
| Alloy | Material & machining characteristics | When it may be more economical | Main limits |
|---|---|---|---|
| 1100 | Near-pure aluminium, high formability, relatively low strength; soft states can produce gummy chips | Conductivity, thermal or low-strength uses where the design suits the material | Not a default for precision CNC milling; chip and surface management can add cost |
| 3003 | Aluminium-manganese alloy, good formability and corrosion resistance in sheet applications | Parts dominated by sheet forming, welding or forming with light CNC work | Machined-only parts may not beat 6061; soft chips and deburring can add time |
| 6061-T6 | Balanced strength, machinability, supply and anodizing response | Most general CNC aluminium parts, where common bar and plate stock supports the program | Not for every high-strength, fatigue or corrosion requirement |
| 6082-T6 | Common in European mechanical and structural parts, good strength and machinability | European programs where local stock and supply form are favorable | Cost versus 6061 depends on actual stock, specification and machining conditions |
| 7075-T6 | High strength and strength-to-weight ratio | High-load, weight-sensitive designs that really need the properties | Higher material price; welding, corrosion and stability need review |
| 2011 / 6262 free-cutting | Alloys optimized for free machining or high-volume production | Where product structure, batch size, environment and specification fit | Availability and environmental or customer limits confirmed per project |
Why 6061-T6 Is Often a Cost-Effective CNC Choice
6061-T6 is widely stocked in bar, plate and sheet forms, machines predictably, and responds well to common finishes such as anodizing. For many projects, this combination lowers both material wait time and machining cost.
6061-T6 is the heat-treated condition of the alloy — purchasing standard 6061-T6 stock does not mean each machined part needs an extra T6 heat-treatment charge. If a specific structure distorts in machining, material condition, stress management or process sequence are reviewed per part.
Where the design needs specific strength, fatigue, corrosion or certified properties, the material is re-evaluated rather than assumed.
When 1100 or 3003 Makes Sense
Sheet or formed parts, conductivity and thermal applications, low-strength uses, or welded fabrications where forming matters more than machined precision.
Parts with deep pockets, precise hole patterns, threads, mating faces or high-quality surfaces machined from solid stock. Machinability, chip control and deburring can outweigh the material price.
US vs European Aluminium Supply
Material economy follows local stock, not a global price list:
| Region | Common CNC stock | What to confirm |
|---|---|---|
| US market | 6061 in bar and plate is a common starting point | Grade, temper, bar or plate size, finish and delivery |
| European market | 6082-T6 is common for structural, plate and mechanical parts | Local stock, dimensions, material state and certification |
Quote against the material that can actually be supplied in the specified size, temper and quantity — not a single global per-kg figure.
How Part Design Changes CNC Cost
Before switching alloys, review the design. These changes often reduce cost more than a material change:
Geometry
- Relax non-functional tolerances to the range the function needs
- Reduce unnecessary deep pockets, thin walls and narrow tool access
- Place features on fewer faces to reduce setups
- Use internal radii that suit standard tools
Stock & program
- Match the stock form to the part — plate, bar, tube or extrusion
- Evaluate near-net preforms where material removal is large
- Confirm which dimensions need CMM or special inspection
- Confirm whether the surface finish is necessary before quoting
Quantity changes the picture too: programming, setup and inspection costs spread differently over prototype, first order and repeat volumes. The production route is evaluated on structure, tooling, change probability and life-cycle demand — not a fixed piece-count rule.
Finishing and Inspection Costs
Anodizing, blasting and other coatings change cost, appearance and sometimes final dimensions. The RFQ should confirm:
- Material state before and after machining
- Surface treatment type, color or appearance reference where required
- Which final dimensions are measured after finishing
- Inspection reports, first-article checks and material certificates
- Finishing order — machining before anodizing, or the reverse for specific features
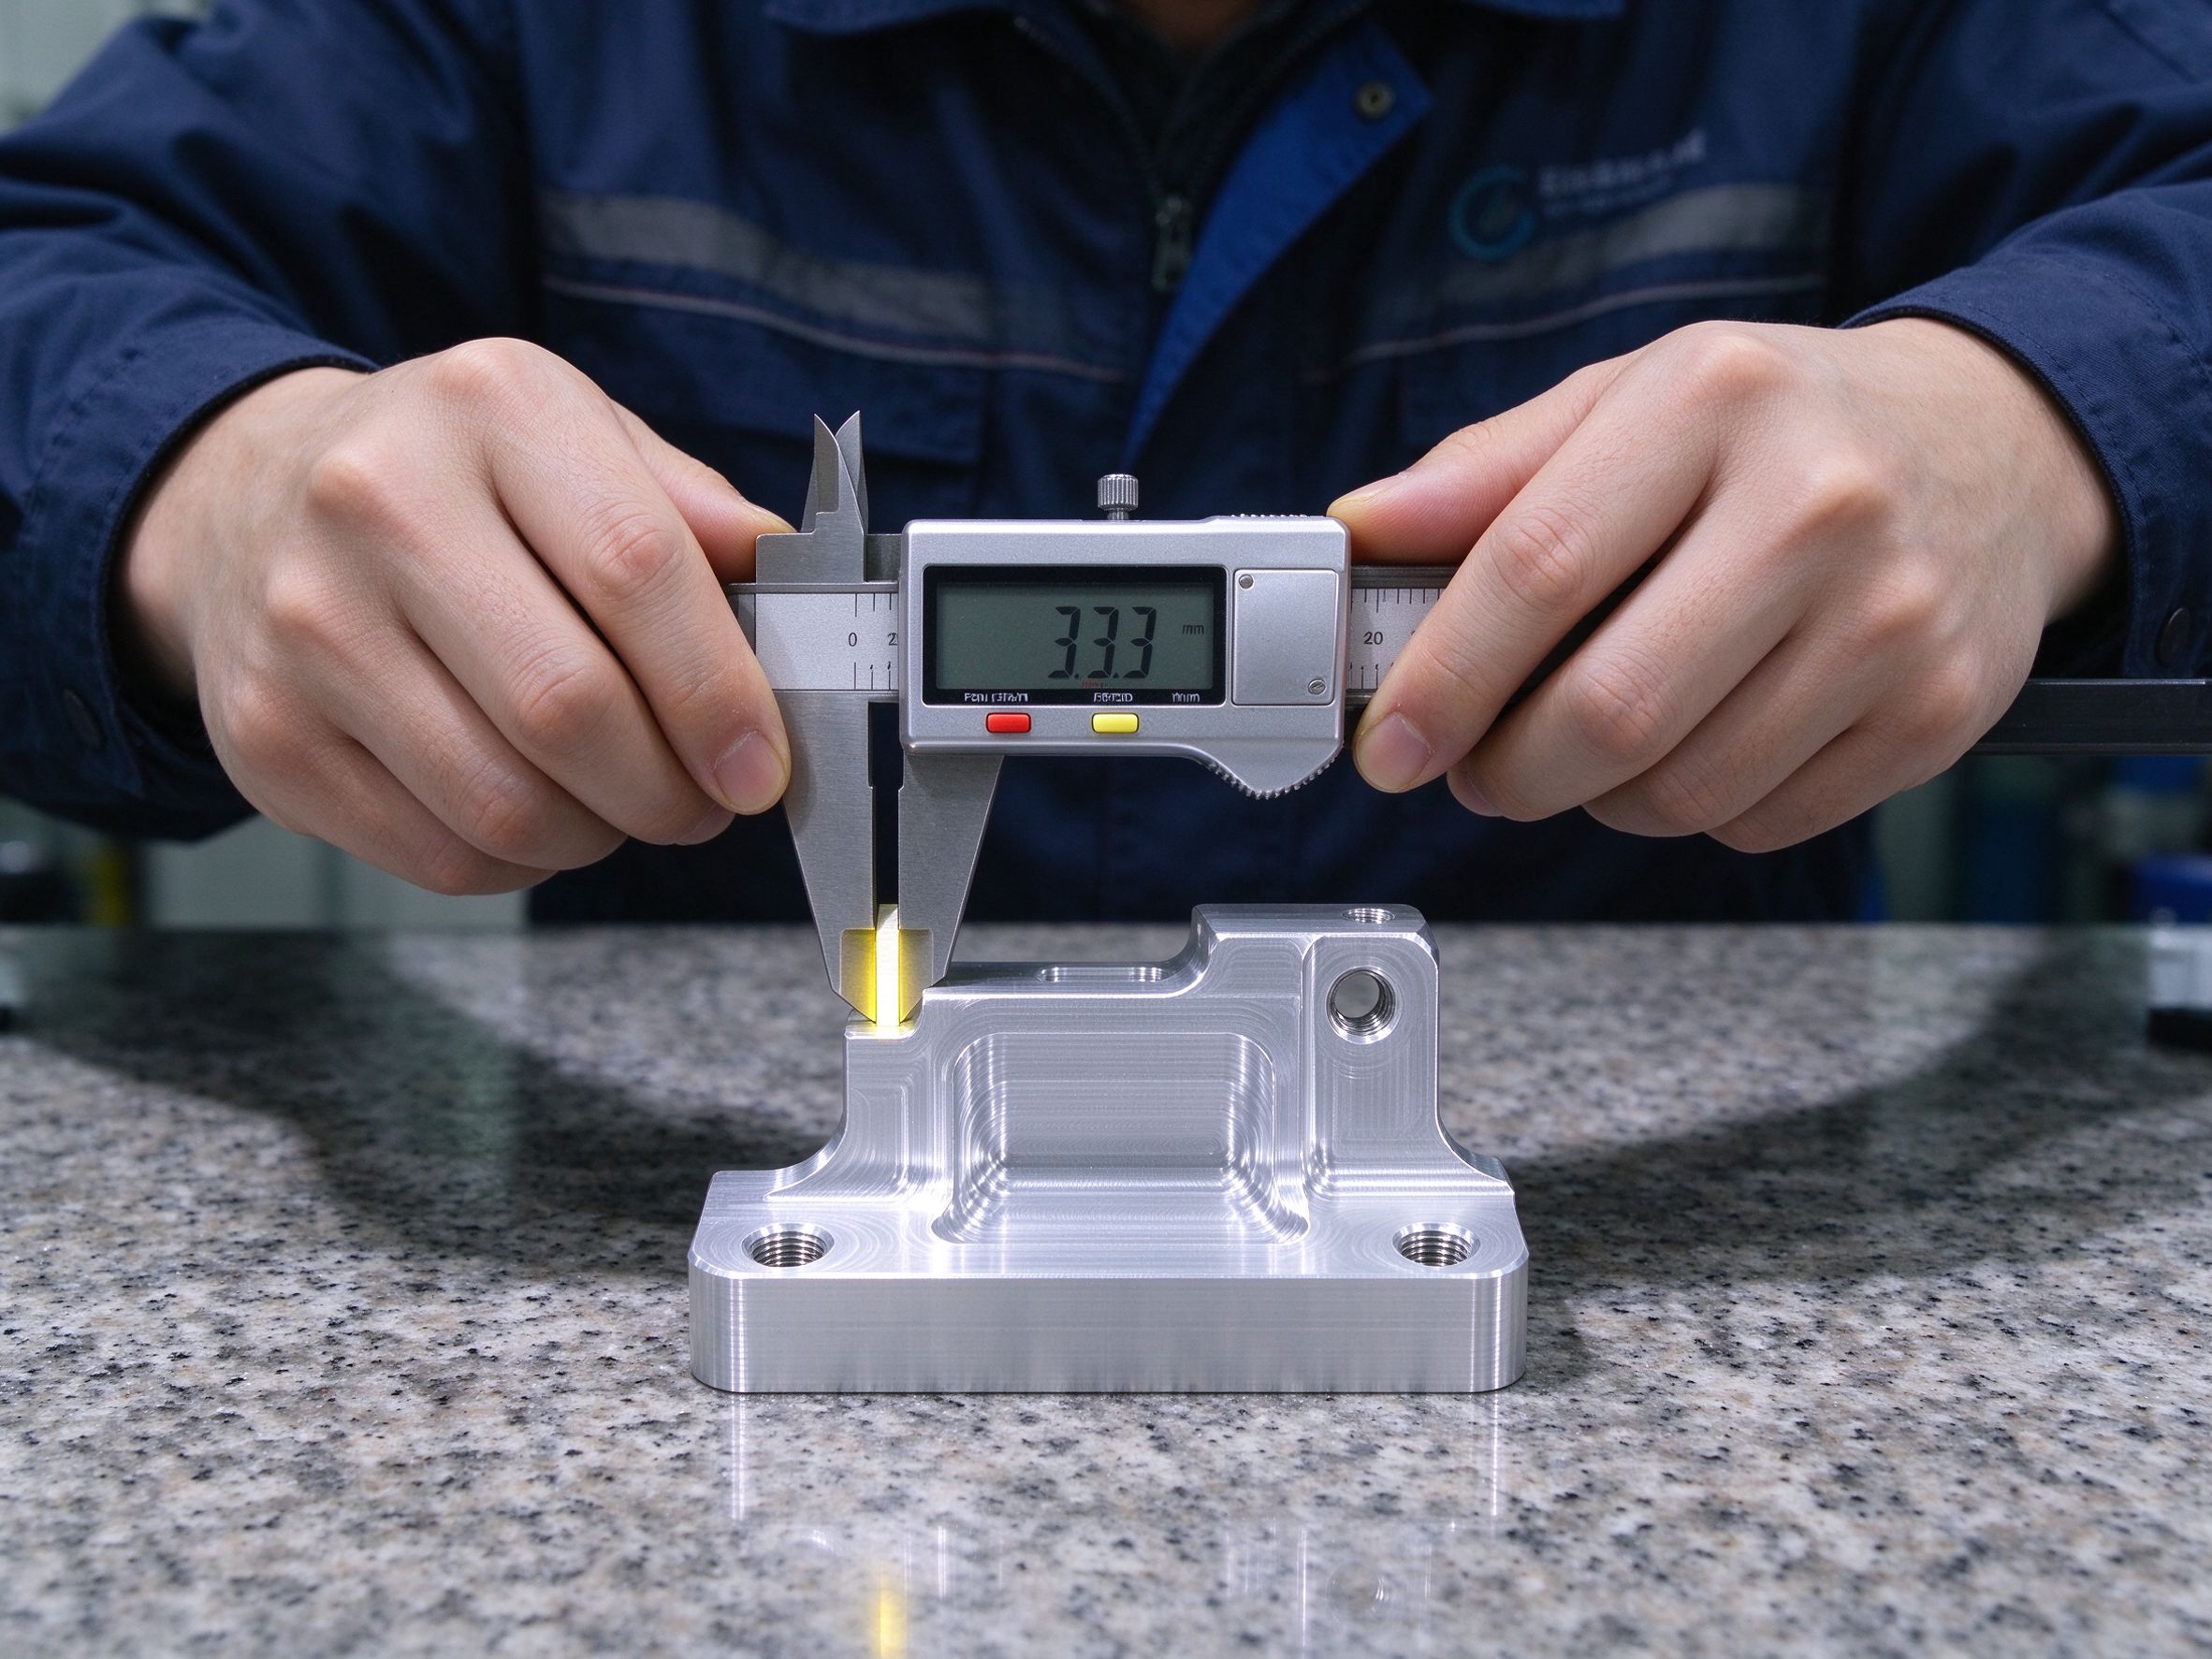
RFQ Checklist for Cost-Effective Aluminium CNC Parts
Supplying the same input set lets suppliers quote comparably:
Part & material
- 3D CAD model and current 2D drawing
- Material grade and temper, applicable standard
- Stock form — bar, plate, sheet, tube or extrusion
- Required dimensions and available sizes
Program & quality
- Quantity, batch size and annual forecast
- Critical dimensions, GD&T and surface requirements
- Finishing and post-processing steps
- Inspection documents, delivery, packaging and material certificates
Frequently Asked Questions
Is 6061 the cheapest aluminium for CNC machining?
Is 1100 or 3003 cheaper for machining?
Should a European buyer compare 6061 or 6082?
How can I reduce the cost of a CNC aluminium part?
Does machining 6061 require an extra T6 heat treatment?
What information do you need to quote an aluminium CNC part?
Request a Material & Cost Review
Send your drawing and CAD. We will review the alloy, temper, stock form, geometry and quantity, confirm the most economical machining route, and return a quote with finishing and inspection scope.
Xiamen Goldcattle · Manufacturing since 1998 · CNC machining of aluminium alloys · DFM and finished-part cost review · Related: 6061-T6 machining services →