Injection Molding Supplier in China for Custom Plastic Parts
Most of this page is written for the person who has to justify the decision. It sets out how to qualify an injection molding supplier in China on evidence instead of price: the scored audit, the document behind every score, the ownership and tooling terms to lock before metal is cut, and the records your US or EU market will ask for.
At a Glance
A China injection molding supplier is qualified on evidence, not on price. Five things decide whether a supplier belongs on your shortlist: DFM is done before the tool is cut; the mold class, steel and expected tool life are stated in writing; there is a dimensional record you can compare against your own drawing; the resin grade and batch are traceable; and ownership of the tool is defined in the agreement, not in conversation.
Everything else on this page exists to support those five points — the scoring instrument, the document behind each score, the commercial rules for tooling changes, and the records you should expect with the shipment.
What You Are Actually Buying from an Injection Molding Supplier
Short answer: you are buying four separate commitments, and a supplier can be strong in one and weak in another. A capable mold shop is not automatically a capable production supplier, and a busy production molder is not automatically a good toolmaker. Qualify them separately.
| Commitment | What you are buying | How it typically fails | Evidence that it will hold |
|---|---|---|---|
| Engineering / DFM | A moldability review before the tool is designed: draft, wall thickness, ribs and bosses, undercuts, gate and ejection positions, parting line, shrinkage allowance | The supplier builds exactly what the drawing says; the tool cannot hold tolerance or cannot eject the part cleanly | A written DFM report with marked-up geometry and a list of recommended changes, issued before tooling release |
| Tooling | A mold of a defined class: steel, cavity count, cooling design, runner type, expected tool life, and the ability to run your resin at your cycle | The tool is built to fit a budget rather than the volume; cavitation or cooling is undersized and cycle time never comes down | A tooling proposal stating mold class, steel, cavity layout, cooling, runner type and a tool-life statement |
| Production | Repeatable parts at an agreed cycle, with process parameters held between runs and across shifts | First samples are good; the second shipment drifts in dimension, colour or surface | Process parameter records, in-process check data and evidence that the second batch is measured, not assumed |
| Verification & delivery | Measurement against your drawing, documentation with the shipment, packaging that protects the part, and delivery on the agreed terms | Parts arrive with no dimensional record, mixed in a bag, and the buyer has to inspect everything to accept anything | Sample report formats, a packaging specification and a defined document list per shipment |
When China Sourcing Is the Wrong Decision
A supplier assessment is only useful if it can also produce a “no”. These are the programme profiles where a China-based molder is normally the wrong answer — not because of capability, but because of the economics or the constraints around the programme.
China Supplier vs Local or Regional Supplier
Short answer: there is no universal winner. The comparison is programme-specific, and the deciding variable is usually not the part price — it is tooling economics, change management, freight and the cost of being wrong.
| Factor | China supplier | Local / regional supplier | What it changes for you |
|---|---|---|---|
| Tooling build cost | Often lower, driven by labour and a dense mold-making supply chain | Often higher, driven by local labour rates and capacity | Affects the fixed block of the project — it matters most when volume is low and amortisation is thin |
| Tooling lead time | Longer elapsed time because of shipping and inspection at arrival | Shorter, and a visit to see the tool is practical | Affects launch date more than unit price |
| Freight and duty | Freight, duty, clearance and inland transport are added to the part cost | Usually domestic transport only | Turns a per-part saving into a landed-cost calculation — see total cost of ownership |
| Inventory and cash flow | Larger shipping batches encourage safety stock; longer pipeline ties up working capital | Frequent small deliveries are practical | Shifts cost from the purchase order into inventory and cash |
| Change management | Every change crosses a language, time-zone and revision-control boundary | Changes can be discussed on site in hours | Raises the value of strict revision control and a defined change process |
| Engineering access | DFM and mold engineering are usually included in the quotation process | Similar, with easier face-to-face reviews | Decides how early design problems are found — the cheapest place to fix them |
| Communication | Depends entirely on the supplier; an English-speaking engineering contact is now a normal expectation, not a bonus | Same language and working hours | Affects how quickly problems are understood rather than how often they happen |
| IP enforceability | Contractual protection is real but practical enforcement is harder | Practical enforcement is easier | Matters most for novel, easily copied products |
| Resilience | Diversified capacity and a broad supplier base, but exposed to freight disruption | Exposed to local capacity peaks | Has more effect on continuity than on price |
Supplier Qualification as a Scored Audit, Not a Checklist
Short answer: an unweighted checklist always ends in a pass, because a supplier only has to answer “yes” somewhere. A weighted audit forces a trade-off: a supplier that is strong on tooling but has no measurement record cannot reach the threshold.
Score each dimension from 0 to 5 on the same evidence standard: 0 no answer, 1 verbal assurance, 3 a document is supplied, 5 a document that is independently verifiable through an audit, a sample measurement or a third-party certificate.
The Evidence Behind Each Score
Ask for these documents by name. The difference between a weak and a strong answer is usually not the number — it is whether anything written was produced at all.
| Dimension | Document to request | Weak answer | Strong answer |
|---|---|---|---|
| Engineering / DFM | Written DFM report with marked-up 3D or drawing views | “The part is fine to mold” | Named issues with a recommendation per issue: draft angle additions, wall transitions, rib thickness, gate location, ejection plan, expected shrinkage |
| Tooling | Tooling proposal stating mold class, steel, cavity count, cooling layout, runner type, tool life | A single tooling price | A defined asset, with the cavitation and cooling justified by the annual volume rather than by the budget |
| Production control | Process parameter sheet and in-process check plan | “Experienced operators” | Recorded parameters (fill, hold, cooling, cycle) plus the specific in-process checks and their frequency |
| Metrology | Sample dimensional report with the measurement method per characteristic | “We check the important sizes” | A report showing each toleranced characteristic, the instrument used, and results against the drawing limits |
| Material control | Resin data sheet, material certificate, lot or batch traceability | “Equivalent grade” | Named resin grade and supplier, with a certificate per batch and a change note whenever a substitution is proposed |
| Ownership & IP | Written ownership, storage, maintenance, access and transfer terms; NDA | “The mold is yours, don’t worry” | Clauses in the quotation and agreement covering title, maintenance, storage, third-party access and transfer conditions |
| Export | Document list per shipment, packaging specification, Incoterm | “We ship worldwide” | A defined document pack, packaging that protects the finished surface, and the Incoterm named on the quotation |
| Communication | Named engineering contact and response commitment | A sales contact only, with no engineering path | A named engineer who answers technical questions in writing and owns the action list between gates |
Red Flags in a China Injection Molding Audit
Each flag below appears on real programmes, and each one has a question that exposes it before money is committed.
Decision Gates from RFQ to Repeat Production
Short answer: a molding programme is a sequence of decisions that each produce a document. When a gate has no document, the next decision is being made on trust — and that is where programmes go wrong.
Is this part moldable, and by which route?
Inputs: CAD model, drawing, resin or performance requirement, expected annual volume, first-order quantity, target market. Output: a DFM report, a recommended tooling route and an indicative cost.
Frozen at this gate: part geometry revision and design intent.The mold is defined as an asset, then authorised
Output: mold class and steel, cavity count, cooling and runner design, expected tool life, tooling lead time, tooling price, and the ownership, maintenance and change terms.
Frozen at this gate: the accepted DFM and the drawing revision. Anything later is a change, not a correction.Physical parts against the drawing, not against a photo
Output: T1 samples, a dimensional report listing each toleranced characteristic, a cosmetic assessment against an agreed standard, and a list of proposed corrections with the cost responsibility marked.
Frozen at this gate: which corrections are inside the tooling price and which are change orders.The process is defined before the volume starts
Output: process parameter sheet, capability or measurement data from the approval run, packaging specification, and the document list that will accompany each shipment.
Frozen at this gate: the approved process window and the reference sample.Repeat runs are measured, not assumed
Output: per-shipment dimensional checks and material records, plus periodic re-verification. This is where drift appears, and where a documented baseline makes it visible early.
Nothing new is frozen. The job is to hold the baseline and detect movement.One revision, one owner
Every gate references the drawing revision and the mold file revision it was executed against. A supplier who can name both, and show you the records, is operating a controlled process rather than a competent workshop.
Who Owns Which Decision
Most disputes in an overseas molding programme come from an activity that both sides assumed the other one owned. Agree the split explicitly at Gate 0.
| Activity | Buyer | Goldcattle |
|---|---|---|
| Function, fit and design intent | Defines | Reviews for moldability and flags conflicts |
| Geometry and revision control | Issues and freezes the revision | Works to the named revision; raises conflicts, never edits geometry |
| DFM recommendations | Approves or declines each one | Proposes, with the consequence of each change stated |
| Tool design and build | Reviews the tooling proposal | Designs, builds and proves the tool |
| Tool ownership | Holds title when the tool is paid for | Stores and maintains it under the agreed terms |
| Cosmetic standard | Defines the acceptance level, ideally with a reference sample | Produces to the agreed level and reports deviations |
| Resin grade and substitution | Approves the grade and any substitution | Confirms availability, properties and process behaviour |
| Process parameters | Receives the parameter sheet | Sets, records and maintains the window |
| Dimensional verification | Accepts on the report, and may audit or re-measure | Measures, reports and retains the records |
| Corrective action | Raises the non-conformance and accepts or rejects the fix | Owns the analysis and the correction |
| Change orders | Approves scope and price before the change is made | Prices the change and states the lead-time effect |
| Packaging specification | Approves | Executes and documents |
| Market-access documentation | Defines the required standard for the destination market | Issues the matching material and process documents |
| Import clearance and duty | Owns, unless the quoted Incoterm places it elsewhere | Prepares the export document pack |
Tooling Changes and Revision Rounds: The Commercial Rules
Short answer: agree the boundary between a correction and a change before the tool is cut. After T1, every conversation about who pays is a negotiation; before tooling release, it is a specification.
| Type | Definition | Typical examples | Who normally bears the cost |
|---|---|---|---|
| In-scope correction | The tool does not deliver the accepted DFM or the frozen drawing revision | A dimension outside the drawing limits, a sink mark from a cooling deficiency, a short shot from a gating problem, an ejection mark in a functional area | The supplier — the tool has not met the specification it was ordered to |
| Change order | The buyer introduces a requirement that was not in the accepted DFM or the frozen revision | Adding a boss or rib, moving a feature, tightening a tolerance on a new characteristic, changing texture or colour, altering ejection positions | The buyer — priced and scheduled before the work starts |
| Design revision | The part geometry itself changes after tooling release | A new revision of the model or drawing that alters the mold form | The buyer, and the cost depends on whether the change is weldable or needs a new insert |
| Ambiguity resolution | A drawing conflict or an undefined requirement surfaces only at sample stage | Conflicting tolerances between views, an undefined cosmetic level, an unspecified gate or ejector position | Shared or charged, depending on when it was raised — which is why Gate 0 exists |
What to agree in writing before Gate 1
- How many T-sample rounds are included in the tooling price, and what a further round costs.
- The lead time of a sample round, so the programme schedule reflects reality rather than hope.
- Whether each tool modification is recorded in the mold file, with a mold file revision number that the next sample round references.
- What happens to the reference sample and the inspection baseline after a modification — they must be re-established, not carried over.
- How a supplier-caused delay is treated, and how a buyer-caused change is priced and scheduled.
Mold Ownership, Transfer and Continuity
Short answer: when a customer pays for a custom mold, the mold is the customer’s asset. But ownership, access and transferability are three different questions, and all three need to be in the agreement before the tool is built — not discussed after it exists.
| Question | What to have in the agreement | Why it matters later |
|---|---|---|
| Who holds title? | The customer owns the tool once it has been paid for, and the tool is listed as customer property in the quotation and purchase agreement | Affects your asset register, your insurance and your ability to change supplier |
| Who may use it? | No third party runs the tool, and no parts from it are sold, without written consent | Prevents uncontrolled production and grey-market parts |
| Where is it stored, and who can touch it? | Storage location, an asset identifier under your part number, and a named access list | Makes the tool findable and accountable years later, after staff change |
| Who maintains it? | Maintenance responsibility, what counts as normal wear against damage, who pays, and whether maintenance records are kept | Tool condition is the main long-term driver of part quality and downtime |
| What makes it transferable? | Mold drawings, cooling and runner layout, the process parameter sheet, the dimensional baseline and the reference sample are yours or are supplied on request | Without this documentation a tool is only nominally portable — it arrives but cannot be run |
| How is a transfer executed? | Condition of the tool when released, who prepares and crates it, the preparation cost, and the documents released with it | Prevents a disagreement at exactly the moment you have least leverage |
| May a duplicate be built? | Whether a copy tool is permitted for backup or second-sourcing, who builds it and who owns it | Continuity planning needs to be agreed, not discovered |
| What happens at end of life? | Retirement, scrapping or return of the tool, and deletion or return of the digital files | Closes the loop on both the asset and the geometry |
Design Rights, Confidentiality and Exclusivity
Short answer: an NDA protects information; it does not decide who owns what, and it does not control access. Those are three separate agreements, and all three are normal to discuss at the start of a programme.
Which Tooling Route Fits the Programme
Short answer: the route follows the volume and the design risk — not the buyer’s preference. The right question is not “what does the tool cost?” but “what does the tool cost per good part at my annual volume?”
| Situation | Route | What it changes commercially |
|---|---|---|
| Design is still changing | Rapid or soft tooling | Low tooling investment and fast samples; accept a short tool life and a higher unit price, and do not expect a production asset |
| Prototype validation before launch | Aluminium or softer-steel tool | Real molded parts from the real geometry without committing to production tooling; the tool normally becomes a bridge, not the production asset |
| Bridge production while demand is proven | Intermediate tooling | Covers the gap between pilot and full programme at a moderate investment; the production tool is still justified later |
| Stable, recurring volume | Hardened production tool | Highest tooling investment, lowest unit cost and a defined tool life — the route that makes sense when the design is frozen |
| High volume with a long horizon | Multi-cavity with hot runner | Large tooling investment offset by cycle time and material savings; requires a realistic annual volume commitment to be justified |
| Several related parts of similar size | Family tool | One tooling investment covering several parts; shared risk — a fault or a shortage of one cavity affects the whole family |
| Two materials or two colours | Two-shot / 2K | Removes an assembly step; adds machine and tooling complexity and reduces the number of capable suppliers |
| A metal component must be integrated | Insert molding | Removes assembly labour and can improve joint strength; adds insert loading, positioning and tool-wear considerations |
Machine Fit, Capacity and Scheduling Reality
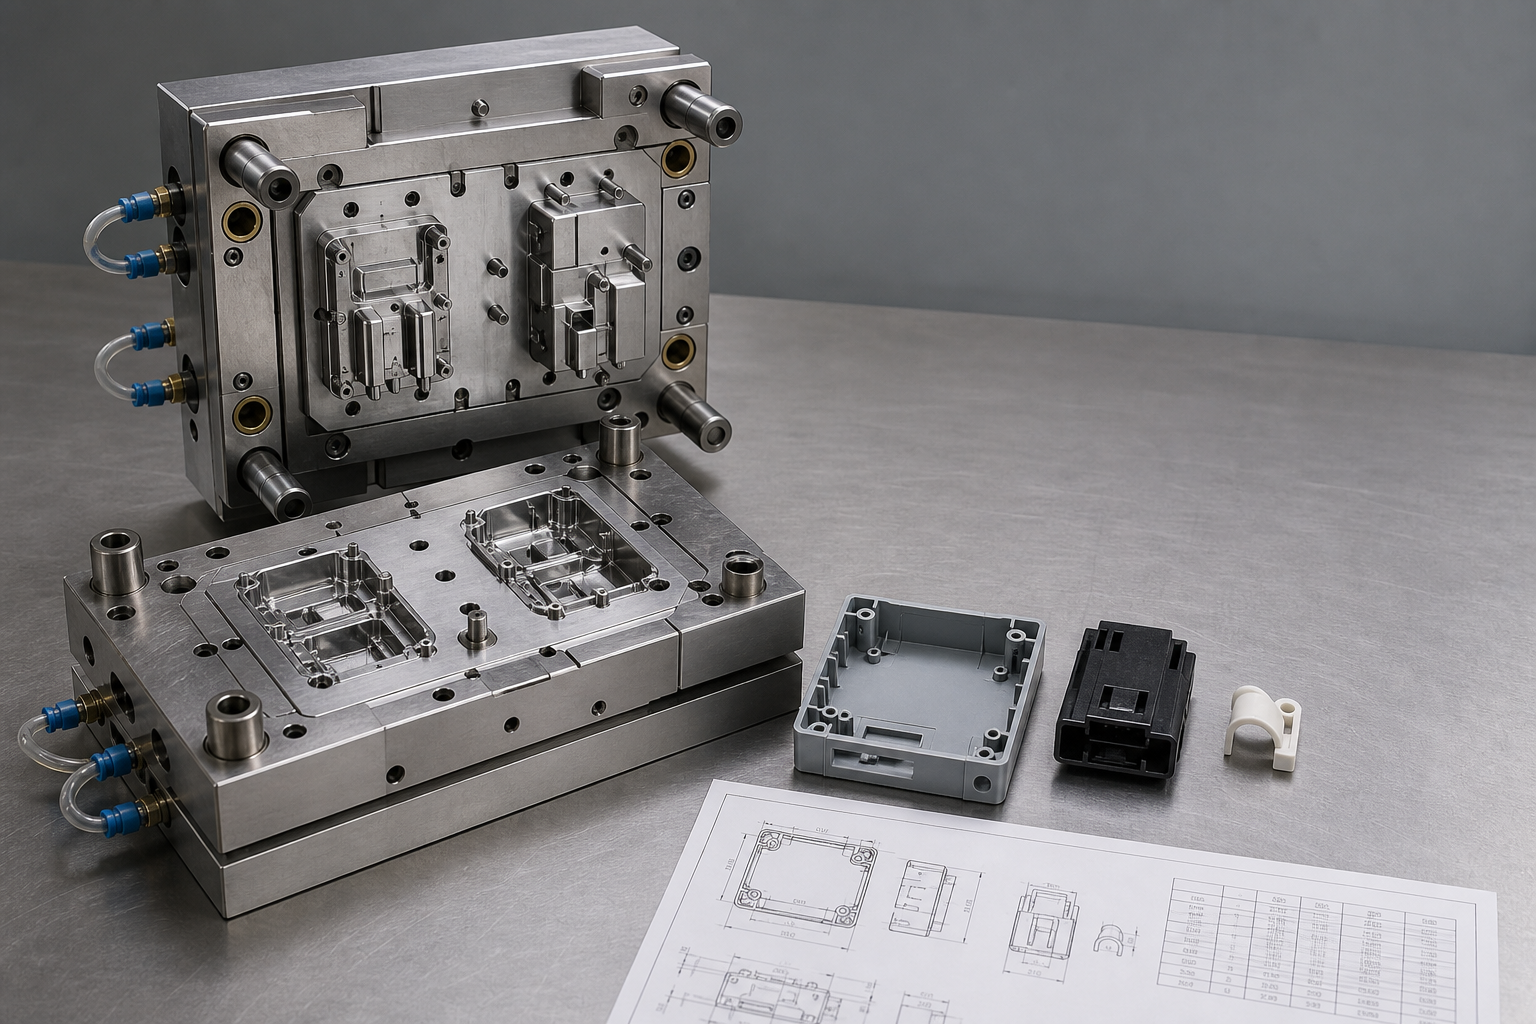
Short answer: ask two questions that are rarely asked — which machine will run my part, and what else is scheduled on it. The first determines whether the part can be made; the second determines whether it is made on time.
How the machine is selected
- Projected area and clamp requirement — driven by part size and injection pressure, not by part weight alone.
- Shot size against part weight plus runner — an oversized barrel spends resin on residence time, an undersized one cannot fill the part.
- Part envelope against the platen and tie-bar spacing — a part that fits the tonnage can still fail the geometry.
- Resin and process requirements — drying, hot-runner zones, temperature control units and ejection strategy.
- Volume and cavitation — the cavity count chosen at Gate 1 dictates the press that will run the job for the life of the programme.
What to verify before committing volume
| Verify | Why |
|---|---|
| The machine is named in the tooling or production proposal | Otherwise the tool may be built for a press nobody intends to use |
| How the press is shared with other programmes | Shared capacity is normal; unexplained scheduling risk is not |
| Capacity at the specific time you need it, not on an annual average | Seasonal peaks are the usual cause of a missed schedule |
| Who runs the second and third shift, and to the same parameters | Drift between shifts is a classic source of batch-to-batch variation |
| What happens if the tool is moved to another press | A press change normally requires a fresh process setup and may require re-approval of the part |
| The escalation path when capacity tightens | Tells you whether you will hear about a problem early or late |
Resin Selection as a Purchasing Decision
Short answer: choose in this order — duty cycle, then compliance, then process, then grade. Most expensive resin mistakes come from picking a familiar grade before anyone defined what the part has to survive.
Duty cycle — static or cyclic load, impact, operating temperature range, chemical and UV exposure, expected service life.
Compliance — destination market, food contact, flammability or electrical requirements, and which declarations your customer requires.
Process fit — wall thickness, flow length, shrinkage and warpage behaviour, drying requirements, and whether the geometry suits the family at all.
Grade and supplier — the specific grade within the family, its documented properties, and its availability for your volume.
Commodity (PP, PE, PS), engineering (ABS, PC, PA, POM, PBT, PC/ABS), reinforced (PA-GF, PBT-GF, PC-GF), high performance (PEEK, PPS, PEI) and elastomers (TPU, TPE).
Send the application, operating temperature, chemical exposure, mechanical requirement, appearance requirement and target volume, and the engineering team can shortlist candidate grades with their trade-offs.
Material Traceability and Batch Records
Short answer: traceability is a chain from the resin lot to the shipped carton, and it breaks at the weakest link — usually an undocumented substitution or a merged batch.
A batch record normally links resin lot → machine → operator → inspection result, so that a question raised months later can be answered from documents rather than memory. Ask who holds those records, how long they are kept, and whether they can be supplied with a specific shipment when a customer’s own audit requires it.
US and EU Market-Access Documentation
Short answer: market-access documentation is scoped — it depends on the material, the application, the destination market and who carries the legal obligation. A blanket statement such as “all our parts are RoHS and REACH compliant” is not meaningful without that scope.
| Requirement | What it actually applies to | What a molder can issue | What a molder cannot decide for you |
|---|---|---|---|
| RoHS | Restricted substances in electrical and electronic equipment — scope follows the product category and its market placement | A declaration for the materials and parts supplied, against a named RoHS version, based on material declarations from the resin and additive suppliers together with the process inputs used | Whether your finished product falls inside the scope of the directive in your market |
| REACH / SVHC information | Substances of very high concern present in an article above the applicable concentration threshold, which triggers an information obligation in the supply chain | Information passed through from resin, masterbatch and additive suppliers, plus a statement of the process inputs used in molding | The final article-level assessment for your product, which needs the complete bill of materials including components you supply |
| SCIP / EU article data | Data on articles containing candidate-list substances that are placed on the EU market; the duty typically sits with the EU-based supplier or importer | The material and substance data the EU party needs in order to submit | Acting as the EU responsible party on your behalf |
| Food contact | Materials and articles intended to come into contact with food, where the specific material must be authorised for the intended use | The regulatory status of the grade supplied and the full list of process inputs, so the assessment can be made | Certifying a finished article as suitable for a specific food-contact application — that requires the declaration for the exact grade and use |
| Flammability and electrical ratings | A named grade at a defined thickness under a specified test standard | The certification evidence for the specified grade | Extending that rating to a different grade, thickness or wall section |
| Medical and other regulated programmes | Biocompatibility, process validation and documentation requirements defined by the device or product programme | Material certificates, lot traceability, dimensional records, process records and inspection data | Holding the regulatory responsibility for the finished device, which stays with the legal manufacturer |
How to specify documentation in the RFQ
- Name the destination market and the standard or directive that applies to your product.
- State who is the legal manufacturer or importer for that market, because that determines who carries the obligation.
- List the declarations your customer will ask you for, so the pack is assembled once rather than retrieved later.
- Ask for the documentation pack to be quoted as part of scope, not handled informally after the order.
Quality Records: What the Documents Actually Prove
Short answer: the stages of a quality system are machinery; the records are the output. When you evaluate a supplier, ask what you will receive, and read each document for what it can and cannot establish.
| Document | What it proves | What it does not prove |
|---|---|---|
| Material certificate | The resin grade and lot as supplied to the molder | That the part was molded from that lot, or under the correct conditions — pair it with the batch record |
| Process parameter record | The settings used for a defined run | That the settings held for the whole run or across shifts |
| In-process check data | Readings for the characteristics sampled, at the intervals recorded | Anything about characteristics that were not checked, or between the samples |
| Dimensional report | Measured values against the drawing limits for the listed characteristics | Characteristics omitted from the report — which is why the report scope must be agreed |
| First-article inspection | Every characteristic documented for one part at one revision | That later production parts match it, unless the baseline is maintained |
| Certificate of conformity | A declaration that the parts meet the drawing and specification | It is an assertion, not a measurement — read it as a commitment, not as evidence |
| Capability data | How a characteristic behaves statistically over the measured sample | Behaviour over the whole population, if the sample is small or unrepresentative |
| Packaging specification | How the part is protected and identified | Nothing about the part itself |
Total Cost of Ownership for a Molded Part
Short answer: tooling is the most visible cost in a molding programme and rarely the largest one. Once production starts, resin, cycle time, secondary operations, inspection, freight and the cost of a quality escape accumulate against a number that you approved in a single line on a quotation.
How tooling amortisation behaves
The arithmetic below is illustrative: it demonstrates how a tooling investment behaves across a programme, not a price and not a quotation. It assumes a tooling investment of $8,000.
The same tooling investment is $4.00 per part on the first order and $0.13 per part across a three-year programme. That is why a tooling decision should be made against the programme, not against the first purchase order — and why a three-cent difference in unit price across 60,000 parts is worth $1,800, a number that should be placed beside the cost of one avoidable tooling correction round, the cost of a late shipment, and the value of a supplier who answers technical questions in writing.
Why the Lowest Tooling Quote Is Usually Not the Lowest Project Cost
Short answer: a cheaper tool is not automatically a bad tool — it is a different asset. The problem is not the price; it is comparing tooling prices without comparing what each tool is built to do.
| What a cheaper tool changes | Where the cost reappears |
|---|---|
| Tool steel grade and hardness | Shorter tool life, more frequent maintenance and repair, higher risk of cavity damage during a run |
| Cavity count | Longer cycle time per part and higher unit cost for the whole programme, unless the annual volume genuinely does not justify more cavities |
| Cooling design | Longer cycle, warpage that has to be corrected by process compromise or by accepting a wider tolerance band |
| Runner type | Higher material waste per shot and additional handling of runners |
| Sliders, lifters and inserts | Manual insert loading between shots, longer cycle and a dependence on operator discipline |
| Surface and texture work | Secondary finishing, or an appearance standard that quietly cannot be met |
| Spare cores and inserts | Days of downtime when a cavity fails with no spare on the shelf |
| Tool documentation | The buyer inspects at receiving, and the tool cannot be moved or re-tooled without going back to the same supplier |
Three Project Profiles and How to Qualify Them
Qualification questions differ by programme type. Below is what to verify for three common profiles. These are evidence requirements, not case studies: no project data is presented here, and published project examples are on the injection molding services page.
Profile 1 — High-volume recurring part
A housing, closure or functional component produced continuously against an annual volume.
- What dominates costCavitation, cycle time
- Second factorCooling design, tool life
- Third factorProcess consistency across runs
- Main riskSilent drift between batches
Demand at qualification: a tool-life statement and the cavitation rationale; the cooling layout and how it supports the quoted cycle; capability or measurement data from an approval run; the in-process check plan and frequency; a maintenance schedule and spare-cavity plan; and how parameters are controlled on second and third shifts.
Rejection signal: a cycle time quoted without a cooling design, or an inability to state what happens when a cavity is damaged mid-run.
Profile 2 — Complex engineering part
Undercuts, tight tolerances on functional features, and a visible appearance surface.
- What dominates costDFM depth, tool design
- Second factorSlider and lifter design
- Third factorGate and weld line position
- Main riskWarpage and appearance disputes
Demand at qualification: a written DFM report with the undercut strategy and ejector plan; the gate and weld line positions with their cosmetic consequence; a defined appearance standard with a reference sample; a stated tolerance approach for each critical feature; and revision-control rules that name the drawing revision on every document.
Rejection signal: a tooling quotation with no DFM, or a cosmetic standard defined only as “good quality” with no reference part.
Profile 3 — Regulated or quality-sensitive part
A programme where material, traceability and documentation are part of the product requirement.
- What dominates costDocumentation and verification
- Second factorMaterial grade control
- Third factorChange control
- Main riskAn undocumented grade substitution
Demand at qualification: the material certificate per lot and the batch record that links it to the run; a first-article inspection in a defined format; the records-retention period; the non-conformance and corrective-action process; audit access, including third-party audits; and written confirmation of the certification scope your programme requires.
Rejection signal: traceability that stops at the resin supplier, or a substitution proposal that arrives without a change note and an approval step.
Direct Answers to Supplier-Assessment Questions
Short, self-contained answers, written so they can be quoted directly.
What to Send for a Supplier Assessment
The first six items are the minimum to receive a real tooling and unit-cost proposal. The remainder remove the assumptions that otherwise end up as change orders.
- 3D CAD model (STEP, IGES or native)
- 2D drawing with critical dimensions and tolerances
- Resin grade, or the performance requirement if the grade is open
- Expected annual volume and first-order quantity
- Colour and surface finish requirement, ideally with a reference sample
- Target market and the standard or directive that applies
- Insert, overmolding or assembly details
- Cosmetic acceptance level for visible surfaces
- Packaging, labelling and delivery destination
- Required documentation list per shipment
- Target delivery date and the programme horizon
- Existing tool details, if a mold or drawing set is being transferred
Ten questions that separate a supplier from a broker
- Which mold class, steel and cavity count do you propose, and what tool life do you expect?
- Which press will run my part, and what else is scheduled on it?
- Which operations are in-house, and which are subcontracted?
- Can you send a sample dimensional report from a previous project, with the drawing removed?
- What is the ownership, maintenance and transfer clause for the tool?
- Which drawing revision is this quotation based on, and how is a revision change handled?
- How many sample rounds are included, and what does an additional round cost and take?
- How do you notify and approve a resin substitution?
- Which records accompany each shipment, and for how long are they retained?
- When a defect is found in your plant, what is the corrective-action process?
Injection Molding Supplier FAQ
How do I choose an injection molding supplier in China?
Score the supplier on evidence rather than price. The five decisive points are whether DFM is completed before the tool is cut, whether the mold class, steel and expected tool life are stated in writing, whether a dimensional report can be compared with your own drawing, whether the resin grade and batch are traceable, and whether ownership of the tool is defined in the agreement. A supplier who answers all five is running a controlled process; a supplier who answers only the commercial questions is selling a price.
What should I send to a China injection molding supplier for a quote?
A 3D CAD model plus a 2D drawing with dimensions and tolerances, the resin grade or performance requirement, colour and surface finish, expected annual volume and first-order quantity, the target market and its regulatory requirements, insert or assembly details, packaging requirements and the delivery destination. If the annual volume is not yet known, send the range — it changes the recommended tooling route rather than the part itself.
How much does injection mold tooling cost in China?
There is no fixed figure, and a quotation that gives one without defining scope should be treated as indicative only. Tooling cost is driven by mold class and steel, cavity count, sliders and lifters, hot runner, cooling design, tolerance and surface requirements, the validation and documentation scope, and the tool life specified. A tool built for a few thousand prototype parts and a tool built for millions of shots are different assets with different prices.
How long does injection mold tooling take?
Tooling lead time has several sequential phases — mold design and review, steel and standard-part procurement, machining, EDM and grinding, polishing and assembly, then trial and sample. The quoted time also depends on what it is measured from, so ask whether it starts at quotation acceptance, at DFM approval or at the frozen drawing revision, and whether the sample round and any correction round are inside the quoted period.
Who owns the injection mold?
When a customer pays for a custom mold, the mold is the customer’s asset. Beyond title, four terms should be written into the quotation and purchase agreement: where the tool is stored and who may access it, who maintains it and what counts as damage rather than wear, what documentation makes it transferable, and the conditions and cost of preparing it for shipment. Settle these before the tool is built.
Can I use my own mold with a China injection molding supplier?
Often yes, provided the tool arrives in a known condition. A transfer normally requires the mold drawings, cooling and runner layout, the last process parameter sheet and the dimensional baseline; the receiving supplier will inspect the tool, confirm it fits an available press, establish a process window and run samples for approval. Tools without drawings or records can still be run, but the first process setup has to be established from scratch, and that cost belongs in the plan.
What materials can a China injection molding supplier process?
Commodity resins such as PP, PE and PS; engineering resins including ABS, PC, PA, POM, PBT and PC/ABS; glass-reinforced grades; high-performance materials such as PEEK, PPS and PEI; and elastomers including TPU and TPE. The grade should be selected from the duty cycle first — load, temperature, chemical exposure and life — then checked against compliance, process fit and availability.
Can you support low-volume injection molding?
Yes. Low-volume production is normally served with rapid or bridge tooling in aluminium or a softer steel, which keeps the tooling investment proportionate to demand and allows production-grade parts to be produced before a hardened tool is justified. The route should be chosen from the tooling investment, the annual volume, the resin and the part complexity — not from the size of the first order alone.
Can you provide DFM before tooling?
Yes, and it should be treated as a precondition rather than an option. A useful DFM report is a written document with marked-up views that names each issue and its recommendation: draft angles, wall thickness and transitions, rib and boss proportions, undercut strategy, gate and ejector positions, parting line, and expected shrinkage. It is also the document that defines which later changes are corrections and which are change orders.
How do you control part-to-part consistency?
By freezing the process window in a recorded parameter sheet, applying the same parameters across shifts, checking defined characteristics in-process at a defined frequency, and periodically re-verifying dimensions against the approved baseline rather than against the previous shipment. Consistency problems nearly always come from an unfrozen process or a baseline that was never documented, not from a machine that cannot hold tolerance.
Can you provide material certificates and inspection reports?
Yes. Resin is lot-tracked from receiving through molding, so a material certificate can be linked to the run that produced your parts, and shipments can be accompanied by a dimensional inspection report, a first-article inspection report and a certificate of conformity. Agree the report scope, the sampling rate and the document list before the first production order, so the pack is complete on arrival rather than retrieved later.
Can you export injection molded parts to the US and Europe?
Yes. Export packaging, labelling, Incoterms and the document pack are agreed per order. On market-access documentation the position is deliberately scoped: declarations such as RoHS or REACH information are issued according to the material, the application and the destination market, and the legal obligation normally sits with the manufacturer or importer placing the product on that market. Tell us the destination and the standard, and the matching documentation is quoted as part of scope.
How are tooling modifications handled?
Two categories, agreed before tooling release. Corrections — where the tool does not deliver the accepted DFM or the frozen drawing revision — are the supplier’s cost. Changes — where the buyer introduces a requirement that was not in the accepted scope — are priced and scheduled before the work starts. Each modification is recorded in the mold file, and the reference sample and inspection baseline are re-established afterwards.
Do you sign an NDA?
Yes, a mutual NDA can be signed before drawings are exchanged. It is worth separating three topics that an NDA does not cover: confidentiality of your information, ownership of the product geometry versus the molder’s mold design and process know-how, and exclusivity if the part must not be produced for anyone else. Each is a short conversation at the start of a programme and an expensive one later.
Start a Supplier Assessment
Send the CAD model, the 2D drawing and the volume expectation. The engineering team returns a DFM report, a recommended tooling route with its commercial consequences, and a quotation that states mold class, steel, cavity count, tool life and the ownership and change terms in writing.
Upload CAD / Request a Quote →Free DFM review · NDA available on request · Tooling and unit cost quoted together
See the full manufacturing scope →Scope, claims and how this page is maintained
- Purpose: this page is a supplier-assessment framework for buyers sourcing molded plastic parts from China, and a description of how Goldcattle supports that assessment. It is not a price list and not a certificate of conformity.
- Cost figures: all amounts on this page are arithmetic examples, labelled as illustrative, used to demonstrate how tooling amortisation behaves. They are not quotations, not market averages and not derived from any customer order.
- Market comparison: the China versus local comparison uses general market characteristics and deliberately avoids percentage claims, because tooling and unit-cost differences depend on mold class, steel, cavitation, tolerance, validation and volume.
- Compliance statements: product-compliance documentation is scoped to the material, the application and the destination market, and the legal obligation normally sits with the party placing the product on that market. No blanket compliance claim is made on this page. Confirm the applicable documentation for your programme before ordering.
- Certification scope: confirm the specific certification scope required by your programme, and review the current certificates, before awarding tooling. Current certificates and available documentation are listed on the quality and certifications page.
- Capacity and equipment: machine and capability figures are confirmed per project in the tooling proposal. Current published capability is on the injection molding services page.
- Review: maintained by the Goldcattle injection molding engineering team and updated as tooling practice, materials and documentation requirements change. Updated September 2026.