
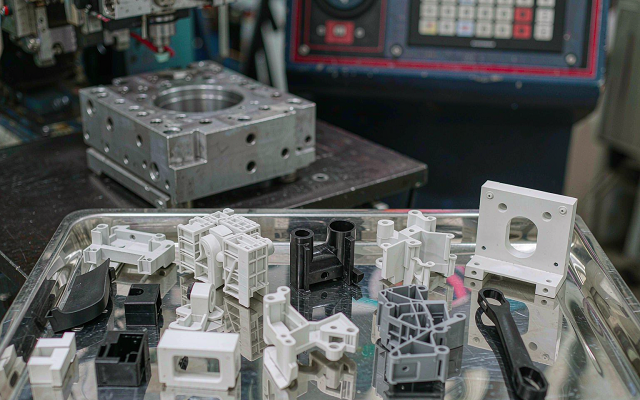
Need injection-molded parts faster? We build rapid tooling in-house — aluminum or soft steel, simplified and standardized — then mold your parts in the production resin you actually intend to use. Real molded parts, for product validation, pilot runs, bridge production and low-volume output.
Rapid injection molding at a glance
A short summary for engineering and procurement teams evaluating whether rapid tooling is the right route for the next stage of a program.
What rapid injection molding actually means
The short answer
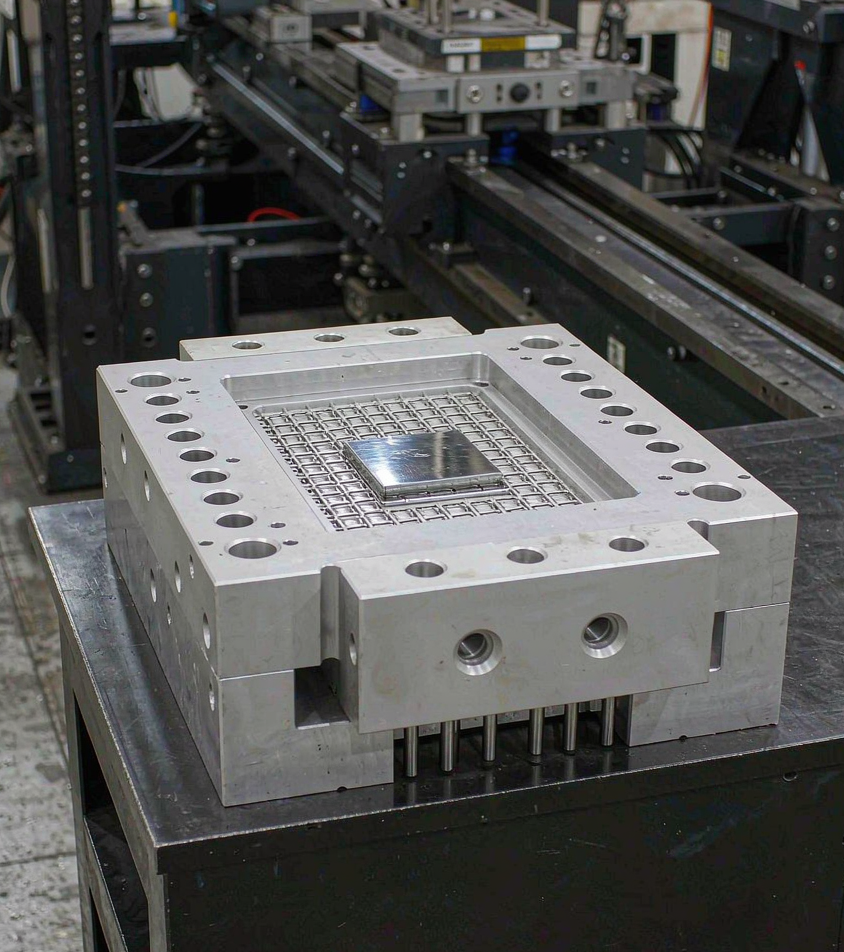
Rapid injection molding is not a different molding process — it is a different tooling strategy. The plastic is melted, injected, packed, cooled and ejected exactly as it is in production. What changes is the tool: instead of building hardened, multi-cavity production tooling, we build a simpler aluminum or soft steel mold that can be machined and put on the machine much faster.
That is the whole reason it is "rapid": you get to first molded parts sooner, in the resin and by the process your production parts will use, without first committing to full production tooling.
This matters because a prototype that is not molded by the production process hides the problems you are most likely to hit later. A machined or printed part can look correct while telling you almost nothing about gate placement, weld lines, sink marks, warpage, ejection, shrinkage or how the part behaves in assembly. Rapid tooling surfaces those problems while the design is still cheap to change.
Why is rapid injection molding faster?
Four practical reasons — all of them about reducing the time between a frozen-enough CAD model and first molded parts in your hand.
Rapid tooling instead of hardened tooling
Aluminum and pre-hardened steel machine faster than tool steel and need no subsequent hardening cycle. The tool is ready for the machine sooner.
- No heat-treatment step before sampling
- Faster cavity machining and finishing
- Easier to modify when the design changes
Simplified, standardized mold design
Rapid tools are built around standard mold bases and standardized components, with simplified cooling and ejection layouts.
- Standard bases and components off the shelf
- Lower cavitation — often single or low-cavity
- Less design and detailing time before cutting steel
Tool making and molding under one roof
The tool is designed, machined, assembled and sampled by the same team that runs it. There is no hand-off, no re-quoting and no queue at a second supplier.
- DFM, tooling and sampling in one schedule
- Direct feedback loop between tool maker and process engineer
- Faster decisions when a modification is needed
Faster path to first samples (T0 → T1)
The goal of the first trial is not a perfect part — it is information. Getting to T1 sooner means you find the real molding issues earlier, when they are cheap to fix.
- T0 confirms the tool fills, opens and ejects
- T1 gives measurable sample parts for review
- Design and tool corrections happen in the same loop
Rapid injection molding vs production injection molding
Same process, different tooling strategy. The table below shows what actually changes when you choose a rapid tool.
| Factor | Rapid injection molding | Production injection molding |
|---|---|---|
| Purpose | Validate the design, then supply pilot / bridge / low-volume parts | Supply high-volume output at the lowest practical unit cost |
| Tooling material | Aluminum or pre-hardened / soft steel | Hardened tool steel |
| Mold design | Standard base, simplified cooling and ejection, minimal automation | Optimized cooling, hardened wear surfaces, automation and cycle-time driven |
| Cavitation | Typically single or low cavity count | Multi-cavity or family tooling sized to annual volume |
| Expected tool life | Lower than hardened tooling. Expected shot life is stated per tool, per resin and per geometry before you commit. | Designed and maintained for long production runs |
| Tooling lead time | Shorter — driven by machinability and simplified design | Longer — driven by hardening, detailing and validation |
| Unit cost | Higher per part at high volume; competitive at pilot and low-volume quantities | Lower per part once volume amortizes the tooling investment |
| Tolerance to design change | High — the tool is deliberately easy to modify or re-cut | Low — changes are expensive and slow once hardened |
| Resin choice | Same production resin where a grade is available | Production resin, validated for long-run processing |
| Typical next step | Validate geometry → build dedicated production tooling → transfer | Steady-state supply, tool maintenance and periodic re-qualification |
The honest trade-off: rapid tooling buys you time and design freedom, not durability or lowest unit cost. If your annual volume is high and your geometry is already stable, production tooling is usually the better economic answer — and we will tell you that rather than sell you a rapid tool you will outgrow.
When should you use rapid injection molding — and when not?
The fastest way to waste tooling budget is to build a mold at the wrong stage. Use this as the first check before requesting a quote.
Rapid tooling is usually the right choice when…
Choose another route when…
Not sure which route fits your program?
Send the CAD model and your target volume. We will tell you whether rapid tooling, production tooling, CNC machining or 3D printing is the better answer — including the cases where rapid tooling is not.
How our rapid injection molding process works
Eight steps from RFQ to low-volume output. The point of the sequence is to compress the loop between design and first real molded parts.
Quotation & DFM review
We review geometry, wall thickness, draft, ribs, gate and ejection options, and flag mouldability risks before any tooling is cut.
Tooling proposal
Tooling route, cavitation, gating, expected tool life and inspection scope are agreed and confirmed in writing.
Mold design
3D mold design for review, using standard bases and components to keep the build short.
Rapid tooling manufacture
CNC machining, EDM where required, fitting, assembly and bench testing — performed in-house.
T0 — first trial
The tool is mounted and run to confirm it fills, opens and ejects. This is a tool-function check, not a part approval.
T1 — first samples
Measurable sample parts are produced for dimensional, appearance and assembly review, with the inspection scope agreed at RFQ.
Adjustment & iteration
Based on your feedback we modify the tool, the process, or help you adjust the design — whichever actually solves the issue.
Pilot / bridge / low-volume output
Once samples are approved we run the agreed quantity, then support transfer to production tooling if volume grows.
T0 and T1 explained — the two milestones buyers actually wait for
First trial
The tool has been mounted and run for the first time. The objective is to confirm the tool functions.
- Cavity fills and packs
- Tool opens and part ejects
- Obvious defects identified (short shots, flash, sticking)
- Not a dimensional approval
First samples
Parts are produced under stabilized conditions and supplied to you for real evaluation.
- Dimensional inspection on agreed features
- Appearance and surface review
- Fit and assembly testing
- Functional testing in the production resin
Approval & output
After your approval, the agreed quantity is produced, or the validated geometry moves to production tooling.
- Tool modification where geometry allows
- Pilot or bridge run at agreed quantity
- Transfer to production tooling as volume grows
- Documentation scope as agreed at RFQ
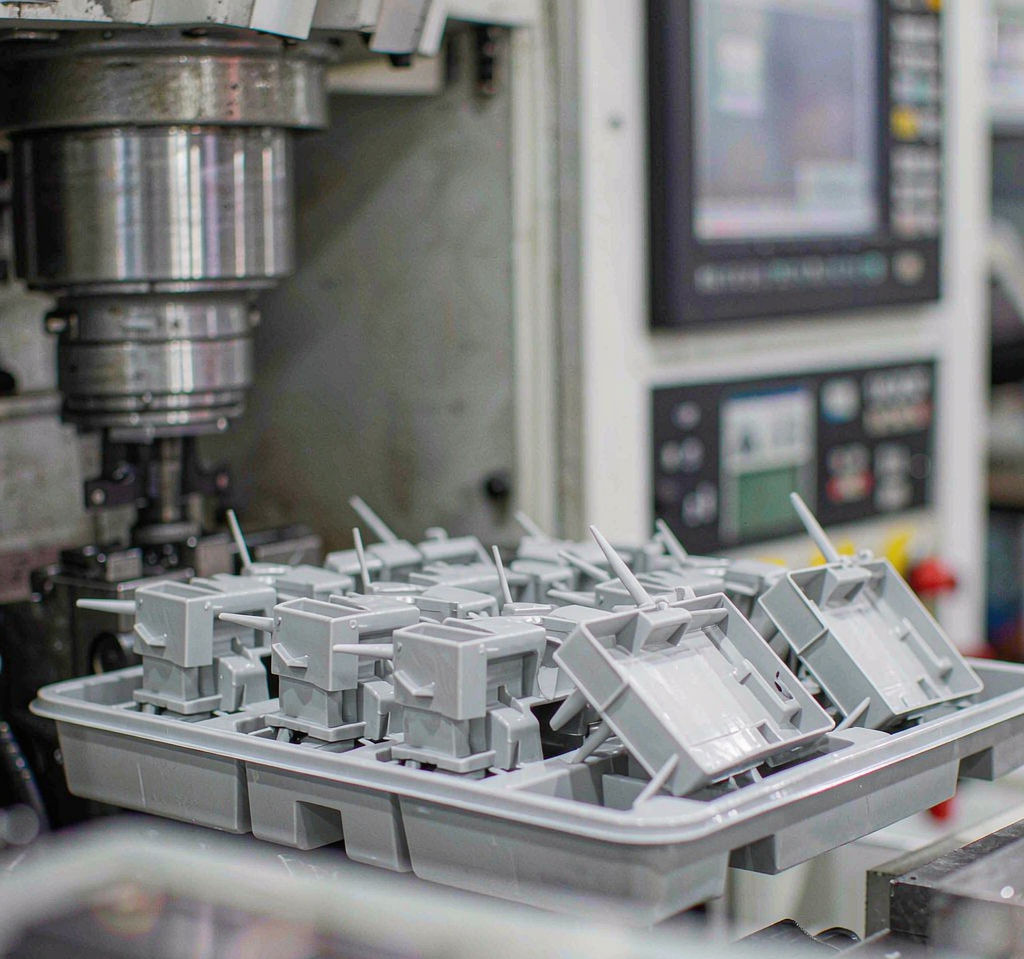
On schedules: tooling build time is driven by part geometry, cavitation, resin, gating and finishing requirements, so we quote the T1 date per project after DFM review rather than quoting a fixed number. For machining-only prototypes our quoted prototype lead time is typically 3–7 working days; rapid injection molding includes a tooling build and is therefore quoted on its own schedule.
Rapid tooling options
The tooling route is chosen from your volume, geometry and how much design change you still expect — not from a fixed menu.
| Option | Best for | Relative tooling cost | Relative lead time | Expected tool life | Notes |
|---|---|---|---|---|---|
| Aluminum rapid tool | Prototype, pilot and low-volume runs; fastest route to first samples | Lowest | Shortest | Lower than steel; stated per tool, per resin and per geometry | Machines quickly, easy to modify. Not suited to abrasive or glass-filled resins at long runs. |
| Pre-hardened steel tool | Bridge production and higher low-volume quantities | Medium | Short to medium | Longer than aluminum; no hardening cycle required | Better wear behaviour with filled resins and higher cavitation. |
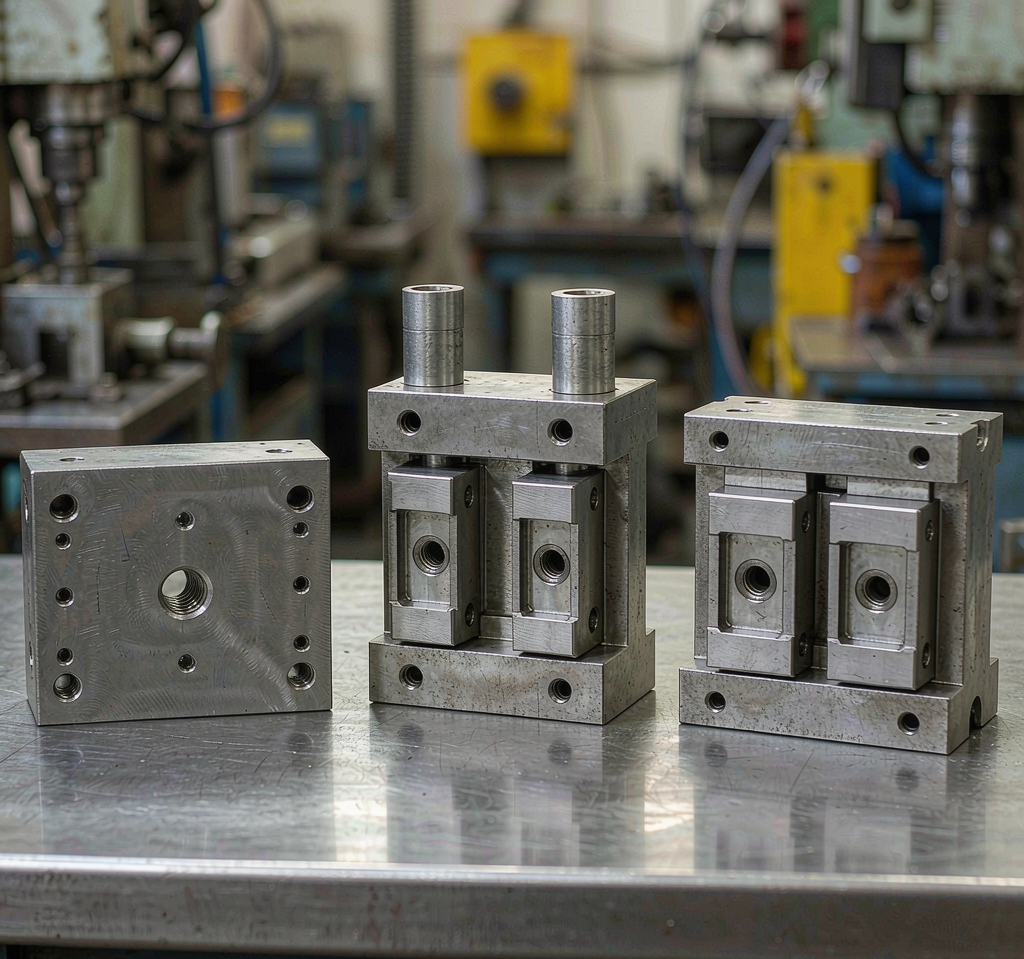
| Modular insert tooling (MUD) | Multiple part variants, families of small parts, repeat programs | Lower per variant | Short for subsequent variants | Insert-dependent | One standard master frame accepts interchangeable cavity inserts — good for design iterations. |
| Prototype / soft tooling | Very small sample batches and early feasibility checks | Lowest | Shortest | Limited — intended for sampling, not supply | Useful when the question is "will this part mold at all" rather than "supply me parts". |
| Production tooling (hardened steel) | Volume programs with a validated, stable design | Highest | Longest | Designed for long production runs | The destination after rapid tooling has de-risked the geometry. |
Materials for rapid injection molding
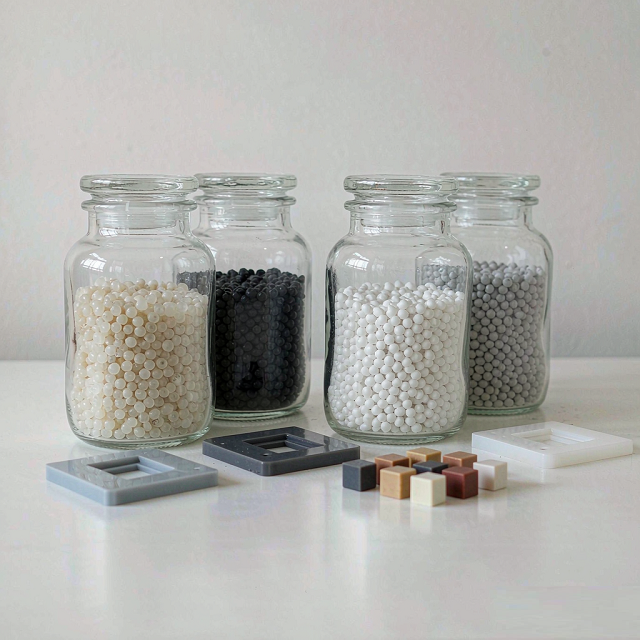
Running the production resin is usually the point of building a rapid tool. Availability of a specific grade is confirmed before the order — if a grade cannot be sourced, we tell you at quotation and propose the closest alternative.
| Material | Why it is chosen | Typical parts |
|---|---|---|
| ABS | Good balance of stiffness, impact and surface finish; easy to paint and plate | Housings, covers, consumer enclosures |
| PC (polycarbonate) | High impact strength and transparency; higher processing temperature | Light covers, transparent shields, protective housings |
| PC-ABS blend | Combines PC impact with ABS processability | Electronics housings, internal structural parts |
| PP (polypropylene) | Chemical resistance, low density, good fatigue behaviour for living hinges | Containers, clips, appliance components, hinge features |
| PA6 / PA66, glass-filled | High strength and wear resistance; moisture-sensitive, needs careful drying | Structural brackets, gears, under-hood-style parts |
| POM (acetal) | Dimensional stability, low friction, good fatigue resistance | Gears, bushings, precision mechanical parts |
| PMMA (acrylic) | Optical clarity and weatherability | Lenses, light guides, display windows |
| PBT, glass-filled | Electrical insulation, dimensional stability, heat resistance | Connectors, electrical housings |
| TPE / TPU | Soft-touch and flexible features; can be overmolded onto rigid substrates | Grips, seals, overmolded handles |
Resin and tooling interact. Glass-filled and highly abrasive resins accelerate wear on aluminum tools; hygroscopic resins such as PA require controlled drying. Both affect tooling route, achievable surface finish and tool life expectation — which is why resin is confirmed before the tooling route is fixed.
Rapid injection molding vs CNC machining vs 3D printing
Three different answers to three different questions. The right one depends on what you need the parts to prove and how many you need.
| Factor | Rapid injection molding | CNC machining | 3D printing |
|---|---|---|---|
| Best for | Production-representative molded parts at pilot / low volume | One-off precision parts, tight features, no tooling | Concept models, complex geometry, same-day iteration |
| Tooling required | Yes — rapid mold | No | No |
| Material authenticity | Production resin, molded by the production process | Production-grade stock material | Process-dependent; not equivalent to molded properties |
| Reveals molding issues (weld lines, sink, warpage) | Yes — this is the main reason to use it | No | No |
| Geometry freedom | Limited by draft, wall thickness and ejection | Limited by tool access | Highest |
| Consistency across units | High — one tool produces the run | High | Process-dependent |
| Cost at 1–5 parts | Highest — tooling dominates | Low to medium | Lowest |
| Cost at pilot / low volume | Competitive — tooling amortized across the run | Rising with quantity and cycle time | Rising with quantity |
| Speed to first part | Tooling build required | Fast | Fastest |
| Design change after first part | Tool modification or new insert required | Program change only | File change only |
| Path to production | Direct — validated geometry transfers to production tooling | Indirect | Indirect |
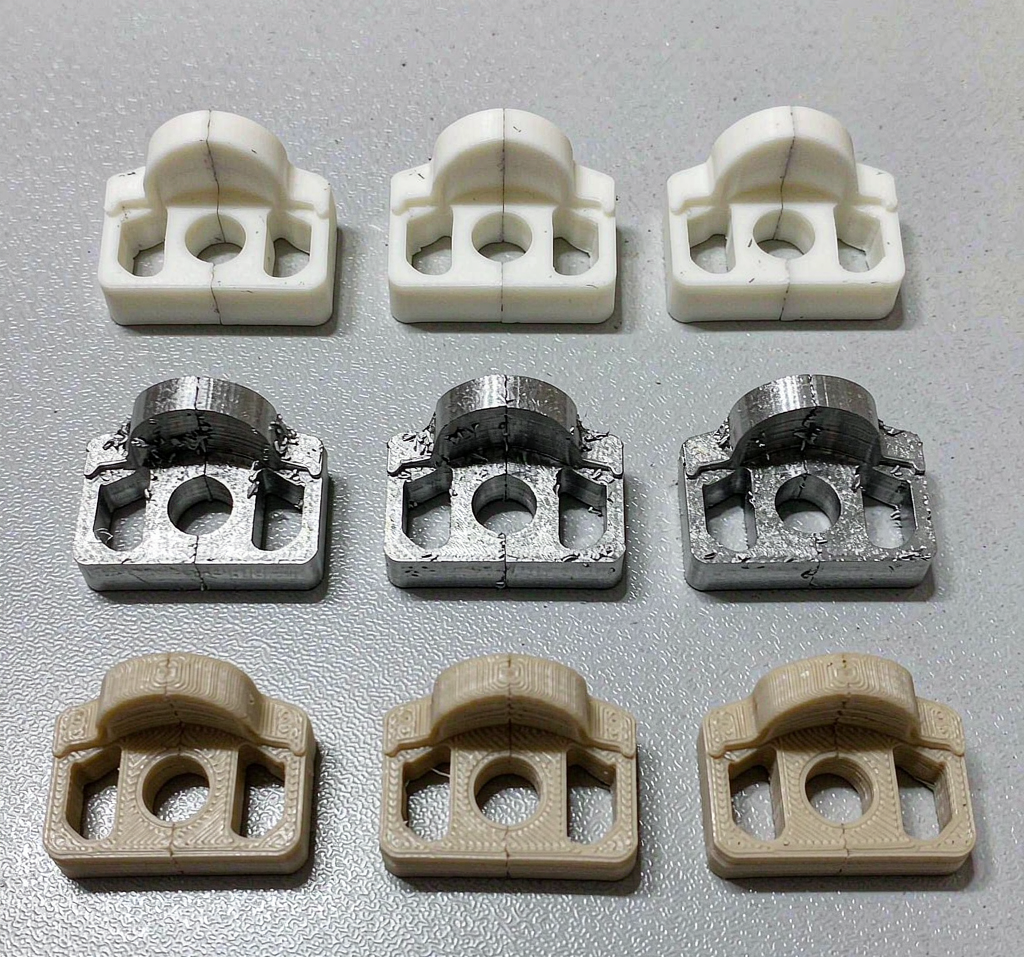
A common and effective sequence is: 3D printing or CNC machining to converge the concept, then rapid injection molding to validate the molded part, then production tooling once volume justifies it. If you are still deciding between machining and printing at prototype stage, see our CNC prototyping guide.
Typical applications for rapid molded parts
Representative part types we are asked to support with rapid tooling. Every program is quoted from your drawings, volumes and documentation requirements.
| Application | Typical parts | Why rapid tooling is used |
|---|---|---|
| Consumer electronics | Housings, bezels, covers, internal brackets, button panels | Appearance surfaces and snap-fit behaviour must be validated on real molded parts before tooling investment |
| Household appliances | Control panels, knobs, covers, latches, internal structural parts | Pilot builds for testing and certification samples ahead of production tooling |
| Automotive — interior & non-safety components | Trim clips, brackets, covers, connector housings | Pre-production validation and bridge supply during program ramp |
| Industrial equipment | Enclosures, guards, cable management parts, machine covers | Low-volume programs that never reach production-tooling volumes |
| Medical & laboratory — non-implantable | Device housings, instrument components, consumable parts | Documentation and process controls confirmed according to project requirements |
| Connectivity & electrical | Connector bodies, terminal blocks, insulating parts | Material and dimensional validation before committing to multi-cavity tooling |
Regulated applications: for medical, automotive safety or other regulated parts, the documentation package, material traceability and validation scope are agreed per project before tooling starts. Regulatory obligations such as device registration, biological evaluation, sterilisation validation and homologation remain with the product manufacturer — we supply the manufacturing capability and the documentation we can support.
Quality control for rapid molded parts
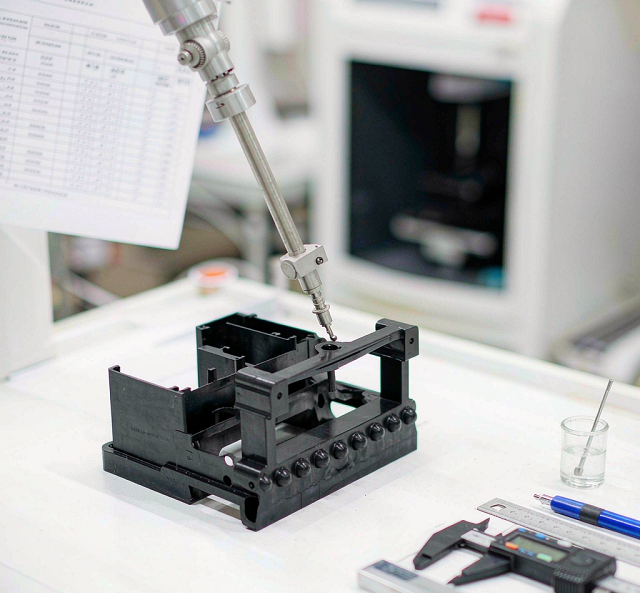
Inspection scope is agreed per project and stated in the quotation — we would rather define exactly what gets measured than claim everything is fully inspected.
| Stage | What is checked |
|---|---|
| Incoming material | Resin grade and batch identification; supplier certificate retained where provided |
| Tool qualification | T0 confirms fill, open and eject; tool function issues corrected before sampling |
| First article inspection | Dimensional inspection on the features agreed at RFQ; report supplied |
| In-process control | Process parameters recorded per run; appearance criteria checked against the agreed reference |
| Final inspection | Agreed sampling or feature-level inspection using CMM and calibrated 2D equipment |
| Records | Inspection results and process records retained per project for traceability |
What we do not claim: not every part receives full dimensional measurement on every feature, and inspection scope is not automatically identical across programs. If your program needs feature-level reports, capability data or PPAP-style documentation, specify the requirement at RFQ so it can be quoted and planned rather than assumed.
Why choose Goldcattle for rapid injection molding
Xiamen Goldcattle Plastic & Metal Products Co., Ltd. — an OEM/ODM custom manufacturer founded in 1998, serving customers in 100+ countries.
Have a part you need molded fast?
Send the 3D model and your target quantity. We will confirm the tooling route, the achievable tolerances and the T1 schedule per project.
Representative project: bridge tooling before production
A representative project type, described without client identification. Specific results are always project-specific.
Consumer device housing — pilot supply while production tooling was built
The value in this type of program is not tooling speed alone — it is that the weld line, sink and ejection problems were found on a rapid tool, where the fix is a re-cut and a modified model, rather than on hardened production tooling, where the same fix is expensive and slow.
Project descriptions are anonymized and representative. Tool life, tolerance outcomes, defect rates and schedules vary with part geometry, resin, tooling route, volume and inspection scope; we quote against your drawings rather than publishing representative values.
What to send for a rapid injection molding quote
The more of this you provide up front, the more accurate the tooling route, tolerance statement and T1 schedule will be.
Frequently asked questions
What is rapid injection molding?
Rapid injection molding is the production of real injection molded plastic parts using rapid tooling — typically aluminum or soft steel molds built with a simplified, standardized design — instead of full hardened production tooling. It delivers parts in the intended production resin and by the intended production process, at prototype, pilot, bridge and low-volume quantities.
How is rapid injection molding different from production injection molding?
The molding process is the same; the tooling strategy is different. Production tooling is hardened, multi-cavity and built for long tool life and lowest unit cost at high volume. Rapid tooling is softer, simpler and faster to build, which shortens time to first samples at the cost of shorter expected tool life and a higher unit cost at high volume.
How fast is rapid injection molding?
Tooling build time depends on part geometry, cavitation, resin, gating and finishing requirements, so the schedule is quoted per project after DFM review rather than quoted as a fixed number. The practical speed gain comes from building simpler tooling in-house and moving to first samples without a supplier hand-off between the tool shop and the molder.
How many parts should I order with rapid tooling?
Rapid tooling is normally chosen for prototype, pilot, bridge and low-volume quantities — from a handful of samples up to the point where hardened production tooling becomes the lower-cost option per part. We review your annual volume and expected growth, then tell you which tooling route makes more sense before you commit.
Can rapid tooling run the same resin I plan to use in production?
In most cases yes, which is one of the main reasons to choose rapid injection molding over a machined or printed prototype. Confirming the exact grade and any additive or colour requirement before tooling starts helps keep the prototype representative. If a specific grade is not available, we tell you before quoting and propose the closest alternative.
What tolerances can rapid injection molding hold?
Achievable tolerances depend on resin shrinkage behaviour, wall thickness, part geometry, gate and cooling layout, and the inspection method agreed for each feature. We state achievable tolerances per feature after DFM review. Where a feature is tighter than the molding process can reliably hold, we say so before tooling starts and propose a design change or a secondary operation.
Can a rapid tool be converted into production tooling?
Usually not by conversion — a rapid tool is designed for speed, not for long-run durability. The more useful path is to use rapid tooling to de-risk the design, then build dedicated production tooling from the validated geometry. Rapid tooling can also serve as a bridge while production tooling is being built.
What information do you need for a rapid injection molding quote?
A 3D CAD file in STEP, STP or IGES format, a 2D drawing showing tolerances and critical features, the required resin grade and colour, target quantity per order and per year, the surface finish requirement, any inspection or documentation requirement, and your target date for first samples.
Do you provide inspection reports?
Yes. Inspection scope is agreed per project and confirmed in the quotation. Typical output includes first article inspection on agreed features, dimensional reports measured by CMM or calibrated 2D equipment, and material documentation from the resin supplier where available. Not every part receives full dimensional inspection — the scope follows the features that matter for fit and function.
Can you mold medical or otherwise regulated parts?
We support plastic component manufacturing for medical and other regulated applications with process controls aligned to the project's documentation requirements. Regulatory obligations such as device classification, registration and listing, biological evaluation, sterilisation validation and technical documentation remain the responsibility of the device manufacturer, and the specific documentation package is confirmed per project.
What happens if I need design changes after T1 samples?
Design changes after first samples are expected and are the reason rapid tooling is worth building. Depending on the change, we modify the existing tool where the geometry allows — for example by re-machining a cavity or changing an insert — or we build a new cavity or tool if the change is structural. We explain the cost and schedule impact of each option before proceeding.
Is rapid injection molding cheaper than CNC machining or 3D printing?
It depends on quantity and on what you need the parts to prove. At very low quantities with no tooling, CNC machining or 3D printing is usually the lower-cost and faster route. Once you need production-representative parts in production resin at pilot or low-volume quantities, the tooling cost of rapid injection molding is spread across the run and the per-part cost typically becomes competitive.
Technical note: achievable tolerances, tool life, surface finish and schedules are part-specific and are confirmed after review of your geometry, resin, volume and inspection requirements. Nothing on this page should be read as a guaranteed process capability or a certification of conformity; those are stated in the quotation and inspection documentation agreed for your project.
Need injection-molded parts faster?
Send your CAD model and target quantity. We will confirm the tooling route, flag mouldability risks before steel is cut, and quote the T1 schedule for your part.
Accepted files: STEP · STP · IGES · DWG · PDF