Custom Silicone Injection Molding for Precision Silicone Parts
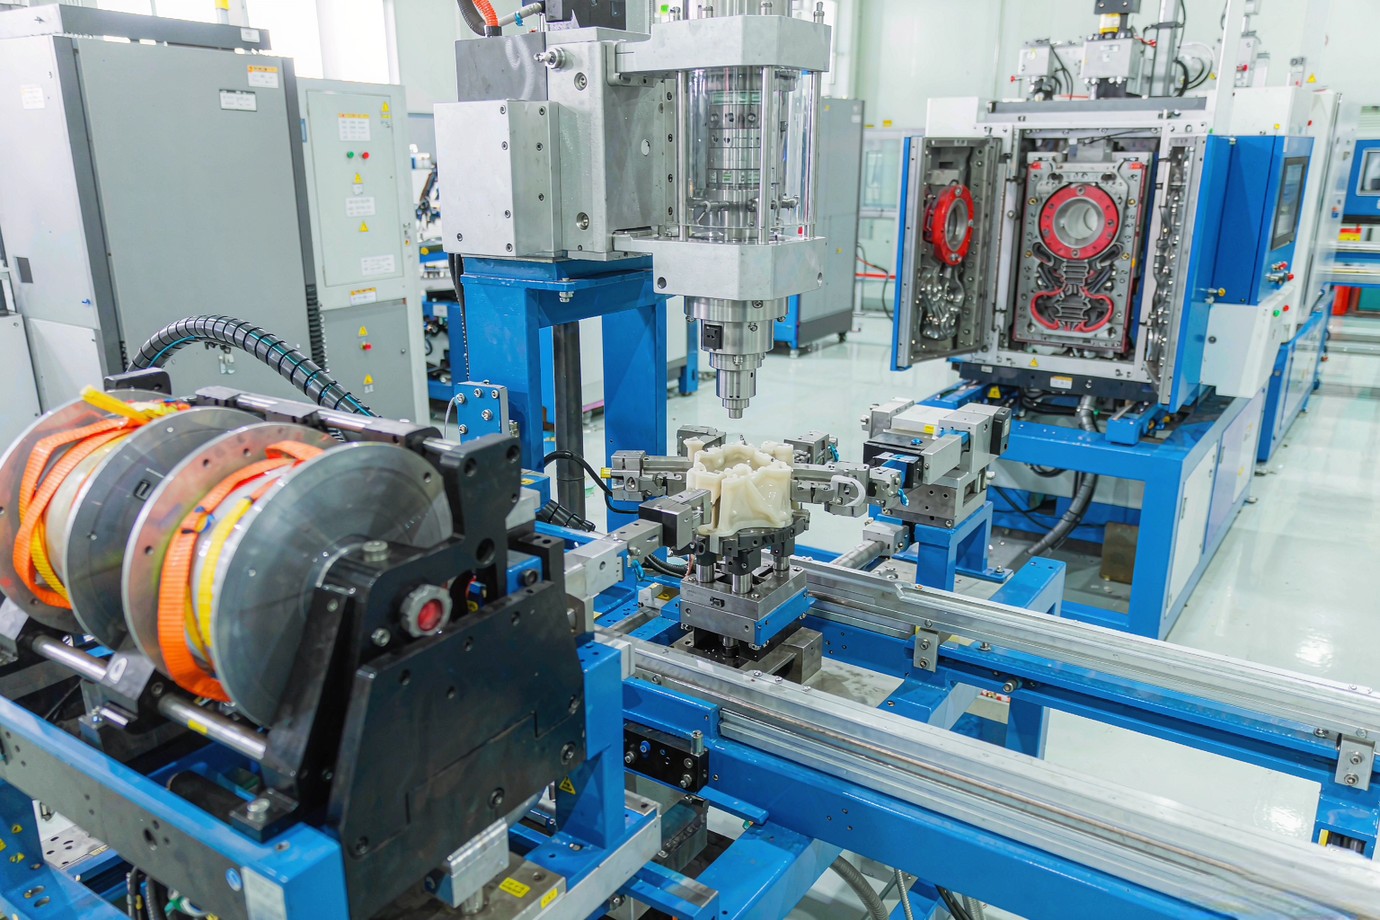
Build-to-print silicone parts from your drawing — LSR liquid injection, HCR/HTV compression, transfer and insert/overmolding. We run in-house LSR injection equipment and take the part from DFM review and tooling through mold trials to sampled production, with material verification and per-project compliance support.
At a Glance
If you need a precision silicone part, the practical path is to send the 2D/3D drawing, the silicone type or target (LSR or HCR, hardness, colour), the process preference if known, the estimated volume and the end-use. We review the part for moldability and for the risks specific to silicone — flash, venting, seal geometry and shrinkage — recommend the right process, plan or build the tool, run mold-trial samples to set the limit sample, then move to production. Material grade, compliance and achievable tolerance are confirmed per your project, not assumed.
Which Process Fits Your Part
Silicone is not one process. The four routes below cover most buyer needs; the right one is set by geometry, volume, tolerance and hardness, then confirmed on trial parts. We run all four in-house, including our own LSR liquid injection equipment.
| Process | Best for | What the buyer must confirm |
|---|---|---|
| LSR liquid injection | Complex, thin-wall, tight-tolerance, high-volume parts; consistent flash control via a heated mold | Two-part material spec, shot size, cure window, tool cost vs volume |
| HCR / HTV compression | Larger, simpler or lower-volume solid-silicone parts; lower tool cost | Part size and simplicity, hardness, volume that justifies the route |
| Transfer molding | Parts with inserts or where flash control matters at mid volume | Insert type, cavity count, flash acceptance |
| Insert / overmolding | Silicone bonded or locked onto plastic or metal; seals, grips, two-material parts | Substrate material, bond method (adhesion vs interlock), cure window |
Materials & Performance
We process VMQ, LSR, HCR/HTV, FVMQ and selected specialty grades. The table states the trade-off; the grade is specified per project from your application and any compliance need. For a decision-oriented reference across our molding materials, see our materials page.
| Grade | Property profile | Typical use |
|---|---|---|
| VMQ (methyl) | Wide temperature range, good general properties, translucent option | General seals, gaskets, insulation |
| LSR (liquid) | Flows for thin walls, consistent cure, high-volume capable | Precision, complex, flash-sensitive parts |
| HCR / HTV (solid) | Robust, lower tool cost, broad hardness range | Larger or lower-volume solid parts |
| FVMQ (fluoro) | Fluid and fuel resistance above standard VMQ | Automotive, fuel and chemical exposure |
| Specialty | Conductive, flame-retardant, high-tear or optically clear grades | Application-specific needs |
The properties buyers compare are hardness (Shore A), tensile strength, elongation, tear strength, compression set, temperature range, fluid resistance, UV and ozone resistance, and transparency. Typical reference values (per grade, confirmed per project, not assumed for every part): Shore A around 30 to 80; tensile strength commonly 6 to 11 MPa; elongation often 200 to 700 percent; tear strength about 10 to 40 kN/m; compression set typically 15 to 30 percent after 22 hours at 175°C; service temperature roughly -60 to +200°C depending on grade. We report against the maker's data sheet and the lot declaration rather than a generic figure.
Design for Molding (DFM)
Silicone behaves differently from rigid plastic, so the DFM review focuses on the failure modes that are specific to it. Each row below is an engineering decision we apply, not a marketing claim.
Wall Thickness
Keep walls uniform; abrupt changes cause fill and cure imbalance. Silicone flows well, but sharp thick-to-thin transitions are planned, not left to chance.
Parting Line
Low-viscosity silicone will flash at the parting line. Precision parting-line and vent design, plus controlled clamp and fill, keep flash within the agreed limit.
Gate & Vent
Vent placement and a fill profile that displaces air prevent bubbles and air traps — the most common cosmetic and sealing defects in silicone.
Undercuts
Undercuts are resolved with mold splits or post-machining; we flag them at DFM and propose the lower-cost route per part.
Insert & Substrate
For overmolding, the substrate, the bond method and the cure window are planned together so the two-material part holds in use.
Shrinkage
Silicone shrinks as it cures, typically about 1.5 to 4 percent; the mold is sized to the grade and the feature, and tolerance is confirmed per feature at trial.
Custom Parts We Manufacture
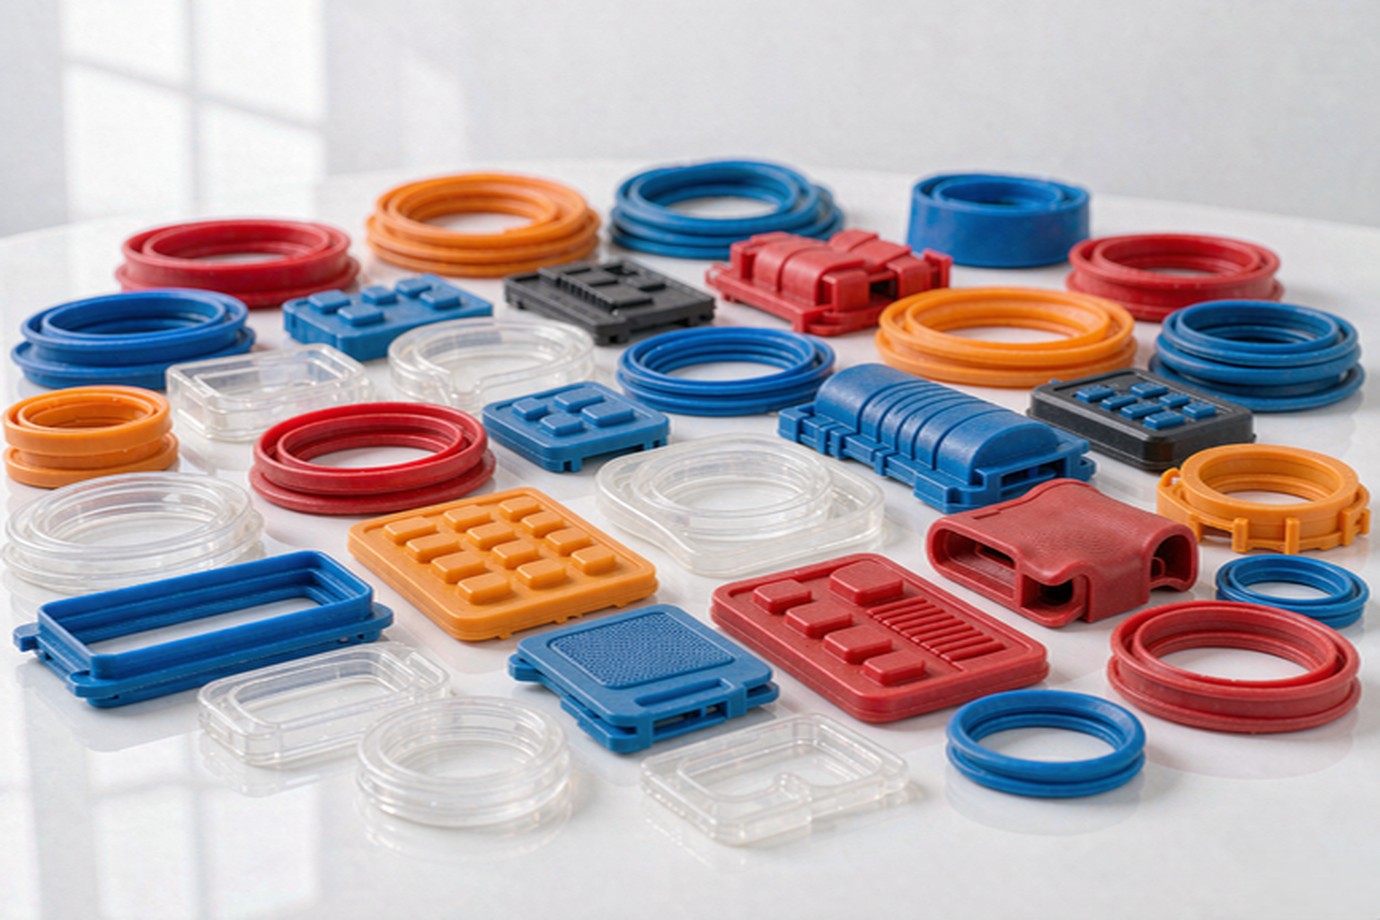
We quote and mold to your drawing rather than to a fixed catalogue. The categories below are how buyers usually specify a silicone part; each carries different hardness, tolerance and compliance needs that we confirm against the drawing.
Seals & Gaskets
O-rings, flat and formed gaskets where compression set and flash at the seal lip decide the performance.
Membranes & Diaphragms
Thin, consistent-cure silicon membranes for pressure and fluid devices.
Caps, Plugs & Connectors
Insulators, port seals and connector bodies with consistent wall and flash control.
Dampers & Mounts
Vibration and noise-control parts where elastic recovery is the function.
Buttons & Keypads
Soft-touch buttons and keypads with defined actuation feel and colour.
Overmolded Grips
Silicone over plastic or metal for grip, seal and comfort in one part.
Mold Development → Sampling → Production
The same flow applies whether the part is LSR or HCR. We treat mold trial as the moment the limit sample is set, not as a formality.
DFM & Quote
Receive 2D/3D drawing, grade or target, process preference, volume and end-use; flag moldability and silicone-specific risk.
Tool Build
Build the mold (LSR cold-runner design where used); verify parting line, vent and gate before trial.
Mold Trial
Run trial parts; check flash, bubbles, fill and hardness; set the approved limit sample.
Sample Approval
Submit samples with the material declaration; release to production after your acceptance.
Production
Run volume production to the approved material, process window and inspection plan, with records per project.
Quality Control & Testing
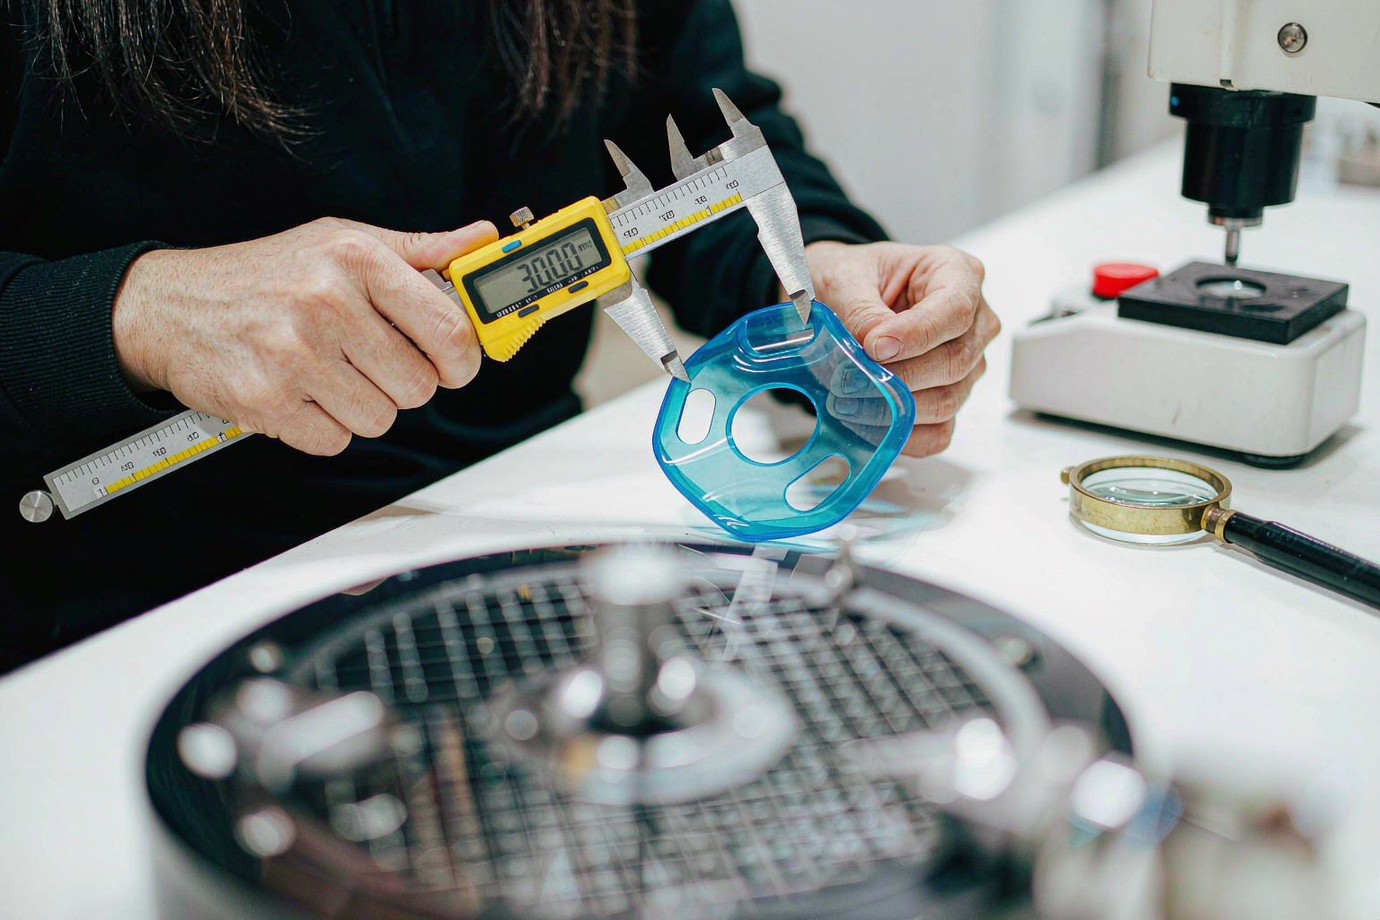
Silicone defects are specific, so the inspection plan is specific. The four below are the ones we design and process against at mold trial and hold in production.
We verify material per lot against the maker's declaration and data sheet, check hardness with a Shore A durometer, confirm dimensions against the drawing and the approved limit sample, and run compression-set and visual inspection where the application calls for it. Higher-precision features are checked on a CMM as needed, and records are supplied with the shipment on request. For the broader injection scope and tooling, see our injection molding services page.
Industries & Applications
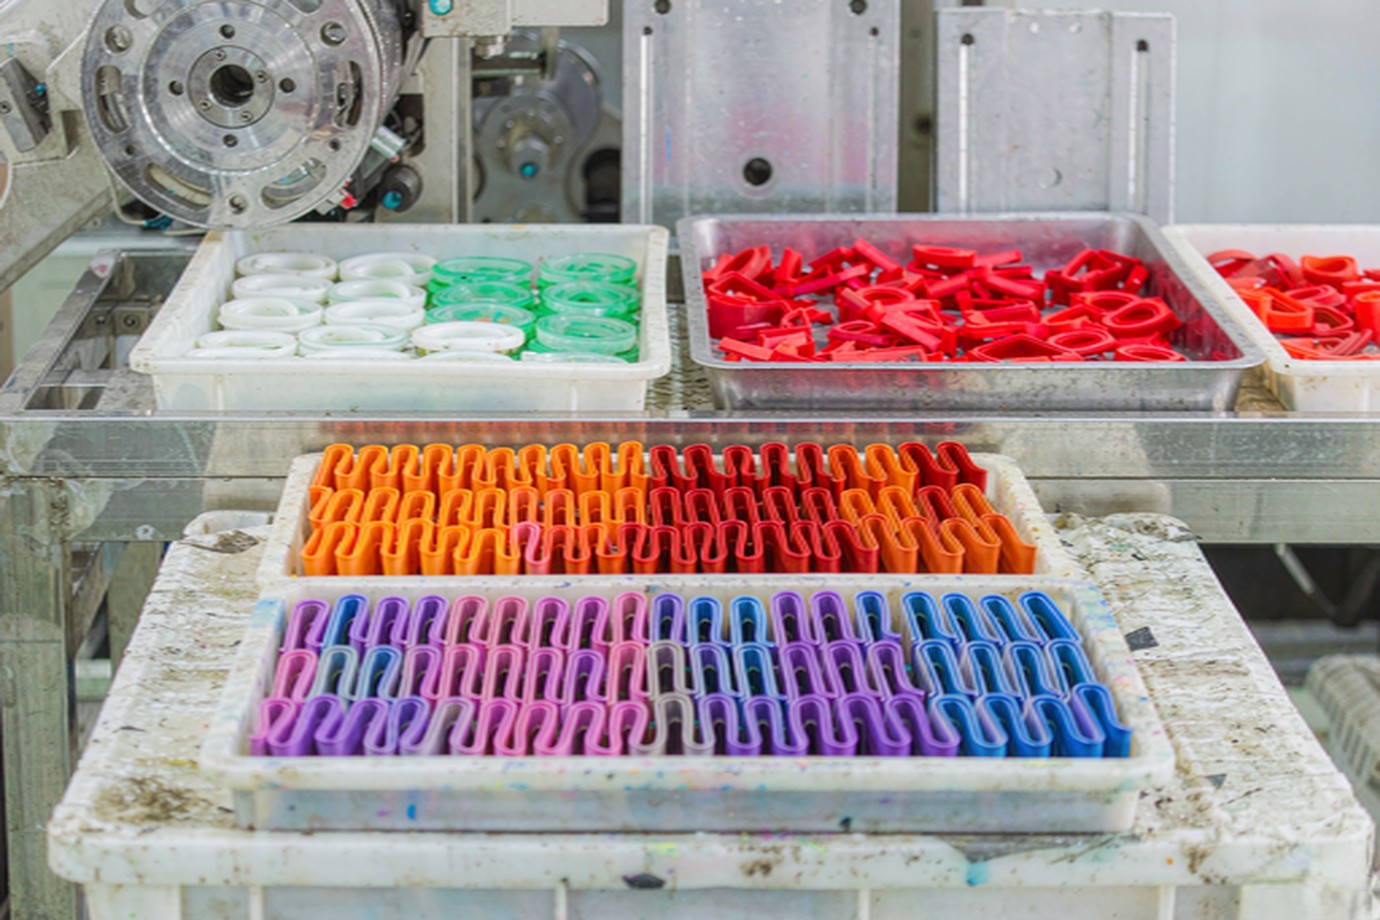
The same molding discipline serves different product lines; the grade and the compliance evidence differ by where the part lives. We state which grade and which documents apply to your part, rather than claiming all parts comply.
Medical & Healthcare
ISO 13485-aligned process; biocompatibility testing per ISO 10993 supported on the chosen grade, per project and per customer specification.
Food & Beverage
Food-contact suitability confirmed per project against FDA 21 CFR 177.2600 or EU 1935/2004 with material declaration and test reports.
Automotive
IATF 16949 supported as a system requirement; fluid- and temperature-resistant grades for seals and dampers.
Electronics
Insulators, keypads, connectors and sealed enclosures where elastic recovery and colour matter.
Cost & Lead Time
For EU and US buyers the real questions on a silicone part are tool cost versus volume, the grade and its documents, and the inspection plan — not a wall of certificate names. We state which apply to your part.
Tooling Trade-off
An LSR tool costs more upfront but pays back at volume and gives flash control; HCR compression costs less for lower volumes. The break-even is confirmed per project.
Lead Time
Prototype about 3 to 7 working days; production about 15 to 25 working days after tooling is approved. Confirmed at quotation.
Minimum Order
Prototype and trial volumes can start from 1 piece after the tool is planned; production unit cost is quoted per project.
Material & Inspection
Maker, grade, data sheet and lot declaration supplied per project; inspection records on request.
Case Study, RFQ & FAQ
Representative project — sealed LSR component
A two-material sealed part needed a soft LSR layer over a rigid substrate, with flash controlled at the seal lip and repeatable compression-set performance across lots.
- ApproachDFM of the seal lip and gate/vent layout; in-house LSR tool with cold-runner design; mold trial to set the limit sample; compression-set and visual plan per lot.
- OutcomeFlash held to the agreed acceptance; lot-to-lot hardness and dimension stable against the limit sample; part moved into sampled production.
This is a representative composite of project types we support, written without a named customer or fabricated measurements — specific results and references are shared under NDA.
What to send for a silicone quote
Required fields let us scope the project; optional fields sharpen the estimate.
Note: drawings are handled under NDA on request. We respond with a moldability and silicone-risk review and a project-specific quotation — not a generic price list. You can also open our injection molding quote page.
FAQ
What is the difference between LSR injection molding and HCR/HTV compression molding?
Can you mold silicone over plastic or metal (overmolding / insert molding)?
What silicone materials do you process?
What hardness and dimensional tolerance can silicone parts achieve?
Are your silicone parts suitable for food or medical contact?
How do you control flash, bubbles and short shots in silicone molding?
What are typical lead times and minimum order quantities?
What information should I send for a silicone molding quote?
Do you handle two-shot and insert molding with metal or plastic substrates?
How is silicone material and part quality verified?
Ready to review your silicone part project?
Send the drawing, the silicone type or target, and the end-use. We will return a moldability and silicone-risk review and a tooling-and-unit-cost estimate scoped to your part — not a one-size-fits-all number.
Request a Silicone Quote Explore all injection molding servicesXiamen Goldcattle Plastic & Metal Products Co., Ltd. — Founded in 1998 · ISO 9001:2015 certified · OEM/ODM build-to-print.