What Are CNC-Turned Parts? A Guide to Types, Materials & Applications
CNC-turned parts are components shaped by rotating a workpiece while a tool removes material. This guide explains which parts suit turning, how materials and features affect manufacturability, and what to specify when you source turned components.
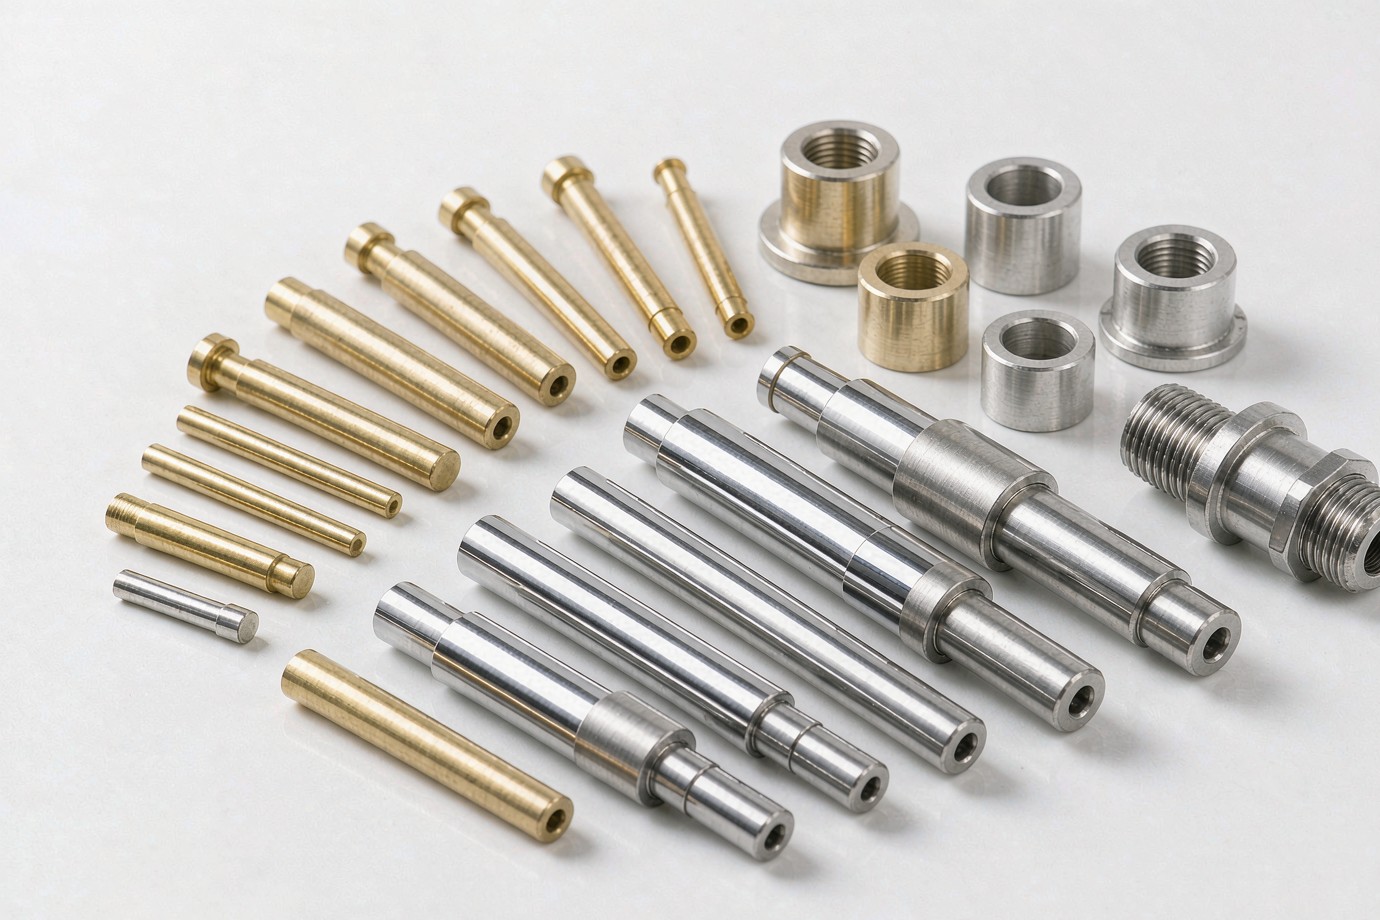
CNC-turned parts are components made by rotating a workpiece while a cutting tool removes material under computer numerical control. The process suits parts with rotational geometry — shafts, pins, bushings, sleeves, spacers, threaded components and cylindrical housings. A lathe with live tooling can also add selected milled features such as flats, slots and cross-holes. The right route depends on the part's geometry, material, dimensional needs, quantity and inspection requirements.
What Are CNC-Turned Parts?
CNC turning produces parts by holding a workpiece in a chuck or collet and spinning it on its axis while a single-point cutting tool feeds along the surface to remove material. Because the cut happens around a central axis, the process naturally creates round, axially symmetric features: outside diameters, bores, tapers, grooves, chamfers and threads.
What distinguishes a turned part from a part made by another method is its geometry. If the dominant shape is rotation about an axis, turning is usually the most direct way to make it. If the dominant shape is a flat plate with pockets or a contoured 3D body, milling is usually a better fit. Many production parts combine both, which is where turn-mill machines earn their place.
How CNC Turning Works
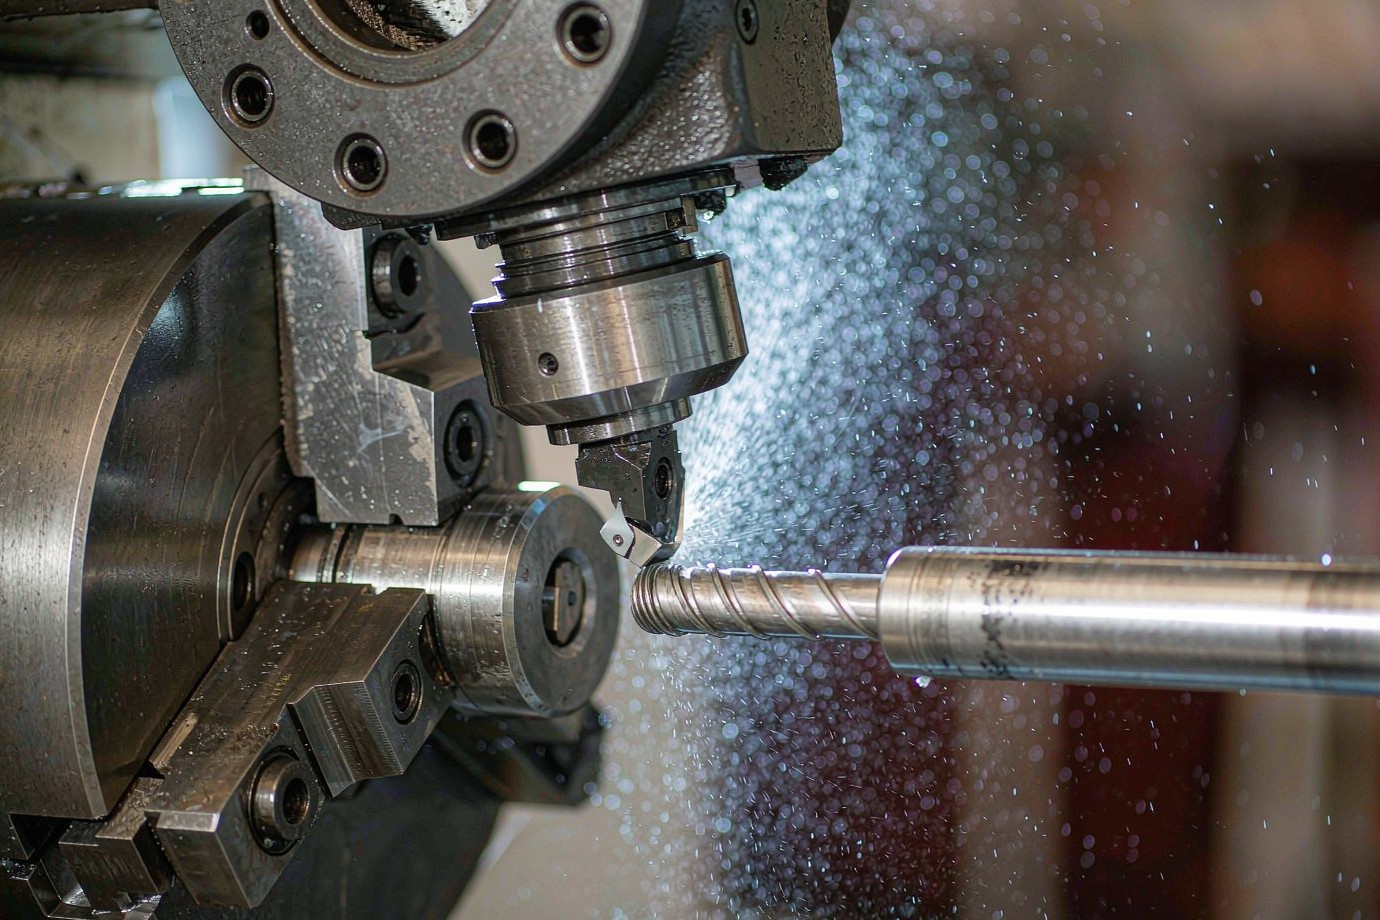
A turning cycle follows a consistent sequence: the bar or blank is clamped and aligned, the control executes the programmed tool path, the tool removes material to the target diameters and features, and the finished part is verified against the drawing. The diagram below shows the basic arrangement.
Common Types of CNC-Turned Parts
Buyers rarely search for "turning" first; they search for the part they need. The table groups the categories that are most often produced by turning and the features that matter for each.
| Part type | Typical features | What to define |
|---|---|---|
| Shafts / spindles | Diameter steps, shoulders, journals, grooves | Diameter, roundness, runout, concentricity |
| Pins / spacers | Cylindrical form, length, end faces | OD, tolerance, length, face quality |
| Bushings / sleeves | OD and bore, step or groove | OD-to-bore relation, concentricity, fit |
| Threaded components | External / internal thread, shoulder | Thread standard, pitch, class, effective length |
| Connectors / fittings | Rotationally symmetric body, holes, grooves | Sealing face, thread, assembly features |
| Rollers / housings | Long cylinder, bore and OD | Length, diameter, surface finish, wall |
Scope note: these are typical part categories, not a claim that every listed product has been produced. Confirm specific capability with the supplier against your drawing.
CNC Turning vs CNC Milling
The practical question is not "which process is better" but "which one matches the geometry." Use the table as a first-pass filter; a turn-mill machine covers parts that sit between the two.
| Condition | Usually the better route |
|---|---|
| Primary geometry rotates around a central axis | CNC turning |
| OD, bore and cylindrical profile are the main features | CNC turning |
| Pockets, flat faces and side features dominate | CNC milling |
| Cylindrical body plus flats, slots or cross-holes | Turning with live tooling or turn-mill |
| Very small, slender part needing guide support | Evaluate Swiss-type turning where available |
| Simple standard shape at very high volume | Also evaluate dedicated or forming routes |
For general CNC background, see the introduction to CNC and the CNC machining services overview.
Materials Used for CNC Turning
Most engineering metals and many plastics can be turned. The selection is a trade-off between function, machinability, corrosion resistance and cost — not a matter of listing material names. The table frames the decision.
| Material family | What to weigh when choosing |
|---|---|
| Aluminum alloys | Weight, machinability, temper, finish and cost |
| Brass / copper alloys | Conductivity, composition, machinability, end use |
| Stainless steel | Grade, corrosion need, work hardening, surface |
| Carbon / alloy steel | Strength, hardness, heat treatment, wear route |
| Titanium | Strength-to-weight, corrosion, heat, tool wear, cost |
| Engineering plastics | Cutting deflection, thermal growth, moisture, stability |
For grade-level detail and stock options, see the materials hub.
Features That Affect Manufacturability
Geometry drives the manufacturing plan more than the machine brand. The diagram marks the features a reviewer looks at on a turned shaft.
- Outside diameter and length set the stock size and how the bar is supported.
- Bore and hole depth affect tool rigidity; deep holes need careful planning.
- Length-to-diameter ratio influences deflection and whether steady rests or guide bushings are needed.
- Grooves, threads and cross-holes add operations and tool access considerations.
- Thin walls can deflect under the cut and need gentler parameters.
Tolerances & Surface Finish
A tolerance is only meaningful when tied to a feature. Specifying one blanket tolerance for an entire part can push cost up without improving function. Define the tight numbers where the part actually contacts, seals or locates, and relax them elsewhere.
- Diameter — nominal size, tolerance and where it is measured.
- Roundness — form of a single cross-section where sealing or bearing fit matters.
- Runout / concentricity — relationship of features to a datum axis; state the datum.
- Bores — inside diameter, depth and positional relation to the OD.
- Threads — standard, class and effective length, plus inspection method.
- Surface finish — Ra value and its location, since finish varies along the part.
These are the items a supplier quotes and inspects against. The achievable values depend on the feature, material, setup and measurement method — they should be confirmed per project rather than assumed as a universal figure.
When CNC Turning Is the Right Choice
Turning is the natural choice when the part's identity is rotational: a shaft that transmits motion, a bushing that locates a pin, a spacer that sets a gap, or a fitting that seals a connection. It is not the best route when flat patterns, deep pockets or freeform contours dominate — those belong to milling, and combined geometries belong to turn-mill.
A useful test: if you can describe the part mostly by diameters, lengths and a center axis, turning leads. If you describe it by faces, cavities and contours, milling leads. When both descriptions fit, ask the supplier about a turn-mill strategy that reduces handling and setups.
What Affects the Cost of CNC-Turned Parts?
Cost is an outcome of the specification, not a single rate. The factors buyers can influence:
- Material grade and the stock size it is cut from
- Part diameter and length
- Geometry complexity and number of operations
- Deep bores and slender features needing support
- Threads, grooves and cross-holes
- Tolerances and the inspection they require
- Surface finishing and secondary operations
- Quantity and the repeat-order profile
Buying tip: the lowest unit price is not necessarily the lowest total procurement cost. Material certification, critical-feature inspection, finishing, packaging and repeat-order consistency should be compared under the same specification.
Quality Inspection
Inspection follows the features you defined. What gets checked depends on the drawing, not on a generic "precision" claim.
| Inspection object | What the buyer should specify |
|---|---|
| Diameter | Nominal size, tolerance, measurement location |
| Length / shoulder | Total length, step length, face position |
| Roundness | Applicable location and allowed value |
| Runout / concentricity | Datum, method and functional need |
| Bores | ID, depth, relation to OD, surface state |
| Threads | Standard, class, effective length, check method |
| Surface finish | Ra, location, post-processing state |
| Material | Grade, condition, certificate requirement |
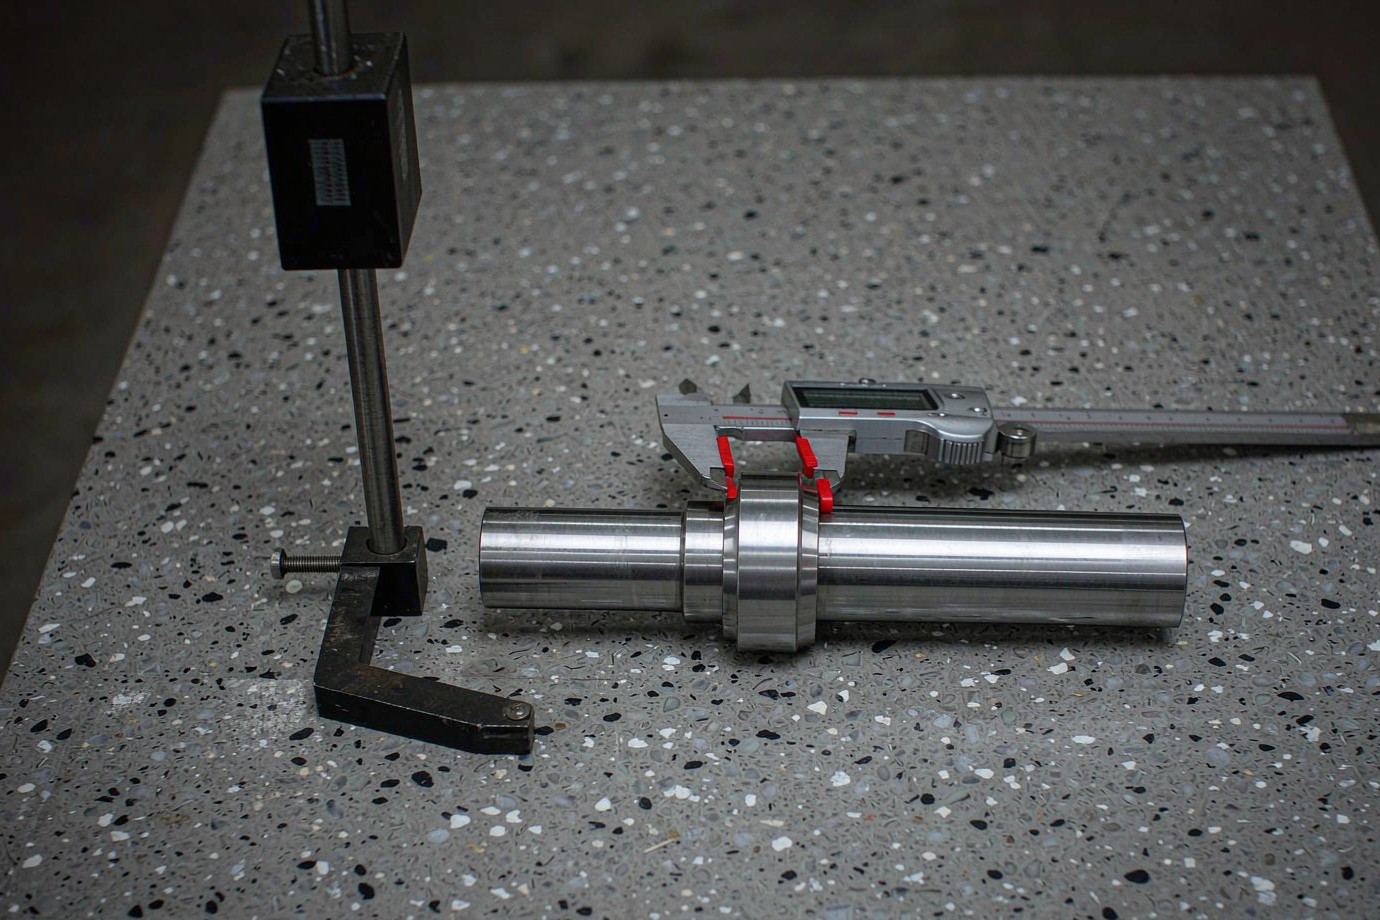
What Information Should You Send for CNC Turning?
A model alone rarely carries the full requirement. Send enough that the supplier can plan the route and quote like-for-like:
- 3D CAD model and 2D engineering drawing
- Material grade and condition
- Critical diameters and lengths
- GD&T and datum requirements where applicable
- Thread specification
- Surface roughness and finish requirements
- Prototype quantity and production forecast
- Material certificates or inspection reports required
- Packaging, marking and destination
For turned parts especially, do not send only a STEP file without marking the functional diameters, datum, thread standard and key dimensions. The model shows geometry; it does not always state material, final tolerance, finish or inspection.
When your specification is ready, you can start a quote through the online CNC quote or the project form.
Goldcattle CNC Turning Services
Xiamen Goldcattle Plastic & Metal Products Co., Ltd. (Founded in 1998) performs CNC turning as part of its six in-house core processes — CNC machining, injection molding, mold making, 3D printing, die casting and sheet metal fabrication — under one ISO 9001:2015 quality system. For verified turning capabilities, machine configuration, quality documentation and pricing, see the dedicated CNC turning services page.
Discuss Your Custom Turning Project
Send your drawing and requirements. Our engineering team will review geometry, materials and critical features, then propose a turning route and a like-for-like quote.
Discuss Your Custom Turning Project Review full turning capabilities