Custom ABS Parts · OEM / ODM
Custom ABS Plastic Parts Manufacturing
One supplier from grade selection to finished ABS components — CNC machined, injection molded and 3D printed parts built to your drawing, with DFM feedback and a quote returned within 24 hours.
- Send CAD / drawing / sample
- CNC · Injection molding · Prototyping
- MOQ 1 piece
ISO 9001:2015 certified Founded in 1998 100+ machines across six processes
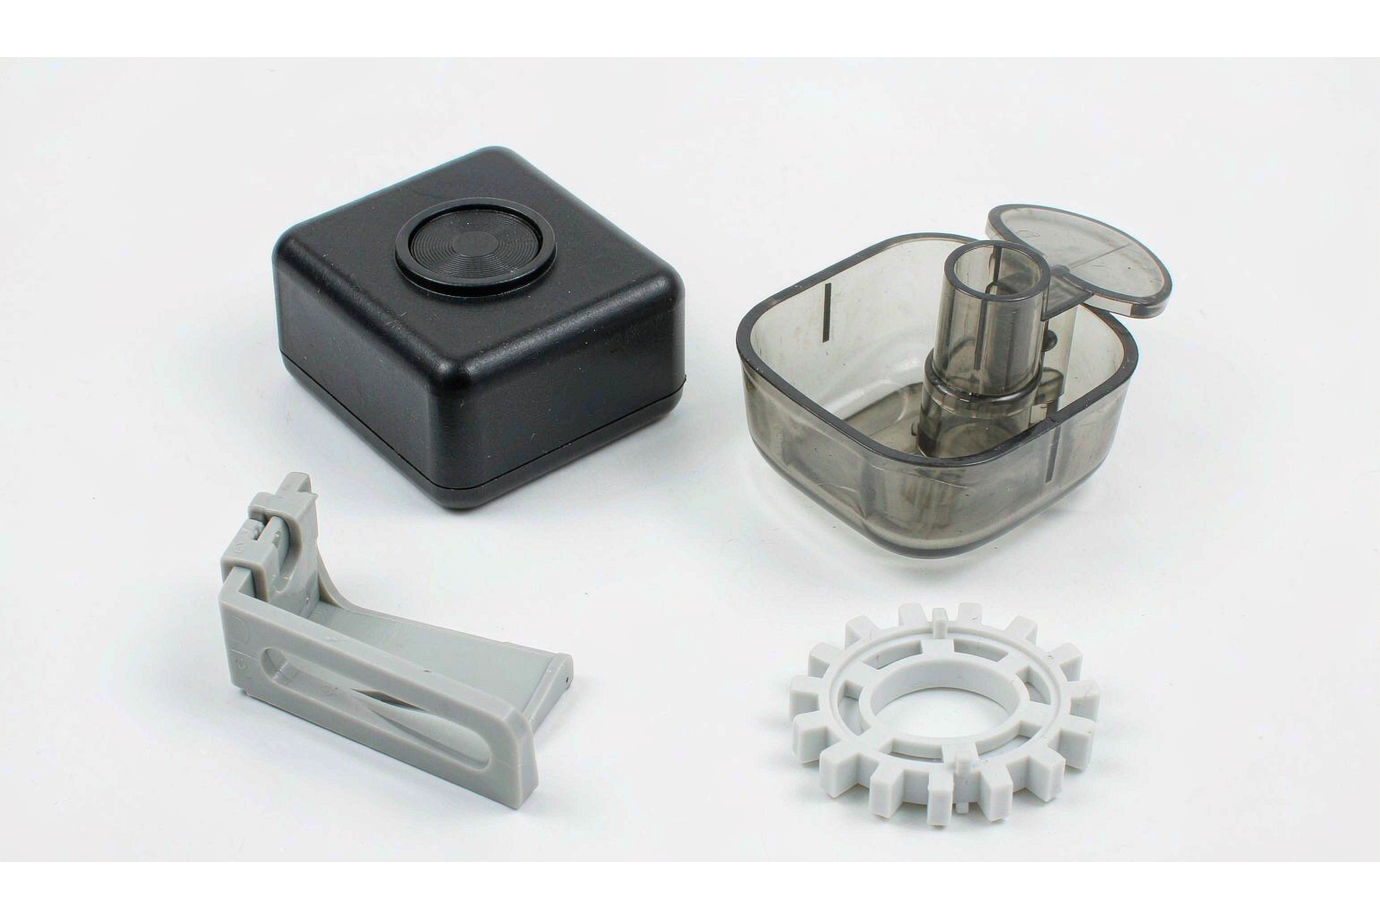 Made to drawing
01 — What We Make
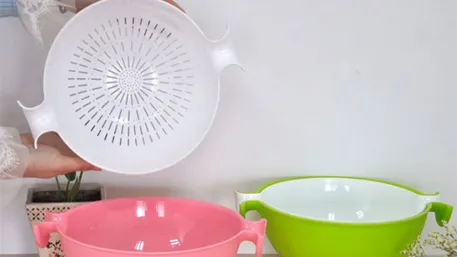
ABS parts we build for equipment, appliance and automotive buyers
If it is a custom ABS component defined by a drawing, it is on this list.
Housings & enclosures
Electronic and appliance bodies with snap-fit lids, boss patterns and connector cutouts.
Covers & panels
Cosmetic faces in textured, painted or high-gloss finish to your surface spec.
Brackets & clips
Mounting features machined from plate or molded with snap and retention geometry.
Gears & rollers
Tooth forms CNC cut or injection molded; sliding duty referred to POM options.
Knobs & handles
Tactile consumer parts with defined torque feel, finish and color standard.
Trim & fascia
Automotive and appliance interior parts where cosmetics and fit are the spec.
Prototype & pilot parts
Form and fit validation from 1 piece before any tooling commitment.
Sub-assemblies
ABS parts fitted with metal inserts or fasteners, delivered ready for your line.
02 — Why ABS
Where ABS earns its place in a bill of materials
Impact resistance
Absorbs knocks and drops without the brittle failure typical of standard styrenics — the reason it dominates consumer and appliance housings.
Stiffness & stability
Holds shape in thin walls and flat panels, keeping gaps and alignments consistent across a production run.
Cosmetic surface quality
Takes texture, paint and plating exceptionally well, so one resin covers both structural and visible-face duties.
Cost-performance
Mid-range resin price with a wide processing window — forgiving in molding and economical in volume.
Machinability
Cuts cleanly for prototypes and low volumes, letting you validate a design before tooling money is spent.
03 — Grade Selection
Which ABS grade does your part actually need?
"ABS" is a family, not one material. We machine and mold the grade named on your drawing — or help you pick one if the drawing only states performance targets.
General-purpose ABS
Indoor housingsThe default choice for housings, covers and everyday consumer parts where cost and cosmetics lead.
High-impact ABS
Tough dutyFor parts that get dropped, clipped or flexed in service — tool cases, brackets, equipment shells.
Flame-retardant ABS
UL 94 where specifiedElectrical and electronic enclosures where the customer drawing specifies a flame rating for the grade.
High-heat ABS
Warm zonesHigher heat deflection for parts mounted near lamps, power supplies or warm appliance zones.
Plating-grade ABS
Chrome-look partsChemistry tuned for electroplating — decorative knobs, trim and badges with a metal finish.
ABS / PC blend
Step-up optionWhen the part needs more heat and impact than standard ABS — see the comparison below.
Final grade selection is confirmed against the resin datasheet and your application. Property phrases above are qualitative selection guidance, not certified values.
04 — Material Comparison
ABS vs PC/ABS vs ASA vs POM
| Property | ABS | PC/ABS blend | ASA | POM (acetal) |
|---|---|---|---|---|
| Impact toughness | Good | Better | Good | Moderate |
| Heat resistance | Moderate | Higher | Higher | Moderate |
| Outdoor / UV | Limited | Limited | Excellent | Limited |
| Cosmetic finishing | Excellent | Very good | Very good | Good |
| Typical processes | CNC · molding · 3D print | Molding · CNC | Molding | CNC · molding |
| Best for | Indoor housings, trim, covers | Tougher enclosures, warm zones | Outdoor-facing parts | Gears and sliding features (custom acetal parts) |
Comparing ABS with nylon (PA) or other engineering resins? Our materials hub maps the full range we process, and every quote states the exact grade involved.
05 — Honest Limits
When standard ABS is the wrong material
A supplier who flags this before tooling saves you the mold. Four situations where we will steer you away from standard ABS:
L-01Sustained outdoor UV
ABS weathers and fades under long-term sunlight. Move to ASA, a UV-stabilized grade, or a protective coating.
L-02Continuous high heat
Above ABS's heat-deflection range the part can distort in service. Step up to high-heat ABS or a PC/ABS blend.
L-03Heavy wear and friction
ABS surfaces abrade under sliding duty. POM or internally lubricated grades hold up far longer.
L-04Strong chemical exposure
Solvents and some cleaners attack ABS. Chemical compatibility must be verified against your actual environment.
06 — Process Selection
Three ways to make the same ABS part — which fits your volume?
CNC machining
Best for: prototypes · low volume · tight features
- No tooling, start from plate or block
- Ideal for pilots and engineering validation
- Holds the tightest feature tolerances
Injection molding
Best for: volume production · repeatable cosmetics
- Lowest piece cost at volume
- Consistent texture and color part to part
- Tooling planned around shrinkage and gates
3D printing
Best for: fastest form / fit checks
- Days-fast iteration on early geometry
- ABS and ABS-like materials
- Bridge to CNC or molded pilots
07 — CNC Machined ABS
CNC machined ABS: precision without a mold
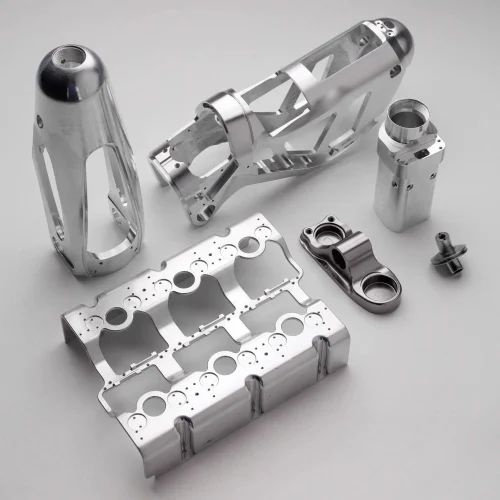
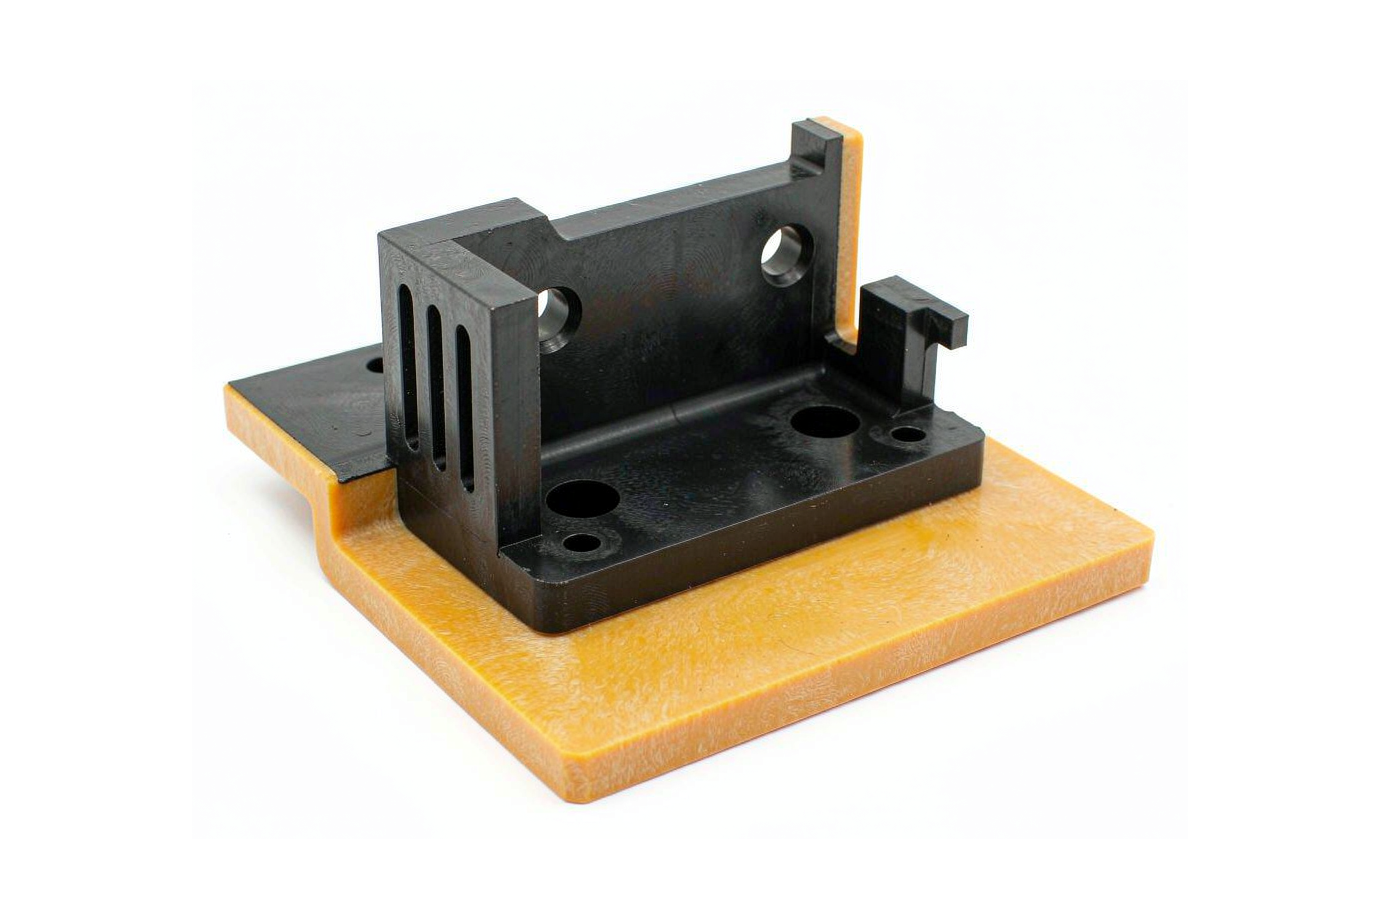
Machining is the fastest route from drawing to a real ABS part. We machine ABS plate and block on 3/4/5-axis centers with sharp, positive-rake tooling and controlled heat input — the two details that separate a clean ABS edge from a melted or stressed one.
- Typical CNC tolerance ±0.01 mm; qualified features ±0.005 mm where geometry allows and material stability is reviewed
- Stress relief / annealing applied where flatness or later use demands it
- Threads, inserts and snap features machined directly for pilot builds
08 — ABS Injection Molding
The volume route, planned around ABS shrinkage
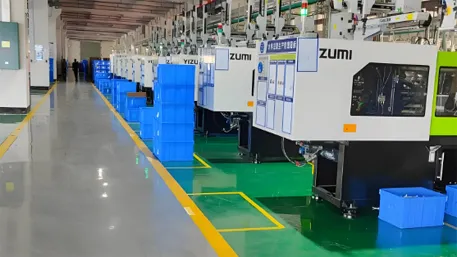
For production volumes, molding is where ABS economics win. Tooling, shrinkage, gate position and parting line decide both the cosmetic result and the dimensional consistency — so those decisions are made in DFM with you, not on the mold floor afterwards.
Our dedicated page covers molding-specific design rules, tooling options and the handover from prototype to production tool.
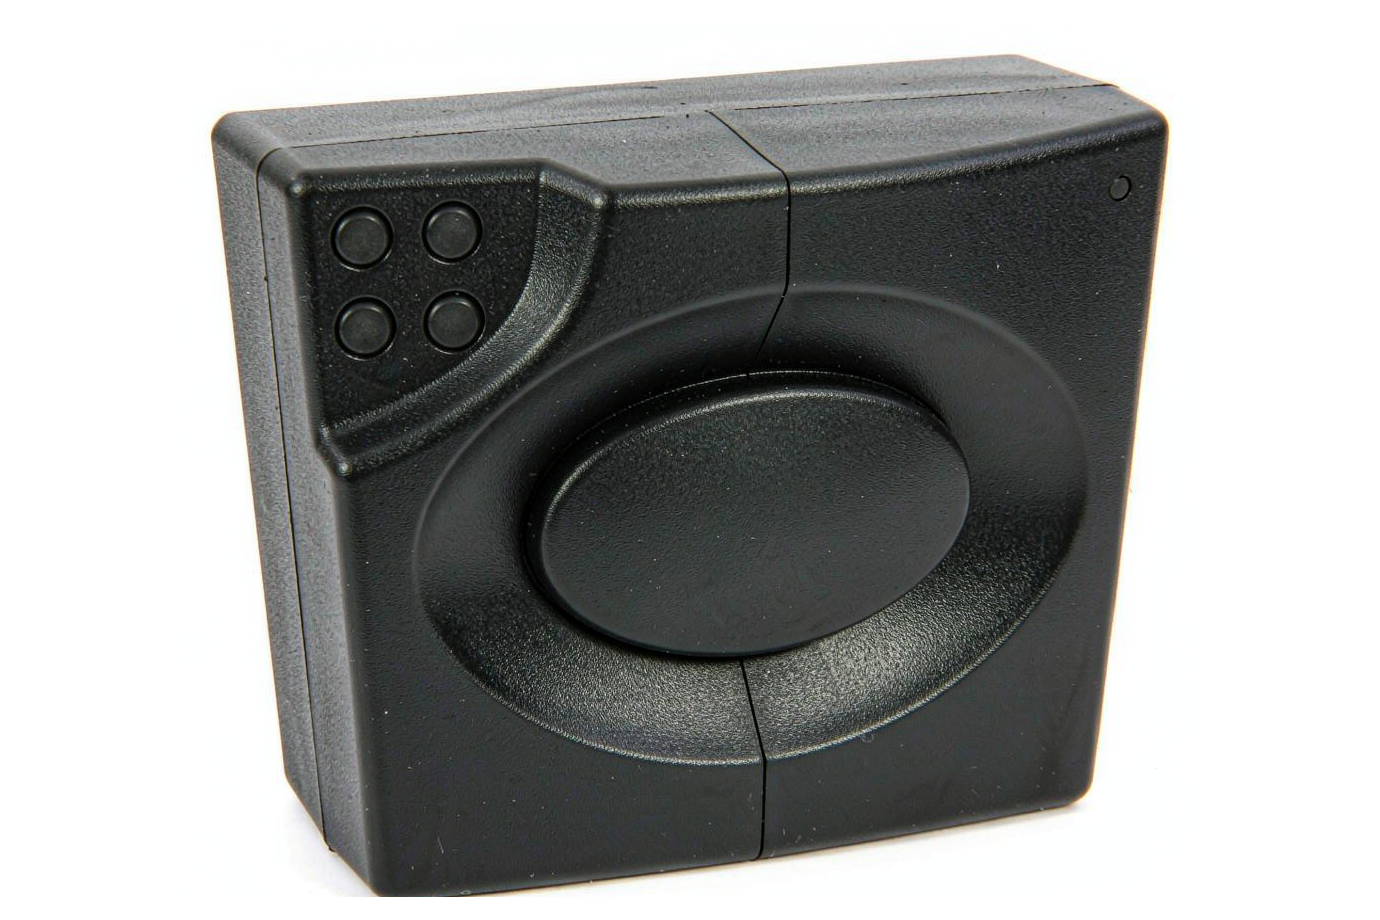
Prototyping note: every ABS program can start at one piece — CNC-machined parts give real-grade material behavior, 3D-printed parts the fastest geometry check. Rapid plastic prototyping covers both routes; MOQ is 1 piece.
09 — DFM Checklist
The eight design decisions that make or break an ABS part
We return this review with every quote, marked against your actual geometry — not a generic PDF.
Wall thickness
Keep walls uniform; thick mass sections cause sink and voids in molded ABS.
Rib design
Rib roots kept at a fraction of the wall add stiffness without sink marks on the show face.
Bosses
Cored and gusseted rather than solid — solid bosses are the classic ABS defect source.
Draft angles
Drafted faces protect cosmetic surfaces through ejection, especially on textured tools.
Snap-fits
ABS snap features work well; assembly strain is checked at DFM before the design freezes.
Gate location
Set with cosmetics, weld lines and filling balance in view — agreed with you, not assumed.
Parting line
Planned onto non-cosmetic faces so the show surface stays clean.
Corners & radii
Radius internal corners to cut stress concentration and improve mold filling.
10 — Surface Finish
Finishes that make ABS look like a finished product
ABS accepts more finishing routes than almost any other thermoplastic. Texture grade, paint class and plating each carry different cost — they belong in the quote, not in an afterthought email.
- Mold texture — from fine grain to heavy texture, defined by texture code on the drawing
- Painting — color and gloss to your physical standard or specified coating system
- Plating — requires plating-grade ABS chemistry, declared before the grade is fixed
- High-gloss vs matte show faces — tooled and processed differently; state which faces matter
11 — Color Control
Getting the color you signed off, part after part
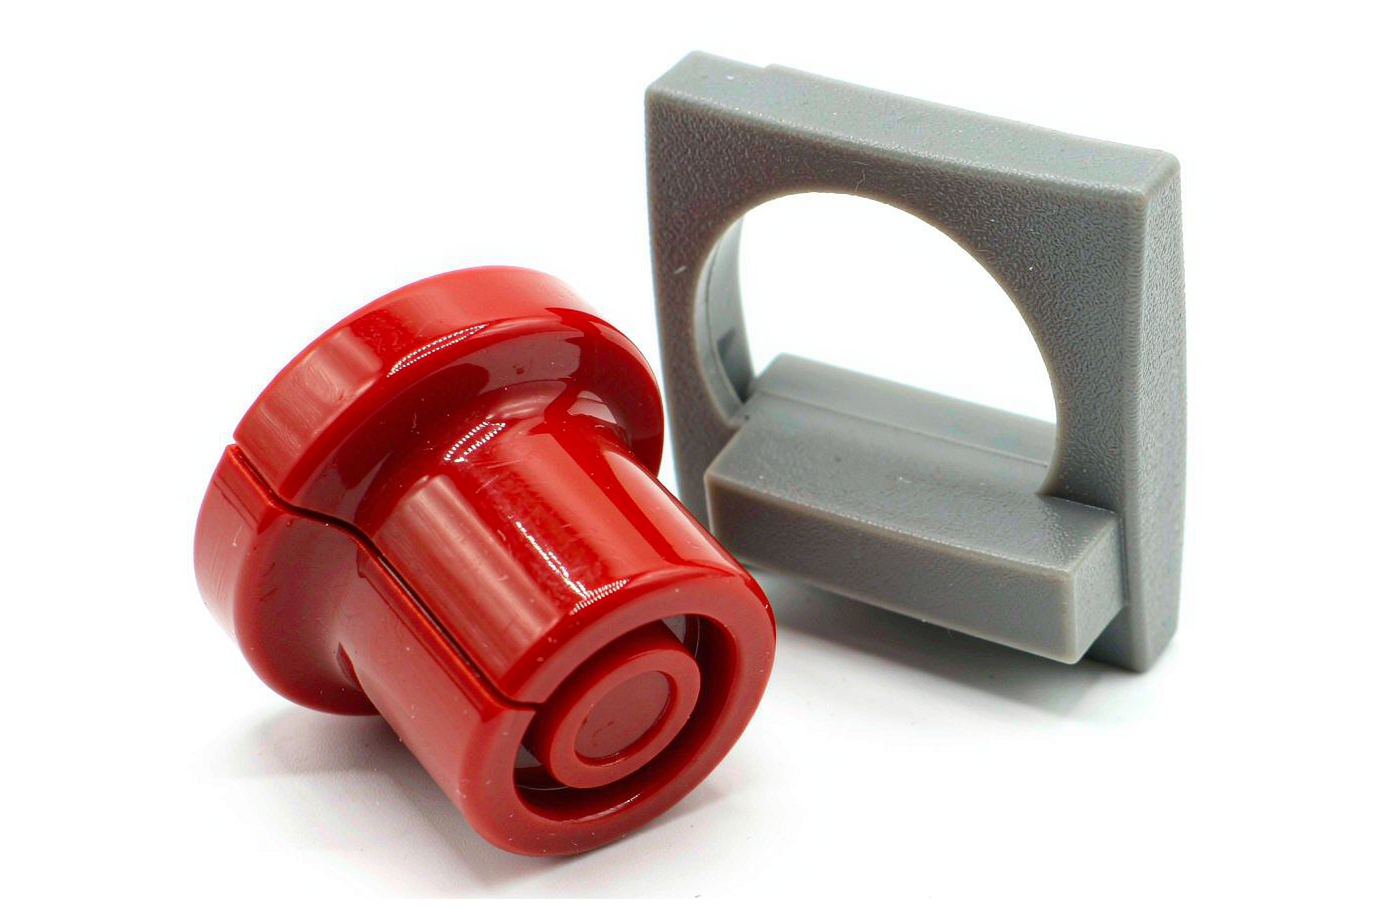
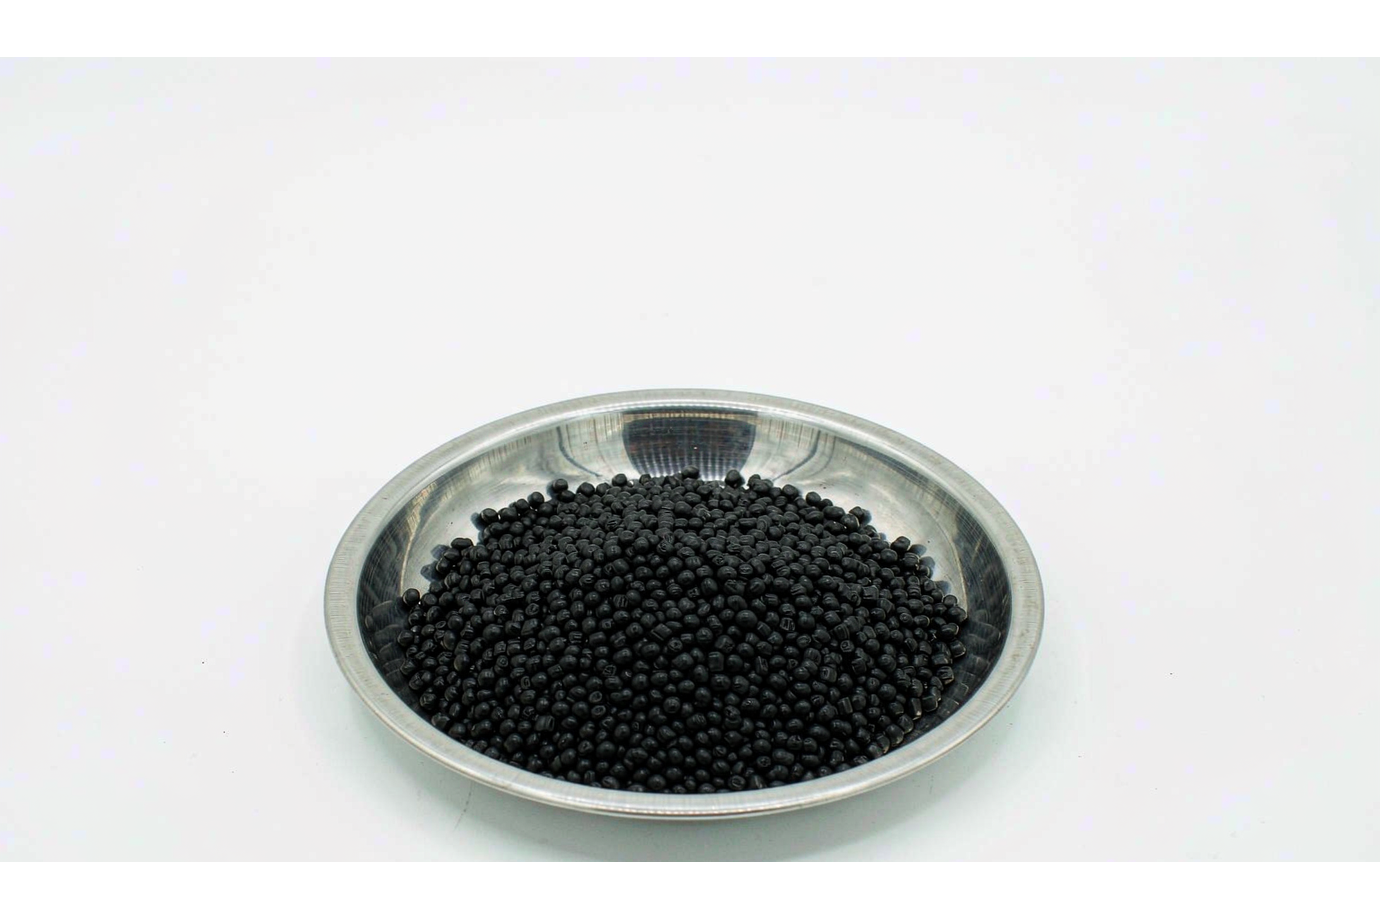
- Natural, pre-colored pellets matched to your colorant standard, or spray-painted to a physical master
- Color sign-off happens on physical samples before production, against your master or stated standard
- For molded parts, color consistency is tied to the same resin lot family and process window — the plan is agreed before release
12 — Flame-Retardant ABS
FR ABS, specified correctly instead of claimed casually
Flame-retardant ABS is available where your drawing specifies it — typically for electrical enclosures and power-adjacent parts. The important discipline: a UL 94 rating belongs to the resin formulation at a given wall thickness. We mold and machine exactly the grade your drawing names and pass through the resin supplier's grade documentation.
- FR grade built to your specification, not substituted at molding
- Rating tied to grade and wall thickness — checked at DFM, stated on the report
- Grade certification from the material supplier ships with the parts
13 — EU / US Documentation
Material paperwork your market actually asks for
- RoHS & REACH: compliance documentation available where required for your market; SVHC screening available on request
- Material traceability: resin grade certification from the supplier, batch-linked to your order
- Inspection records: FAI and dimensional reports per your acceptance criteria
How we state credentials
- Certification held — ISO 9001:2015 certified
- Alignment — IATF 16949 requirements supported
- Documentation — FAI, material certs, RoHS / REACH docs on request
Documentation packages, inspection reports and material certificates are available on request. Certificate copies can be provided under NDA.
14 — Quality Control
How an ABS part gets checked before it ships
- Incoming resin verified against the ordered grade and lot certificate
- First-article inspection against your drawing before any batch release
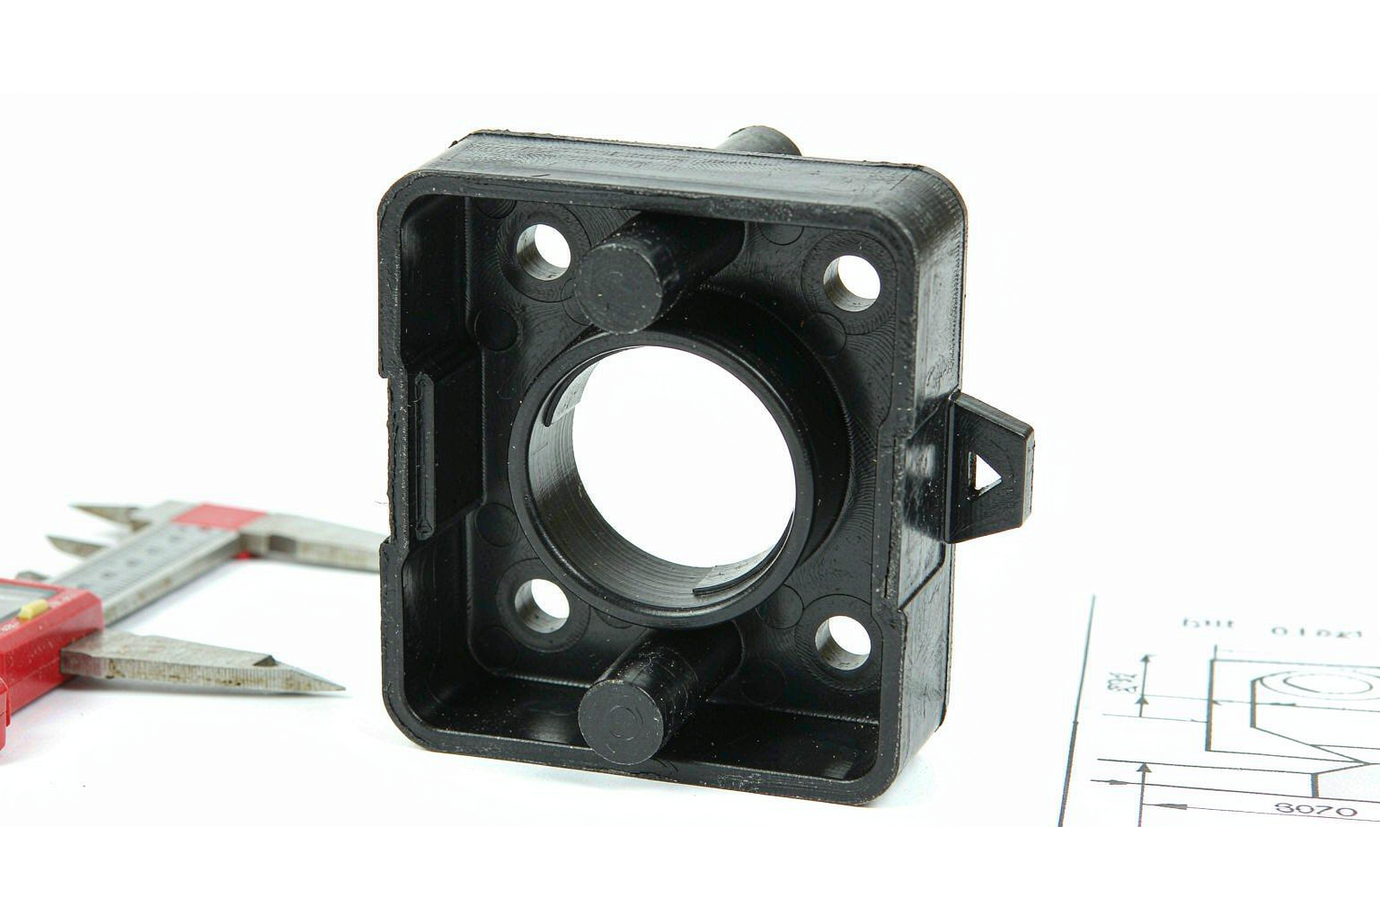
- In-process dimension checks; CMM final inspection on critical features; cosmetic inspection under defined lighting against the agreed appearance standard
- Inspection report included with shipment — you see what we measured
15 — From Prototype to Production
One program, four stages, no surprises between them
Prototype
CNC or 3D printed parts in real ABS, 3–7 working days typical — form, fit and finish validated.
DFM & freeze
Design feedback applied and the drawing frozen: grade, finish, color and critical dimensions locked.
Pilot batch
CNC or bridge-tooled low-volume run, 7–20 working days typical — process proven before hard tooling.
Production
Production mold and mass production, 15–25 working days typical — same quality system throughout.
Lead times are planning ranges confirmed per project; they depend on part complexity, tooling class and order size.
16 — Cost Drivers
Six factors that set the price of a custom ABS part
Knowing the levers makes quotes easier to compare — and easier to reduce.
Part size & wall section
Bigger parts and thicker walls cost more in resin and cycle time — the largest driver in molding.
Tooling class & cavities
Prototype, bridge or hardened production tool; cavity count sets tooling cost and piece price.
Grade & additives
FR, UV-stabilized and plating-grade resins carry premiums over general-purpose ABS.
Cosmetic finish level
Gloss show faces, painting and plating add process steps — priced per part, not hidden.
Tolerance & inspection depth
Tighter critical features and fuller FAI add measurement time — priced, not absorbed.
Order volume
Volume decides the economic process; crossing from CNC to molding changes the cost curve.
17 — Case Study
From one prototype to a molded production program
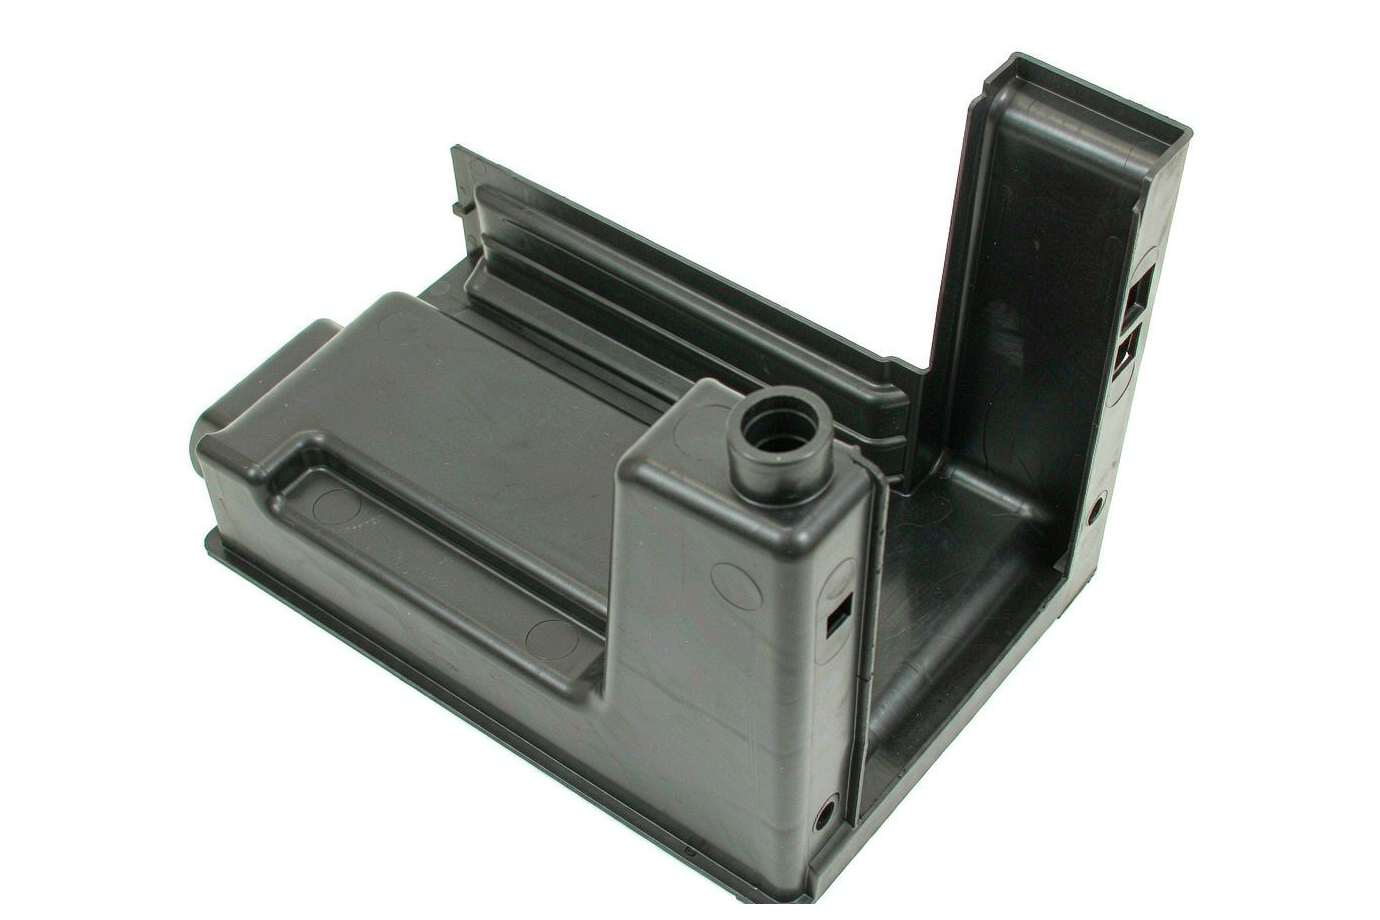
Appliance control enclosure — representative engineering example
- Material — flame-retardant ABS, customer-specified grade
- Envelope — 118 × 86 × 32 mm, wall 2.0 mm
- Route — 3D-printed fit check → CNC pilot batch → production mold
- Critical features — connector bore and snap-fit ribs
- Inspection — FAI report + CMM on critical features
- Documents — resin grade certificate with shipment
- Timing — prototypes inside the 3–7 day window; production per order confirmation
Representative engineering example: figures illustrate the documentation set we provide. Your project is confirmed against your drawing and datasheet.
18 — Request a Quote
What to send for a fast, firm ABS quote
- 3D model or 2D drawing — STEP, DWG or PDF
- ABS grade — or the performance target if the grade is open
- Expected annual volume and first-order quantity
- Cosmetic requirements — texture, color, gloss, faces that matter
- Applicable standards — UL 94 rating, RoHS / REACH documentation
- Target delivery and destination market
Send any subset to start — we reply with a quote and DFM feedback within 24 hours, and flag anything that will cost you money later.
19 — FAQ
Questions buyers ask before ordering ABS parts
Q1What types of ABS parts do you manufacture?
Housings and enclosures, covers and cosmetic panels, brackets and clips, gears and rollers, knobs and handles, interior trim parts, plus prototype and pilot-run parts — all built to your drawing, by CNC machining, injection molding or 3D printing.
Q2Can ABS be CNC machined?
Yes. ABS machines cleanly from plate or block with sharp positive-rake tooling. Typical CNC tolerance is ±0.01 mm, with qualified features to ±0.005 mm subject to a material-stability review, since plastics move more with heat and stress than metals.
Q3Do you provide ABS injection molding?
Yes — from prototype and bridge tooling through hardened production molds, with tooling, shrinkage, gate and parting-line planning handled in DFM. Our dedicated ABS injection molding page covers tooling options and molding-specific design rules.
Q4Which ABS grade should I choose?
General-purpose ABS covers most indoor housings; high-impact grades suit dropped or clipped parts; flame-retardant grades serve electrical enclosures; high-heat grades for warm zones; plating-grade for chrome-look parts; ABS/PC blends where more heat and impact is needed. Selection is confirmed against your datasheet.
Q5Do you offer flame-retardant ABS with UL 94 V-0?
We mold and machine flame-retardant ABS grades where the UL 94 rating is specified by the customer. The rating belongs to the grade formulation at a given wall thickness, so we build exactly the grade named on your drawing and supply the grade documentation — we do not self-certify flame ratings.
Q6Can ABS parts be painted or plated?
Yes — ABS takes paint, texture and plating well. Plating requires plating-grade ABS chemistry, so the finish should be declared before the grade is fixed. Gloss level, texture code and color standard should be stated on the drawing.
Q7Is ABS suitable for outdoor use?
Standard ABS weathers under sustained UV and is best treated as an indoor material. For outdoor-facing parts we recommend ASA, UV-stabilized grades or a protective coating — flagged at DFM before tooling is committed.
Q8ABS vs PC-ABS — which should I use?
ABS when cost and cosmetics lead and the part lives indoors at moderate temperatures. PC/ABS when the part needs higher heat deflection and greater impact toughness. PC/ABS costs more and is slightly less easy to plate.
Q9CNC machining or injection molding for ABS?
CNC has no tooling cost and suits prototypes and low volumes; molding wins on piece price once volumes justify the mold. A common route is CNC or 3D-printed prototypes, a pilot batch, then a production mold once the design freezes. We quote both routes so you can compare.
Q10Can I order just one ABS prototype?
Yes. MOQ is 1 piece for prototypes — validate form, fit and finish with a single CNC-machined or 3D-printed part before committing to tooling.
Q11What do you need to quote an ABS part?
A 3D model or 2D drawing (STEP, DWG or PDF), the ABS grade or performance target, expected annual volume, cosmetic requirements, applicable standards (UL 94, RoHS/REACH documentation), and target delivery. Quote and DFM feedback return within 24 hours.
Q12What inspection documents come with ABS parts?
First-article inspection reports, dimensional reports, resin grade certification from the material supplier, and RoHS/REACH compliance documentation where required. We are ISO 9001:2015 certified; documentation packages on request, certificate copies under NDA.
Send the drawing. Get the grade, the route and the price.
Upload your CAD file, drawing or even a sample part photo. We reply within 24 hours with a quote, DFM feedback and the process route we would actually run — CNC, molding or both.