Heat-Resistant Plastic Injection Molding — Parts That Hold Up in Hot Service
You need a plastic part that survives heat most resins cannot. The real questions: which high-temperature resin fits your service temperature and environment, how is it molded and verified, and what evidence proves the part will hold up in the field?
At a Glance
Yes — we mold heat-resistant thermoplastics including PEEK and PPS, with PEI, PPSU, PPA and LCP evaluated per program. The right resin is chosen by your continuous service temperature, chemicals and load — confirmed by the resin datasheet, a molding trial and dimensional inspection, not a single headline temperature.
What Does “Heat-Resistant” Mean Here?
We define heat resistance by continuous service temperature — the temperature the part sustains in its real operating environment — not by a marketing label. A resin that is “high-temperature” for one application may be marginal for another once you add chemicals, load or thermal cycling.
Four Temperature Numbers Buyers Confuse
A resin datasheet lists several temperatures. They are not interchangeable, and mixing them up is the most common cause of an over- or under-specified part.
| Number | Standard / test | What it actually predicts | How to use it |
|---|---|---|---|
| HDT (heat deflection temp) | ASTM D648 | Short-term deflection under a fixed load during a temperature ramp | Comparison only — never a service limit |
| Continuous use temp (RTI) | UL 746B (UL RTI) | Long-term thermal endurance with properties retained | The primary service-temperature input |
| Tg (glass transition) | DSC / ASTM E1356 | Softening onset; above Tg the amorphous portion loses stiffness | Design below Tg for dimension-critical parts |
| Tm (melting point) | DSC | Crystalline melt; process and upper-use boundary | Sets processing window and upper service ceiling |
How We Select the Resin
We start from your service temperature and environment, then narrow to a short list. Below is the working set we use; PEEK and PPS are confirmed in our process, while the others are evaluated per program once supply, processing and inspection are confirmed.
| Resin | Continuous use (typical) | Why buyers choose it | Status |
|---|---|---|---|
| PEEK | ~250–260°C | Best chemical resistance, high Tg, wear resistance | Confirmed |
| PPS | ~200–220°C | Chemical resistance, dimensional stability, rigidity | Confirmed |
| PEI | ~170°C | High strength-to-weight, stiffness, broad color | Under evaluation |
| PPSU | ~180°C | Toughness, hydrolytic stability, repeated heat | Under evaluation |
| PPA | ~120–160°C | Stiffness at heat, chemical resistance | Under evaluation |
| LCP | High (resin-dependent) | Thin-wall flow, dimensional stability at heat | Under evaluation |
“Typical” ranges describe the resin class from published datasheets; the value for your order is confirmed against the specific grade and standard. For PEEK-specific molding, see our PEEK injection molding page. Material grades and families are reviewed on our materials overview.
Comparing the Main Candidates
| Factor | PEEK | PPS | PEI (eval) |
|---|---|---|---|
| Continuous temp | Highest (~250°C) | High (~200–220°C) | Moderate (~170°C) |
| Chemical resistance | Excellent | Excellent | Good |
| Stiffness | High | Very high | High |
| Cost position | Highest | Moderate–high | Moderate |
| Best when | Aggressive chem + heat + wear | Chem + rigidity + value | Stiffness below PEEK cost |
PEEK leads on chemical and thermal extremes; PPS is the value choice where rigidity and chemical resistance matter at high heat; PEI fits stiffness-driven parts below PEEK’s cost. PPSU, PPA and LCP are evaluated per requirement.
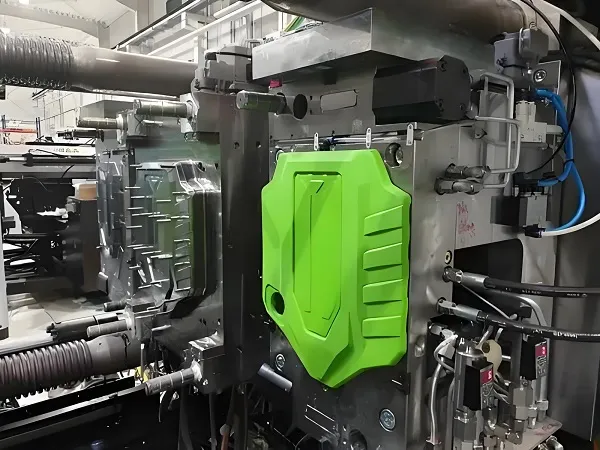
How Heat-Resistant Parts Are Molded
The workflow is the chain a buyer should expect — from resin specification to documented release.
Grade and lot confirmed; most high-temp resins are hygroscopic and dried to the resin’s spec before processing.
Mold designed for the resin — steel choice, gate location, cooling and, where needed, hot runners and tight temperature control.
Set from the resin datasheet — higher melt and mold temperatures than commodity plastics, controlled fill and pack.
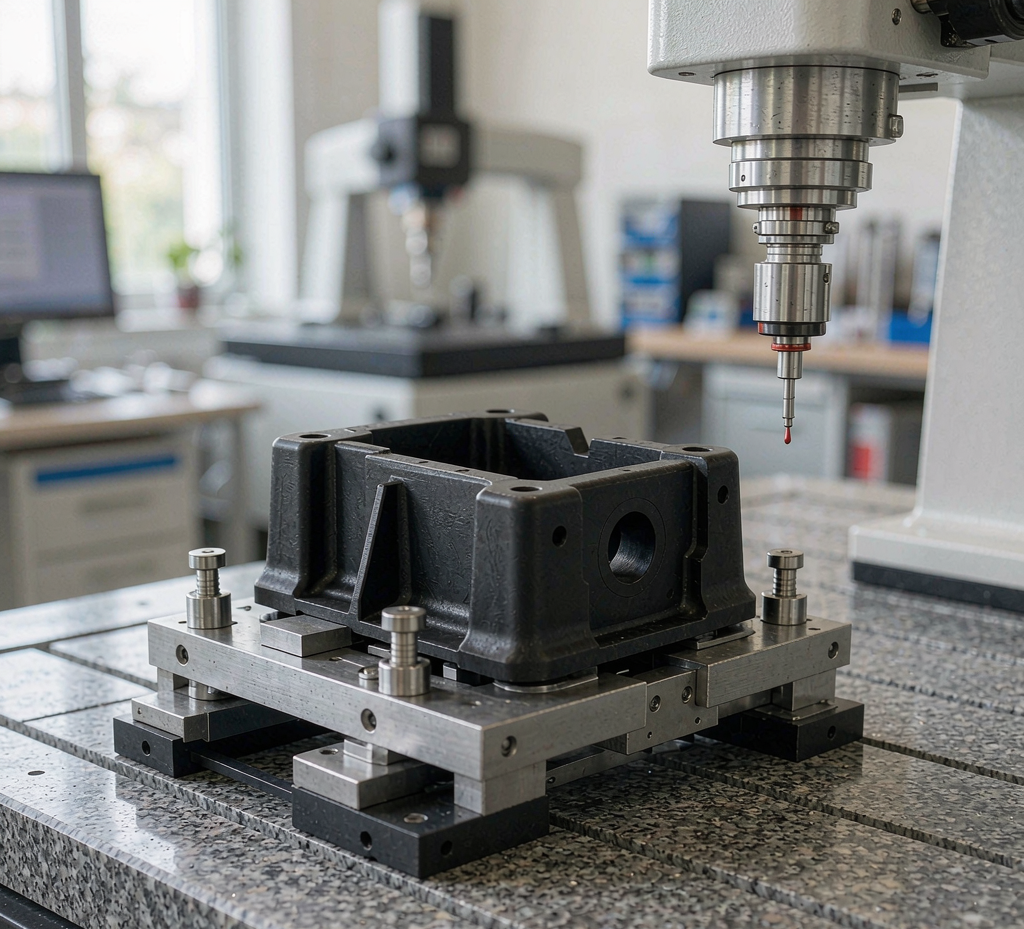
Critical dimensions measured by CMM or optical; resin cert, inspection report and CoC prepared.
DFM for High-Temperature Resins
Most cost and risk are set in design. Review these in DFM:
Shrink and warp scale with thickness; keep walls even and review against the resin’s shrinkage.
High melt temperature and shear need sized gates and good venting to avoid burn.
Rigid, high-temp parts need enough draft and a sound ejection scheme.
Per ISO 20457 / DIN 16742, not one universal number; call out CTQ features on the drawing.
Crystalline resins (PPS, PEEK) shrink more and anisotropically; gate location matters.
Trapped gas burns high-temp melts; vents sized to the resin and fill rate.
Validation & Verification
Heat resistance is proven by evidence, not asserted. For a hot-environment part we:
Confirm grade and lot against the specification before processing.
Check fill, short shots, flash and demold on the actual tool.
Measure critical features by CMM or optical comparator.
Add HDT/deflection or thermal-cycle tests where the application demands proof.
Need a Heat-Resistant Part Molded From Your Drawing?
Send your model and service conditions. We can recommend a resin, run DFM, and define the molding, validation and inspection plan.
Upload CAD / Request a Quote →Free DFM review · Quote typically within 24 hours
Quality Documents You Receive
Expect a resin material certificate (grade and lot), a dimensional inspection report, and a certificate of conformity, under our ISO 9001:2015 system. Resin- or application-specific certificates (for example flame-class or medical grades where applicable) are available on request.
Where Heat-Resistant Molded Parts Are Used
Connectors, sensors, housings near engines and exhaust.
Terminals, insulators, headers needing thermal and dimensional stability.
Pumps, valves, wear parts exposed to heat and chemicals.
Sterilizable instrument components, evaluated per requirement.
Clips, ducts, fittings with flame and heat requirements.
Heat-exposed bezels, sockets, fixtures.
Heat-Resistant Injection Molding RFQ Checklist
- 3D CAD model (STEP, IGES or native)
- 2D drawing with dimensions and tolerances
- Target continuous service temperature and environment (chemicals, load, cycling)
- Resin if known, or ask us to recommend
- Quantity and prototype-vs-production intent
- Critical tolerances and datum strategy
- Surface finish and any flame/class requirement (e.g., UL 94)
- Inspection and documentation requirements
- Application, annual volume and target delivery
Xiamen Goldcattle Plastic & Metal Products Co., Ltd. has provided custom molded and machined parts since 1998, with 100+ machines across six in-house processes under one ISO 9001:2015 quality system.
Frequently Asked Questions
Can you injection mold heat-resistant plastics like PEEK and PPS?
How do you choose the right high-temperature resin?
What does HDT mean, and can I specify by it?
What tolerance can molded heat-resistant parts hold?
Do these resins need special molding?
How do you prove a part will survive its hot environment?
What documents do I receive with molded parts?
What should I send to get a quote for heat-resistant molded parts?
Ready To Specify Your Heat-Resistant Molded Part?
Send your CAD model and drawing with the service temperature and environment. We review the resin fit, run DFM, and define the molding, validation and documentation plan for your program.
Upload CAD / Request a Quote →Free DFM review · Quote typically within 24 hours
Explore Injection Molding Capabilities →