Embossing vs Stamping: What Is the Difference in Sheet Metal?
Embossing is a forming operation performed within the broader metal stamping process — not a separate process competing with it. This guide explains how they relate, where their tooling and forming methods differ, and how to choose the right route for your part, volume and design.
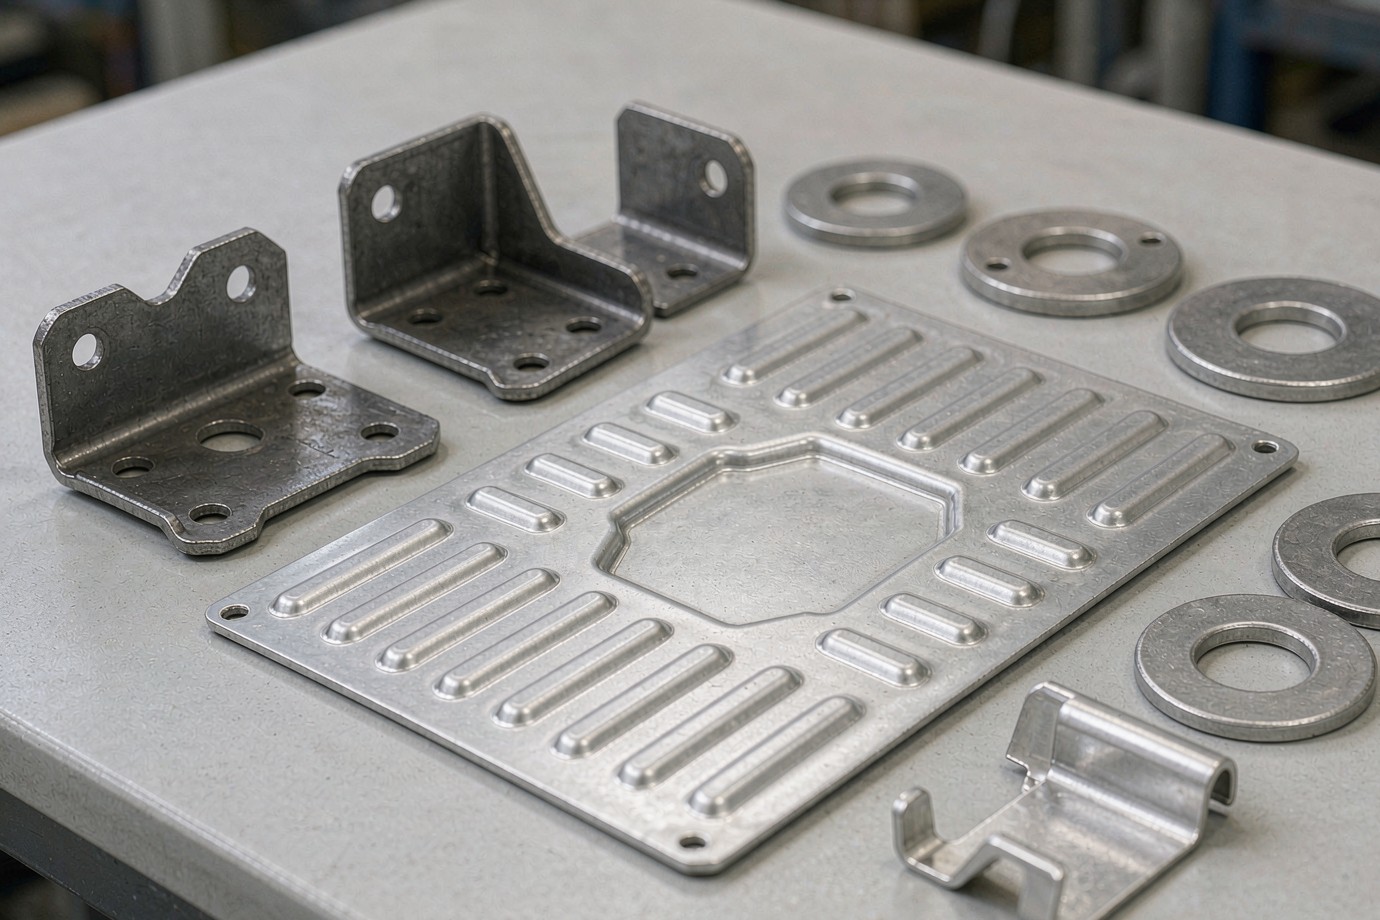
Embossing is generally a forming operation within the broader metal stamping process. Embossing creates localized raised or recessed features — ribs, dimples, logos, spacers or textures — while metal stamping is the wider process used to cut, punch, bend, draw and form sheet metal into finished components.
For an industrial part, the choice is usually not “embossing or stamping.” The real question is whether an emboss feature should be incorporated into the stamping process, and which tooling and forming sequence best fits the material, geometry, tolerance and production volume.
Embossing and Stamping: How Are They Related?
The most common misunderstanding is to treat embossing and stamping as two parallel, mutually exclusive processes. In practice, stamping is the umbrella manufacturing process, and embossing is one of the forming operations that can sit inside it — alongside blanking, punching, bending and drawing. That relationship is the foundation of every decision on this page.
Quick Comparison Table
A short, accurate comparison before the detail: embossing is a feature-level operation; stamping is the part-level production method that may contain it.
| Engineering Factor | Embossing | Metal Stamping |
|---|---|---|
| Scope | Specific forming operation | Broader manufacturing process |
| Main purpose | Create raised / recessed features | Cut, form or shape sheet metal |
| Typical features | Ribs, dimples, logos, spacers, textures | Holes, blanks, bends, forms, draws, embosses |
| Material deformation | Mainly localized | Localized or overall part geometry |
| Tooling | Emboss tool / matched tooling | Single, compound, progressive or transfer tooling |
| Can they be combined? | Yes | Yes |
| Typical role | Feature-level operation | Part-level production method |
| Volume suitability | Depends on tooling and application | Short runs to high volume |
| Cost driver | Tool complexity + material + quantity | Tooling + material + operations + volume + secondary |
| Best selection question | “Do I need this feature?” | “Is stamping the right route?” |
What Is Metal Embossing?
Embossing forms a localized raised or recessed feature in sheet metal using a matched punch and die, without removing material. The sheet thickness stays essentially the same; material is displaced, not cut. That makes it useful for both function and appearance.
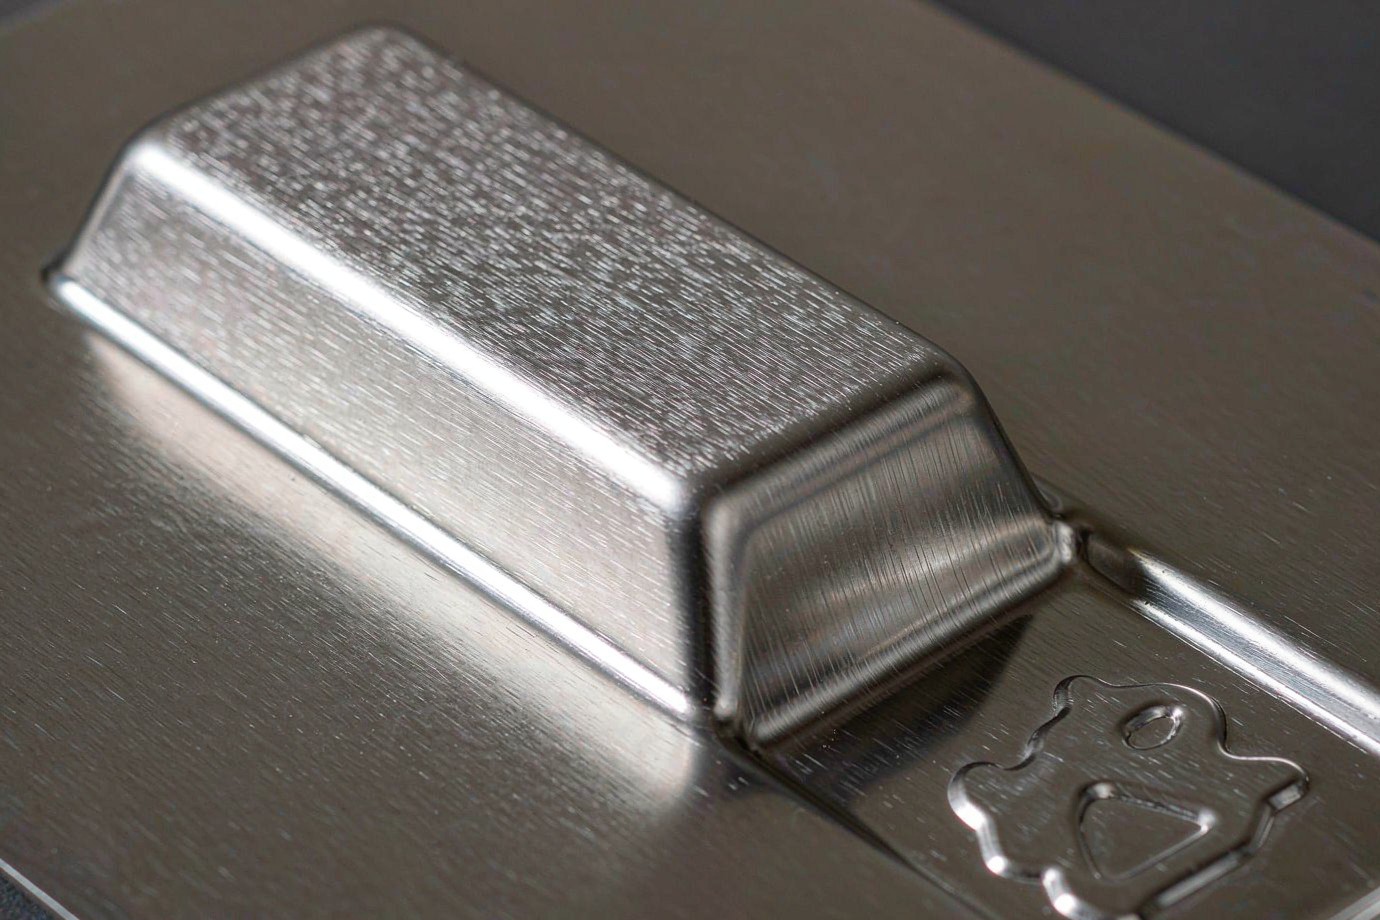
Functional embossing
Industrial embossing is frequently functional rather than purely decorative:
Ribs & stiffening
Local ribs add stiffness without increasing overall sheet thickness or weight.
Stand-offs & spacers
Raised features create clearance, spacing or mounting offsets.
Clearance & retention
Recesses can conceal fastener heads, provide clearance or retain magnets.
Surface function
Textured or tactile features improve grip or readability.
Decorative embossing
Logos, lettering and identification features are common, and many commercial parts combine a functional rib with a decorative mark in the same operation. Whether a feature is “decorative” or “functional” matters for how it is specified and inspected, not for whether embossing is the right method.
What Is Metal Stamping?
Metal stamping is the broader family of press operations that turn flat sheet into finished components. A single part often moves through several of these in sequence:
Cut the outline
Shears the part shape or a blank from the strip.
Holes & slots
Pierces holes, slots and internal features.
Form angles
Creates flanges, brackets and folded geometry.
Deep forms
Forms cups, cans and three-dimensional shells.
Local features
Raises or recesses ribs, dimples, logos or spacers.
Multi-station
Several operations in one die, strip fed station by station.
Because embossing is one of these operations, a “stamped part” typically already includes embossing where the design calls for it. The distinction buyers actually care about is which operations the part needs and how they are organised in the tool.
Embossing vs Stamping: Key Engineering Differences
Beyond the quick table, the engineering behaviour differs in ways that affect design and tooling:
| Dimension | Embossing | Stamping (whole part) |
|---|---|---|
| Deformation mechanism | Local plastic displacement | Cutting, bending, drawing and forming combined |
| Where it shows on the part | At the feature only | Across the whole part geometry |
| Tooling integration | Often a station or insert | The die system that carries the stations |
| Design sensitivity | Depth, radius, spacing to edges/holes | Blank layout, strip flow, springback, tolerances |
| Typical design control | Feature-level | Part-level and process-level |
When Should Embossing Be Added to a Stamped Part?
Embossing earns its place when it solves a specific problem:
Needed
Local stiffness without adding sheet thickness; a raised or recessed functional feature; a spacer, stand-off or mounting point; a controlled visual or tactile pattern.
By default
Do not emboss simply because it looks manufacturable. Evaluate the feature against material formability, sheet thickness, depth, spacing, tolerances, die access, springback and surface finish.
An emboss feature still has to survive the full manufacturing chain: it must form cleanly, hold definition through any finishing, and not interfere with adjacent bends, holes or assembly.
Embossing Design Considerations
Embossing is sensitive to how the feature sits in the sheet. The points below are the ones that decide whether a feature forms cleanly.
| Factor | What to watch |
|---|---|
| Material | Low-carbon steel, stainless, aluminium, copper/brass — same feature can crack, distort or lose definition across alloys |
| Thickness | Evaluate feature geometry against sheet thickness and formability; do not treat a feature height as a fixed number |
| Feature height / depth | Higher features need more generous radii and more formable material |
| Radius | Adequate corner radius reduces cracking and improves definition |
| Edge distance | Keep emboss features away from part edges to avoid distortion |
| Hole-to-feature distance | Spacing to holes and slots prevents wrinkling and thinning |
| Springback | Formed features relax after the punch releases; account for it in the tool |
| Surface requirements | Cosmetic, brushed, anodized or plated surfaces are affected by the forming step |
Stamping Design Considerations
The broader stamping design problem overlaps with embossing but adds part-level concerns:
Material use
How the part is nested on the strip drives scrap and cost.
Station order
The sequence of cut, pierce, form and emboss affects accuracy and tool life.
Bend control
Bends relax after forming; over-bend or coining may be needed.
Confidence
Apply tight tolerances only to functional features; confirm from the drawing.
Embossing, Stamping or Sheet Metal Fabrication?
Stamping is one route among several for sheet metal. The right choice depends on geometry, volume and lead time:
| Requirement | Likely Process |
|---|---|
| Prototype with low tooling commitment | Laser cutting + bending / suitable fabrication |
| Flat part with holes | Laser / punching |
| Bent bracket | Sheet metal bending |
| Repeated formed part at medium / high volume | Stamping |
| Large quantity + stable geometry | Progressive stamping |
| Raised rib / dimple / spacer | Embossing / forming |
| Deep three-dimensional cup | Deep drawing |
| Very tight dimensional features | Evaluate stamping + secondary machining |
For fabrication versus stamping trade-offs and low-volume routes, see our custom sheet metal fabrication service.
How Production Volume Changes the Best Manufacturing Route
Volume is one of the strongest drivers of process choice, but the break-even point is different for every part — there is no single count above which stamping automatically wins.
Flexibility first
Tooling investment, sample validation, setup and flexibility matter more than piece price. Laser cutting, bending, machining or a simple forming setup usually fit.
Amortization
The tooling cost begins to amortize against a lower piece price; the comparison becomes tooling spend versus recurring savings.
Dedicated tooling
Compound, progressive or multi-stage tooling economics become clear when the annual volume and program life support the investment.
Practical buyers compare annual volume, tooling cost, piece price and program life together — not a single volume threshold.
What Drives the Cost of Embossing and Stamping?
Rather than a fixed price list, cost is explained by the factors a supplier actually quotes against:
Die type
Single, compound, progressive or transfer tooling sets the baseline.
Number of stations
More operations mean more die complexity.
Material thickness
Thicker, harder material needs more press tonnage and tool strength.
Feature complexity
Emboss depth, radii and tight features raise tooling effort.
Tolerances
Tight functional tolerances add inspection and process control.
Annual volume
Volume decides whether tooling amortizes against piece price.
Tool life
Expected life and maintenance affect long-run cost.
Secondary operations
Finishing, plating or machining add steps and cost.
Inspection
FAI, PPAP or lot-level checks add documented quality cost.
Can Embossing Be Integrated Into Progressive Die Stamping?
Yes. Embossing is commonly one station within a progressive die, performed as the strip advances through blanking, piercing, bending and other operations. Integrating it removes a separate handling step and keeps the feature located relative to the rest of the part.
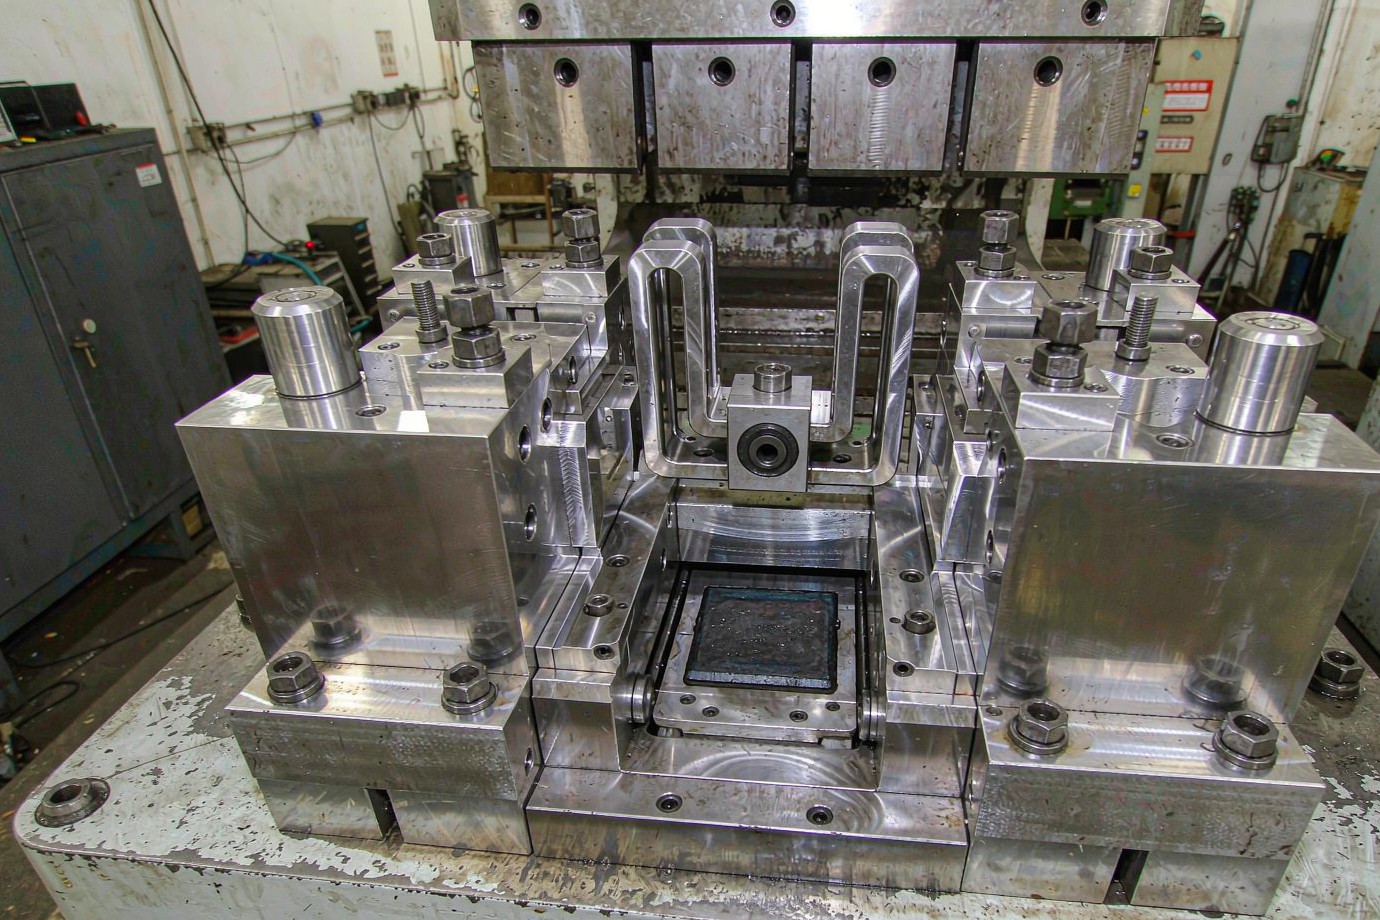
The trade-off is tooling commitment: a progressive die suits stable geometry and higher volume. For low or uncertain volume, a simpler single-operation or fabricated route is usually lower risk.
What Do I Need to Send for a Stamping Quote?
A complete package lets a supplier return a realistic tooling and piece-price quote instead of a range. Send the essentials, and add what you can.
Send these
2D drawing and 3D CAD where available; material grade; sheet thickness; quantity and annual volume; tolerances; surface finish; critical features; application; target launch date.
Add these
Existing tooling information; annual forecast; material certificate requirement; inspection, FAI or PPAP requirements; packaging needs.
How Goldcattle Handles Custom Stamped and Embossed Parts
When a part reaches us, the work follows a consistent path rather than a one-off quote:
Drawing & DFM review
Check feature feasibility, material, thickness, tolerances and forming sequence.
Tooling strategy
Choose single, compound, progressive or integrated emboss tooling from geometry, volume and tool life.
Production
Stamping presses from 25 to 200 tonnes, with bending, custom dies and progressive capability across stainless, aluminium and brass.
Inspection
First article and lot-level checks against the drawing; documented results on request.
Related Manufacturing Processes
Embossing and stamping sit inside a wider sheet-metal and metal-forming toolkit. These pages cover the neighbouring routes:
Frequently Asked Questions
Is embossing a type of metal stamping?
What is the main difference between embossing and stamping?
Can embossing and stamping be used on the same metal part?
Is metal embossing only decorative?
Does embossing make sheet metal stronger?
Is metal embossing cheaper than stamping?
When should I use progressive stamping?
What information should I send for a stamping quote?
What materials can be embossed or stamped?
Not Sure Whether Embossing Belongs in Your Stamped Part?
Send the drawing and tell us what the feature must do — stiffness, spacing, marking or appearance. Our engineering team will review feasibility, recommend whether embossing should sit inside the stamping process, and return findings with your quotation.
Get an Embossing & Stamping Review Or see custom metal stamping parts →A material and DFM review is returned with the quote — typically within one business day for standard parts.