Engineering Practice & Buyer Guide · Updated September 2026
Aluminum CNC Machining: From Material Selection to Production
A practical guide to specifying and sourcing custom aluminum CNC parts — alloy and temper, starting stock, DFM, tolerances, anodizing, inspection, cost and RFQ. Built for engineers and sourcing teams, not beginners.
Quick Answer: How Should You Approach Aluminum CNC Machining?
Successful aluminum CNC machining starts with the part requirement, not the machine. Define the required strength, weight, corrosion resistance, dimensional stability, surface finish and production volume first. Then select the alloy and temper, machining route, workholding, tolerances and finishing around those requirements. The material and the drawing — not the machine list — decide the result.
Aluminum CNC Machining Decision Map
The path from idea to produced part is a sequence, not a single step. Use this map to find the section you need.
- Part Requirement & Application Load
- Material & Temper
- Starting Stock Form
- Geometry & DFM
- 3 / 4 / 5-Axis Configuration
- Tolerance & GD&T
- Surface Finish
- Inspection
- Quantity & Cost
- Production Route
Why Aluminum Is Widely Used for CNC Machined Parts
For procurement, a few properties actually matter — not the metallurgy from ore to metal.
Low Density
About one-third the density of steel, valuable for weight-sensitive structures and portable products.
Good Machinability
Common alloys cut cleanly, which helps cycle time and surface quality versus harder metals.
Strength-to-Weight
Alloys such as 6061 and 7075 cover a wide range of structural needs at low mass.
Corrosion Behaviour
Naturally oxide-protected; varies strongly by alloy and can be improved by anodizing.
Thermal / Electrical
Useful conductivity for heatsinks and electrical housings.
Finishing Options
Anodizing, blasting and coating give both protection and appearance.
Aluminum Alloy Selection for CNC Machining
Select by requirement, not by a league table. The common alloys for Goldcattle’s European and North American buyers:
| Alloy | Why buyers specify it | Watch-outs | Typical tensile* (MPa) |
|---|---|---|---|
| 6061-T6 / T651 | General-purpose, machinable, good corrosion resistance | Lower strength than 7075 | ~310 |
| 7075-T6 / T651 | High strength-to-weight | Higher cost, lower corrosion resistance than 6061 | ~570 |
| 2024-T3 / T351 | High strength / fatigue-oriented use | Corrosion and finishing considerations | ~440 |
| 6082-T6 | Common European structural alloy | Less common than 6061 in some markets | ~310 |
| 5052-H32 | Corrosion resistance / formability | Most useful where sheet or forming matters | ~215 |
| 6063-T5 / T6 | Extrusions, appearance, profiles | Not the first choice for maximum strength | ~185–240 |
* Typical published tensile strength for the temper shown. Actual values depend on product form and temper and are confirmed by the material certificate (for plate and sheet, e.g. ASTM B209). Always specify alloy + temper + applicable specification on the drawing.
Aluminum Alloy vs. Temper: Why T6 and T651 Matter
Write the full callout on the drawing — for example AL 6061-T651 plate — not just “aluminum 6061”. For European or aerospace programs the standard may be EN, AMS or a customer specification; the applicable standard follows the product form and the drawing.
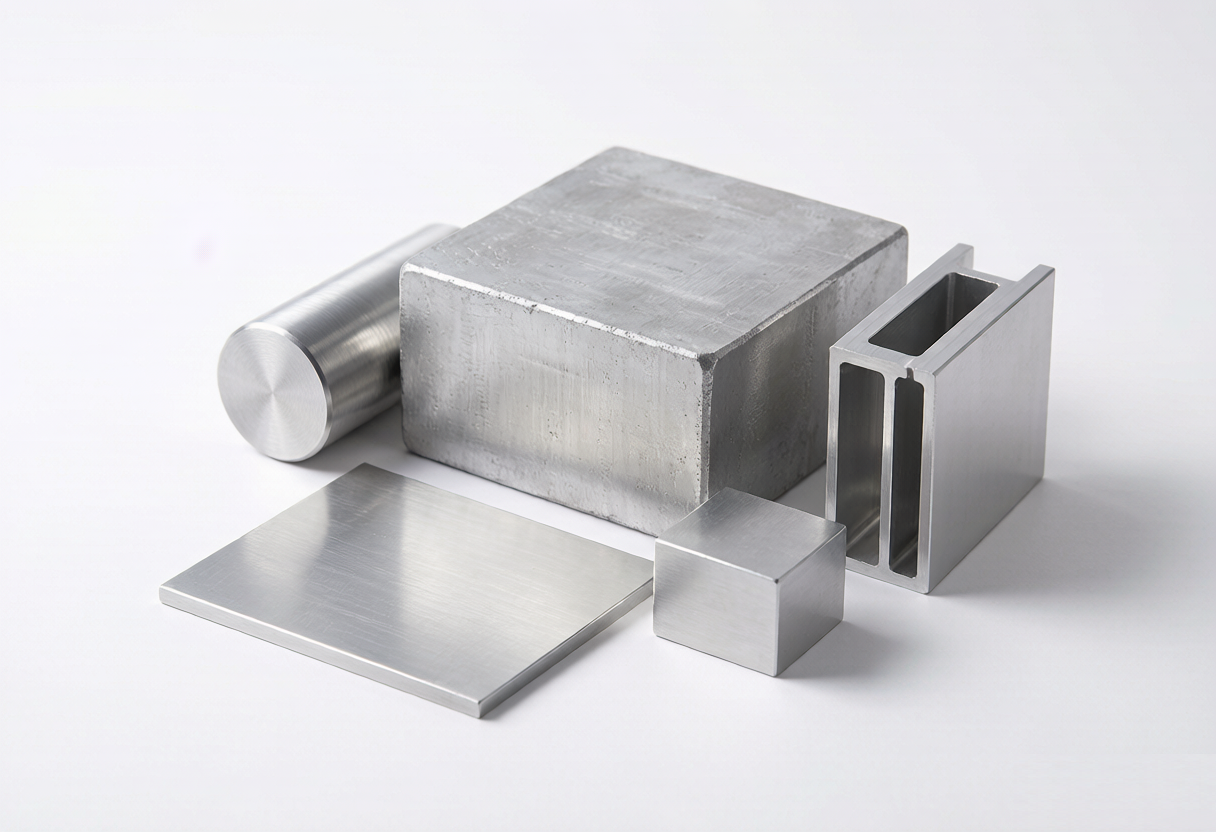
Billet, Plate, Bar or Extrusion: Which Starting Form?
CNC does not start with a machine; it starts with raw material form. The form drives material use, fixturing and cost.
| Starting stock | Best fit |
|---|---|
| Plate | Flat structural parts, machined plates |
| Billet / Block | Complex housings, brackets, prototypes |
| Round Bar | Shafts, turned parts |
| Extrusion | Long profiles, repeated cross-section |
| Forging / Preform | High material efficiency for suitable production designs |
Aluminum CNC Design for Manufacturability
Wall Thickness
Thin walls vibrate and deflect under cutting and can vary after residual-stress release. Keep walls manufacturable and well supported.
Deep Pockets
Deeper pockets need longer tools and raise deflection, chatter and machining time. Match pocket depth to the shallowest that meets function.
Internal Corners
Avoid zero-radius corners; a practical corner radius lets the tool cut instead of plunging.
Ribs
Over-thin ribs deflect and finish poorly; size them for the process.
Holes
Consider drill access, tool size and depth; very deep holes add cost and risk.
Threads
State metric or imperial, class and depth; avoid needless special threads.
Undercuts
May need 3+2, 5-axis, special tooling or a redesigned geometry.
The Most Common Aluminum CNC Design Mistakes
Specifying unnecessarily tight tolerances.
Making walls too thin for the process.
Making pockets deeper than needed.
Using sharp internal corners.
Ignoring tool access and setup count.
Ignoring anodizing thickness and dimensional change.
Choosing 7075 when 6061 is sufficient.
Applying 3D-printing design rules to CNC.
How Aluminum CNC Machining Is Actually Performed
A practical sequence, from file to inspected part:
Process planning and simulation can help find access and collision issues before cutting. Actual dimensional quality is still verified by inspection — simulation is not a substitute for measurement.
Choosing the Right CNC Axis Configuration
| Geometry | Often consider |
|---|---|
| Simple prismatic | 3-axis |
| Wrapped / indexed features | 4-axis |
| Multi-face / angled features | 3+2 |
| Complex continuous surfaces | Simultaneous 5-axis |
This page is an entry point only. For depth, see 5-axis CNC machining services, when to use 5-axis and 7075 on 5-axis.
Common Aluminum CNC Machining Problems
Built-Up Edge
Aluminum can adhere to the tool edge, affecting finish and size.
Chatter
Linked to rigidity, tool overhang and cutting conditions.
Burrs
Common at drilling, slotting and thin edges; need a deburr plan.
Heat
Thermal effects influence size and surface if not managed.
Warpage
Thin walls and plates can move as residual stress releases.
Tool Wear
Varies by alloy and cutting condition; affects consistency.
Symptom → Likely Cause → Corrective Direction
| Symptom | Possible cause | Corrective direction |
|---|---|---|
| Burrs | Tool wear / geometry / condition | Check tool and cutting strategy |
| Chatter | Weak workholding / tool overhang | Increase rigidity |
| Thin wall moves | Cutting force / stress release | Revise wall, strategy, workholding |
| Hole oversize | Tool deflection / runout | Check tooling and compensation |
| Poor finish | Tool condition / chips / vibration | Adjust toolpath and tooling |
| Dimension shifts after finishing | Heat / residual stress | Process sequencing and stock condition |
| Anodized fit too tight | Coating build-up | Allow for finish in design |
How Much Tolerance Do You Really Need?
Tighter tolerance should follow function, not act as a generic quality signal. A high-accuracy machine does not by itself guarantee a tight part tolerance — material stability, fixture rigidity, tool condition, temperature, sequence and inspection all matter.
- General dimensions — use a reasonable general tolerance; do not over-specify.
- Functional dimensions — bearing fits, shaft holes, locating faces and mating surfaces justify tighter control.
- Cosmetic dimensions — rarely need ultra-tight tolerance.
A controlled drawing requirement always overrides a generic supplier tolerance table. State the tolerance where it is functional; let general tolerances cover the rest.
Choosing a Surface Finish for CNC Aluminum Parts
| Finish | Main purpose |
|---|---|
| As-machined | Basic functional parts |
| Bead blasted | Uniform matte appearance |
| Brushed | Directional cosmetic finish |
| Type II anodized | Corrosion resistance and appearance |
| Type III hard anodized | Wear-resistant, harder surface |
| Powder coated | Protection and appearance |
| Chem film (conversion) | Corrosion / electrical / primer base |
For the full finish guide, see aluminum surface finishing and wear-resistant aluminum parts.
Will Anodizing Change My Aluminum Part Dimensions?
Yes. Anodizing grows an oxide coating on and into the aluminum surface, so it affects close-fitting holes, mating faces and interfaces. For US or aerospace drawings, when a spec calls for MIL-PRF-8625, name the anodizing type and class rather than simply writing “anodized.”
Engineers should: define coating thickness, flag critical mating dimensions, consider masking, and plan post-process inspection. This is the difference between a part that fits and one that does not.
Aluminum vs Steel, Stainless and Titanium
The point is not “aluminum wins” — it is knowing when to switch material.
| Factor | Aluminum | Steel | Stainless | Titanium |
|---|---|---|---|---|
| Weight | Low | High | High | Low |
| Strength | Moderate–high | High | High | Very high |
| Machinability | Good | Moderate | Lower | Lower |
| Corrosion | Good | Coating needed | Excellent | Excellent |
| Cost | Moderate | Lower | Higher | Highest |
Replace aluminum when you need extreme wear resistance, high-temperature strength, very high stiffness or a severe chemical environment — then consider tool steel, appropriate high-temperature alloys, or stainless / titanium.
What Drives the Cost of CNC Aluminum Parts?
- Material — 6061, 7075, 2024 and others differ in price and availability.
- Material volume — deep pockets mean more stock removed and more waste.
- Machining time — complex geometry takes longer.
- Setups — more re-fixturing adds engineering and setup cost.
- Tolerance — tighter control needs more process and inspection effort.
- Finish — anodizing, coating or polishing add steps.
- Inspection — CMM, FAI and material certs add documentation cost.
- Quantity — setup cost spreads across the batch.
How to Reduce Cost Without Reducing Function
- Use 6061 instead of 7075 where strength does not justify the premium.
- Remove unnecessary tight tolerances.
- Reduce deep pockets to the functional minimum.
- Add manufacturable internal radii.
- Reduce unnecessary setups.
- Use standard thread sizes.
- Choose a finish appropriate to the application.
- Combine quantities where practical.
How Aluminum CNC Parts Should Be Inspected
| Area | What to verify |
|---|---|
| Material | Alloy, temper, certificate |
| Dimensional | Caliper/micrometer for basics; CMM for complex or critical features |
| Geometric | Flatness, parallelism, perpendicularity, position, runout |
| Surface | Visual, Ra when specified, coating thickness where applicable |
| First Article | Drawing-based inspection report |
Machine accuracy is not the same as part accuracy. A supplier may have a high-accuracy machine, but final part performance also depends on material stability, fixture rigidity, tool condition, temperature, sequence and inspection. Verify, do not assume.
How to Evaluate an Aluminum CNC Machining Supplier
| Area | What to verify |
|---|---|
| Material | Alloy / temper / certificate |
| Machining | Relevant equipment and real examples |
| Process | DFM, fixturing, process control |
| Quality | CMM / FAI / inspection records |
| Supply | Lead time, packaging, revision control |
Do not qualify a supplier by the machine list alone. Equipment is necessary but not sufficient; process control and inspection evidence decide whether parts are repeatable.
What Should Be Included in an Aluminum CNC RFQ?
Part Information
- Name / number
- Revision
- 2D drawing
- 3D CAD
Material
- Alloy
- Temper
- Material specification
Manufacturing
- Milling / turning
- 3 / 4 / 5-axis if required
- Raw material form
Quality
- General tolerance
- Critical dimensions / GD&T
- Surface roughness
- Inspection requirement
Finishing
- Anodizing type / color
- Masking
- Blasting / coating
Documentation
- Material cert
- CMM / FAI
- PPAP where applicable
If Your Drawing Is Incomplete
Send the 3D CAD model, any 2D dimensions you have, the alloy or intended application, quantity and required finish. If material or tolerance is not final, state the functional requirement instead of letting the supplier guess. A supplier can review manufacturability, but final material, tolerance and acceptance criteria should be confirmed before production.
Case Study: Custom 6061-T6 Aluminum Housing
A representative project: a buyer needed a machined aluminum enclosure with milled pockets, multiple holes and angled features. The review confirmed 6061-T651 met the load and corrosion need without paying for 7075. DFM revised a few thin walls and sharp internal corners to improve stability. Multi-face features were planned for 3+2 / 5-axis to reduce setups. Type II anodizing was specified with critical bores masked. Final parts were CMM-inspected against the drawing, with a first-article report provided.
Figures such as weight or cost savings are not stated because every project differs; the value here is the decision path — material, DFM, axis choice, finish and inspection — not a borrowed metric.
When Aluminum Is Not the Right Choice
- Extreme wear resistance → consider tool steel or hardened steel.
- High-temperature strength → consider appropriate high-temperature alloys.
- Very high stiffness → some steels suit better.
- Severe chemical environment → consider stainless or titanium.
- Repeated sliding contact → a different material or finish combination may be needed.
Aluminum CNC vs Other Manufacturing Methods
| Requirement | CNC Aluminum | Die Casting | Extrusion + CNC | Sheet Metal | 3D Printing |
|---|---|---|---|---|---|
| Prototype | Excellent | Tooling needed | Good for profiles | Good | Excellent |
| Complex billet geometry | Excellent | Strong after tooling | Limited | Limited | Strong |
| High volume | Cost-dependent | Strong | Strong | Strong | Often less economical |
| Design iteration | Excellent | Tool changes | Moderate | Good | Excellent |
For the trade-offs, see die casting vs CNC, 3D printing services and sheet metal fabrication.
Goldcattle Aluminum CNC Machining Capability
Manufacturing since 1998, Xiamen Goldcattle runs aluminum CNC under one ISO 9001:2015 quality system: 3 / 4 / 5-axis milling and turning, DFM review, CMM inspection, anodizing and related finishing, and prototype-to-production support from customer drawings and CAD.
Related guides: aluminum CNC overview, best alloys, design for CNC, best practices, 6061 material and CNC services.
Frequently Asked Questions
What aluminum alloy is best for CNC machining?
There is no single best alloy; 6061 is the common general-purpose choice for machinability, corrosion resistance and cost, while 7075 is selected when higher strength-to-weight justifies its higher cost and lower corrosion resistance. The right choice follows the part requirement, not a ranking.
What is the difference between 6061-T6 and 6061-T651?
6061 is the alloy designation. T6 is a heat-treatment temper; T651 is the same T6 condition with stress-relief by stretching, which reduces residual stress and distortion risk in machined parts. Specify the temper your drawing or application requires.
Is 7075 harder to CNC machine than 6061?
7075 machines well but is generally less free-machining than 6061 and can be more prone to built-up edge and tool wear at aggressive conditions. The practical difference is in tooling and cutting strategy, not in whether it can be machined.
Should I use billet, plate or extrusion for aluminum CNC parts?
It follows the geometry: plate for flat structural parts, billet or block for complex housings and brackets, round bar for shafts and turned parts, extrusion for long repeated cross-sections. The starting form affects material use, fixturing and cost.
What tolerance should I specify for aluminum CNC parts?
Tie tolerance to function. General dimensions can use a reasonable general tolerance; only functional features such as bearing fits, shafts and locating surfaces need tighter control. Tighter tolerance adds machining, measurement and inspection effort, so specify it only where it matters.
Can aluminum CNC parts be anodized?
Yes. Type II sulfuric anodizing is common for corrosion resistance and appearance; Type III hard anodizing adds a thicker, wear-resistant coating. When a drawing calls out MIL-PRF-8625, specify the applicable anodizing type and class rather than simply writing “anodized.”
Does anodizing change aluminum part dimensions?
Yes. Anodizing grows an oxide coating on and into the surface, so it affects close-fitting holes, mating faces and interfaces. Define coating thickness, identify critical mating dimensions, consider masking, and plan for post-process inspection.
How do thin walls affect aluminum CNC machining?
Thin walls are prone to vibration, deflection and dimensional variation during cutting and to distortion from residual stress release. Keep walls manufacturable, support them in fixturing, and avoid specifying them thinner than the process comfortably holds.
How deep can an aluminum pocket be machined?
Depth is limited by tool length, rigidity and chip evacuation rather than by a fixed number. Deeper pockets need longer tools, which increase deflection and chatter risk; design pockets to the shallowest depth that meets function, or discuss tool access with your supplier.
Can aluminum parts be made on a 5-axis CNC machine?
Yes. 3-axis suits simple prismatic parts; 4-axis handles wrapped or indexed features; 3+2 and simultaneous 5-axis suit multi-face, angled and continuous-surface geometry. This page points to the right axis configuration rather than replacing the dedicated 5-axis guides.
What documents should I request from an aluminum CNC supplier?
At minimum ask for material certificate (alloy, temper, specification), dimensional report, CMM data for critical features, and first-article inspection where applicable. Do not qualify a supplier by machine list alone; verify process control and inspection records.
Can you machine aluminum from a drawing or CAD file?
Yes. A controlled 2D drawing plus a 3D CAD model is the strongest basis for a quote and DFM review. If the drawing is incomplete, send the 3D model, intended application, quantity and finish, and state functional requirements instead of leaving the supplier to guess.
What information is needed for an aluminum CNC quote?
Part name and revision, 3D CAD and 2D drawing, alloy and temper, material specification, CNC process and axis requirement, tolerances and GD&T, surface finish, quantity and documentation needs. The more complete the RFQ, the more reliable the quote and lead time.
Is CNC machining aluminum cheaper than steel?
Not automatically. Aluminum is often faster to machine, but material cost, alloy choice, geometry, finish and quantity all shift the comparison. The honest answer depends on the specific part; a supplier quote with the route broken out is the only reliable basis.
When should I use 7075 instead of 6061?
Choose 7075 when strength-to-weight or fatigue performance drives the design and the lower corrosion resistance and higher cost are acceptable. If 6061 already meets the load and environment, specifying 7075 adds cost without function.
Ready to specify your aluminum CNC part?
Send the CAD and drawing. We return a DFM review, material and process recommendation, and a quote broken out by route.