304 vs 316 Stainless Steel: How to Choose for CNC Machined Parts
The 304/316 decision is a corrosion decision, not a strength decision — both grades are specified to the same minimum mechanical properties. What differs is molybdenum, and what molybdenum buys is a narrower band of conditions in which the part survives. This guide works that band out from the service environment, then follows it through machining, finishing and verification.
At a Glance
Choose 304 when the exposure is moderate and costing matters; choose 316 when chlorides, salt or a specific chemical medium create a real pitting or crevice risk. The two grades have the same specified strength and hardness, so the decision is not a mechanical one. Work from the medium, its concentration, the service temperature, the standing time and the crevices in the geometry — then write the grade and its governing standard on the drawing. Both grades machine the same way in principle: sharp edge, positive engagement, no dwell, chip control, coolant at the cut. Neither needs a published rpm table, and neither justifies a looser tolerance.
What Actually Differs Between 304 and 316
Both are austenitic stainless steels. Both are non-hardenable by heat treatment, both are nominally non-magnetic in the annealed condition, and both rely on a chromium-rich passive film rather than on alloy strength for their corrosion behavior. The entire meaningful difference between them sits in one alloying element.
| Element | 304 / 304L | 316 / 316L | What it does to the part |
|---|---|---|---|
| Chromium | 18.0–20.0% | 16.0–18.0% | Forms the passive film. Below roughly 10.5% the alloy is no longer stainless; above that, more chromium generally means a more stable film. |
| Nickel | 8.0–10.5% | 10.0–14.0% | Stabilises the austenitic structure. Governs toughness, formability and how the chip behaves. |
| Molybdenum | Not added by design | 2.00–3.00% | The one element that materially changes pitting and crevice corrosion resistance in chloride service. |
| Carbon | ≤0.08% (L ≤0.030%) | ≤0.08% (L ≤0.030%) | Governs sensitisation in welded assemblies, and the guaranteed minimum strength. See Section 06. |
| Nitrogen | ≤0.10% | ≤0.10% | Minor austenite former; contributes to the pitting index. |
Typical ranges as specified for flat-rolled product. Bar product carries the same grade designations under its own standard, with its own permitted ranges — which is the subject of Section 03.
Why molybdenum matters, in one number
Pitting resistance is commonly ranked with a pitting resistance equivalent number, computed from composition rather than measured:
Run the arithmetic and the difference stops being rhetorical. Molybdenum contributes 3.3 points for every 1%, so 2–3% molybdenum adds roughly 6.6 to 9.9 points on its own. With chromium in the specified bands, 304 lands around 18–20 and 316 around 24–28.
That is a real difference, and it is also the whole of the difference. PREN contains no term for temperature, stagnation, surface finish, crevice geometry or residual stress — and those are where stainless parts actually fail. A high index does not survive a badly designed gasket groove.
What the Grade Change Does Not Change
Most of the durable misconceptions about this pair concern properties that are identical between them. Clearing these first shortens every later conversation.
| Common assumption | What is actually specified |
|---|---|
| “316 is the stronger one” | It is not. In the annealed condition both grades carry the same specified minimums: 515 MPa tensile, 205 MPa yield, 40% elongation and a 201 HBW hardness ceiling. There is no strength case for paying the 316 premium. |
| “316 is several times harder to machine” | Both sit at the same machinability index on the common scale, around 45. Mill data that publishes both usually shows reference cutting speeds within roughly 10–20% of each other. The gap between either grade and a free-machining grade such as 303 is far wider than the gap between them. |
| “316 is the marine grade” | 316 is the starting point for chloride service, not a qualification. Warm seawater, stagnant zones, fouling and tight crevices defeat it. See Section 05. |
| “Food equipment must be 316” | Both grades appear in food-contact equipment. What separates them is the cleaning and sanitizing chemistry, the surface finish and the crevice design — not the grade name on its own. |
| “Ra depends on which grade you pick” | It does not. Surface roughness is created by the tool path, the edge condition and the stability of the cut. See Section 09. |
| “316 needs a looser tolerance” | It does not. Tolerance is set by machine capability, fixturing, tool condition, thermal stability and the inspection method. The grade changes the process window and the wear rate, which affects consistency across a run — not the tolerance the drawing can ask for. |
| “A magnet tells you which one you have” | It does not. Both are austenitic and nominally non-magnetic, and machining cold-works the surface enough to make either one slightly magnetic. See Section 11. |
The practical consequence is that the choice is almost never settled by a property table. It is settled by naming the environment precisely enough that the answer becomes obvious.
The Callout Problem: A Grade Name Is Not a Specification
A drawing that says 316 and nothing else does not define a purchasable material. It defines a grade name, which becomes a specification only when it is combined with a product form, a governing standard and a condition. This is the most common avoidable dispute in stainless procurement, and it has nothing to do with corrosion theory.
| What the drawing says | What it permits | What to write instead |
|---|---|---|
| “316” | Any product form, any condition, any mill, any chemistry inside the grade band | Grade + standard + condition + certificate type |
| “316 per ASTM A240” | Plate, sheet and strip — not bar | Correct for a plate part; wrong for a part cut from bar |
| “316 per ASTM A479” | Bar for pressure and high-temperature service | The usual correct default for a machined bar part |
| “316 per ASTM A276” | Hot-finished or cold-finished bar for machining stock | Acceptable, but A276 permits wider chemistry bands than A479 — decide if that matters |
| “316L” with no reason stated | A lower carbon limit, which is a welding provision | State whether L is a functional requirement or a stocking convenience |
| “316” where the customer cites EN 10088-3 | The EN designation (1.4401 / 1.4404), whose ranges resemble but do not exactly match the ASTM bands | Quote against the customer’s standard; dual-certified stock usually satisfies both, but ask for both certificates |
None of this changes the machining. It changes what arrives at the machine, what the certificate says, and whether the part can be accepted. It is worth ten minutes at quotation.
Choosing by Service Environment, Not by Industry
Industry labels are a poor proxy for corrosion risk. Two “chemical plant” parts can face 5% caustic at 30 °C and 20% sulphuric at 80 °C, and the correct answers are different grades. Two “marine” parts can differ by whether one of them is rinsed by rain and the other sits in a sheltered crevice collecting salt.
The order of operations below resolves most of these cases before any grade is named.
- Name the medium, not the sector. Chemical family, concentration, and whether it is a mixture. “Cooling water” is not a medium; chloride content and biocide program are.
- Fix the temperature — both of them. The process temperature and the cleaning temperature. The second is the one that is usually omitted and the one that most often changes the answer.
- Establish time and stagnation. A part that drains dry between shifts is a different risk from one that sits wet in a low-velocity pocket for years.
- Inventory the crevices. Gasket faces, O-ring grooves, thread roots, slip fits, weld toes, blind tapped holes and the gap under a washer. Most stainless failures start in a gap that was never discussed.
- Decide the consequence and the inspection interval. A weeping cosmetic cover and a leaking acid line justify different levels of conservatism at the same corrosion rate.
- Then choose the grade and write the reason down. A one-line justification on the drawing or in the RFQ prevents the next engineer from “optimising” it away.
| Service environment | Start with | Confirm before committing |
|---|---|---|
| Indoor machinery, dry, occasional condensation | 304 | Whether any cleaning agent is chloride-based |
| Food and beverage contact, cleaned in place | 304 or 316 | The cleaning chemicals, their concentration, temperature and dwell — see Section 10 |
| Coastal atmosphere, de-icing salt, road spray | 316 | Sheltering, whether rain washes the part, and how often salt sits on it |
| Warm chloride process water, cooling towers | 316 is the floor, not the answer | Temperature, stagnation, biocide regime, and whether the surface is fouled |
| Seawater, continuous or intermittent | Evaluate duplex or higher | Velocity, aeration, crevices and galvanic couples; 316 only with a defined maintenance regime |
| Strong acids or alkalis at temperature | Neither, by default | The specific medium and concentration — this needs a corrosion assessment, not a grade comparison |
| High-purity fluid path, pharma or semiconductor | 316L, often electropolished | Surface finish, particle and outgassing requirements, documentation |
| Sustained service in the 425–815 °C range | Not a 304/316 question | Sensitisation and creep — a stabilised or higher-alloy grade is the correct conversation |
When 316 Is Not Enough
A page that stops at “use 316 for aggressive service” has taught the buyer nothing about the case where 316 fails in the first year. That case exists, it is common, and it is where a supplier’s competence is actually visible.
| Option | What it buys you | What it costs you |
|---|---|---|
| Duplex 2205 (S32205) | Roughly twice the yield strength of the austenitics and a much higher pitting index (around 34 by the same formula), plus strong resistance to chloride stress corrosion cracking | Higher cutting forces, a different tool strategy, tighter welding discipline, less stock availability, higher price. It is not a drop-in for every chemical medium. |
| Super-duplex 2507 | Further again on strength and chloride resistance | Narrow supply, specialist welding, higher machining risk |
| 904L (N08904) | High nickel with molybdenum; strong in sulphuric and phosphoric acid service where 316 is inadequate | Expensive, gummy to machine, longer lead time |
| 6% Mo super-austenitic | High pitting index, good seawater and chloride resistance while staying fully austenitic | Cost, availability, and a machining behavior that needs its own parameters |
| Nickel alloys | Specific aggressive media that no stainless handles | An order of magnitude in cost and a very different supply chain |
Above 316 the comparison stops being a table. The correct method is to take the actual medium, concentration and temperature and check published iso-corrosion data for candidate alloys, then confirm with a coupon test if the exposure is critical. Any supplier who answers an aggressive-medium question with a grade name and no medium has not answered the question.
304L and 316L: What the L Actually Buys
The L suffix is a carbon limit, and it exists for one reason: welding. It is not a purity upgrade, not a corrosion upgrade, and not a machining improvement.
| Grade | Carbon max | Min tensile | Min yield | What the L buys |
|---|---|---|---|---|
| 304 | 0.08% | 515 MPa | 205 MPa | Baseline |
| 304L | 0.030% | 485 MPa | 170 MPa | Resistance to sensitisation in a welded heat-affected zone |
| 316 | 0.08% | 515 MPa | 205 MPa | Baseline, plus molybdenum |
| 316L | 0.030% | 485 MPa | 170 MPa | Same welding benefit, plus molybdenum |
Minimum values in the annealed condition as commonly specified for these grades. Confirm the exact values against the standard named on your drawing.
Two practical consequences. First, dual-certified 316/316L bar is common: one heat certified to both, giving L-grade carbon with standard-grade minimums. It is a good default for machined parts, provided the certificate actually states both designations and your specification accepts dual certification. Second, if a drawing calls for 316L for a machined-only component and the application is strength-driven, that is worth a question rather than a silent substitution in either direction.
How the Two Grades Behave at the Cutting Edge
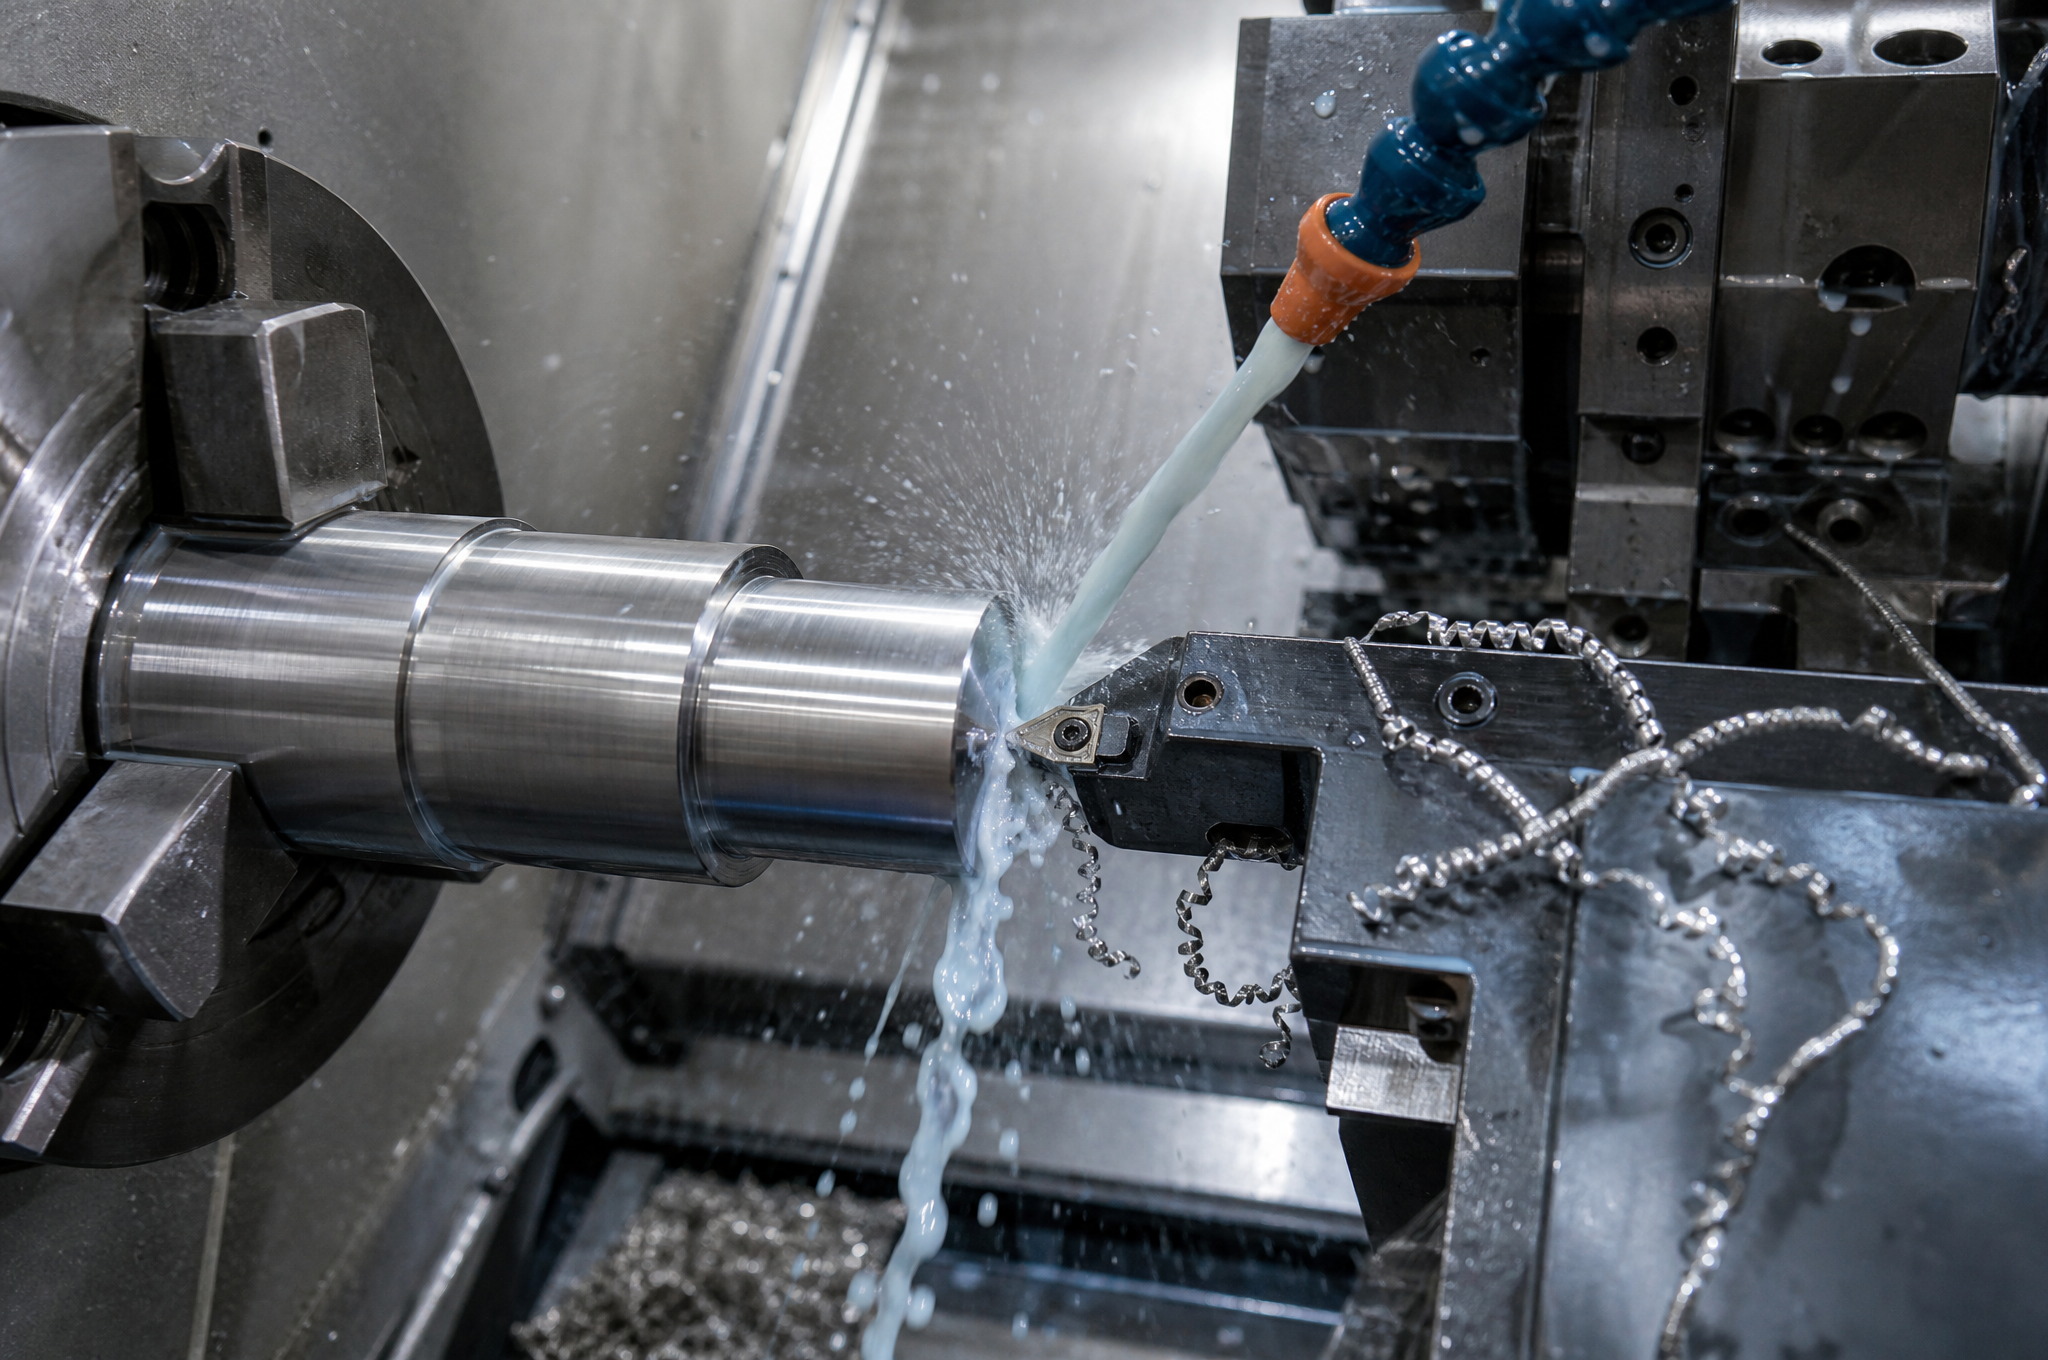
Because the mechanical properties are effectively identical, the machining behavior is too — in kind and, within a modest margin, in degree. Both are austenitic: both work-harden, both produce stringy chips, both keep heat at the edge. Treating 316 as a separate difficulty class leads to over-conservative parameters, which is itself a cause of the problems the caution was meant to avoid.
Why there is no reusable rpm table
The number a tool is actually rated for is cutting speed at the edge, not spindle speed. Spindle speed is derived from it:
The same spindle speed is conservative on a 20 mm cutter and destructive on a 4 mm one, because the diameter in that equation is four times smaller and the edge speed four times higher. This is why a published rpm range without a diameter cannot be reused, and why a shop that quotes one is describing the tools it happens to own.
A quotation should instead show the operations, the number of setups, the fixturing approach, the tool strategy for the hardest feature, and the inspection method for the tightest tolerance. Those five items are what actually determine whether the part comes back correct.
What Changes per Operation
The grade does not change the operation plan; it changes where each operation is likely to go wrong, and therefore what the plan has to say about it.
| Operation | Where it goes wrong in 304 / 316 | What the process has to control | What to look for in the quote |
|---|---|---|---|
| Milling | A rubbing pass hardens a skin, and a thin floor or wall chatters | Sharp variable-helix cutter, climb milling, constant engagement on deep pockets, support under thin floors | A named toolpath strategy, not simply “CNC milled” |
| Turning | Long stringy chips wrap the part and mark the finished diameter; the insert craters | Chipbreaker for stainless, coolant directed at the cut, a finishing pass that is not a spring pass | A chip-control statement, especially for deep bores |
| Drilling | The hole wall work-hardens under a rubbing margin; the drill walks on a curved entry | Spot or pilot, correct point geometry, pecking, coolant through the tool beyond about 3×D | Coolant-through capability where depth demands it |
| Tapping | Small taps snap in work-hardened material; threads tear rather than cut | Forming tap where the material allows it, otherwise spiral-flute with EP coolant; thread depth at least 1.5×D | A stated tap type, and a stated thread depth |
| Thin-wall sections | Deflection, spring-back and chatter; the wall ends up tapered | Support from both sides where possible, sequential roughing, light radial engagement on the finish | A named minimum wall, and a stated support method |
| Sealing bores | Ovality and taper from tool deflection read as a diameter that measures but does not seal | Boring rather than plunging, or a low-engagement finishing pass | Roundness or cylindricity called out separately from the diameter |
| Threads and sealing faces together | A thread root is a crevice, and so is the face under a gasket | Finish and cleanliness at both, not just dimensional compliance | Deburr and cleaning steps named in the routing |
None of these lines would read differently for 304 than for 316. That is the point: the process plan transfers, and the corrosion decision is made on top of it. Which of the operations carries your part depends on the geometry — rotational features on CNC turning, multi-face and angled features on 5-axis machining, and the choice between them is a setup-count question rather than a material one.
Surface Finish Is a Process Output, Not a Material Property
A 304 part and a 316 part machined on the same machine, with the same tool and the same parameters, land in the same roughness band. Publishing a separate Ra range for each grade treats a process result as an alloy property, and it invites a buyer to specify a finish that the drawing never actually controls.
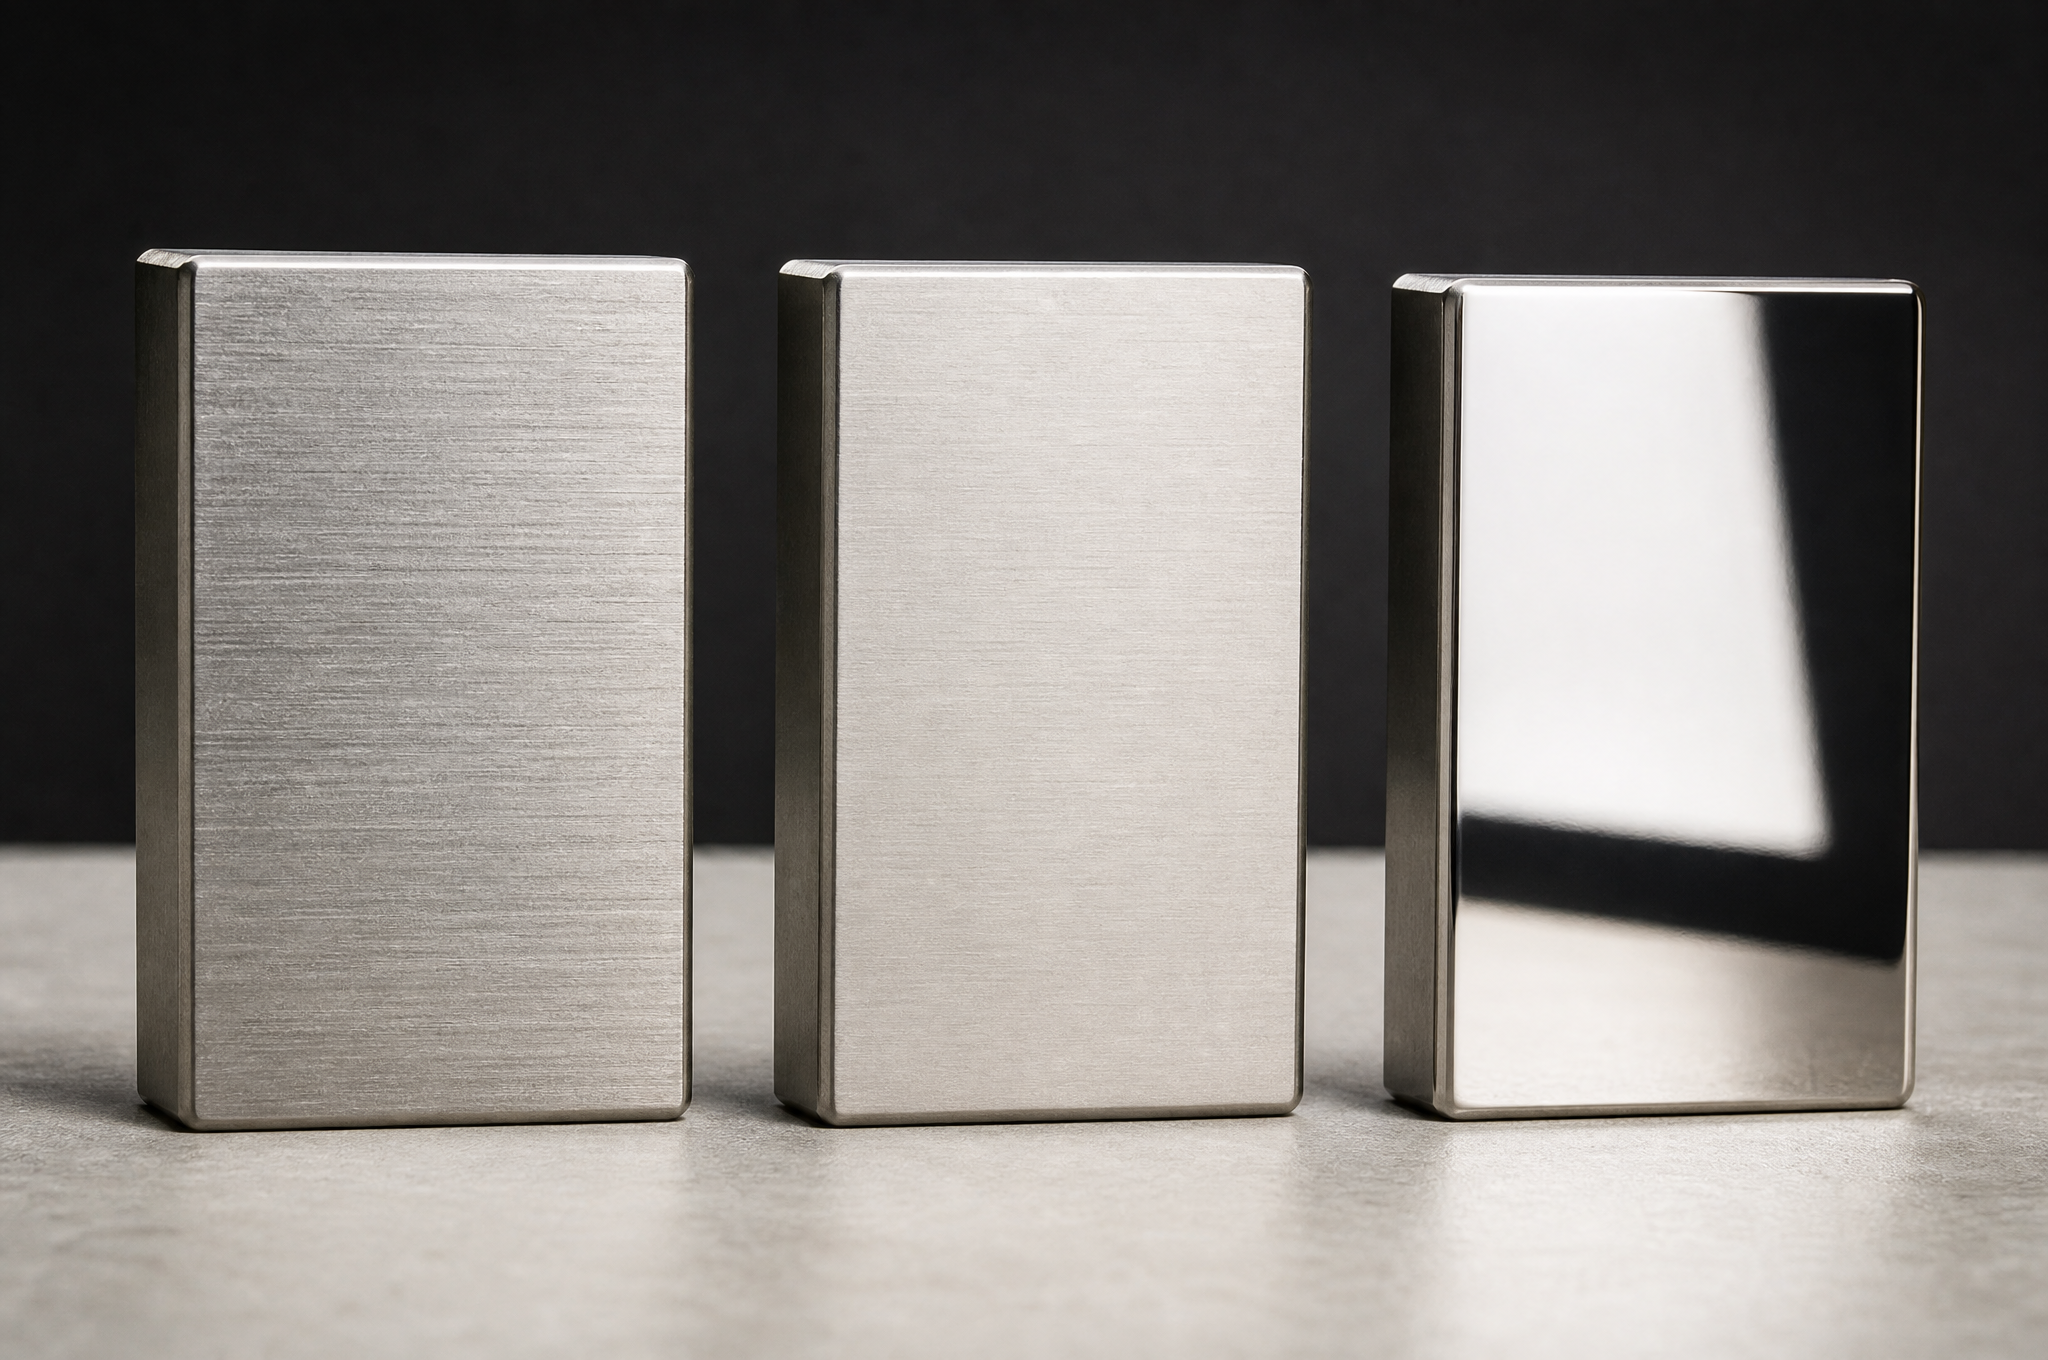
The variables that actually set roughness are the cutting edge, the feed per revolution or per tooth, the stability of the setup, the tool wear state at the finishing pass, and any post-treatment. What the grade changes is how quickly the edge wears, and therefore how much the finish drifts between the first part and the two-hundredth.
| What the drawing should state | Why the wording matters | Example |
|---|---|---|
| The Ra value with units | “Smooth” and “fine” are not acceptance criteria | Ra 0.8 µm max |
| Where it applies | Applying a seal-face finish to the whole part is a cost with no function | On the sealing face only; Ra 3.2 µm elsewhere |
| Direction of measurement | A gasket face and a sliding face are sensitive to different directions relative to the lay | Measured across the lay |
| Measurement method and cutoff | Two labs can disagree on the same surface if the cutoff differs | Stylus profilometer, 0.8 mm cutoff |
| Whether polishing is permitted | Polishing rounds edges and can alter a bore; it is not a neutral operation | Polishing permitted on external faces only |
| Functional or cosmetic | Cosmetic Ra on a hidden face is money spent on nothing | Cosmetic requirement: brush finish, no Ra callout |
Passivation, Pickling and Electropolishing: Three Different Jobs
These three are routinely specified interchangeably and they are not interchangeable. Each removes something different, and each leaves a different surface behind.
| Process | What it actually removes | What it does not do | Standard to name |
|---|---|---|---|
| Cleaning | Coolant, oils, handling soils and loose debris | Does not restore a passive film that machining or contamination destroyed | — |
| Pickling | Heat tint, weld scale, embedded iron, and a thin layer of the base metal itself | Leaves a brighter but slightly rougher surface, and removes microns of material — it is not dimensionally neutral | ASTM A380 for the practice |
| Passivation | Free iron contamination on the surface; encourages the chromium oxide film to re-form | Does not dissolve heat tint, scale or weld oxide | ASTM A967, with A380 for context |
| Electropolishing | A controlled layer of metal, levelling micro-peaks and leaving a chromium-enriched surface | Does not repair a roughness created by a bad cut, does not remove deep scratches, and does round edges | ASTM B912 |
For machined parts with no weld, the usual requirement is a cleaning step followed by passivation to ASTM A967, in either the nitric or the citric family. Which family, and for how long, belongs in the specification rather than in a shop-floor habit. Where the part is for a high-purity fluid path or a hygienic surface, electropolishing is the specification that carries the intent, and the Ra callout should be written to match it rather than in parallel with it.
The wider sequence — identifying why a stainless part stained, separating iron contamination from chloride attack, and controlling handling and packaging after finishing — is covered in how to prevent rust on CNC-machined stainless steel parts. Once the grade is fixed, the grade-specific process pages carry the detail: 304 stainless steel CNC machining and 316L stainless steel CNC machining.
Confirming the Grade You Actually Received
304 and 316 are visually indistinguishable. Color, sheen and the “feel” of the chip will not separate them, and neither will the tests that circulate in workshops. The following is what each form of evidence can and cannot establish.
| Evidence | What it proves | What it cannot prove |
|---|---|---|
| EN 10204 3.1 certificate | The heat’s composition and mechanical results, traceable to a named mill and a heat number | That the part in your hand came from that heat, unless the number is checked |
| Heat or lot number marked on the part or its packaging | The link between the physical part and the certificate | Anything at all if nobody reads the number |
| PMI by handheld XRF | Whether chromium, nickel and molybdenum are present — which separates 304 from 316 | Carbon. It cannot separate 304 from 304L, or 316 from 316L. |
| PMI by optical emission (spark OES) | Including carbon, so it can separate the L grades from the standard ones | Nothing beyond the spot it measured; it is a point test, not a whole-part test |
| A magnet | Nothing useful for this question | Both grades are austenitic, and machining makes either slightly magnetic |
| Spark testing | A very rough separation of alloy families at best | 304 from 316 reliably. It is not an acceptance method. |
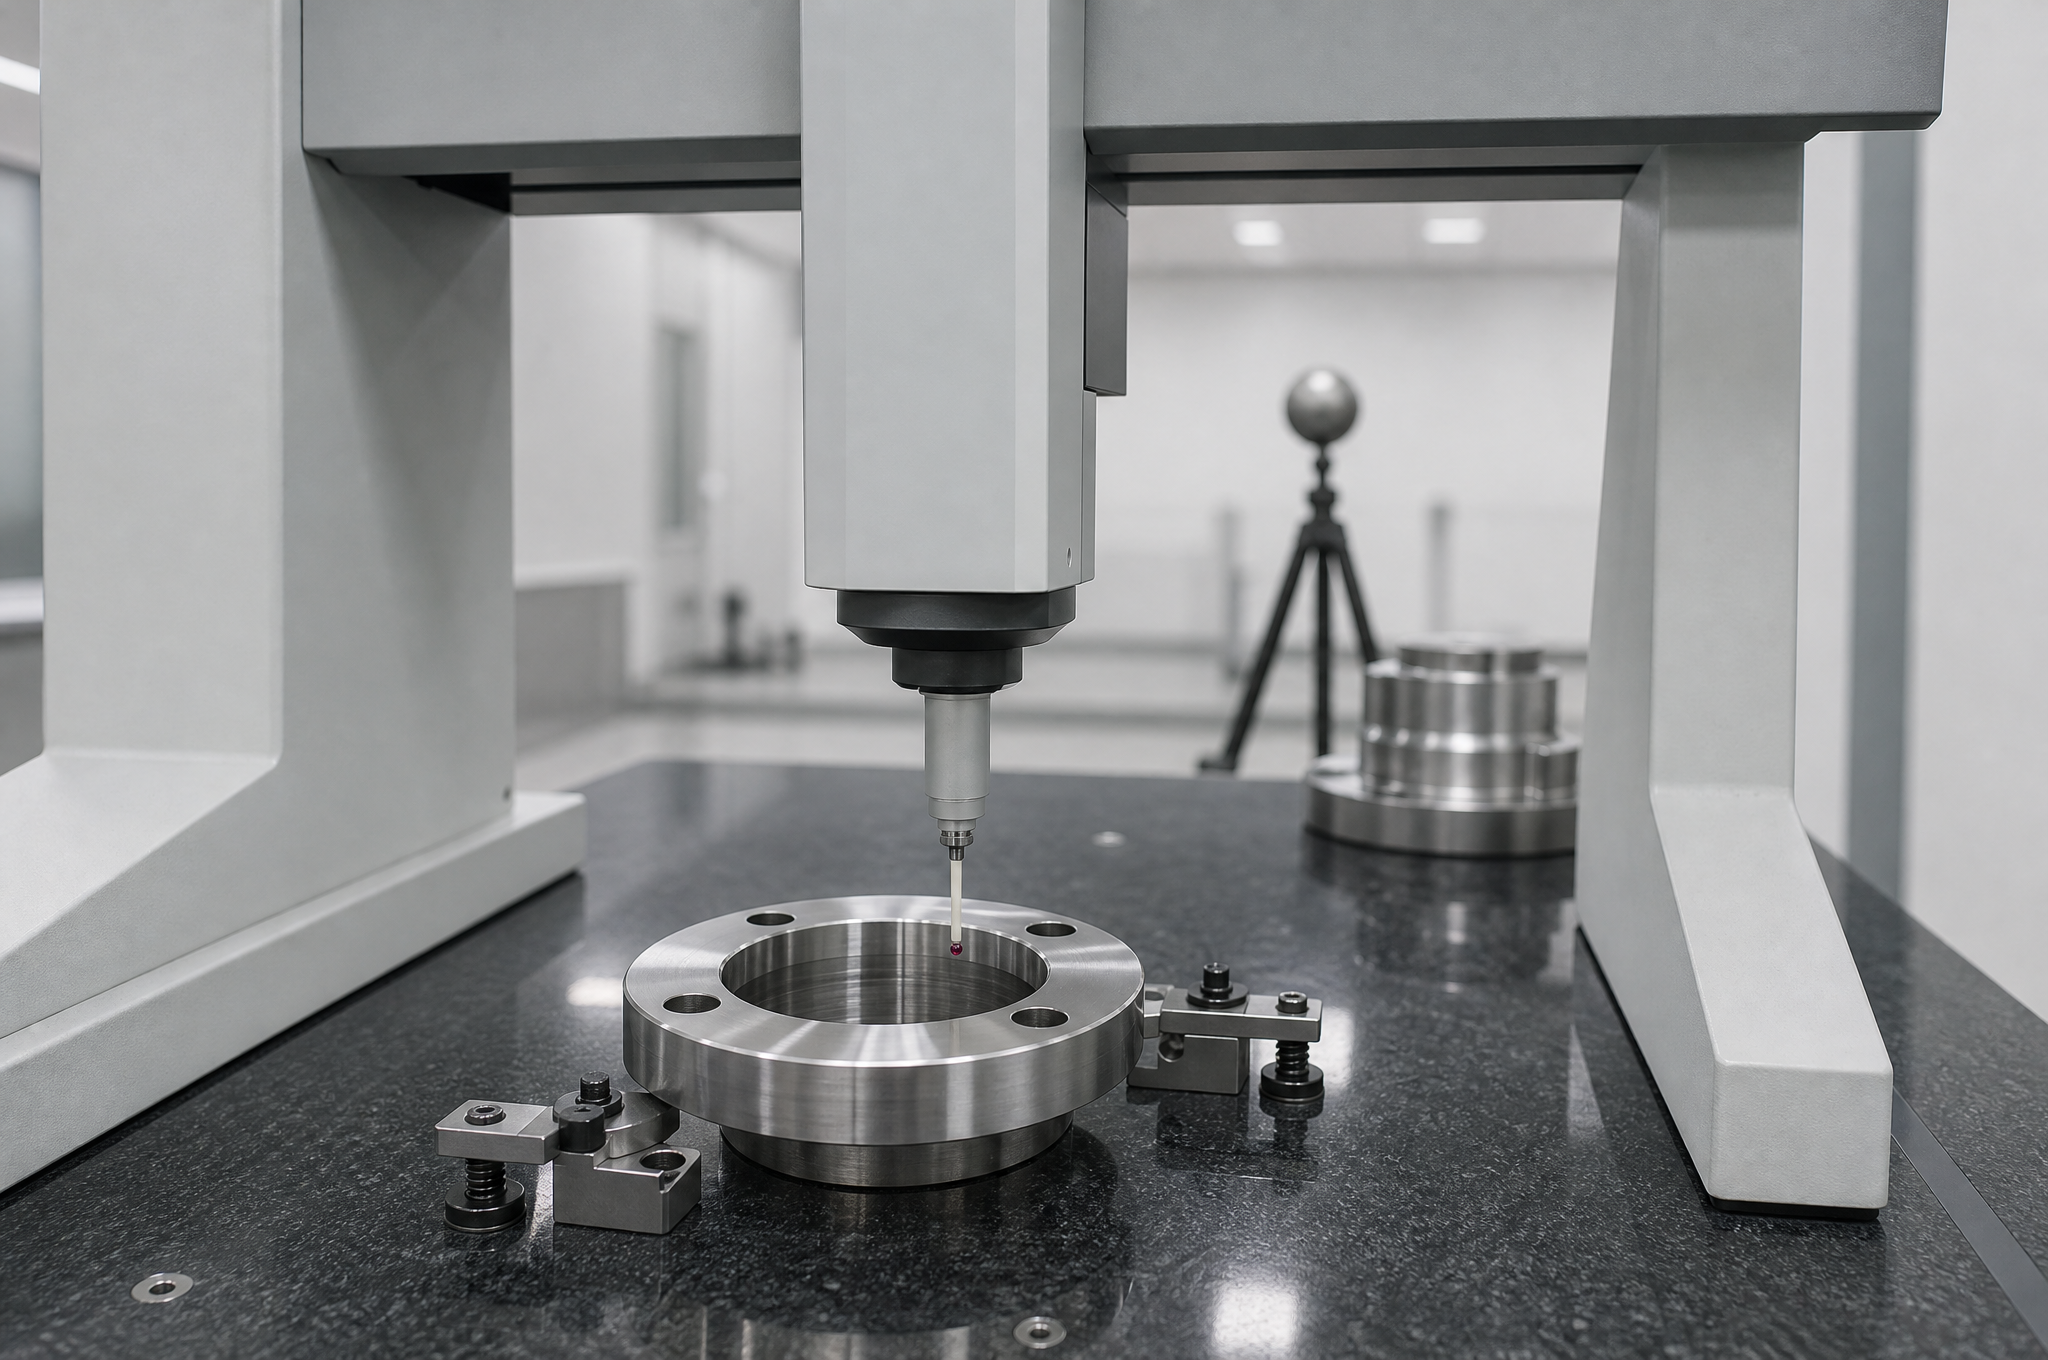
| Dimensional inspection report | The features that were measured, by the method used | Anything that was not measured, and nothing about the material |
| Specimen corrosion tests (ASTM G48 for pitting, ASTM A262 for intergranular attack) | How a specimen of that heat behaves in a defined laboratory test | The life of the part in your actual medium. These are comparative tests, not service predictions. |
The cheapest verification happens before the material arrives. Putting the grade, the governing standard, the condition and the certificate type on the purchase order costs nothing and resolves the argument permanently. If your specification also requires G48 or A262, raise it at RFQ: those are specimen tests run by a laboratory, they add lead time and cost, and they qualify the heat rather than the part.
What Drives the Price Difference Between the Two
316 carries a material premium over 304, and that premium moves with nickel and molybdenum surcharges rather than sitting at a fixed percentage. Anyone quoting a stable multiplier is quoting a snapshot. What does not move is the structure of the cost, and that structure is what a buyer should be comparing.
| Cost line | What actually moves it | Why the grade is only part of the answer |
|---|---|---|
| Raw material | Alloy surcharge on nickel and molybdenum, product form, cut length versus full bar, stock versus mill order | The 316 premium is a moving market number; it has to be quoted on the day, not remembered |
| Material yield | Bar diameter against the part envelope, and how much becomes swarf | Designing from the nearest stock size usually saves more than changing grade |
| Machining time | The process window and the hardest feature, not the grade name | Two shops can differ more on strategy than the two grades differ on machinability |
| Tooling | Wear rate, and the wear criterion the shop sets | The criterion is a decision: an over-tight one consumes inserts to no benefit |
| Fixturing and setups | Number of setups, soft jaws or a dedicated fixture | One additional setup frequently costs more than the material premium |
| Secondary operations | Passivation, electropolishing, mechanical polishing, marking | These are priced per part and per fixture load, not per kilogram |
| Inspection | Which features, by which method, with what report | A CMM report on ten features is a different product from a caliper check |
| Quantity | Setup amortisation, material buying, tooling amortisation | The same part at ten and at a thousand is two different prices |
The only meaningful comparison is the same geometry, the same drawing and the same inspection requirement quoted in both grades. Everything else compares two businesses rather than two alloys.
Where Each Grade Is Used, and Why
The “why” column is the useful one. It shows that the grade follows the environment even inside a single sector — and that the industry label alone decides nothing.
| Part or sector | Usual grade | Why — and the caveat |
|---|---|---|
| General machinery: guards, frames, shafts, brackets | 304 | No chloride exposure and no wetted surface; 316 buys nothing here |
| Pump and valve bodies, mild process water | 304 | Adequate until chloride content or temperature rises, and both creep up over a plant’s life |
| Food and beverage contact, cleaned in place | 304 or 316 | The cleaning chemistry decides, not the sector — see the note in Section 04 |
| Marine hardware above deck, rain-washed | 316 | Works because it is washed; the sheltered unwashed crevice on the same part is where it fails |
| Coastal architectural brackets and fixings | 316 | The fastener is often the first failure and is often a different, cheaper grade than the bracket |
| Chemical dosing skids, dilute acid transfer at ambient | 316, medium permitting | Dilute sulphuric at ambient is a different case from hot concentrated acid; get the medium assessed |
| Pharmaceutical and high-purity fluid path | 316L, often electropolished | The finish and the documentation carry most of the value and most of the cost |
| Semiconductor gas and vacuum components | 316L, electropolished | Inclusion content and surface finish matter more than the grade name |
| Exhaust and manifold hardware, hot section | Stabilised or higher grade for the hot zone | Sensitisation, not corrosion, is the failure mode; a 304 or 316 flange may still be correct |
| Medical instruments and sterilisation trays | 304 or 316, per the cleaning cycle | Repeated autoclave cycles plus chloride disinfectants are the real exposure, not the procedure |
What to Send With an RFQ
The list below is ordered by how much each item changes the answer. The first six resolve the grade; the rest resolve the price.
| Field | Why it changes the quote | What a complete answer looks like |
|---|---|---|
| Drawing, 2D and 3D | Geometry, tolerances and GD&T | STEP plus a PDF with the tolerance block and datums |
| Grade | Material and cost | 316L |
| Standard and product form | What the mill must certify, and what chemistry is permitted | ASTM A479 bar |
| Condition | Machining behavior and strength | Annealed, cold drawn |
| Medium and concentration | The grade decision itself | 5% sodium chloride solution, continuous |
| Process and cleaning temperature | The number that most often changes the answer | Process 40 °C; CIP 80 °C for 30 minutes, daily |
| Crevice inventory | Where pitting actually starts | Two O-ring grooves, one blind M6 tapped hole |
| Surface finish, and where | Process time and secondary operations | Ra 0.8 µm on the seal face, 3.2 µm elsewhere |
| Post-treatment | A separate operation with its own lead time | Passivated to ASTM A967, nitric family |
| Documentation | Inspection time and administrative cost | 3.1 certificate, first article report, CMM report on eight features |
| Quantity and forecast | Setup and material buying | 50 pieces now, 200 per year forecast |
| Delivery and destination | Scheduling and freight | Six weeks, FOB Xiamen |
If the grade is genuinely undecided, say so and send the medium, the temperatures and the crevice list. A selection decision taken with those three facts is worth more than a grade guessed from an industry name.
Frequently Asked Questions
What is the main difference between 304 and 316 stainless steel?
Is 316 stainless steel harder to machine than 304?
Should I use 304 or 316 for marine CNC parts?
What is the difference between 304 and 304L?
Does 316 always cost more to machine than 304?
Can 304 stainless steel be passivated?
How can I confirm whether a CNC part is 304 or 316?
Is 316 stainless steel food safe?
Why does 316 stainless steel sometimes rust?
Can 304 and 316 be machined to the same tolerance?
Send the Part, the Medium and the Requirement
If the grade is still open, send the drawing, the medium, the process and cleaning temperatures, and the crevices you know about. We will review the geometry for machinability, confirm the grade against the exposure, and quote the same part in both where the answer is close.
Request a Stainless Steel QuoteDrawing review before quotation, typical reply within one working day
Explore CNC Machining Capabilities →