How Much Does an Injection Mold Cost in China?
A budgeting guide to injection mold cost in China: what drives the price, what a quote includes, how to compare suppliers on the same basis, and how to separate one-time tooling cost from total program cost.
At a glance
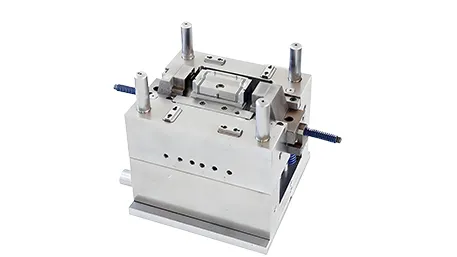
The cost of an injection mold in China depends on part geometry, mold size, cavity count, steel grade, required tool life, surface finish and validation scope. As an initial budgeting reference, simple prototype or bridge tools may fall around US$1,000–5,000, while production tooling commonly starts in the several-thousand-dollar range. Multi-cavity, hot-runner, two-shot or high-precision molds can cost tens of thousands of dollars or more. These are preliminary market references, not a supplier quotation. To compare prices accurately, confirm what each quote includes — mold design, steel and machining, trial samples, correction rounds, inspection, mold ownership and shipping.
What does an injection mold cost depend on?
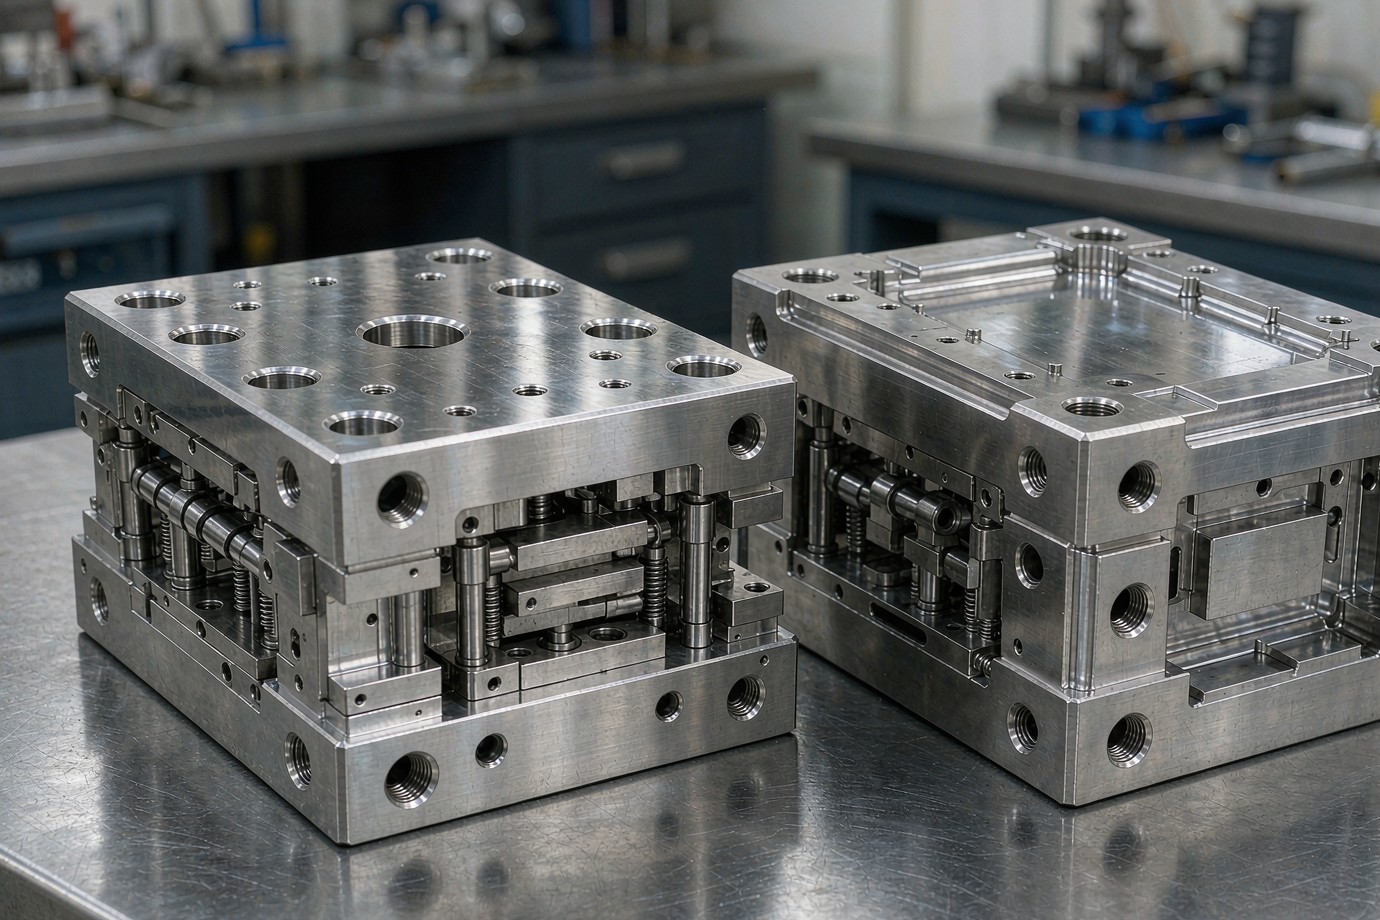
Two molds that look similar can differ in price several times over. The cost is set by a small number of engineering choices. For each driver below, the useful question is not only "what is it" but "do I actually need it for my volume, or can it be optimized."
| Cost driver | What it is | How it changes cost / when to optimize |
|---|---|---|
| Part geometry & size | Overall envelope, wall thickness, undercuts, fine detail | Larger or more intricate parts need more steel and machining; simplifying geometry is the biggest single lever |
| Cavity count | How many parts the tool makes per cycle | More cavities raise tooling cost but lower cost per part; choose from annual volume, not first order |
| Steel grade & tool life | Mold steel hardness, wear resistance, target shot count | Harder steels cost more but last longer and hold tolerance; match steel to volume and resin |
| Runner system | Cold runner vs. hot runner | Hot runners add cost and a controller but reduce scrap at volume; cold runners are cheaper upfront |
| Actions & mechanisms | Sliders, lifters, unscrewing, collapsible cores | Each moving mechanism adds design, machining and maintenance; remove only where the part allows |
| Surface finish | Polish grade, texture, high-gloss or matte zones | High finish and texture add polishing and EDM time; finish only the surfaces that matter |
| Dimensional tolerance | Tight tolerances on critical features | Over-specifying tolerance raises machining and inspection cost; set tight tolerance only where needed |
| Trial & correction scope | Number of trial (T0/T1) rounds and correction cycles | Agree how many trial and correction rounds are included; extra rounds are often billed separately |
| Validation & documents | Dimensional reports, capability studies, customer qualification | Deeper validation and formal packages add cost; align the scope to your industry and customer needs |
| Lead time & load | Tool build schedule and expedite | Expedited builds and high shop load can raise price; plan lead time into the program, not as a rush |
For the mold types, steel options and tooling structures behind these factors, see our custom plastic injection mold page and our mold making process in China.
Injection mold cost in China by tooling type
Because "how much" is the starting question, the table below gives an initial budgeting range by tooling class. Treat it as a way to place your project in the right neighborhood before you request a formal quote.
| Tooling type | Initial budget reference (USD) | Typical assumptions |
|---|---|---|
| Prototype / bridge tool | $1,000–$5,000 | Low-volume validation; aluminium or pre-hardened steel; limited tool life |
| Simple single-cavity production tool | $3,000–$9,000 | Simple geometry, cold runner, standard surface requirement |
| Medium-complexity single-cavity steel tool | $6,000–$18,000 | More complex structure, machining, polishing or tool-life requirements |
| 4–8 cavity production tool | $9,000–$40,000+ | Multi-cavity build; cost set by size, layout, balance and run requirements |
| High-complexity or high-life tool | $18,000–$70,000+ | Hot runner, sliders/lifters, unscrewing, two-shot/overmold, precision or special finish |
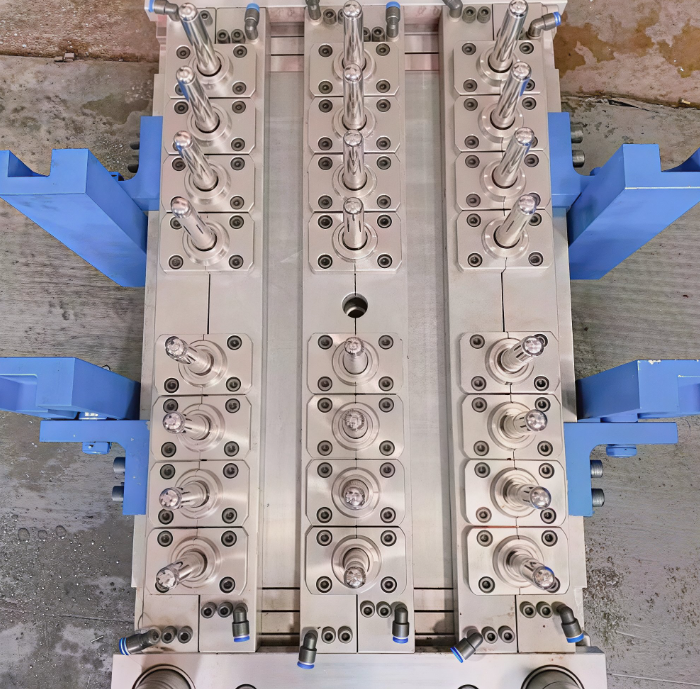
What is included in a China injection mold quote?
Quote scopes are not standardized. Two suppliers can quote very different totals for the same part simply because they include different things. Read the scope, not just the number.
Mold design, steel & mold base, CNC/EDM machining, polishing, assembly, T1 trial, sample parts, dimensional report, agreed correction rounds
Freight & shipping, hot-runner controller, extra correction rounds, special inspection (e.g., extended CMM), spare parts & maintenance, export documentation
Before you compare, confirm in writing what the quote covers: how many trial and correction rounds, what inspection and reports are provided, whether the hot-runner controller is included, and what is excluded. This is the single fastest way to avoid a low headline price that grows later.
Why do injection mold quotes differ so much?
Send the same CAD file to several suppliers and you will get a spread of prices. Most of that spread is not quality — it is different assumptions. Before comparing the bottom line, align these items so you are comparing the same tool:
- Cavity count — is everyone quoting the same number of cavities?
- Steel grade & tool life — which steel, and for how many shots?
- Runner system — cold or hot runner, and is the controller included?
- Surface & finish — polish grade, texture, and which zones.
- Sampling & correction — how many T1 samples and correction rounds are in scope?
- Inspection & reports — what dimensional reporting is provided?
- Ownership & delivery — who owns the mold, and on what delivery terms?
Once the configuration matches, a genuine price comparison is possible. To extend this into supplier screening and risk, see our guide on how to choose an injection molding supplier in China.
How to reduce mold cost without creating production risk
Lowering tooling cost is legitimate — but the wrong savings move risk into production. Optimize the design and the tooling plan, not the quality controls.
- Remove unnecessary mechanisms. Eliminate sliders, lifters and undercuts where the part design allows.
- Right-size the cavity plan. Match cavity count to realistic annual volume instead of over-building for a first order.
- Choose the runner by volume. A cold runner lowers upfront cost; a hot runner pays back at volume through less scrap.
- Zone the surface finish. Apply high polish or texture only where it is visible or functional.
- Set achievable tolerances. Tighten only the critical dimensions, not the whole part.
- Match tool class to demand. A bridge tool for validation, a production tool for volume — do not force one to do the other.
Mold tooling cost vs. total program cost
The mold is a one-time investment; the molded parts are a recurring cost. A mold quote is not the total program cost, and the per-part molding cost is a separate line driven by material, cycle time and machine time.
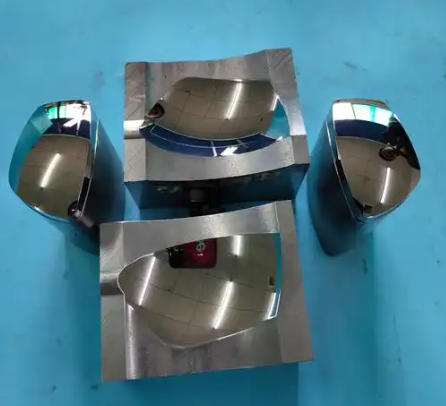
A practical way to see the tooling trade-off is to spread the one-time mold cost across the parts it produces:
What information do you need for an accurate mold quote?
A precise price needs a precise input. The more of this you can provide, the narrower — and more reliable — the range becomes:
- 3D CAD model — STEP or IGES of the final part geometry.
- 2D drawing — with critical dimensions, GD&T and tolerances called out.
- Resin grade — material family, grade, colour and any filler or additive.
- Volume — first-order quantity and expected annual volume.
- Tool life — target shot count and how long the tool must run.
- Surface & appearance — finish, texture and any cosmetic requirements.
- Market & compliance — end use, target market and any quality files or customer requirements.
- Delivery — destination and preferred Incoterms, plus timing.
If the design is not final, share the preliminary geometry and a volume range. That supports an initial assessment, but be clear it is not a fixed price until the drawing and requirements are confirmed. When you are ready, request a project-specific injection mold quote.
Frequently asked questions
How much does an injection mold cost in China?
Why do injection mold prices vary so much for the same part?
What is the difference between mold cost and molding cost?
Single-cavity or multi-cavity mold - which is more cost-effective?
How does steel grade affect mold cost and tool life?
What is normally included in a China injection mold quote?
Do I own the mold, and can I move it to another supplier?
How long does an injection mold take to make in China?
When is a prototype or bridge mold a good choice?
What information do you need for an accurate mold quote?
How we quote a mold
We would rather give you a defensible range than a headline number that moves. When you request a mold cost estimate from us:
- We separate one-time tooling from the recurring per-part price, so nothing is hidden in the mold line.
- We state the assumed cavity count, steel grade, runner system, tool life and surface scope behind the number.
- We confirm trial and correction rounds, inspection and reports, mold ownership and delivery terms in writing.
- Mold making, engineering review and dimensional inspection are performed in-house under one ISO 9001:2015 system; some surface finishing is handled by qualified partners under our quality control.
Send your 3D CAD model, 2D drawing, resin grade and expected volume, and we will quote the mold scope against the agreed specifications — or tell you plainly what still needs to be confirmed first.
Get a project-specific injection mold cost estimate
Send your 3D CAD model, 2D drawing, resin grade and expected production volume. We will review the tooling requirements and quote the mold scope against the agreed specifications.
Get a Project-Specific Mold Cost EstimateNot all project details are finalized? Share the information available so far and identify the items that still need confirmation.