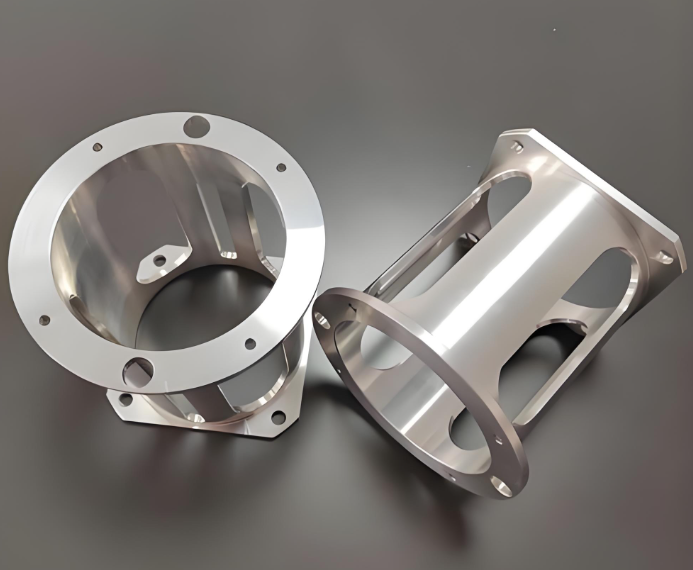
Precision CNC machining of stainless steel and titanium components from your drawings. We work with 304, 316L, 17-4 PH and Ti-6Al-4V, with grade-specific process control, dimensional inspection and material documentation.
At a Glance
Stainless steel is chosen for corrosion resistance and durability at moderate weight; titanium is chosen when strength-to-weight and corrosion resistance justify the higher cost. Both are CNC-machined from your drawing, but they machine very differently. Stainless work-hardens; titanium runs hot and wears tools faster. We adjust tool engagement, workholding and cooling to the grade and geometry, not to a generic cutting-parameter table.
Stainless Steel vs Titanium: At a Glance
The material name is only the starting point. Your grade, standard, stock form, condition, geometry and documentation requirements determine the manufacturing route. The table below is a starting point for comparison, not a verdict.
| Factor | Stainless steel | Titanium |
|---|---|---|
| Corrosion resistance | Good to excellent, grade-dependent | Excellent in many environments |
| Weight | Denser (~7.9 g/cm³) | About 45% lighter (~4.5 g/cm³) |
| Strength-to-weight | Good | Excellent |
| Machining difficulty | Grade-dependent; work-hardening on austenitic grades | Typically higher; low thermal conductivity, tool wear |
| Material cost | Lower for common grades | Higher |
| Typical buyer driver | Corrosion, durability, cost | Weight, performance, biocompatibility |
Stainless or Titanium? Choose by Application
Corrosion at moderate weight
Weight is not the primary concern, corrosion resistance is required, and 304 or 316L provides adequate performance. Lower material and machining cost.
Weight reduction matters
Strength-to-weight ratio, biocompatibility or severe corrosion justifies the higher material and machining cost. Common in aerospace, medical and motorsport.
Stainless Steel CNC Machining
Stainless steel is selected when corrosion resistance, mechanical strength, hygiene or temperature performance outweigh cost. We machine the grades most often called out on industrial drawings:
General-purpose
Good corrosion resistance and formability. Used in housings, brackets, food equipment and general machinery where 316L is not required.
Higher corrosion resistance
Molybdenum-alloyed for chloride and chemical resistance. Common in marine, pharmaceutical, food processing and medical hardware.
Precipitation-hardened
High strength and hardness after heat treatment. Used in shafts, valve components and high-load structural parts. Specify the condition (H900, H1025, etc.).
Why Stainless Machining Needs Process Control
Not all stainless is equally easy to machine. 303 cuts more freely than 316L; 17-4 PH in the hardened condition behaves differently from annealed stock. The risk areas:
Austenitic grades (304, 316) harden if the cutter rubs rather than cuts.
Stainless does not dissipate heat like mild steel.
Long, stringy chips in deep pockets or bores can recut and damage the surface.
Titanium CNC Machining
Titanium is selected for high strength-to-weight, corrosion resistance and biocompatibility. The grades we most often machine:
Commercially pure
Good ductility and corrosion resistance, lower strength. Used in chemical processing and where formability matters more than high strength.
The workhorse alloy
The most widely used titanium alloy. Heat-treatable, high strength-to-weight. Common in aerospace brackets, medical components and motorsport.
Extra low interstitial
Tougher and more ductile than Grade 5. Used in medical and specialized applications where fracture toughness matters.
Why Titanium Is Harder to Machine
Heat stays at the cutting edge instead of flowing into the chip.
Titanium can weld to the cutting edge under poor conditions.
Titanium is springy and cuts with high radial force.
5-Axis Titanium Machining
Not every titanium part needs 5-axis. It becomes useful when the geometry requires multi-face access, angled holes, deep pockets or contoured surfaces where a long, slender tool would deflect. Tilting the spindle keeps the cutter short and rigid, and reduces re-fixturing that can move the datum between setups.
Grade, Standard, Stock Form and Condition
These four terms are not interchangeable. A complete material callout on the drawing should specify all four:
| Term | What it means | Example |
|---|---|---|
| Grade / alloy | The material composition | 316L, 17-4 PH, Ti-6Al-4V |
| Standard | The procurement specification | ASTM A276, ASTM B348, AMS 4928 (confirm matches stock form) |
| Stock form | How the raw material arrived | Bar, plate, tube, billet, forging |
| Condition | Heat-treated or annealed state | Annealed, H900, H1025, solution-treated + aged |
Material Traceability & Documentation
A material certificate proves the raw stock meets its specification. A part inspection report proves the finished component meets the drawing. They are different documents, and both matter for medical, aerospace and regulated projects.
| Document | What it confirms |
|---|---|
| Material certificate / MTR | Heat/lot, chemistry and mechanical properties of the incoming stock |
| Dimensional inspection report | Critical features measured against the released drawing revision |
| FAI | First-article inspection where the project requires it |
Surface Finishing by Material
Passivation, electropolishing, polishing, bead blast
CNC machining is in-house; selected finishing processes are managed through qualified partners to your specification.
Anodizing, bead blast, polishing, cleaning
Finish options depend on grade and application. Confirm the required finish on the drawing — passivation or plating suitability is checked per project.
Applications by Material
| Industry | Stainless steel | Titanium |
|---|---|---|
| Medical | 316L housings, surgical hardware | Grade 5 / Grade 23 components |
| Aerospace | Selected structural fittings | Grade 5 brackets, lightweight components |
| Marine / chemical | 316L valves, fittings, hardware | Corrosion-resistant components where weight matters |
| Food / pharma | Process equipment components | Project-specific |
| Motorsport / industrial | Shafts, brackets, housings | Lightweight high-performance parts |
What to Specify in a Stainless or Titanium RFQ
The more completely the RFQ describes the material and application, the fewer surprises later. Send:
Material
- Exact grade (304, 316L, 17-4 PH, Gr5, etc.)
- Standard and stock form
- Condition / heat treatment
- Material certificate requirement
Part & project
- 3D CAD + 2D drawing, revision noted
- Critical dimensions, GD&T, surface finish
- Quantity (prototype / annual / per batch)
- Application environment and inspection level
Two Materials, Two Machining Approaches
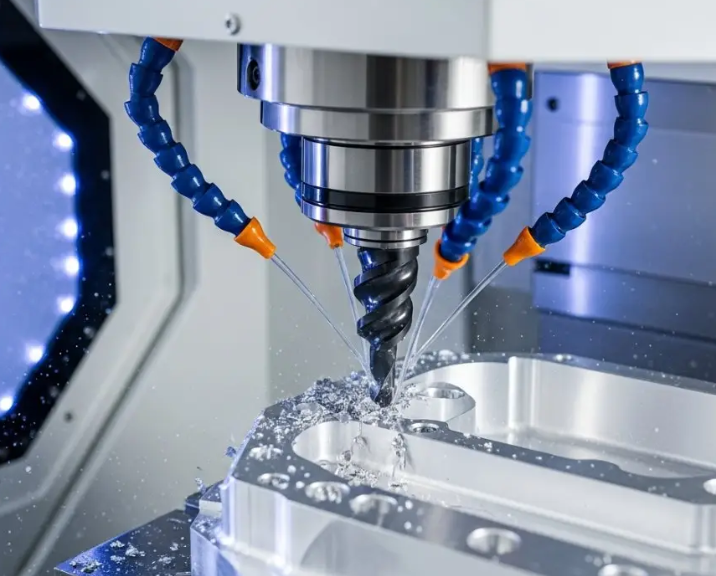
- Material316L stainless, annealed bar
- Process3-axis milling + tapping
- ChallengeWork-hardening, chip control
- FinishPassivation where specified
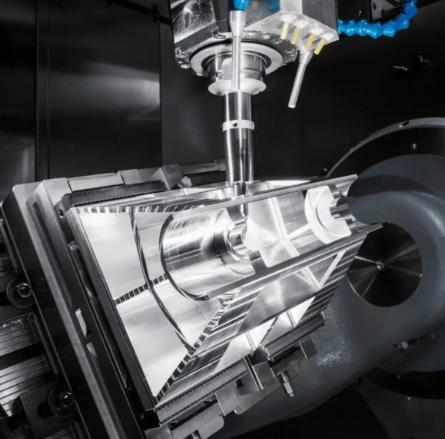
- MaterialTi-6Al-4V Grade 5
- Process5-axis milling
- ChallengeHeat, tool wear, thin sections
- InspectionCMM on critical datums
Frequently Asked Questions
What stainless steel grades can you CNC machine?
What titanium grades can you machine?
Is 17-4 PH difficult to machine?
Does titanium always need 5-axis machining?
Can you provide material certificates (MTR)?
What tolerances are achievable on stainless and titanium?
Can 316L be passivated after CNC machining?
Stainless or titanium — which should I choose?

Request a Stainless or Titanium CNC Quote
Send your CAD, drawing and required material grade. We will review geometry, grade, workholding and inspection scope, and come back with a machining approach and lead time.
Xiamen Goldcattle · Manufacturing since 1998 · 3/4/5-axis CNC · CMM inspection on qualified features · Material certificates where supplied