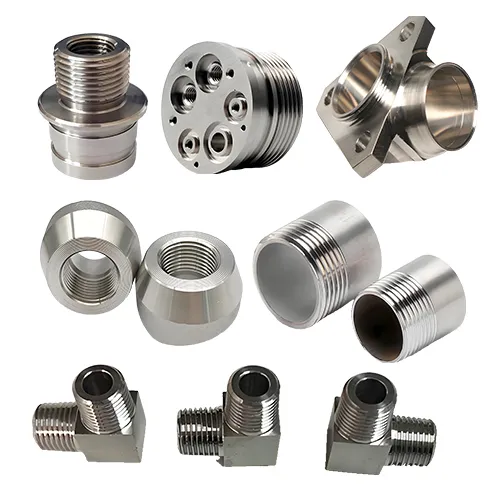


CNC Threaded Blocks | Stainless & Aluminum OEM
Place of Origin : XiaMen, China
Brand : JSD
Model : CNC-43
Material : Customer’s request
Process : CNC machining
Product Name : Professional Precision CNC Machining Parts
Surface treatment : Customer requirements
Service : Customized OEM CNC machining
Equipment : CNC machining center
Application : Industrial equipment
Color : Custom color
Size : Customized size
Description
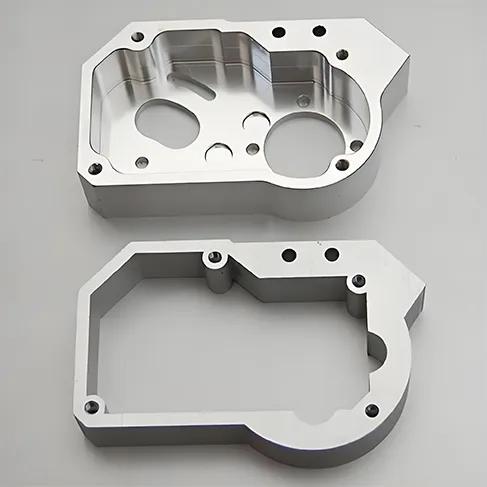
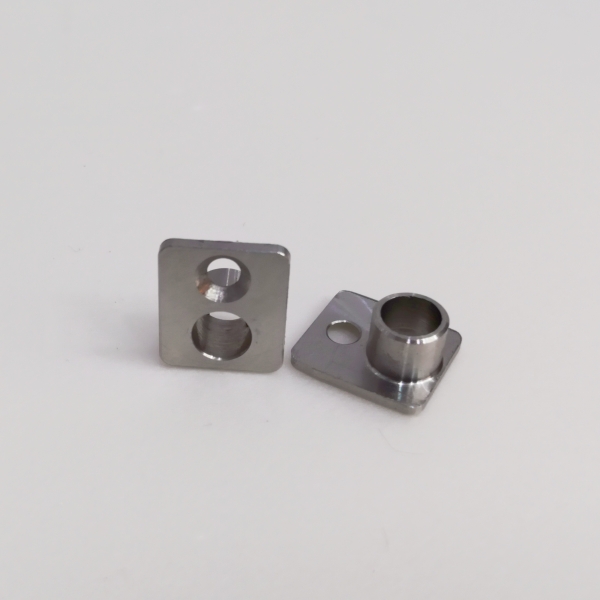
Custom CNC Machined Threaded Blocks
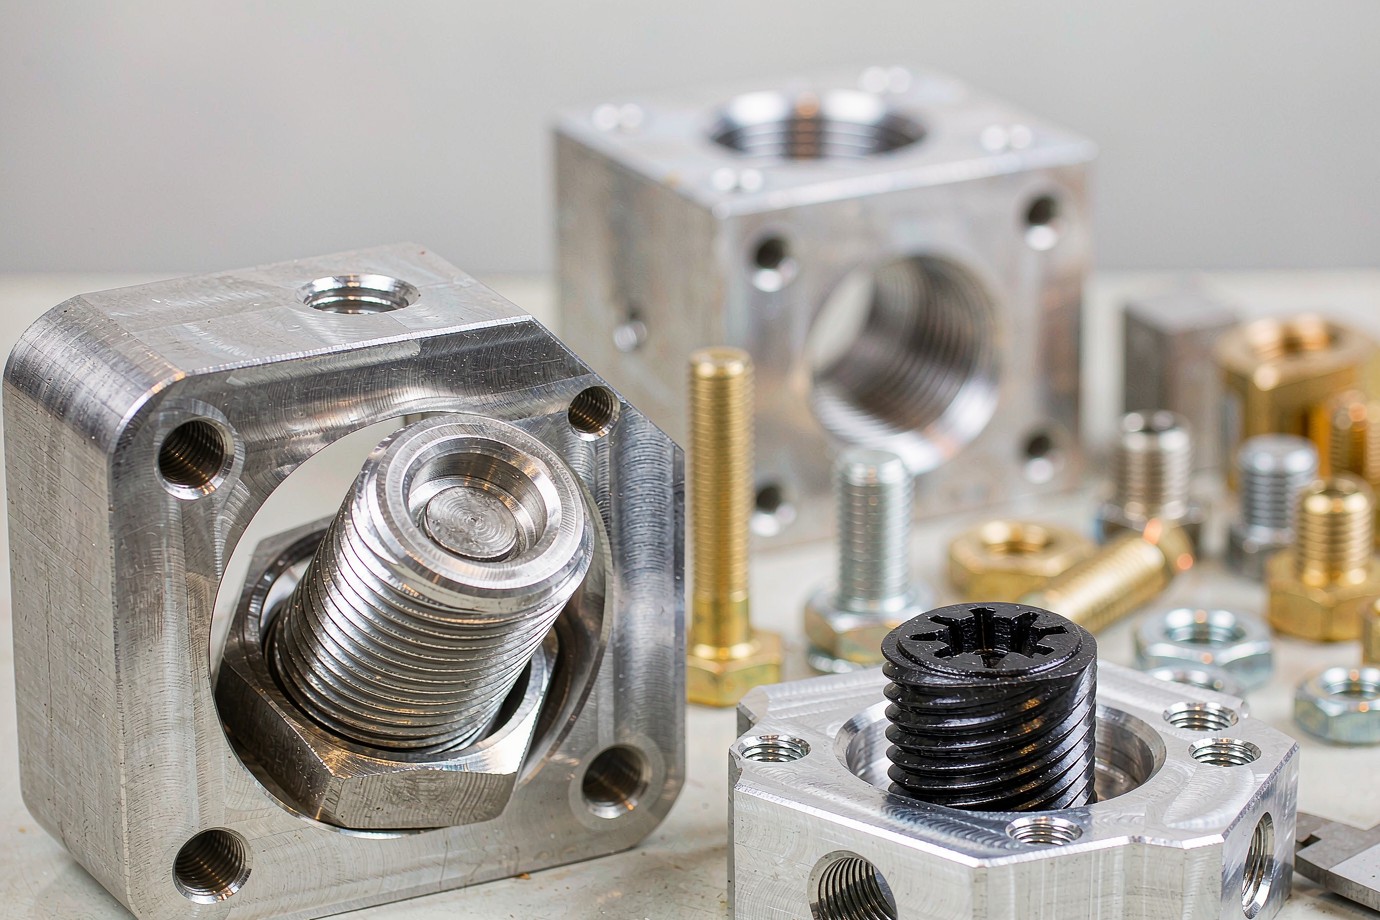
Metal threaded blocks machined from your drawings in aluminum and stainless steel — with tapped holes, counterbores, milled faces and other features cut to the approved drawing, then inspected for thread, hole position and critical dimensions.
Drawing-based threaded blocks for equipment that has to bolt together
Xiamen Goldcattle provides drawing-based CNC machining for custom metal threaded blocks made from specified aluminum alloys and stainless steels. These components can be manufactured with customer-defined dimensions, drilled holes, tapped holes, counterbores, milled surfaces and other machined features according to the approved drawing. For threaded block projects, important manufacturing details include thread size and pitch, thread tolerance, effective thread depth, hole position, datum relationships, surface finish and the fit with mating components. Material and machining methods are selected according to the part geometry, mechanical requirements, operating environment and production quantity. Dimensional and thread inspection can be arranged according to the agreed quality requirements.
The threaded block is a functional interface — a block, boss or seat that lets two larger assemblies meet, carry load and be serviced. We cut its thread class, bore position and mating-face flatness against the same datum as the rest of your assembly, so the part drops in rather than being forced in.
| Threaded block type | Typical structure |
|---|---|
| Blocks with tapped holes | Internal threads, plain or patterned, through or blind |
| Threaded mounting blocks | Mounting face, tapped holes and locating holes |
| Threaded connection blocks | Threaded interface and joining face between modules |
| Multi-hole positioning blocks | Multiple holes with positional relationships and datums |
| Custom CNC machined blocks | Slots, steps, counterbores and irregular features |
We confirm the actual form from your drawing. The types above describe the range we machine, not a fixed catalog — send the part and we quote to it. For our broader range of non-standard threaded hardware, see custom OEM hardware parts.
Stainless steel and aluminum, chosen for the joint
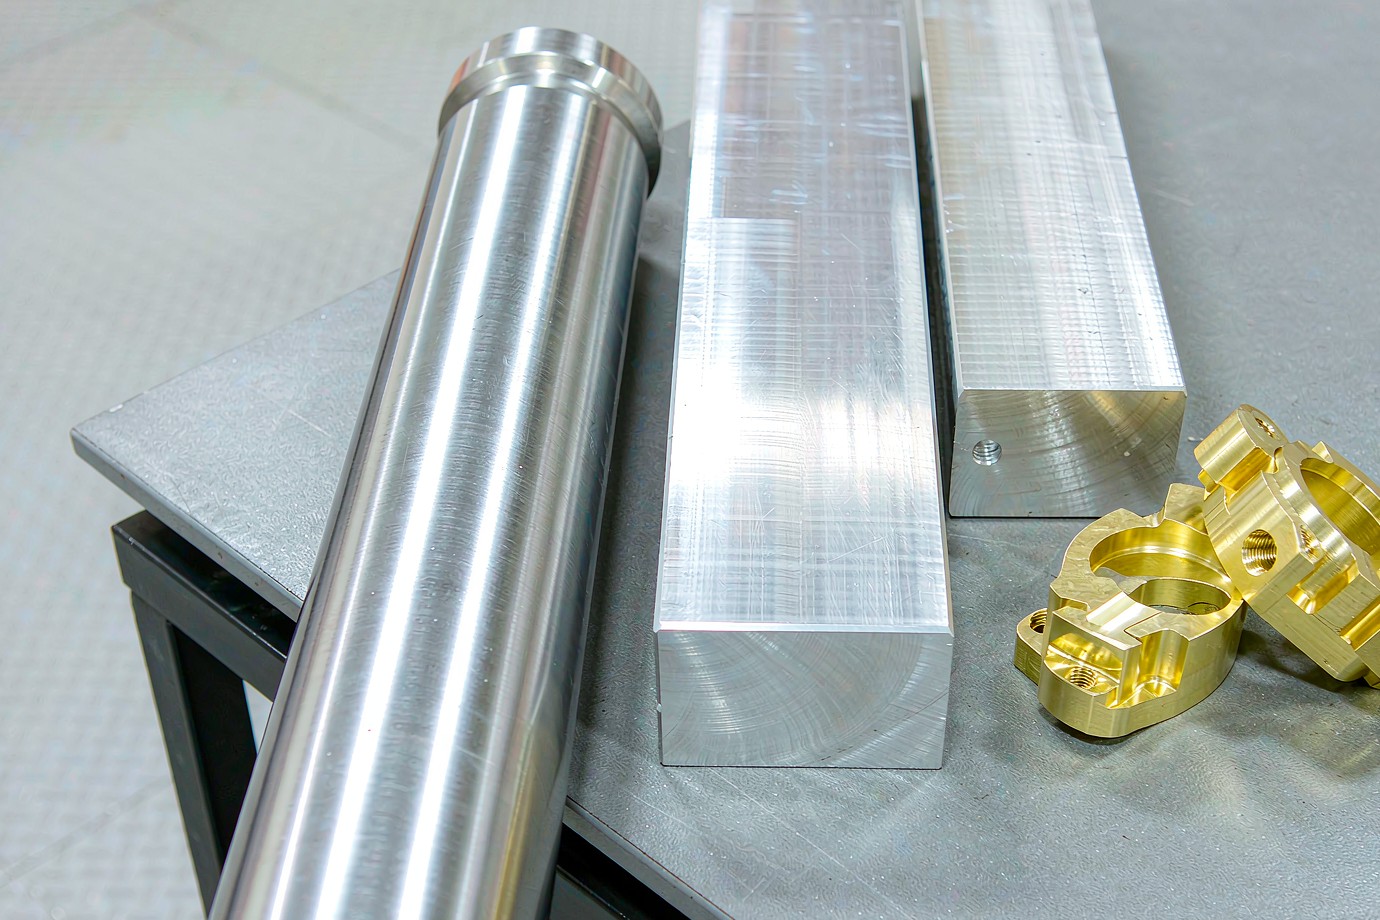
Threaded connection components live or die on material: corrosion resistance, galling behaviour and weight all start with the grade. We machine the alloys below most often and review others against your drawing.
| Material | Typical considerations | What we emphasise |
|---|---|---|
| Aluminum 6061-T6 | General structural blocks, mounting blocks, lightweight parts | Machinability, weight, finish and dimensional control |
| Aluminum 7075-T6 | Parts with specific strength-to-weight needs | Temper, machining distortion, environment and cost |
| Stainless Steel 304 | General industrial metal joints | Corrosion environment, finish and surface state |
| Stainless Steel 316 / 316L | More corrosive industrial environments | Media, temperature, corrosion condition and material certificate |
| Other specified alloys | Other materials on your drawing | Confirm standard, temper and machinability before quoting |
| Material | Surface finishes considered | Note |
|---|---|---|
| Aluminum | Anodizing, sandblasting, brushing, polishing | Anodizing thickness, colour and thread masking |
| Stainless steel | Passivation, polishing, brushing, electropolishing | Grade, roughness and corrosion environment |
| Steel | Black oxide, zinc plating, nickel plating | Coating thickness, dimensional compensation, corrosion need |
Finish and thread fit: where anodizing, plating or other surface treatments are specified, thread fit and critical mating dimensions should be reviewed together with the finishing process. Masking or dimensional allowance may be required for selected features. Only treatments we can actually deliver are listed; some are coordinated through audited external partners, with certificates available on request.
Grade note: the grades above are illustrative of typical work, not an exhaustive catalog. If your drawing specifies another alloy, send it over and we confirm machinability and stock lead time per project. The full material list is on our materials hub.
Thread types and machining requirements
Thread quality is decided by method and by the callout on your drawing, not by machine brand. Tell us the full thread designation — not just "M6" or "1/4 inch" — so class, pitch and engagement are correct.
| Thread type | What to specify |
|---|---|
| Metric thread | Diameter, pitch and tolerance class (e.g. M6 × 1 – 6H) |
| UNC (Unified coarse) | Diameter, threads per inch and class (e.g. 1/4-20 UNC-2B) |
| UNF (Unified fine) | Diameter, threads per inch and class |
| Internal thread / tapped hole | Tap drill size, thread depth, effective engagement length |
| External thread | Major diameter, pitch, tolerance and fit |
| BSP / NPT | Only where the part is genuinely a pipe-interface component |
Fast for holes
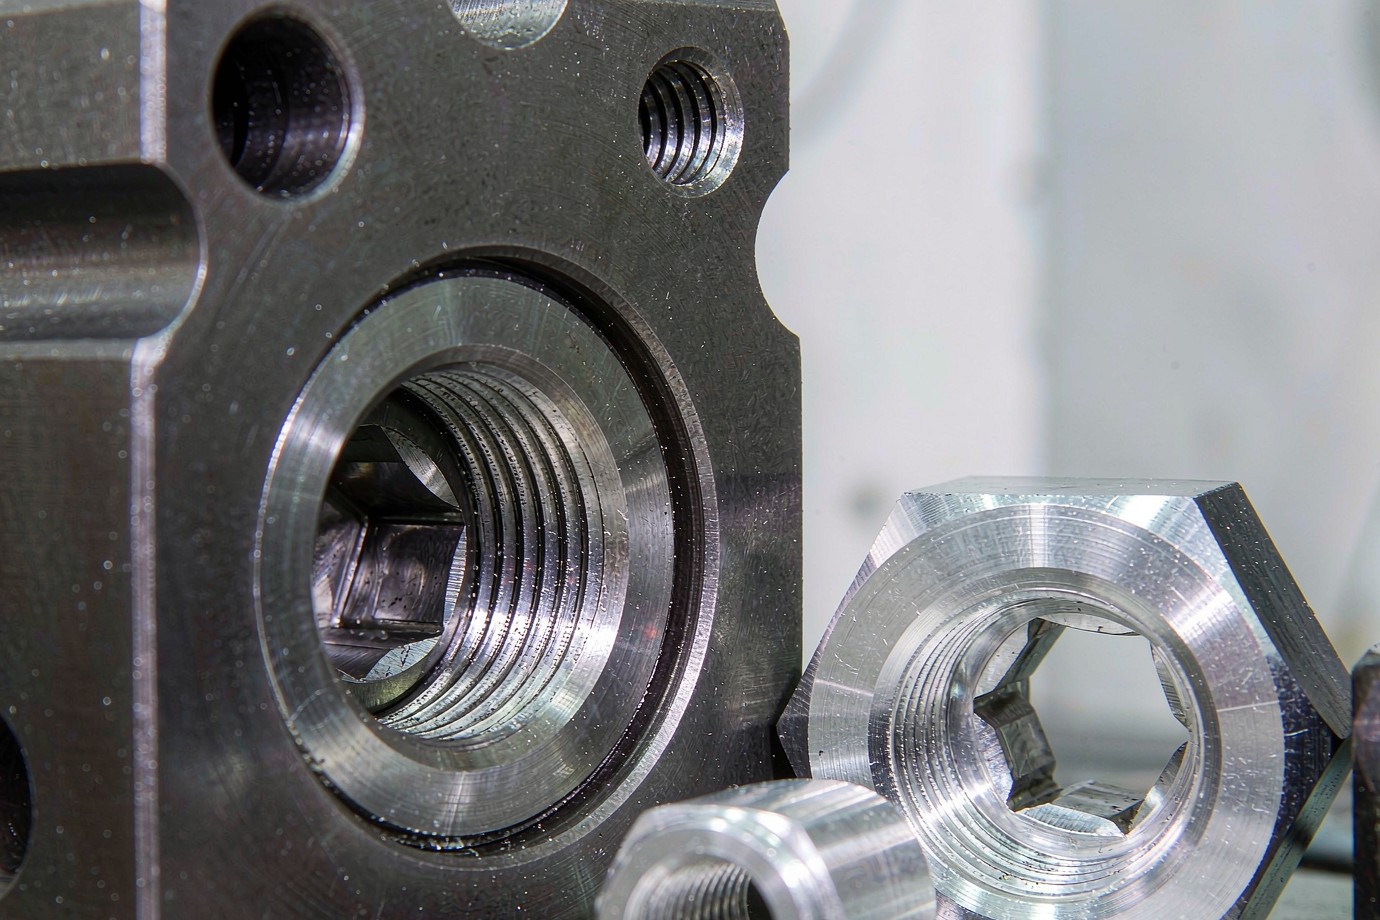
Through and blind tapped holes at volume; rigid tapping with the right lubricant to protect the thread.
Flexible & gentle
One tool covers many sizes, and the interpolating cutter reduces work-hardening on stainless — lower galling risk.
External & large
External threads and larger diameters turned on the lathe to the class on the drawing.
Repairable threads
Seats for wire-thread inserts where the joint is high-cycle or in soft material and must stay serviceable.
| Standard | Common class | Where used |
|---|---|---|
| Metric — ISO 68 / ISO 965 | 6H (internal), 6g (external) | General equipment, EU/Asia supply |
| Unified — ASME B1.1 (UNC / UNF) | 2B (internal), 2A (external) | North American equipment |
| Customer-specified | Per drawing | Fine-pitch, left-hand, or special |
Before quoting a thread, confirm: internal or external; thread size and pitch; thread tolerance class; thread depth; blind or through hole; required engagement length; mating screw / fastener; chamfer and thread entrance; and the inspection required. M6 × 1 – 6H and 1/4-20 UNC-2B are only notation examples, not a claim that every size is on hand.
Reference basis: thread and feature dimensions are confirmed against your drawing together with ASME Y14.5-2018 / ISO 22081:2021 as applicable. ISO and ASME are related but not interchangeable, so the drawing states which standard applies.
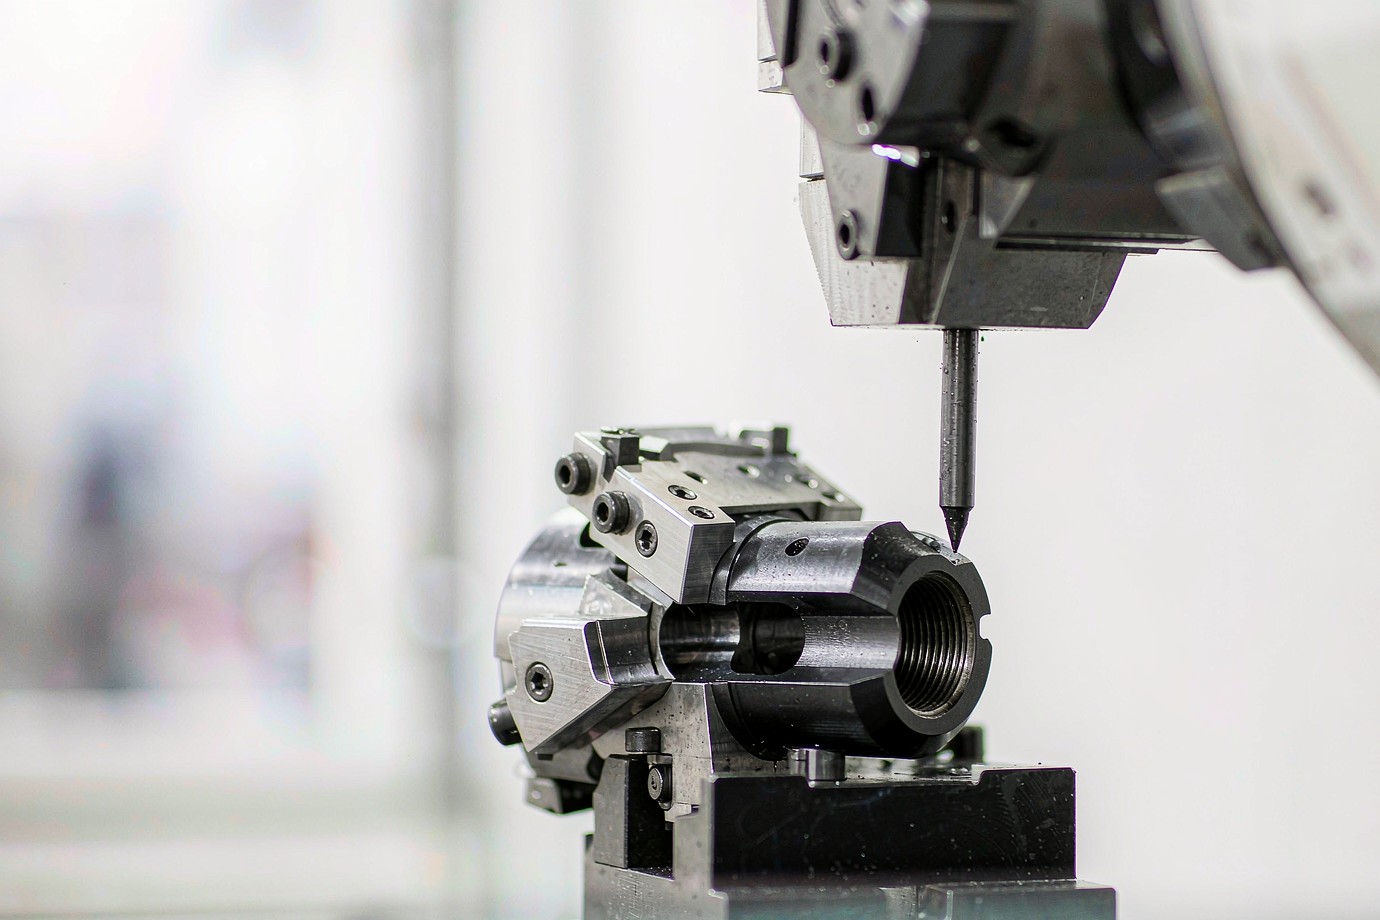
CNC milling, drilling and tapping
One floor, one quality system — so the threaded block and the parts it joins are made to the same standard.
| Operation | Role on the part |
|---|---|
| Face milling | Establishes the machining face and assembly datum |
| Pocket milling | Recesses, cavities and cleared volumes |
| Drilling | Through holes and tap-drill preparatory holes |
| Tapping | Creates the internal thread |
| Thread milling | Chosen by structure and thread requirement |
| Counterboring / countersinking | Seats for screws and fasteners |
| Reaming | Sizing of specific precision bores |
| Deburring | Removes edge, hole-mouth and cross-hole burrs |
Material prep
Cert-verified bar cut to blank.
Mill & drill
Face, bore and feature stock removal.
Threading
Tap, mill or single-point.
Deburr
Edge break and clean threads.
Inspect
Gauges + CMM position.
Finish
Passivate / coat per spec.
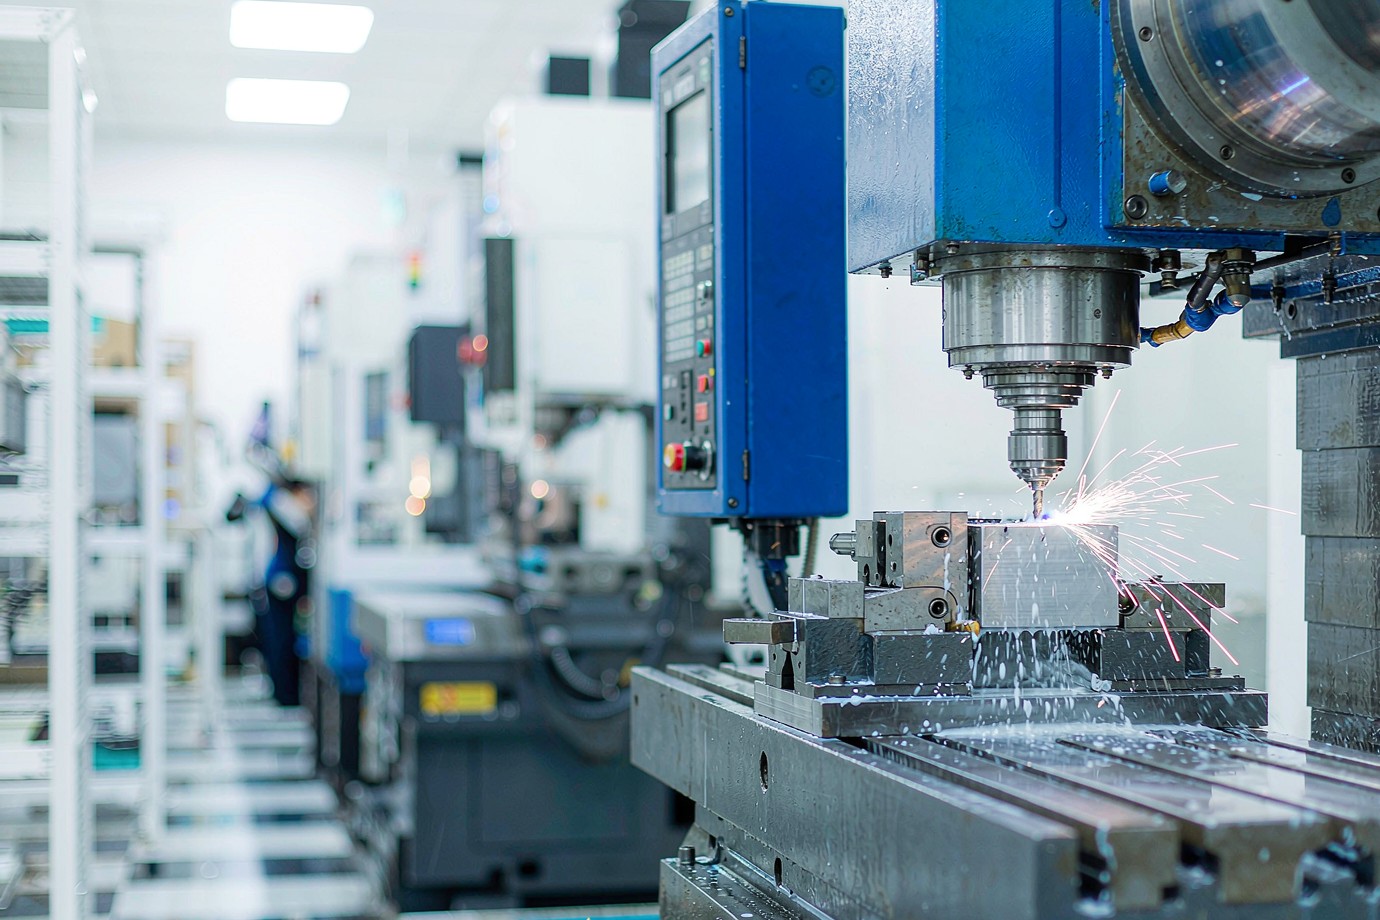
Multi-face features are evaluated by part geometry, tool access, locating datums and clamping — we do not default every complex form to five-axis machining, but select the method by structure, equipment and cost. All six core processes — CNC machining, injection molding, mold making, 3D printing, die casting and sheet metal fabrication — are performed in-house under one ISO 9001:2015 quality system. For the machining scope see our CNC machining services, and for the wider capability our manufacturing services overview.
Critical dimensions and quality control
We control tolerances by CTQ feature rather than applying one number to the whole part. The table shows what we typically watch on a threaded block.
| Key feature | Inspection direction |
|---|---|
| Overall dimensions | Length, width and height to drawing |
| Thread size and class | Plug or ring gauge to callout |
| Thread depth | Depth measurement of the engaged length |
| Hole position | CMM or applicable position measurement |
| Bore diameter | Internal measurement tools |
| Flatness | Measured against the drawing datum |
| Perpendicularity | Geometric tolerance check |
| Surface roughness | Roughness tester where specified |
| Burr removal | Visual or specified inspection |
Tolerance basis: we do not quote a single "±0.005 mm for the whole part." Tighter values apply only to qualified, drawing-defined features; typical machined features are around ±0.01 mm and are confirmed against ASME Y14.5-2018 / ISO 22081:2021 together with your drawing and the functional interface. ISO and ASME are not interchangeable — the drawing states which applies.
Where these components are used
Anywhere equipment needs a removable, repeatable joint between plates, frames or enclosures. The list below is potential procurement context, not a claim of existing customer cases.
Mounting & connection
Equipment mounting blocks, connection blocks and fixed blocks.
Locating & clamping
Locating blocks, clamp blocks and support blocks with repeatable fit.
Tooling
Jig blocks, adjustment blocks and mounting blocks with threaded depth and datums.
Non-standard joints
Non-standard threaded connection blocks by material, size and thread.
Interfaces
Equipment interface blocks and structural connectors with multi-face work.
Spares
Sample replication, old-part reverse measurement and material matching.
Thread and dimensional inspection
A threaded block fails quietly — a crossed thread or an out-of-class pitch diameter only shows up at your assembly line. We check before it ships.
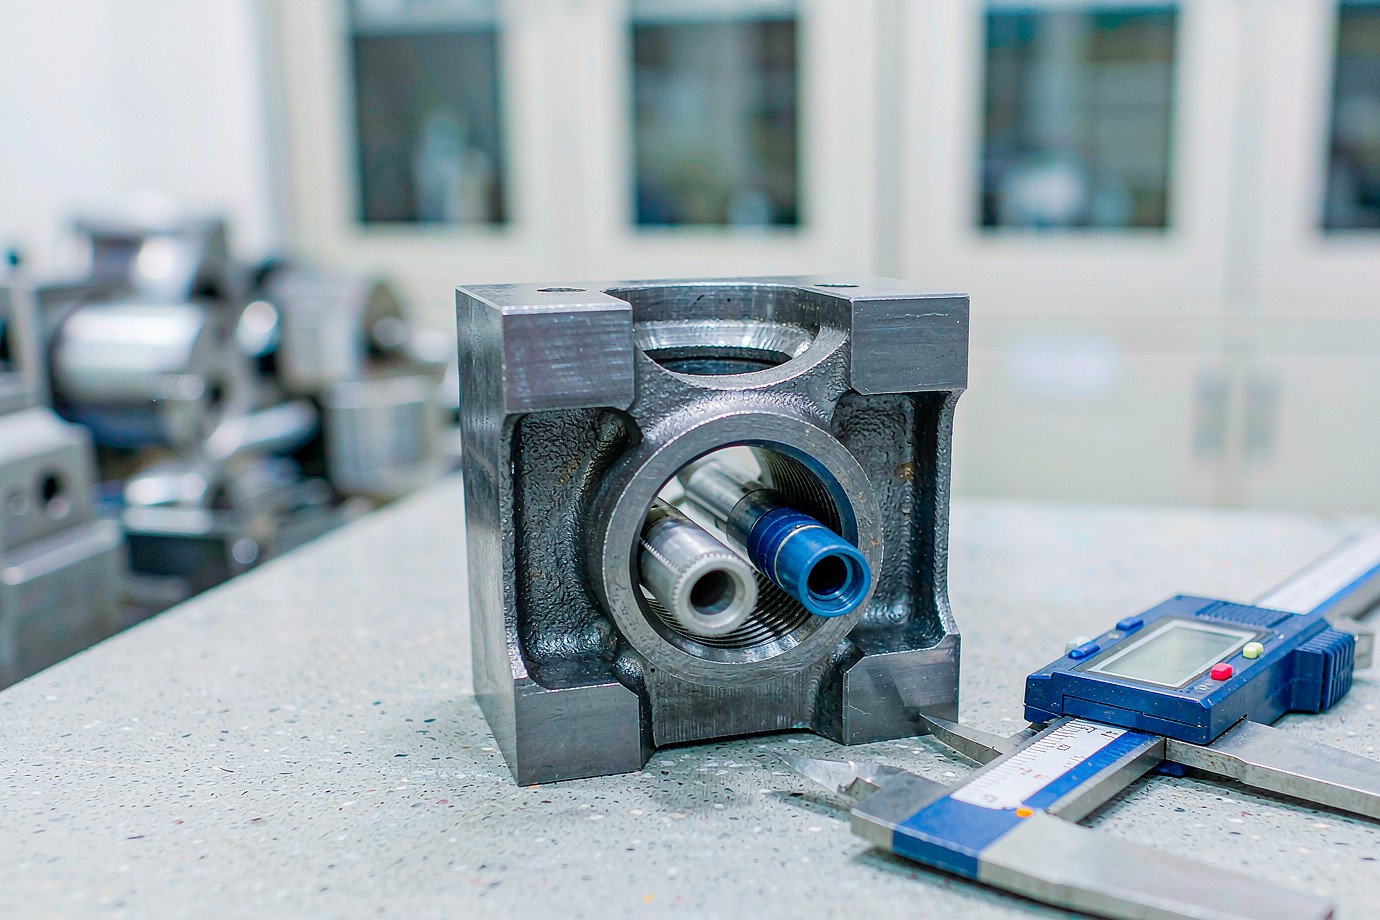
Thread inspection and fit verification
- Internal threads — checked with plug gauges sized to the specification.
- External threads — checked with ring gauges sized to the specification.
- Thread location — position checked against the drawing datum.
- Thread depth — effective thread depth measured.
- Thread entrance — chamfer, burr and entry damage checked.
- Assembly fit — verified with the specified fastener where the project requires it.
Material mill/test certificates are checked on arrival; dimensional reports, thread gauging records and FAI per AS9102 are available on request, scoped to your quality requirements.
Request a custom threaded block quote
The fields below are what helps us quote accurately. There is no input form on this page — use the button to open our secure quote window and send your drawing and the details.
Information that speeds up your quote
Send a 2D drawing and/or 3D CAD file. The more of the following you include, the faster and more accurate the quote.
Note: this page intentionally carries no input form. Click Upload Your Threaded Block Drawing to open our secure quote window, or email your files with the details above.
Send your 2D drawing or 3D CAD file with thread specifications, material, quantity and critical tolerances. We review the machining requirements before quotation.
Frequently asked questions
Can you manufacture custom CNC threaded blocks from drawings?
What materials are available for custom threaded blocks?
Can you machine metric and UNC/UNF threads?
How do you inspect internal threaded holes?
Can you machine multiple threaded holes on different faces?
Can you add counterbores and recessed features?
Does anodizing affect threaded holes?
Can you provide material certificates and inspection reports?
Can you produce prototypes and production batches?
What information is needed for a threaded block quotation?
Ready to machine your custom CNC threaded blocks?
Send your drawing and we will return a transparent, drawing-based quote with material, thread standard, tolerance and finishing options spelled out — from one prototype to production.
Xiamen Goldcattle Plastic & Metal Products Co., Ltd. — Founded in 1998 · Customers in 100+ countries · ISO 9001:2015 certified.