What Is CNC? How Computer Numerical Control Works in Manufacturing
CNC is the digital control layer behind modern machine tools. This guide explains what CNC means, how it differs from CNC machining, how a CAD file becomes a finished part, and how to judge whether CNC machining is the right process for your design.
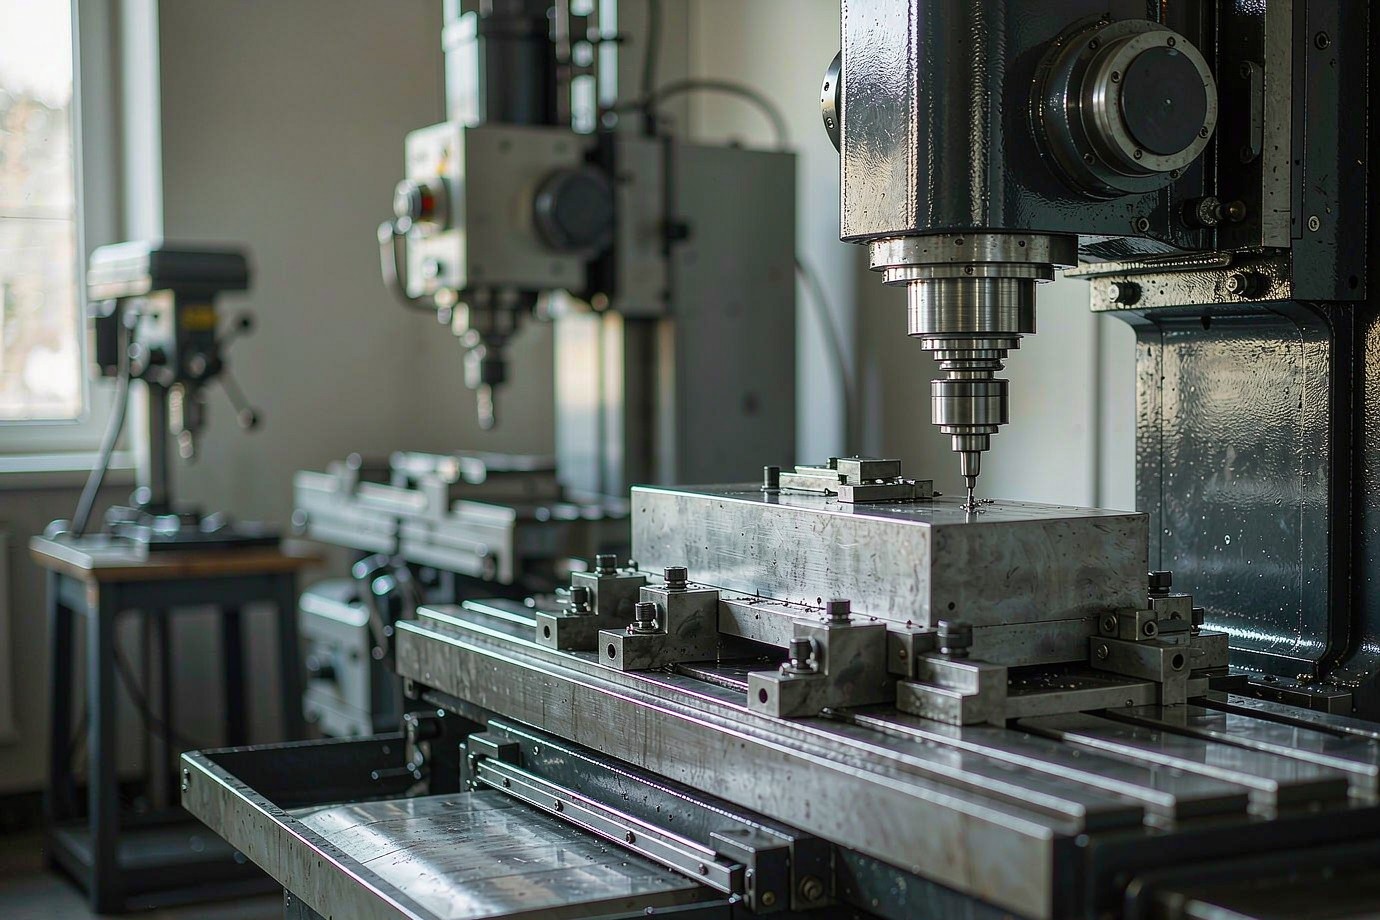
CNC stands for Computer Numerical Control. It is a method of controlling machine tools through programmed digital instructions. CNC can control equipment such as milling machines, lathes and other machine tools. CNC machining is a subtractive manufacturing process in which programmed cutting tools remove material from a solid workpiece to create a finished part.
In simple terms: CAD defines the part, CAM generates the machining strategy, the CNC controller executes the instructions, and the machine tool performs the physical operation. Embossing, bending, laser cutting and many other operations can also be CNC-controlled — CNC is the control method, not the process itself.
| Term | What it means |
|---|---|
| CNC | Computer Numerical Control — the digital control method for machine tools. |
| CNC machine | A machine tool operated by a CNC control system. |
| CNC machining | Subtractive manufacturing using CNC-controlled cutting. |
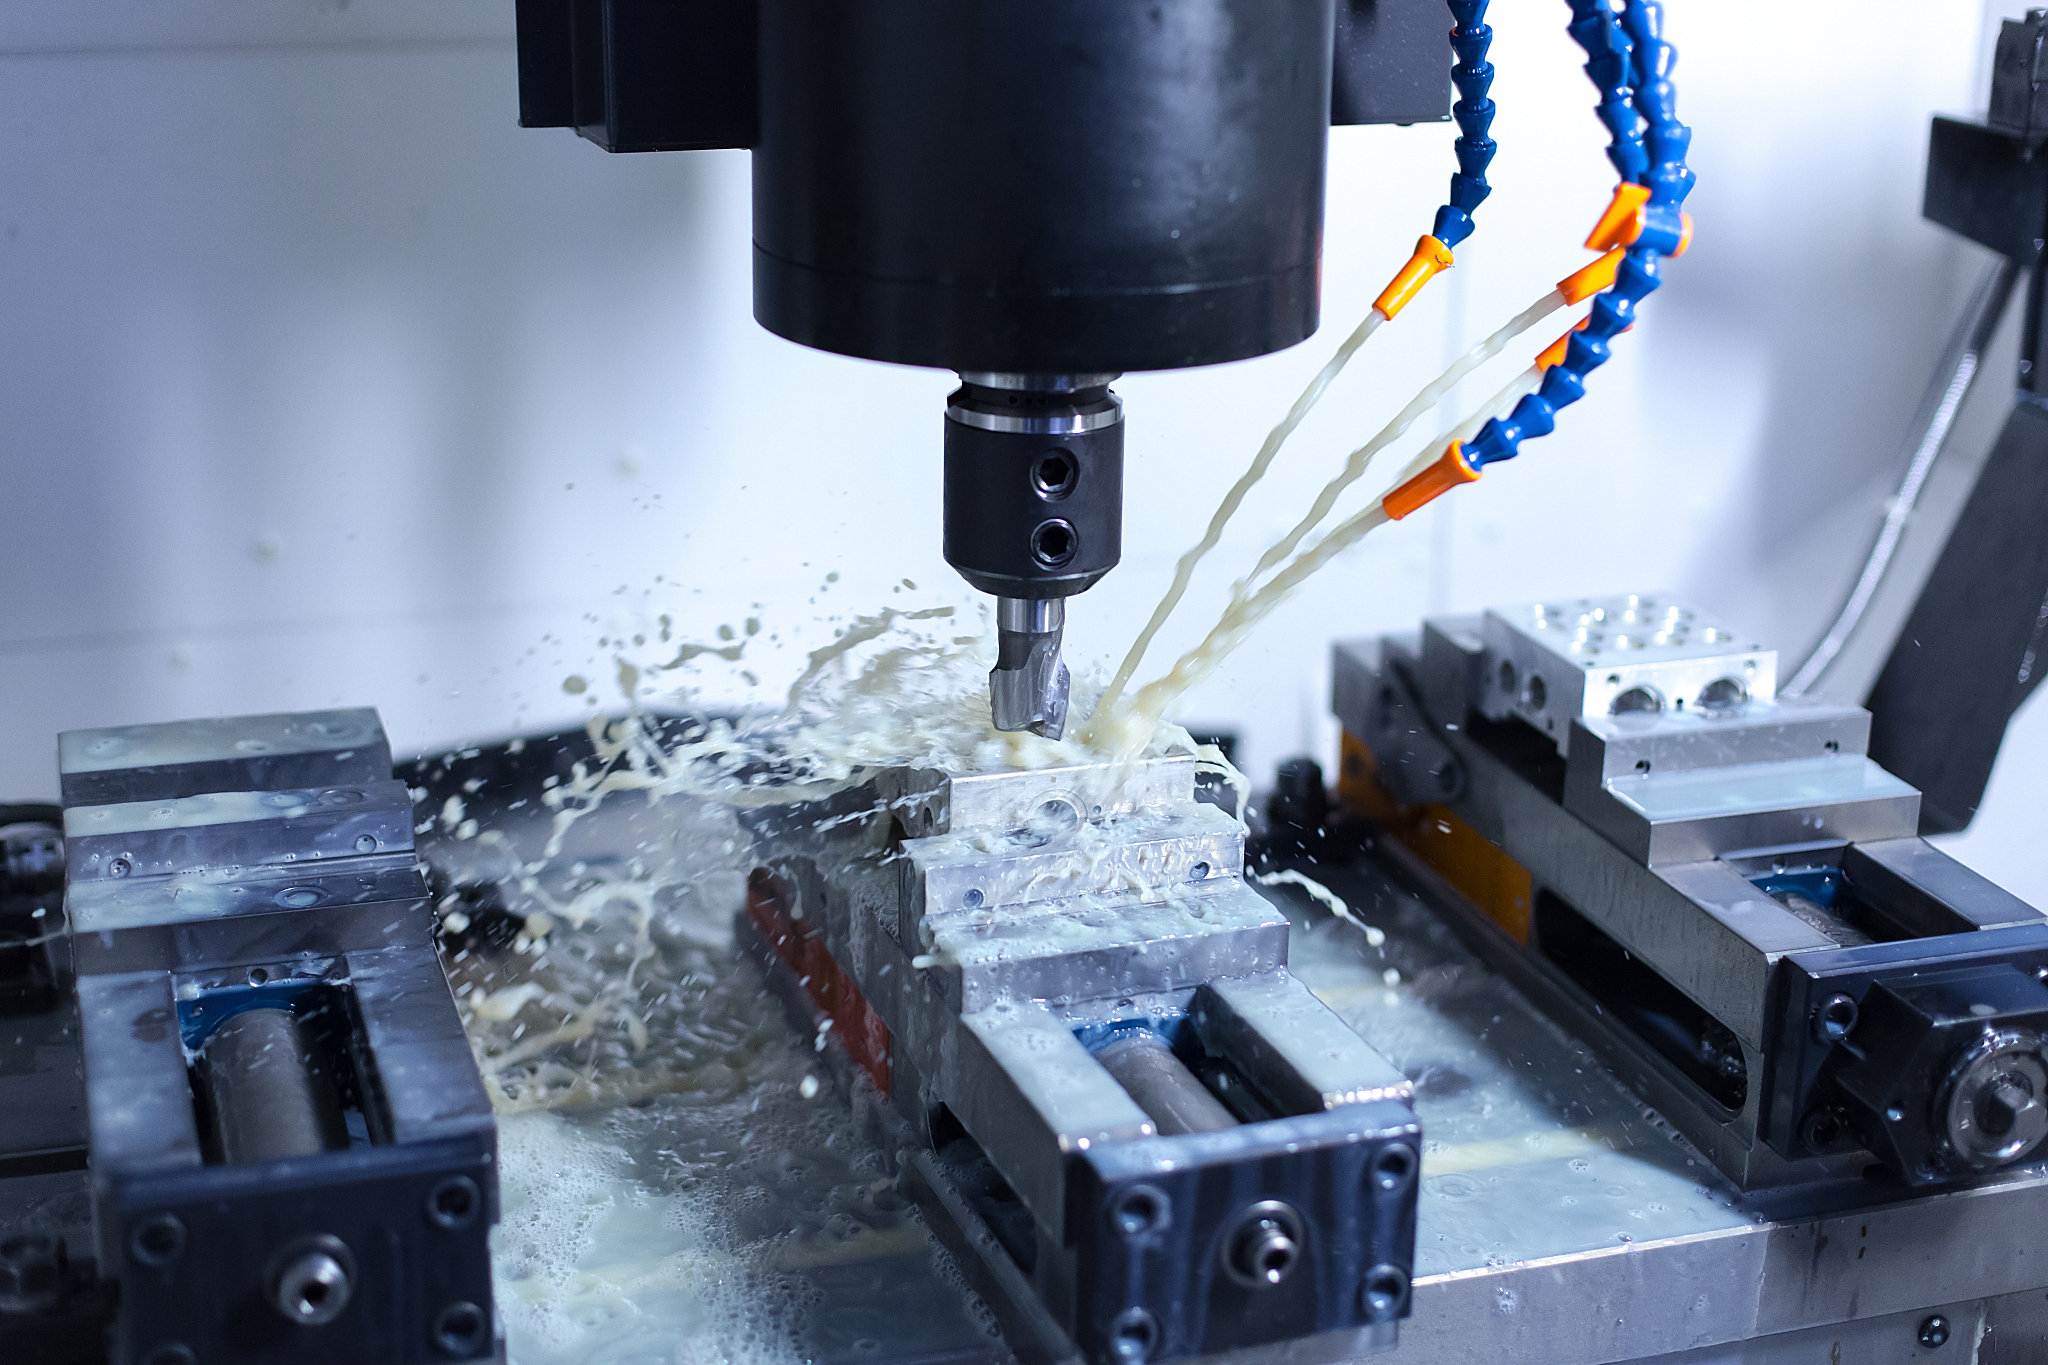
| CNC milling | Material removal with a rotating cutting tool. |
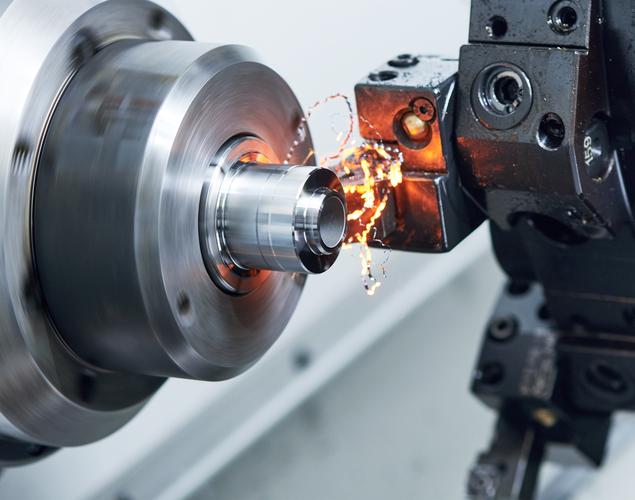
| CNC turning | Material removal from a rotating workpiece. |
| CAM | Software that generates machining toolpaths. |
| G-code | Machine-executable instructions for a specific controller. |
What Does CNC Stand For?
CNC is the abbreviation for Computer Numerical Control. At its core it is a way to control a machine's motion and operations from a stored program rather than from a person turning handwheels at the machine. The program describes where the tool moves, how fast it moves, and which operations happen in what order.
This matters because "CNC" is a control technology, not a single manufacturing process. The same control principle is used across very different equipment — machining centers, lathes, grinders, routers, EDM, laser and plasma cutters, and even some forming and measuring equipment. When buyers talk about "CNC parts," they are usually referring to parts made by CNC machining, which is one important application of CNC control.
CNC vs CNC Machining: What Is the Difference?
The two terms are related but not interchangeable, and confusing them is one of the most common sources of muddy technical writing:
CNC
The control layer. A method of running machine tools through programmed instructions. It is the "how the machine is steered" part of the story.
CNC machining
An application of CNC. A subtractive process where cutting tools remove material from a solid workpiece to make a part.
Why it matters
CNC can drive cutting, forming, cutting-fluid control, probing and inspection. Machining is only one family of processes that CNC can control.
A useful way to picture it:
| CNC (control) covers | CNC machining (process) covers |
|---|---|
| Motion control, axes, feeds and speeds | Milling, turning, drilling, boring, threading |
| Program storage and execution | Material removal strategy and toolpaths |
| Probing, offsets, in-process measurement | How stock becomes a finished geometry |
So when a page asks "what is CNC," the honest answer is about the control method; the question "how does CNC machining work" belongs to the machining process. Both are covered here, but they are kept distinct.
How Does CNC Work?
A CNC part is the output of a chain that starts with design and ends with inspection. The steps below are the standard path from a model on a screen to a measured part in a box:
Figure 1 — CAD defines the geometry, CAM plans the machining, the controller runs the program, the machine removes material, and inspection confirms conformance.
Step by step:
- Define the part. A 3D CAD model and, where tolerances or GD&T matter, a 2D drawing.
- Review manufacturability. Material, tolerance, tool access, workholding and machining strategy.
- Generate toolpaths. CAM turns the geometry into cutting operations and feeds/speeds.
- Post-process. The toolpaths become machine-specific code for the controller in use.
- Set up the machine. Tools, fixture, workpiece and work offsets are established.
- Machine. Milling, turning, drilling, threading or other operations remove material.
- Inspect. CMM, gauges, surface finish checks and visual inspection confirm the result against the drawing.
CAD, CAM and the CNC controller are different layers. CAD defines what the part is; CAM plans how it is cut; the controller executes the resulting program. They are not simply "parts of one CNC box."
What Are the Main Types of CNC Machines?
Most buyers will encounter a few families. Which one fits depends on the part shape, not on a general "more axes is better" rule.
CNC milling
A rotating cutting tool removes material from a generally stationary workpiece. Suited to prismatic blocks, pockets, holes, slots and complex 3D surfaces.
CNC turning
The workpiece rotates while a stationary tool cuts. Suited to shafts, pins, bushings, threaded cylindrical parts and round features.
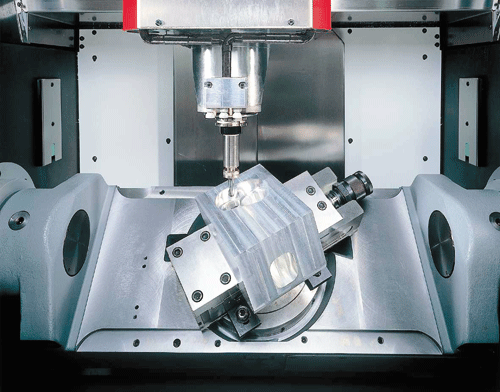
4-axis / 5-axis
Adds rotational axes so the tool or table can tilt, improving access to angled faces and reducing setups. Selected when geometry or setup control justifies it.
CNC grinding
An abrasive process for tight surface finish and dimensional control, often after hardening or on hardened features.
CNC routing
Similar in principle to milling but commonly used for larger, softer or non-metal sheets and panels.
Other CNC equipment
EDM, laser and plasma cutting, and some bending or measuring equipment are also CNC-controlled.
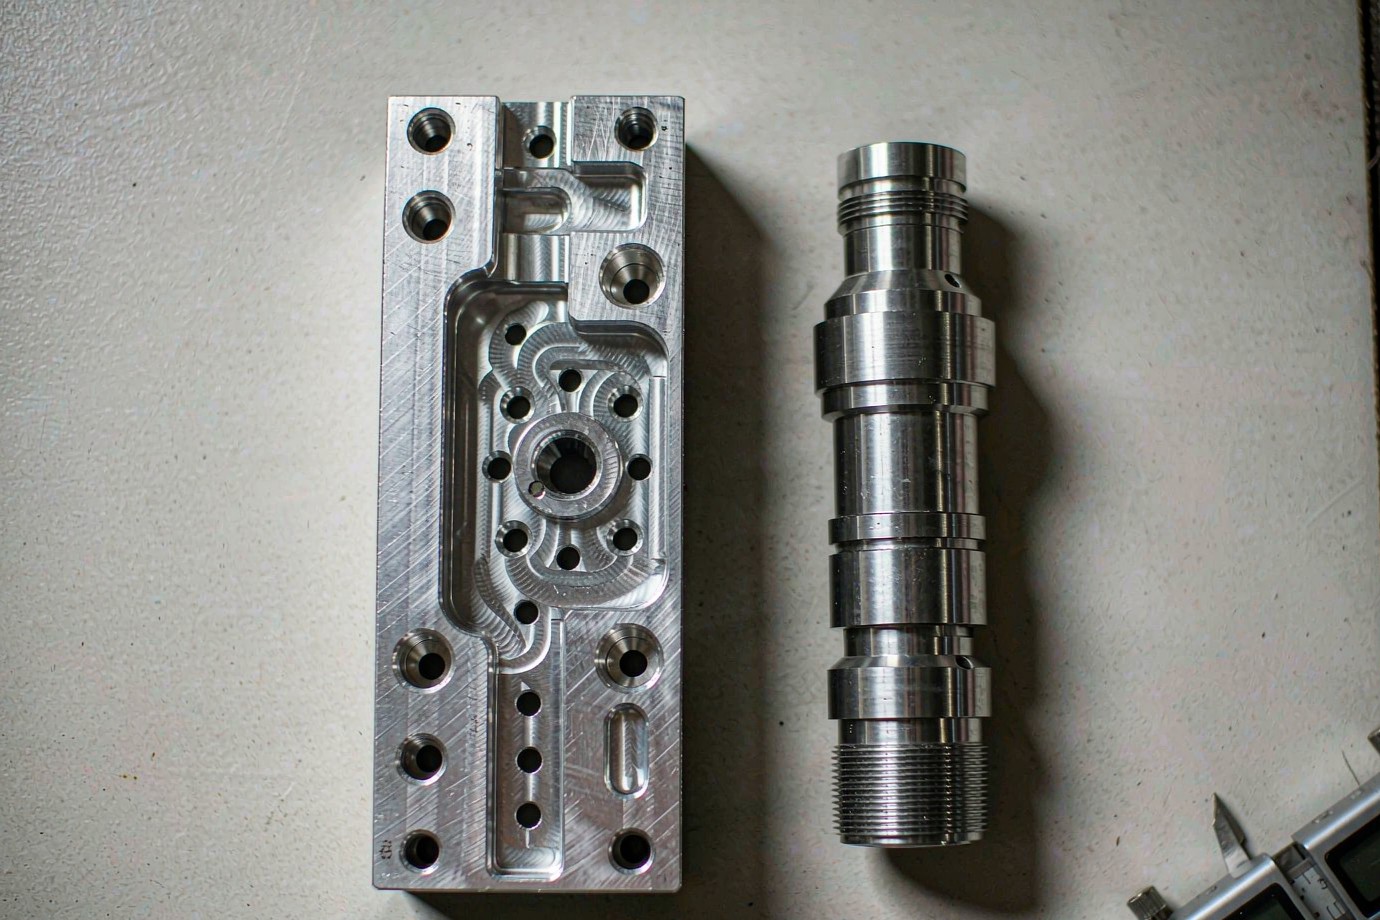
| Part characteristic | Likely CNC process |
|---|---|
| Prismatic block, pockets, holes | CNC milling |
| Cylindrical shaft, pin, bushing | CNC turning |
| Complex multi-face geometry | 4-axis / 5-axis machining |
| Long, slender rotational part | Turning, or mill-turn by geometry |
| Tight internal contour, hard access | Milling, or EDM where access is blocked |
| Hardened cavity or finish-critical | Milling + grinding where needed |
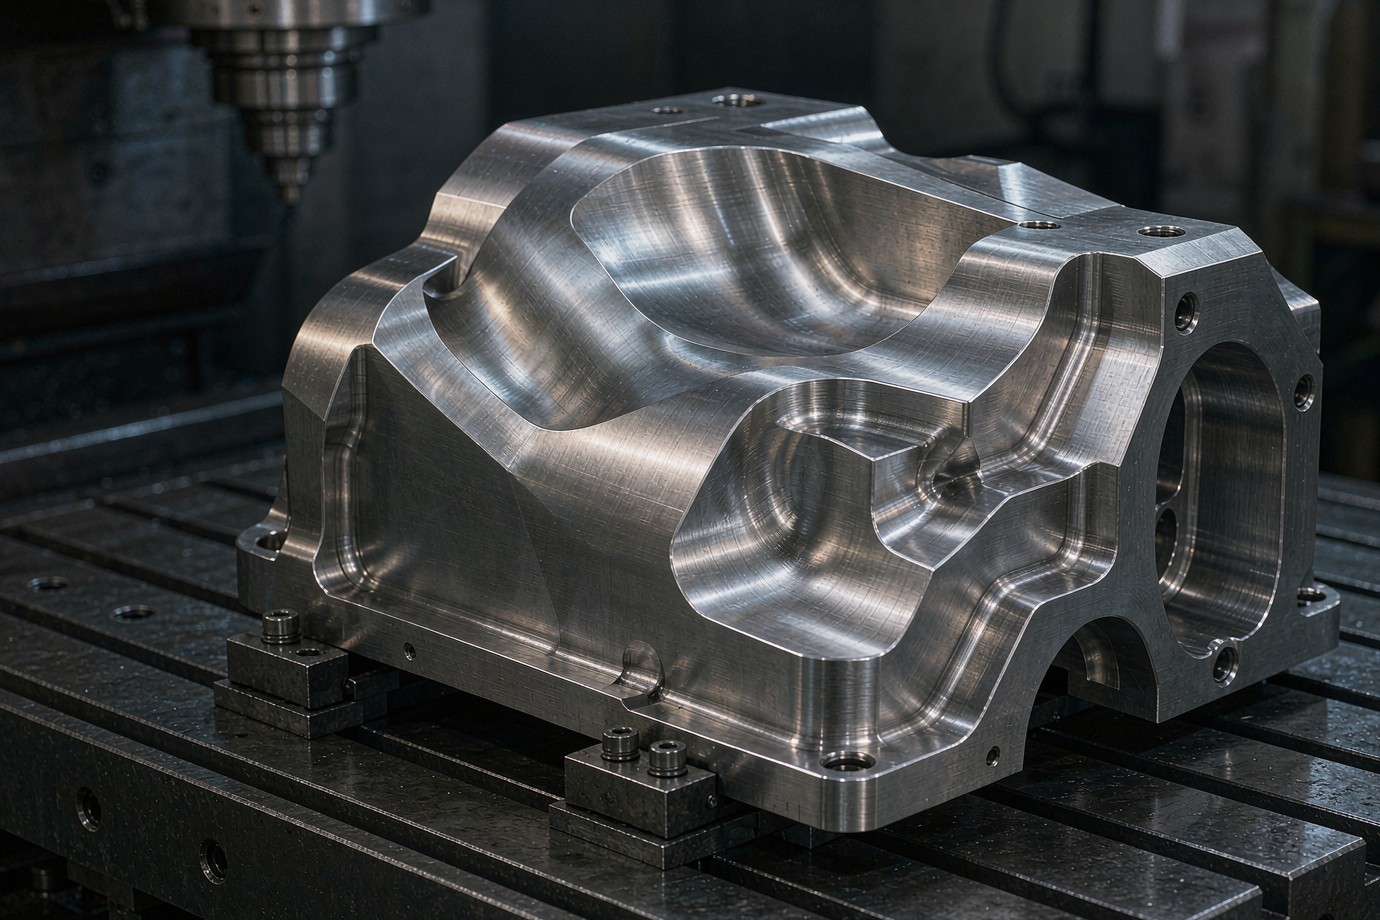
What Materials Can CNC Machines Process?
CNC machining is material-flexible. The practical limits come from machinability, tooling and the behavior of the material under cutting forces and heat.
Aluminum
Easy to machine, light, good strength-to-weight. A common default for prototypes and production alike.
Stainless & steel
Strong and wear-resistant; harder on tooling and more sensitive to heat. Needs planned speeds and coolant.
Titanium
High strength and corrosion resistance, low thermal conductivity. Demands careful tooling and process control.
Brass & copper
Excellent machinability and conductivity; used for fittings, electrical and decorative parts.
Engineering plastics
PEEK, POM, nylon, PC, ABS. Used where weight, insulation, wear or chemical resistance matter.
Selection criteria
Strength, weight, corrosion, temperature, wear, electrical needs, machinability and surface finish drive the choice.
Material choice interacts with geometry and tolerance: a grade that machines easily may still be the wrong choice if the part needs high temperature resistance or electrical insulation. The material is reviewed together with the drawing, not in isolation.
How Accurate Is CNC Machining?
The most misleading content on many "what is CNC" pages is a single universal tolerance quoted to micron level, as if it applied to every part. Real capability is not one number.
Achievable accuracy depends on several factors working together:
Machine
Rigidity, thermal stability, axis calibration and repeatability of the specific machine.
Material
How the material moves, springs back or work-hardens during cutting.
Geometry
Thin walls, deep features and aspect ratios that amplify deflection.
Setup
Fixturing and datum strategy that hold the part stable and consistent.
Tooling
Tool stiffness, wear and runout during the cut.
Inspection
How conformance is measured and recorded against the drawing.
The useful rule: specify tolerance by function on the drawing, and let the supplier assess tighter features against the drawing and process review. A supplier may quote a standard general tolerance and separately evaluate the features that truly need to be tight. Over-specifying tolerances that a function does not require adds cost and lead time without improving the part.
At Goldcattle: tight tolerances are supported on qualified features after the drawing and process are reviewed. The achievable value depends on material, geometry, machine strategy, setup and inspection — it is confirmed against the specific part, not assumed as a blanket number.
What Makes a CNC Part Easy or Difficult to Machine?
Design for manufacturability (DFM) is where most cost and lead-time are decided. A few principles cover most cases:
Tool access
If a cutter cannot physically reach a feature, the part needs another setup or a different process.
Internal radii
Sharp internal corners force small tools and long cycle times; a practical radius helps.
Pocket depth
Deep, narrow pockets are harder to clear and hold than shallow ones.
Wall thickness
Very thin walls deflect and chatter; practical thickness keeps them stable.
Setups
Fewer setups mean fewer datum transfers and tighter feature-to-feature control.
Tolerances
Tight tolerances only where function requires them; everywhere else, standard is enough.
For a deeper treatment, see the CNC design-for-manufacturability guide.
CNC Machining vs Other Manufacturing Processes
CNC is one option among several. Matching the process to the part is part of good sourcing, not a weakness of CNC.
| Process | Best suited for | Compared with CNC |
|---|---|---|
| CNC machining | Precision parts, prototypes, low-to-medium volume, complex machined geometry | Baseline — uses the actual material, no tooling investment |
| Injection molding | Very high-volume plastic components | Lower unit cost at volume, but needs a mold |
| Die casting | High-volume metal housings and components | Fast cycles at volume, but needs die tooling |
| Sheet metal | Thin-gauge formed and bent parts | Better for skins and brackets than for solid blocks |
| 3D printing | Fast prototypes, complex additive geometries | Less established material properties at volume |
The practical question is rarely "is CNC good?" It is "for this geometry, volume and material, is CNC the most sensible route, or should molding, casting, sheet metal or additive take the lead?"
When Should You Use CNC Machining?
Prototypes
You want the real production material and geometry to validate fit and function before committing to tooling.
Low-to-medium volume
Volume does not yet justify the cost of a mold or die.
Tight tolerances
The part needs controlled dimensions that forming or casting struggle to hold.
Complex geometry
Features, pockets and contours that are hard to make any other way.
Fast iteration
Designs change and you cannot wait for tooling lead time.
One-off or spare parts
Replacement or custom parts where no production tooling exists.
When Is CNC Not the Best Choice?
An honest supplier will tell you when another process fits better. CNC is not automatically right for every part.
Very high-volume plastic parts
Once the forecast is stable, injection molding usually wins on unit cost.
High-volume metal housings
Die casting offers faster cycles at scale once tooling is justified.
Thin sheet components
Sheet metal fabrication or stamping suits formed, thin-gauge parts.
Complex internal lattices
Additive manufacturing can build geometries machining cannot reach.
Large welded structures
Fabrication from stock may beat machining a solid block.
Soft, very compliant parts
Some elastomers and flexible parts are better molded than machined.
What Actually Determines CNC Part Quality?
Two shops can receive the same CAD file and deliver different parts. The outcome is the sum of how the job is planned and controlled, not just "the machine is automated."
Figure 4 — Quality is built across drawing, DFM, planning, machine, fixturing, machining, inspection and documentation.
The factors buyers can reasonably weigh before ordering:
| Factor | Why it matters |
|---|---|
| Machine | Rigidity, envelope and axis capability set the ceiling. |
| Tooling | Cutting-tool selection and condition affect finish and consistency. |
| Workholding | Stable fixturing keeps the part where it should be. |
| Datum strategy | Good datums keep feature-to-feature accuracy under control. |
| CAM programming | Toolpath quality and collision avoidance protect the part. |
| Material behavior | Machinability and thermal response change the result. |
| Inspection | Measurement and records are the evidence of conformance. |
What Affects CNC Machining Cost?
There is no honest "CNC costs $X per part" figure, because cost is a sum of drivers. The realistic model is:
Material + stock size + machining time + geometry complexity + number of setups + tolerance / GD&T + surface finish + inspection + secondary operations = total CNC cost.
The biggest levers are usually machining time and setups, which is why DFM (fewer setups, reachable features, sensible tolerances) pays back directly. Secondary operations such as anodizing, plating, heat treatment and special inspection add line items on top of the cutting time. Volume changes the math: at higher quantities, setup amortization and process optimization matter more than the per-part cycle.
What Do You Need to Send a CNC Supplier?
Required
- 3D CAD model
- 2D drawing if tolerances or GD&T matter
- Material and grade
- Quantity and annual volume
- Revision and critical dimensions
- Surface finish requirements
Helpful
- Application and operating environment
- Plating / anodizing / coating needs
- Inspection, FAI or PPAP requirements
- Material certificate requirements
- Existing tooling details
- Target delivery date
Send the model in a common format and include the drawing whenever a dimension or callout is binding. The more the supplier knows about function, the better the tolerance and process decisions.
From CAD to Finished Part: A CNC Workflow Example
The example below is illustrative of a typical small-batch job and shows how the steps above turn into a real part. It is a representative workflow, not a specific customer project.
Example: a machined mounting bracket
- Requirement: a 6061 aluminum bracket with dowel holes, a recessed pocket and two threaded standoffs.
- Material: 6061-T6 aluminum, chosen for machinability and weight.
- Process: CNC milling from plate, with a second operation for the back face features.
- Setups: two setups — one for the front profile and pocket, one to flip and finish the back.
- Tolerance: general ±0.1 mm, with the dowel holes held tighter because they locate the assembly.
- Finish: deburred and bead-blasted; clear anodize requested for corrosion resistance.
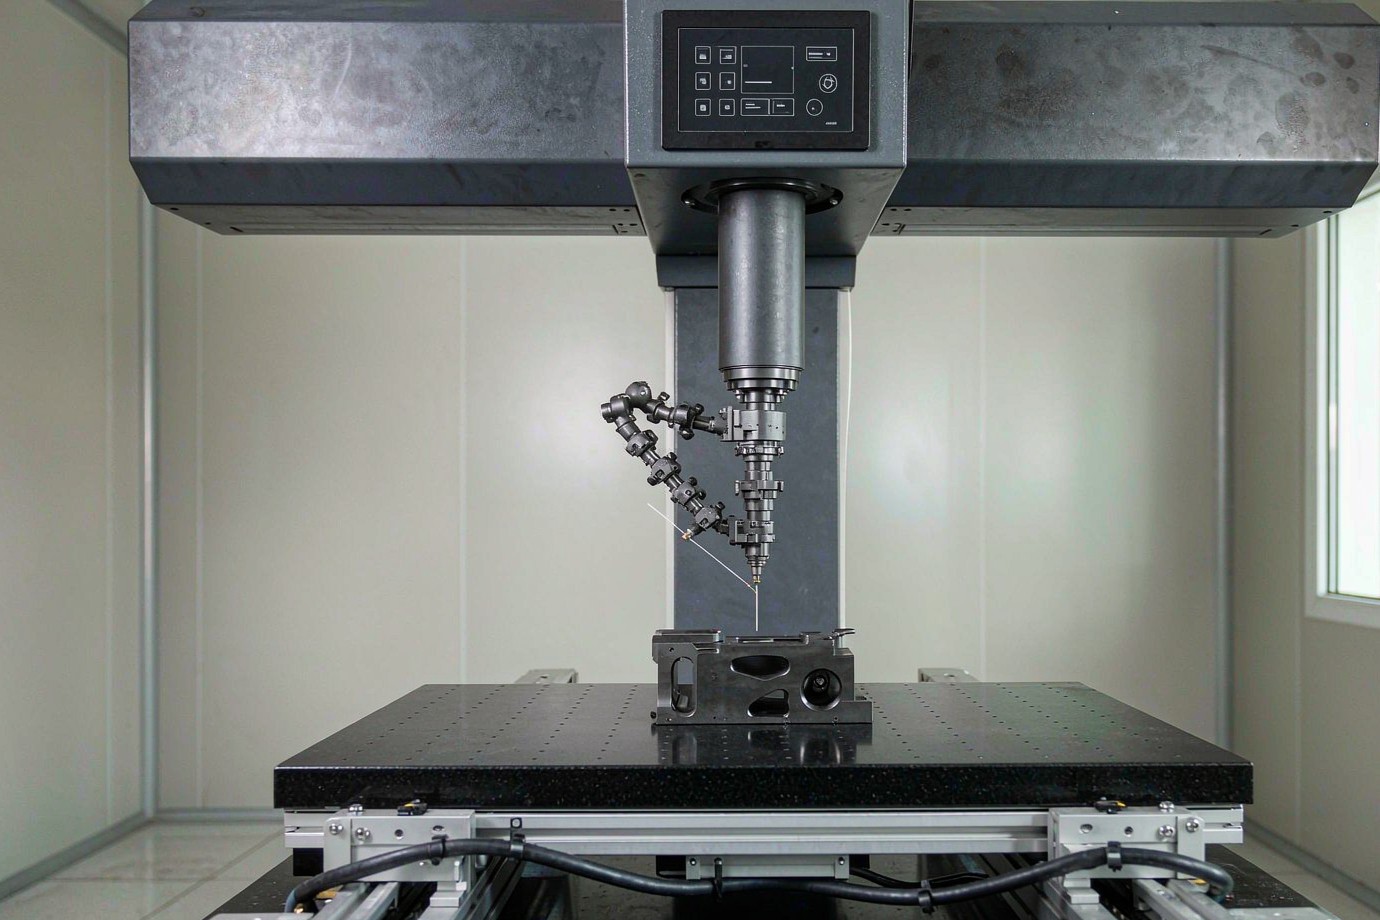
- Inspection: CMM check of the holes and profile against the drawing; report issued with the batch.
CNC Machining at Goldcattle
Xiamen Goldcattle Plastic & Metal Products Co., Ltd. is a manufacturing supplier established in 1998 that runs CNC milling, CNC turning and 3-, 4- and 5-axis machining alongside injection molding, mold making, 3D printing, die casting and sheet metal fabrication. For CNC work the practical span covers aluminum, stainless steel, steel, titanium, brass, copper and engineering plastics, with processes planned around the drawing, DFM and inspection rather than a one-size tolerance.
Capability is quoted against the part: material, geometry, machine strategy, setup, tolerance and inspection are reviewed together, and tight features are supported on qualified features after process review. Inspection is documented, and material certificates can be supplied on request. This is the difference between "a machine that cuts" and a supplier that delivers conforming parts repeatedly.
Related CNC Resources
These pages go deeper on the topics above. They are kept distinct in intent so each answers a different question:
CNC machining services
Custom CNC Machining Services — capabilities and how to start a project.
CNC machining explained
CNC Machining: Process, Materials, Tolerances — the deeper machining guide.
CNC milling
What Is CNC Milling? — milling-specific detail.
Multi-axis
CNC turning
Materials
Quote
Frequently Asked Questions
What does CNC stand for?
CNC stands for Computer Numerical Control. It is a method of controlling machine tools through programmed digital instructions, and it can be applied to many equipment types, not only machining.
What is the difference between CNC and CNC machining?
CNC is the control technology; CNC machining is one application of it. CNC machining is a subtractive process where cutting tools remove material from a solid workpiece. CNC is the "how the machine is controlled" layer; machining is the "how the part is made" process.
Is CNC machining subtractive manufacturing?
Yes, in the conventional sense. It starts from solid stock and removes material to reach the final shape, which is different from additive manufacturing where material is built up.
How does a CNC machine read a CAD file?
CAD defines the geometry; CAM converts it into toolpaths and operations; a post-processor turns those into machine-specific code (commonly G-code); the controller executes it; the machine tool cuts the workpiece.
What is the difference between CAD and CAM?
CAD defines part geometry and the drawing. CAM plans how the part is machined — tools, strategy, feeds, speeds and toolpaths. CAM output feeds the controller; CAD output feeds CAM.
What is G-code?
G-code is a set of machine-executable instructions that tell a CNC machine how to move and operate. In modern production, CAM generates the machine-specific program, so complete G-code is rarely written by hand.
What is the difference between CNC milling and turning?
In milling, a rotating tool removes material from a generally stationary workpiece, suited to blocks, pockets and holes. In turning, the workpiece rotates while the tool cuts, suited to shafts, pins and threaded cylindrical parts.
Is 5-axis CNC always better than 3-axis?
No. 5-axis is selected when geometry, tool access, multiple faces or setup reduction justify it. For simple prismatic parts, 3-axis is often more economical.
How accurate is CNC machining?
There is no single universal tolerance. Accuracy depends on the machine, material, geometry, setup, thermal conditions, tooling, inspection and the tolerances specified on the drawing. Tolerances should be set by function.
What materials can be CNC machined?
Metals such as aluminum, stainless steel, steel, titanium, brass and copper, and engineering plastics such as PEEK, POM, nylon, PC and ABS. Choice depends on strength, weight, corrosion, temperature, wear, electrical needs and machinability.
Is CNC machining suitable for prototypes and production?
Yes. It is widely used for prototypes because it reproduces the final material and geometry, and it scales to low and medium production. Very high volumes may be better served by molding, die casting or stamping.
When should I use CNC instead of 3D printing or injection molding?
Use CNC when you need the actual production material, tight tolerances, established properties, or low-to-medium volume without tooling. Use 3D printing for complex additive geometries, and injection molding for very high-volume plastic parts.
What information is required for a CNC quote?
Send the 3D CAD model, a 2D drawing where tolerances or GD&T matter, material and grade, quantity and annual volume, critical dimensions, surface finish and application. Add revision, environment, finishing, inspection and certificate needs where relevant.
Upload CAD & Request a Manufacturing Review
Send your model and drawing and we will review manufacturability, suggest the right process, and return a quote with a clear lead time.
Request a CNC Manufacturing Review