Aerospace & Aviation Manufacturing
Custom Aircraft Precision Components
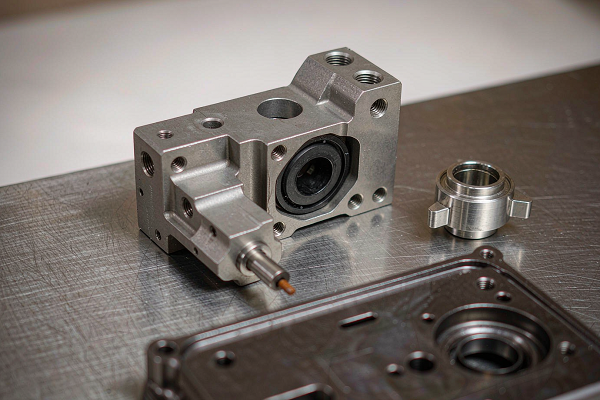
Machined aircraft components built to your drawing — brackets, housings, fittings, shafts and structural hardware in aluminum, titanium and stainless steel. Send the print; we quote the material, process and inspection plan.
- Made to your drawing — material, tolerances and finish to your specification
- 3-, 4- and 5-axis milling and precision turning under one roof
- Incoming, in-process and final inspection with documentation
Materials
Aluminum · Titanium · Stainless steel
Machining
3 / 4 / 5-axis milling & turning
Tolerances
Quoted to your drawing
Documentation
Material certs & inspection reports
What this page covers
This is our component page: the aircraft part families we machine, the materials we work with, the design rules that keep a part manufacturable, and how each order is inspected and documented. Everything here starts from your drawing — we manufacture to your specification rather than to a house design.
Looking for the service overview?
If you want to understand how our aerospace machining capability and process controls are organised, start with Aerospace CNC Machining. This page handles the parts; that page handles the service.
Component families
Components We Manufacture
Aircraft hardware rarely fits a single category. These are the component families we routinely machine for airframe, equipment and ground-support applications — each one quoted and produced to the drawing you supply.
01
Mounting Brackets
Angle, L- and formed brackets that locate and support equipment, with lightening pockets and drilled or tapped mounting patterns.
02
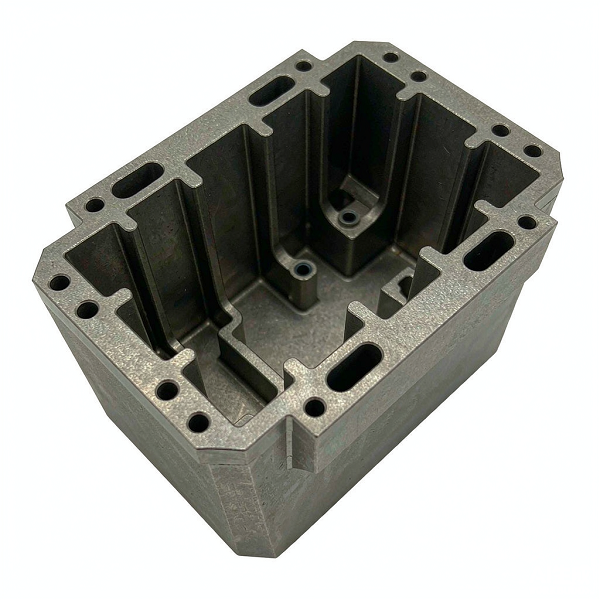
Housings & Enclosures
Machined housings with internal pockets, ribs, sealing faces and bolt-hole flanges for sensors, actuators and electronics.
03
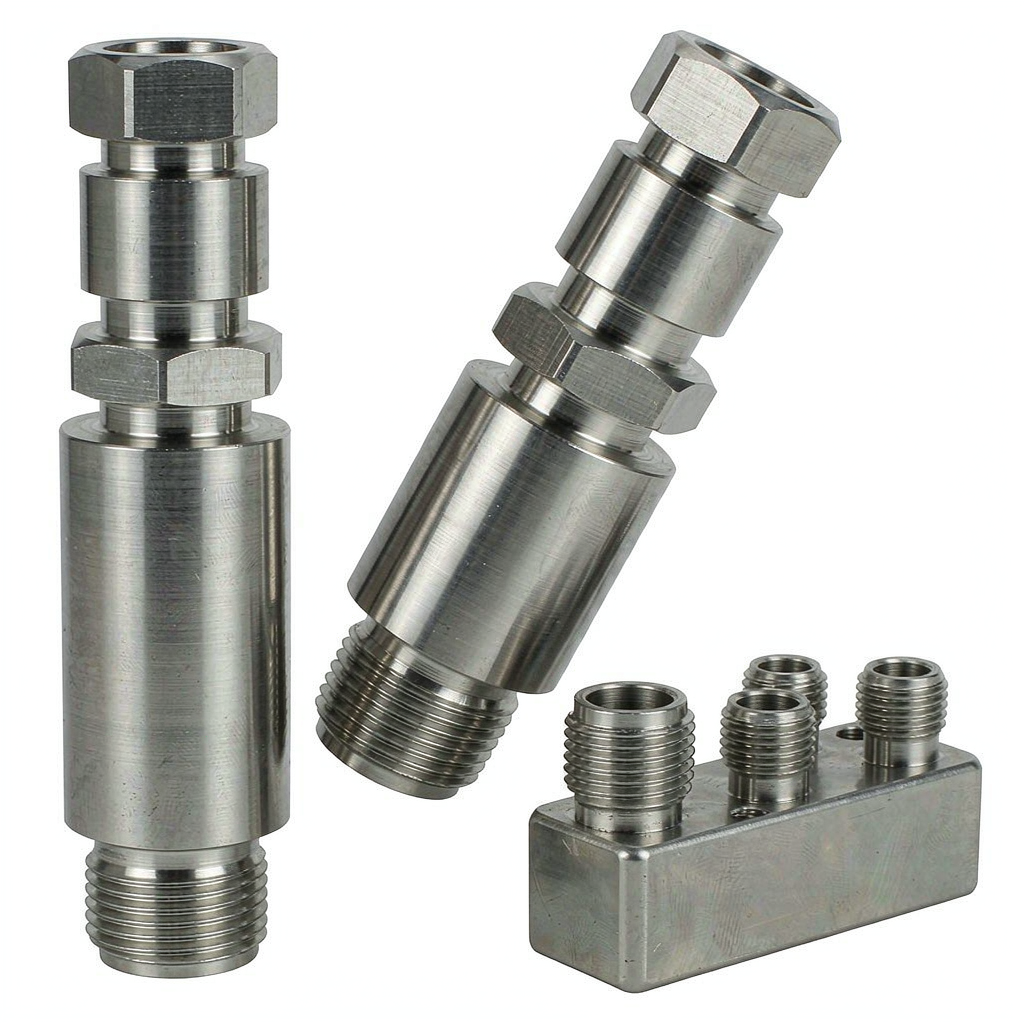
Fittings & Connectors
Fluid and hydraulic fittings, adapters and small manifolds with threaded ports and controlled sealing surfaces.
04
Shafts & Bushings
Turned shafts, pins, spacers and bushings held to diameter and concentricity requirements on the print.
05
Structural Brackets & Ribs
Load-path hardware with pocketed or ribbed geometry that trades part weight against stiffness.
06
Equipment Mounting Hardware
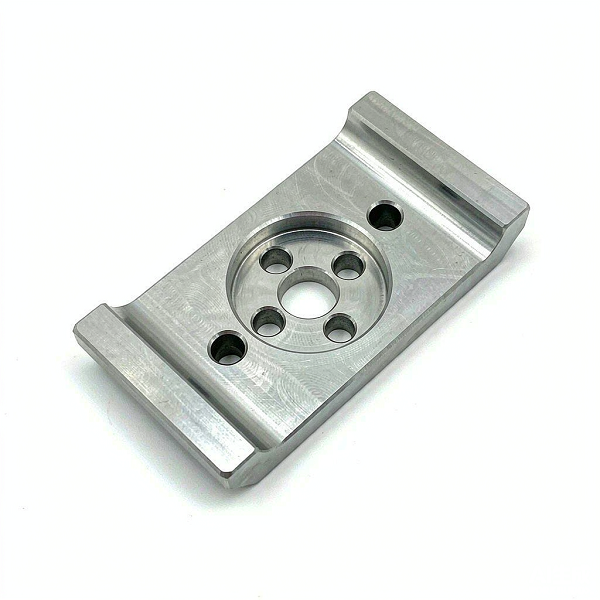
Interface plates, adapter blocks and mounting feet for avionics, cabin and equipment installations.
07
Ground-Support Components
Machined parts for ground-support and maintenance tooling, where robustness and repeatability matter more than weight.
08
UAV & Drone Parts
Airframe brackets, motor mounts, gimbal plates and chassis hardware for unmanned platforms.
Component types & critical features
What Usually Drives the Machining on Each Part
The same component family can be a simple 3-axis job or a five-axis problem, depending on which features are critical. This table maps the families above to the features that most often decide the process route.
| Component family | Typical materials | Features that drive the route | Common processes |
|---|---|---|---|
| Brackets & mounting plates | Aluminum, titanium, stainless | Pocket depth, wall thickness, hole position and edge break | 3-axis milling, drilling, deburring |
| Housings & enclosures | Aluminum, stainless | Internal pockets, sealing faces, bore concentricity, flange flatness | 3/4-axis milling, boring, turning |
| Fittings & fluid connectors | Stainless, aluminum, titanium | Thread form, port sealing surface, internal passage cleanliness | Precision turning, milling, threading |
| Shafts & bushings | Stainless, titanium | Diameter and roundness, concentricity, surface finish on bearing seats | CNC turning, grinding where specified |
| Structural brackets & ribs | Aluminum, titanium | Compound angles, contoured ribs, fillet radii, weight-reduction pockets | 3/5-axis milling, EDM where needed |
| Ground-support & UAV hardware | Aluminum, stainless | Interface location, assembly fit, robustness over weight | 3-axis milling, turning, drilling |
Materials
Materials for Aircraft Precision Components
Material is usually set by the drawing, not by us. These are the families we machine most often; where a grade is critical, the certificate follows the mill lot.
Aluminum Alloys
6061 · 7075 · 6082
The default for weight-sensitive brackets, plates and housings. Good machinability and strength-to-weight make aluminum the fastest route to a lightweight part. See our 6061 aluminum capability for typical tolerances and finishes.
Titanium Alloys
Ti-6Al-4V (Grade 5) · Grade 2
Chosen for high strength-to-weight and corrosion resistance in fittings, fasteners and load-bearing hardware. Titanium machines more slowly and tool wear is higher, so it is quoted with that in mind. See titanium CNC machining.
Stainless Steel
304 · 316L · 17-4PH
Used where corrosion resistance and strength are both required — fittings, shafts and hardware. 17-4PH can be supplied in a specified condition when the drawing calls for higher strength. See stainless steel CNC machining and the 304 vs 316 comparison.
Nickel & High-Temperature Alloys
Available subject to mill availability
Nickel-based and other high-temperature alloys can be machined where the drawing specifies them, subject to mill availability and the required certification. Because supply and lead time vary, we confirm grade, condition and documentation before quoting.
When 5-axis earns its place
Five-Axis Machining — Only When the Geometry Justifies It
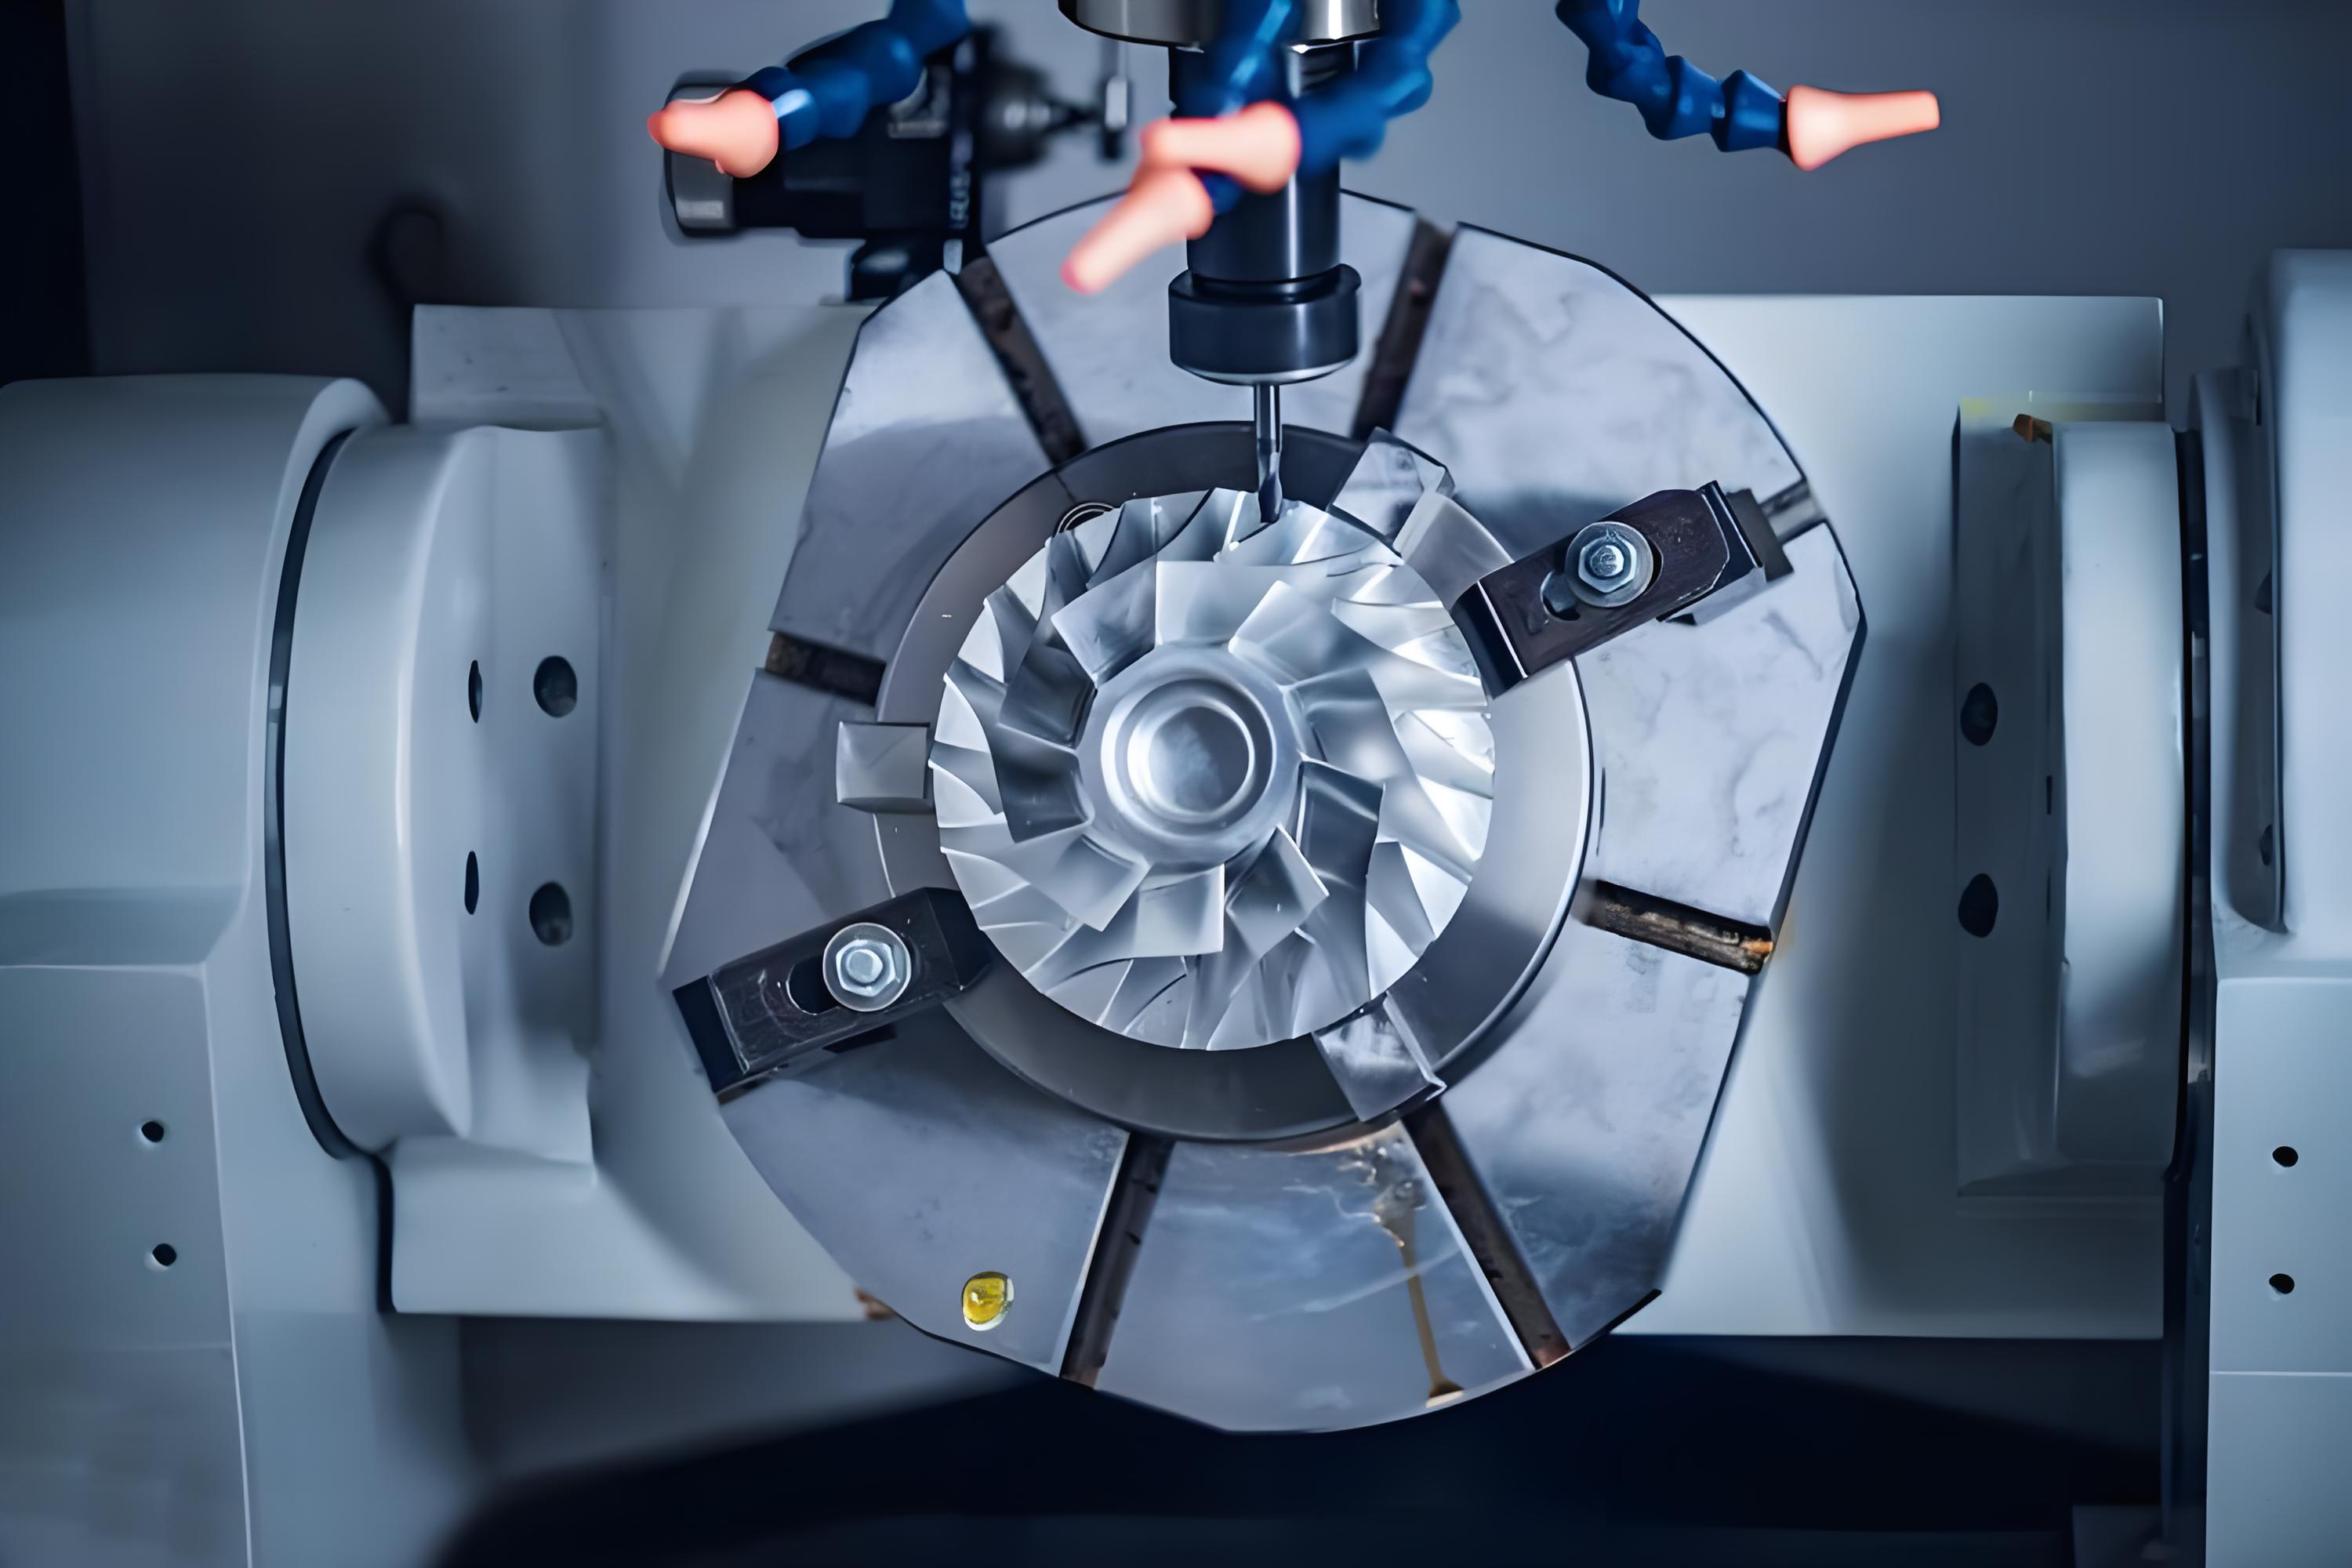
Five-axis is a tool, not a default. It pays off when a part has compound angles, contoured surfaces, deep pockets or features on several faces, because it cuts the number of setups and improves positional consistency between those faces. For simple 2.5D plates and brackets, 3-axis machining is usually faster and cheaper — and that is what we will quote.
- Compound angles and angled faces that would otherwise need several fixtures
- Contoured or sculpted surfaces following a 3D model
- Features on multiple faces that must stay in position to one another
- Deep pockets reached at an angle to avoid tool rubbing
Where five-axis improves the part, we use it; where it does not, we say so. Read more about our 5-axis CNC machining services.
Design for machining
Design Considerations for Aircraft Components
Most cost and quality problems in a machined component are decided at the design stage. These are the points we review before quoting, and the feedback we return with every RFQ.
- Wall thickness. Very thin walls deflect under cutting forces — consistency matters more than the absolute value.
- Corner radii. An internal corner needs a radius at least as large as the cutter; sharp internal corners force EDM or hand work.
- Tolerances. Reserve tight tolerances for the features that need them. A blanket tight tolerance multiplies cost and inspection time.
- Datums & stack-up. Clear datums let us inspect the same way the part is used, and avoid tolerance stack-up surprises.
- Pocket depth. Keep depth-to-width ratios within reach of a standard cutter to avoid long, thin tools and chatter.
- Hole & thread standards. Standard callouts reduce tooling risk; non-standard forms may need special taps or gauges.
- Surface finish. Specify finish only where it matters — sealing faces, bearing seats — and leave the rest as-machined.
- Feature access. Recesses and undercuts may need a longer reach, a different orientation or five-axis work.
- Deburring. Note whether edges must be broken and to what style; hidden burrs affect assembly and safety.
- Marking & traceability. Tell us where a part number or lot marking may sit and whether it is allowed on a functional face.
Weight & stock form
Lightweighting, and Where the Metal Comes From
Weight reduction and stock selection are two sides of the same decision: how much metal you remove, and what shape you start from. Both are governed by volume, load path and lead time.
Reducing component weight
Weight is usually removed by pocketing, ribbing and thinning walls rather than by changing material. We can machine pockets and ribs to your model, but remember that every pocket adds machining time and another wall to control — so the cheapest weight saving is usually the one the drawing already designed in. Where your model leaves room, we can flag obvious over-thickness as DFM feedback.
Billet vs forging vs casting
Billet (plate or bar) suits low volume and short lead times with homogeneous properties. Forging improves grain flow for load-bearing parts but adds tooling lead time and a minimum quantity. Casting gets close to net shape for complex geometry and is economical at higher volume, with porosity and dimensional variation to manage. The right start point depends on quantity, load path and how near-net the geometry allows.
Drawing to finished part
From Your Drawing to an Inspected Component
Every order follows the same route, so you always know where a part is and what has been checked. Nothing moves to production until the first article is confirmed against the print.
-
Drawing & requirement review
We read the drawing and model, confirm material and grade, and return DFM notes on features that are hard to machine or tighter than they need to be.
-
Material sourcing & certification
Stock is ordered to the specified grade and condition, with the mill certificate retained against the order for traceability.
-
Process planning & programming
The route is set — 3-, 4- or 5-axis milling, turning, EDM — and CAM programs and fixtures are prepared for the chosen stock.
-
First-article machining
A first article is machined and can be supplied as a sample for approval before the production run begins. This is also where our custom CNC prototype service fits.
-
Inspection & first-article report
Critical features are measured against the drawing and a first-article report is issued on request, prepared to AS9102 where required.
-
Production machining
The approved process runs to the same programs and fixtures, with in-process checks to catch drift before it becomes scrap.
-
Finishing & final inspection
Any specified finishing is applied, then final inspection and documentation are completed against the order.
-
Packing & delivery
Parts are protected individually where needed and packed to avoid transit damage, with the document pack issued alongside.
Processes & finishing
Machining and Finishing Options
Machining and finishing are chosen from the drawing. If a callout needs a third-party-approved special process, we confirm the source before quoting rather than assuming it.
CNC Milling
3-, 4- and 5-axis milling for pockets, contours, faces and complex geometry. CNC machining services.
CNC Turning
Precision turned shafts, bushings, fittings and spacers with controlled diameters and finishes. CNC turning services.
EDM
Wire and sinker EDM for sharp internal corners, fine slots and features a cutter cannot reach. EDM machining services.
Drilling & Threading
Standard and non-standard hole patterns, tapped holes and threaded ports verified with gauges where specified.
Passivation
Passivation for stainless steel parts to clean the surface and support corrosion resistance. Passivation for stainless steel.
Anodizing & Coatings
Anodizing, conversion coating and plating applied per the drawing. Where a coating is a third-party special process, we confirm the approved source before quoting.
Inspection
Critical Features We Inspect
Inspection is planned from the drawing, not bolted on at the end. Which features get measured, and to what level, is agreed at quoting so the report matches what your own receiving inspection will check.
Dimensional accuracy
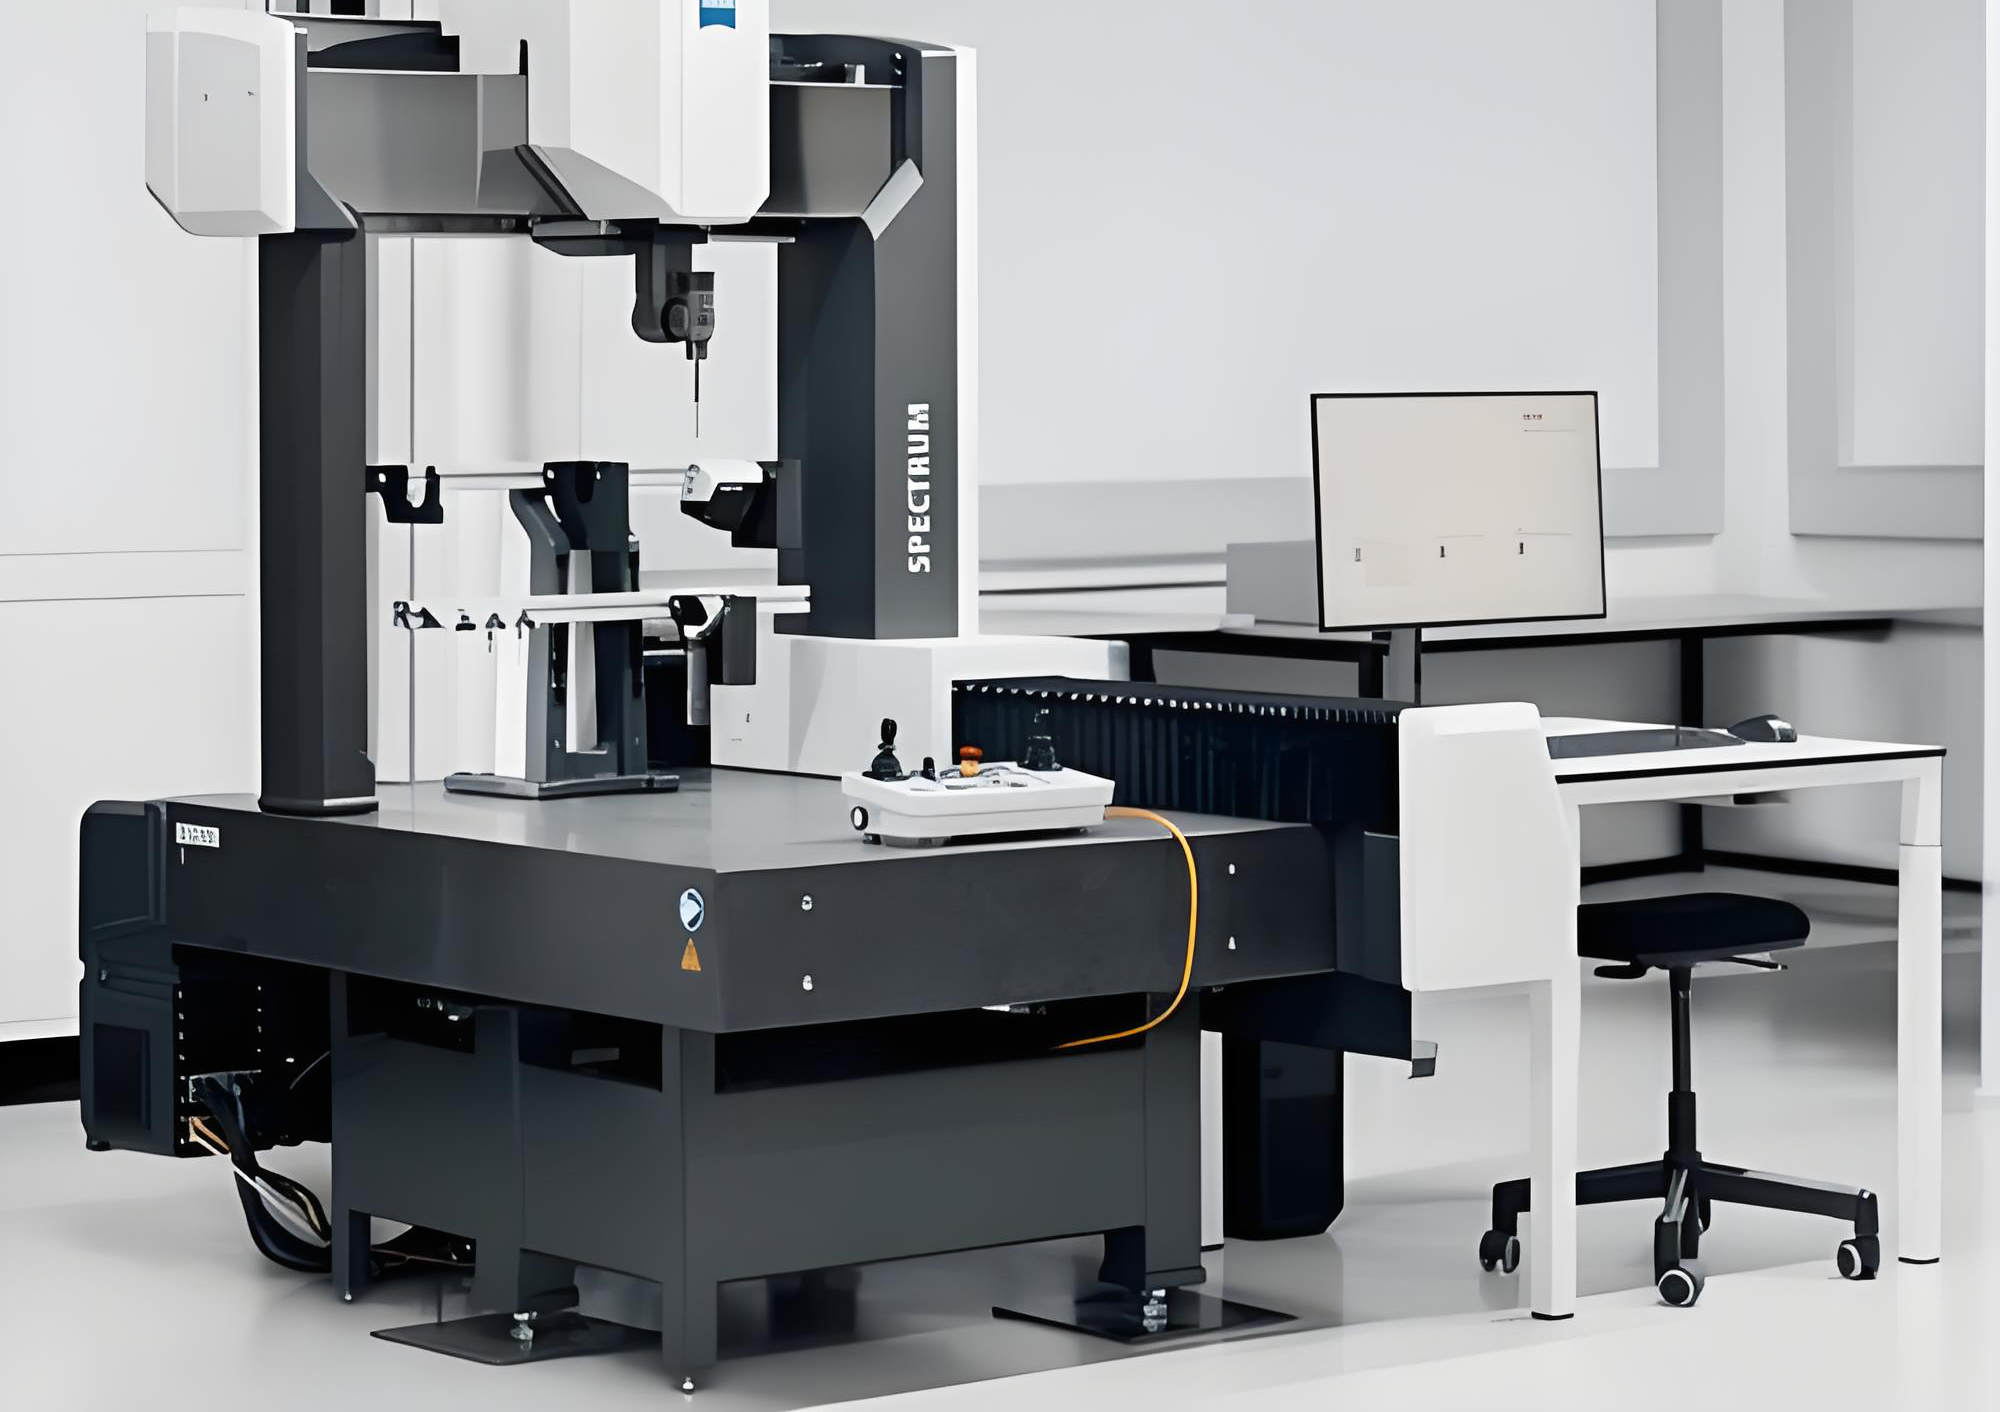
Caliper, micrometer and CMM measurement of the dimensions called out as critical on the drawing.
GD&T verification
Form, position and orientation tolerances checked against the stated datums where the drawing applies them.
Surface finish
Ra on sealing faces, bearing seats and other finished surfaces, verified against the finish callout.
Threads & holes
Thread form and pitch checked with gauges; hole size and position confirmed against the pattern.
Material & hardness
Mill certificates retained against the lot, with hardness verification where the drawing specifies a condition.
Visual & cosmetic
Deburring, edge break, marks, scratches and transit protection checked against the agreed standard.
Quality documentation
What Can Travel With the Parts
Documentation is agreed at quoting. Tell us the package your quality or receiving department needs — material traceability, dimensional records, conformance, or first-article inspection — and we build it into the order rather than adding it afterwards.
Our quality system is ISO 9001:2015 certified, and we operate AS9100-aligned process controls. We are deliberately precise about what that means: alignment is not certification. Where a drawing requires a third-party-approved special process, we confirm the approved source before quoting.
Documents available on request
- Mill / material certificates matched to the production lot
- Dimensional inspection reports for the agreed critical features
- First-article inspection reports, prepared to AS9102 where required
- Certificates of conformance
- Hardness and surface-finish records where specified
- Packing list and document pack issued with the shipment
Scope note: we manufacture to your drawing and do not hold design authority or airworthiness approval. Conformity and airworthiness certification remain with the customer or OEM. See also what certifications a CNC supplier should have.
How an order runs
A Representative Component Example
Machined aluminum mounting bracket — drawing to inspected batch
A customer supplied a 2D print and STEP model for a pocketed mounting bracket. We reviewed tool access and fillet radii, machined a first article from 6061-T6 aluminum, issued a dimensional report for the critical features, and after approval ran the production batch on the same programs and fixtures.
This is a representative example that describes a typical order, not a named customer case. We do not publish client-identifying work, drawings or data without permission, so we show the process rather than invent a quotation of results.
Understanding cost
What Drives the Cost of an Aircraft Component
We do not publish a price list, because two identical-looking brackets can cost very different amounts. These are the factors that move a quote, and the ones worth optimising before you send the drawing.
Material & grade
Titanium and nickel alloys cost more per kilogram, machine more slowly and wear tools faster than aluminum.
Geometry complexity
Deep pockets, thin walls and multi-face features add setups, programming time and risk.
Tolerance & finish
Tight tolerances and fine finishes need more passes, slower feed and more inspection.
Quantity
Setup and programming are paid once, so unit cost falls as quantity rises — up to the point a different stock form wins.
Inspection level
A full first-article report and CMM verification cost more than a basic dimensional check.
Finishing & special processes
Anodizing, plating and any third-party special process add lead time and an external step.
FAQ
Custom Aircraft Precision Components — FAQ
Which aircraft components can you machine?
Do you work from our drawings, or can you help with design?
What materials can you machine for aircraft components?
What tolerances can you hold?
How do we start — what do you need to quote?
How is this different from your aerospace CNC machining service?
Can you supply material certificates and inspection reports?
Do you hold AS9100 or airworthiness approvals?
What is the typical lead time?
Can you handle complex geometry or tight features?
Request an Aircraft Component Review
Send your drawing or 3D model and we will confirm material, process route, tolerances and documentation — and return DFM notes with the quote.
Related capabilities
Continue Exploring
Aerospace CNC Machining
Our aerospace machining service overview and process controls.
5-Axis CNC Machining Services
Simultaneous five-axis capability for complex geometry.
CNC Machining Services
Milling, drilling and the broader machining service.
CNC Turning Services
Precision turned shafts, bushings and fittings.
Custom CNC Prototype Parts
First articles and prototypes before a production run.
Passivation for Stainless Steel
Surface cleaning to support corrosion resistance.